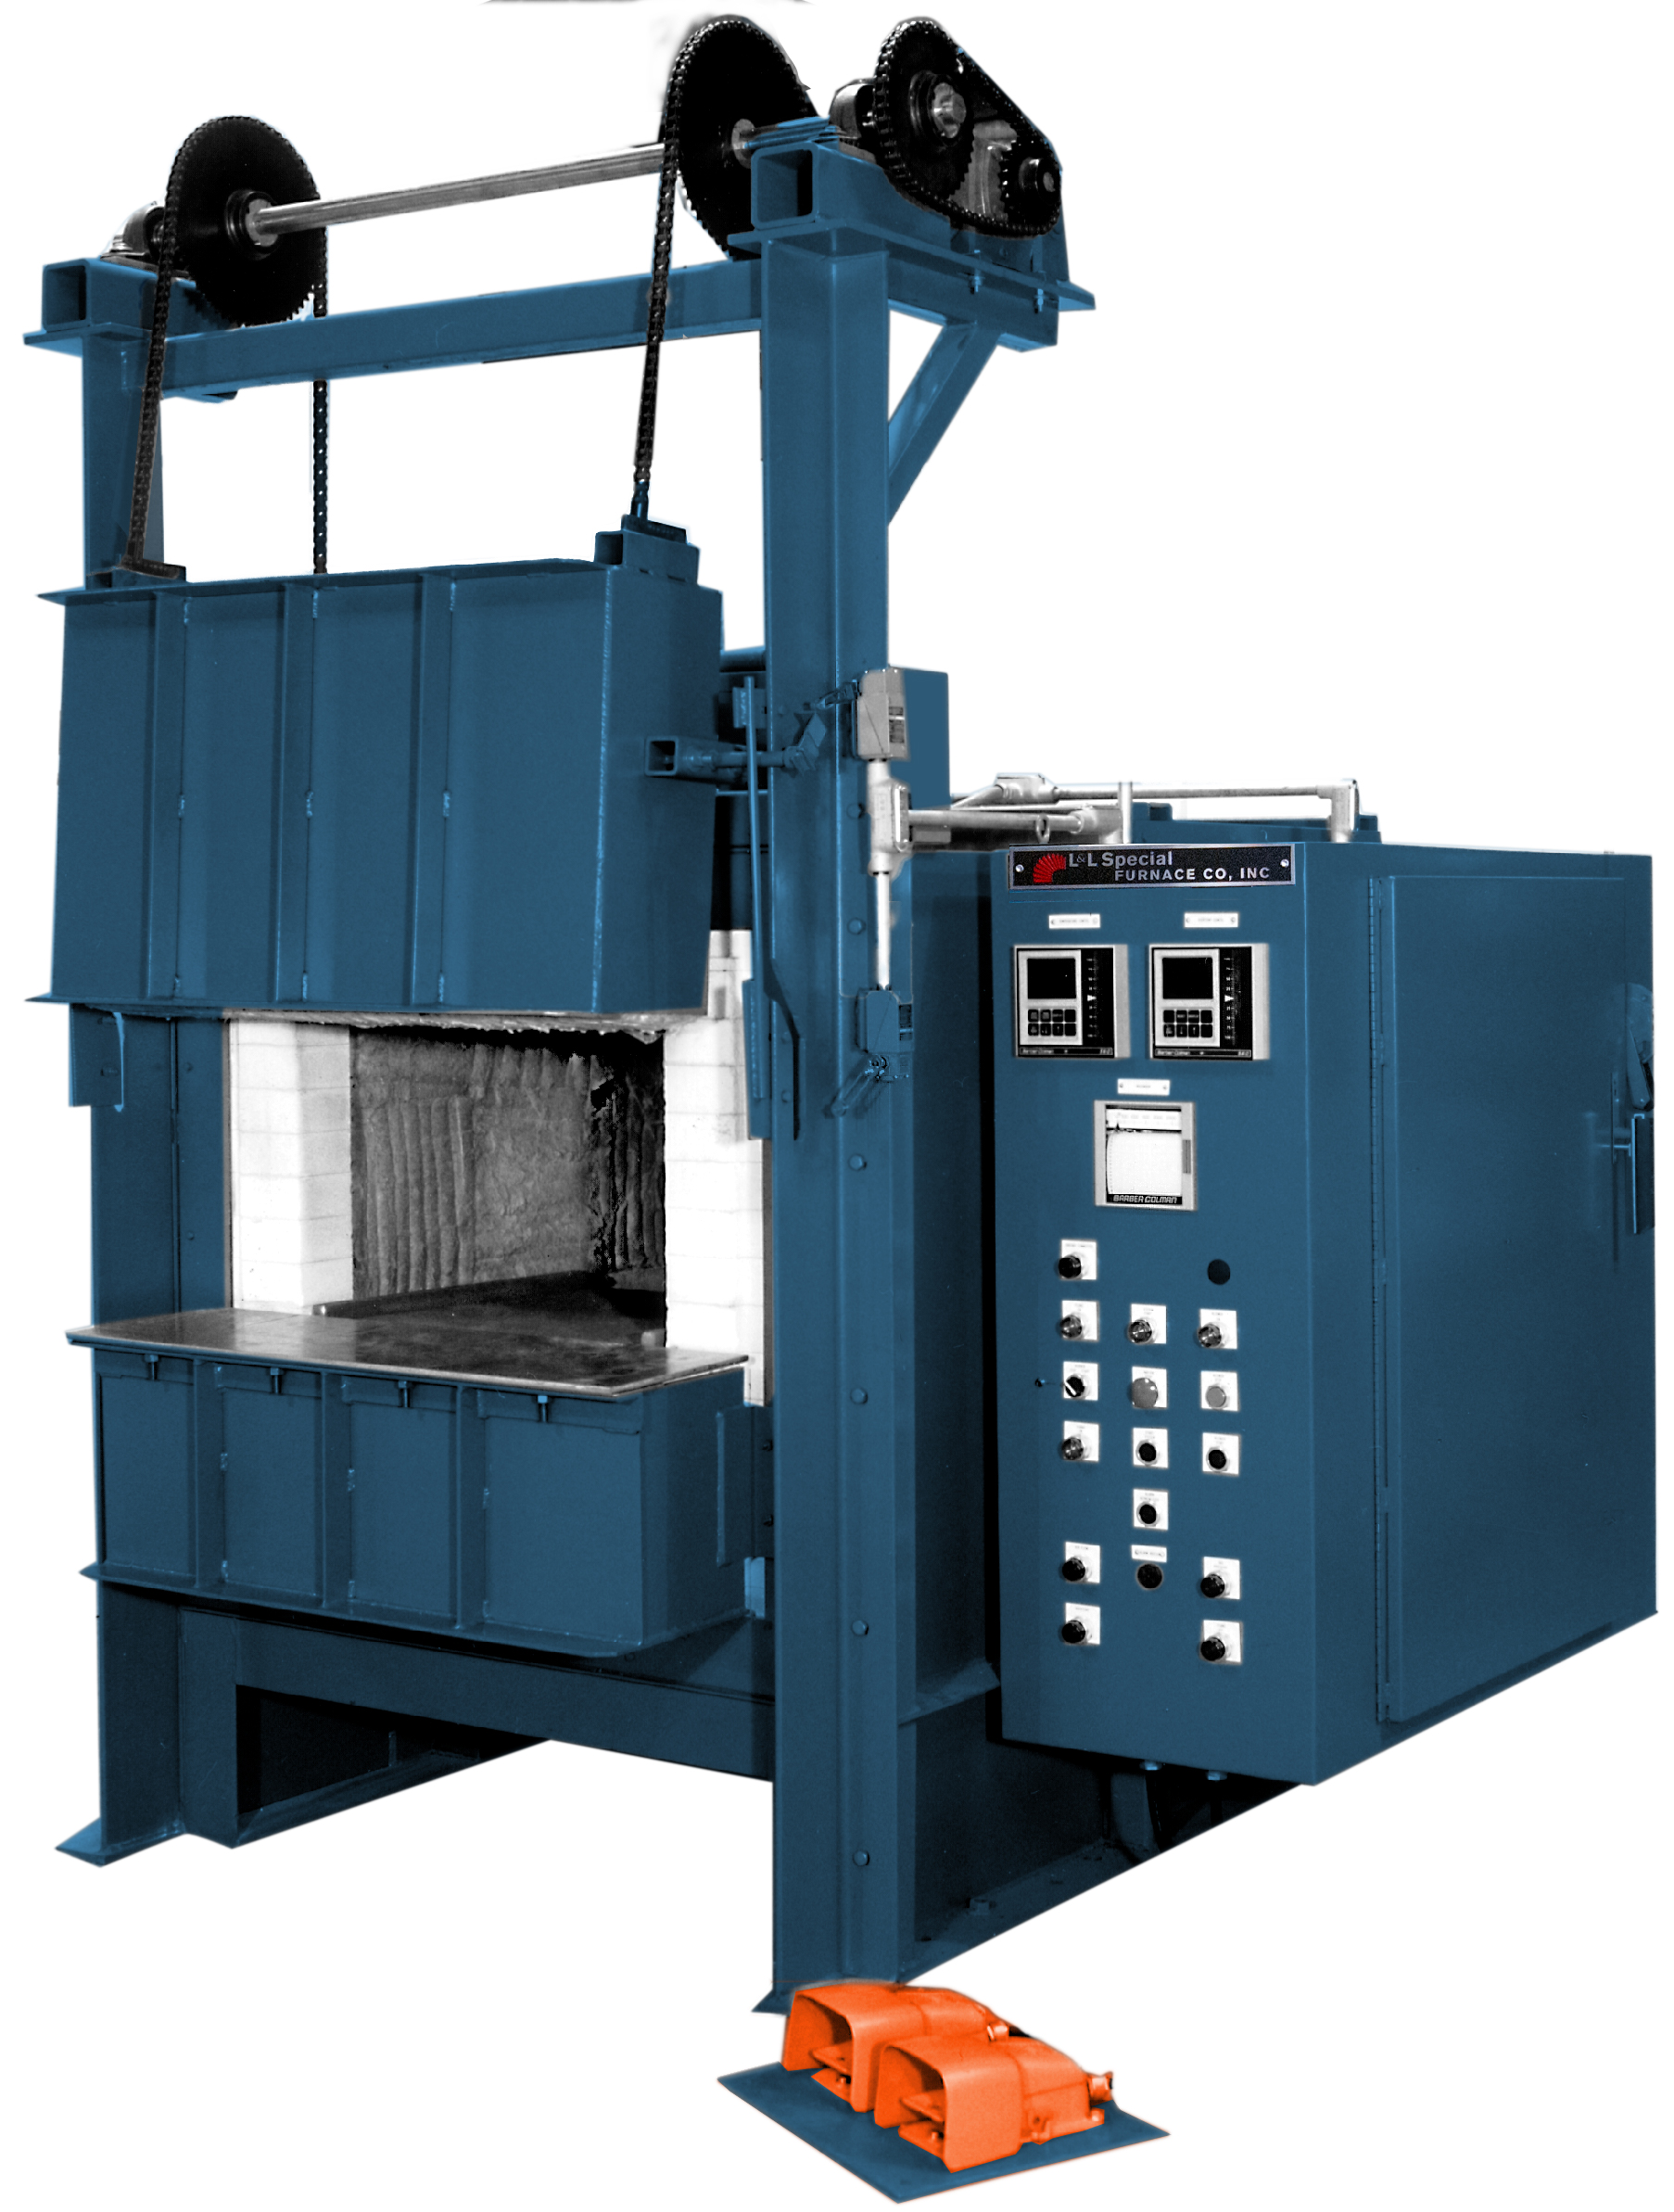
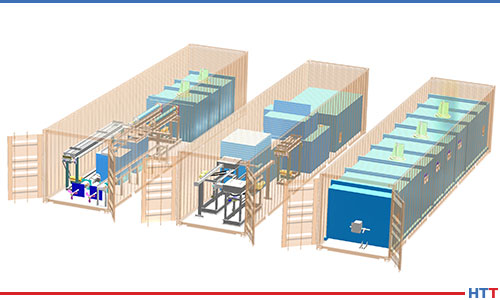
A furnace manufacturer based in Pennsylvania, USA, has shipped a floor standing forging furnace for use in hot forming of medical implant parts along with a floor standing tempering furnace to a manufacturer of medical implant components located in the Northeastern United States.
The FWE422 forging furnace
The forging furnace is a L&L Special Furnace Co., Inc. model FWE422 with working dimensions of 48” wide by 24” high by 24” deep and heats to a temperature of 1,800°F. The furnace features a vertical door with adjustable stops. These stops allow the door to be stopped at a predetermined location during the heating process for minimal heat loss.
The tempering furnace is model XLE3636 with a vertical door and 12” diameter, air-cooled convection fan and roller hearth. It has an effective work zone of 34” wide by 30” high by 32” deep. The furnace is used to temper hot formed parts and other thermal processing duties.
ITW Company Buehler recently celebrated the 100-year anniversary of its Wilson® hardness brand, which was originally known as the Wilson Mechanical Instrument Company. Stanley Rockwell and founder Charles H. Wilson introduced the Rockwell hardness tester. Later, Wilson became the home of the Tukon line of micro-indentation testers, known for Knoop and Vickers testing. These early inventions paved the way for Wilson today.
Buehler is proud to commemorate and celebrate the legacy of the Wilson name. Buehler’s affiliation with Wilson began in 2012 when the Wilson® brand of hardness testers encompassing Reicherter, Wilson, and Wolpert products became part of Buehler’s offering.
Julien Noel, General Manager, Buehler
According to Buehler General Manager, Julien Noel, “We are proud to continue the 100-year legacy of innovation and excellence in Wilson Hardness. By having our engineering, manufacturing, and service in-house, Buehler’s Wilson products have become the preferred choice for demanding labs that need to consistently meet quality standards. In the coming year, Buehler will continue to focus on exceeding customer expectations with a new and improved Rockwell tester, and an extended range of hardness reference blocks according to ISO, ASTM and JIS standards.”
Come visit the 31st AeroMat conference and exposition! AeroMat is the premier event for aerospace materials and applications for the global industry. Over 700 attendees will be on hand to learn about your company’s latest advances.
AeroMat still holds up as the annual forum that showcases the interchange of pertinent technical information on aerospace industry material and processes. With over 150 technical presentations, come hear plenary speakers featuring the aerospace industry’s most pre-eminent leaders in aerospace materials and take part in a diverse exposition.
This HTT Technical Tuesday feature originally appeared in heat processing, a Vulkan-Verlag GmbH publication that serves mostly the European and Asian heat treat markets and with whom we are partneringto share the latest news, tech tips, and cutting-edge articles that will serve our audience – manufacturers with in-house heat treat.
Carsten Stölting CEO Aichelin Service GmbH
In this article, Carsten Stölting, CEO of Aichelin Service GmbH, explores bringing maintenance systems into the digital era with a digital assistance system for thermal processing plants.
"To this day, the maintenance of heat treatment plants is characterized mostly by manual work; very few digital tools exist for information display, plant support, data acquisition, or data collection. This means that, in this field, only very few of the possible advantages of digitization are being used. Mobile maintenance assistants are thus a real opportunity to support maintenance departments in their daily work. They also increase the potential for cost savings due to their better efficiency and the fact that they reduce down times. This article provides a general overview of the status quo. Moreover, #jakob\safe.sound, a novel mobile assistance system for thermal processing plants is presented."
In general, it has become clear over the course of recent years that manufacturing companies see maintenance no longer as a mere cost factor and a necessary evil, but have rather come to recognize it as a real value-adding factor for their production. Many production managers know about the relevance of a well-functioning maintenance system for the economic success of their production. And yet, maintenance as a non-direct profit earner remains under great pressure from cost savings. Saying that well-functioning maintenance guarantees efficient and successful production while at the same time being under pressure due to cost factors in fact demonstrates two diametrically opposed assumptions. This should create an ideal environment for innovative solutions and approaches. Regrettably though, especially in the heat treatment industry, this trend towards innovation has not quite been acknowledged.
Even companies with a strong maintenance strategy lack method to take their maintenance system into the digital era to increase their cost saving potential and efficiency gains. This may in part be due to the installed base of the plants, which are often 10, 15, 25 years old, sometimes even older. Production plants with such an advanced age easily suggest that there is only very little to no valid digital data such as sketches, parts lists, sensor readings, etc. Which in turn suggests that digital assistant systems cannot be used. The much-lauded digital twin seems like a distant dream in such cases.
Yet maintenance should have special significance for the heat treatment industry and should inspire the development of extensive assistance systems. There is, for instance, the factor of plant safety. Few other production plants emanate similarly high-risk potential. The constant risk of fire, deflagration, and explosion and even the leakage of poisonous gases – all are potential hazards that can occur due to false or incorrect maintenance of heat treatment plants. But also, from a purely financial point of view, maintenance of heat treatment plants is of importance. Unlike with most conventional production facilities, cases of damage of a relatively simple component can lead to considerable and unplanned down times. Depending on mounting position inside the furnace, a simple exchange that takes only two hours can lead to a down time of several days or, in larger plants, even up to a week or two, despite direct availability of the spare part. As the plant must cool down, two to three days may pass (in some cases even considerably more) until the part becomes accessible. The controlled heating, the setting of the furnace atmosphere and the retraction of the plant then takes another four to five days. Hence, the more information and support the maintenance staff can get, the better will they be able to service the plant, the more efficient will they be able to operate. Unplanned down times and production interruptions can thus be avoided or at least shortened considerably.
ASSISTANCE SYSTEMS IN GENERAL (CMMS SYSTEMS)
The market offers many so-called CMMS systems (Computerized Maintenance Management Systems). Different producers often have different industry focus. However, all systems share the fact that they come without application, meaning without being set up for one specific plant. This means that the systems do not usually have any plant-specific content and are thus empty. The user must feed the systems with plant-specific information first. But this type of information is not usually available, or if yes, it is only rudimentary. Descriptive documents and the occasional spare parts lists are often available, usually in pdf format. More in-depth, plant-specific information such as plant structures, extensive parts lists, wear data, specific maintenance instructions or maintenance plans are usually missing. Moreover, clear SPS data from the existing plant that is also relevant for maintenance is often not accessible or not integrable. Feeding these systems thus becomes a monumental, almost impossible task for the respective department. Furthermore, many of the systems on the market are often very extensive, almost like ERP systems. While this does offer multiple evaluation and controlling options, it also complicates applications during the operation of a plant. This may be because these systems are described as Computerized Maintenance Management Systems. The root and focus lie within the management of maintenance, but not primarily in its implementation. This focus has only evolved over recent years with the emergence of mobile IT.
File input is usually via PC, meaning that anything operated on the machine directly must be saved temporarily (usually the analog way with an infamous handwritten slip) and then entered into the PC afterwards. Often this means double the work, leading to very poor acceptance of the systems by the maintenance staff. Another aspect that maintenance staff often note is that the basic needs for the maintenance of the plant are not met by the systems, while numerous reporting and analysis functions do exist.
Digital Assistance System for the Industry
The challenges mentioned above have multiple causes. Providers of CMMS systems do not have the necessary knowledge and information on the plants to configure their systems accordingly. The users, too, do not have, or have only a limited amount of data such as documents, parts information or access to SPS information. Up to now, the plant manufacturer was not a necessary stakeholder in the set-up of such systems. Which is why, in June 2018, a joint project was launched, consisting of a software manufacturer (Humai Technologies GesmbH from Vienna, Austria), a plant manufacturer (Aichelin GesmbH from Mödling, Austria), an industrial maintenance and service provider for heat treatment plants (Aichelin Service GmbH from Ludwigsburg, Germany), and two production companies in the automobile industry (a Bavarian tractor manufacturer with a large pusher-type furnace and an Upper-Austrian automobile supplier with three large pusher-type furnaces). It is a collaboration between companies, supported by the Austrian Berndorf AG and brought together under one roof. The objective is to develop a mobile assistance system for the maintenance of heat treatment plants. Particular attention shall be paid to finding a solution that
is manufacturer-independent (multiple plant manufacturers
can be integrated into existing plants
does not require high additional installation effort for sensors
enables the operating maintenance staff to use existing devices (i.e. mobile phone, tablet) to run the application directly at the plant
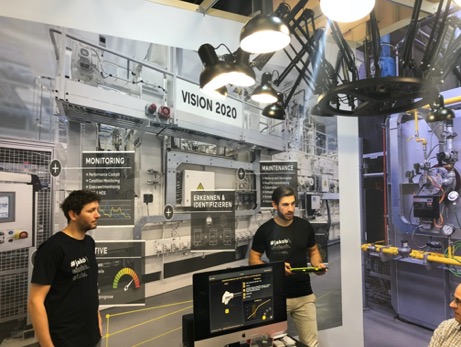
Figure 1. Presentation of the first prototype at the Heat Treatment Congress 2018
The interdisciplinary team had discussions about the technical possibilities for this endeavor. Just in time for the Heat Treatment Congress in Cologne in October 2018, we were able to deliver a live presentation of a first prototype to a selected expert audience (Fig. 1). The aim was to receive comprehensive feedback from users and experts about the focus of the project and integrate accordingly. The feedback turned out very positive and confirmed our basic assumptions and approaches. The maintenance assistant, called #jakob/safe.sound, should simply provide operative maintenance staff with a maximum of all existing information and it should be simple to handle. “All information” means the manifold data from different sources, such as: item master data and multi-level bills from ERP systems, construction data of the plants, the entire plant documentation and the most recent maintenance and set-up protocols. Moreover, edited monitoring data of relevant SPS data such as power consumption, positioning times, temperature curves, set-up parameters etc. should be made available to the maintenance staff in the simplest manner possible. The objective of maximum security/reliability means that the maintenance staff, but also the operator of the plants are guaranteed the secure knowledge of the status quo of their plant and whether there is a risk of unplanned down times.
With this requirement, #jakob was divided into the following main areas and functions. It is used to support the user in:
Identifying components (object recognition)
Spare parts supply/spare parts management
Maintaining and servicing/information procurement
Monitoring the state of the plant
Predictive maintenance
OBJECT RECOGNITION
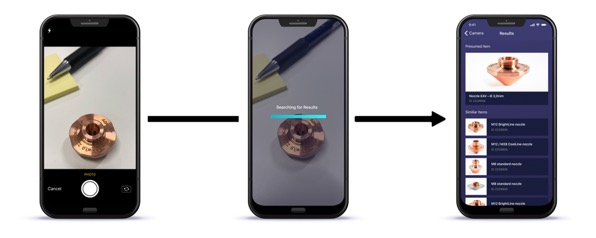
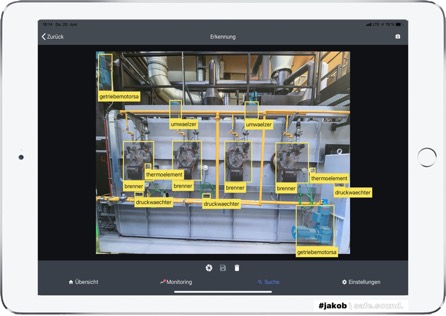
Figure 2. Existing technical solutions for component recognition [Source: Humai Technologies]The project team is convinced that the key to success lies in the simplicity of operating the system by using innovative technologies. A conscious decision was made to forge new paths with technology, while remaining down to earth at the same time. Existing solutions for the identification of spare parts or components in mechanical engineering companies from Germany (2017) are primarily based on RFID, bar code, and QR code technologies. Fig. 2 shows that this is only successful in 50 % of the cases, as existing applications such as RFID, bar code, and QR code often do not work in environments with heat, dirt or wear and tear, or for various other reasons. It was also consciously decided not to focus on prestigious eyecatchers such as Augmented Reality Data glasses (Google Glass or Microsoft Hololens), due to two essential reasons: one, the digital maintenance assistance should be easily available and always at hand for all maintenance staff. This could not be guaranteed with expensive and sensitive data glasses. However, almost everyone these days carries a mobile device such as smart phones or tablet computers, regardless of whether running on Android or Apple iOS. (Fig. 3)
Figure 3. Object recognition with standard mobile devices
Moreover, data glasses require perfect data structures (i. e. 3D models of the plants and parts), which has yet to become a standard even in newly built plants in the thermal processing industry. It was decided that the approach would be to only rely on existing data and information in order to equip as many plants as possible – even older ones – with the maintenance assistant and thus be able to provide significant support for the entire hardening industry. In this respect, it can be said that the assistant supports all maintenance staff as a personal assistant and a colleague who is always available.
OBJECT AND SPARE PART RECOGNITION
Figure 4. Example of component identification with AI detection
The assistant breaks new ground in the field of spare parts recognition. Via AI-App on your smart phone, parts and components can be scanned and identified within only a few seconds. The automatic recognition of spare parts saves employees a lot of time. In 2017, it was shown that it takes experts approximately 12 min to find the right spare part in the various documents and systems. The time for such a search will continue to increase in the future, as plants are growing more and more complex and employees are less experienced. The reliable identification of parts paves the way for more information on them. How many times is this specific part installed, what is its article number, how much does it cost, what is the delivery time? The connection with information from procurement history, date of installation and expected mean risk of malfunction provides every part with a résumé (Fig. 4). In a last step, the selected spare/wear part can be placed in a shopping cart for a quotation request.
MAINTENANCE PLANNING AND IMPLEMENTATION/INFORMATION PROCUREMENT
Maintenance staff receive all relevant data and settings of the detected parts and components at the tap of a screen. Questions such as: How do I service a power unit? When was it last done? How do I set up a part correctly? – are all detected by semantic search algorithms from the existing sources of information and then processed. This means that the maintenance staff have all the answers available right from the start, directly at the plant thus offering support for seasoned and experienced staff just as well as for neophytes. Moreover, step by step, the work is made available analogically with the manufacturer-specific service plans and guarantees that no relevant steps or parts are overlooked. At the same time, status assessments can be made for down time – critical parts, which enable predictions of malfunctions and their proactive prevention.
MONITORING
The permanent monitoring of critical areas of the plant is to prevent unplanned down times. Down time-critical components are, if possible, monitored with existing sensors. Component monitoring was realized in the most recent version of Focos 4.0, the process data recording system developed by Aichelin. For the past three years, this software has been installed dozens of times and relies on existing sensors in the plant, thus enabling the use of existing systems and making their data/information accessible. The clearly prepared monitoring data are then compared to expert knowledge and recommendations for action to the users can be derived from that. Moreover, the data is also saved for further use in the course of the Predictive Maintenance Module planned for the future.
PREDICTIVE MAINTENANCE
The most important objective of this development project is to offer a so-called Predictive Maintenance Solution to customers. By means of the numerous sources of information from maintenance intervals, status assessments, sensor data, and also indirect process data and the underlying algorithms, it will be possible to issue warnings and tips even before the malfunction of a part. For this purpose, we have been working with our cooperation partner, the Fraunhofer Austria Research GmbH, to develop methods to receive reliable predictive status assessments. Especially in the hardening and heat treatment industry, the key to success does not lie with the numerous sensors, which are not even built into existing, pre-installed plants, and for which the retrofitting would render any ROI approach pointless. The focus instead is placed on acquiring data indirectly, if possible, and with as few sensors as possible. In combining and integrating diverse information available on the existing plant, it will be possible to make accurate down time and status predictions and thus forecast predictive maintenance tasks.
PROFITABILITY ASSESSMENT
As mentioned above, one of the main objectives of the project is to establish a digital maintenance assistant not only for new plants, but for the much more numerous existing plants in the heat treatment industry. Aside from the mentioned challenge regarding master data, this also sets significant requirements for profitability. It goes without saying that the mentioned functions cannot be simply implemented using only a minimal effort. While it is relatively easy and comes with only low additional cost to provide and integrate all necessary data sources, it also comes with considerable effort for existing plants. To reduce this effort down to a degree, where the installation of such a system pays off within one year, is the challenge the project team is facing. The key lies in the consistent use and smart connection of all existing data sources, rather than in the creation of new data and the installation of additional hardware.
However, the first pilot applications already show clearly that the use of such a mobile assistant that is available 24/7 creates considerable added value in terms of cost and quality for both the maintenance staff and the plant operator. Specifically, this means:
Time for spare part identification is drastically reduced
Incorrect orders and deliveries can be avoided
More efficient information retrieval and more concrete, immediate, and faster support through “smart” access to all available information from handbooks, lists, sketches, etc.
Reduction of incorrect settings on the plant
Reduction of energy consumption due to enhanced plant settings
Significant reduction of cost of unplanned plant down times
These experiences have convinced the current project team to continue onwards with this assistant and thus be able to offer maintenance staff in the heat treatment industry important support in their daily work.
About the Author: Carsten Stölting is CEO of Aichelin Service GmbH in Ludwigsburg, Germany. He has been with Aichelin and furnace manufacturing for 8 years.
STALMAX, a manufacturer of fasteners, is investing in a belt furnace for tempering in a protective atmosphere. The provided equipment is designed for hardening fasteners, such as bolts and nuts, intended for the automotive industry. The main element of the line is a belt furnace equipped with a muffle, in which the heat process is conducted in a protective endothermic atmosphere.
The applied design solutions allow for a high evenness of temperature uniformity to be achieved. The automated process of the work of the ATG processing line by SECO/WARWICK, equipped with a weighing system, enables a precise loading of the treated elements on the hardening furnace belt.
STALMAX vice president, Robert Jeż, says, “SECO/WARWICK with their solutions answers real manufacturing needs, and ATG-type line is a guaranteed fulfillment of the industry’s and the clients’ requirements. The partner has not only offered an excellent furnace, but also protected us in case of an unwanted failure. In accordance with individual needs, components of element coding have been introduced and are connected to the alarm base (PLC) and electric documentation of the control system. Such a solution allows to immediately identify the failure and the damaged element.”
Dr. Randall (Rand) German, FAPMI, founder of German Materials Technology, will receive the Kempton H. Roll Powder Metallurgy (PM) Lifetime Achievement Award by the Metal Powder Industries Federation (MPIF). The award will be presented during WorldPM2020, World Congress on Powder Metallurgy & Particulate Materials, in Montreal, Canada, on June 28.
German has distinguished himself through his research and teaching of the net-shape fabrication of engineering materials via sintering techniques as used in PM, cemented carbides, and ceramics. He has promoted the growth of PM technology during his 50-year career through his involvement in 12 start-up companies, supervising well over a hundred graduate and post-doctoral students, and prolific PM industry publications. German has also been an active member in APMI International, the American Society for Metals, and the American Ceramics Society.
After completing his bachelor’s degree in material science and engineering at San José State University, German began his PM industry career at Battelle Lab, Columbus, Ohio, prior to joining Sandia National Labs (SNL). He obtained his master’s degree in metallurgical engineering from The Ohio State University and his PhD in engineering at the University of California—Davis before taking a director of research position at Mott Corporation, Farmington, Connecticut.
Dr. Randall German Founder, German Materials Technology
German’s nearly 40-year academic career began in 1980 at Rensselaer Polytechnic Institute (RPI), where he earned the HuntChair while teaching and conducting research. In 1991, he accepted a position at The Pennsylvania State University where he became the Brush Chair Professor in Materials and the director of the Center for Innovative Sintered Products (CISP) before retiring as an emeritus professor. In 2005, German became the inaugural director for the Center for Advanced Vehicular Systems (CAVS) at Mississippi State University prior to joining San Diego State University in 2008 as associate dean for engineering research until 2013.
German has published 20 books and has 25 patents. He has shared his expertise at powder injection molding tutorials since 1990, and co-chaired over 30 conferences.
Joby Aviation has spent the last 10 years hammering out the designs and flight dynamics of its tilt-rotor eVTOL (electric vertical take-off and landing) aircraft . Thanks to an investment round led by Toyota, they now have substantial funding to continue development.
Toyota's share of the US$590 million series C finance round was $394 million, and it comes with a commitment to bring its manufacturing, quality, and cost control approaches to the table as Joby prepares to move closer to FAA certification and commercialization of its five-seat electric VTOL air taxis.
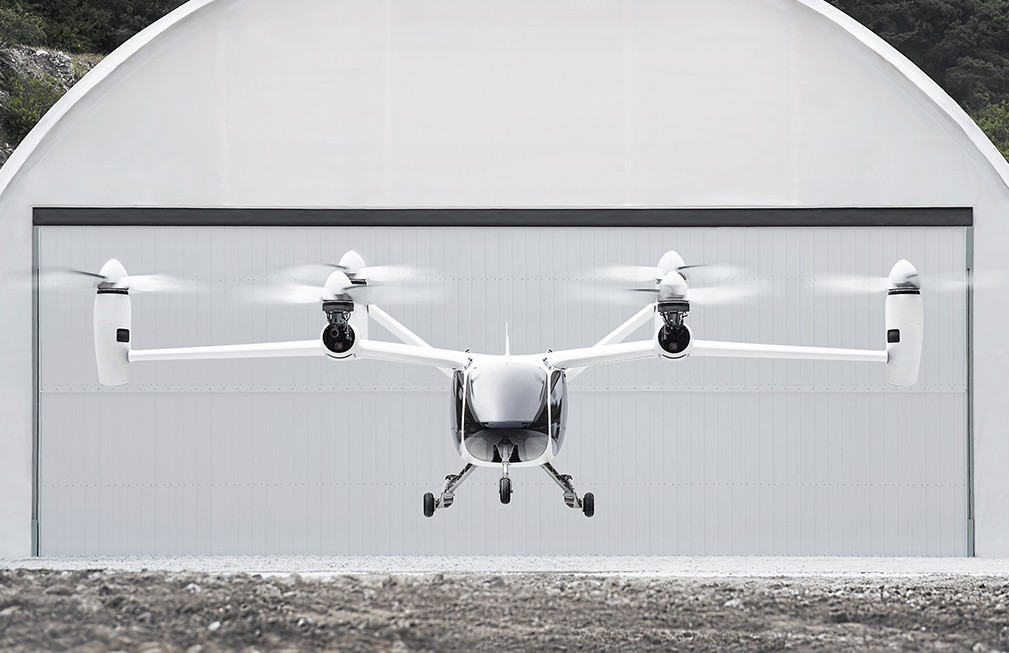
Joby's full-scale prototype features thin wings supporting four tilting prop units, the outer ones on swivel mounts and the inner two extending out and upward on short arms. A V-shaped tail unit carries two more swivel units for a total of six rotors, each about six feet (1.8 m) in diameter with five uniquely shaped blades.
The idea is to have an electric aircraft capable of taking off and landing vertically on a helipad or similar that can then transition to winged forward flight once it's airborne for efficient cruising at high speeds. Joby claims its vehicle is capable of 200-mph (322-km/h) flight, and that its small rotors produce about 1 percent of the noise of a regular aircraft on takeoff. In winged cruise mode, the company says it will be virtually silent on the ground.
With six tilting rotors, Joby's eVTOL can do 200 mph, with a range of more than 150 miles per charge (credit: Joby Aviation)
Toyota may also bring hydrogen powertrain to the table. Toyota and Hyundai/Kia are more or less the only companies still forging ahead with hydrogen powertrains for cars, but Japan and Korea are investing in hydrogen in a massive way, envisioning a transport future largely running on fuel cells, using imported energy from overseas to move some of their emissions out of their choked megacities and into the skies of countries like Australia, which is gearing up to become an energy exporter in the form of liquid hydrogen.
Moving to a hydrogen powertrain solves the problem of energy density for eVTOLs in a single stroke. Liquid hydrogen might be a pain to handle and deal with (and explosive in an accident), but its energy density is superb. Running a hydrogen eVTOL air taxi service would enable super-quick refueling and ultra-long-range flight, maybe 10 times the range of what current battery technology can deliver.
A common topic regarding eVTOL is safety, a problem that still needs an answer. The Joby aircraft, like the vast majority of other designs, offers a certain degree of redundancy in case of rotor failures. The problem nobody seems to be able to deal with yet is what happens in case of total catastrophic failure below a height of about 120 ft (37 m). Ballistic parachutes remain troubling, and while helicopters have the ability to autorotate safely to land without power, multirotor eVTOLs do not.
Joby is right at the forefront of eVTOL development right now, alongside other well-funded companies. It has recently signed a deal with Uber to supply and operate these aircraft under an Uber Elevate service. Uber is promising to build and run the skyports and support services for these air taxis as well as managing last-mile connection transport at either end of a journey. Uber is targeting 2023 as a launch date.
Scientists from the Alliance for the Development of Additive Processing Technologies (ADAPT) at Colorado School of Mines who took part in an international research team have helped develop a nickel-titanium elastocaloric cooling shape memory alloy (SMA) that is highly efficient, eco-friendly, and easily scaled up. The alloys, in which hafnium acts as a strengthening precipitate, hold the promise of requiring only heat treatment to attain functional shape memory performance.
The international team, led by University of Maryland Professor Ichiro Takeuchi, developed the improved elastocaloric cooling material using a blend of nickel and titanium metals, fabricated by a 3D printer, that is not only potentially more efficient than current technology, but is completely “green.” Moreover, it can be quickly scaled for use in larger devices.
Dr. Aaron Stebner, Rowlinson Associate Professor of Mechanical Engineering
“The key finding of the research is that while elastocaloric materials typically used for solid-state cooling show a degradation in cooling behavior after hundreds of cycles, laser melting these metals creates fatigue-resistant nanocomposite microstructures that can cycle, with consistent cooling capacity, a million times,” said Aaron Stebner, Rowlinson Associate Professor of Mechanical Engineering and a co-author of the paper.
Professor Ichiro Takeuchi, Graduate Program Director in Materials Science and Engineering, University of Maryland
“Dr. Stebner’s expertise played a crucial role in developing understanding of the fundamental mechanism behind fatigue-resistant behavior of additively manufactured shape memory alloys. His group’s in situ synchrotron diffraction and finite element modeling capabilities gave us unique insight into the inner workings of the material,” Prof. Takeuchi said.
The work, which was published in the Nov. 29 issue of Science, is the result of a collaboration led by researchers from the University of Maryland, together with Ames Laboratory, Mines, Iowa State University, and China’s Xi’an Jiaotong University.
Automotive part designs and heat treating processes have undergone many changes over the years, especially the powertrain. By looking back at the progress of these changes, we can learn more about emerging trends in automotive heat treating today.
In this Heat Treat Today Technical Tuesday feature,Bill Disler, president and CEO of AFC-Holcroft, brings his familiarity with big atmosphere carburizing systems and LPC automotive cell carburizing systems and looks at how the evolution of equipment and process requests says a lot about the trends we see today in automotive heat treating.
Although many components undergo heat treatment processes, the powertrain—specifically, gears— typically requires more carburizing time than other automotive parts. Not surprisingly, the powertrain has also seen many changes in heat treatment trends.
Not only have powertrain designs gone through tremendous transformations but so has the equipment being used to process those evolved components. Having spent years on the supplier side of atmosphere furnaces, vacuum carburizing, and gas quench as well as induction systems, I find it interesting to look back at some of the drivers that have helped morph this industry’s heat treat needs.
Traditional Continuous Atmosphere Furnace
Large atmosphere pusher furnaces produced nearly all of the powertrain gears 20+ years ago. Today, cellular low-pressure carburizing (LPC) and gas quench systems carry the load, although the results have not been cost saving. Moving from high volume gas heated carburizing equipment to small batch carburizing in electrically heated furnaces did not reduce utility costs per part; instead, other areas adjusted to compensate. Eliminating the expense of hard grinding transmission gears was an acceptable rationale for this increase in both capital expense and operating costs. Eventually, streamlining the overall gear manufacturing process, combined with locating heat treat within machining lines, produced positive measurable results. Plant traffic decreased, minimizing safety risks. Cooler and cleaner furnace systems were designed. And installations were made easier. Many agreed the changes were justified.
Integrated Vacuum Heat Treat Cells
As we look back, many of these drivers for change proved valid. Others, not so much. In most cases, consumer preference for quiet powertrains necessitates hard grinding of gears. Green is in and talk of the absolute need for zero intergranular oxidation (IGO) in carburized gears has slowed. LPC/Gas post quenched parts are perceived as cleaner and leaner; however, it is often difficult to differentiate green parts from processed parts, so it has become a best practice to add part marking after carburizing and hardening to avoid even the remote risk of sending soft parts down the line to the next stage of manufacturing. Shot peening is still common for strength reasons. The ability to nest large cellular LPC systems within machining has been a success, but rarely are the installations as quick and easy as promised.
Hybrid Furnace Concepts
Conventional atmosphere furnace technology has advanced as well, although at a slower pace, in step with a renewed interest in energy efficiency, particularly in the U.S. where gas is cheap and electric is not. Combustion systems operate cleaner and at much higher efficiency than in the past. Having said that, it is curious how little interest end users have in trading cost-saving gas-heated systems for the easier to install, neater looking electric heating options. In addition, it is no longer common to use water for cooling conventional atmosphere furnace systems as end users do not want to deal with the cost and complications that accompany this option. The market is polarized over this. LPC systems rely on large water volumes for cooling, and they are small batch, electrically heated systems. At the same time, gas quench systems consume huge quantities of water and require giant 300 HP plus motors that are tough to manage in plant power systems.
Flexible and Re-deployable Heat Treat Systems
It is my observation that the automotive market is anticipating the next iteration of heat treat equipment. One type of process or equipment style will not fit all needs, yet all hope for the perfect single part flow solution—an elusive dream due to physics. The cost/time equation still does not balance, and carburizing offers the benefits many manufacturers are looking for, despite the desire to design the process out of practice. Many automotive transmission parts that were originally processed in LPC and gas quenched now use gas nitriding instead, even though gas nitriding is another long process, and nitriding introduces ammonia back into the process—something most automotive plants are not enthusiastic to have in their plants. Two steps forward and one step back.
Repackaging Continuous Furnace Systems
With the widening range of processes and solutions under exploration, as well as ever changing powertrain systems designed to accommodate supplemental electric motors, lighter weights, smaller cars, and larger SUVs, all we can be certain of is ongoing change. I believe that we have witnessed major adjustments in automotive heat treat processing as the pendulum has swung from big, multi-row atmosphere pushers with salt or oil quench to electric-heated cellular LPC and gas quench units. One surprising result has been the resurgence of salt quenching, which controls distortion of high-pressure gas at a much lower cost with less complexity. Salt, like gas, is a single-phase quench media: It does not boil in these processes like oil does, and it can be used at temperatures that support martensitic quench with far less thermal shock and much higher heat transfer than the options. Older processes carry the baggage of tarnished past reputations, but I no longer count them out. Today’s automation, process control technology, and innovation can provide the foundation for brand new concepts, repackaging of older ideas, and hybrids of multiple technologies. Together, these create building blocks that heat treat equipment suppliers will use to meet changing trends in automotive carburizing and heat treatment. It will be interesting to be involved in the journey as these changes take place.
About the Author: Bill Disler is president and CEO of AFC-Holcroft, part of the Aichelin Group located in Vienna, Austria. He is a member of the Board of Trustees -Metal Treating Institute (MTI), and a member of the Board of Advisors at Lawrence Technical University, College of Engineering in Southfield, Michigan. This article originally appeared in Heat Treat Today’sJune 2019 Automotive print edition.
Join aluminum extrusion industry professionals from more than 50 countries at the International Aluminum Extrusion Technology Seminar (ET Seminar)! This seminar features more than 100 technical sessions, an exposition featuring products, equipment, and services from industry suppliers, networking events, and much more!
Delegates from around the world gather to hear about the latest industry developments. At the core of the ET program are the technical sessions which feature research that is new or updated.
Please Note: The ET ’20 program has a new pattern compared to previous years. The program will open on Tuesday, May 19th with the Opening General Session, including Best of Track paper presentations. The final session of ET is scheduled for Thursday afternoon, May 21st, and will contain the Best Paper of ET presentation plus the remaining Best of Track Paper presentations.
To get the most value out of ET, delegates should not plan to leave before the end of the Closing General Session at 5:00 p.m. on Thursday, May 21st.
Please make a note of this new pattern when making your travel arrangements!