MANUFACTURING HEAT TREAT

Why Now? Women in Heat Treat

Women are taking on increasingly influential technical, operational, and leadership roles across the heat treat industry. Learn about the importance of building community and connection through Women in Heat Treat and preview the learning, leadership, and networking opportunities coming to Cleveland this November.

This community-focused feature was first released in Heat Treat Today’s September 2026 People of Heat Treat print edition.


Women Are Here. But How Many?

How many women are actually working in heat treating? It is a surprisingly difficult question to answer.

The only industry-level data point we have found comes from a 2005 EEO Aggregate Report. At that time, women represented 14.8% of the commercial heat treating workforce. That number is more than 20 years old, and it doesn’t tell us how today’s workforce breaks down across commercial heat treaters, captive operations, suppliers, engineers, operators, and leadership.

So, is the number higher today? Lower? We don’t really know.

What we do know is that women are here. We are increasingly seeing women step into technical, operational, leadership, and decision-making roles throughout the industry. These women are bringing technical expertise, discipline, and a passion for their work to wherever their boots land every day.

That matters because heat treating has long been a field defined by a certain kind of culture: practical, technical, problem-solving, action oriented. If you’re here to do good work, you’re welcome.

But being welcome and feeling fully at home are not necessarily the same thing.

Making Space to Just Be

It isn’t controversial to acknowledge that heat treating has traditionally been a male-dominated industry. There are norms that don’t need to be spoken because the people who have been in the room for generations already understand them.

For women entering that room, some of those norms can be more noticeable. For women who have been in the industry for many years, those norms may still stand out as unwritten rules to navigate.

Sometimes it is wondering whether the way you speak in a meeting will be received differently than it would from one of your male colleagues. Sometimes it is second-guessing what to wear to an industry event. Sometimes it is walking into a social setting and realizing that the conversation, atmosphere, or expectations don’t quite resonate with you.

Women shouldn’t have to become less themselves to be taken seriously as professionals. Nor should any woman have to spend valuable energy wondering whether she is presenting herself in the “right” way when what matters most is the knowledge, experience, judgment, and value she brings to the room.

The answer lies in making room for women to bring their whole professional selves to the industry, even in spaces where doing so may not come naturally.

An Invitation

Creating that space where the women of this industry can bring their strengths with confidence is one reason we’re excited about Women in Heat Treat. For two and a half days in Cleveland, women from across the industry will have the opportunity to learn from experienced professionals, build technical expertise, explore the technologies shaping the future of heat treating, and have candid conversations about leadership and professional growth.

The most important part may be simpler than any of that: standing side-by-side in a room full of women who understand the work. From the challenges you’re trying to solve, to navigating a career decision you’re facing now, to simply being introduced to interesting people you want to know — and who want to know you — this space is designed for you.

Professional growth doesn’t happen in isolation. It happens through technical learning, mentorship, relationships, and conversations that continue long after a formal session ends. As a team made up largely of women ourselves, we’re especially excited to create more of those connections.

A Community Worth Building
There have been commendable efforts over the years to create more opportunities for women to be recognized, heard, and taken seriously in heat treating. Women in Heat Treat builds on that momentum by creating something very simple, but very intentional: a place for women in this industry to gather as professionals, learn from one another, and simply be in the room together.

So, if you’re a woman working in heat treating — whether you’re building technical expertise today, operating equipment, engineering processes, managing a team, making strategic decisions, or preparing for the next stage of your career — consider this your invitation.

Come learn. Come contribute. Come meet the women who are shaping where this industry goes next.

And, perhaps most importantly, come as yourself.

We’ll see you in Cleveland this November.

www.heattreattoday.com/womeninheattreat


Keynote Speakers:
Katie Rucker
Co-Owner, Strategic Insights & Foresight Partner
MacKenzie Corp & Next Gen Collaborative

Katie will encourage attendees through her presentation, “The Other Side of Your Comfort Zone.” The other side of your comfort zone isn’t just about doing something scary. Sometimes it’s about giving yourself permission to imagine something you haven’t seen modeled before. You are in for a treat!
Susan Lanz
Educator & Writer

“What’s Your 100 Miles?” That’s the question Sue will explore. We live in a culture that celebrates breakthrough moments and overnight success. But real transformation rarely happens in a single leap. It is built through small, courageous decisions — often made when no one is watching, and there is no guarantee of success.


Sneak Peek of Some of the Sessions

Live Recorded Panel Discussion

A live podcast filming devoted to the unique challenges and opportunities of being a woman leader in heat treating. Women on this panel include metallurgy and engineering decision-makers and OEM leaders.

The panel will be hosted by leading industry voice and founder/president of Falcone Consulting, Heather Falcone. Heather is the host of Heat Treat Radio, a podcast by Heat Treat Today, where the recording of the panel will be broadcast and made available to a wider audience.

Heather Falcone, Founder/President of Falcone Consulting

Breakout Session: Claiming Technical Authority at the Standards Table

Women in quality, engineering, and operations are often responsible for turning dense technical requirements into work the shop floor can execute and records an auditor can follow. This session will examine common requirements, including AMS2750 for pyrometry and other major material processing specifications, Nadcap audit criteria, and ASTM testing methods. Andrew Bassett and Sarah Lombardo will also discuss how AMEC, ASTM committees, and the Nadcap Heat Treating Task Group influence industry requirements. Attendees will strengthen their ability to interpret revisions, manage flow downs, resolve conflicts, and lead specification compliance with confidence.

Sarah Lombardo, Quality Assurance Manager, Vacu Braze
Andrew Bassett, President, Aerospace Testing and Pyrometry

Breakout Session: Programming for Advanced Manufacturing

Programming and digital fluency can expand the paths available to women in manufacturing, from process engineering and automation to research, operations leadership, and entrepreneurship. Zachary Menard will explore the skills required to design, run, and improve advanced manufacturing systems. Drawing on research and development work and the experience of launching a new company, he will discuss emerging tools, workforce readiness, and the connection between technical knowledge and reliable production. Attendees will gain a clearer view of what is available now, where the field is heading, and how women can prepare themselves, mentor others, and help shape the next generation of manufacturing technology.

Zachary Menard, Co-Founder & President, HRC Labs

Breakout Session: The Ins and Outs of Process Change

Women in engineering, quality, and operations frequently carry responsibility for coordinating process changes across technical teams, production, customers, and suppliers. Our speaker will walk through the questions that help leaders evaluate a change before implementation, including technical risk, validation, customer approval, specification requirements, documentation, and communication. The session will also address how women can build credibility when raising concerns and keep the right voices involved throughout the decision. Attendees will leave with a practical framework for moving improvements from idea to controlled execution while protecting product performance and customer confidence.

Speaker TBD

Breakout Session: Future-Proofing Heat Treat: Digital Tools That Strengthen People and Performance

Digital transformation is changing the way heat treaters operate, but technology alone isn’t the solution. Explore how modern digital systems are reducing administrative burden, simplifying workforce training, preserving institutional knowledge, improving compliance, and helping organizations adapt more quickly to changing customer and industry requirements. Matthew will discuss practical strategies for implementing technology that supports people, drives consistency, and prepares companies for the future.

Matthew Wright, Vice President, C3 Data

Breakout Session: Cross-Cultural Challenges

In North American manufacturing, trust is built differently across cultures — but trust remains essential to quality partnerships. What are the differences in professional expectations from Mexico-based professionals and U.S. Why do technically strong projects sometimes fail? Where do misunderstandings originate? How can purchasing, quality, and operations improve collaboration? Attendees will leave with practical insights for navigating cultural differences, strengthening communication, and building more effective working relationships.

Ana Laura Hernández Sustaita, Founder, Consultoria Carnegie
Víctor Zacarías, Managing Director, GTS México

Breakout Session: AI for Operation Controls

Women working in operations, quality, and technology have an important opportunity to shape how AI enters manufacturing. Our speaker will examine practical applications for AI in process monitoring, data analysis, traceability, exception management, and operational decision-making. The session will explore the data discipline, cybersecurity, governance, and human oversight required to introduce these tools responsibly. Attendees will leave with a grounded framework for evaluating AI, asking informed questions, and determining where it can improve consistency and performance. The conversation will also encourage women to take an active role in the technology decisions influencing the future of their organizations.

Speaker TBD

Breakout Session: The Power of the Seat You’re In

Women often carry leadership responsibility before authority and title catch up. Our speaker will explore how women can build influence, earn trust, make sound decisions, and create momentum from wherever they sit in an organization. Through practical examples, they will discuss communicating with confidence, developing others, advocating for ideas, and staying grounded when the path forward is unclear. Attendees will be encouraged to recognize the leadership opportunities already within reach and consider how their experience, judgment, and perspective can strengthen the teams around them. They will leave with practical ways to contribute, grow, and lead with purpose in the work directly in front of them.

Katie Rucker, Co-owner, Strategic Insights & Foresight Partner, MacKenzie Corp & Next Gen Collaborative
Sue Lanz, Educator & Writer
Why Now? Women in Heat Treat Read More »
WH Kay Marks 90 Years by Staying in the Flow

Ninety years is a remarkable milestone for any company. In the heat treating industry, where technologies, markets, and client expectations have continually evolved, reaching that anniversary requires more than longevity — it requires adaptability.

For W.H. Kay Company, that adaptability has been the defining characteristic since William Henry Kay founded the company in 1936, during the final years of the Great Depression. What began as a Cleveland-based manufacturer’s representative for Eclipse Combustion Equipment has grown into a company recognized throughout North America for combustion systems, used heat treating equipment, and practical process solutions.

Along the way, W.H. Kay has come to describe itself as “The Elder Statesman of Used Ovens and Treating Furnaces” — a moniker that reflects both the longevity of the business and the used-equipment specialty it developed over decades.

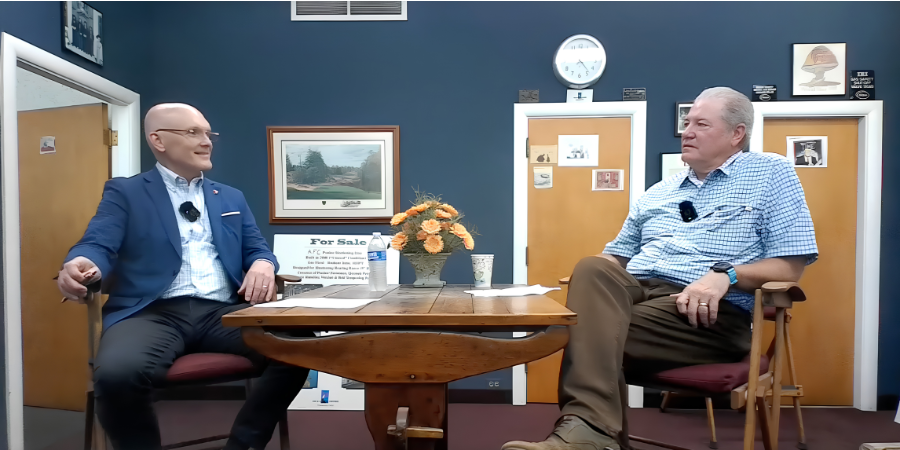
Doug Glenn, publisher of Heat Treat Today (left), sat down with Michael Kay, president of W.H. Kay (right), about the company’s 90-year journey — from its beginnings as a combustion equipment representative to becoming a trusted resource for industrial thermal processing solutions. | Image Credit: Heat Treat Today

Today, under the leadership of third-generation owner Michael Kay, the company continues to serve commercial heat treaters and manufacturers while maintaining a relationship with Eclipse — now part of Honeywell — that has lasted since the day the company opened its doors.

“It’s amazing,” Kay said. “We’ve represented Eclipse since 1936.”

From Representation to Reinvention

W.H. Kay’s history reflects many of the changes that have shaped industrial thermal processing over the past nine decades.

William Henry Kay, Michael Kay’s grandfather, represented Eclipse Burners and Furnaces throughout northern Ohio. When Eclipse phased out of furnace manufacturing, Michael Kay’s father, Frank, and uncle, Bill, continued serving longtime clients who wanted additional furnaces like the Eclipse equipment they already operated. Using existing furnace prints, W.H. Kay had units fabricated to meet those clients’ needs.

That work eventually opened another avenue for the company as clients purchasing new equipment began asking what to do with their existing furnaces. W.H. Kay started accepting equipment on trade and finding new buyers for it, gradually establishing the used-equipment business that remains a significant part of the company today.

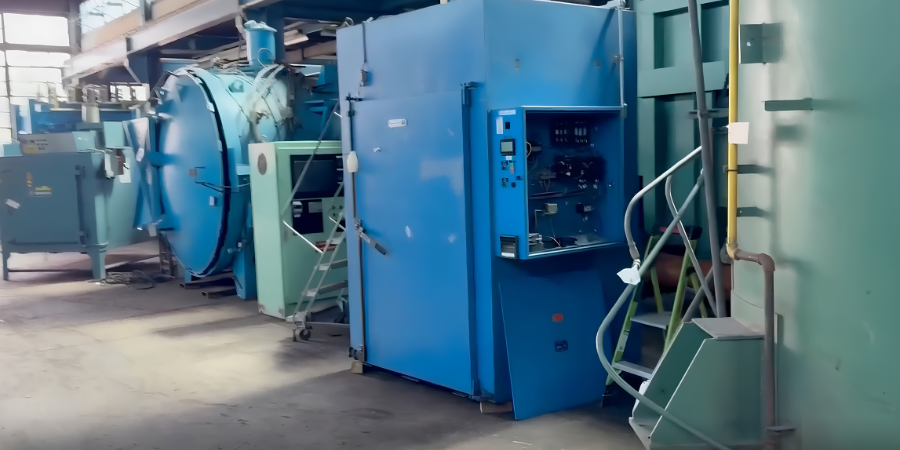
A variety of equipment at the W.H. Kay facility | Image Credit: Heat Treat Today

Today, the company’s Solon, Ohio, warehouse houses hundreds of pieces of equipment ranging from tempering ovens and pit furnaces to vacuum furnaces, integral quench systems, atmosphere generators, and ancillary processing equipment.

The Value of Staying Close to the Client

Although W.H. Kay still supplies combustion products and represents JPW Industrial Ovens & Furnaces, Kay believes the company’s success has never been about simply selling products. “If you’re just taking orders, you’re kind of in trouble,” he said. “You’ve got to be proactive.”

That approach extends to how the company works with clients, beginning with an understanding of the application rather than simply supplying the equipment initially requested. A client inquiring about a 1600°F furnace, for example, may actually be operating at only 900°F — a distinction that can point to an entirely different equipment solution. “You’ve got to listen,” he said. “What they’re asking for might not be what they actually need.”

The willingness to listen can remain valuable long after the initial sale. Kay recalled a recent call from a client who had purchased a furnace seven years earlier, and, no longer needing it, approached the company about buying it back. Other clients contact the company when they need something larger or have equipment they no longer use. For W.H. Kay, responding to those changing needs has made used equipment more than an inventory business; it has become another way to provide clients with options.

Providing a used-equipment option does not, in Kay’s experience, come at the expense of new furnace sales. Over his four decades in the industry, he said, clients who intend to purchase new equipment generally do so, while those considering used equipment often have a different set of requirements. “In the course of 40 years, I’ve never seen a used [furnace] take over a new account,” he said. “If people are buying new, they’re buying new. If they’re buying used, they’re buying used.” Instead, he sees used equipment as another way to help clients solve a problem.

If a manufacturer needs an oven immediately rather than waiting several months for a new build, used equipment can provide an option that better fits the client’s timeline. “We could quote him a new one in 16 weeks,” Kay said. “Or we could have one in four days.” With hundreds of pieces of equipment in its Solon warehouse, the company can sometimes match a client’s requirements with a unit already in inventory, providing an alternative when lead time is as important as the equipment itself.

Understanding those circumstances requires more than waiting for an inquiry. It also means getting out of the office and spending time with clients. “You’ve got to get in the flow,” he said.

Whether checking on a furnace sold years earlier or simply stopping in to ask how things are going, those visits help the company stay aware of how clients’ operations and equipment needs are changing. A conversation might reveal a furnace the client no longer uses, a need for something larger, or anther equipment requirement that W.H. Kay can help address.

“My father used to say you can waste a lot of time coming into the office every day,” Kay recalled. “You need to be out with [clients].”

The practice has endured even as industrial sales have changed around it. Kay remembers beginning his career in 1985 carrying a substantial Eclipse product catalog on sales calls, followed by the arrival of fax machines that dramatically shortened the time required to submit and acknowledge orders. Email and the internet have transformed the process again, while the number of salespeople regularly making in-person calls has declined. “In some cases,” he said, “people tell me they haven’t seen a salesperson in six months.”

For W.H. Kay, continuing to make those visits is less about maintaining an old-fashioned sales practice than staying close to the client. The tools of industrial sales may have changed considerably over 90 years, but the company still sees listening, understanding the operation, and building rapport as essential to finding the right solution.

Listening before selling, understanding the application, and building long-term relationships have remained central to the company as the business has weathered changing technologies, shifting markets, and multiple generations of industrial manufacturing.

Creating Your Own Good Luck

W.H. Kay’s nine decades have included more than changes in how equipment is bought and sold. The applications themselves continue to evolve.

Kay has seen growing activity around aluminum heat treatment, including aging and drop-bottom furnace applications, as manufacturers pursue lighter materials. The company has also supplied ovens for composite curing and other lower-temperature processes. Additive manufacturing presents another evolving area; even when parts are produced through 3D printing, Kay noted, thermal processes such as stress relieving can remain necessary.

Through those changes, Kay expects industrial heating and thermal processing to continue finding applications in emerging manufacturing technologies. The greater lesson he draws from more than four decades in the business, however, is less about predicting which technology or market will come next than about remaining engaged enough to respond when it does.

Kay returned to one idea again and again: success isn’t about waiting for opportunities to arrive — it’s about putting yourself where they can happen. Whether checking in on clients, making sales calls, or simply staying engaged with the industry, he believes consistent effort creates its own momentum. The advice he offers today is the same philosophy that has guided his career for more than four decades.

“Create your own good luck,” Kay said. “Keep at it. Get out of the office.”

Ninety years after William Henry Kay founded the company, the equipment, technologies, and methods of doing business have changed considerably, but the philosophy remains much the same: listen to clients, stay engaged, and keep showing up. It continues to guide his company — one client visit, one solution, and one furnace at a time.

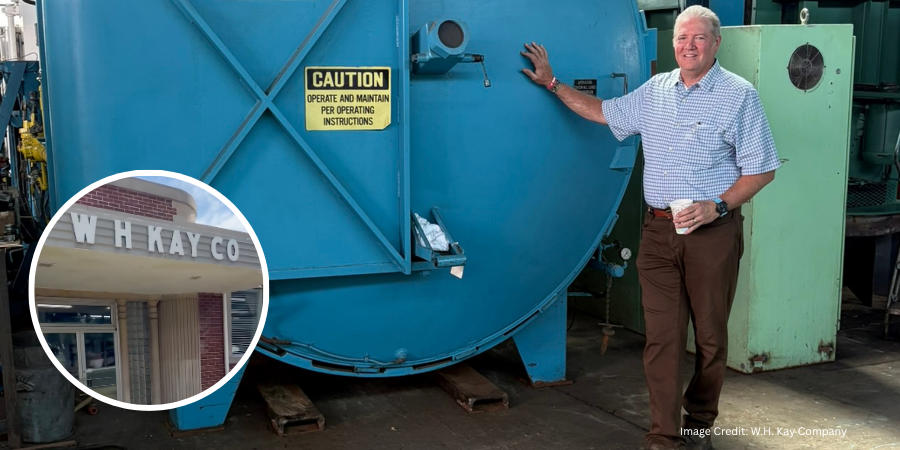
Main image shows Michael Kay posing with a vacuum furnace with a photo inset of the entrance to the W.H. Kay facility. | Image credit: W.H. Kay Company
If you have any comments or queries on this article, let us know at editor@heattreattoday.com.

WH Kay Marks 90 Years by Staying in the Flow Read More »

Stack Metallurgical Group Increases Operations with Horizontal Vacuum Furnace

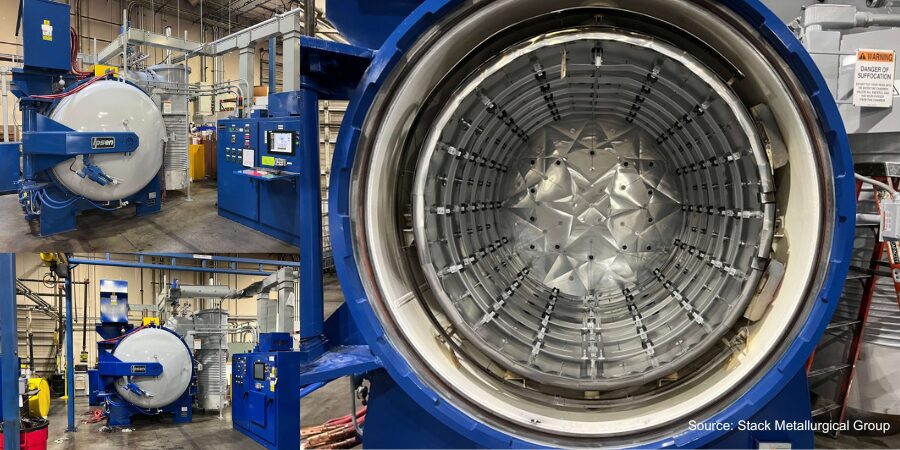
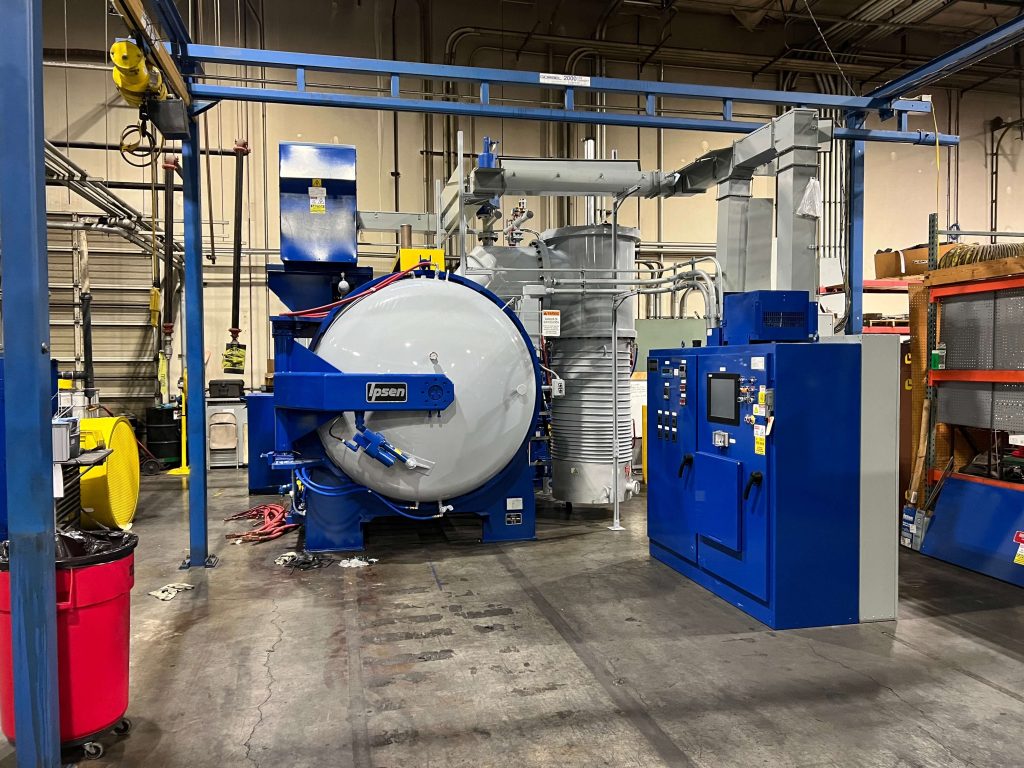
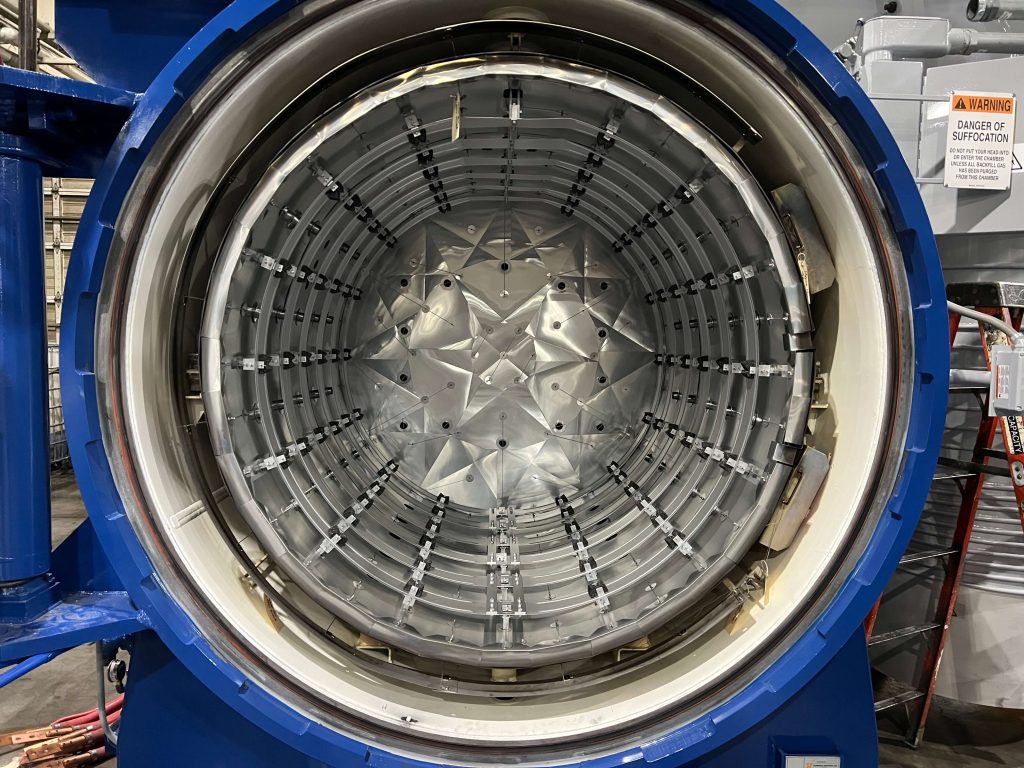
A U.S. heat treater has expanded their operations with the installment of a horizontal vacuum furnace. Stack Metallurgical Group announced the addition of a 6 bar quenching TurboTreater furnace at their Portland facility.

Stack services aerospace, medical, and cutlery industries, among others. The company shared, “Stack is continuing to show our commitment to excellence by investing in a brand new 6 Bar quenching, Turbotreater horizontal vacuum furnace from Ipsen. This is more than a purchase; it’s a substantial investment in our facilities and, more importantly, in our valued customers.”

The Ipsen vacuum furnace features internal quenching with 360-degree cooling uniformity, decreases cycle times up to 20%, and reduces gas consumption up to 40%. The furnace handles heavy loads and operates for multiple processes, including hardening, tempering, brazing, sintering, and annealing.

Press release is available in its original form here.


Stack Metallurgical Group Increases Operations with Horizontal Vacuum Furnace Read More »
IperionX Granted $1.3 Million for U.S. Critical Titanium Components

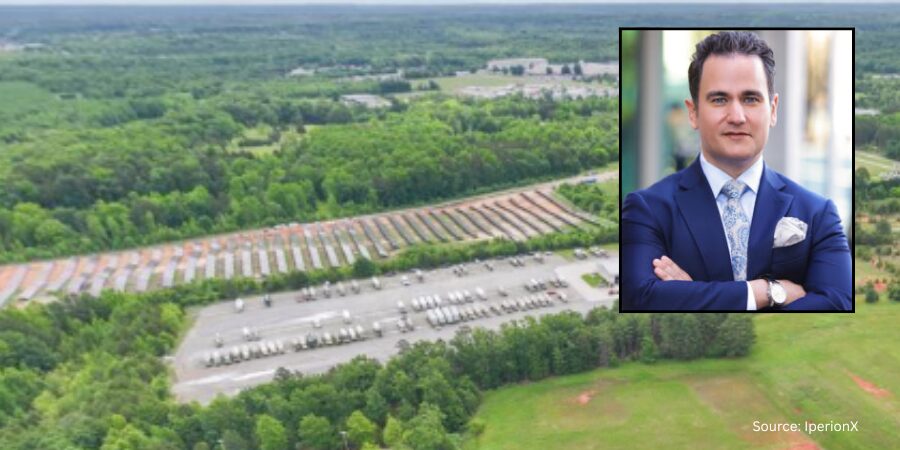
A U.S. titanium metal and critical materials company has been granted $1.3 million for forged critical titanium components. IperionX will produce the titanium parts for U.S. Army ground vehicle programs at their Titanium Manufacturing Campus in Virginia.

Anastasios (Taso) Arima
CEO
IperionX
Source: IperionX

The task order will be fulfilled using titanium production and advanced forging processes.

“Securing this first U.S. Army task order is a decisive step toward reshoring the nation’s titanium supply chain,” said Anastasios (Taso) Arima, IperionX CEO.

The project is the first of further task orders expected under the US $99 million SBIR Phase III contract, which enables any DoD and U.S. Government agency to support production capabilities by procuring titanium parts and materials directly from IperionX.

All technical specifications, performance requirements, and delivery schedules are governed under the U.S Controlled Unclassified Information Program (Executive Order 13556), ensuring protection of sensitive defense information.

For additional information about IperionX’s heat treat capacities, click here.

Source: IperionX

Press release is available in its original form here.


IperionX Granted $1.3 Million for U.S. Critical Titanium Components Read More »

Smarter Furnace Systems: Engineering Energy for Sustainability from the Ground Up 

There are many avenues for achieving new feats in sustainability. One foundational method of pursuing sustainability is efficient furnace design. In this Control’s Corner installment of Technical Tuesday, Stanley Rutkowski III, senior applications engineer, RoMan Manufacturing, Inc., explores ways to design furnace electrical power systems for efficiency.

This informative piece was first released in Heat Treat Today’s June 2025 Buyers Guide print edition.


In the world of industrial heat treating, sustainability isn’t just a buzzword; it’s a measurable outcome of engineering decisions. While discussions around energy usage often focus on renewable sources or carbon offsets, the path to sustainability begins much earlier — with the design of the furnace’s electrical power system. 

From transformers and load configurations to modern control technologies, every part of the furnace power pathway affects how efficiently energy is used — and how much of it is wasted. A well-designed system doesn’t just heat effectively; it does so with less resistance, fewer losses, and minimal disruption to the power grid. 

The Power Triangle: Real, Reactive, and Apparent 

Understanding sustainability starts with understanding how energy is consumed. Utility companies bill based on more than just energy (kWh). They measure and potentially build via: 

  • Real power (kW): the usable energy 
  • Reactive power (kVAR): the energy lost due to inductance and system inefficiencies 
  • Apparent power (kVA): the total power delivered, including losses 
  • Power factor: the ratio of real power to apparent power, indicating system efficiency 
  • Peak demand: the highest level of power drawn during a billing period 

Furnace systems with poor power factor or high reactive power incur more cost, even if their real energy usage is low. That’s why electrical design is so critical. 

Control Systems: The Shift to Digital 

Legacy systems, such as tubes or saturable reactor-based VRTs, have largely given way to more efficient SCR- (silicon controlled rectifier) and IGBT- (insulated-gate bipolar transistor) based controls. IGBT technology, in particular, offers high-frequency switching, reduced losses, and excellent power factor performance. These systems also provide communication protocols — giving real-time insight into power draw, voltage stability, control temperatures, and even predictive maintenance alerts. 

Digital communication allows users to evaluate trends over time. For example, changes in DC bus voltage or output current may signal a degrading heating element, enabling early intervention. Smart controls also help avoid peak demand charges by shifting high-load operations to off-peak hours or adjusting recipes to consume less total power. 

Load Configurations and Layout

Load configuration is equally as important: single-phase, Scott-T two-phase, or balanced three-phase arrangements. Poorly balanced systems place stress on utility infrastructure and reduce power factor. Balanced loads, especially when combined with IGBT control, lower disturbances to the grid and increase efficiency. 

Physical layout also plays a key role. Long conductor runs increase resistance and inductive reactance, which raises energy consumption and heat loss. “Close coupling” the transformer and conductors near the furnace feedthrough reduces losses and improves power delivery, which is important for sustainability and cost savings. 

AC vs. Rectified DC Power

Finally, consider how power is delivered. While AC remains common and easy to install, rectified DC systems eliminate voltage zero-crossings, resulting in more stable heating and reduced thermal stress on elements. For high-precision applications like carburizing or annealing, DC systems can extend equipment life and improve thermal uniformity. 

Conclusion 

Energy sustainability in heat treating isn’t just about switching to greener sources — it starts with how power is delivered, controlled, and consumed. Getting a power conversion expert involved early in the planning and system design process ensures that every component is optimized for efficiency, reliability, and long-term performance. This early collaboration helps manufacturers reduce energy costs, extend equipment life, and achieve more sustainable operations without compromising results. 

About The Author:

Stanley F. Rutkowski III
Senior Applications Engineer
RoMan Manufacturing, Inc.

Stanley F. Rutkowski III is the senior applications engineer at RoMan Manufacturing, Inc., working on electrical energy savings in resistance heating applications. Stanley has experience in welding, glass and furnace industries from R&D, design, and application standpoints. For more than 15 years, his focus has been on energy savings applications in industrial heating applications.

For more information: Contact Stanley at srutkowski@romanmfg.com.


Smarter Furnace Systems: Engineering Energy for Sustainability from the Ground Up  Read More »

Vacuum Furnace System For Increasing In-House Heat Treat Demands

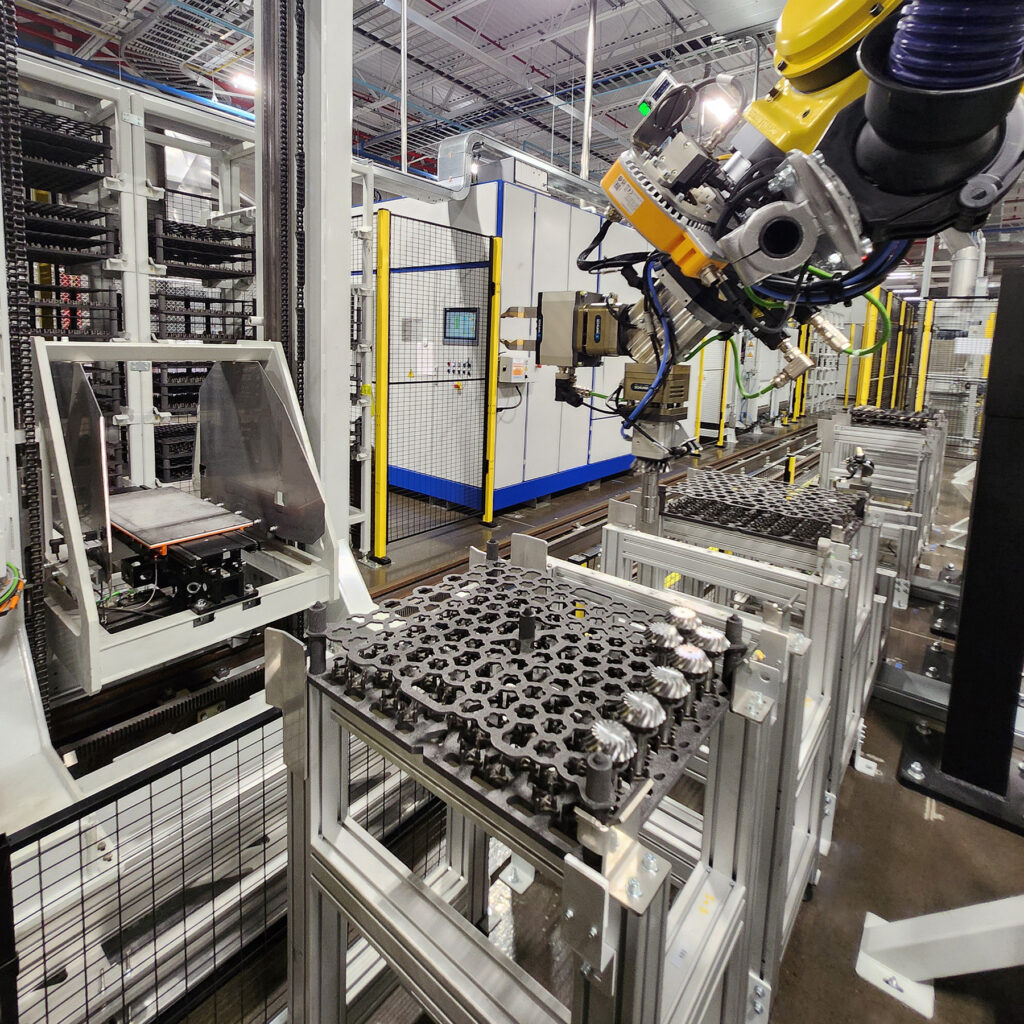
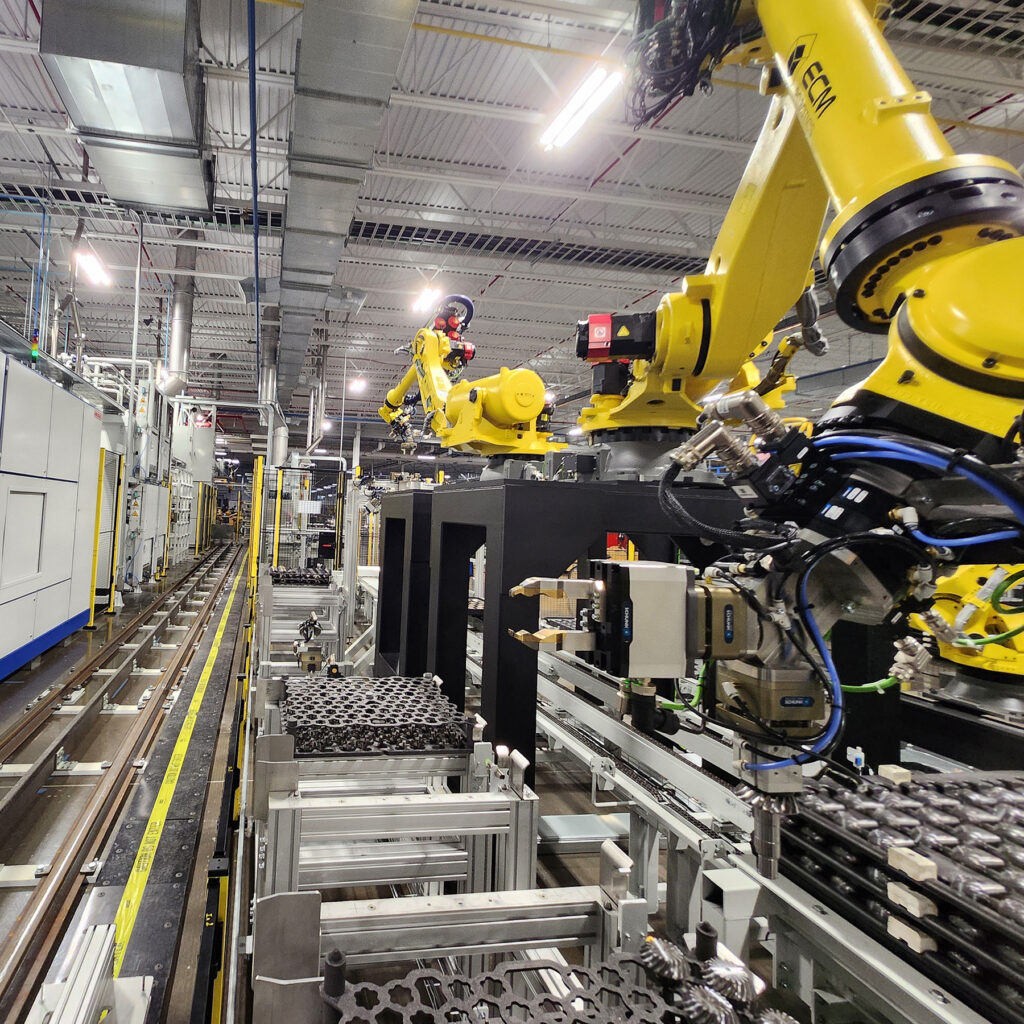
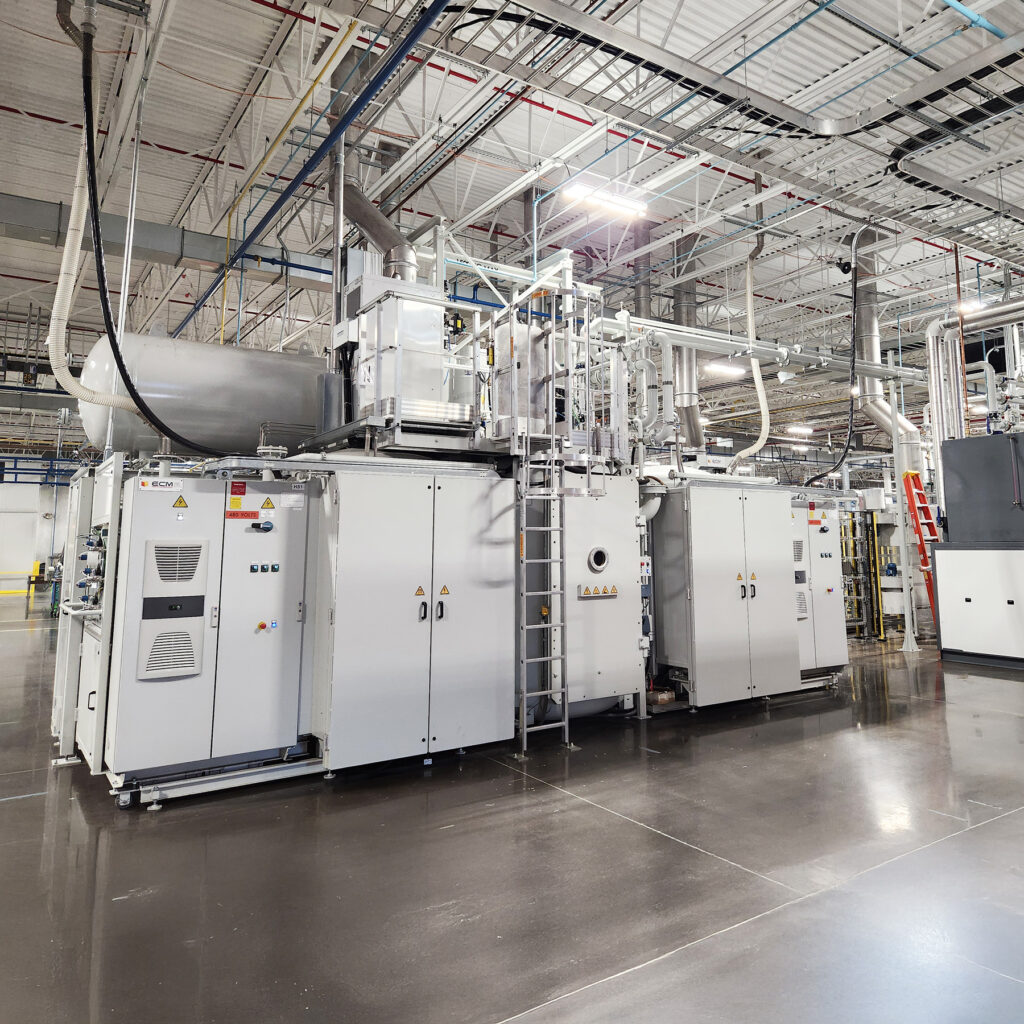
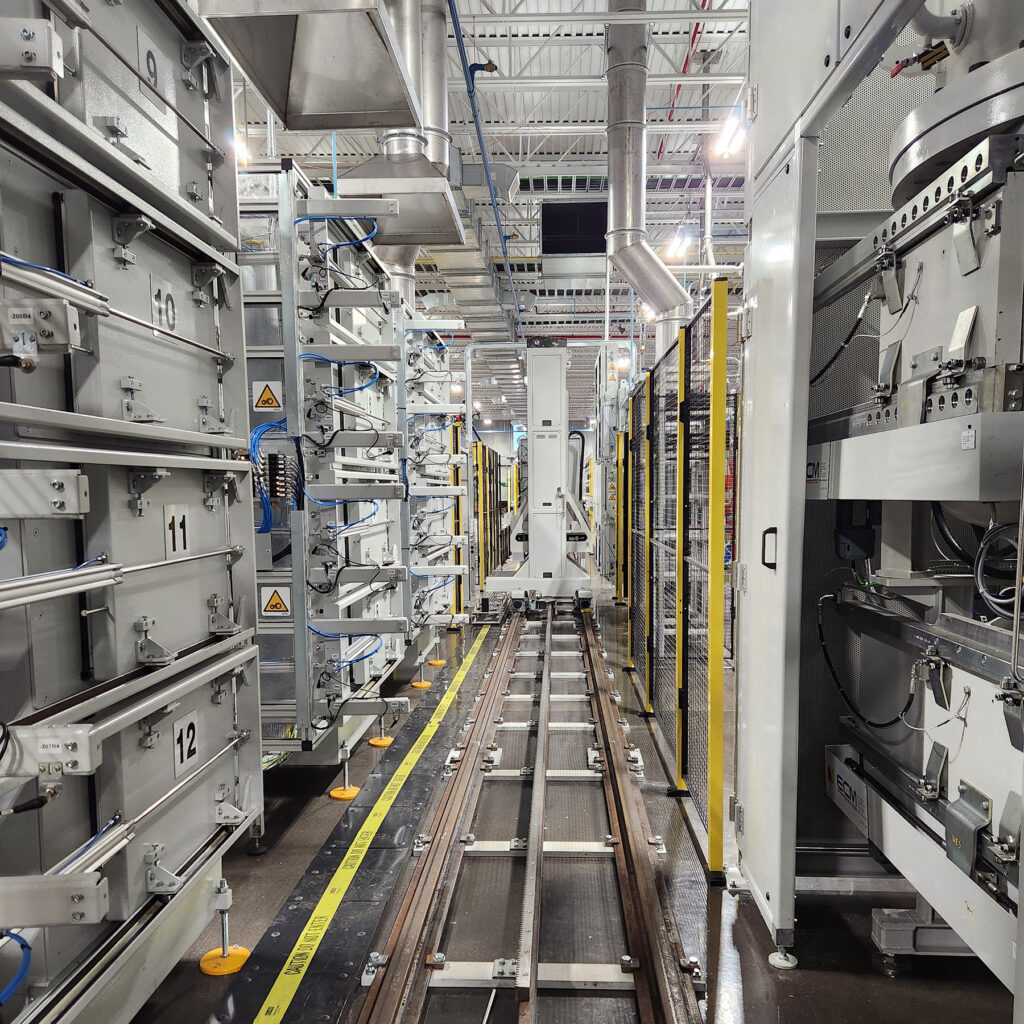
A modular NANO vacuum furnace system was commissioned for increasing in-house heat treat demands in drive technology. The furnace has reached its final acceptance.

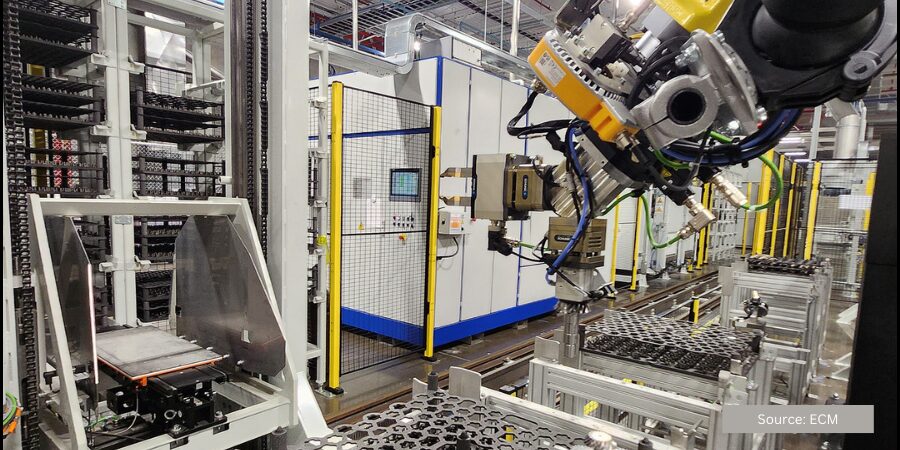
SEW-EURODRIVE completed their fully automated in-house vacuum furnace system integrated with their patented MOVI-TRANS® inductive energy power transfer system (pictured parallel with ECM’s transfer system rails). SEW EURODRIVE partnered with ECM USA to commission the furnace which is completely integrated with advanced automation for their Lyman, South Carolina facility.

This 6 chamber, 20 bar quench NANO vacuum furnace system provides flexibility and integration utilizing the addition of 16 tempering positions, advanced solvent based washer (both oil and water based contaminants), and robotic workload assembly/disassembly. . . Specifically designed to run multiple materials (including carburized grades and tool steels) this system has modular flexibility to adapt to increased production demands for various load scenarios and processes.

Press release is available in its original form here.


Vacuum Furnace System For Increasing In-House Heat Treat Demands Read More »

The Evolution of Cleaning Technology in Heat Treating: Time To Rethink the Approach

This instructive piece was first released in Heat Treat Today’s April 2025 Induction Heating & Melting print edition.


In heat treating, clean parts are essential for repeatable, high-quality results. Yet cleaning is often seen as a necessary evil rather than a strategic process. That mindset must change. 

For decades, gas carburizing with oil quenching has dominated the industry despite challenges, such as contamination, environmental concerns, and part distortion. These issues have driven growth in alternative processes, such as vacuum carburizing with gas quenching and nitriding, which eliminate post-quench oil contamination. However, not all metallurgical requirements can be met with these newer processes, and gas carburizing with oil quenching remains necessary for many part sizes, geometries, and material types. Furthermore, some alternative processes require more advanced pre-cleaning technology, adding complexity. 

I briefly left heat treating in 1998 — I call it my sabbatical from heat treating — to work in advanced industrial cleaning and automation. When I returned about five years later, I was struck by how far behind the industry was in cleaning technology. While other manufacturing sectors had embraced modern solvent and hybrid cleaning systems, heat treating continued to rely on outdated aqueous washers that struggle to clean oil-contaminated parts effectively. It goes back to the old axiom: oil and water don’t mix. Spraying harder only emulsifies the oil further, making separation and disposal even more difficult, increasing costs, and creating sustainability concerns. 

Paths Forward 

  1. Process shift — Where practical, companies have transitioned from oil quenching to vacuum carburizing with gas quenching, nitriding, and other alternative processes that reduce contamination issues. Of course, such changes are not driven solely by cleanliness — metallurgical requirements and process economics are complex topics. Gas carburizing with salt quenching is an often overlooked alternative, which offers superior heat transfer over gas quenching, reduces distortion, and is environmentally sustainable. Unlike oil quenching, cleaning aft er salt quenching is far simpler, as hot-water washers reclaim over 99% of the salt in a closed-loop system. The old negative mindset about salt, which questions the safety and toxicity of high temperature salt, has restrained process growth in this area. New equipment designs could create interesting, alternative paths with multiple benefits. 
  2. Mindset shift — If oil quenching remains necessary, cleaning processes must improve. Conventional aqueous washers are inefficient, and while modern cleaning systems are effective, they are costly. However, when considering part quality, sustainability, efficiency, and long-term cost savings, these systems provide a strong ROI and should not be dismissed. 
  3. Technology shift — Sustainability in cleaning cannot be ignored. Water-based systems with distillation attempt to recycle but have high energy costs, making solvent-based systems with integrated distillation more practical for higher efficiency and lower hazardous waste output.  
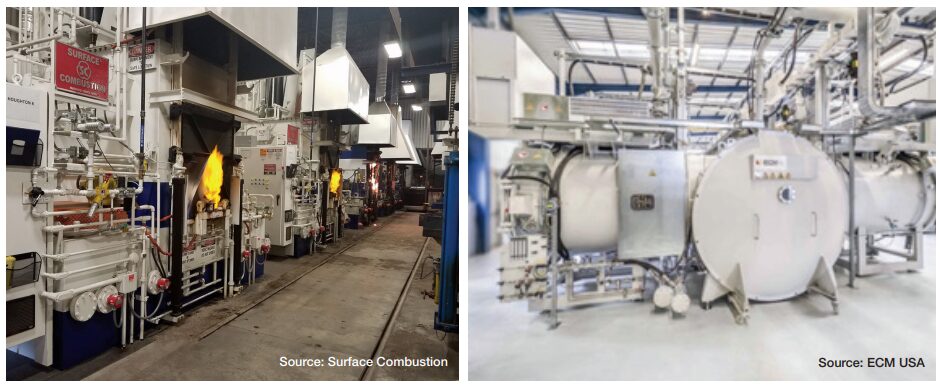
Rugged environments (left) require cleaning systems that modern washers are not often built for. Many new washers are more suited to clean controlled environments like vacuum heat treating (right). (Images from “All About IQ Furnace Systems,” 16)

Challenges with Modern Washer Designs — Thoughts for Manufacturers  

One major barrier to adopting advanced cleaning systems is cost, driven by their design. Many new washers are built for clean, controlled environments like vacuum heat treating but are poorly suited for traditional heat treat shops using oil quenching. Th ese shops have different requirements — floor space constraints, varied load configurations, and harsher conditions — meaning rugged, adaptable, and cost-effective solutions are needed. Function must take priority over aesthetics. 

Washer manufacturers should rethink their designs to better fit conventional operations by focusing on durability, modularity, and cost-conscious engineering. Doing so could lower costs while improving adoption rates and accelerating industry-wide improvements in part cleanliness, quality, and sustainability. 

Conclusion 

Heat treating is changing, and cleaning technology must evolve with it. Whether by adopting better process alternatives, improving cleaning methods, or rethinking equipment design, companies that embrace innovation will reduce waste, improve efficiency, and ensure long-term success with a stronger commitment to sustainability and environmental responsibility. 

The industry is evolving. It’s time to evolve with it. 

References

About The Author:

William (Bill) Disler
President
WDD Consulting LLC

William (Bill) Disler entered the heat treat industry as a young engineer, quickly establishing himself as a hands-on expert and eventually leading an international heat treat supplier company as CEO/president. He now serves the industry as a strategic advisor and partner to the C-Suite, as an engaged board member, through his consultancy, WDD Consulting, and in roles where he can make a positive impact. 

For more information: Contact Bill Disler at wdisler@wddconsulting.com 


The Evolution of Cleaning Technology in Heat Treating: Time To Rethink the Approach Read More »

A New Era: Tracking Quality Digitally

What are advanced management systems and how does deep integrative system management software help automotive heat treaters improve processes while saving on time and unnecessary expenses? Explore the future of software technology for the management of heat treating operations in this Technical Tuesday by Sefi Grossman, founder and CEO of CombustionOS.


The heat treating industry is on the brink of a technological transformation. Just as the momentous adoption of websites and emails transformed the nature of work for manufacturers, the advanced software systems are thrusting us into a new era of simplicity, automation, and deep integrations.

This article explores how advanced systems — an application of ERP (enterprise resource planning) and MES (manufacturing execution systems) combined with the power of AI — is revolutionizing facility operations, enhancing quality, efficiency, and profitability.

What Are Advanced Systems?

Advanced systems simplify, streamline, and automate operations by lifting the data burden off of plant personnel. While most existing systems focus on the part inventory workflow, more advanced systems go beyond by directly integrating into the heat treat process to track at bin/tray/tree level.

This requires real-time scheduling control, barcode scanning, digitizing recipe and process (no more paper), and direct sensor/PLC integration. Because of its critical nature, an advanced system is most likely an on-premise and cloud “hybrid solution” that is not crippled by internet connectivity issues. This allows it to still utilize rapidly evolving cloud systems that provide external services like messaging, big data storage, and AI to name a few.

Precise Processing

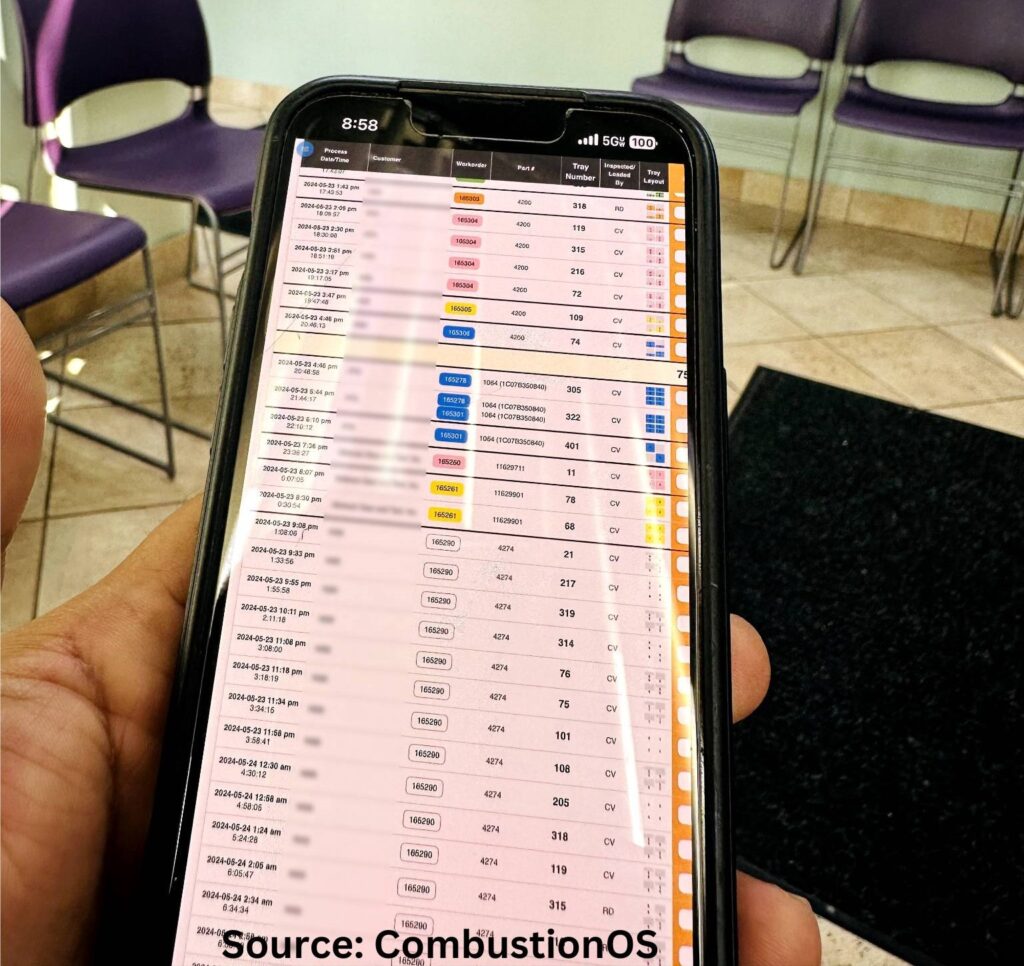
Figure 1. CombustionOS developers spend extensive time with operators and plant managers to create interfaces that are intuitive and easy to use. Pictured is access to job data stats from a mobile device being used outside of the manufacturing plant.

Repeatable, accurate methods to ensure optimal time, temperature, and atmosphere of the decided heat treatment processes are possible with advanced systems.

Utilizing existing sensors and hardware interfaces, data is collected in short intervals, transformed into meaningful data formats, and stored in a database. Network technologies such as HTTP, Modbus, and other analog to AI technologies make this possible with minimum additional hardware. The data is managed locally on the facility network, and synchronized with cloud services for further processing, analysis, and long-term history storage.

With a close monitoring of all these variables, facilities can tighten acceptable specification ranges. Deep integration with equipment ensures that data flows seamlessly from sensors and devices to the central system.

This real-time data collection and processing enables facilities to monitor operations continuously and make informed decisions quickly. For example, integrating data from temperature sensors, pressure gauges, and other monitoring devices ensures that all critical parameters are tracked and managed effectively. Additionally, if a temperature reading deviates from the acceptable range, the system can immediately alert the relevant personnel, allowing them to take corrective action before it becomes a critical issue.

 In addition to quality assurance, integrated artificial intelligence tools optimize job scheduling. Unlike traditional date/time calendar methods, AI systems predict job completion times based on real-time process data. This is particularly useful for roller furnace setups, where continuous processing occurs, but it is also beneficial for batch furnaces. Optimized scheduling improves resource allocation and operational efficiency, ensuring that jobs are completed on time and to the required specifications. The difference between a “calculation algorithm” and AI is that, with AI, you do not have to pre-program it. It automatically learns and adjusts for known variability in your hardware and even the personnel that are operating the equipment.

Finally, the automation of these systems captures and records all necessary information accurately. This reduces the risk of non-compliance, improving the overall quality of the final product. For example, a Detroit-based heat treating facility reported that accessing real time data to ensure compliance with industry standards has allowed them to spend 40% less time on documentation tasks.

Figure 2. Having increased control over the process gives more peace of mind to operators that components perform as needed.

Alleviating Burden on Maintenance and Inventory

Predictive maintenance is one of the most significant applications of AI in the heat treating industry. Traditional maintenance schedules are often based on fixed intervals, which can lead to unnecessary downtime or unexpected failures. AI driven predictive maintenance, on the other hand, uses real-time data to determine the optimal times for maintenance activities. This approach not only reduces downtime but also extends the lifespan of equipment.

A Detroit-based heat treating facility implemented an AI-driven predictive maintenance system (PMs) and saw a 25% reduction in equipment downtime. By analyzing data from critical parts, inventory, process tracking history, and various sensors, the AI system could predict when components were likely to fail, allowing the maintenance team to inspect and address issues proactively beyond their standard PMs. This not only improved operational efficiency, but also saved significant costs associated with emergency repairs and unplanned downtime.

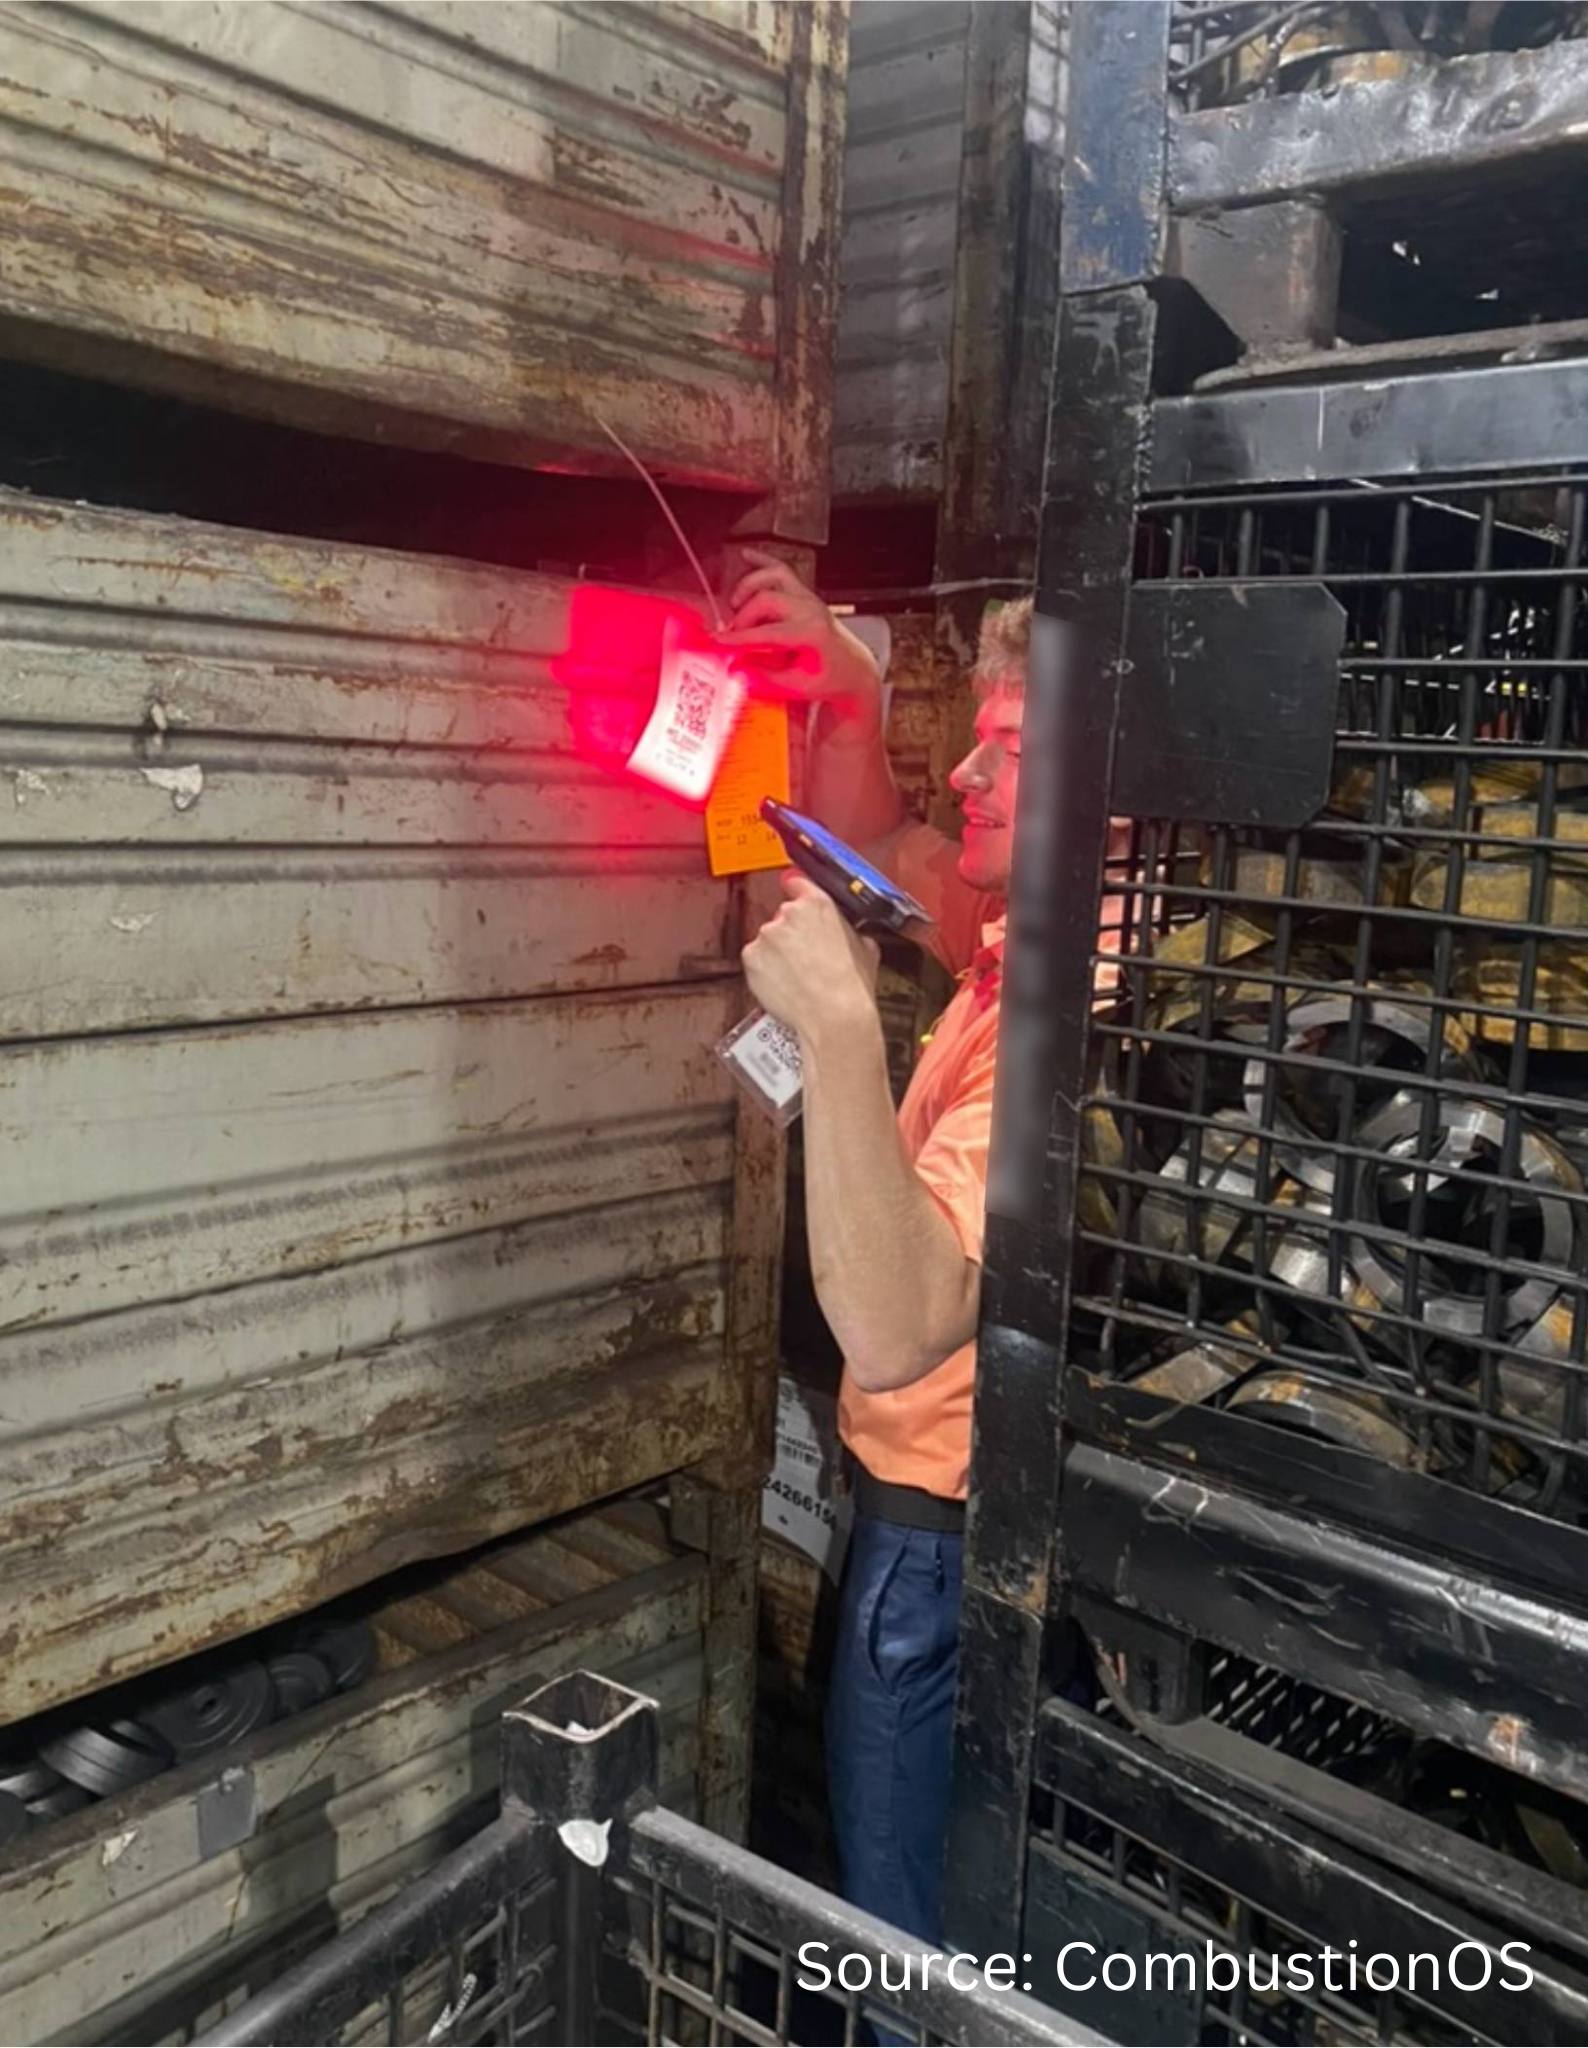
Additionally, the integration of QR codes for inventory and process tracking enables quick and accurate data entry compared to manual logging. For instance, when racking parts out of bins, operators can simply scan QR codes, which automatically update the system with the relevant information. This not only speeds up the process but also minimizes the chances of human error.

Reducing Operational Costs

The adoption of advanced ERP and MES systems has led to substantial cost savings for many facilities. These systems reduce operational costs through the implicit automated integrations that technologies like CombustionOS bring. Here are just a few ways that operational costs have been cut:

  • Decreasing shipping and receiving management from three to just one employee
  • Minimizing rework costs by timely process alerts
  • Reducing personnel by replacing constant manual oversight with accurate, digital tracking systems
  • Lowering administrative costs by utilizing a more efficient and accurate invoice automation platform

Case Study: A client reported comprehensive cost savings, including a 20% reduction in shipping and receiving time, fewer logistics and furnace operators needed, a 33% decrease in rework costs, a 15% savings in maintenance costs, and a 25% reduction in accounting overhead. These efficiencies translate into substantial payroll savings and improved profitability.

How To Implement

Figure 3. When racking parts out of bins, operators can simply scan QR codes, which automatically update the system with the relevant information.

One of the most significant advancements in heat treating technology is the deep integration with various equipment types. Unlike traditional ERP systems, which often lack true integration, advanced systems work backwards from equipment data, building ERP functionalities around this integration to ensure seamless and accurate data flow.

First, there are advanced systems that can handle data from both digital and analog sensors. So, for heat treaters who are juggling a variety of sensors and systems, looking for an integrative advanced system that has adaptability will ensure compatibility with existing equipment while keeping an eye on cost. Facilities can continue using their current equipment while benefiting from advanced monitoring and control capabilities.

Second, advanced ERP/MES systems can take collaboration with multiple vendors. Rather than uproot current systems and relationships, work with an advanced systems provider who is able to collaborate with other software and systems. Advanced ERP/MES systems provide comprehensive solutions that include deep equipment integration and full ERP functionalities. This approach reduces the complexity and cost of integration, ensuring that all components work together seamlessly.

Key Applications

Most operations in a heat treat department will benefit from advanced systems due to the time-saving automations that the system integrates. But many heat treaters are looking to adapt and integrate older systems and often more complex designs, like roller hearth furnaces. Here are some steps that experts will take to guide you through to make the digital integration smooth and effective:

  1. First, it is important to understand you don’t need to boil the ocean. Starting with a more advanced inventory tracking system that employs barcodes can set the underpinnings for a more integrated system while providing immediate benefits to your logistics.
  2. Then, it is also key to get a deep understanding of your current process and map out your operational workflow. Using a flowchart program helps
    visualize the process to make sure all stakeholders are on the same page.
  3. Some aspects of your current process are probably outdated (perhaps created by someone who is no longer at the company), while others are key to the core of how you operate. Understanding the difference is crucial to make sure you unlock potential automation without disturbing your core process and flow.
  4. You’ll then need to prepare every required form, document, chart etc. that you use in the operation. For process control, recipes, and lab testing, provide many parts/iterations to capture the complexity.
  5. Finally, take inventory of any existing digital systems you have adopted, like inventory tracking, spreadsheets, or custom software. The existing system
    network, including servers, Wi-Fi setup, and hardware (PCs, printers, scanners, etc.) will be utilized as much as possible in the transition to reduce the need to purchase and set up different equipment.

Conclusion

The future will require constant innovations and thoughtful leveraging of increasingly advanced systems. Unlike static, homegrown, or “pieced together” solutions, the most advanced systems are constantly updated with new features, ensuring they remain at the cutting edge of technology. Engaging directly with plant personnel to understand their needs and challenges allows systems like CombustionOS to evolve and improve continuously.

The heat treating industry is on the cusp of a technological transformation, driven by advancements in ERP, MES, and AI. These technologies offer the potential to enhance quality, efficiency, and profitability, making them essential for the future of manufacturing. By embracing automation, integrating advanced AI capabilities, and committing to continuous innovation, the industry can achieve new levels of operational excellence.

About the Author:

Sefi Grossman
Founder & CEO
CombustionOS
Source: Author

Sefi Grossman has been at the forefront of technology revolutions for the past two decades and has been leading the technology company CombustionOS for nearly seven years.


For more information: Contact Sefi at sefi@combustionos.com.


Find Heat Treating Products And Services When You Search On Heat Treat Buyers Guide.Com

A New Era: Tracking Quality Digitally Read More »

This Week in Heat Treat Social Media

Welcome to Heat Treat Today’s This Week in Heat Treat Social Media. We’re looking at hot summer events, hot summertime activities, and hot heat treat industry events coming soon to a social media page near you. Check out these posts, podcasts, and videos for a roundup in Heat Treat Social Media.

As you know, there is so much content available on the web that it’s next to impossible to sift through all of the articles and posts that flood our inboxes and notifications on a daily basis. So, Heat Treat Today is here to bring you the latest in compelling, inspiring, and entertaining heat treat news from the different social media venues that you’ve just got to see and read! If you have content that everyone has to see, please send the link to editor@heattreattoday.com.


1. Heat Treating Skateboards > Hot Moves

This space is usually reserved for something rich and technical, but it’s summertime in the northern hemisphere and heat treating is just as essential for the proper working of items affiliated with leisure and outdoor activities as the products that make the world go round (e.g., automotive, aerospace, etc.). “Skateboarding is not just a sport; it’s an art form, a mode of transport, and a way of life for many. But did you know that the metal trucks on a skateboard—those T-shaped pieces that mount the wheels to the deck—are a product of meticulous heat treatment?” (from Bodycote on LinkedIn, November, 2023)

Check out this recent post from Bodycote laying out how critical it is to safety and experience for skateboard trucks to be heat treated with the same level of skill that it takes to execute an ollie or a shuvit.

2. It’s a Beautiful Day in the Heat Treat Neighborhood

What’s everyone been up to on the social channels?

Summer Engineering Institute reshaping the Future of Heat Treating

Future Leaders: Report to the Dome!

Take Us Out to the Old Ballgame!

It may Be Summer but It’s Never Too Early to Think About the Fall

‘Tis also the season for Registration for 2024’s industry events and social media provides an excellent platform for getting the word out. Here are some of the events taking place just in September — don’t delay! Registration is still open for all of these!

Marking Milestones

3. Learn with Us

Sometimes, it’s the small things on social media that grab your attention or give you the “ah ha!” moment. And sometimes things affecting the industry in other places cause us to go “hmm.” Do any of these short posts make you say “eureka”?

Queueing and Sequencing (and more!)

Quiz Time

4. Open Your Ears: The Podcast Corner

You can’t read everything, we get it. Heat Treat Today is here to recommend two informative podcasts to enjoy on your daily commute!

Tune in to Listen to Heat Treat Radio #110! Isolated Heat, the Future of Vacuum Furnaces

smiling bearded man on blue background, HTR 110 logo, isolated heat text

Sharpen your hearing: Heat Treating Knives on the TTT Podcast

5. Junk Food and a Logo Extravaganza

Click through to see what Kowalski Heat Treating thinks about junk food and how that thinking gets them counting logos.

Have a great weekend!


Find Heat Treating Products and Services When You Search on Heat Treat Buyers Guide.com

This Week in Heat Treat Social Media Read More »

Green-toned electric socket photo bg w/professional headshot in fg

US DOE Strategy: Ramifications for Heat Treaters

As heat treaters strive for a sustainable future, pressure mounts to make the right choices while running commercially viable operations. In this Technical Tuesday installment of a continuing series, guest columnist Michael Mouilleseaux, general manager at Erie Steel, Ltd., explores the potential ramifications of the DOE effort for industrial decarbonization in the heat treating industry. The first installment, “US DOE Strategy Affects Heat Treaters”, appeared on April 10, 2024, in Heat Treat Today, as well as in Heat Treat Today’s March 2024 Aerospace print edition.

This informative piece was first released in Heat Treat Today’s May 2024 Sustainability Heat Treat print edition.


As regulatory agencies set industrial decarbonization goals aimed at achieving net zero greenhouse gas emissions (GHGE) by 2050, heat treaters should prepare for action. But where do heat treatment technologies stand today, and what is the path going forward?  

Background

President Biden’s 2021 executive order calling for a “clean energy economy” led the U.S. Department of Energy (DOE) and the Environmental Protection Agency (EPA) to develop “The Industrial Decarbonization Roadmap,” a strategic plan for reducing industrial emissions. The plan identified five sectors — chemical, petroleum, iron and steel, cement, and food and beverage production — as targets for mitigation efforts. According to “The Roadmap,” process heating operations within these five industries represent the greatest opportunity to apply what were established as four pillar technologies:

  • Energy efficiency
  • Low carbon fuels, feedstocks, and energy sources (LCFFES)
  • Carbon capture, utilization, and storage (CCUS)
  • Industrial electrification using green electricity

In May 2023, heat treating was specifically named as a target process for reducing GHGE during the DOE’s Office of Energy Efficiency & Renewable Energy’s Low Carbon Process Heating Forum.  

A Closer Look at the Technology Pillars

To determine the path forward, it’s important to understand where heat treatment technology stands today regarding the four pillars.

Energy Efficiency: Among energy efficiency opportunities are furnace insulation, controls, and burner design. According to furnace and controls manufacturers that I have spoken with, advancements in insulation and heating system controls offer less than a 20% opportunity in efficiency improvement over

LCFFES: In the U.S., the primary hydrocarbon fuel for heat treating is natural gas, which has an average (commodity) cost of $2.57/MMBTU. Hydrogen has been endorsed as the preferred replacement. Hydrogen manufacturing and distribution issues aside, hydrogen has a 2023 (commodity) cost ranging from $14.00 to $40.00 per MMBTU, and a carbon footprint of 30–130% that of natural gas. “Green hydrogen” is “under development.”

CCUS: Carbon capture, utilization, and storage is currently relegated to natural gas production operations where the captured CO2 is injected into existing wells to “enhance” production. Although the DOE suggests development of advanced CO2 capture technologies are still underway, a 2023 Congressional Budget Office report states there are “fifteen CCS facilities . . . operating in the United States . . . [with] an additional 121 . . . in development.” It is fair to state there are no CCS (carbon capture and storage) facilities currently operating on the scale of a heat treating operation.

Electrification: For electrification to be impactful, electricity must be generated via green sources. Currently, 40% of the electricity generated in the U.S. comes from natural gas, 20% from coal, 19% from nuclear, 10% from wind, and 3% from solar. It is my opinion that, regardless of the incentives federal and state governments offer wind and solar energy operations, they will not reach the scale — and most certainly not the reliability — necessary to achieve the stated 2035 GHGE goals.

Cost also must be considered. The average U.S. cost for electricity was $0.086/KWH in 2023. In California, however, the cost for electricity generated with 40% renewables was $0.1819/KWH. In Germany, it was $0.289/KWH with 55% renewables. To put this into perspective, today the differential in (industrial) electricity (commodity) costs demonstrably increase as the percentage of that electricity is generated by “green” sources. To think that this trend is going to be reversed by federal mandate is paradoxical.  

A Realistic Look at the “Road Map”

While industrial decarbonization targets called for an 85% reduction in GHGE by 2023 and net zero by 2050, the goals seem unreachable using currently available technology. Replacing natural gas with hydrogen will result in significant cost increases as the commodity is 5–15 times more expensive, the equipment will require retrofitting to accommodate hydrogen, and the national infrastructure will need to be modified for hydrogen.

Electrification of existing gas-fired processes will result in a cost increase of four times, according to DOE estimates; however, based on today’s cost trends, 7–9 times higher is more likely. Additionally, the cost of converting equipment to electric operation must be considered. Mitigation efforts suggested by the DOE include improvements in efficiency that rely on yet-to-be-developed technologies and cost reductions in electricity facilitated by the wholesale use of renewable energy.

Overall, decarbonization efforts are noble. The timeframe and methodology, however, are unrealistic as they are based on the use of still-conceptual technologies.  

What Can Heat Treaters Do?

Following the lead of the automotive industry may be key. This sector reacted to the government mandates for GHGE reductions by going all in for electrification — with projections of 50% electric vehicles by 2030. A funny thing happened; these vehicles were not wholly accepted by the American public. The auto industry, led by the dealers, with the support of the UAW, and the car manufacturers petitioned their U.S. Representatives to “pause” these requirements. This political pressure caused the EPA to roll-back the implementation schedule.

Heat treaters must act now with a similar effort, but it must be aimed at preventing the promulgation of regulations that rely on still-conceptual technologies within an unachievable timeframe. Contact your local government leaders; let them know what we do means jobs and tax revenues. Contact your U.S. Representatives and Senators to let them know heat treaters are critical to our national security, the transportation system, and, in fact, the infrastructure of this country. What we do should not be outsourced, and we need to be given all the considerations of a critical industry.

The next column in this series will address the role of process heating in GHGE, analyze DOE assessments of GHGE for industry and process heating operations, and propose a fact sheet intended for use in our effort to set a realistic timeline for decarbonization goals In the next column, we’ll address potential ramifications of the DOE effort for industrial decarbonization in the heat treating industry to help you be better informed and prepared.    

About the Author:

Michael Mouilleseaux General Manager at Erie Steel, Ltd.

Michael Mouilleseaux is general manager at Erie Steel, Ltd. He has been at Erie Steel in Toledo, OH since 2006 with previous metallurgical experience at New Process Gear in Syracuse, NY, and as the director of Technology in Marketing at FPM Heat Treating LLC in Elk Grove, IL. Michael attended the stakeholder meetings at the May 2023 symposium hosted by the U.S. DOE’s Office of Energy Efficiency & Renewable Energy.

For more information: Contact Michael at mmouilleseaux@erie.com.  

Attend the SUMMIT to find out more about the DOE’s actions for the heat treat industry.

Find Heat Treating Products and Services When You Search on Heat Treat Buyers Guide.com

  1.  

US DOE Strategy: Ramifications for Heat Treaters Read More »