At Heat TreatToday, we want to make sure everyone in the North American heat treat industry is well informed so they can be happier and make better decisions. With that in mind, we have been growing our library of Spanish heat treating content.
Below, click the blue headings to learn from Víctor Zacarías about pyrometry standards in the aerospace and automotive industries, from Carlos Carrasco about selecting heat treating equipment, from Bill Munn about leadership and motivation, and from Erika Zarazúa about CQI-9's probe method A. If you'd like to view this content in English, click the America flag icon.
Víctor Zacarías General Director Global Thermal Solutions Mexico
"Las operaciones de tratamiento térmico son percibidas generalmente como cajas negras cuyos resultados son poco predecibles. Si bien, entendemos los mecanismos físicos involucrados para modificar las propiedades de un material, los hornos de tratamiento térmico son sistemas termodinámicamente imperfectos, y por ende los resultados finales en ocasiones también lo son."
Contact us with your Reader Feedback!
"Heat treatment operations are generally perceived as black boxes whose results are not very predictable. Although we understand the physical mechanisms involved in modifying the properties of a certain material, heat treatment furnaces are thermodynamically imperfect, and sometimes the final results are too."
This article first appeared Heat Treat Today's March 2022 Vacuum Furnace print edition.
Carlos Carrasco Founder Carrasco Hornos Industriales
"Este artículo ayuda a los ingenieros a comprar equipos de tratamiento térmico. Hay muchas razones para seleccionar cuidadosamente los hornos industriales. Uno, es el costo del horno en sí y otro, es que el producto que se está tratando térmicamente afectará los resultados de su empresa."
"There are many reasons to select industrial furnaces carefully. One is the cost of the furnace. Another is realizing heat treating will affect the product and the bottom line. There is more specialized engineering in heat treating equipment than is apparent from the outside."
This article first appeared in Heat Treat Today's November 2021 Vacuum Furnaceprint edition.
Bill Munn Leadership Coach Bill Munn Source: Bill Munn Coaching
Por definición, de aquí se desprende que no se desempeña solo; es más, está posicionado no solo para trabajar en conjunto con otros seres humanos sino también para liderarlos; si su potencial se ha de realizar, puede que ya haya entendido bien que en esas personas reposa la verdadera clave del éxito que a futuro pudiera conseguir ¿Cómo, pues, lograr su compromiso?
By definition, this means that you are not functioning alone. Moreover, you are positioned not only to work with fellow human beings, but to lead them. And if your potential is to be realized, you may already know well that those people are the true key to your future success. So how will you engage them?
This article first appeared in Heat Treat Today's September 2022print edition.
Erika Zarazúa Regional Purchasing Manager Global Thermal Solutions México Source: Global Thermal Solutions México
"Las pruebas SAT deben realizarse a todos los sistemas de control, monitoreo y registro de los equipos de procesamiento térmico. Esto no aplica para los sistemas de ‘alto-límite” cuya única función es la de proteger al horno de un sobre calentamiento."
"System Accuracy Tests (SATs) must be performed on all control, monitoring, and recording systems of thermal processing equipment. This does not apply to “high limit” systems, whose sole function is to protect the furnace from overheating."
This article first appeared in Heat Treat Today's August 2022 Automotive print edition.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
The monthly Industrial Heating Equipment Association (IHEA) Executive EconomicSummary this September reiterates the point that it has been making for several months this year: economic growth plus negative economic indicators equals “I don’t really know” what will happen in the economy.
Industrial Capacity Utilization Source: IHEA
First, the summary takes time to look at contradicting economic indicators. The first example is in GDP growth: While Q1 and Q2 exhibited persistent negative GDP growth, Q3 projections of 1.3% positive growth is a promising sign that the threat of a recession is starting to fade. Other indicators also show borderline economic stability and possibly growth; with unemployment rates being low and seeing capacity utilization numbers in normal range and the Purchasing Manager’s Index in expansion zone (both just barely), “there are as many factors suggesting recession as there are factors that point towards slow growth but growth, nonetheless.” The economic summary projects the following in this borderline hopeful situation: “My own analysis of the situation (for what it is worth) is that the US will escape a formal recession in 2022 or 2023 but will experience a downturn of some significance as compared to where we were in 2021.”
Purchasing Managers’ Index Source: IHEA
Second, the summary evaluates the causes for inflation, a hot topic and a very visible, uncomfortable sign. We’re looking at three variables for this assessment: lockdowns, the energy crisis, and reshoring. “The estimate,” relates the economic summary, “is that the lockdowns cost upwards of $10 trillion in lost wages, shuttered business, health care costs and the like. The $800 billion [in U.S. stimulus money] did not offset the economic loss and was therefore not inflationary. There was a surge in inflation in early 2021 as the restrictions started to lift and people started to spend again but most of that pressure had dissipated by Q3. There would have been reduction in inflation pressure had there not been other factors.” The next cause for inflation, the energy crisis, was caused by the War in the Ukraine since Russia’s invasion of the Ukraine effectively cut off the world’s second largest producer of oil from the global economy. The energy crisis and inability to access many goods after shutdowns and wartime supply chain disruptions has also led to much reshoring in the U.S. With reshoring — an indication of growth — comes near inevitable price increases at the expense of more secure supply chain lines: “As companies return to the U.S., they will naturally encounter higher costs – for labor, for land and the like. They will see higher regulatory costs and will encounter more limits. These will add to the costs even as these companies benefit from a more reliable supply chain.”
Anne Goyer Executive Director IHEA
Check out the full report to see specific index growth and analysis which is available to IHEA member companies. For membership information, and a full copy of the 11-page report, contact Anne Goyer, executive director of the Industrial Heating Equipment Association (IHEA). Email Anne by clicking here.
Today’s episode revolves around gun parts: How are they heat treated? How many gun component manufacturers are there in the U.S.? Doug Glenn, publisher ofHeat Treat Today and host of this podcast, and Steve Kowalski, president at Kowalski Heat Treating, dive into this topic and what it takes to heat treat gun parts.
Below, you can watch the video, listen to the podcast by clicking on the audio play button, or read an edited transcript.
The following transcript has been edited for your reading enjoyment.
Doug Glenn (DG): Well, welcome to another episode of Heat Treat Radio. I have the immense pleasure of being able to sit down today with Steve Kowalski of Kowalski Heat Treating. Steve, you know, it’s nice to finally sit down with you. We’ve been talking for quite some time about doing this, so first off, welcome to Heat Treat Radio.
Contact us with your Reader Feedback!
Steve Kowalski (SK): Well, good morning, Glenn. Thank you very much for having me today.
DG: You are very, very welcome. Now, we have to start, as I told you before hit the record button, over your left shoulder there is an interesting ball. You need to tell us about that real quick.
SK: Can you see it?
DG: Yes, yes, we can see it.
SK: For you and folks at home, this is a rubber band ball. For perspective, how’s that? It’s twenty-two plus years in the making.
"For you and folks at home, this is a rubber band ball. For perspective, how’s that? It’s twenty-two plus years in the making." -Steve Kowalski
DG: For those of you who are on the audio only version, it’s about the size of a basketball. Steve was telling us that you guys [Kowalski Heat Treating] have been using only the stuff that comes in the U.S. mail. It’s very impressive. It has nothing, absolutely nothing, to do with heat treating, but I did want to say that it’s pretty interesting.
Anyhow, Steve, we’re going to talk a little bit today about the heat treatment of guns, ammo, and that type of stuff. That’s just to whet the appetite of those who are listening and watching; that’s what we’re going to be talking about a bit, your organization does it.
But I’d like to have you take a minute just to talk about your background, very briefly. I know that it’s a long, long background . . . . ~chuckle~
SK: Careful, careful!
DG: Yes, I know! Trust me, you and I graduated from college the same year, so I know. So, it has been a long background. But briefly, tell the listeners/viewers about you, about the company, and then we’ll jump in with some questions about firearms.
SK: Wonderful. I’m second generation. My dad started the business back in 1975, so I was underage working, yes. Those of us in the commercial heat treat, a lot of us have grown up in businesses where we were the underaged employees. The transition took place about 15 years ago. We started off with one building, roughly 3,000 square feet, to process tools and dyes. Back in the day, Cleveland was one of the tool and dye capitals of the world- we had tons of tool and dye makers. Well, that business has evolved away.
Since 1975, we’ve grown the business to now having nine facilities on our campus, roughly 80,000 square feet, and those of you who know Kowalski Heat Treat, we specialize in those PIA jobs — it’s what we do. If it’s a problem, it’s pretty sure that it’s going to be coming to our facility.
We started in salt bath. Over the years we added high pressure quench vacuum processing, plasma nitriding, plasma nitrocarburizing, heat pyrogenics. One of our divisions specializes in nothing but keeping parts flat- round and flat. You can go to our website at KHTE.com and check out the various divisions and what we do. Basically, in our world today, we rack or assemble 95-97% of everything that comes through this door — it’s specially handled.
DG: The PIA, the “pain in the ass” ones is what you’re talking about. Do you guys have, therefore metallurgists and things of that sort on staff, as well, I assume?
SK: We have 48 people, we have 8 engineers on staff — anything from chemical to mechanical to electrical. We do not have any metallurgists on staff. We have access to great metallurgists in the area.
DG: Cleveland has them.
SK: Oh, my gosh, we actually are blessed here in Cleveland. If you need something — one phone call and we can find it.
You’re from Pittsburgh, aren’t you?
DG: Yes, just north of Pittsburgh. Don’t hold that against me.
SK: No, no, it’s okay — you’ve done remarkably well. ~chuckle~
DG: All things considered, there you go. I appreciate that. How very gracious of you, Steve!
SK: Oh, my pleasure.
Kowalski Heat Treating is a family company. Source: Kowalski Heat Treating
DG: You’re right, though. Cleveland, I think, especially. Ohio, in general, but Cleveland, in general, are kind of like the forging center of the world. There’s just a lot that goes on there. But heat treat, in between Detroit and Cleveland, it’s kind of “heat treat central.”
Well, listen, that’s great. You’ve obviously been very successful. You’re good at what you do. I know it’s still a family business --- you’ve got you and your sister, at least, involved, right?
SK: Sisters, yes, correct. Two sisters are involved: one in the back office and Peggy Andrews is inside sales customer service. You’ve met Peggy.
DG: We’ve met Peggy; we know Peggy. Peggy is wonderful.
SK: And for all of you listening — I’m the quiet one in comparison.
DG: I believe that, now. I’ve met Peggy and she’s great.
Also, you’ve been a little bit humble because you were the president of the Heat Treat Society not too long ago, were you not?
SK: Yes.
DG: Which is quite an honor.
SK: Before me was Roger Jones and after me was Jim Oakes.
DG: Let’s talk firearms for a second. You know, it’s kind of interesting, because when you talk firearms, it’s always a little bit controversial. Obviously, there’s a political side to this conversation. We don’t really want to go down that road too much because we’re just going to talk about heat treatment. But I do want to ask you, which could be slightly bumping up against the political side: Have you seen, recently or in the recent past, any increase in that business that Kowalski is doing as far as firearms go?
"Well, in our firearms business (and I know we’ll be talking about the who, what, where, when, why of firearms and how processing is incredibly important), we work with the DOD (Department of Defense) and very unique programs, we work across the spectrum in the firearms from long guns to handguns and there seems to be a huge misconception in the world on firearms. ATF controls that world from the registration standpoint."
SK: Well, in our firearms business (and I know we’ll be talking about the who, what, where, when, why of firearms and how processing is incredibly important), we work with the DOD (Department of Defense) and very unique programs, we work across the spectrum in the firearms from long guns to handguns and there seems to be a huge misconception in the world on firearms. ATF controls that world from the registration standpoint. Every firearm has a serial number (certain components of it) so it is tracked. Our systems have evolved over the years — we’ve developed specific systems that are very sophisticated to be able to track the product that we process. The key components that require serialization or a serial number — we track them. We do hundreds of thousands of units a year, and they’re all tracked so that you and I can go across the political side. We’re really very, very proud of the fine work that my team does in the firearms industry. Most of our first responders, law enforcement, defense — they require and depend on what we do. I can make it very dramatic, but in reality, if we don’t do our jobs correctly, they can’t do their jobs correctly.
DG: Yes. And it’s somewhat of a life and death thing, too. I mean, if you’ve got malfunction because of a defective heat treat, or for any reason, it can be an issue.
SK: Our business has definitely grown in the last seven years. We’ve built a very good reputation in this industry. If you have a problem, chances are we’re going to be working with you to help you solve your problem. Firearms are extremely highly engineered with very tight tolerances.
DG: It’s kind of interesting, here, because you’re talking about serialization of parts and things of that sort that come in; you’re not getting fully assembled guns — you’re getting parts and pieces. So, you’re able to track— I’m curious, is that tracking a barcode, is it optical — how do you do it?
SK: The answer is “yes” to all of the above. It depends on the customer. If you have a sales agent, you have a serial number or you have a code and, in some cases, some of our customers are moving toward QR codes. So, if you receive in 10,000 units, whatever they may be, well that’s 0 to 10,000 and you need to ship 0 to 10,000 back. If you do not, ATF is notified.
DG: That’s interesting. Types of furnaces: Are you guys running batch furnaces or are you running continuous furnaces?
SK: We do batch. The majority of what we process for the gun world, for the firearms world, would be either salt to salt rack austempering or marquenching, vacuum and actually plasma processing, whether it’s FNC or nitriding. Those three areas, we’re involved with the gun world.
DG: Yes, I was curious, because you hear a lot about, especially. It’s a different market, but in the faster world, you hear fallout. If you’re going through a mesh belt furnace, you know, “Oh well, you lost a few fasteners down on the bottom of the furnace.” That would not work in your . . . .
SK: I can make light and we joke a little bit about it, but you do not want folks with three letters on the back of their coat coming in.
DG: Exactly. If that happened, probably the next interview we’d do with you, you’d be wearing an orange suit and maybe you’d have a roommate.
SK: And I just don’t look good in orange.
DG: So, now, as far as the firearms industry, there are a lot of different metals and materials of that sort, but there are two basic things — I mean, I always talk about it and we talked about this a little bit before we hit the record button: There is ammunition and then there are gun components. You guys do not do ammo, correct?
SK: Correct. That is not a world we’re in. We are in the gun side — all of the components for guns. On any given firearm, you may have, in our particular case, we may be processing 12–15 different components for a handgun — anything from a barrel to a slide to a receiver to a firing pin, ejectors, extractors, triggers, trigger guard — the list goes on. It tends to be a different material; there are different properties that they develop that they need a firing pin versus a trigger guard versus a slot.
DG: Just a quick example if you don’t mind. It’s important for the heat treater to know what they’re doing, obviously, right? Why is that? Can you give us an example of why it is?
On any given firearm, you may have, in our particular case, we may be processing 12–15 different components for a handgun — anything from a barrel to a slide to a receiver to a firing pin, ejectors, extractors, triggers, trigger guard — the list goes on. It tends to be a different material; there are different properties that they develop that they need a firing pin versus a trigger guard versus a slot.
SK: Well, when you say “a barrel” is true. If a barrel is not “true,” straight, no distortion. We’ve all seen various TV shows where the person swings the gun around and the bullet shoots around the corner. No. Doesn’t happen. So, if the barrel isn’t true and hasn’t been processed appropriately and correctly, it’s not going to function the way it was designed.
A firing pin, which is a very distortion-sensitive component- if it’s bent, it doesn’t work. The gun will not fire. We could go on: slides and receivers. If they’re distorted, they’re not going to work. It’s not going to function. So, each component must be processed to achieve dimensional tolerance control. And then metallurgically, the structure: A gun has a very aggressive action.
DG: Mini explosions, basically.
SK: Literally. And so, it’s been designed to support all of that.
DG: The different components that I think about are the firing pin you were mentioning, right? It’s going to have a lot of impact on the shell casing on the firing pin.
SK: In that particular case (and we’re not giving any IP away), but those are austempered for structure. Doug, are you a metallurgist?
DG: No, I am not, actually.
SK: Nor am I. I’m a marketing guy, folks, with experience.
DG: Same here, same here.
SK: The design — if that pin chips, cracks, breaks, it doesn’t fire.
DG: Exactly. So, you’ve got the high impact parts like the firing pin, you’ve got barrels where you want good wear resistance and things of that sort and, obviously, they need to be true and straight. You’ve got springs in a lot of guns, especially your Ruger style where the receiver’s back — those things have to be heat treated appropriately.
Steve, what type of alloys typically are we talking about in some of these different parts?
SK: They range from high carbon materials (1050, 1060, 1070) up to high temp stainlesses, whether it’s 400 series, whether it’s a precipitation hardened series, mid to high alloy materials (4340, 4150) and then, as we get into the specials, the engineering world is continually trying to make a better product- a longer acting product, a more robust product- so we’re starting to see materials that, historically, weren’t used in this area. Plus, things that we don’t deal with, there are many components that are carburized using 8620, 9310, carburized and hardened, for the same purpose: wear and performance.
DG: Being in the Cleveland area, you are kind of in another hub and that’s where a lot of this 3D printing, additive manufacturing; I mean, there’s a lot that goes on there. I think there’s an organization in Youngstown, or in that area, that’s kind of a central hub there. Are you guys seeing any of that, whether it be in firearms or not? Have you had any experience with any of the AM?
SK: The answer is yes. AM is absolutely taking place; it’s incredible. The technology — what you can do today that you couldn’t do two or three years ago and then you have to effectively engineer backward forward, make it, and then make it right, then produce it, thermally process it (maybe); so, it’s one of those.
DG: It’s an interesting and evolving technology.
As a heat treater of gun components, not that you want to help any competitors or anything of that sort….
SK: Heck no, we love all of our competitors who are not working against us, how’s that?
DG: That’s fair enough, that’s fair enough.
As a heat treater, what are the things that jump into your mind that you have to be careful about when heat treating gun components? And if it helps, pick a specific component, whether it be a pin, a barrel or whatever. What do we need to be careful of?
SK: I’m looking up over your head (which is beautiful, by the way) at the sky here in Cleveland, Ohio. The way I’m going to answer this is this: You are dealing with a component that, if we take guns out of it and, say, use medical devices. We’ll use medical devices in lieu of saying guns so people can appreciate where I’m going with this. You have bad players out there — people who are trying to circumvent the system. With medical devices, you need to have approvals — you need to have FDA. It’s very similar in the gun world- you need approvals, you need make sure that they’re making components that comply with, whether it’s the OEMs’ specification or ATF specification being sterilization (making sure things are marked appropriately). Internally, here, we have secure quarantined areas where we do all of this work. Your personnel — I have to be approved to be able to process these parts. My background has to be checked.
This company, my company, approves those people who can touch these components. Internally, we have secure, bonded areas. Parts are bonded in and they are bonded out. Use the terminology you like, but basically, you’re securing from our floor to an area because it is that important. If we’re dealing with the aerospace world or nuclear world, you are going to make sure your systems and processes and procedures are all locked down.
DG: So that’s a procedural, operational uniqueness, let’s say, to handing guns. How about technically? Like in the aerospace industry, you’ve got NADCAP, in automotive you’ve got, you know, in aerospace still you’ve got AMS for pyrometry, CQI-9 and things of that sort. The medical industry, which you mentioned, Steve, has MedAccred and things of that sort. Any such beast in the firearms? I haven’t heard that there is.
SK: Basically, we have overlapped between our guns and gun industry as a whole with the DOD work that we do, so we go back and forth. What you mentioned here, most of those requirements and procedures are already in place. It makes it easier if you’re doing CQI-9 relevant work, you’re not going to start and stop. So, the equipment is already covered in those areas. The procedures — you build them so that you’re not building fourteen different procedural systems. It’s difficult to control.
DG: You’ve already kind of answered this but let me just ask it straightforward just in case there’s something else, and if there’s nothing else, that’s fine. For the people in your company and for you guys, generally speaking, is there any specific training or knowledge or experience that you have to have to be heat treating gun components?
SK: Yes. And those are: one, experience is an incredible teacher and often times. For Kowalski Heat Treat (I can’t speak for competitors, I’ll speak for us), normally, if a product hits our floor, hits our dock, hits my inbox, historically, somebody has had a problem with processing that component — whether it’s distortion, whether it’s metallurgically the properties they’re achieving, whether it’s actually out in the field — you’re my favorite, you’re my test. You’re going to call and say, “Hey, Steve, I got this thing and I’m not happy with its performance and I need to improve its performance. What can we do?” Then you start the entire investigatory process of what have you done, what have you achieved, did you actually test or are you just feeling that what you’re telling me is you’d like to have something better but you don’t know what? So, we have a design team here that will work very closely with your folks to help design a better process, a more robust process. If we’re talking to the general industry, as we are right now, I think we can all agree that the quality and consistency of the materials that we are receiving in today are dramatically different than they were five years ago, eight years ago, ten years ago.
SK: Worse. Worse being not as consistent as they were. Yes, we all have that grade A and four of us will process grade A today and we will get result B. Next week you’re going to get B-, B+, possibly an A, maybe a C.
We’re joking internally, but the first thing most heat treaters do — because, quite frankly, we’re paranoid; the entire world is out to get us and it’s always the heat treaters fault. . . . It’s always our fault. So, the first thing we do when enter into a relationship is we say, “Doug, hi, I’m Steve. I’m sorry.”
DG: Get that out of the way, start out that way.
SK: Then we move forward from there. But that has been a serious challenge on the consistency of the materials coming to us.
DG: So, you guys test all incoming material?
SK: Yes. And don’t use the word “all.” But yes, we have an inspection and we work closely with customers. As you get your material in, send it to us. Before you start making a product, send us something that we will process and validate for you so that you know that what you’ve got will respond the way you thought it’s supposed to respond. Then, we can move forward being more efficient with that.
DG: You’ve hit on this before, too, but I just wanted to see if there are any other comments that you want to make on this and that is the type of equipment that is necessary for doing the heat treating of these gun components. I know you mentioned salt, so you’re in a salt bath, right?
SK: Salt neutral hardening, salt hardening, and then marquenching or austempering, depending on the component. It’s critical. There are a significant number of parts that respond extremely well to rack austemper, rack marquenching. Extremely well. And we’d probably say that our team here, they’re spectacular. I get to talk about it which is really pretty cool. Hey, I’ve got these great people with me that do this great work, and they do! Their job is to make me look good. As you know, your support staff, yes, don’t even say it, I know it’s a fulltime job, it’s never done . . . . ~chuckle~
DG: You took the words out of my mouth! ~chuckle~
SK: So, salt is critical in this industry. Vacuum processing.
DG: Why did you go vacuum, by the way?
SK: With stainlesses and the various materials that we’re currently using, having high pressure quench vacuums/high pressure quench, it allows for a significant amount of flexibility. We can finetune a recipe, or cycle, to achieve properties that the customer needs where it makes it repeatable.
DG: And you’ve got, what, how high pressure? What bar are we? Ten bar quench?
SK: Yes.
DG: So, you’ve got salt to salt, you’ve got high pressure gas quenching coming off of a vacuum heat treat. Anything else?
SK: And then we do plasma nitriding. I will say that we have the technology we have utilized to optimize processing. Is ours the best for everything? Absolutely not. No question about it. And when it’s not, we’re going to say, “Hey, Billy, I need you to call Doug and I need you to tell Doug that Steve said to call him and ask the following three questions. Doug’s got the answer for you.” And your equipment for his application is better than mine; it works best. So, I think anyone in the heat treat world can recall the scars on our backs from the days that we thought we could give you exactly what you need [indiscernable]. It’s not the best answer.
DG: Do you do much heat treating of gun components in straight atmosphere or air furnaces?
SK: We don’t have them.
DG: You don’t have them at all. And do you do induction?
SK: No, not yet. No oil quenching here whatsoever. We’re here in Cleveland in a residential area and we are zero quantity generator of hazardous waste.
DG: Nice. I’m sure your neighbors appreciate that.
SK: Oh, they absolutely do.
DG: If they know.
SK: Oh, they do.
We know what we’re really good at and that’s our work.
DG: A couple more questions on this. We talked about the uniqueness of heat treating gun components because of the traceability and the serialization and all that stuff. Is there anything else technically unique about the heat treatment of any of these gun parts that kind of make them interesting or more of a challenge?
SK: Yes. Have you met my wife?
DG: I don’t believe that I have.
SK: There is a comment that she tells me all the time: Everything that goes through my mind doesn’t have to come out my mouth. She’s incredibly wise and way smarter than I am!
In the heat treating world of gun components, one of the areas that would be critical is it is not a bulk processing world. It’s not about running more and more and more parts at one time. You will not get optimum results. It’s a sensitive process. We’re heat treaters and we’re very sensitive with what we do.
But distortion is critical. The way the parts have been designed, you cannot effectively, in my humble opinion, put them into a 2436 or 3648 basket and max load it — you will not get optimal results. It’s not going to happen. So, there is a tremendous amount of racking.
"In the heat treating world of gun components, one of the areas that would be critical is it is not a bulk processing world. It’s not about running more and more and more parts at one time. You will not get optimum results. It’s a sensitive process. We’re heat treaters and we’re very sensitive with what we do." - Steve Kowalski, Kowalski Heat Treating
DG: That, actually, was my question: Not that you would know this number right off the top of your head or anything, but the percentage of time spend racking, I assume, is higher.
SK: It’s 2:1, 3:1, 4:1, 5:1.
And, for those of your listeners who understand salt processing, we can rack for two days and process for an hour/two hours.
DG: Let’s say it’s just manually intensive, then.
SK: We have an incredible team of individuals here who do things that, if you watch, you’re just like…. In some cases, it’s truly awe-inspiring because they create for us success. They help us learn new ways of processing. It’s not, hey, you’re going to do it the way Steve says. Critical process control, but they provide us the answers on making things better.
DG: I’ve got two other quickie questions for you. We may have already covered them. One was just if there is any common mistakes? I know you guys don’t make mistakes, but . . . .
SK: Heat treaters do not make mistakes!
Source: Kowalski Heat Treating
DG: That’s correct. But is there any common mistakes with the heat treatment of gun components? Because, if you guys really are, as you say, the people that are taking care of the PIA jobs, it’s usually coming from people who have made a mistake.
SK: Yes. It’s when to say no. You and I have talked and we’ve talked to our peers — they’re brilliant people. We tend to all lament, usually, the same thing. Something comes in and it’s not quite right or correct and we don’t say, “Stop. Doug, you did not make this correctly. We can’t do what you want us to do because of you’ve provided to us.” Or the next step would be folks who assume.
But the rest of it is process control. Once you develop, you rock the process and when you do that, the only real big issue we’ve run into anymore is consistency of material coming in.
DG: I’ve heard, and I want to be careful, and we may have to edit this out, but you mentioned incoming material specs being an issue, the consistency of the material coming in. I have heard that a lot of times the inconsistency in that material is coming in from overseas, let’s just put it that way, and not necessarily Europe.
SK:Far overseas.
DG:Far overseas. Let’s just say far to the East overseas. I guess my question is: Is that still the source of it or are you seeing less issues with that?
SK: Because of what we’ve run and because of the customers that we’ve worked with, historically, that hasn’t been a big problem — not in this market. Although there is high volume, it’s not a tremendous amount of weight. It’s more of the chemistries, the supply chain. We’re hearing it. Part of it is frustrating stop saying supply chain when your guy just didn’t show up and do his job. But, as heat treaters, we will say, we have to be very diligent in contract review. There is mentoring of our younger employees, customers mentoring their younger employees who don’t have the knowledgebase, yet, to understand what they’re actually working with. It’s not a disparaging comment — you learn from making mistakes. You absolutely learn, and that’s experience. So, we’ve seen a talent drain in the last few years. And that is exacerbating the problem.
DG: Right now, you’re doing heat treatment of gun components. Obviously, I’m not going to ask you company names because that wouldn’t be the right thing to do, although it would be fun to do, but it wouldn’t be the right thing to do. But are you pulling in business, let’s say, from pretty much nationwide?
SK: Yes. We don’t get a significant business from overseas. This is due to transportation challenges. Plus, it’s part of our continuous supply chain worth being manufactured, let’s just say, in England, and then ship it to the states to do X, Y and Z, and it ends up being assembled in some state in this country. But as far as countrywide, continent-wide: yes, we’re all over the country.
DG: Do you think the normal guy, like myself (I’m going to classify myself as a normal guy, in this case), would be surprised at the number of gun component manufacturers in this country?
SK: Yes.
DG: Because when I think of gun manufacturers, I’m thinking there are maybe a half dozen to a dozen at most.
SK: Try a different number.
DG: Try a different number — maybe add or multiply that. See, I don’t know!
SK: We’ve been very fortunate that we’ve attended and been at the SHOT show; it’s been held in Las Vegas for the last number of years. You get a better perspective attending that. Now, you have to be approved to attend it, and those who have understand where I’m going with this. There are a number of manufacturers in this country. And we’re not talking about folks who . . . . I’m a family business — we are a family business; we have 45–48 people. We are a small business. I’m talking about companies with hundreds of employees that you’ve never heard of that make components and guns and support that industry.
It’s a significant industry and, by and large, without getting into the politics of this, some of the nicest people we have ever met — truly just generous. I’m talking about even purchasing agents! (For those of you who have dealt with purchasing agents in industries that we will not discuss that have four wheels and an engine!) They’re basically decent people. It’s fascinating.
DG: It kind of rocks your world when a purchasing agent is a real person. It’s like, Oh really, they have heart.
Well, listen Steve, congratulations. It sounds like you guys are doing great work there. I know that you guys do more than guns. Do you care to share, just briefly, what else you do?
Rolls, slitter blades racked, and SS valve seats for vacuum processing Source: Kowalski Heat Treating
SK: Those that know the company, when we say PIA stuff: if it’s a problem, it’s coming to us. Distortion sensitive. We have a significant market in power transmission, clutch plates, brake discs, big round flat things, visually, from three inch in diameter to 50 inches in diameter — that’s our world. You name the market: power transmission, auto . . . . We don’t do much in the aerospace industry; it’s just not something that my people and I want to deal with. Other than that area, medical, nuclear, Department of Defense. We do a significant amount of research and development where folks like you say, “Hey! I have an idea! Can you help us?” and we assist them on the metallurgical heat treat side on building processes. Outdoor power equipment. Basically, if you have a problem, I’ve got 10 guys for you who are incredible at what they do. We just like having problems. I’m telling you how we work: If I can solve your problem, if our team can solve your problem, are you going anywhere else?
DG: Exactly right. Nope, not going to do it.
SK: And we like to try and have fun doing it.
DG: Yes, that’s right. Get the work done and enjoy it if you can.
Steve, listen, I really appreciate you being here, I appreciate you talking to us a little bit about guns and ammo, I guess mostly gun parts. And, again, congratulations, it sounds like you guys are doing well. We appreciate your insights.
SK: It’s a pleasure, an absolute pleasure. Thanks, Doug.
GHH Series Box Furnace for Ceramic Matrix Composites Source: L&L Special Furnace Company, Inc.
A U.S. manufacturer with a plant in the Midwest received and commissioned a large high-temperature box furnace for processing ceramic matrix parts that will be used in military and aerospace applications.
L&L Special Furnace Company, Inc.'s GHH3350 has an effective work zone of 32” wide x 30” high x 50” deep. The furnace is capable of reaching temperatures up to 3100°F/1700°C under partial atmospheric pressure. A vacuum pump helps to remove oxygen prior to beginning the thermal cycle. The case is sealed for use with inert atmosphere.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Since February 2021, Heat Treat Today has had the privilege of publishing the Combustion Corner. In each of these columns, John Clarke, technical director at Helios ElectricCorporation, shares his expertise on all things combustion. In this Technical Tuesday, we're taking a moment to review more of the key points from John's columns. As always, we hope this review helps you to be more well informed, and to make better decisions and be happier. Enjoy these five summaries of the second half of the Combustion Corner columns. To view each installment, click the blue heading below.
Process consistency and energy savings are inextricably linked. To lower operating costs and increase process consistency, John Clarke suggests asking three questions: What temperature is my furnace or oven, really? Do I have excessive safety factors built into my process to compensate for not knowing the temperature at the core of the part being heat treated? How much fuel can I save with a shorter cycle?
Reducing natural gas consumption is not the only way heat treaters can save money. Verifying internal furnace pressure, rebuilding door jams, and taking the time to consider if excess air is reducing combustion efficiency are all as good as cashing a check. Maintaining a consistently uniform furnace temperature saves more money than the energy conserved from using less fuel.
"To not invest money on worthwhile projects makes as much sense as not depositing your paycheck."
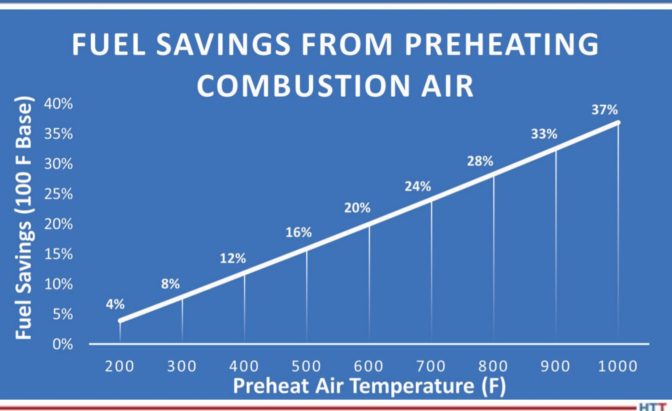
The biggest question mark in a heat treater’s mind is often, “What will natural gas prices be in the future?” Since we cannot know the answer to that question, what are some things heat treaters can do to prepare for unpredictable natural gas prices? Burner recuperation, using the waste heating exiting the furnace to preheat combustion air, is a tried-and-true method for reducing consumption. Before trying burner recuperation, the following questions need to be asked: How much will it cost? How much can be saved? Can the existing furnace accept the higher flame temperatures?
In this installment of the Combustion Corner, John Clarke takes some time to reassure the heat treating industry of two key facts about the United States' natural gas market:
40% of the electricity in the U.S. is generated using natural gas.
U.S production of natural gas was at al all-time high in 2021 and is rising. The U.S. is the largest producer of natural gas in the world.
With these two facts in mind, John postulates that the U.S. can be sure of a reliable supply of natural gas in the future, but, given the price differential between European and U.S. markets, American heat treaters are likely to see an increase in price per mmBTU.
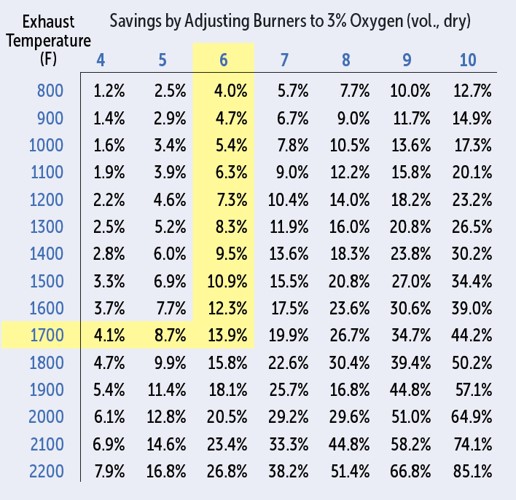
Saving money is the same as making money. Adjusting the oxygen levels of flue products measured with a handheld combustion analyzer to operate at an optimal percentage may yield more savings than you think. Reducing a non-recuperated burner from 6% oxygen to 3% oxygen garners $17,792 extra a year for the heat treater. A quick solution with a hefty payback rate.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
What makes the North American heat treat industry of 2022 what it is? As with any industry, the heat treating world is made up of the people who now inhabit it and the people who paved the way for them. Let’s take a moment to think about the past and what we owe to the industry giants, those trailblazers who have guided so many. In that spirit, enjoy the life stories of these three Heat TreatLegendsfromHeat TreatToday'sSeptember 2022print edition. After all, the industry is only as good as the people in it.
To listen to the life stories onHeat TreatRadio, click the section headings below.
Lost patents, risking a million dollars, and unleashing an entrepreneurial spirit he didn’t know he had. These are just a few things that characterized Bill Jones’ life.
Contact us with your Reader Feedback!
“First, you want to do something that you’re happy doing . . . Then, you must be properly prepared for it. You must have enough education to go forward.” So says Bill Jones, CEO of Solar Atmospheres Group of Companies. A self-proclaimed “technocrat,” Bill remembers being interested in technology from an early age. Technology was the “something” Bill was happy doing.
Throughout Bill’s career, his love of technology often led his peers to complain, “You know, Bill, you’re always interested in technology, and you’re not interested in whether you’re making money or losing money.” The complainers may have been right about Bill’s interests, but they were wrong about how much his love of technology would hinder his ability to make money. Today, Bill and his wife Myrt are the sole owners of four successful, family-owned heat treat companies based in North America: Solar Atmospheres, Solar Manufacturing, Magnetic Specialties, and Vacuum Furnace Systems.
"There is nothing that beats hard work and dedication to what you are trying to do." - William Jones
How did Bill go from being simply a technocrat to the owner of multiple businesses? Bill’s answer: work ethic and education. There is no substitute for being willing to put in more than 40 hours a week and to dedicate yourself to your work. But, Bill says, education is also a must: “We, as practical people in the heat treat industry, tend to pooh-pooh education,” and “[the] basis of what we do comes from chemistry. Metallurgy grew out of chemistry. If you don’t have a decent educational background, then you don’t know the basis of where we came from because that’s the basis of where we’re going.”
Armed with his education and his work ethic, Bill began his journey into the world of technology by working with dew point analyzers. At the time, there was no way to continuously monitor dew point or moisture, and Bill’s first project was to produce a dew point analyzer that could measure one to two parts per million. From measuring dew point, Bill moved on to measuring temperature, and this was his introduction into the furnace industry. In 1963, Bill began a career at Abar, where he used his experience designing optical pyrometers to produce thermocouples that could be used at above 4000°F.
At Abar, Bill worked as the equivalent of a chief engineer on a project that he would later characterize as one of the greatest accomplishments of his life: designing a vacuum furnace with a horizontal ring hot zone. When the new furnace started up for the first time, Bill saw what a ring hot zone could do. Bill still remembers the experience: “When I tested that first round hot zone, I did it by myself at night in a plant where I was the only one there. We had a big sight glass in the front of the furnace, and I could see the entire hot zone, the heating element, the heat shield, the ring and so forth, and I was able to measure the temperature and it was [like] ‘WOW. This thing works!’”
True to his technocrat identity, Bill views this furnace as his greatest accomplishment, not the success of starting his own companies. Along with the development of this furnace, Bill helped to develop the graphite hot zone, which later replaced the metal hot zones at Abar. With graphite hot zones, riveting was unnecessary, and the elements could be bolted together with graphite screws and nuts. One of Bill’s greatest regrets in life was not patenting the horizontal ring furnace. “We should have,” Bill says, “but we didn’t know what we had, honestly, and then it got out into the fi eld anyway and we couldn’t patent it.”
Lost patents, however, did not get in Bill’s way. Bill is also proud of the car bottom furnaces built at Solar’s Hermitage location in Western Pennsylvania. Bill remembers the weekly design meetings and running the furnace for the first time. The car bottom furnace was designed to process heavy titanium coils, and Bill was so confident in his work that he insisted on running the furnace for the first time with a million dollars of titanium coils inside. A coworker, Bob Hill, said, “Bill, you’re not going to run the final product first. I think we should make a run with just some scrap steel that we have around.” Bill replied, “No, Bob. I am thoroughly convinced this furnace is going to work and work right.”
Today, Bill and his wife Myrt are the sole owners of three successful, family-owned companies based in North America: Solar Atmospheres, Solar Manufacturing, and Magnetic Specialties.
Bill’s confidence paid off ; the car bottom furnace worked correctly the first time.
Chronicling his experiences, Bill wrote The Golden Nugget: An Entrepreneur Speaks. Bill’s identity as an entrepreneur was a surprise to him. Bill credits Dr. George Bentley with inspiring his entrepreneurial spirit: “Bill, I want to tell you something,” Dr. Bentley said, “I have observed you over the years and I can tell you, you are never going to be happy until you run your own business.” At the time, Bill did not realize the wisdom of the advice, he did not see himself as an entrepreneur. But now, Bill realizes, “Until you’re sitting in the top chair and until you’re making the decisions of winning and losing, you don’t know what it’s all about.”
Entrepreneurship (no matter how unplanned), innovation, valuing education, worth ethic, and above all else, a love of technology all helped Bill Jones along the road to success. And the main motivation? “Well, it’s very simple: Money is not a driving factor in my life or in my wife’s life. Money is not it. You know, the old saying is, when you go to the grave, there’s not going to be a U-Haul behind you.”
What’s the job of a good doctor? First, do no harm. This mantra, combined with Dan Herring’s love of doing good by solving critical problems, made him what he is today: The Heat Treat Doctor®.
The Heat Treat Doctor® has worn many, many hats throughout his more than 50 years in the heat treating industry. He was a metallurgist, a corporate trainee, an international marketing worker, an applications engineer, a technical director, a research and development director, a product manager, a chief engineer, and finally: an entrepreneur, the owner of his own consultancy, The HERRING GROUP, Inc. In Dan’s own words: “You might say that I’ve been chief cook and bottle washer of the industry, if you will.” These various jobs, and the multitude of different responsibilities that went along with them, taught Dan everything he knows today, developed him into The Heat Treat Doctor®, and made him worthy of being a Heat TreatLegend.
Looking back on his success, Dan points first to his parents for helping him to become the best version of himself. Dan grew up with one parent that gave him a love of technology and equipment and with one parent that give him a love for language and writing. Dan’s father, a machinist, was a hands-on worker and “one of the most inventive people that I ever met.” Later, Dan combined the technical skills he learned from his father with his education as an undergraduate in engineering and a graduate student at the Illinois Institute of Technology.
Dan’s mother, a registered nurse, was “an English teacher in disguise.” She gave Dan a love of writing. For over 10 years, Dan authored a monthly column for Industrial Heating. Columns, however, are not the extent of Dan’s writing expertise. He has also authored: Vacuum Heat Treating, Volumes I & II, and Atmosphere Heat Treating, Volumes I & II. These four books are excellent resources for heat treaters, both novices and experienced industry professionals. Dan has written 10 books in total, six of which deal with the heat treating field. Dan is proud of these books because he can share what he knows with others forever, just as others passed knowledge to him.
“I think it’s interesting,” Dan says, “I have had the extremely good fortune of working for two or three people that actually fell in the genius category. These people were absolutely, positively of genius intellects and they worked within the heat treating industry.” During Dan’s time at Lindberg, he met Hobart Wentworth. Wentworth taught Dan the discipline of engineering, taking Dan’s university knowledge into the real world. Also at Lindberg, Dan was introduced to Russ Novy, chief metallurgist. Dan commends Novy for his “infinite patience . . . to tell you what he had learned and explain things and talk about the root cause of things.” When Dan worked at C.I. Hayes, he met Herb Western, a man who holds over 300 patents in the state of Rhode Island. Western showed Dan how to be creative and inventive within the heat treating industry.
Vacuum Heat Treating, Volumes I & II Atmosphere Heat Treating, Volumes I & II (For more information: www.heatreattoday.com/industryresources/books/herring-books)
One of Dan’s greatest accomplishments was establishing The Heat Treat Doctor® brand. “The brand,” Dan says, “has brought heat treating into the forefront of manufacturing, into the forefront of the industry, into the forefront of engineering, that yes, there is something called heat treating and it is a solution to your needs. So, I view the brand as not so much a personal accomplishment but as an industry accomplishment.”
Dan’s love of words gives him a unique skill set. Not only does he understand metallurgy and engineering, but he is also patient enough to explain it and has the communication skills to explain it well.
When it comes to business, Dan’s main rule is: “Be honest . . . be ethical, be fair, try hard, communicate well and have infinite patience. In other words, not everyone understands what you’re saying. You must take the time to explain what you mean to the people you’re dealing with. Although that’s a strange answer on the business side, I think it’s most impactful.” Dan takes pride not only in doing good throughout the industry, but also, like a good doctor, doing as little harm as possible. Helping others with critical problems, getting companies back in operation, and preventing layoffs are events that stand out the most to Dan.
When it comes to life, Dan’s mantra is: Enjoy the moment. “I remember the first day I started to work at Lindberg,” Dan says, “I took the train to work, it was right across the street from the train station, I was walking across the street, I was 21 years old, and I said to myself, ‘Only 44 years to go.’ And I turn around and the 44 years have disappeared like it was yesterday. So, you must enjoy what you do, and you’ll never work a day in your life.”
Dan attributes his success in the industry to the people around him. He points not only to his parents for his success, but also to the “geniuses” he has worked with along the way, and to the industry at large. Speaking of his entry into Heat Treat Legend status, Dan says, “I just want to say that I consider this a distinct privilege to be considered one the Heat TreatLegends. But I’d also like to point out to everyone . . . that no one individual can do it by themselves. So, I’m accepting this accolade, if you will, on behalf of the many men and women who toiled in, what I’m going to call, relative obscurity and who made this industry what it is today. On their behalf, I’m more than willing to be considered one of the Heat TreatLegends.” Spoken like a true legend.
“Happy, happy, happy.” In Suresh Jhawar’s experience, the best way to run a business is to focus on happy employees, happy customers, and happy bottom lines.
What happens when a young man comes to the United States against his parents’ wishes to earn a bachelor’s degree in Engineering? He becomes the sole owner of G-M Enterprises and gets the title of Heat TreatLegend. At least, that is what happened for Suresh Jhawar, a self-proclaimed “average student in India.”
Without the support of his parents, Suresh weighed the odds of coming to America versus studying in Germany or the U.K. and applied for his visa and passport in a library, away from his parents. When Suresh discovered he could earn his degree in half the time with his advanced credit, he chose the United States and boarded a plane, arriving in the States in 1962. At Marquette University in Milwaukee, Suresh went on to earn a master’s degree in Mechanical Engineering and an MBA in Marketing.
Before taking ownership of G-M Enterprises, the two heat treating companies that were most influential for Suresh were Abar and Ipsen. Suresh began his time with Ipsen in 1970 as a project engineer for vacuum furnaces. Suresh was in the top five at Ipsen, and, looking back, he sees himself driving the company in cost savings, product improvement, and customer relationships.
As the assistant to the president at Ipsen, Suresh traveled extensively to Poland to visit a facility for steel milling and annealing silicon steel coils for transformer steel. During this time of heavy travelling both at Ipsen and later at Abar Furnaces — Suresh visited Poland ten times in less than two years — he remembers the difficulty of keeping a healthy work/life balance. But he succeeded most of the time: “[W]hen Andy [Suresh’s son] was getting an award at his high school, I was coming from Europe . . . I missed my connection. Now it became difficult as to how to get to Philadelphia to attend that awards ceremony for my son . . . I went from one airline to another. I got on a plane, reached Philadelphia airport at the time when the program started, but I was at the school at the right moment when Andy’s name was called. I was there!”
Difficult though it may have been, Suresh often succeeded in keeping work and life in balance. At Ipsen, work consisted of many projects, one of which involved helping Ipsen book an order for 10 large car bottom furnaces. While Ipsen’s president handled the commercial aspect of the order, Suresh handled the technical side of things. He had to make sure the company had the right product and the right solution. And the 10 car bottom furnaces — 84 inches wide by 45 inches high by 32 feet long, made in four bolted sections — were indeed the right solution.
“What I believe is ‘happy, happy, happy’: happy employee, happy customer, happy bottom line.” - Suresh Jhawar
It was at the same time as this project that Suresh was also working on Ipsen’s license agreement with Elterma, which later became SECO/WARWICK. Suresh’s work at Ipsen lasts to this day. Without Suresh, Ipsen would have no manufacturing base in India. Suresh enlisted Wessman Engineering as a sales agent for Ipsen, which began Ipsen’s history in India.
Abar was Suresh’s act two. Suresh wanted to run the entire operation, and Abar gave him the opportunity to do this. Under Suresh’s leadership, Abar increased its profit significantly, and Suresh was asked to write a justification for the merger between Ipsen and Abar. At G-M Enterprises, Suresh’s skills were on full display. Suresh entered G-M Enterprises as a partner holding 15% interest. Within a year, Suresh bought out one of the other partners, and later, in 2005, Suresh took full ownership of the company. He changed the official name of the company to Jhawar Industries and continued to do business as G-M Enterprises. When Suresh joined G-M Enterprises, it was a break-even company. By the time he retired, it was doing business all over the world. “I’m pretty sure,” Suresh says, “that we had the highest bottom line in the industry.” In 2005, Suresh hired his wife, Veena Jhawar, as the director of supply chain, enabling him to focus entirely on developing customers and innovating vacuum furnaces. Suresh’s innovation did not stop there as he was also instrumental in developing the MIM furnace. By 2018, G-M Enterprises was a leading supplier to GE from Singapore to Japan and Brazil.
How did he do it?
“What I believe is ‘happy, happy, happy’: happy employee, happy customer, happy bottom line.” When it comes to happy employees, Suresh says, “The most important thing is to treat your employees like you treat yourself. When I worked at G-M, out of any of the other places, I didn’t work as being ‘the boss’ or on a high platform; I worked shoulder to shoulder with them.” In order to be successful, Suresh believes you must respect your employees and reward them for their contribution, and hopefully, they will be loyal to the company.
Loyal employees make for happy customers. Happy customers, in Suresh’s thinking, have to feel they are a critical part of the solution. This was one of G-M Enterprises’ best qualities. If a customer had a problem, someone from G-M would jump on a plane and fix it, attending to the problem first and worrying about the terms later. Listening to what customers actually wanted, rather than simply giving them what the company already had, was a crucial part of building customer loyalty. With these two principles in place — happy employee and happy customer — the bottom line grew happier and happier.
With these two principles in place — happy employee and happy customer — the bottom line grew happier and happier.
Along the way to a happy bottom line, Suresh discovered the importance of meeting deadlines. Suresh remembers showing up to a production control meeting with no drawings in hand and the others in the room laughing at him. Suresh could tell they were thinking, “He puts pressure on us, but he doesn’t do his own job.” And so, Suresh never went home that day, but instead worked through the night. In the morning, he put all the drawings into the hands of the engineering crew. “Meeting deadlines and commitment, to me, is always number one. No excuses . . . That helps you to expect [the same] from other people, [because] when they see you — that you do that — they follow.”
Reminiscing, Suresh remarks, “We always treated our employees as family members and gave them due respect for their contribution.” For Suresh Jhawar, success in business is all about happiness.
Find heat treating products and services when you search on Heat TreatBuyers Guide.com
Heat Treat Todaywill be a sponsor for the technology trade fair quartet in Düsseldorf, Germany, and we hope to see you there in June 2023. To learn more about GIFA, METEC, THERMPROCESS, and NEWCAST, check out this interview with Friedrich-Georg Kehrer, global portfolio director at Messe Düsseldorf GmbH, about Messe Düsseldorf’s ecoMetals Campaign.
Friedrich-Georg Kehrer Global Portfolio Director Messe Düsseldorf GmbH
The technology trade fair quartet GIFA, METEC, THERMPROCESS and NEWCAST will again provide a complete overview of the foundry technology and metallurgical sectors from June 12–16, 2023 in Düsseldorf, Germany. Which trend topics will particularly characterize the trade fairs?
Contact us with your Reader Feedback!
Friedrich-Georg Kehrer: How green are the energy-intensive foundry and steel sectors of industry? How sustainably do they produce and how eco-friendly is their use of materials? These are the crucial questions dominating the agenda and providing ample food for thought at GIFA, METEC, THERMPROCESS and NEWCAST 2023. Tasked with achieving climate neutrality by no later than 2050, these industries face what is probably the biggest transformation in their history. This decisive development will be reflected by the Düsseldorf trade fair quartet: on the one hand, the challenges that the sectors face; on the other hand, the innovations that machinery and plant manufacturers offer to the metallurgical and casting industries worldwide clearly making them part of the solution rather than the problem. Through in-depth exchange with the professional bodies and experts from all stages of the value chain we have identified the following three mega trends:
Sustainability in the sense of energy and resource efficiency, for instance in the form of green steel or green iron as well as the decarbonization of the steel and iron industry using hydrogen as a catalyst – summarized succinctly under the “ecoMetals” motto.
The use of digital technologies in manufacturing, i.e. the buzzword “Industry 4.0” in steel mills and foundries also remains another mega trend.
Also, automotive lightweight construction as well as the latest additive manufacturing processes for steel and metal working continue to play a key role.
With our four trade fairs and the extensive line-up of ancillary events we offer a unique platform worldwide to discuss these important topics.
The buzzword “ecoMetals” is mentioned in connection with GIFA, METEC, THEMPROCESS and NEWCAST time and again. What does it mean and what role does the campaign play in the events?
Friedrich-Georg Kehrer: Messe Düsseldorf’s ecoMetals Campaign forms an integral part of the “Bright World of Metals” and has a long-standing success story. It refers to the ecological path of the casting and metal processing industries and promotes exhibiting companies that invest in innovative, sustainable and economically competitive technologies. Trade visitors can easily identify the award-winning innovations and are guided to the respective exhibitors at GIFA, METEC, THERMPROCESS and NEWCAST by complimentary daily Guided Tours – so-called ecoMetals Trails. Furthermore, these exhibitors are especially highlighted in the respective Internet portals as well as in the catalogue and their exhibition stands are marked. The ecoMetals campaign was already received very well at the previous edition of the trade fair quartet. Our visitors highly appreciated this guidance. I am particularly pleased to see that some of our other capital goods trade fairs such as wire and Tube or decarbXpo have also adopted this concept this year. With this move Messe Düsseldorf also wants to live up to its ecological responsibility and provide the drivers for environment-saving products, production and processes with a special forum.
So the ecoMetals Trails will enable trade visitors to discover “new pathways for value creation” at the trade fairs?
Friedrich-Georg Kehrer: Yes, exactly! The ecoMetals brand focuses on three fields of sustainability: Resources, Innovation and Production and/or Processes. How can raw materials be extracted in a more resource-efficient way and processed more efficiently? What is trending in metal and non-metal recycling? Which new technologies, machines and plants are used to improve the energy and CO2-balance? The sustainability drivers exhibiting at GIFA, METEC, THERMPROCESS and NEWCAST will share their solutions for all of these challenges. At their exhibition stands they will explain how they reduce their carbon footprint at their production sites and merge business with environmental protection. Overcoming these challenges is as important as ever to hold your own against international competition as a valued business partner.
How much does participation in the ecoMetals Trails cost?
Friedrich-Georg Kehrer: Participation in the ecoMetals Trails is free of charge for all visitors. Registrations can be submitted on the respective websites in the run-up to the trade fairs. Of course, those deciding onsite to take part are welcome to join a tour without prior registration.
On September 21 this year the ecoMetals Day will be held as the “Steel Day of the Future” at the Düsseldorf Exhibition Centre. What kind of event is this and how does it relate to the Bright World of Metals?
Friedrich-Georg Kehrer: The ecoMetals Day will be held for the first time, concurrently with glasstec, as part of our new event decarbXpo. The ecoMetals Day will attract the Who’s Who of the steel sector and cover all topics relevant to the technical, economic and ecological transformation of the steel industry in form of unique lectures. These impulses are, of course, also of enormous importance for THERMPROCESS 2023.
Can you already reveal any details regarding registration levels? How are the trade fair preparations going in general?
Friedrich-Georg Kehrer: The preliminary work has been completed successfully, many companies have already registered and the allocation of exhibition space is in full swing. Now the time for finetuning has come and, of course, for the visitor promotion campaigns. Our exhibitors are eager to inspire the trade fair audience at GIFA, METEC, THERMPROCESS and NEWCAST with their technologies and innovations. All renowned companies will be represented in Düsseldorf again plus many new exhibitors taking part for the first time. GIFA, METEC, THERMPROCESS and NEWCAST are the most relevant events for their respective industries; they thrive on personal encounters and the exchange of ideas in this special setting. Everyone is particularly looking forward to this — especially after such a long time!
Leadership coach Bill Munn writes to Heat TreatToday’s40 Under 40 Class of 2022: "[You] are positioned not only to work with fellow human beings, but to lead them. And if your potential is to be realized, you may already know well that those people are the true key to your future success."
Bill Munn, leadership coach at Bill Munn Management Coaching, wrote this article for Heat TreatToday’s September 2022 Tradeshowprint edition. Read the Spanish translation when you click the flag to the right!
Bill Munn Leadership Coach Bill Munn Management Coaching Source: Bill Munn Management Coaching
Congratulations to the Heat Treat Today 40 Under 40 Class of 2022! This accolade is an honor, and it marks you as one carrying a unique and important responsibility: You are a leader.
Contact us with your Reader Feedback!
By definition, this means that you are not functioning alone. Moreover, you are positioned not only to work with fellow human beings, but to lead them. And if your potential is to be realized, you may already know well that those people are the true key to your future success.
So how will you engage them?
✔ Step one: Embrace a teachable spirit. Bring enough humility to your role to pursue advice, insight, and continuous learning.
✔ Step two: Learn how to motivate people.
The 3 Pillars of Team Motivation
After over five decades of working closely with hundreds of excellent leaders and their teams, I have identified and repeatedly confirmed that three key factors motivate engagement and performance in people: vision, autonomy, and growth.
Vision
People want to be part of something important.
They want what they’re doing to matter. They want to not only understand the vision of their team and organization, but to also believe in it.
You don’t need to be saving the world in order to cast such a vision. Simply take the time to think through your core values as an organization. Ask, “Why is this important? What is key to us being here, doing what we’re doing?” Then communicate that message to your team.
This process is essential, powerful, and far too often overlooked.
Autonomy
People hate to be micromanaged.
True or not, micromanagement communicates two messages that kill motivation: “I don’t trust you” and “I think you’re incompetent.”
On the other hand, when you give your team members assignments and invite them to ask questions, gain clarity, and then charge in on their own, you communicate exactly the opposite message. You say, “I trust you” and “I believe you can do this.” That is incredibly motivating.
Bonus: Your team members will learn and grow farther, faster when given the autonomy to do so. And they will take greater ownership in the organization and its vision.
In short, they will be more engaged and effective.
Growth
Your people want to receive input, attend seminars, participate in training programs, read great and informative magazines like this one, and have access to help, coaching, and development in their area of focus.
Too many leaders go to their people and say, “You should be better at X” or “You should improve Y,” but they don’t support them in doing so. So, what they communicate is a lack of investment in that person’s long-term success, which in turn makes that person less invested in the organization and its goals.
If you want a team made up of valuable people, show your people that you value them by supporting their growth.
People want to be developed. They want to feel — throughout their lives and careers — that they are growing and improving, becoming better at what they do.
The Results of Effective Motivation
Motivated teams are engaged, and engaged teams are effective. As a high-potential leader, you have a unique opportunity to ignite the people you work with — and improve your own outcomes in the process.
Set the vision. Unleash autonomy. Nourish growth. It is now your responsibility and a great honor to do so — one your career and your people will thank you for.
Best of luck to you.
About the Author: Through strategic visioning and in-the-moment issue resolution, Bill Munn helps executives manage teams to their greatest potential. As a 32-year management-coaching veteran and former Dow 30 top executive, Bill has supported hundreds of corporate leaders worldwide with practical wisdom, real-world action tools, and out-of-the-box insight. An MBA and former professor of fi nance and economics, Bill is a dynamic public speaker and Amazon best-selling author of Why Make Eagles Swim? Embracing Natural Strengths in Leadership & Life and Lead or Be Led.
ThermTech, heat treat service provider in Waukesha, WI, has increased their capabilities to provide services for the medical, aerospace, mining and oil, nuclear, and agricultural industries.
Jason Kupkovits, vice president of Sales & Strategic Direction at the company, commented on that ThermTech will be continuing their 40 years of quality assurance, turnaround time, on-site engineering, and customer service standards.
Ben Gasbarre Executive Vice President of Sales Gasbarre Thermal Processing Systems
Partnering with Gasbarre Thermal Processing Systems, ThermTech significantly increased their normalizing, annealing, stress relieving, tempering, and neutral hardening capacity through the acquisition of three new furnaces. These three furnaces --- now fully operational --- include: a dual zone, direct-fired box austenitizing furnace; a large batch tempering furnace; and an additional tempering furnace. These furnaces are compliant with AMS2750 at different class certifications.
ThermTech has also added two additional vacuum furnaces from Ipsen, USA. The furnaces have dimensions of 36” wide x 36” tall x 48” long with capabilities of quenching up to 6 bars of pressure utilizing nitrogen or argon gas as the quench medium. These large vacuum furnaces are AMS class 3 (+/-15°F) certified capable of AMS2750.
ThermTech added a solution annealing furnace from Williams Industrial Service to give their operational aluminum line additional heat treat capabilities. This line is capable of a sub-15 second transfer to air blast quench, a water quench range of 55°F up to boiling, a sub-7 second transfer to water quench which exceeds AMS 2770/AMS2771 specifications, as well as load thermocouple monitoring during the solution treatment, quenching, and aging.
Daniel Hill, PE Sales Engineer AFC-Holcroft Source: AFC-Holcroft
Another recent acquisition includes a new austempering/marquenching furnace from Michigan based AFC-Holcroft. This furnace can handle a single part racked in the vertical orientation up to 56" long. The working dimension of the furnace is 36" W x 72" L x 56" H and is capable of operating with salt temperatures ranging from 350°F -- 750°F. "The UBQA system is an environmentally friendly ‘green technology,’" commented Dan Hill, sales engineer at AFC-Holcroft, "which can be used to impart resistance to distorting, cracking or warping of heat-treated components.” Applicable processes include marquenching, austempering, and carburizing with additional washing and tempering capacity accompanying the new marquenching/austempering furnace. Installation is expected in early 2023.
The heat treat service provider's long-term strategy is to increase growth in the Midwest and on a national scale. This includes adding more workers and integrating the use of a robotics handling systems, which is expected to be installed in late 2022.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Imagine this: A huge lab facility nestled in the south of France . . . teams of scientists and technicians striving to bring carbon-free energy solutions to the world . . . “replicating the high-energy fusion reaction that powers the sun and stars.” To complete the project, what heat treat solution is needed? Read more in thisTechnical Tuesday to find out.
This article by Rafal Walczak,product manager at SECO/VACUUM, will be published in Heat Treat Today’s December 2022 Medical & Energy print edition.
Introduction
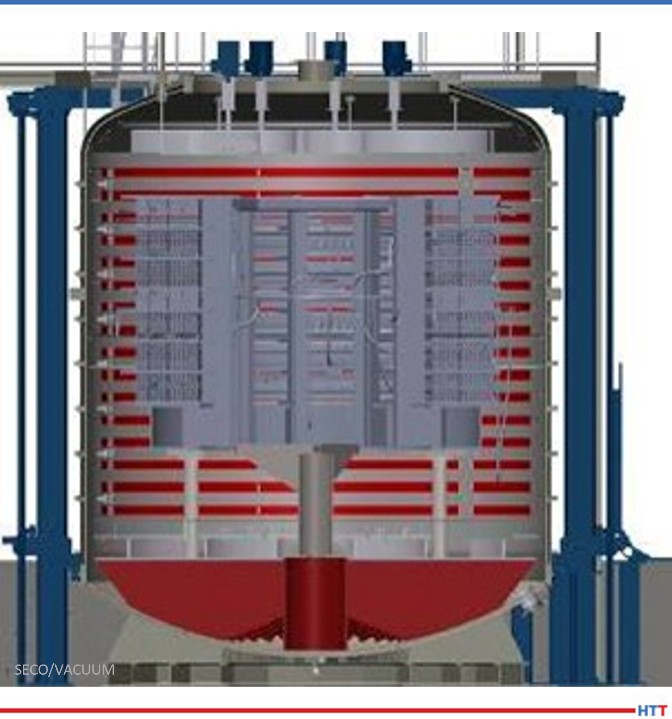
For this case study, we will discuss how SECO/VACUUM built a highly specialized custom heat treating furnace used in the construction of the central component of a large, multinational science experiment.
The Experiment
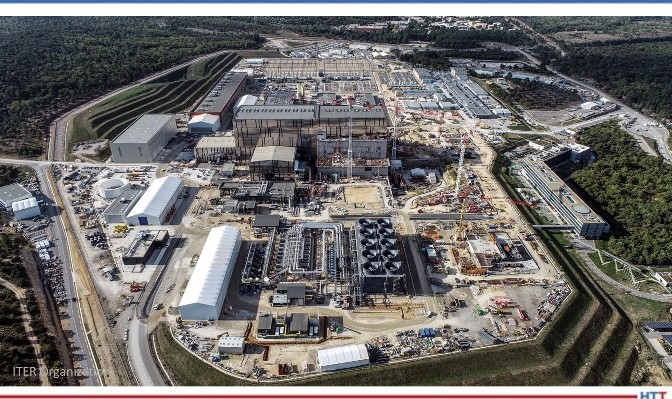
ITER (standing for International Thermonuclear Experimental Reactor and meaning “the way” in Latin) is the largest high-energy science experiment ever conducted. At a giant lab facility in southern France 35 countries, hundreds of vendors, and thousands of scientists and technicians are collaborating on a device to demonstrate the feasibility of clean, safe, carbon-free energy production by replicating the high-energy fusion reaction that powers the sun and stars.
Figure 1. ITER Laboratory at the Cadarache research center in southern France Source: ITER Organization
There are no solid materials that can touch, much less contain, such a high-energy reaction without immediately vaporizing. Instead, this super-hot cloud of plasma must be contained by a special configuration of magnets called a tokamak, which can trap charged particles in a toroidal or donut-shape cloud. This tokamak has 10 times more plasma containment volume than any other tokamak ever built.
The term “tokamak” comes to us from a Russian acronym that stands for “toroidal chamber with magnetic coils” (тороидальная камера с магнитными катушками).
The Magnet
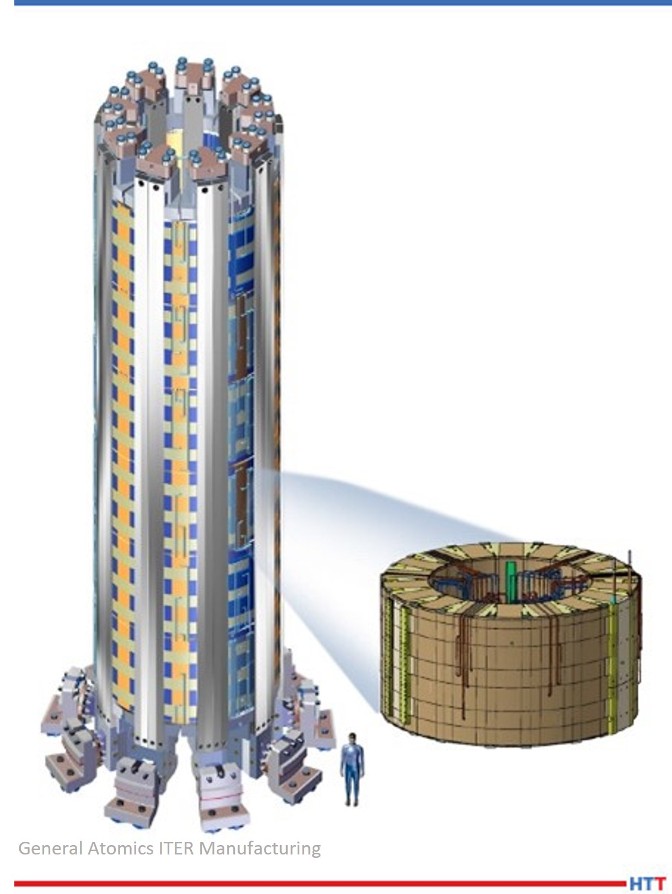
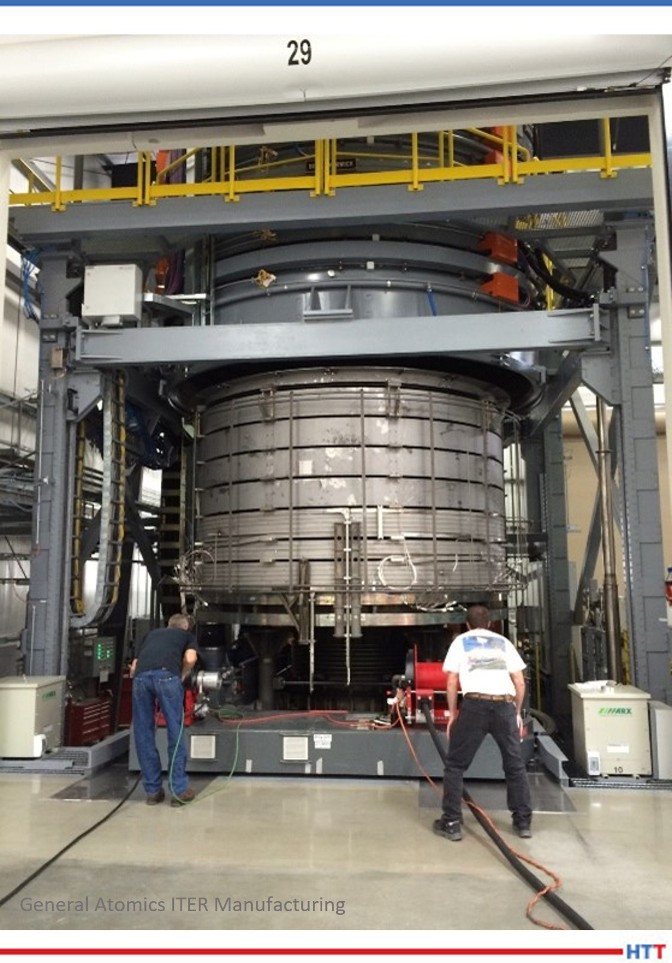
Figure 2. ITER central solenoid and one isolated solenoid module Source: General Atomics ITER Manufacturing
General Atomics’ Magnet Technologies Center near San Diego, CA was contracted to build the ITER tokamak’s large central magnet, the most powerful superconducting magnet ever built, strong enough to lift an aircraft carrier. Other magnets in the tokamak serve to contain the plasma. The central solenoid is an oscillating magnet responsible for inducing current in the plasma cloud similar to how an induction stove heats a pan, except it is heating the plasma to 15 times the temperature of the surface of the sun. Far too large to be constructed and transported in one piece, the 12-meter-tall, 4-meter-wide coil of wires must be built in six 2-meter-tall modules to be joined once they are all on site at the lab. A seventh module will be built as a spare.
Kenneth Khumthong, technical lead for final testing and fabrication certification for ITER Central Solenoid at GA, described the tests on each module of the magnet, saying, “We run a battery of tests on each and every module subjecting them to voltages as high as 30,000 volts and powering them with as much current as 40,000 amps. This is done to ensure that every module meets all of ITER’s specifications prior to shipping them out to France.”
Embrittlement vs. Field Strength Tradeoff
Other superconducting electromagnets in the ITER tokamak will be made using coils of relatively durable niobium-titanium alloy. Past experiments have demonstrated that magnetic fields greater than 12 Tesla disrupt the superconducting properties of Nb3Ti. The ITER central solenoid, however, must sustain magnetic field strengths above 13 Tesla. For this reason, the central solenoid coils must instead use niobium-tin as its superconducting wire, which more reliably maintains superconducting properties in such high magnetic fields but is also more brittle and too fragile to bend after reaction to Nb3Sn. In order to accommodate for the brittle wire, General Atomics had to first coil the wire and jacket into their final shape before heat treating the metals into their superconducting, albeit brittle, alloy Nb3Sn.
The Wire
Figure 3. A dissection of the central solenoid conductor strands, central spiral, and structural jacket Source: ITER Organization
Niobium-tin wire strands react to become Nb3
Copper strands serve as traditional conductors to safely dissipate stored energy when the superconductivity experiences a disruption. The copper strands do not react with the niobium-tin.
A central spiral maintains a hollow channel to circulate liquid helium to chill the Nb3Sn wires to 4°K, below their superconducting temperature of 12°
Creating such strong magnetic fields inside a coil of wire will also tear apart the coil of wire itself if that wire is not supported inside a high strength jacket. The ITER central solenoid wire bundle is about 38.5 mm diameter, housed inside a 50 x 50 mm stainless steel jacket.
Total maximum current in the superconductor wire is 48,000 amps.
Worldwide niobium production increased six-fold for several years just to meet the niobium demands of the ITER project.
The Heat Treating Furnace
Figure 4. Technicians ensure proper placement before lowering heat treat furnace Source: General Atomics ITER Manufacturing
In order to convert the niobium-tin metal conductors into superconductors, each of these 4 meter by 2 meter 110 ton solenoid sections must be heat treated for five weeks, exceeding 1200°F (650°C) at its peak. The heat treatment serves to alloy the niobium and tin together into Nb3Sn, which becomes a superconductor when chilled with liquid helium to 4°Kelvin. No such heat treating furnaces existed, so General Atomics turned to SECO/VACUUM to build a custom heat treating furnace large enough to fit these solenoids and packed with all the technology needed to meet the strict quality control standards of this monumental experiment.
Five inch wide metal band heaters ring around the walls of the furnace with nearly 900kW of heating power. Covering 50% of the walls, they provide a very uniform heat. This is brought about by the following seven steps.
The Heat Treating Sequence
In addition to alloying the niobium-tin wires, the furnace also serves to remove the stresses in the stainless steel jacket housing the superconducting wire and to bake off any residual contaminants prior to reaching reaction temperature.
1. Complete a quality control test: Vacuum seal the untreated solenoid coil in the room temperature furnace and charge the inside of the conductor jacket with 30 bar high pressure helium to test for leaks after forming and welding.
Monitor furnace atmosphere with ultra-high sensitivity mass-spectrometer helium detectors.
2. Purge with argon gas while slowly ramping up heat.
This drives off hydrocarbons and oxygen before system reaches reaction temperatures.
Monitor furnace atmosphere with gas chromatograph to find impurities from residual oils and lubricants leftover from manufacturing process.
Monitor and control argon circulation and exchange with mass flow sensors and circulation blowers that penetrate the furnace lid with ferrofluidic feedthrough seals around the blower motor shafts.
3. Maintain at 1058°F (570°C) for about 10 days. Confirm stabilized temperature and pure atmosphere.
4. Proceed to 1202°F (650°C) for four days. This is the actual reaction phase that achieves the primary objective of converting the niobium-tin into the superconducting alloy Nb3
5. Very slowly and uniformly ramp back down to room temperature to avoid additional stresses in the coil.
6. Complete another quality control test: Evacuate the argon and once again vacuum seal the solenoid coil in the room temperature furnace and recharge with 30 bar high pressure helium to test for leaks after heat treating. Monitor atmosphere for the presence of helium, which would indicate a leak in the coil.
7. Only then is it ready for the post-heat treating stages of wrapping with insulation and encasing in epoxy resin for rigidity.
Options, Upgrades, Special Features
Figure 5. Cutaway illustration showing the furnace construction Source: SECO/VACUUM
There was no room for error. SECO/VACUUM collaborated with the engineers at General Atomic to create a heat treat furnace that can assure temperature variation within the coil never varies by more than 18°F (10°C) anywhere in the furnace at any time in the five-week cycle and achieves near-perfect repeatability for all seven modules.
They accomplished this with quadruple-redundant control thermocouples and feeding temperature data from 150 points in the coil into the control computers. To shield against impurities, the furnace is first evacuated to a vacuum pressure of 0.001 Torr, and then purged with pure argon to drive out any residual oxygen or hydrocarbons that could contaminate the purity of the superconductor. Monitoring the argon atmosphere for impurities are redundant mass spectrometers. The argon is circulated by seven convection fans to heat the solenoid assembly evenly. Each of these fans must be driven through ferrofluidic feedthrough seals which allow the rotating shafts to operate through the furnace walls without compromising the vacuum seal of the furnace.
Consult, Collaborate, and Partner with SECO/VISORY
General Atomics first began discussing this project with Rafał Walczak, the product manager at SECO/VACUUM, in early 2010. Both teams spent over two years on conceptual discussions, preliminary designs, and process simulations before SECO was even awarded the contract. Once SECO was on board, it took another two years of design, fabrication, and installation before the furnace could be put into operation. SECO/VACUUM built it to handle a lifetime of use without error so they could be sure that it would work flawlessly for the seven cycles that it actually had to run.
The SECO/VISORY Heat Treat Advisory Council is a team of SECO/VACUUM heat treat experts and consultants with diverse thermal experience and process knowledge who are available to help companies solve their specific heat treat equipment challenges.
About the Author: Rafal Walczak is the product manager at SECO/VACUUM. Rafal joined SECO/WARWICK Group as a service engineer in Vacuum Furnaces Division soon after graduation from Technical University of Zielona Góra in 2002. Since 2008, he has been involved in vacuum furnace sales in Europe and the USA. The combination of his technical background and field service experience help him provide outstanding support to his SECO/VACUUM customers. For more information, contact Rafal at Rafal.Walczak@SecoVacUSA.com.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com

 "Las operaciones de tratamiento térmico son percibidas generalmente como cajas negras cuyos resultados son poco predecibles. Si bien, entendemos los mecanismos físicos involucrados para modificar las propiedades de un material, los hornos de tratamiento térmico son sistemas termodinámicamente imperfectos, y por ende los resultados finales en ocasiones también lo son."
 Por definición, de aquí se desprende que no se desempeña solo; es más, está posicionado no solo para trabajar en conjunto con otros seres humanos sino también para liderarlos; si su potencial se ha de realizar, puede que ya haya entendido bien que en esas personas reposa la verdadera clave del éxito que a futuro pudiera conseguir ¿Cómo, pues, lograr su compromiso?
 Find heat treating products and services when you search on Heat Treat Buyers Guide.com






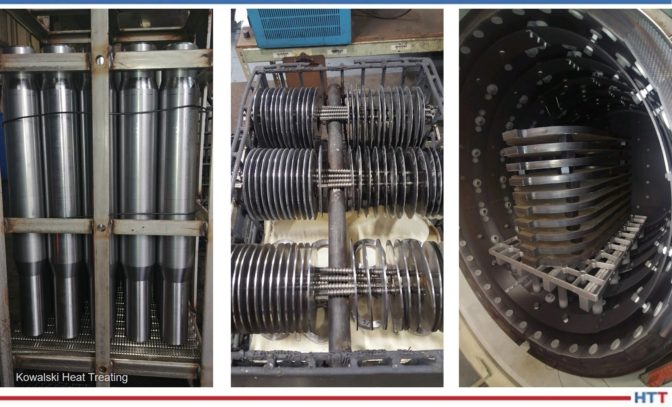
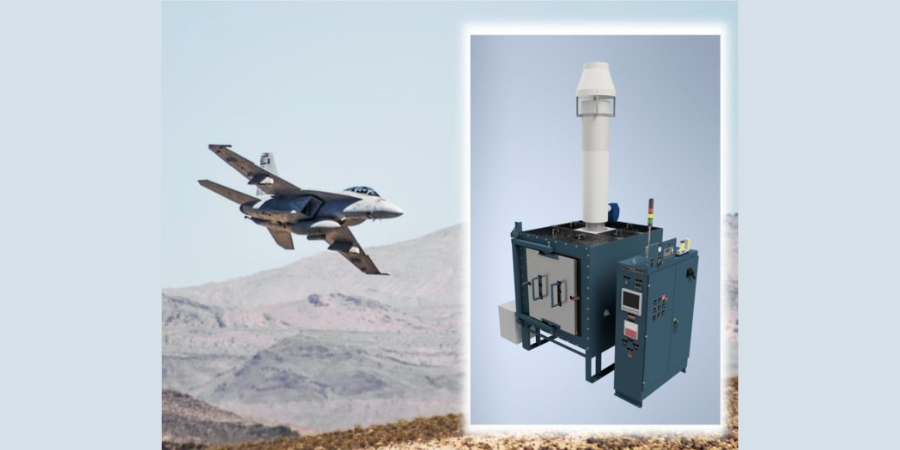

 A U.S. manufacturer with a plant in the Midwest received and commissioned a large high-temperature box furnace for processing ceramic matrix parts that will be used in military and aerospace applications.

 Since February 2021,