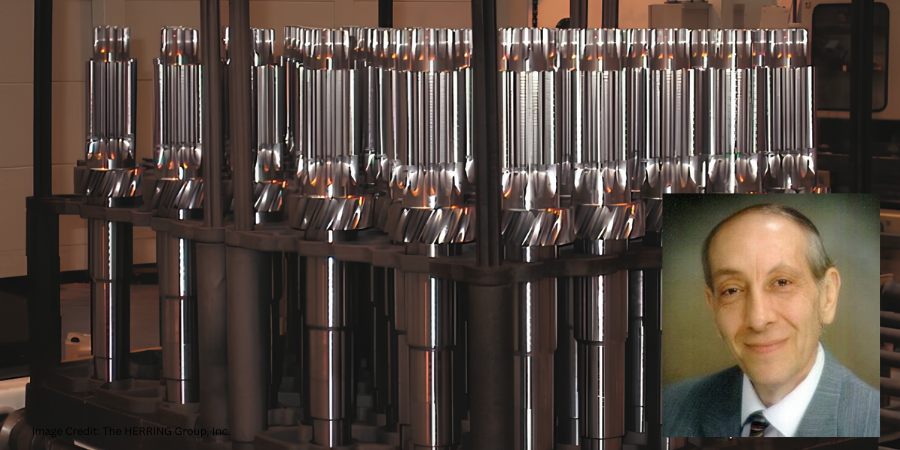
Heat Treat Today launches a new contributing experts series on emerging technologies reshaping heat treat operations. In this first installment, Zach Menard, CEO and co-founder of HRC Labs, demystifies deep neural networks (DNNs)— a technology quietly used in industrial settings for years — and explains how they turn accumulated furnace cycles, recipes, and quality records into predictive models that help heat treaters develop new recipes, minimize distortion, and cut cycle times.
This informative piece was first released in Heat Treat Today’sAugust 2026 Annual Automotive Heat Treating print edition.
Large language models (LLMs) have dominated recent conversations around artificial intelligence, but they are only one application of deep neural networks (DNNs). Years before DNNs were applied to human language, they had been deployed in industrial settings to optimize processes, improve yield, and support quality control.
These same, well-established approaches can be applied to heat treatment by learning relationships between process inputs — such as temperature, time, atmosphere, and alloy composition — and resultant metallurgical properties like hardness, distortion, or case depth.
It’s the first word in the acronym, DNN, that makes this learning possible. The neural network is said to be “deep” because of its many successive layers of neurons. Each neuron on its own is very simple. All it can do effectively is multiply and add together the numbers it has received from earlier neurons. However, when this process is repeated across many layers, the overall network is able to learn complex relationships that influence the heat treatment process.
By training on historical production data, DNNs can transform years of accumulated process knowledge into predictive models. Patterns that may otherwise remain buried across thousands of furnace cycles, recipes, and quality records can be captured quantitatively by the model itself.
In this way, operational experience and historical records become structured, reusable intelligence that can aid decision-making. Examples include when heat treaters are developing a new recipe, considering how to minimize distortion, or lowering cycle times.
As heat treatment operations continue accumulating larger volumes of process data, applying DNNs to this data offers a clear path toward AI-assisted process optimization, operational intelligence, and more adaptive heat treatment systems.
About the Author
Zachary Menard CEO and Co-Founder HRC Labs
Zachary (Zach) Menard is the CEO and co-founder of HRC Labs, an industrial AI company focused on process optimization and decision support for heat treatment. He holds a B.S. in physics from Vanderbilt University with a background in computational physics and machine learning research.
Ask The Heat Treat Doctor® has returned to bring sage advice to Heat Treat Today readers and to answer your questions about heat treating, brazing, sintering, and other types of thermal treatments as well as questions on metallurgy, equipment, and process-related issues. In this Technical Tuesday installment, Dan Herring explores the fundamentals of vacuum oil quenching — the three stages of oil quenching, the properties that make oil an effective quenching medium, and the ways pressure control, oil circulation, and temperature can be used to minimize part distortion — and offers step-by-step guidance on properly conditioning and degassing vacuum quench oil to ensure consistent, repeatable results.
This informative piece was first released in Heat Treat Today’sAugust 2026 Annual Automotive Heat Treating print edition.
Oil quenching in vacuum furnaces is a technology that has been around for over 65 years. The popularity of oil as a quench medium is due to its excellent performance and stability over a broad range of operating conditions. Proper application, testing, and conditioning of the oil are necessary to ensure its effectiveness. Let’s learn more.
For many, the choice of oil is not only due to metallurgical transformation and resultant properties it can achieve, but also to a number of other factors, including:
The first criterion that any quenchant must meet is its ability to approach an ideal quenching medium.
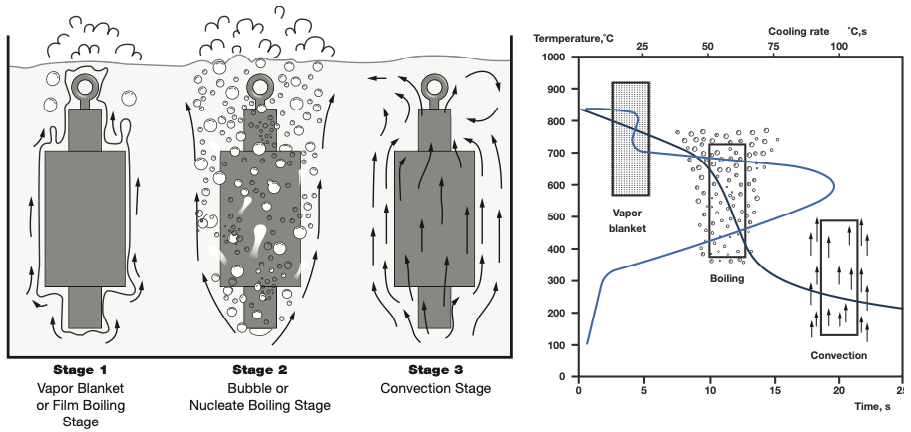
Figure 1a-b. Three stages of oil quenching
Regardless of the type of liquid (brine, water, polymer, oil, molten salt, or air mist), the ideal quenching medium (Figure 1) is one that would exhibit high initial quenching speed in the critical hardening range (Stages 1 and 2) and a slow final quenching speed through the lower temperature range (Stage 3). Thus, the ideal quenchant is one that exhibits little or no vapor blanket stage, a rapid but controlled nucleated boiling stage, and a slow cooling rate during convective cooling.
The high initial cooling rates allow for the development of full hardness by ensuring the steel misses the “nose” of the time-temperature-transformation diagram (i.e., quenching faster than the so-called critical transformation rate). This is followed by cooling at a slower rate beginning at the time the steel is forming martensite, which allows for better stress equalization so that the potential for distortion and cracking is reduced.
When conventional quenching oils are used, the duration of Stage 1 is longer, the cooling rate in Stage 2 is considerably slower, and the duration of Stage 3 is shorter. As such, the “quenching power” of oil is far less drastic than other quenchants. Water and water-based quenchants exhibit high initial cooling rates. Unfortunately, because of water’s low boiling point, this fast cooling persists until the steel is cooled to below 300°F (150°C). As most steels have formed or are forming martensite by this point, stresses are given little time to equalize. Thus, water is typically limited to low hardenability materials and relatively simple geometries.
Oil has a major advantage over water or polymer due to its higher boiling range. A typical oil has a boiling range between 450°F (230°C) and 900°F (480°C). This causes the slower convective cooling stage to start sooner, enabling the release of transformation stresses. Oil, therefore, is able to quench intricate shapes and high hardenability alloys successfully.
As it is heated, oil has a proportional drop in viscosity. This allows the quenchant to move more freely, increasing, in general, the tendency to break the vapor blanket layer. The nucleate boiling stage is not drastically altered by changes in bath temperature. The cooling rate in the convection stage, however, will slow as the bath temperature increases. This is advantageous for obtaining a slower rate of cooling through the austenite-to-martensite transformation range.
In general, as the temperature of a quenching oil increases, the overall quenching rate increases. Practical heat transfer coefficient (α) values are in the 1,000 to 2,500 W/m²K range depending on oil characteristics and degree of agitation. Peak α values are in the order of 4000 to 6000 W/m²K, or a cooling rate greater than 100°C/sec (180°F/sec).
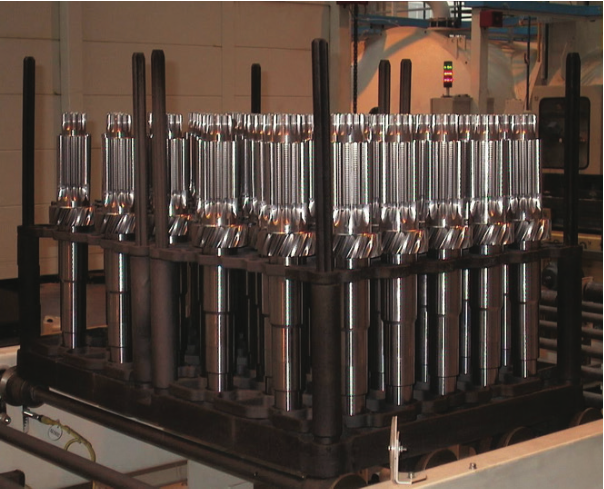
Figure 2. Typical commercial heat treat load | Image Credit: The HERRING GROUP, Inc.Figure 3. Die cutting punches benefiting from controlling the pressure over the oil | Image Credit: The HERRING GROUP, Inc.
The use of vacuum oil quenching has been found to reduce distortion in many components including gears, pinions, and shafts (Figure 2). Oil quench vacuum systems also offer an attractive alternative to conventional atmosphere oil quenching, given their ability to vary a quench related variable not otherwise possible, namely controlling the pressure over the oil (Figure 3). This technique can be used to extend the range of part cross sections and materials that can be successfully hardened (Herring 1987, Sugiyama and Uchigaito 1987).
Pressure control along with oil temperature and oil circulation improves the predictability of distortion. The lower pressure allows for longer “vapor blanket” stages and a somewhat long “vapor transfer” stage, due to the reduced boiling point of the oil. This may reduce distortion and provide the desired hardness if the material’s transformation ranges are accommodating.
Distortion minimization methods have been used in combination with changes to flow characteristics. Some manufacturers pull oil down through the workload as opposed to pushing it upward. Also, oils formulated for vacuum service typically have a low vapor pressure, allowing them to be easily degassed.
Finally, vacuum systems do not permit the buildup of water in the quench tanks. In a vacuum furnace system, where vacuum is used to process the work or purge the quench environment, moisture will be removed as the system is evacuated and the oil circulated. Circulating the oil carries any moisture to the oil surface, where it vaporizes and is removed by the vacuum pumping system.
Maintaining Your Vacuum Quench Oil
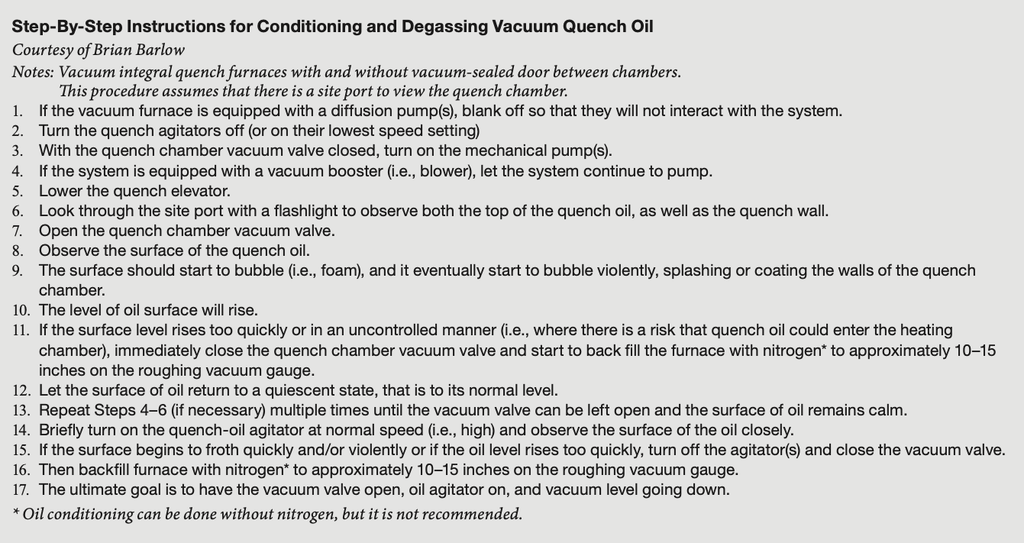
One of the aspects of vacuum oil quenching that is seldom documented is how to condition the quench oil. See “Step-By-Step Instructions for Conditioning and Degassing Vacuum Quench Oil” below.
Final Thoughts
As with all quenching, the key is to understand and control the key process variables. Proper selection of the type and use of oil under ideal conditions in a well-designed and well-maintained quench tank will ensure consistent and repeatable results.
Oil quenching should be applied in applications where its advantages outweigh its disadvantages and, as with all technologies, should be as completely understood as possible with respect to the performance requirements of the product so as to meet the application end use.
References
Brian Barlow. 2025. Private correspondence. Gasbarre Thermal Processing Solutions.
Herring, Daniel. H. 2002. “A Review of Factors Affecting Distortion in Quenching.” Heat Treating Progress Magazine. December. 2012. Vacuum Heat Treatment, Volumes I. BNP Media Group.
Herring, Daniel H. 2016. Vacuum Heat Treatment, Volume II. BNP Media Group.
Herring, Daniel H., Steven D. Balme. 2007. “Oil Quenching Technologies for Gears.” Gear Solutions. July.
Herring, D. H., Sugiyama, M., Uchigaito, M. 1986. “Vacuum Furnace Oil Quenching – Influence of Oil Surface Pressure on Steel Hardness and Distortion.” Industrial Heating Magazine. June.
Sugiyama, M., Uchigaito, M. 1987. “Controlling Oil Surface Pressure in Vacuum Oil Quenching.” Heat Treating Magazine. July.
About the Author
Dan Herring “The Heat Treat Doctor®” The HERRING GROUP, Inc.
Dan Herring has been in the industry for over 50 years and has gained vast experience in fields that include materials science, engineering, metallurgy, new product research, and many other areas. He is the author of six books and over 700 technical articles.
For nearly five decades, Heat Treating Services Corporation of America (HTS) has built its reputation on reliability, production capacity, and long-standing client relationships in the thermal processing industry. Since its founding in 1978, the family-owned company has steadily expanded its footprint and capabilities, growing from a single furnace installation into a multi-facility operation serving a wide range of industries.
This heat treater’s story began with a straightforward objective: provide dependable heat treatment. The company installed its first furnace to heat treat steering knuckles for Ford, marking the beginning of a business model centered on responding directly to client requirements.
The company grew by adding equipment and processes to support real production demand, leading to significant expansion. In 1990, HTS purchased its second facility, followed by the acquisition of a third plant in Pontiac, Michigan, in 1996. These additions laid the groundwork for the company’s current scale, operating three primary heat treating facilities totaling more than 161,000 square feet and capable of producing approximately 84 million pounds of heat treated and cleaned parts per month.
Further growth came in the early 2000s as the company expanded its operational footprint and service capabilities. An additional property adjacent to its first plant was acquired in 2002 to support value-added services and logistics, enabling more efficient drop-shipping directly to clients’ end users. In 2005, they expanded again with the acquisition of Trojan Heat Treat in Homer, Michigan, adding a 50,000-square-foot facility focused on non-quench heat treating processes.
Today, the company employs approximately 250 people and supports clients across automotive, aerospace, military, mining, agriculture, and construction sectors, delivering consistent results on high-volume workloads while maintaining the flexibility required for complex components and varied metallurgical requirements.
At the heart of their operations is a broad suite of heat treating services designed to enhance the performance of metal components through carefully controlled thermal cycles. These processes include annealing, quenching, tempering, normalizing, and stress relieving, each applied to improve critical material properties such as hardness, strength, toughness, and ductility. By controlling both heating and cooling conditions, the company ensures that parts meet precise mechanical and structural specifications required for demanding industrial applications.
Much of the production work centers on toll processing of rough forgings and castings. Key processes include quench and temper operations, normalizing, and isothermal annealing. Additional treatments, such as spheroidize annealing, inter-critical annealing, sub-critical annealing, stress relieving, and carbide removal, allow the company to tailor metallurgical properties to a wide range of component requirements.
The company’s equipment infrastructure supports both batch and continuous production environments, handling parts ranging from ounces to more than 750 pounds. High-capacity systems, including a large roller hearth furnace capable of processing up to 10,000 pounds per hour, allow HTS to deliver high throughput without sacrificing process control or consistency.
HTS maintains backup furnaces for critical production lines, ensuring that client work continues uninterrupted even if equipment requires maintenance. This level of preparedness reflects a broader commitment to reliability, one of the qualities the company hopes clients associate with its name. This commitment is reflected in the longevity of their client relationships. A large portion of HTS work comes from clients who have partnered with the company for more than three decades, an indication of the trust built through consistent service and dependable turnaround times.
Over the decades of work, one project stands out as particularly memorable. During Operation Desert Storm, the company heat treated track shoes, center guides, and end connectors for the Abrams M1 tank. The work earned HTS a letter of recognition from General H. Norman Schwarzkopf Jr., a moment the company recalls as both an honor and a testament to the importance of dependable manufacturing support during critical operations.
Looking ahead, HTS is focused on continuing to modernize its operations. Automation initiatives, paperless processing systems, and the integration of artificial intelligence tools are all part of the company’s strategy to improve productivity and strengthen profit margins in the coming decade.
Through these investments, this heat treater aims to maintain the qualities that have defined its history: fast service, reliable delivery, and the consistent quality that has kept clients returning for generations.
For more information:
Heat Treating Services Corporation of America
217 Central Ave. Pontiac, Michigan 48341
awhaley@htsmi.com https://www.htsmi.com/
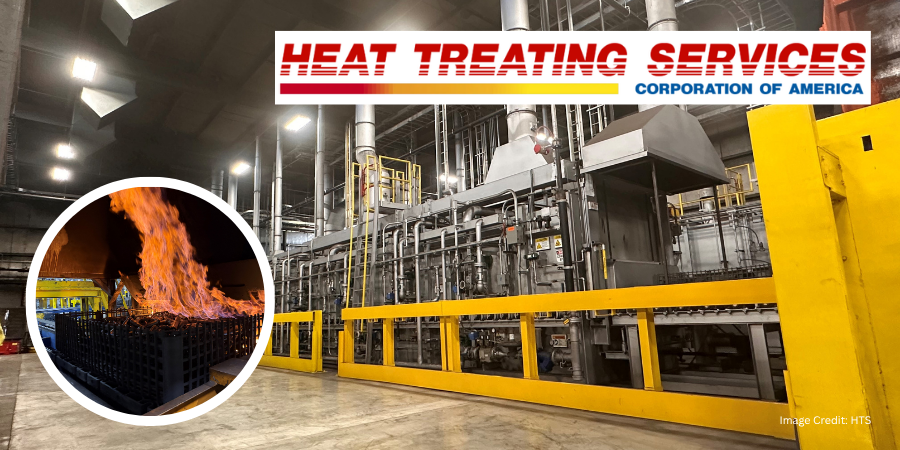
Main image: Roller hearth furnace 10,000lb/hr process capability; normalizing, isothermal annealing, or oil quench and temper capabilities | Image Credit: HTS
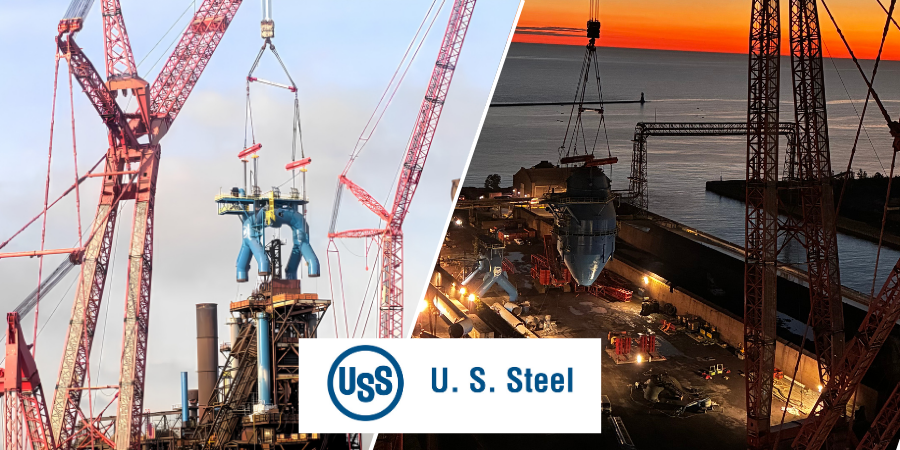
U.S. Steel has completed a $350 million blast furnace reline at its Gary Works operation in Indiana, returning more than 2 million tons of annual hot metal production capability to service. The project replaced the furnace’s refractory lining and restored critical systems supporting high-temperature ironmaking operations and long-term steel production.
Blast Furnace No. 14 has returned to service following completion of the reline project. The furnace is the largest at Gary Works and in U.S. Steel’s operating footprint.
The reline included replacement of the furnace’s refractory lining as well as restoration of critical systems designed to support safe, reliable operation and extend the furnace’s productive life. During the outage, teams also completed maintenance on supporting infrastructure, including the furnace gas, cooling water, hoisting, and stove systems.
The project required more than 1 million labor hours from employees and contractors, with a peak workforce of approximately 1,000 contractors on site per day.
David Burritt President and CEO U.S. Steel
“The return of Blast Furnace No. 14 is a great example of disciplined execution at U.S. Steel and is a testament to the skill, dedication, and unwavering focus on safety demonstrated by our employees, contractors, and partners,” said David B. Burritt, president and CEO of U.S. Steel. “This investment positions Gary Works to continue serving [clients], supporting American manufacturing, and creating value for years to come.”
Blast Furnace No. 14 is capable of producing more than 2 million tons of hot metal annually. The furnace incorporates large carbon block refractory produced by NDK, and it uses iron ore pellets sourced from U.S. Steel’s Minnesota Ore Operations as part of the company’s integrated steel supply chain.
The project comes as U.S. Steel continued hot strip mill and related steel shop upgrades at Gary Works intended to enhance capabilities, environmental performance, and operational reliability.
Press release is available in its original form here.
In today’s News from Abroadinstallment, we highlight several major global developments in thermal processing — from commercial-scale DRI smelting and the return of primary aluminum production to expanded vacuum heat treating capacity and a new induction melting furnace — reflecting continued investment in furnace technology and metals production worldwide.
Heat TreatTodaypartners with two international publications to deliver the latest news, tech tips, and cutting-edge articles that will serve our audience — manufacturers with in-house heat treat. Furnaces International, a Quartz Business Media publication, primarily serves the English-speaking globe, and heat processing, a Vulkan-Verlag GmbH publication, serves mostly the European and Asian heat treat markets.
DRI Smelting Technology Reaches Commercial Scale
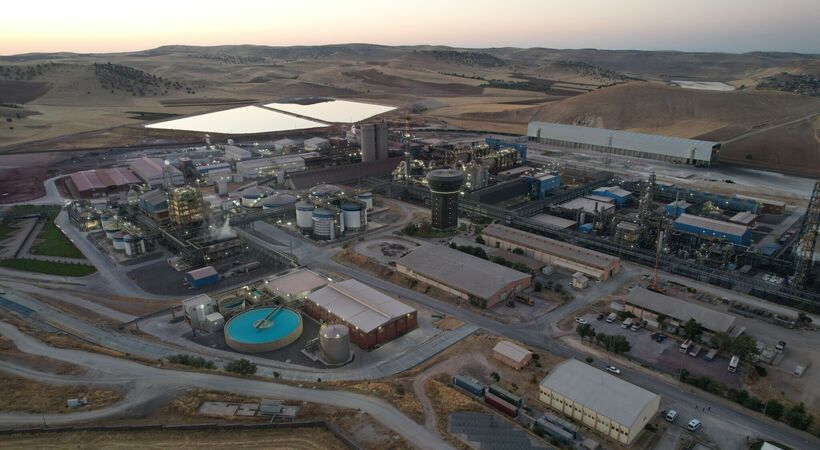
Metso will supply a DRI furnace to Türkiye-based metals and fertilizer producer Eti Bakir at its Mazidagi facility.
“Metso has received a €55 million order for a DRI furnace from a Türkiye-based metals and fertilizer producer. It will be the first commercial-scale delivery of Metso’s DRI Smelting Furnace technology.”
” The delivery scope includes engineering, as well as supply and advisory services for an SL/RN Xtra rotary kiln pellet direct reduction process integrated with a 30 MVA Metso Outotec DRI Smelting Furnace. The system includes a hot feeding system for the DRI smelter.”
Primary Aluminum Production Restarts After Three-Year Pause
Slovalco plant in Žiar nad Hronom, Slovakia, restarts aluminum production.
“Slovalco has begun the restart of production at its aluminium smelter in Žiar nad Hronom, Slovakia.”
“The funds are being directed to the preparation of equipment, start-up of electrolytic pots, and other upgrades required to ensure a stable return to production. The first phase of the restart represents 75,000 tons of annual capacity.”
Vacuum Heat Treating Capacity Grows for Tool Steels
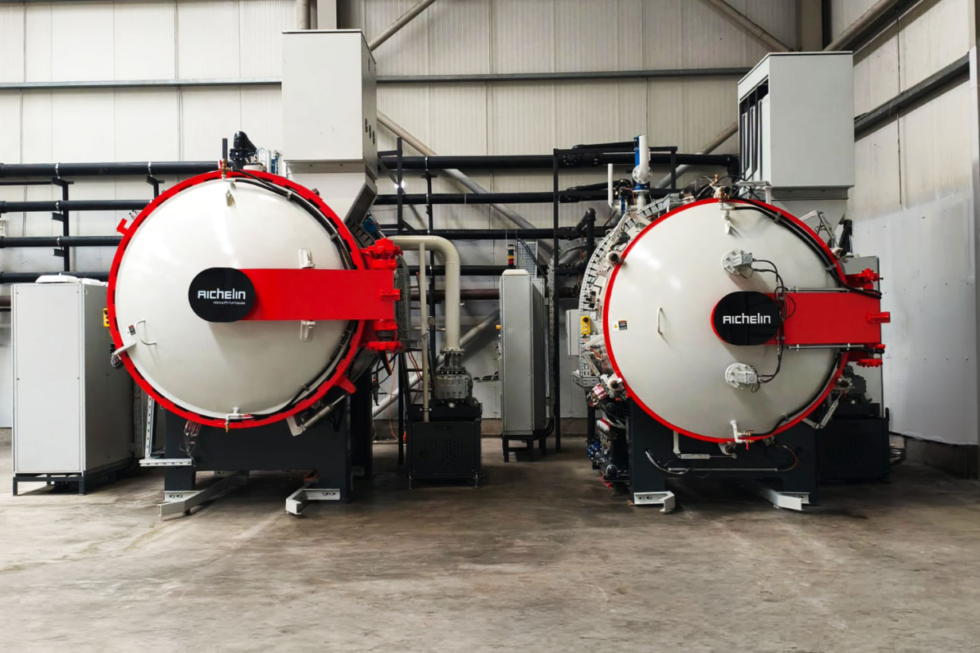
Aichelin vacuum ovens have installed on-site at the client’s premises.
“Aichelin has successfully delivered, installed, and commissioned a new vacuum heat treatment system for Ayhan Takım Çelik A.Ş., one of Turkey’s leading suppliers of tool steels and engineering materials. This investment expands the company’s heat treatment capabilities and supports the processing of high-quality tool steels with consistently high process reliability and precision, including materials for demanding tools in aluminum extrusion and die casting.”
The induction furnace was installed and commissioned in 19 days.
“ABP Induction has successfully demonstrated its ability to deliver highly efficient project execution with the installation of a state-of-the-art FS40 induction furnace system at South32 Hillside. Equipped with digital DICU3 technology, an emergency UPS tilting system and advanced digital functionalities, the solution enhances both safety and process optimization — another milestone in the sustainable transformation of the metals industry.”
A manufacturer of gas turbine and aircraft engine components has ordered a vacuum furnace for heat treating high-temperature alloy turbine blades. The system’s all-metal hot zone, high vacuum, temperature uniformity, and high pressure gas cooling are designed to support the clean, repeatable processing required for components operating in the hot sections of turbines.
Image Credit: SECO/WARWICK
SECO/WARWICK, a global heat treatment equipment manufacturer with operations in North America, will supply its Vector single-chamber vacuum furnace to the China-based manufacturer. The order marks the second Vector furnace delivery to the manufacturer in recent months and follows an earlier furnace installation with a graphite hot zone in 2023.
The new furnace will feature an all-metal hot zone and operate at temperatures up to approximately 2550°F (1400°C). It will provide temperature uniformity of ≤±5.4°F (≤±3°C), gas cooling at pressures up to 12 bar, and a maximum gross load weight of approximately 1300 lbs (600 kg). The furnace is designed to operate in a high-vacuum range of 10-3 Pa.
The specifications exceed the standard configuration for this type of furnace with a metal hot zone, which provides 10 bar gas cooling and temperature uniformity of ≤±9°F (≤±5°C). The high-vacuum environment helps reduce the risk of intergranular oxidation and supports the surface quality of treated turbine components.
Maciej Korecki Vice President of the Vacuum Segment SECO/WARWICK Group
“In this project, the key was to combine two things: the proven design of the Vector furnace and a very specific adaptation to the [client’s] process,” said Maciej Korecki, vice president of the Vacuum Segment at SECO/WARWICK Group. “We are talking about parts that operate in the hot section of turbines, where the margin for error is minimal. High vacuum, very good temperature uniformity, and fast, controlled gas cooling creates that conditions for stable, repeatable heat treatment of high-temperature alloy blades.”
The all-metal hot zone is intended for processes requiring a clean environment with reduced risk of contamination. Combined with temperature control and gas cooling, the configuration can also support processes for aerospace, energy, medical, and additively manufactured components.
SECO/WARWICK teams in China and Poland jointly developed the furnace configuration to meet the manufacturer’s process requirements. The order follows a 2025 production need for an all-metal hot zone, higher gas cooling pressure, and tighter temperature uniformity than the standard Vector configuration.
Press release is available in its original form here.
A nearly $3 million federally funded project will develop an induction smelting process to produce pig iron from low-cost, low-grade ores, adding a continuous smelting step to direct reduced iron (DRI) processing. The technology is intended to remove impurities and increase productivity while expanding the types of domestic iron ore that can be used for steelmaking.
The project, titled Induction Smelting of DRI-Processed Low Grade Ores for Steelmaking, will develop technology to produce pig iron from lower-cost, low-grade ores. Conventional direct reduced ironmaking typically requires more expensive high-grade ores. The additional smelting step is designed to remove impurities from lower-grade material, creating another pathway for its use in DRI-based ironmaking. The process will allow smelting to occur continuously rather than in batches, increasing productivity.
The project is one of 56 selected for a total of $117 million in DOE funding aimed at developing technologies to lower production costs and improve energy productivity across U.S. industrial sectors.
Press release is available in its original form here.
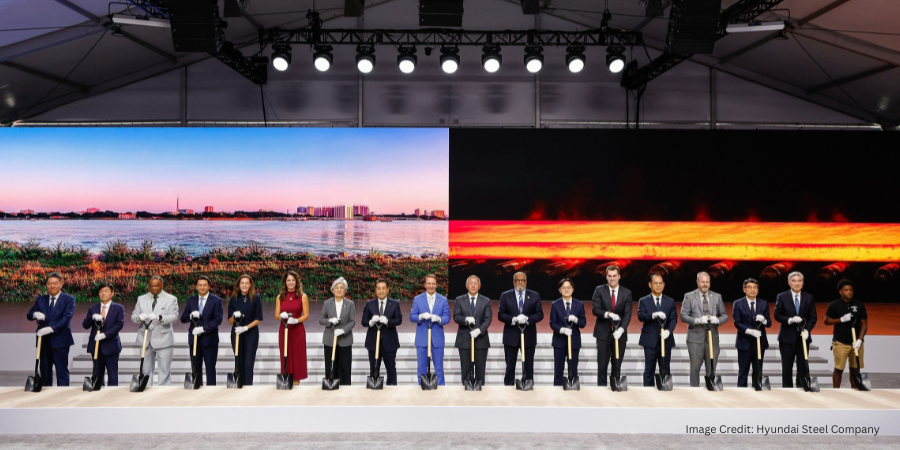
A $5.8 billion electric arc furnace (EAF)-based integrated steel mill project has launched in Louisiana, establishing a new domestic source of automotive steel that will combine on-site direct reduced iron (DRI) production with EAF steelmaking. The facility is targeted to begin commercial production in 2029 with an annual capacity of 2.7 million metric tons of hot-rolled and cold-rolled steel sheet, primarily for automotive applications.
The facility will establish an integrated production system connecting on-site DRI production with EAF steelmaking and downstream production of automotive steel. A direct reduction plant will produce DRI on site and feed it directly into two EAFs through a continuous charging system. The configuration is designed to improve production efficiency and enable a higher share of DRI to be used in producing advanced steel grades.
Advanced refining and continuous casting facilities will be used to manage impurities such as nitrogen and sulfur to meet automotive steel quality requirements. The production route is expected to reduce carbon emissions from molten steel production by approximately 70% compared with the company’s conventional blast furnace process in Korea.
The facility will also incorporate carbon capture capabilities and is being designed to gradually replace the natural gas used in the direct reduction plant with hydrogen as infrastructure and availability develop.
With an annual steel production capacity of 2.7 million metric tons, the Louisiana mill will supply automotive steel to Hyundai Motor’s Alabama plant, Kia’s Georgia manufacturing facility, and Hyundai Motor Group Metaplant America, as well as other U.S. automakers. Producing automotive steel closer to clients is expected to strengthen supply stability, shorten delivery lead times, and enable faster technical and quality support.
Bo-Ryong Lee President and CEO Hyundai Steel Company
“Today, we are not simply announcing the construction of a new steel mill. We are standing at the starting point of a journey to shape the future of industry in Louisiana together,” said Bo-Ryong Lee, president and CEO of Hyundai Steel. “We aim to serve as a key supply chain partner to the North American automotive industry by providing a stable supply of high-quality automotive steel to [clients] in the United States and around the world.”
The project is part of Hyundai Motor Group’s $26 billion U.S. investment commitment through 2028. The Louisiana mill is expected to support 5,400 jobs, including 1,300 direct positions.
Press release is available in its original form here.
Heat Treat Todaypublishes twelve print magazines a year and included in each is a letter from the editor. This letter is from the August 2026 Annual Automotive Heat Treatingprint edition. In today’s letter,Bethany Leone, former managing editor at Heat Treat Today, shares her insights on why technical standards and specifications only become truly valuable when paired with the shared experience of the people who apply them — and how learning from others’ failures, engaging with the heat treat community, and contributing your own perspective all strengthen the industry’s collective problem-solving.
Technical excellence isn’t built only through standards and specifications. What gives that information practical value is the shared experience of the people behind it.
Technical Info Needs People
Specifications explain what should happen. Experience teaches why it sometimes doesn’t. Studying standards and expanding your technical knowledge will make you an amazing engineer in theory, but the core identity of a heat treater is one who crafts solutions for ever-evolving situations. This comes through testing, practice, creative problem solving, and, inevitably, failure.
Failure teaches, though we often cringe at the word. It’s true, failure always comes with risk. So how do we fail well? One way is to listen to the stories of others: the trials, the testing, the creative problem solving, and even the mistakes.
Knowing the people in this community is the first step toward becoming part of its ongoing conversations. This is how trust is built. You may experience this by following your favorite author or speaker through various industry platforms.
Once we understand how others solve problems, standards and new processes become much easier to apply in our own work. Whether it be hearing the short shop analyses or reading fully published case studies, absorbing the problem-solving experiences of others informs our own problem solving.
Finally, after observing and learning from the heat treating community, the greatest value comes from being a part of the conversation yourself — from lighthearted comments to rigorous skeptical commentary.
In sum: Technical ideas become more useful when they’re shared by the people who put them into practice.
License to Engage
This publication reflects this reality of connected technical decision-making. Not only do we publish articles, we invite your participation.
Expanding how you can feel and be a part of the heat treat community and conversation, we are now spotlighting readers at the end of each magazine (see page 60).
We are also launching a few new features on page 59 of this issue that test your knowledge from the articles you read (Heat Treat Trivia) and encourage you to have a chuckle (Heat Treat Humor).
And of course, you may have noticed the Reader Feedback icon on various pages, reminding you that our door is always open for your questions, queries, and comments. Keep writing — we so appreciate your thoughts, however short or long.
Read…Then Contribute
Often, our most engaged readers become the clearest contributing authors.
But even if that’s not you, we want to hear from you: what you thought of that polarizing article about process change, whether you agree with the Heat Treat Trivia results or had a better answer, or are looking forward to an article on a specific topic. Every perspective strengthens the conversation, whether you realize it in that moment or not.
In aerospace heat treatment, few specifications carry as much weight — or as much apprehension — as AMS2750. This Technical Tuesday installment, adapted from a recent Heat Treat Radio conversation with ATP President Andrew Bassett and podcast producer/host Heather Falcone, offers insight into the evolution of AMS2750 and practical strategies for managing pyrometry compliance.
This informative piece was first released inHeat Treat Today’sAugust 2026 Annual Automotive Heat Treating print edition.
The Evolution of AMS2750
For many heat treat operations, AMS2750 represents the backbone of pyrometry compliance, yet it also presents a complex web of requirements that must coexist with broader quality management systems, client specifications, and audit expectations. Despite decades of revisions and clarifications, pyrometry continues to generate a disproportionate share of audit findings.
According to Andrew Bassett, president of Aerospace Testing and Pyrometry (ATP) and a long-time member of the teams responsible for writing the specification, the challenge is not simply the complexity of the standard; it’s how organizations manage it day to day.
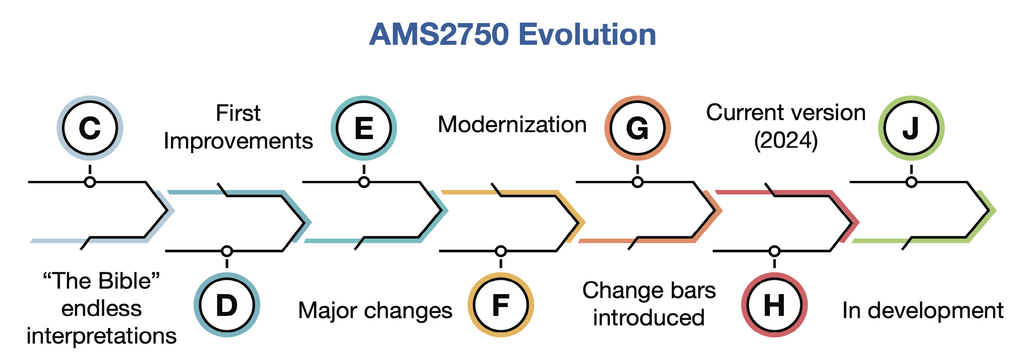
When Andrew first entered the industry, AMS2750 was at Revision C, a version many longtime heat treaters remember well. “Those who’ve been around long enough know that this revision of the spec was like the Bible,” Andrew says. “You gave it to a hundred different people, and you got a hundred different interpretations.”
Ambiguity in early versions of the specification created inconsistent interpretations across the industry. Over time, successive revisions, particularly the transitions through Revisions D and E, introduced significant changes aimed at improving clarity and consistency. The current Revision H reflects years of refinement.
Even so, Andrew believes the industry can continue improving how the specification communicates its intent. “My goal personally is to make sure that document is clear and understandable,” he explains. “Even if it’s 300 pages and we use stick figures and crayons to explain what the intent is — I’m okay with that.”
While aerospace heat treating specifications are generally clear about their purpose, pyrometry has historically been viewed as more difficult to interpret. Andrew hopes continued revisions and education will eventually eliminate that perception.
To Aerospace and Beyond
Although AMS2750 originated as an aerospace specification, its influence has expanded. According to Andrew, the standard is now widely used internationally and has been adopted by industries outside of aerospace manufacturing. In particular, the U.S. Food and Drug Administration has begun requiring compliance with AMS2750 for certain medical manufacturing processes. This means companies producing items such as dental drill bits or orthopedic implants must follow the same pyrometry standards used in aerospace heat treatment.
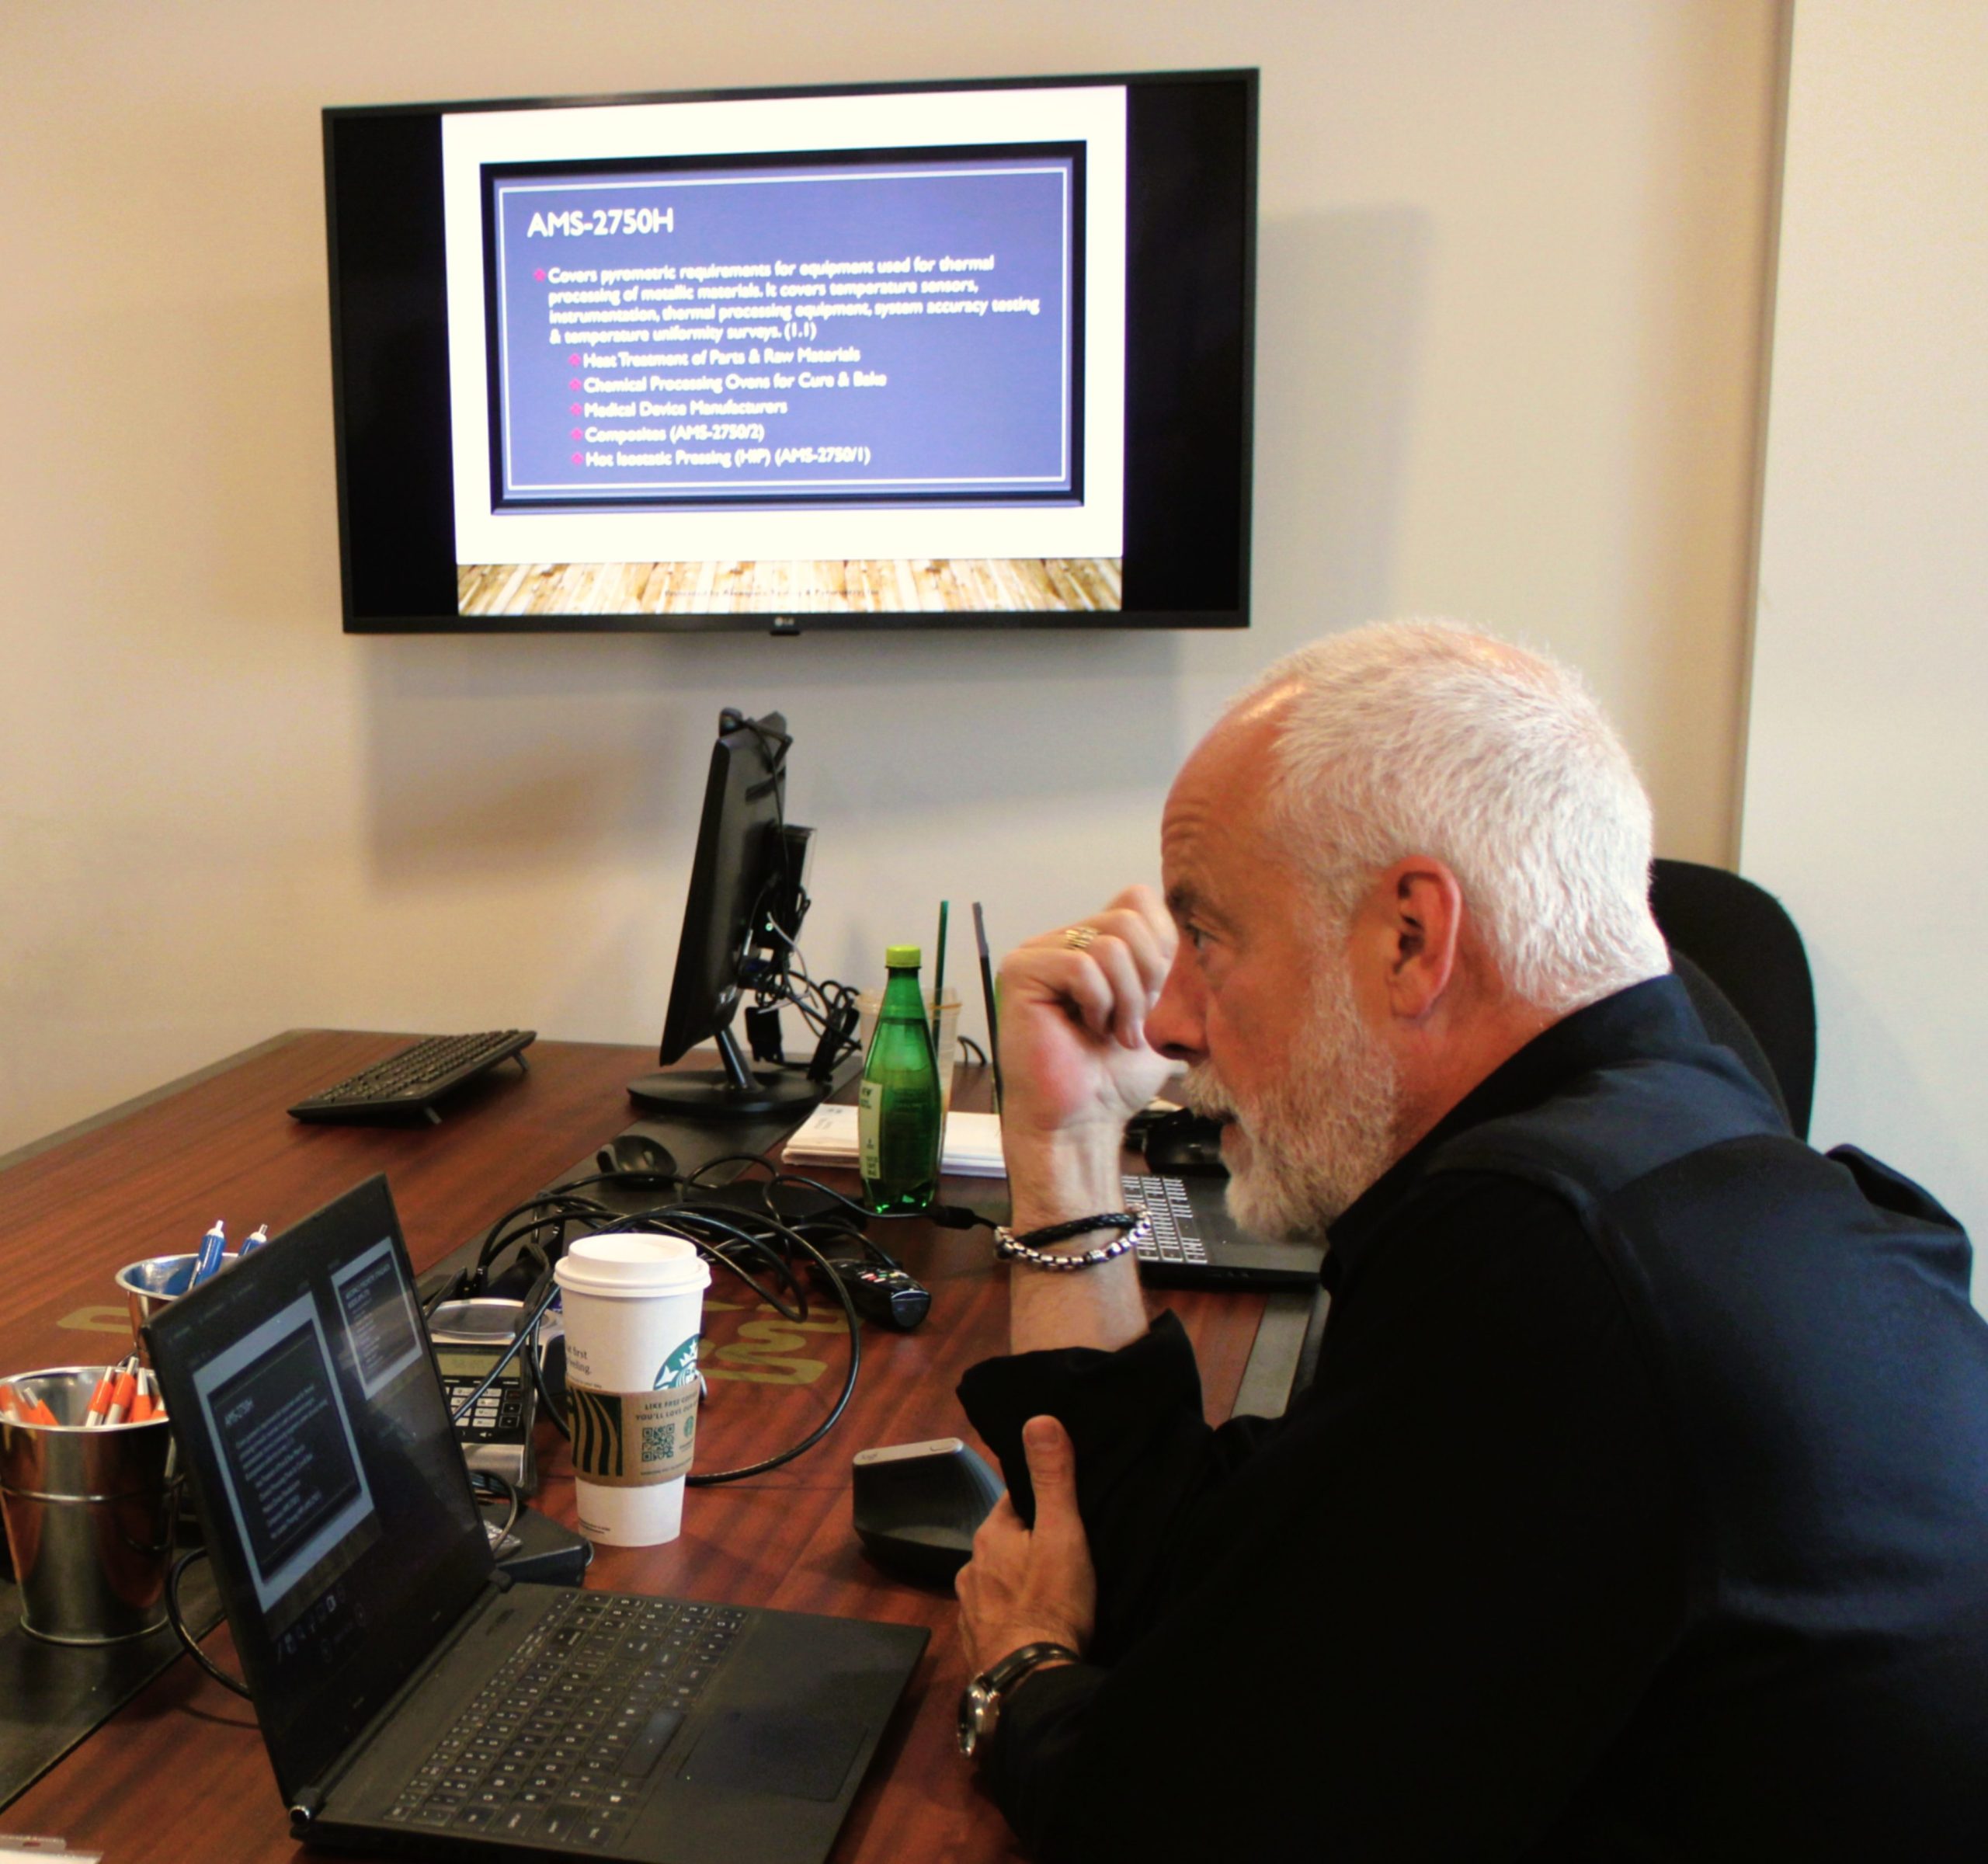
Andrew Bassett of ATP providing AMS2750 training | Image Credit: ATP
The expansion highlights the importance of understanding the intent of the specification, not just the literal wording of its requirements, for accurate interpretation at specific heat treat operations. For many organizations, achieving that understanding requires training and careful study.
Andrew notes that explaining the specification in practical terms has become increasingly important. When Andrew originally began providing training on AMS2750 at ATP, it was a 6- to 8-hour day class, providing a 30,000-foot view of the standard. Now, this has evolved into an easier to digest training program extended over two days at a “crop-dusting training level” that is designed to help suppliers interpret and apply the standard in real operating environments.
The Challenge of Managing Compliance
Understanding AMS2750 is one challenge; managing it alongside other requirements is another. Many heat treaters must balance pyrometry requirements with broader quality management frameworks such as ISO and Nadcap, as well as client-specific specifications from aerospace primes.
Andrew emphasizes that the first step in managing this complexity is gaining a clear understanding of what work is being performed and who the ultimate client is. For example, a commercial heat treater may receive a purchase order from one supplier, but the parts may ultimately be destined for a major aerospace manufacturer with its own pyrometry requirements. Without that insight, organizations can unknowingly miss critical compliance obligations. Once the applicable requirements are understood, companies must establish systems to manage them consistently, particularly when multiple specifications overlap or conflict.
In some cases, individual client specifications may differ from or extend beyond AMS2750 requirements, creating additional layers of oversight. For example, certain aerospace primes have their own pyrometry requirements that differ slightly from the standard. Managing those differences across multiple furnaces, calibration schedules, and testing procedures can quickly become a significant administrative challenge.
Documentation Drives Compliance
For many heat treaters, managing pyrometry compliance historically meant relying on manual systems: spreadsheets, paper logs, and physical binders containing calibration reports, temperature uniformity surveys (TUS), system accuracy tests (SAT), and thermocouple records.
Andrew remembers those early days well. “When we would get a new client, I would go buy a bunch of notebooks from Staples and put in their little dividers of a pyrometry program together,” he recalls. While the system worked, spreadsheet-based tracking introduced the possibility of human error, as it relied heavily on manual data entry and careful recordkeeping. But Andrew emphasizes, “When it comes to compliance audits, human errors cannot happen.”
Why Pyrometry Generates So Many NCRs
One of the most striking statistics in aerospace heat treatment audits is that 80% of nonconformance reports (NCRs) is tied to pyrometry. For someone involved in writing the specification, that statistic raises an important question: why?
Andrew believes part of the issue lies in how requirements are interpreted and implemented across different organizations. Even when the specification is clear, documentation gaps or process breakdowns can lead to findings.
A common example involves maintenance documentation. When a furnace undergoes preventive or unscheduled maintenance, the work must be recorded and reviewed to determine whether additional pyrometry testing is required. In some cases, maintenance may be completed and documented, but the required quality approval is never recorded.
These types of seemingly small documentation gaps can easily lead to NCRs during audits.
Moving Compliance from Paper to Platform
As documentation requirements have grown more complex, many aerospace heat treaters have found that the real challenge is not only collecting the data; it is organizing, reviewing, and presenting it in a way that satisfies auditors. Nadcap accreditation, AMS specifications, and client requirements all demand rigorous process monitoring and recordkeeping.
Recognizing these challenges, ATP developed Aerospace Compliance Software (ACS), a software platform designed to support aerospace compliance and documentation requirements tied to standards such as AMS2750 while also helping companies prepare for Nadcap audits and maintain the documentation expected by aerospace primes and OEMs.
“Now we have a system that’s 100% not just a pyrometry tool — it’s also a compliance tool,” says Andrew. “New features we keep adding into the system is with the focus on compliance, just not pyrometry-related tools.” This includes preventative maintenance leak rate testing checks and thermocouple replacement schedules. Andrew adds, “It’s also and most importantly a self-checking software to not only the industry specifications, but client internal specifications. It doesn’t have to be solely what AMS2750 says,” allowing users to verify compliance with various specifications.
By organizing documentation in a structured, traceable format, tools like ACS can help heat treaters more easily verify compliance with aerospace requirements and prepare for audits. As specifications continue to progress, many in the industry are turning to digital systems to simplify documentation while maintaining the level of process control that aerospace work demands.
The Value of Industry Participation
For Andrew, one of the most effective ways companies can improve their understanding of compliance requirements is by participating directly in the industry organizations that shape them. “This is something I preach constantly with our client base,” he says. “If you’re Nadcap accredited, firstly, go to a meeting.”
Misconceptions about who is involved in writing the standards often deter heat treat industry representatives. “I had this myth early on in my career that this golden group of aerospace gods were creating standards,” Andrew recalls. “When I showed up to the meeting, there were more suppliers there writing the standards than there were the primes.” That participation ensures the specification reflects real-world operations, and it gives companies a voice in the requirements they must ultimately follow.
Staying Ahead of the Standard
Click on the image above to get the full interview with Andrew Bassett of Aerospace Testing and Pyrometry.
In aerospace heat treating, compliance is never static. AMS2750 will continue to evolve, though Andrew expects future revisions to focus primarily on clarification rather than sweeping changes. The current review efforts for Revision J is already underway. As with previous updates, the committee maintains a running list of questions and issues that arise after each release. These items are reviewed and incorporated into future revisions when appropriate.
Maintaining precise pyrometry practices and ensuring that information is recorded and readily available during audits is key to complying with AMS2750. Standards like AMS2750 remain central to ensuring thermal processes are controlled, repeatable, and fully traceable. For heat treaters operating in aerospace, success increasingly depends not only on achieving the correct metallurgical results, but also on demonstrating compliance through clear, well-managed process data.
The Benefit of Knowledge Sharing
After more than three decades working with pyrometry and industry standards, Andrew says the most rewarding part of his work remains helping others understand the requirements. “Anytime I meet somebody and we talk pyrometry, my business card comes out,” he says. “If there’s a question you have, I’m more than happy to answer it to the best of my abilities.”
For him, the goal is simple: ensuring that suppliers understand the specification well enough to succeed. This is more than just passing audits; it means building robust and reliable thermal processing systems. Because in the end, managing AMS2750 is not just about checking boxes. It’s about building the knowledge and systems that keep the entire heat treating process running accurately, consistently, and safely.
This article was written by Heat Treat Today’s Editorial Team.