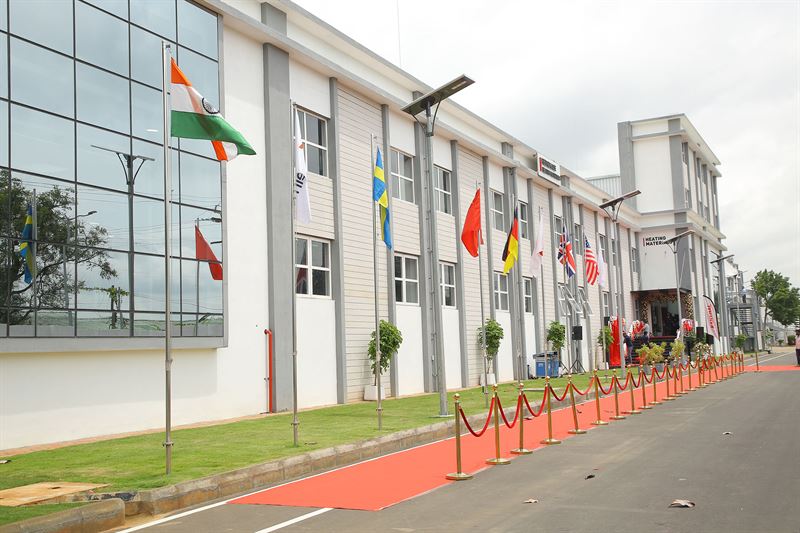
With around 250 new employees in the U.S., Poland, Germany, France, and China, the AICHELIN Group is expanding to over 1,350 employees. The deal represents the largest acquisition in the company’s history.
The acquisition expands the Group’s technology portfolio with leading expertise in nitriding furnaces. The integration of the NITREX sites will take place step by step in coordination with local leadership teams.
Christian Grosspointer CEO AICHELIN Group Source: AICHELIN Group, Tobias Fröhner
“This acquisition is an important step in the execution of our strategy. We want to grow meaningfully, with a strong foundation, local proximity, and technological excellence. Together with NITREX, we are combining know-how and regional strengths for the benefit of our customers, employees, and all stakeholders,” said Christian Grosspointner, CEO of the AICHELIN Group.
The AICHELIN Group has set a clear roadmap for sustainable growth and technological advancement. The focus is on diversification into new industries and applications, driven both by in-house development initiatives and targeted acquisitions.
Press release is available in its original form here. Earlier developments of this story were reported on by Heat Treat Todayhere.
Heat Treat Today is pleased to begin a new column series, Below Zero with Jack Cahn, co-founder of Deep Cryogenics International, a deep cryogenics treatment (DCT) company. In this series, Jack will explore the science, applications, limitations, and challenges of cryogenic treatment, including technology adoption, equipment, test methods, service providers, and end users.
This informative piece was first released inHeat Treat Today’sSeptember 2025 Annual People of Heat Treat print edition.
What is DCT?
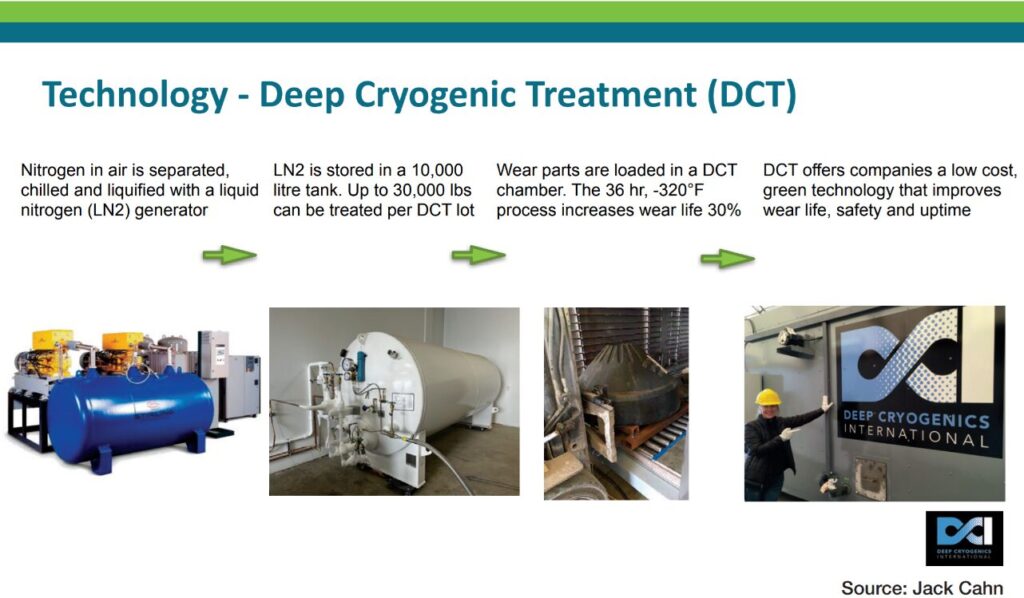
So, what is DCT and how does it differ from shallow cryogenics (-60°F to -176°F)? DCT uses a 36-hour process at -230°F to -320°F, which refines atomic-level grain structure, precipitates carbides in alloys, triggers the TRIP/TWP effect, and increases dislocation density in metals. This results in 20-40% greater wear life, 10-20% higher yield strength, and 10-20% less corrosion.
Unlike heat treatment or coatings, DCT is non-toxic, chemical-free, and generates no environmental waste. It is low-cost, works on both ferrous and non-ferrous materials, supports mixed alloys during treatment, and allows economy-of-scale batch processing. However, despite academic backing, cost-effectiveness, and acceptance by the heat treat community, DCT has remained in the undeveloped backwater of material improvement processes.
DCT doesn’t work on all metals all the time. Despite early studies and claims of 200% benefit, DCT improvement depends on the alloy chemistry, the method of manufacture, prior heat treatment, and the item’s failure mode. While lab results show significant improvements, field results often fall short, requiring further research to match materials to specific benefits. Some materials don’t improve from DCT, while others show benefit only in a single metallurgical characteristic. Extensive applied research is needed to link each material alloy to specific end-use and actual benefits.
Limited Industrial Equipment and Scale-Up
Most DCT chambers are small, modified deep freezers with high LN2 consumption due to latent heat loss. Very few can handle large industrial volumes at the required low temperatures. Until recently, DCT has bottlenecked at early Technology Readiness Levels, which has slowed adoption, especially in sectors like energy, aerospace, and automotive.
Figure 2. The DCT process
No Certification, Acceptance, or Test Standards
While heat treatments are ISO, Nadcap and ASTM certified, DCT lacks similar standards, hindering widespread industry acceptance. Although sectors like motorsports and knife-making are advocates, they don’t require testing, limiting DCT’s scalability.
Lack of Collaboration Among DCT Service Providers
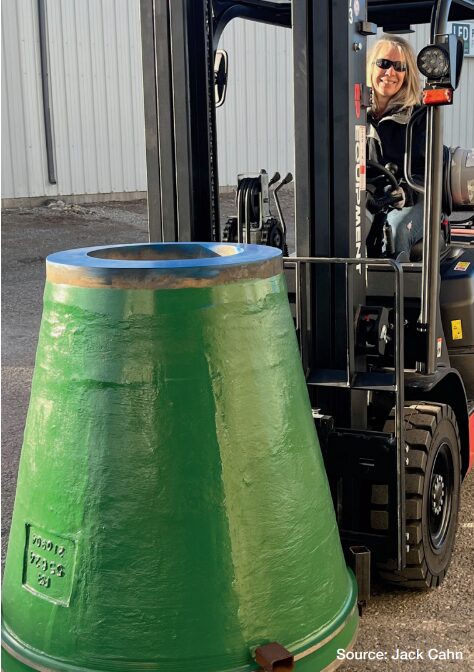
Figure 3. DCI President Linda Williams loading a 3,500-pound pump cyclone for DCT
The DCT industry is fragmented. We are generally independent service providers who offer localized DCT; some of us also build DCT chambers. Fewer than 50 companies globally offer DCT as a stand-alone service, and another 750-1,000 companies (mostly existing heat treaters) provide cryogenic treatment as an ancillary service. There are dozens of heat treat organizations, industry trade groups, and trade journals that share technical advice, innovation news, or a community forum — deep cryogenics has nothing like that. Just our individual company websites, occasional articles, and reliance on DCT “chatter.”
After discussing the industry’s challenges with Applied Cryogenics Inc. President Dr. Jeff Levine and DCI President Linda Williams, I reached out to 100 DCT providers, scientists, and industry professionals. About 25% responded — scientists curious about DCT, engineers interested in certification standards, heat treaters seeking greater opportunity, and service providers keen to work together — who supported the formation of a trade organization to:
Promote DCT technology awareness and adoption
Create a working group to develop DCT standards and certifications
Showcase companies, services, and products
Increase professionalism and quality in cryogenic treatment
Foster collaboration and knowledge-sharing
Both Megan Galeher and Anne DiPaola have offered to promote an emerging cryogenic treatment group under the CSA mantle, lending its scientific and professional credibility. Doug Glenn, publisher of Heat Treat Today, has offered similar support. Heat treaters have thrived globally by navigating the scale-up process and adhering to certification standards required by commercial and industrial users. They have also focused collaboratively on quality, innovation, and knowledge-sharing within their industry.
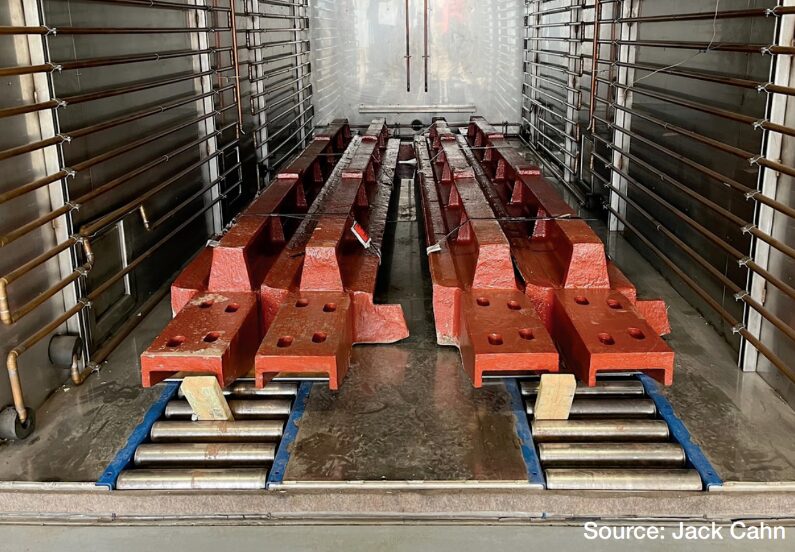
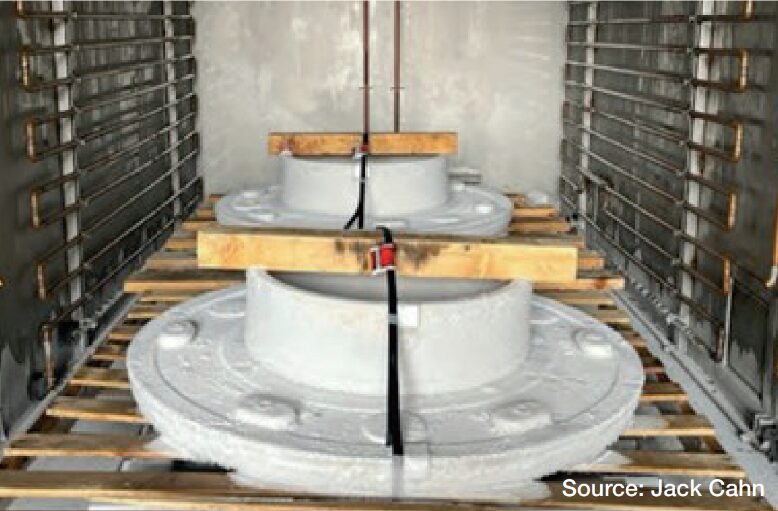
Figure 4. DCT of O&G slurry pump bushings
I believe a cryogenic treatment organization could launch under the combined CSA/heat treat umbrella. What do you think? Email your thoughts to me at jack@deepcryogenics.com, and I’ll share them in my next column. Thanks for welcoming DCT into the community!
About The Author:
Jack Cahn Chief Technologist Deep Cryogenics International
Jack Cahn is the chief technologist and co-founder of Deep Cryogenics International (DCT) — a U.S. cryogenic treatment facility and equipment manufacturer. With over 25 years conducting scientific testing and publishing technical articles, Jack and DCI President Linda Williams provide DCT awareness, adoption, equipment, and treatment services worldwide.
For more information: Contact Jack Cahn at jack@deepcryogenics.com.
Arconic Corporation (“Arconic” or the “Company”) will boost high purity aluminum (HPA) capacity for aerospace and defense applications at its Davenport Works plant, a facility with in-house heat treatment. The $57.5 million project has effectively doubled domestic production of high purity aluminum, a critical material to aerospace and defense applications.
Diana Perreiah Executive Vice President of Rolled Products North America Arconic Source: Arconic
The expansion is being carried out at the Davenport Works plant in Iowa and was commissioned on September 25. The project was supported by an award of $45.5 million from the U.S. Department of War in 2023, utilizing Defense Production Act (DPA) Title III authorities. The Defense Production Act Title III program supports domestic industrial capabilities essential to national security.
Diana Perreiah, executive vice president of Rolled Products North America for Arconic, said, “Arconic is honored to support American leadership in advanced manufacturing by expanding domestic production of high purity aluminum for next-generation aerospace and defense applications. This project strengthens critical supply chains and supports national defense priorities, while reinforcing our role as a trusted partner in delivering materials essential to U.S. security and competitiveness.”
With the design and installation of two new furnaces and advanced control and automation systems, the project provides the United States surge capacity for HPA production and mitigates potential risks to national security in the event of an industrial mobilization. Among the defense applications that require HPA are the bulkheads for the F-35 and advanced armor plate for the Joint Light Tactical Vehicle.
At a ribbon-cutting ceremony on September 25, distinguished guests included Iowa Governor Kim Reynolds, Lieutenant Governor Chris Cournoyer, U.S. Senator Joni Ernst, U.S. Representative Mariannette Miller-Meeks, State Representative Gary Mohr, Riverdale Mayor Anthony Heddlesten, Iowa Association of Business and Industry President Nicole Crain, and Quad Cities Chamber of Commerce president and CEO Peter Tokar III to mark the milestone of commissioning the facility.
Arconic Corporation, headquartered in Pittsburgh, Pennsylvania, is a leading provider of aluminum sheet, plate and extrusions, as well as innovative architectural products, that advance the ground transportation, aerospace, building and construction, industrial and packaging end markets. For more information, visit www.arconic.com.
Press release is available in its original form here.
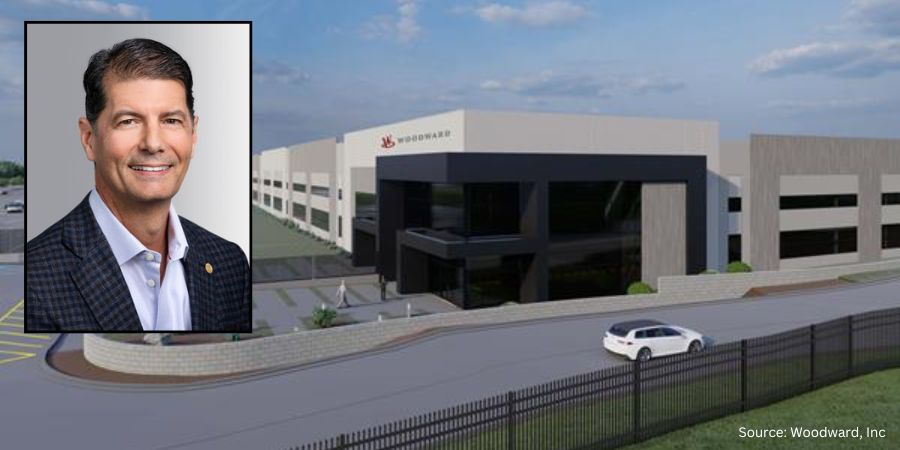
We’re celebrating getting to the “fringe” of the weekend with a Heat TreatFringe Fridayinstallment: Woodward, Inc, a manufacturer with in-house heat treat operations which serves the aerospace industry, has announced its plan to build a precision manufacturing facility in Greer, South Carolina, in Spartanburg County. The new site is a strategic investment for the company. The 300,000-square-foot facility is set to open in 2027 and will focus on production of servo-hydraulic actuation systems, which are critical components used in aircraft flight control.
While not exactly heat treat, “Fringe Friday” deals with interesting developments in one of our key markets: aerospace, automotive, medical, energy, or general manufacturing.
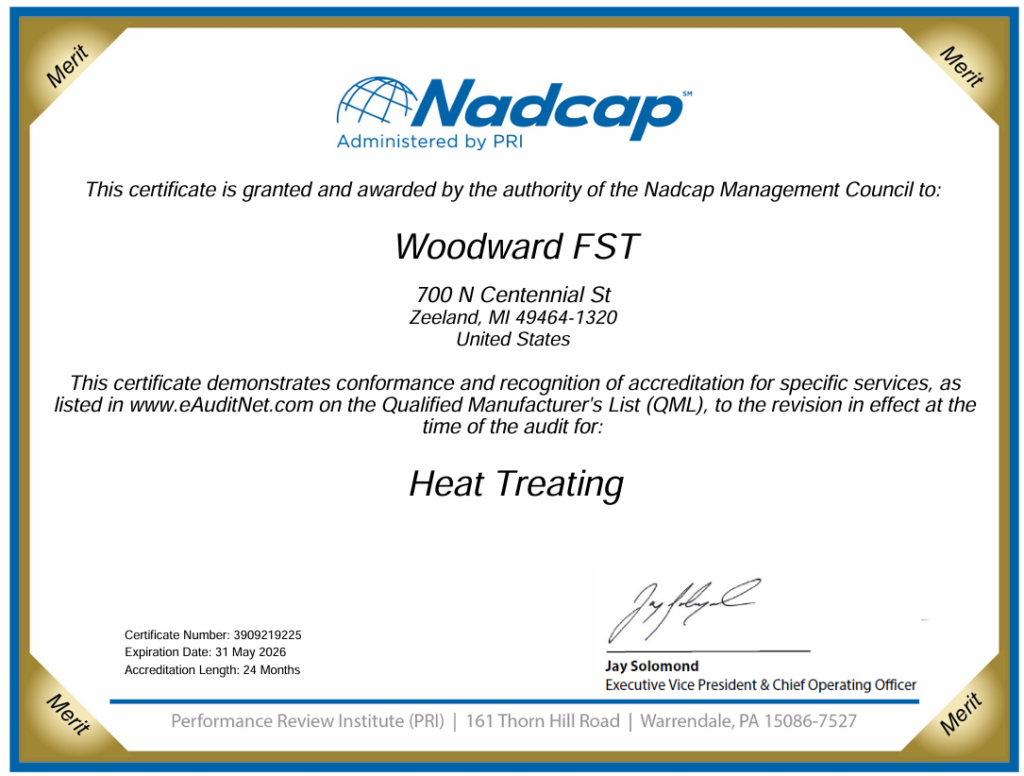
Woodward’s Nadcap certification Source: Woodward, Inc.Chip Blankenship Chairman & CEO Woodward, Inc.
Initially, most of the factory’s capacity will be dedicated to producing spoiler actuation for the Airbus A350. These critical control systems are mounted on the upper surface of aircraft wings and play a vital role in managing lift and enhancing flight performance and safety. The site has potential to expand capacity as the company meets growing demand for its aerospace technologies.
The facility is expected to create approximately 275 high-quality jobs in manufacturing, engineering, and business operations, with potential for significant workforce expansion in the future.
“The selection of Woodward to supply Airbus with spoiler actuation systems and our investment in South Carolina represent a major milestone for Woodward and our commitment to delivering leading controls solutions to our customers,” said Chip Blankenship, chairman and CEO of Woodward, Inc. “It will be a showcase manufacturing site, much like our Rock Cut campus, vertically integrated, highly automated, and built on the capabilities and methodologies in operational excellence we’ve developed through our LEAP and GTF aircraft engine programs.
“Beyond supporting the Airbus A350, this facility positions us to extend our hydraulic flight control design and industrialization expertise to additional applications as well as other commercial aircraft manufacturers. We’re proud to bring jobs and economic opportunity to Spartanburg County as we fulfill our purpose to design and deliver energy control solutions our partners count on to power a clean future.”
Henry Dargan McMaster Governor of South Carolina Source: South Carolina Office of the Governor
After an extensive nationwide search, Woodward selected Spartanburg County for its robust manufacturing infrastructure, access to highly skilled aerospace talent, and proximity to key suppliers. The investment is supported by an incentive package from the State of South Carolina, Spartanburg County, and local economic development organizations.
“When global companies like Woodward, Inc. decide to invest in our state, it further solidifies South Carolina’s impressive reputation in the manufacturing industry. We look forward to creating a long-standing partnership with the company and seeing the strong impact of these approximately 275 new jobs in Spartanburg County,” said Henry McMaster, Governor of South Carolina.
Press release is available in its original form here.
Argonne scientists have been investigating 3D-printed steels for use in next-generation nuclear reactors. In two studies, they used X-ray diffraction and electron microscopy to reveal how heat treatments can help 3D-printed steels endure nuclear service.
Heat Treat Todayhas added additional resources for heat treaters, those in the nuclear energy sector, and new professionals in the industry who would like to learn more throughout this release. Make sure to click the links throughout to access all of the information!
Crucial components within nuclear reactors are often made using stainless steel; it fortifies falls and withstands decades of extreme heat, pressure, and irradiation. Additive manufacturing — or 3D-printing — offers a way to produce complex stainless steel parts more efficiently, however it can leave behind defects in the microscopic structures of steel parts, impacting their performance. Two recent studies have shown how additively manufactured steels compete with their conventional counterparts.
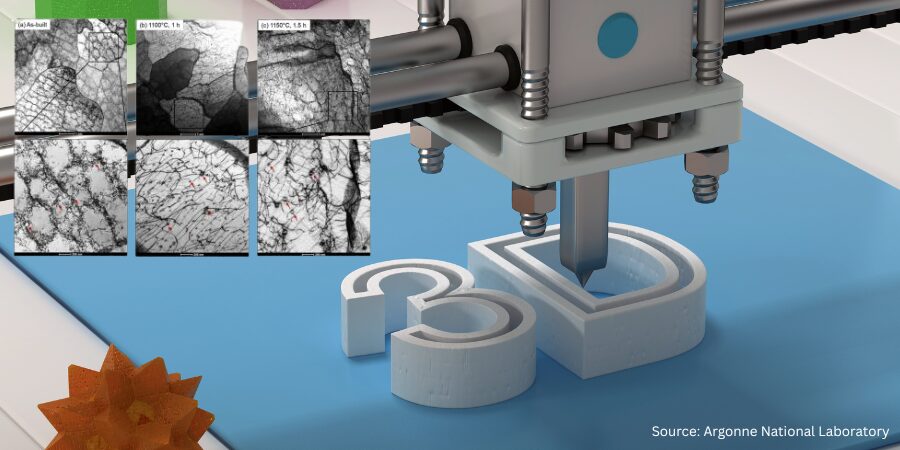
Scanning transmission electron microscopy images of 3D-printed 316H stainless steel before (a) and after (b and c) two heat treatment techniques. Red arrows indicate nano oxides, which greatly impact the steel’s response to heat treatment. Source: Argonne National Laboratory
Researchers at the U.S. Department of Energy’s (DOE) Argonne National Laboratory used X-ray diffraction and electron microscopy to discover nanostructures of steel made with an additive manufacturing method called powder bed fusion (LPBF).
They printed two samples of stainless steel alloys with LPBF. In one study, they focused on 316H, an established type of stainless steel for structural components in nuclear reactors, and in the other they focused on Alloy 709 (A709), a newer alloy designed for advanced reactor applications. Both studies revealed the differences between 3D-printed steel and conventionally wrought steel, and also highlighted how printed steels responded to various heat treatments.
Before these steels can be relied upon in reactor environments, the nuclear industry has discovered their growing need for a deeper understanding of how to control 3D-printed steels.
“Our results will inform the development of tailored heat treatments for additively manufactured steels,” said Srinivas Aditya Mantri, an Argonne materials scientist who co-authored both studies. “They also provide foundational knowledge of printed steels that will help guide the design of next-generation nuclear reactor components.”
Using Heat Treatment for Repair
In LPBF, a laser melts precise designs into a metal powder one layer at a time until a solid, 3D metal object is formed. The repeated heating and cooling caused by the laser changes the microstructures of the steel.
Printed steels, for example, show higher numbers of dislocations — a defect of non-uniform shifts in a steel’s structure. Dislocations strengthen steel, but they also increase its internal stress, leaving it more vulnerable to fracture.
Heat treatment is a way to relieve this stress. Heat treatment changes the microstructures of a metal and can repair dislocations as high temperatures allow atoms to shift. Recrystallization is a product of heat treatment where new, strain-free grains replace the original structure. However, keeping some dislocations can have benefits of promoting precipitation of particles that can improve a material’s performance.
3D-printing 316H, a Standard for the nuclear industry
In one of the studies, researchers focused on 316H, comparing the microstructures of wrought and LPBF-printed samples by scanning electron microscopy (SEM) and scanning transmission electron microscopy.
Transmission electron microscopy images of 3D-printed and heat treated Alloy 709 stainless steel. The experiments revealed a high number of dislocations in their microstructures. Source: Argonne National Laboratory
At a second office, they used in situ X-ray diffraction experiments. At beamline 1-ID, the team evaluated the samples using high-energy X-rays while they underwent varying heat treatments of solution annealing.
“The high flux of photons provided by the APS allowed us to track the evolution of the microstructures in real time during the dislocation recovery process,” said Xuan Zhang, another materials scientist at Argonne and co-author on both studies. “That’s something you can only achieve with a synchrotron X-ray facility like the APS.”
What was revealed is that recrystallization was inhibited by nano oxides, which are nanoscale defects common in 3D-printed steel.
“Nano oxides act as a sort of barrier to the movement of dislocations and the growth of new grains, causing some dramatic differences between the response of LPBF-printed and wrought steels to heat treatment,” Zhang said. “For example, the printed samples started to recrystallize at temperatures several hundred degrees higher than their wrought counterparts.”
The effects of these discoveries on the mechanical properties of the metal are essential, particularly strength under tension and resistance to creep. Creep is the slow deformation of a material under consistent mechanical load, which is relevant for nuclear applications.
3D-printing A709, An Up-And-Coming Heavy-Hitter
The other study focused on A709, a newer advanced stainless steel designed for high-temperature environments such as inside sodium fast reactors. Researchers studied samples of A709 printed with LPBF, making it the first experimental look at an additively manufactured form of the alloy.
While investigating the strengths of the heat treated samples under tension, both at room temperature and 1022°F (550°C) — a temperature relevant to sodium fast reactors — the printed A709 showed higher tensile strengths than the wrought A709. This is most likely on account of the printed samples beginning with more dislocations, which also led to the formation of more precipitates during heat treatment.
“Our research is providing practical recommendations for how to treat these alloys,” said Zhang, “but I believe our biggest contribution is a greater fundamental understanding of printed steels.”
Press release is available in its original form here.
A leading aviation technology company will receive two new furnaces from a manufacturer of metal heat treatment solutions with North American locations. The furnaces will be used in the production of engine components, particularly directionally solidified and single crystal castings.
Sławomir Woźniak CEO SECO/WARWICK Group
SECO/WARWICK will provide a Vector vacuum furnace and a VIM JetCaster furnace with a capacity of 25 kg, enabling the melting of nickel and cobalt alloys at temperatures up to 1700℃ (3092°F) to the Chinese aviation manufacturer.
“The device ensures a low percentage of casting defects, both macro and microstructural, as well as a significant reduction of the directional solidification casting process compared to the classical process due to increased mold withdrawal speeds,” said Sławomir Woźniak, CEO of SECO/WARWICK Group.
The latest jet engines use advanced blades cast produced by single crystal technology. The control system meets the needs of precise processes: casting, temperature control, as well as comprehensive data collection.
The Vector vacuum furnace is designed for aging and solution heat treatment processes. It achieves a maximum temperature of 1400℃ (2552°F) with a uniformity of ±5℃ (9°F) and can handle components with a total mass of up to 800 kg. Due to a high level of vacuum (up to 10⁻³ Pa), processes take place without intergranular oxidation, resulting in a quality surface for the components.
Press release is available in its original form here.
Heat Treat Today publishes twelve print magazines annually and included in each is a letter from the publisher, Doug Glenn. This letter is from theSeptember 2025 Annual People of Heat Treat print edition.
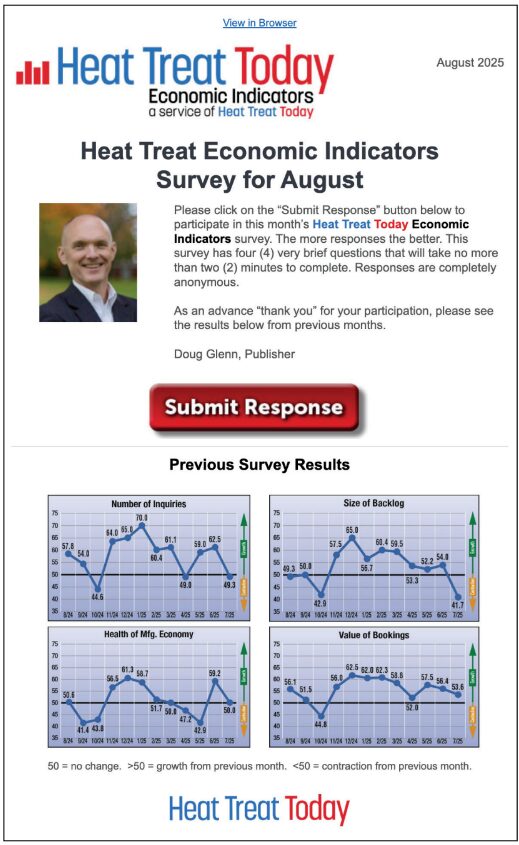
Knowing whether the North American thermal processing economy is up or down compared to last month or last year is a question that many want to know. And, as you may already know, there are essentially ZERO industry-specific economic indicators measuring our market. Except for one — Heat Treat Today’s Economic Indicators, or the heat treat economic indicators (HTEI).
A Little History
A little history and then let’s discuss Heat Treat Today’s HTEI. Back in the mid-1990s or early 2000s, I and the team at Industrial Heating established the first industry-specific economic indicators. Those indices survived for roughly 20 years before passing into oblivion when Industrial Heating shut their doors in 2023.
The data for the indicators were not saved…to the best of my knowledge. During those 20 years, many, many companies in the thermal processing industry relied on the data from those indices to help plan their business. I recall specifically speaking to one of the top-level guys at Bodycote who confessed that they used the economic indicators together with some other macro-economic data to help with their annual strategic planning. There were many others as well who either called or emailed asking questions about the indicators or asking for permission to use them in reports.
After Industrial Heating shuttered the indices, Heat Treat Todaypicked them up and has been collecting and reporting industry-specific economic data since that time.
The 4 Indices
There are four indices. All four are forward looking and none require a company to report any numbers back to us. Here’s how they work.
On the first business day of each month, Heat Treat Today sends an email survey to over 800 supplier contacts in the North American heat treat market. Recipients are asked four simple opinion questions. All four questions ask essentially the same thing: Do you think the next 30 days will be better or worse or the same as the past 30 days? We ask this question for four specific areas:
The number and/or value of inquiries
The number and/or value of bookings
The size of the company’s backlog
The general health of the manufacturing economy
Respondents pick a number between −10 and +10 for each of the four questions with −10 being much, much worse and +10 being much, much better. Respondents can also skip one or more questions if they have no opinion or do not want to share.
The responses are aggregated and converted into an index very similar to the Purchasing Managers Index where the index number 50 represents no change, numbers above 50 represent growth, and numbers below 50 represent contraction.
More Responses Are Better
As with any statistical analysis, the larger the sample set, the more reliable the data. This is true for HTEI as well. With over 800 solicitations going out each month, we’re getting a pretty decent response, but more responses would be better. Responding to the survey takes less than two minutes, so time is not really an issue. No numbers need to be compiled or calculated to respond, which keeps it simple. The questions are all “opinion” questions about whether you anticipate the next 30 days will be better than the past 30 days.
We would love to have you join the ranks of people that respond regularly to the HTEI monthly emails. If you would like to receive the monthly survey on the first business day of each month, please send your email address to me and I’ll add you to the list. You can email me at doug@heattreattoday.com.
Thanks for participating.
Doug Glenn Publisher Heat TreatToday For more information: Contact Doug at doug@heattreattoday.com
In this Technical Tuesday installment, Jim Roberts, president of U.S. Ignition, examines various flame profiles in heat treat operations. Today’s Combustion Corner compares gravitational lift, premix burners, fuel nozzle fixed air mixing burners, and nozzle mixing burners, while exploring design improvements to keep you well informed.
This informative piece was first released inHeat Treat Today’sAugust 2025 Automotive Heat Treating print edition.
A furnace guy walks into a bar and shouts, “Straighten UP!” The other furnace guys respond, “It won’t work!”
Thus begins another wander down combustion lane where we try to figure out what I’m talking about. We have discussed in other articles how various fuels and sources of air (and everything else) can affect the heating rates produced by our combustion equipment. We have talked about fire. We haven’t talked about what fire looks like.
So, in the following column and subsequent releases we are going to talk about flames and fire, and why there are a fairly substantial number of flame profiles available to heat treaters, steel makers, and all of you high-temp-type people. Why are there different flame shapes, and what does flame color do for you?
Burner Types
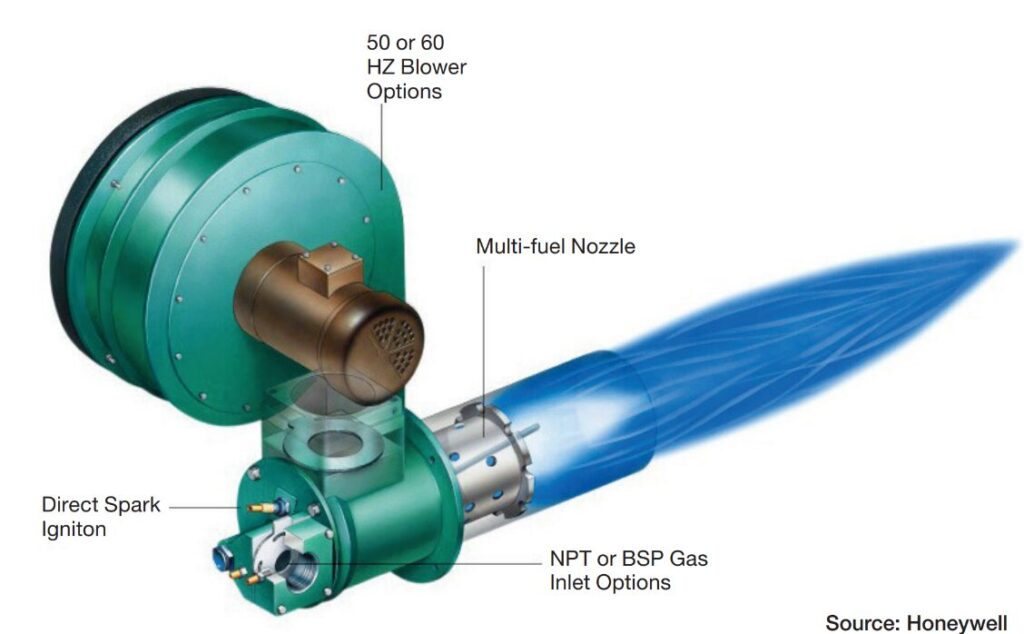
Figure 1. Nozzle-mixing burner ThermJet cutaway
Firstly, let’s start with the various types of burners commonly used in the art of high-temp processing work.
Gravitational lift: This type of burner is exactly what it sounds like; it works just like a candle. The fuel/air mix is naturally rising with the thermal current of the flame and combusting as the flame rises, climbing the heat column.
Premix burners: This is where the fuel and air are mixed together and then ignited. By controlling the percentages of fuel and air in the mixture, we control the characteristics of this flame.
Fuel nozzle fixed air mixing burners: This is where a steady stream of oxidant (air) is flowing, and the fuel is throttled up and down to affect ignition and capacity of fuel.
Nozzle mixing burner: Finally, and by far the most used in our industry, this is where the fuel and oxidant mix internally in the burner, and a flame configuration is determined by the burner outlet or the mixing nozzle. (See Figures 1 and 2.) You may hear burner nozzles referred to as a cup, a spinner, flame retainer, just about any type of reference. You may also hear them referred to as a danged hot thing — an accurate description as well — so don’t touch.
Design Improvements
With development of the nozzle mixing burner 60+ years ago, design improvements began in earnest. One of the first patents for nozzle mixing industrial burners was issued to Eclipse Fuel Engineering in 1967. Pretty soon there were all sorts of designs and patents, as burner companies raced to improve reliability, performance, and heat delivery characteristics.
Figure 2. Nozzle-mixing burner Eclipse Thermair
Some of the concepts that came along in the subsequent years were “air staged” burners. In this design feature, the fuel is delivered in the center of the flame nozzle. Progressively changing air holes in the nozzle stages the combustion of the fuel as it makes contact with the air. As the gas burns and the exhaust gas expands, it will often increase volumetrically by up to seven to eight times its cold state condition. That’s a lot of expansion, and it forces the pressure in the burner body to increase at an amazing rate. As the flame progresses through the burner and seeks the exit point (the part we see, you know, the fire), it can be moving along at — get this — flame speeds up to 400 feet per second!
That’s enough for today. We’ll pick this conversation back up next month.
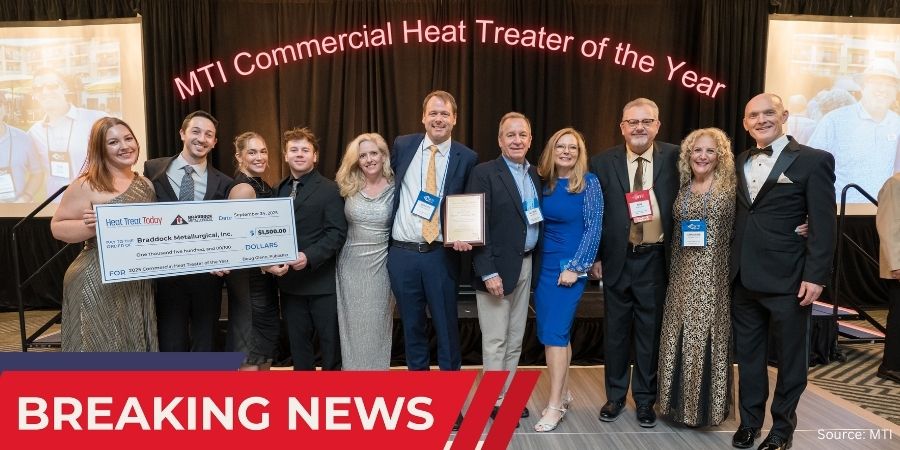
On Wednesday, September 24, Heat Treat Today, in cooperation with the Metal Treating Institute (MTI), presented the 2025 Master Craftsman Award (also known as the Commercial Heat Treater of the Year Award) to Braddock Metallurgical, Inc.
The award was presented at the formal awards presentation banquet at the Metal Treating Institute Fall Meeting and Conference in Napa, California. Pictured above from left to right is Natalie Littler, Jason Kusher (Plant Manager, Braddock Metallurgical), Grace Blasco, Erik Gieger (Quality Manager, Braddock Metallurgical), Mary Braddock, Griffith Braddock (VP, Braddock Metallurgical), George Gieger (CEO, Braddock Metallurgical), Rose Gieger, Roy Adkins (Corporate Director of Quality, Braddock Metallurgical), Christine Adkins, and Doug Glenn (Publisher, Heat Treat Today).
This award, whose applicants are judged by a panel of previous recipients, is given to the company that demonstrates making a positive impact on their community and their industry. Recognition is based on quality programs, pollution and hazardous waste control, community involvement, and industry leadership.
At the award presentation, Doug Glenn highlighted how “the company’s commitment to quality and innovationis evident in the numerous quality certifications and its approach to assisting customers. To name just one quality system accomplishment, the company has achieved Merit Standing for their AS9100 Rev D Quality System for four of their locations.”
He continued, “When it comes to the company, it has been actively working towards reducing its carbon footprint, promoting resource conservation, and adopting sustainable sourcing practices by: Monitoring asset utilization to reduce wasted energy, recycling oil and wastewater, performing thermal surveys of electrical panels, tuning combustion systems, using only Federal and state regulated waste removal companies, and monitoring storm water activities at all facilities.”
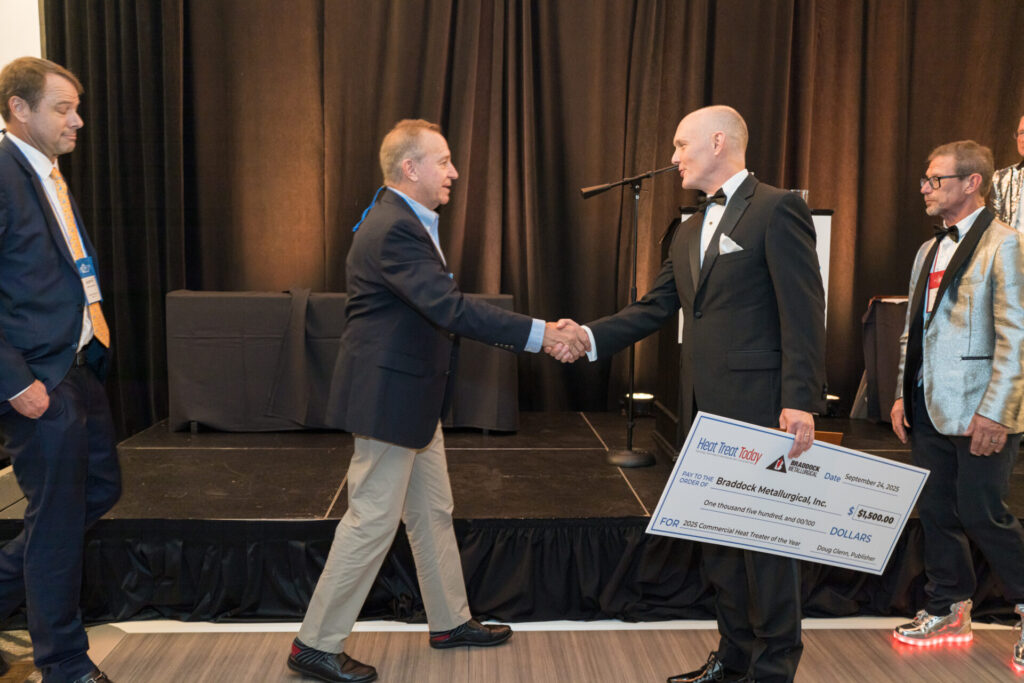
Commercial Heat Treater of the Year CertificateGeorge Gieger shaking hands with Doug Glenn
Braddock Metallurgical, Inc. received a plaque commemorating this auspicious recognition and a scholarship fund of $1500 from Heat Treat Today that was matched with another $1500 from MTI’s Education Foundation. The heat treater will award this $3000 to a high school or college student who is pursuing an education in heat treat.
Congratulations to Braddock Metallurgical, Inc. on this award.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Heat TreatToday offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry. Enjoy these 13 news items, featuring the Nitrex/AICHELIN Group merger, Super Systems 30th Anniversary, Heat TreatToday’s40 Under 40 Honorees, and more!
Equipment
1. Tenova continued its collaboration with Topy Industries Ltd., starting a Phase II integration of the Tenova acoustic water detection system on the EAF shaft panels.
2. Rheintmetall and Lockheed Martin presented a world first in the field of combat vehicles at the DSEI UK trade fair: the Fuchs JAGM is a highly mobile combat vehicle designed to combat a wide range of threats on land and in the air.
3. SMS Group received final approval from WISCO for the successful modernization of its high-capacity hot strip mill. The project focused on automation upgrades, including X-Pact® Profile, Contour and Flatness Control (PCFC), and new CVC® blocks.
4. Kanthal, a global resistance materials producer, expanded its wire production capacity in Hosur, India. The new 1,980 square meter facility will more than triple its production capacity at the Hosur plant.
Tenova acoustic water detection systemRheinmetall and Lockheed Martin reveal vehicleSMS receives final acceptanceKanthal new facility expansion
Company & Personnel
5. NITREXwill soon be part of the AICHELIN Group. AICHELIN signed an agreement to acquire the NTS & UPC business divisions of NITREX.
6. Phoenix Heat Treating announced their acquisition of Mesa Custom Machining. Mesa Custom will continue to operate as an independent company.
7. Solar Atmospheres of California announced the addition of Eric Cavenee to their Western Region Outside Sales team.
Aichelin acquires NitrexPhoenix Heat TreatingSolar Atmospheres welcomes Eric Cavenee
Kudos
8. Super Systems celebrated their 30th anniversary, which included Bill Thompson (Founder), Steve Thompson (CEO), and Will Thompson (Employee), who are father, son, and grandson.
9. Advanced Heat TreatCorp achieved a 24-Month Nadcap® merit status for heat treatment. The renewed status is valid until November 30, 2027.
10. Wirco celebrated 20 years since acquiring the foundry in Champaign, Illinois. They honored long-tenured retirees at the occasion.
11. Heat Treat Today announced its 40 Under 40Class of 2025 Honorees. The 40 Under 40 initiative is an opportunity for the heat treat community to give loud applause to the ladies and gentlemen rising up as leaders in the North American heat treat industry.
12. The MTI Educational Foundation announced that 17 outstanding students have been awarded scholarships totaling $80,000 to support their pursuit of education and careers in materials science, metallurgy, engineering, and related industrial and technical fields.
13. Trinity Forge — one of Mansfield’s oldest active manufacturers — is celebrating 70 years in business! Founded in 1955, Trinity Forge has grown from a small forging shop into a versatile manufacturer serving industries from aerospace and defense to transportation and heavy equipment.