Annealing Furnace Delivered to Manufacturer

A supplier of Thermal Processing equipment since 1938, Park Thermal International recently delivered and commissioned a fifth Electric Atmosphere Annealing Furnace for use in manufacturing, 48” wide x 36” high x 162” long, 20,000 Lbs capacity, 254 KW (2 zones of control), 1,600°F.  This furnace is complete with ceramic fiber insulation, vertical rising door, rod overbend heating system, nitrogen atmosphere, three roller rails with wheels, three re-circulating fans and powered cooling.  The furnace includes a free standing control panel complete with digital instrumentation, chart recorder and SCR control.

Annealing Furnace Delivered to Manufacturer Read More »

Aerospace Manufacturer Replaces Batch IQs with Integrated Vacuum System

A North American based aerospace manufacturer is replacing two integral quench batch furnaces with an integrated vacuum furnace heat treat system. In addition to running low pressure carburizing (LPC), the vacuum heat treat furnace is also capable of austenitizing, brazing, gas quenching, cryogenic treating and tempering. The SyncroTherm(r) system, provided by ALD Vacuum Systems, Inc. a wholly owned subsidiary of Advanced Metallurgical Group N.V., is believed to be the first of its type to be installed west of the Mississippi. This is the third unit being installed in the aerospace industry capable of performing processes compliant with Nadcap (National Aerospace and Defense Contractors Accreditation Program). The vacuum heat treat furnace will have five independently controlled hot zones each rated for load sizes of 24″ x 20″ x 9″ high and up to 110 lbs. The complete systems will be a “lights-out,” fully-automated system with individual part tracking and complete process history retention along with a consistent process cadence.

Aerospace Heat Treating
Photo Credit: www.corelitecomposites.com

Aerospace Manufacturer Replaces Batch IQs with Integrated Vacuum System Read More »

Medical Manufacturer Chooses Vacuum Furnace System

A vacuum heat-treating system with 2-bar gas quenching was shipped to Costa Rica and will be used to manufacture surgical components. The TITAN® H2, manufactured by Ipsen, helps companies accelerate the pace of innovation while satisfying the strict legal requirements of the medical industry.

The standardized vacuum furnace features an 18″ x 24″ x 18″ (455 mm x 610 mm x 455 mm) all-metal hot zone with a 1,000-pound (450 kg) load capacity. It is capable of operating at temperatures of 1,000 °F to 2,400 °F (538 °C to 1,316 °C) with ±10 °F (±6 °C) temperature uniformity. Equipped with the PdMetrics® platform for predictive maintenance – which securely connects to a network of integrated sensors on the furnace to gather and analyze data, run algorithms and provide real-time diagnostics – the furnace provides sophisticated monitoring of critical systems and key parameters that improve the health and integrity of the equipment. The company also received a gas backfill reservoir, a loader with a 2,000-pound (907 kg) load capacity and a complete air-cooled, closed-loop water system.


Medical Manufacturer Chooses Vacuum Furnace System Read More »

Dana Breaks Ground on New Gear Manufacturing Facility in Europe

Dana Incorporated broke ground on a state-of-the-art gear manufacturing facility in Europe to support new business in the region.  The 140,000 square-foot (13,000 square-meter) facility in Győr, Hungary will provide customers in the region with access to Dana’s advanced design, engineering, and manufacturing expertise to support their sourcing initiatives and technology strategies.

The company is investing approximately €46 million in the new facility, which will begin production in early 2018 employing approximately 200 highly qualified associates when full production is reached in 2020.

The facility will produce Spicer® AdvanTEK® hypoid or spiral bevel ring and pinion gear sets.  Dana manufactures gears for traditional banjo and beam axles, as well as all-wheel-drive systems.  Full axle assembly on the site is possible in the future.

The company’s AdvanTEK line of gears offers best-in-class noise, vibration, and harshness (NVH) performance, as well as greater power density in a compact package.  When integrated into an axle, these gear sets are responsible for transmitting driving torque to the wheels – delivering improved fuel efficiency, enhanced vehicle performance, and maximum durability for the complete spectrum of light and commercial vehicles.

The new plant will serve as the company’s fourth operation in Hungary.  The decision to develop another plant within the country was made possible by the Hungarian Investment Promotion Agency (HIPA), which awarded Dana development grants and tax incentives.

“We are excited to be building this new gear-manufacturing facility to support new business growth in Europe,” said Bob Pyle, president of Dana Light Vehicle Driveline Technologies.  “This plant is strategically positioned in close proximity to our existing Győr operations and will enable us to deliver technologies to our European customers more quickly and cost effectively.

“We are grateful for the strong support that HIPA and the Hungarian government have provided as we expand our gear-manufacturing capacity in the region.  Dana has operated in Győr for more than 10 years, and we know from experience that we can find exceptional employees there,” Pyle added.


Dana Breaks Ground on New Gear Manufacturing Facility in Europe Read More »

New Monolithic Refractories Manufacturing Facility to be Built in Ohio

The Point Industrial Park in South Point, Lawrence County, Ohio will be the location for the construction of a new, state-of-the-art monolithic refractories manufacturing facility by Harbison Walker International. The site is subject to completion of the company’s due diligence and finalization of one additional grant application that is in process.

Citing monolithics as a growth area, HWI announced in February 2017 that it is investing $30 million to build a technologically advanced monolithics plant as the next step in its strategy to continuously improve performance and respond to customers’ needs. The new facility will be one of the most technologically advanced refractories plants built in the U.S. and will be operational by early 2018.

The Point: Unique Location and Amenities

“Unlike any other location, The Point offers unique transportation, logistics and business amenities that combine to create an ideal and cost-effective match for the requirements of our new facility. The intermodal transportation features at The Point will ensure efficient delivery of raw materials from nearby suppliers and finished products to customers. The site offers efficiencies that are simply not possible elsewhere,” said Douglas Hall, senior vice president, Integrated Supply Chain, HarbisonWalker International.

Further, the close proximity to suppliers, a supporting infrastructure, incentives, and the potential for long-term partnerships in the area led to the location selection, according to Hall.

“HarbisonWalker International’s progressive attitudes, commitment to its workforce and customers, and emphasis on quality and technology are a perfect fit with our overall approach. We’re so pleased to welcome such an exciting and dynamic company to The Point,” said Bill Dingus, executive director of the Greater Lawrence County Area Chamber of Commerce and the Lawrence Economic Development Corporation (LEDC), developers of The Point.

Encompassing 500 acres and located in Ohio River Valley in the northern Kentucky / southern Ohio region of the United States, The Point is one of Ohio’s fastest-growing industrial parks. The site is strategically positioned to provide HarbisonWalker International with the capability to move its monolithics from the southern-most point in Ohio to any location around the globe.

Set on the section of the Ohio River that is the largest weight/volume inland port in the United States, The Point invested $4.5 million to build a port that offers a direct link to destinations around the world at the lowest possible price.

Businesses residing at the Point also benefit from the only public rail and truck scales in the area, a utility and road infrastructure built for heavy manufacturing, a four-lane rollout to Interstate 64 and competitive incentive programs. In addition, plans are well underway for a $20 million wellness center to serve employees at The Point and an R&D facility that presents opportunities for future partnerships.

“We are delighted that HarbisonWalker International chose South Point for its new state-of-the-art monolithic refractories manufacturing facility. The site’s excellent road, river and rail transportation assets were a major factor in the decision to make the investment here”, commented John Molinaro, president and CEO of the Appalachian Partnership for Economic Growth (APEG), the region’s JobsOhio partner.

The New Plant: HWI’s Advanced Monolithic Refractories

With a history that spans more than 150 years, HarbisonWalker International (HWI) has created many of the refractory industry’s most significant technologies.

Monolithic refractories (those which can be molded or shaped for a variety of requirements) pose one of the strongest product growth categories for both HWI and the industry. For HWI, the new state-of-the-art plant will enable the company to further elevate product quality and consistency, and it illustrates the company’s forward-thinking strategy to harness new technology and invest for future growth.

HWI expects initial capacity at the new monolithic plant to be approximately 80,000 metric tons per year. The plant will feature new state-of-the-art automation and technology, and will utilize new lean techniques throughout its operations to maximize material flow efficiency and production. It will employ highly-trained and highly-skilled technicians and staff in a team-based environment. In addition, the facility will introduce advanced packaging technologies that are new to the North American market.

Groundbreaking for the new facility is expected to occur in early summer, 2017. Additional details about the new facility and construction plans will be announced as they become available.


New Monolithic Refractories Manufacturing Facility to be Built in Ohio Read More »

Manufacturing Space Purchased from Plymouth Tube

A  facility offering over 130,000 square feet of manufacturing space has been purchased from Plymouth Tube.  Wisconsin Oven recently closed on this property located on Young Street in East Troy Wisconsin, between two other Wisconsin Oven factories. Wisconsin Oven’s total investment in the community will exceed $2.5M after purchase and renovation. Wisconsin Oven President and CEO, Dave Strand, commented “ We are very excited to secure this facility. Over the next year we will be doing some extensive renovation, and plan on hiring 80-90 employees between 2017-2019.” Wisconsin Oven Corporation was founded in 1973, and has grown to be a world leading manufacturer of industrial  ovens and heat treating equipment.

Manufacturing Space Purchased from Plymouth Tube Read More »

Premier Global Tier One Auto Supplier Formed by Union

Metaldyne Performance Group Inc. has been acquired by American Axle & Manufacturing Holdings, Inc. . The transaction was unanimously approved by the boards of directors of both companies and recently approved by stockholders of AAM and MPG.

“Today is an historic day where we combine the strengths of both AAM and MPG into a premier, global Tier 1 automotive supplier with broader capabilities across multiple product lines,” said David C. Dauch, AAM Chairman and Chief Executive Officer. “This transformational acquisition will allow us to maximize stakeholder value by creating a company with greater size, scale and increased business diversification that delivers efficient, powerful and innovative solutions for our customers.”


Premier Global Tier One Auto Supplier Formed by Union Read More »

ASM International Developing Stronger Relationships

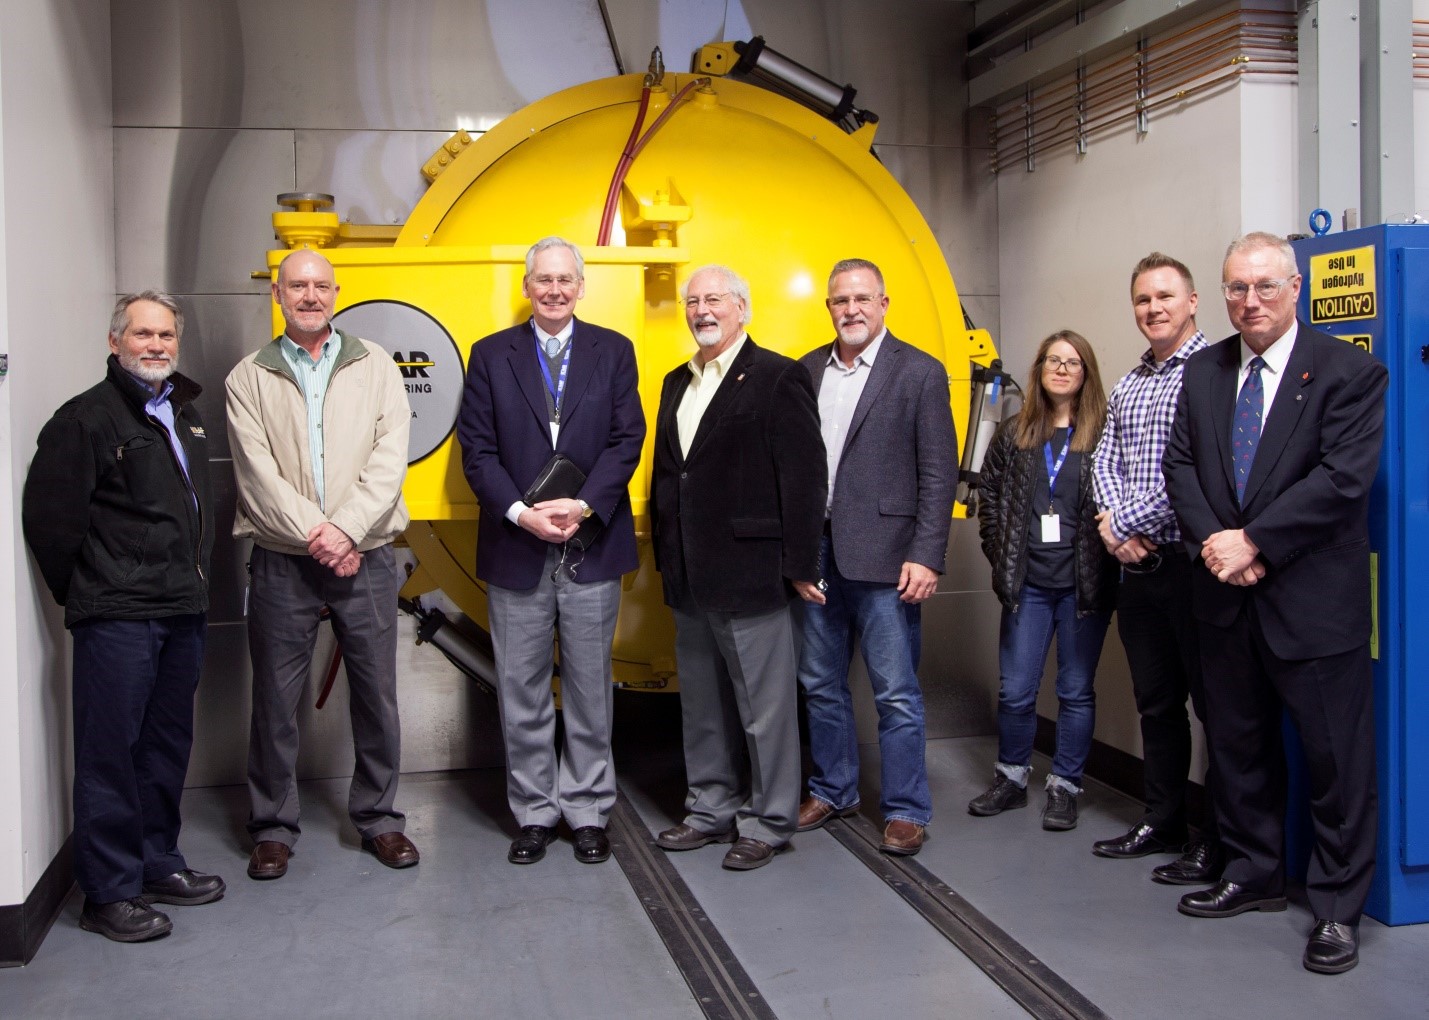
ASM Leadership Visits Solar Atmospheres & Solar Manufacturing
Pictured left to right: Jim Nagy, President, Solar Manufacturing; Don Jordan, FASM, Vice President/Corporate Metallurgist, Solar Atmospheres; Bill Mahoney, Managing Director, ASM International; Fred Schmidt, Vice President, ASM; Ron Aderhold, Associate Managing Director and Chief Information Officer, ASM; Rachel Stewart, Student Board Trustee, ASM; Jamie Jones, VP of Operations, Solar Atmospheres; Roger Jones, Corporate President, Solar Atmospheres. Photo Courtesy: Solar Atmospheres

Souderton, PA – ASM International visited Solar Atmospheres on Wednesday, March 22 to renew stronger relationships with supporting companies, and to gain a better understanding of Solar’s commitment and involvement with ASM.  Managing Director, Bill Mahoney, along with Ron Aderhold, ASM Associate Managing Director and Chief Information Officer, Fred Schmidt, ASM Vice President, and Rachel Stewart, Student Board Trustee, met with representatives from Solar and toured the facility.

ASM presented firsthand information on the objectives and progress of the ASM renewal, spearheaded by Mahoney.  Some of the objectives are pursuing an easier renewal process, developing stronger relations with affiliate societies, improving professional development, and developing a culture of excellence within the headquarters at Materials Park, OH.

Solar Atmospheres came away from this meeting with a high level of confidence with the new team at ASM Materials Park, and we are encouraged with the early results from the renewal deployments, and Solar offers complete support of the program for the betterment of the society.

ASM International Developing Stronger Relationships Read More »