




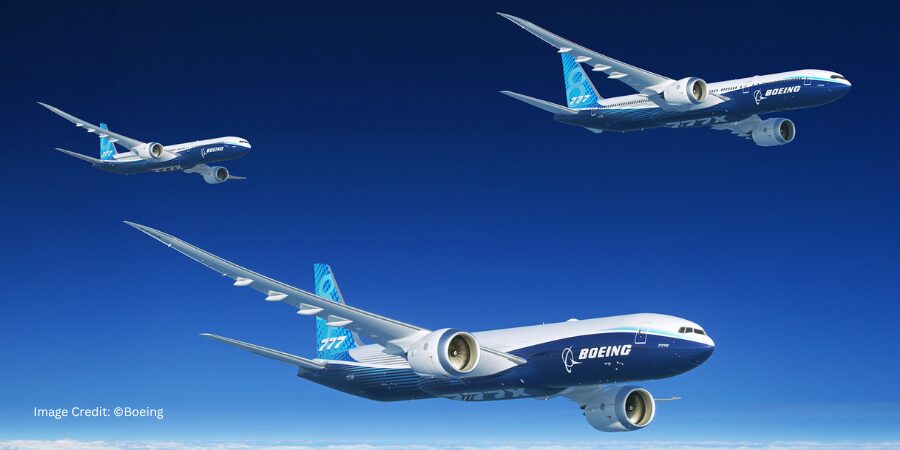
Boeing Adds Vacuum Heat Treat Capacity
Boeing is adding vacuum furnace capacity at its Tube, Duct and Reservoir Center in Algona, Washington, to expand in-house heat treating capability for aerospace tube and duct assemblies. The investment is intended to address production needs across commercial and defense aerospace programs.
President
Boeing Canada
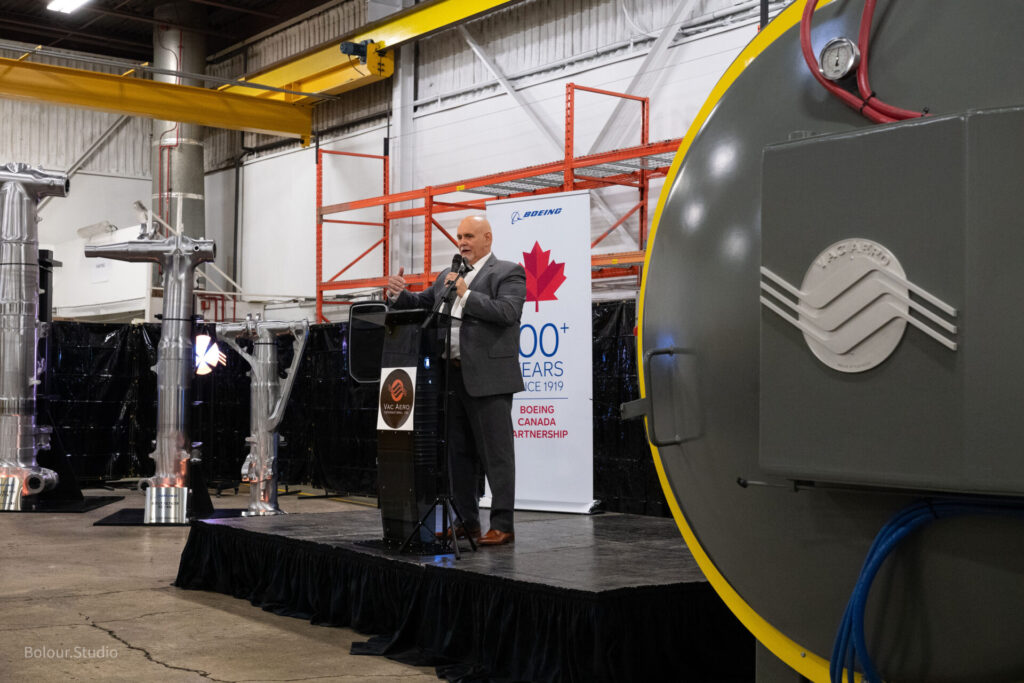
The investment is part of Boeing’s Industrial and Technological Benefits (ITB) commitments tied to Canada’s CP8A Poseidon aircraft program, which includes a multi-million dollar investment in Vac Aero International to strengthen aerospace manufacturing capabilities in Canada.
“We are pleased to support Vac Aero with the purchase of this new equipment for our Fabrication facility, which serves our commercial programs and select space and defense work,” said Al Meinzinger, president of Boeing Canada. “This ITB investment underscores Boeing’s commitment to Canada following the CP8A Poseidon selection and to modern manufacturing and Canadian small businesses in our global supply chain.”
The expansion includes the installation of two vacuum furnaces for vacuum heat treating and annealing of complex tube and duct assemblies at Boeing’s Algona facility. The furnaces, sized at 60″ x 90″ and 60″ x 60″, will be dedicated assets supporting Boeing’s aerospace manufacturing operations for multiple airplane programs.
The furnaces will be co-located within a single heat treat area, a configuration expected to free up approximately 300 square feet of production space. The equipment is scheduled to be ready for use in April 2027.
Press release is available in its original form here. Additional details provided by Boeing.
Boeing Adds Vacuum Heat Treat Capacity Read More »
Helium Leak Detection Seminar Kicks Off in Charlotte
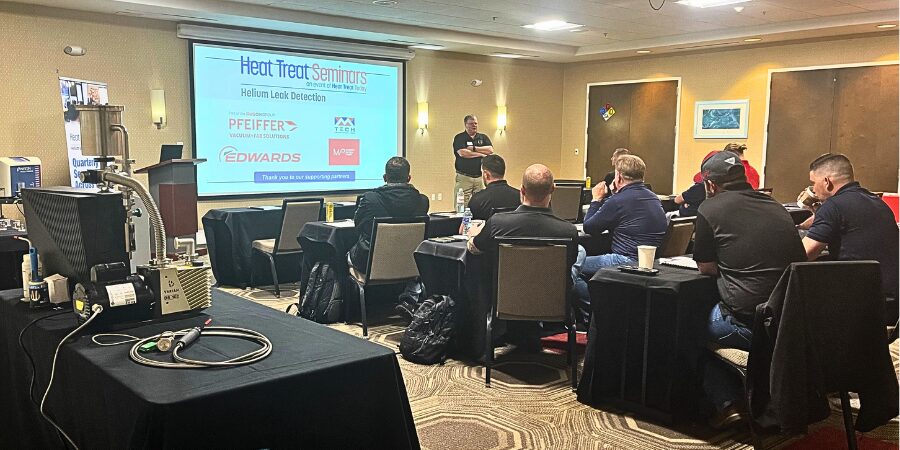
Heat Treat Today has launched its 2026 Helium Leak Detection Seminar series, with the first stop held on March 25, 2026 in Charlotte, North Carolina. The one-day, hands-on training event brought together vacuum furnace users, OEMs, and industry suppliers for practical instruction on leak detection methods and equipment used in thermal processing environments.
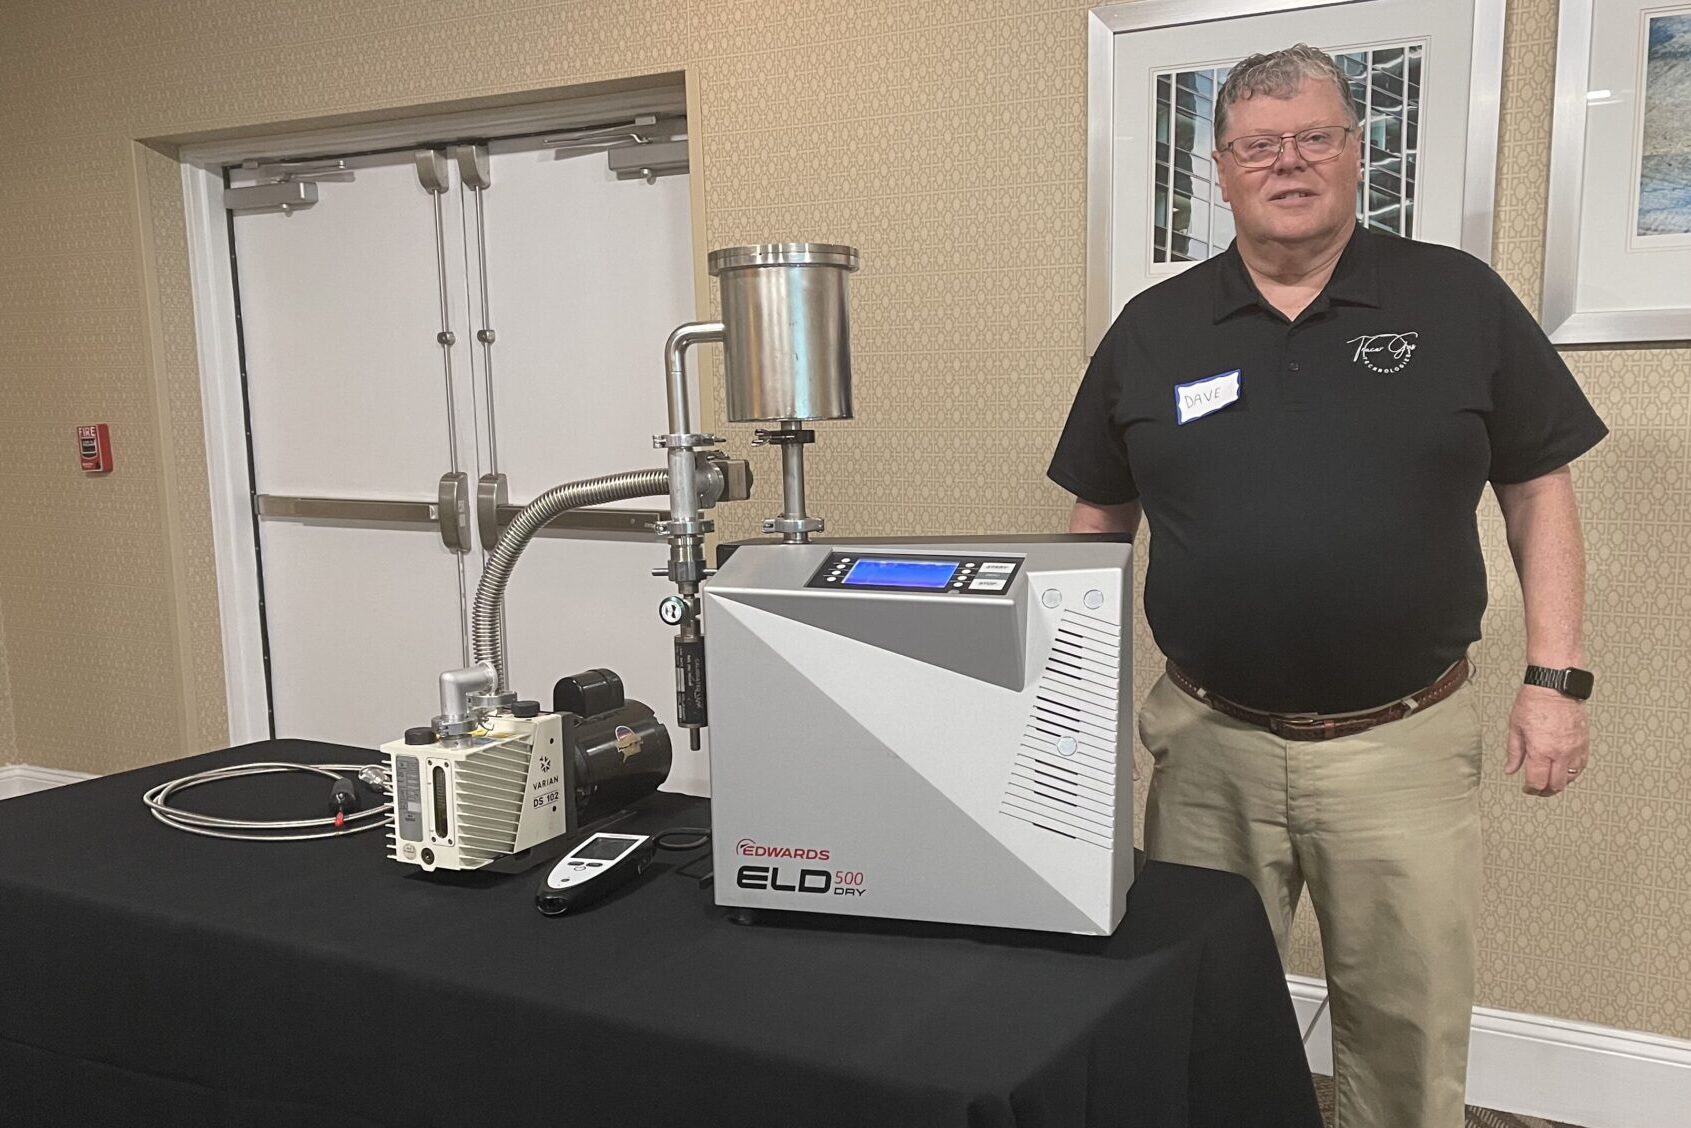
Led by Dave Deiwert of Tracer Gas Technologies, the seminar focused on helping attendees better understand the challenges associated with helium leak detection and how to troubleshoot common issues encountered in vacuum furnace operations. Participants included both end users and manufacturers of vacuum furnaces, reflecting broad industry interest in improving leak detection practices.
The program combined classroom instruction with live demonstrations and hands-on experience using multiple helium detection systems. Onsite sponsors included Aaron Barton of Busch Vacuum Group, who demonstrated the Pfeiffer Vacuum ASM310 helium leak detector and guided attendees through hands-on use. Additional demonstrations were supported by Bob Delabio and Bryant Crisp of Edwards Vacuum, who provided access to the Edwards ELD500 Dry Helium Leak Detector for live testing and application-based learning. Deiwert also incorporated an Inficon Protec 3000 helium sniffing leak detector into the training, offering attendees exposure to multiple leak detection approaches used in vacuum furnace environments.
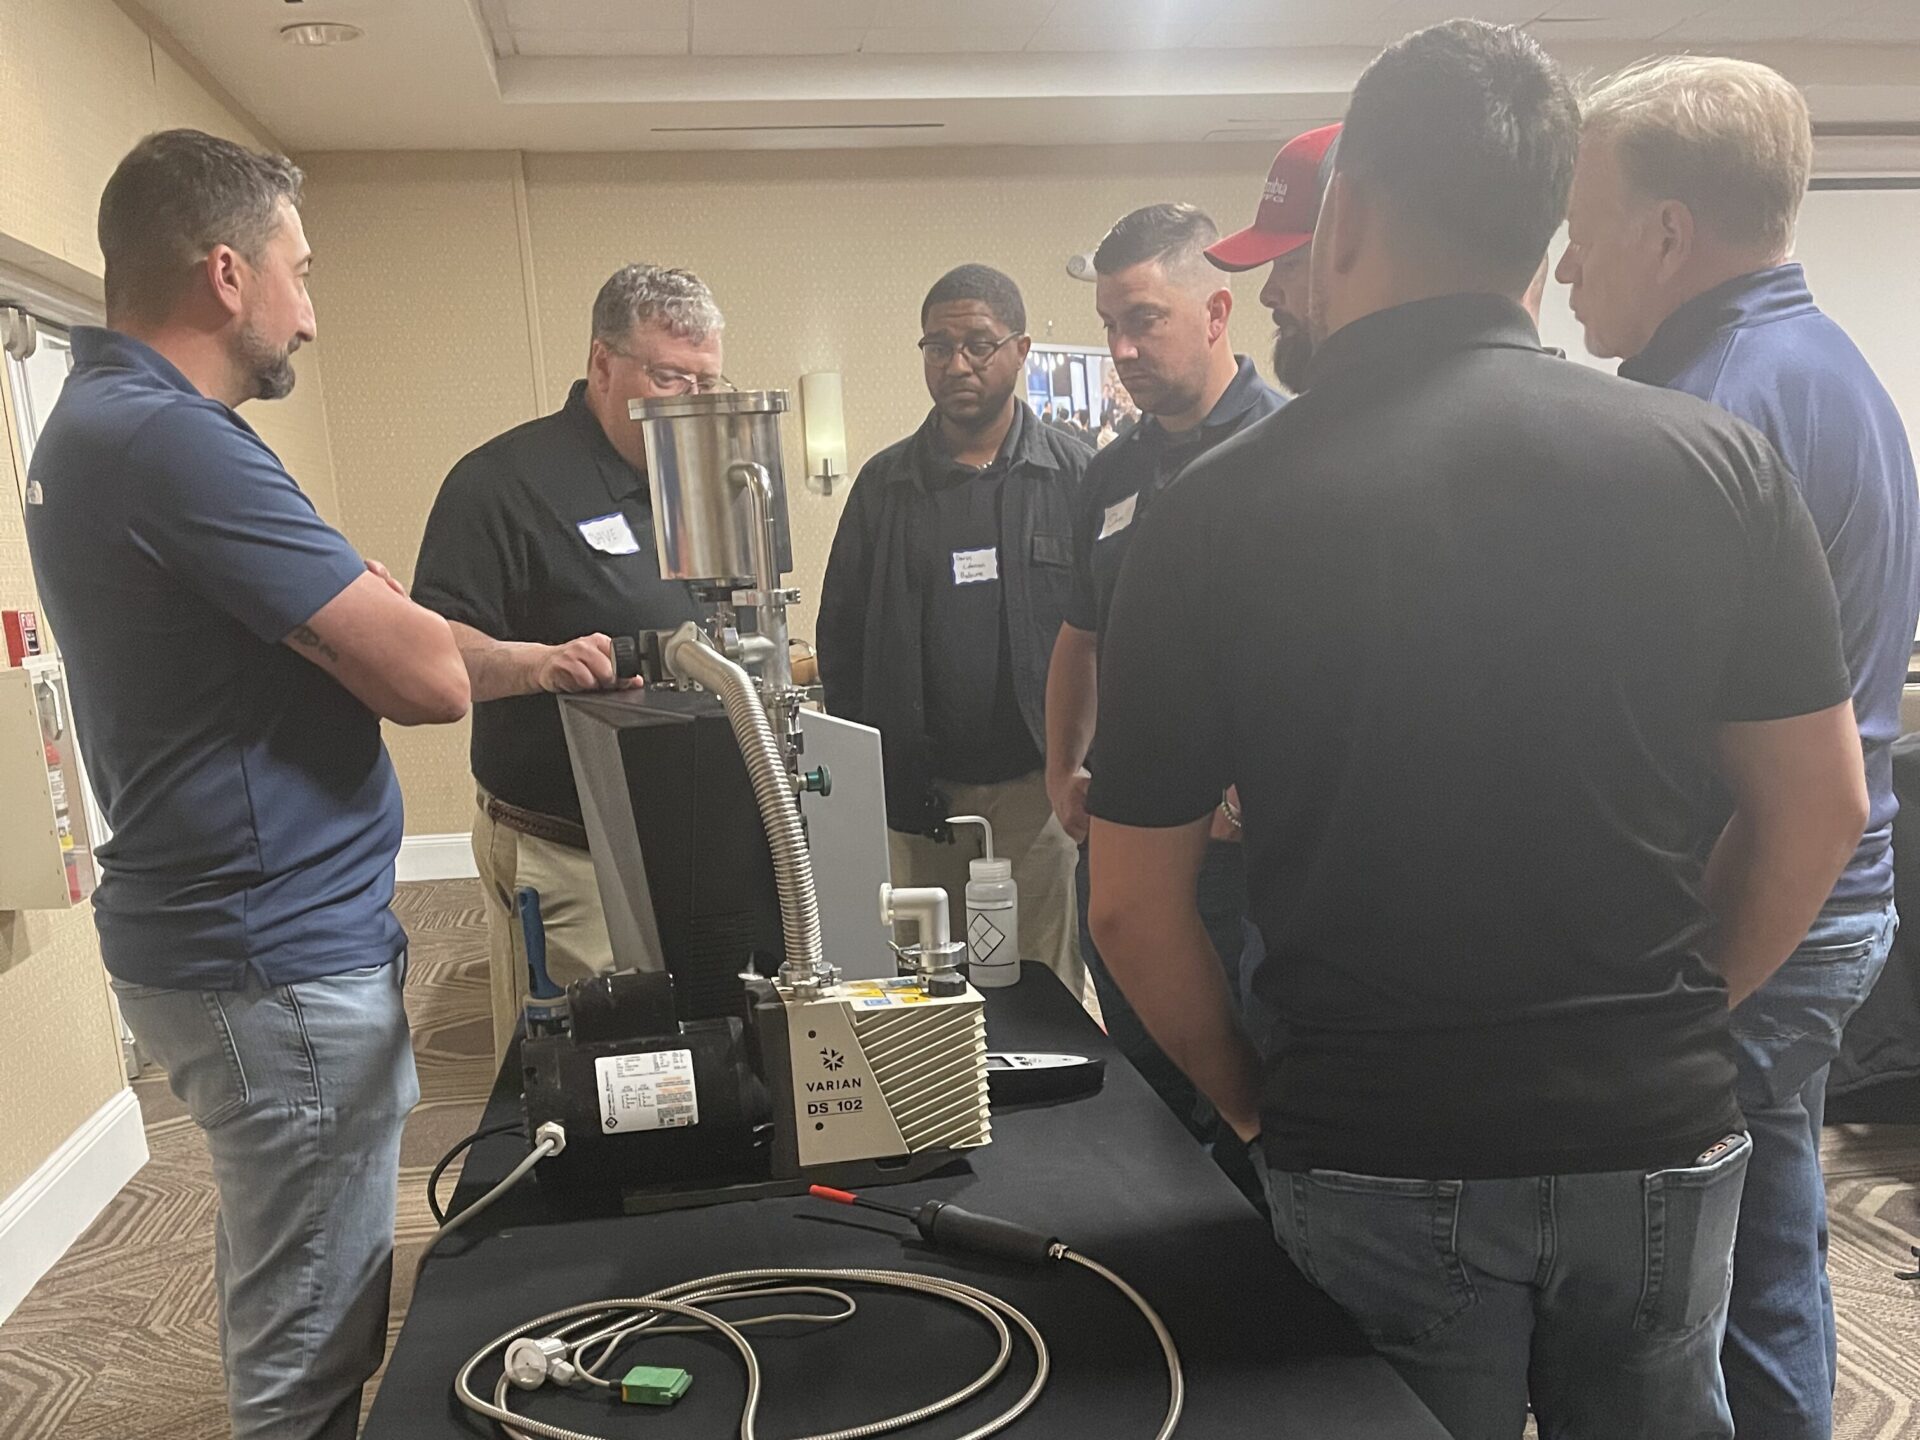
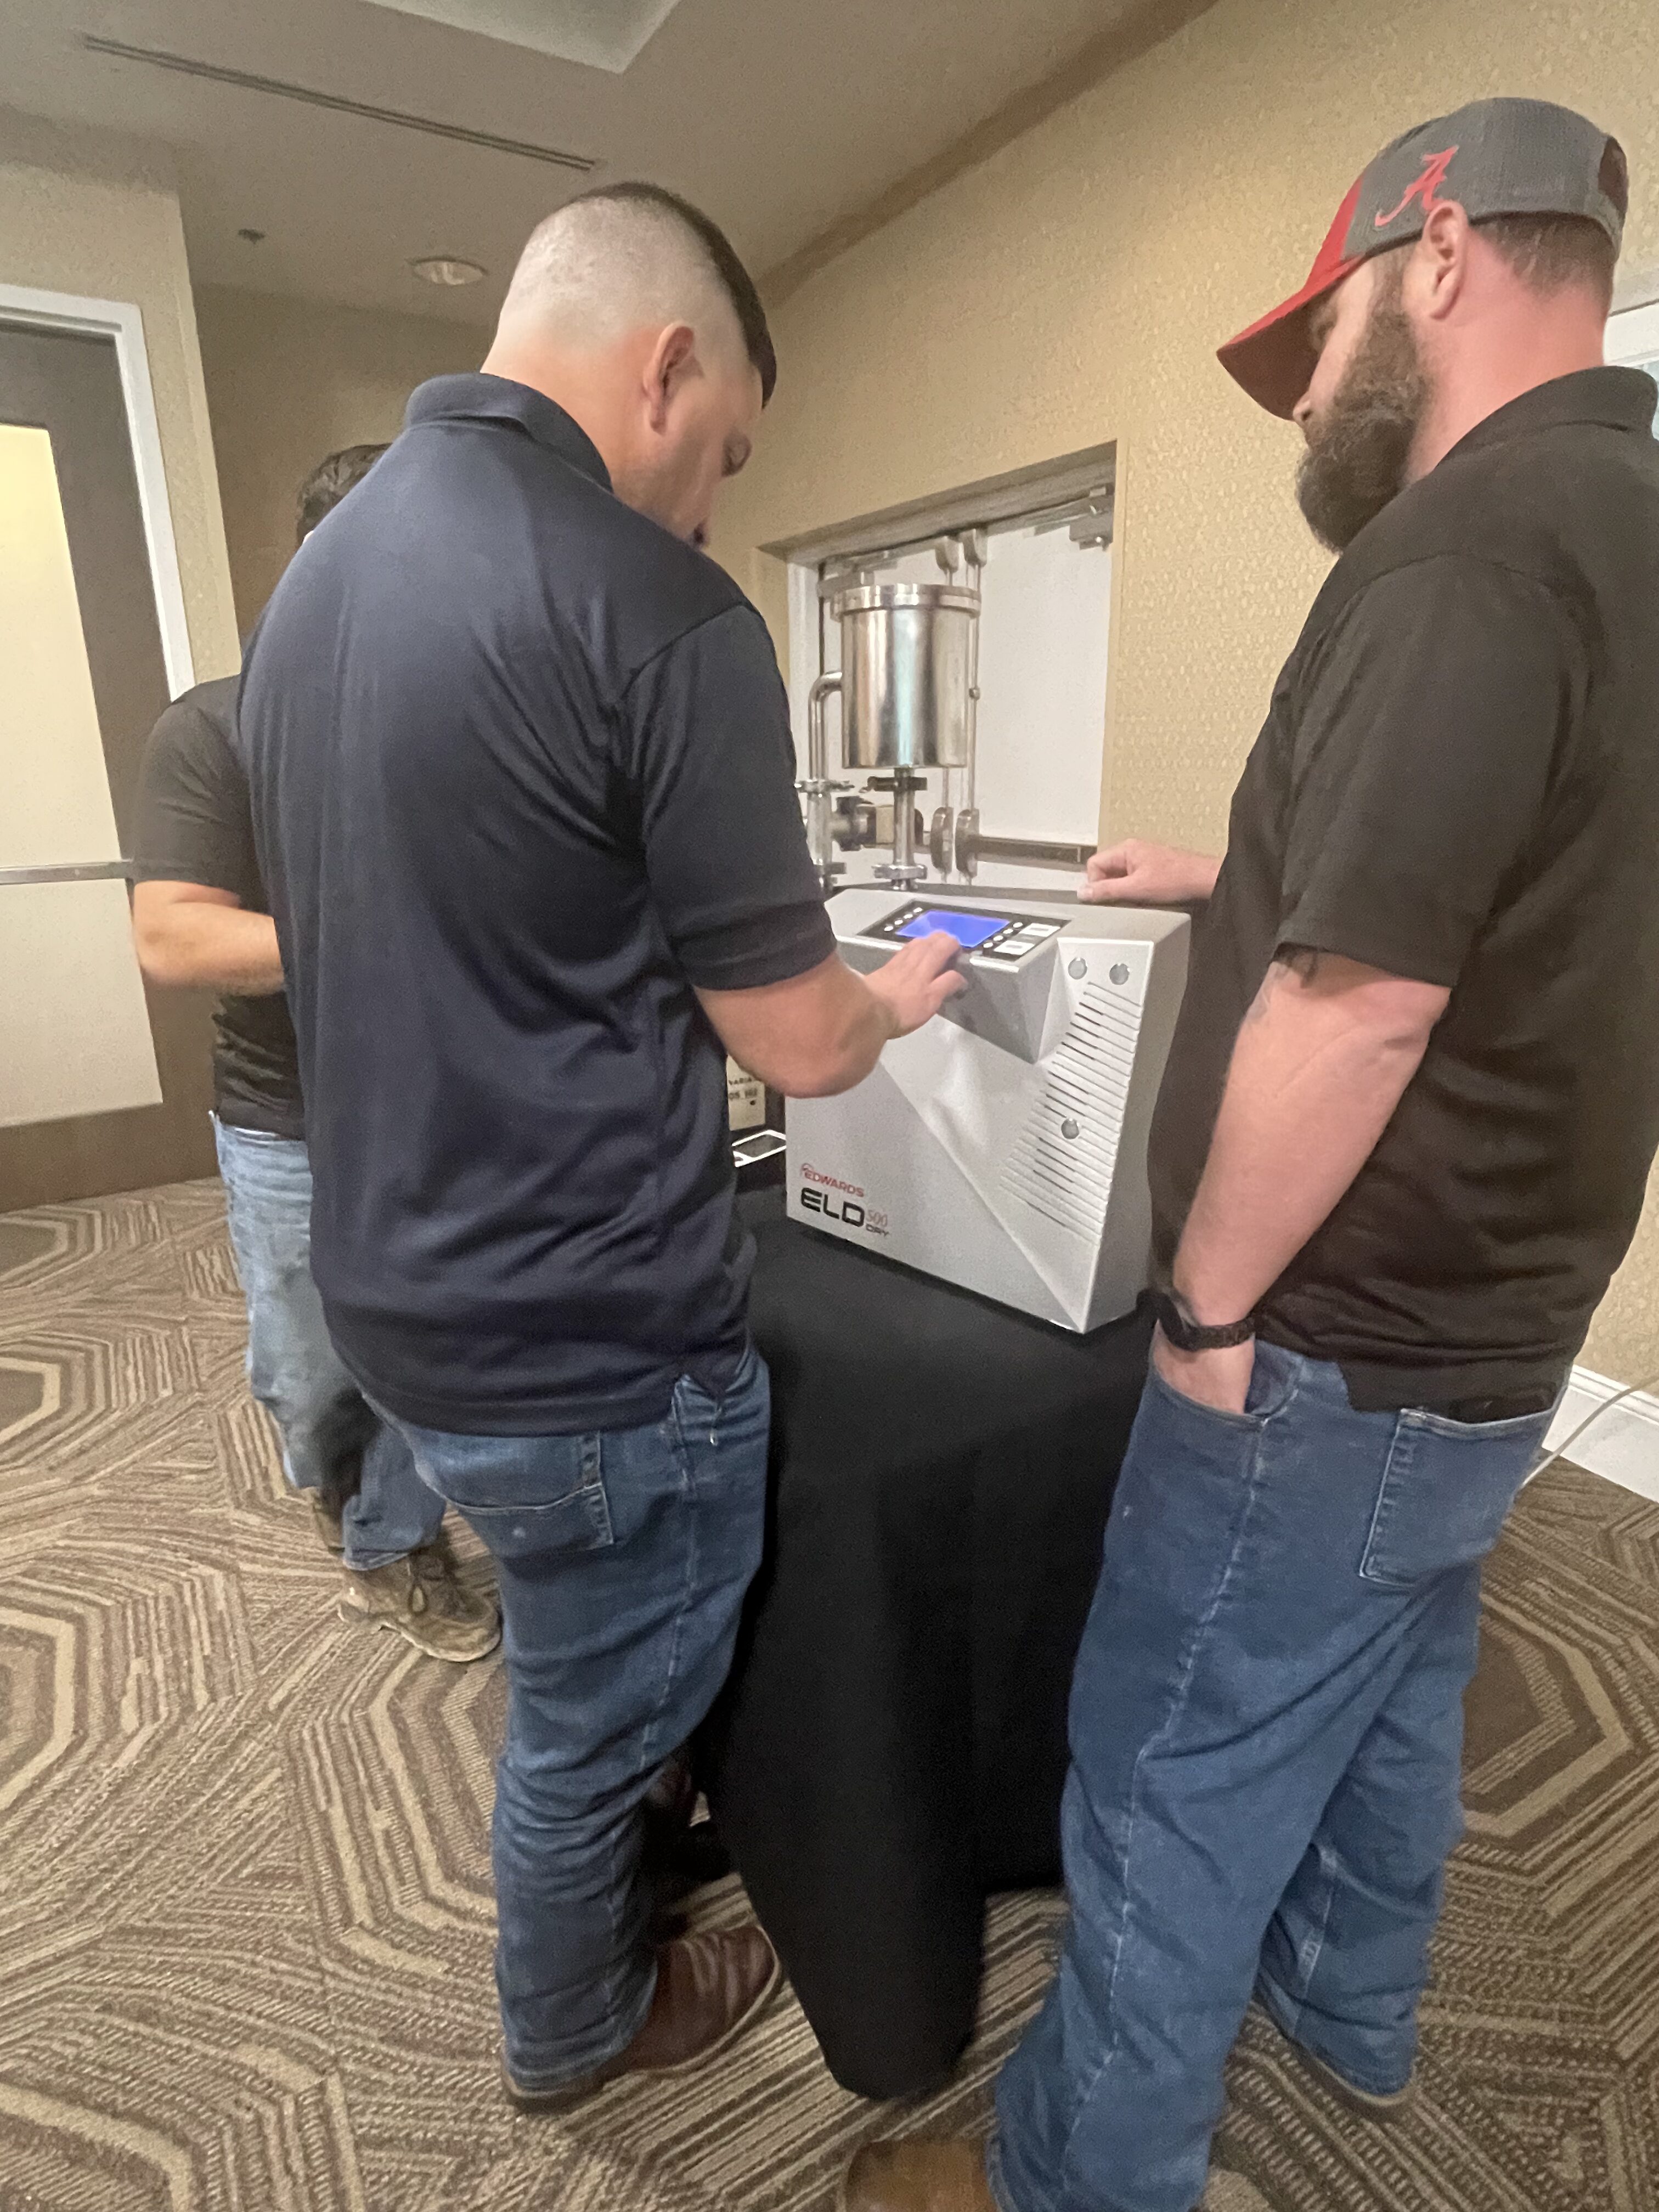
Attendees were encouraged to engage throughout the session, with open discussion around common frustrations in leak detection and strategies for improving accuracy and efficiency. According to Deiwert, many participants identified leak detection as a persistent challenge in their operations, underscoring the value of practical, experience-based training.
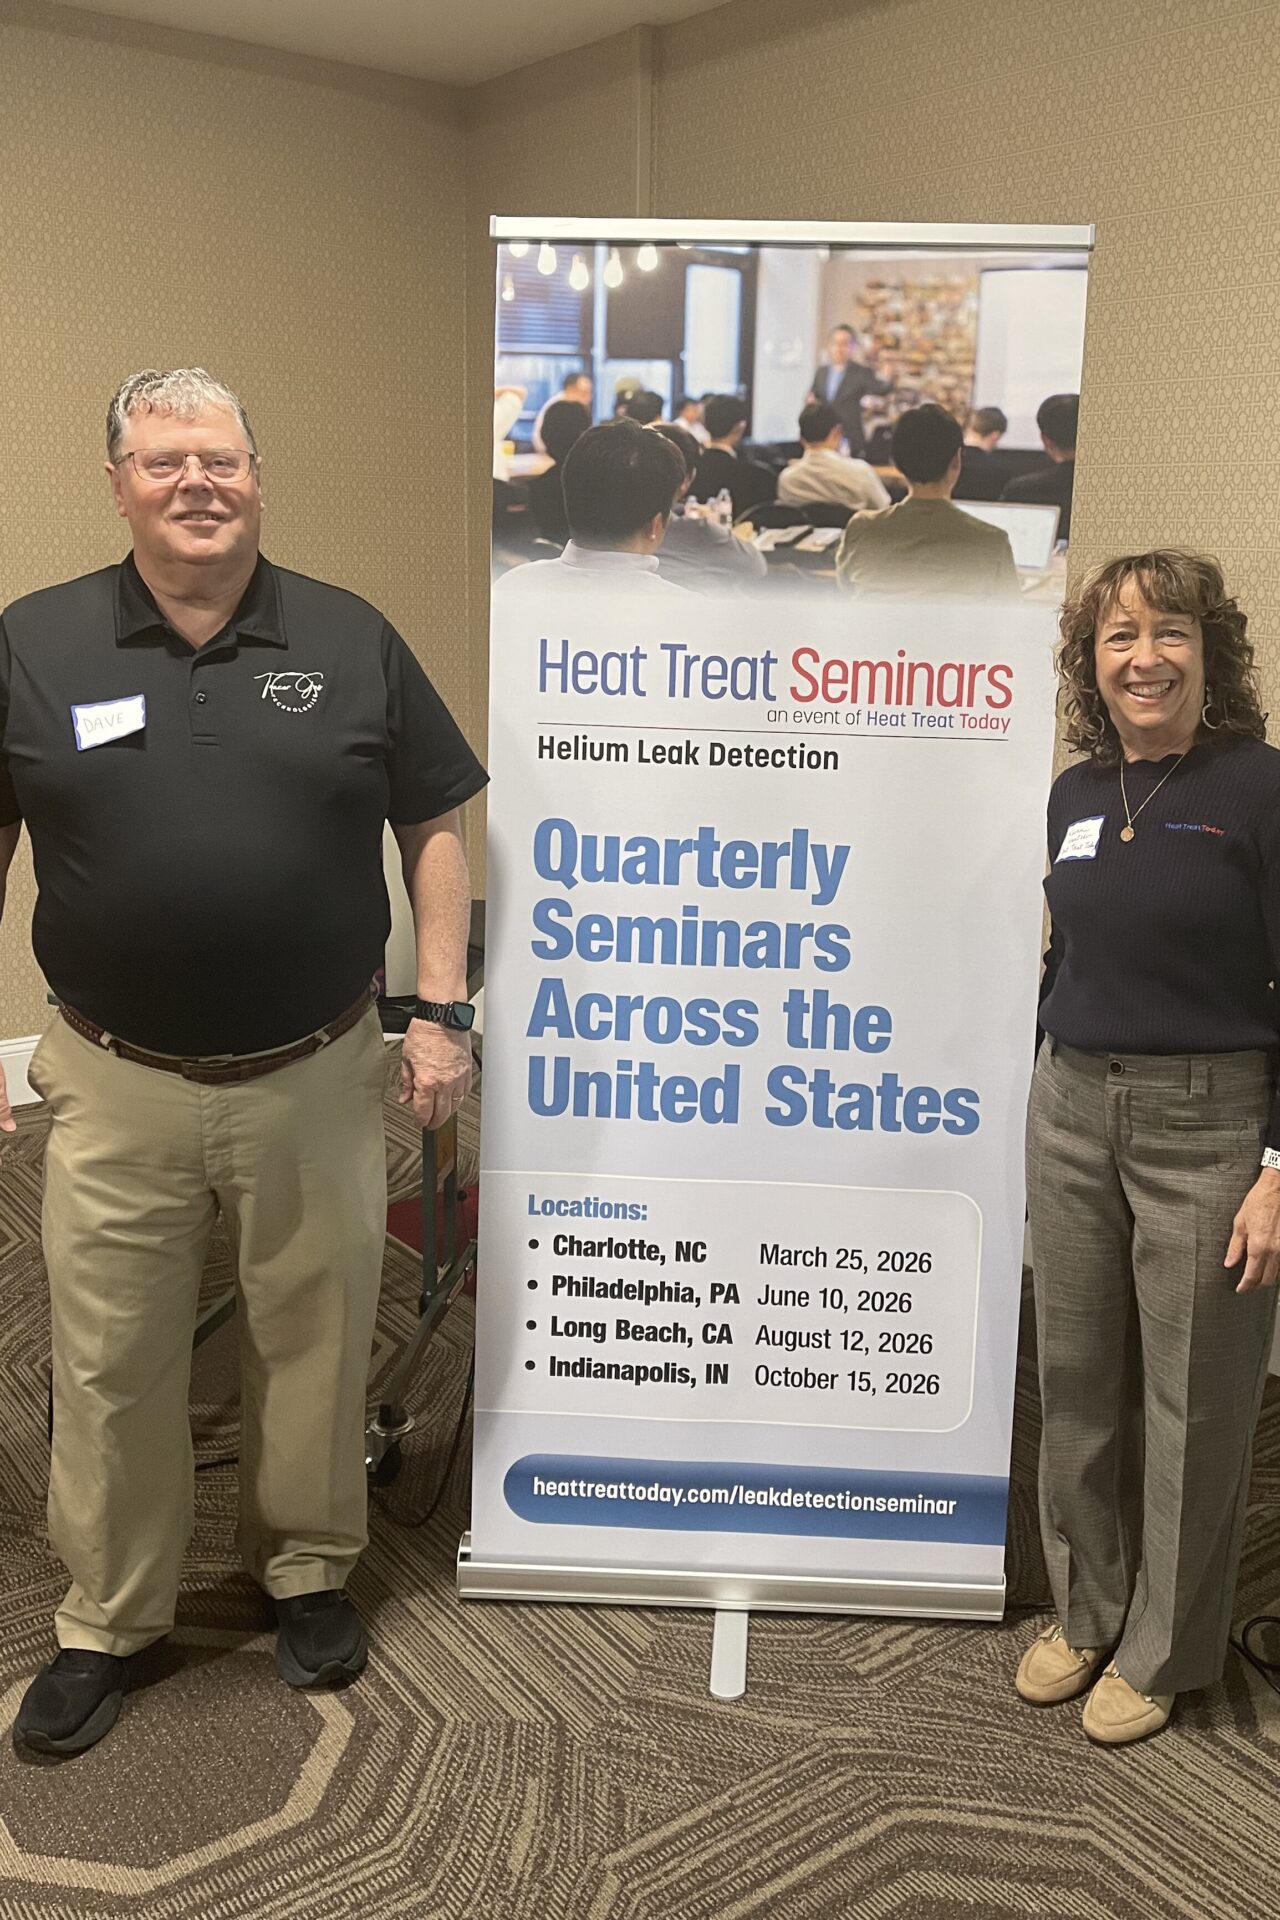
The event was organized by Heat Treat Today, with coordination led by Publisher Doug Glenn and Director of Events Karen Gantzer, who also managed onsite execution in Charlotte.
Deiwert emphasized a service-oriented approach to the training, encouraging attendees to continue the conversation beyond the seminar. “If you help people when they have problems, business seems to take care of itself,” he said, noting that responsiveness and technical support play a key role in building long-term relationships across the industry.
The Charlotte seminar marks the first of four planned stops in Heat Treat Today’s 2026 Helium Leak Detection Seminar series, which aims to provide accessible, application-focused training for professionals working with vacuum furnaces and related equipment.
Want to learn more about helium leak detection? With upcoming stops in Philadelphia, Long Beach, and Indianapolis, you can click here to find a session near you!
Helium Leak Detection Seminar Kicks Off in Charlotte Read More »
Vacuum Furnace Consolidates Multiple Heat Treat Processes
A manufacturer has placed an order for a vacuum furnace system designed to replace multiple heat treating processes, consolidating operations into a single device to streamline thermal processing. The furnace will be used to heat treat components for high-precision small arms intended for civilian markets, including sport shooting and hunting, as well as versions adapted for uniformed services.
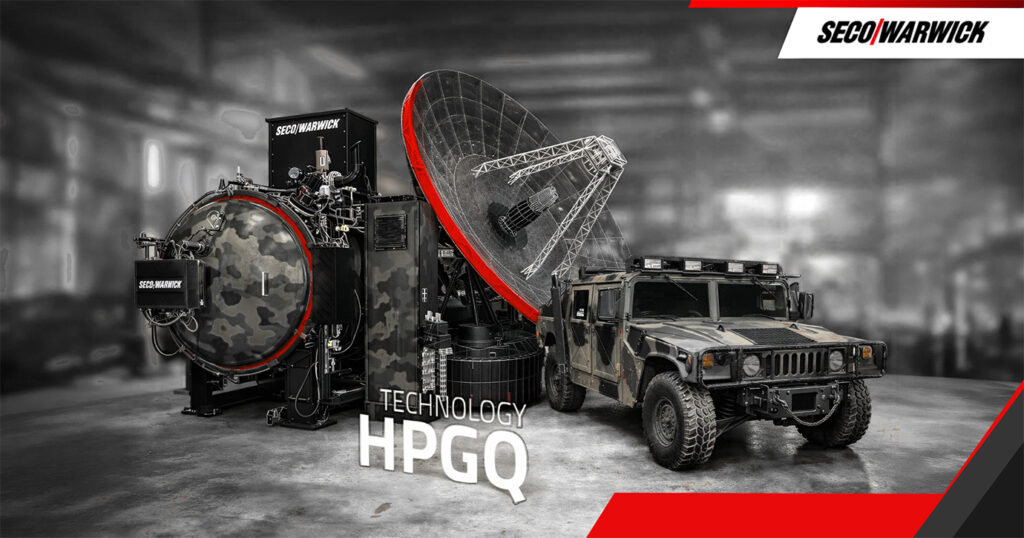
Initial production plans called for four separate units — an oil quenching furnace, tempering furnace, cryogenic unit, and washing system. Following a joint technological analysis, SECO/WARWICK, a global manufacturer of industrial furnaces with operations in North America, demonstrated that these processes could be performed within a single vacuum furnace with gas quenching. Trials confirmed the approach met the client’s requirements while simplifying the overall process.
The system is a horizontal Vector vacuum furnace designed to support multiple heat treating operations in one unit. It features a round heating chamber with temperature uniformity of approximately 5°C (9°F), a convection heating system for improved low-temperature efficiency, and a vacuum pumping system combining mechanical and Roots pump for stable operation.
Additional capabilities include partial pressure control system to limit alloy element evaporation and a 15-bar gas quenching system with inverter controlled to stabilize cooling and reduce power demand peaks. The furnace also supports vacuum carburizing (FineCarb), pre-nitriding (PreNitLPC), low-pressure carbonitriding (LPCN), and deep cryogenic treatment down to −80°C (−112°F) within an automated cycle.
By consolidating these processes, the system is expected to improve repeatability and production efficiency, while eliminating the need for post-quench oil cleaning.
Vice President of Vacuum Business Segment
SECO/WARWICK
“Initially, several separate devices were considered, each handling subsequent stages of the process. After analysis and technological testing, it turned out that all these operations can be carried out in a single vacuum furnace with gas quenching. This means not only substantial investment savings but also simplified production, shorter process times, and reduced labor requirements. For the [client], it is also the first step toward modern vacuum processes and moving away from the atmospheric technologies previously used,” said Maciej Korecki, vice president of the Vacuum Segment at SECO/WARWICK.
Press release is available in its original form here.
Vacuum Furnace Consolidates Multiple Heat Treat Processes Read More »
Ask The Heat Treat Doctor®: Why and How Do We Heat Treat Gears? Part Two
Ask The Heat Treat Doctor® has returned to bring sage advice to Heat Treat Today readers and to answer your questions about heat treating, brazing, sintering, and other types of thermal treatments as well as questions on metallurgy, equipment, and process-related issues. In this installment, Dan Herring continues his discussion on gear heat treatment, exploring vacuum and induction hardening methods for gears — from low-pressure carburizing for advanced materials to single shot and tooth-by-tooth induction techniques — and how each can be matched to the specific demands of any gear application.
This informative piece was first released in Heat Treat Today’s March 2026 Annual Aerospace Heat Treating print edition.
In Part One of this discussion (Air & Atmospheres Heat Treating, February 2026), we discussed various gear types, materials, and how they can be atmosphere heat treated. This month, we are focusing on vacuum and induction heat treating methods. Let’s learn more.
Vacuum Heat Treatment Processing Methods
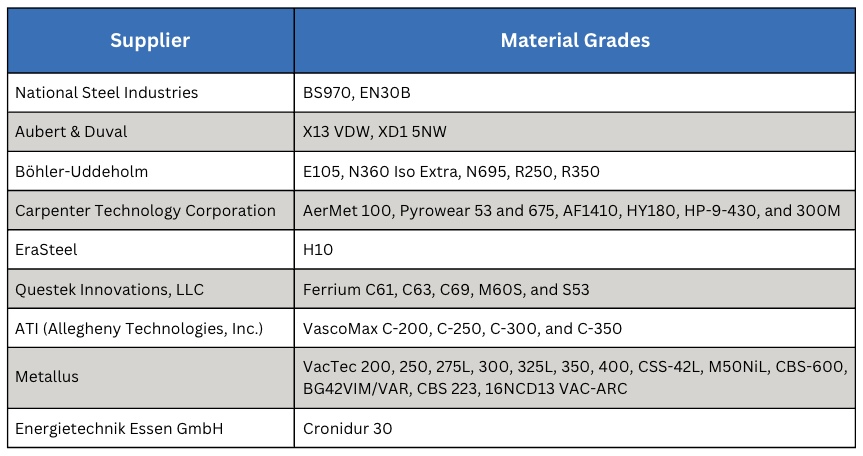
Vacuum processing can be used for most of the atmosphere treatments mentioned in Part One including carburizing (Figure 1). Low pressure carburizing (LPC) is a proven technology and the choice for many advanced applications in aerospace, automotive, off-highway, and motorsports markets, as well as the development of carburizing cycles for high-performance materials (Table A).
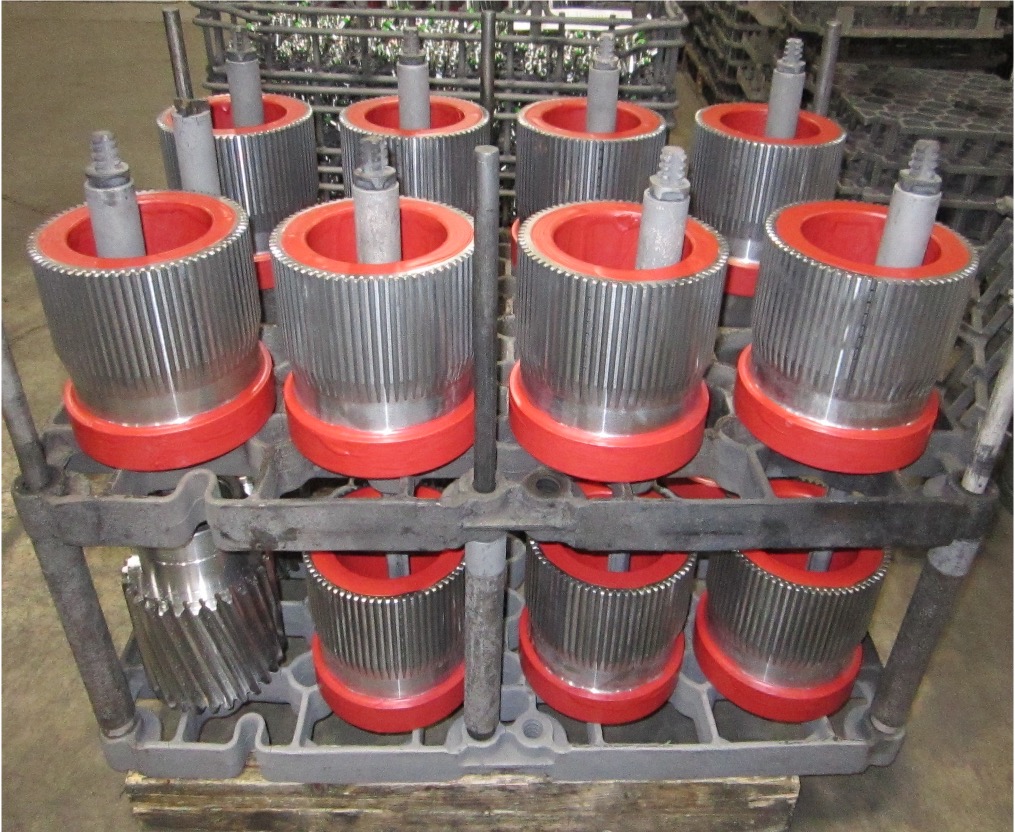
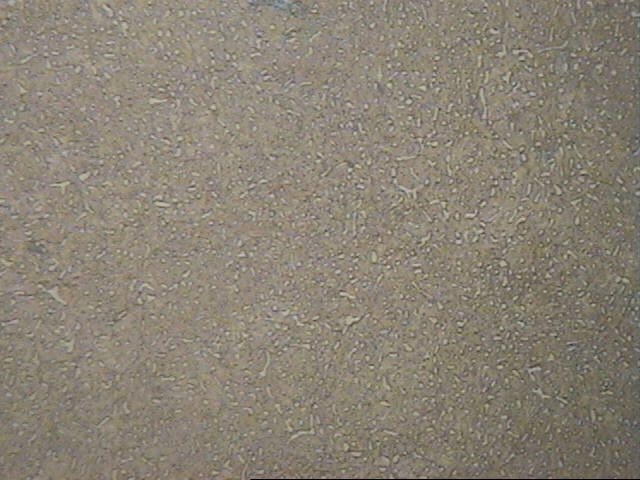
The range of effective case depths for most of these grades can range up to 2.0–3.0 mm (0.080–0.120 inches) without significant sacrifice of microstructure (Figure 2). Furnace variables, such as temperature uniformity (± 3°C or ± 5°F), control of cycle parameters (boost/diffuse times, gas flow rate, pressure, hydrocarbon type) and surface carbon optimize the microstructure, producing case uniformities of ± 0.05 mm (± 0.002 inches). Where permitted, the range of carburizing temperatures now includes the use of high temperature (> 980°C, or 1800°F) techniques.
All these advanced materials required extensive development testing to produce custom designed recipes to optimize cycle parameters. Also, quenching methods (Otto and Herring 2002) have improved, allowing us to achieve desired core properties with quenching parameter selection (high-pressure gas or oil) for distortion-sensitive and distortion-prone part geometries (Otto and Herring 2005, 2008).
Induction Hardening Methods
Various methods of hardening via applied energy are used in manufacturing gears, including flame hardening, laser surface hardening, and induction hardening.
Of the various types of applied energy processing, induction hardening is the most common. Induction heating is a process that uses alternating electrical current that induces a magnetic field, causing the surface of the gear teeth to heat. The area is then quenched resulting in an increase in hardness within the heated area. This process is typically accomplished in a relatively short time. The final desired gear performance characteristics are determined not only by the hardness profile and stresses but also by the steel composition and prior microstructure. External spur and helical gears, bevel and worm gears, racks, and sprockets are commonly induction hardened. Typical gear steels include AISI/SAE grades 1050, 1060, 1144, 4140, 4150, 4350, 5150, and 8650.
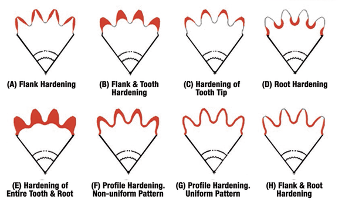
The hardness pattern produced by induction heating (Figure 3) is a function of the type and shape of inductor used, as well as the heating method. Quenching or rapidly cooling the workpiece can be accomplished by spray or submerged quench. The media typically used for the quench is a water-based polymer. The severity of this quenchant can be controlled by the polymer’s concentration. Cooling rates are usually somewhere in between what would be obtained from pure water and oil. In some unusual situations compressed air or nitrogen is used to quench the part.
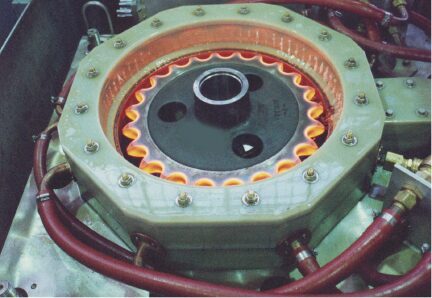
The most common methods for hardening gears and sprockets are by single shot (Figure 4) or the tooth-by-tooth method (Figure 5). Single shot often requires large kW power supplies but results in short heat/quench times and higher production rates. This technique uses a circumferential copper inductor, which will harden the teeth from the tips downward.
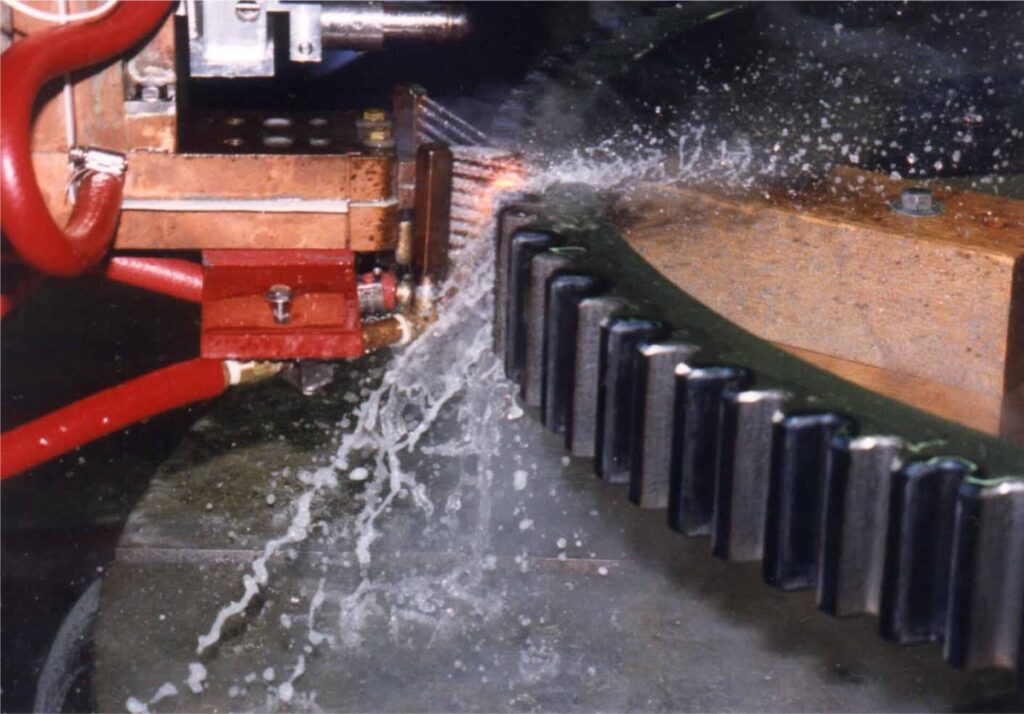
The larger and heavier loaded gears (where pitting, spalling, tooth fatigue, and endurance are issues) need a hardness pattern that is more profiled like those produced by carburizing, which can be obtained by tooth-by-tooth hardening. This method is limited to gear tooth sizes with modulus 4.23–5.08 (6 or 5 DP) using frequencies from 2 to 10 kHz and about 2.54 (10 DP) using a range of 25 to 50 kHz.
The lower the frequency, the deeper the case depth. Tooth-by-tooth hardening is a slow process and usually reserved for gears and sprockets that are too large to single shot due to power constraints. The process involves heating the root area and side flanks simultaneously, while cooling each side of the adjacent tooth to prevent temper-back on the backside of each tooth. The induction system moves the coil at a pre-programmed rate along the length of the gear. The coil progressively heats the entire length of the gear segment while a quench follower immediately cools the previously heated area. The distance from the coil to the tooth is known as coupling or air gap. Any changes in this distance can yield variation in case depth, hardness, and tooth distortion. The gear is indexed after each tooth has been hardened, often skipping a tooth. This requires at least two full revolutions in the process to complete the hardening of all teeth. Straight, spur, and helical gears up to 5.5 m (210 inches) weighing 6,800 kg (15,000 lb) have been processed with this method. The entire process yields a repeatable soft tip of the tooth with hard root and flank. In other applications, the tip and both flanks can be hardened simultaneously and yield a soft root.
In Summary
Today’s design engineer has the good fortune of being able to choose from a number of heat treatment technologies for any given type of gear material and design. When selecting a gear hardening method, it is essential to specify not only the desired mechanical and metallurgical properties, but the critical dimensions that must be held and even the desired stress state of the gears themselves. The secret to success is understanding the advantages and limitations of each technology and taking these into consideration when determining the overall cost of gear manufacturing.
References
Herring, Daniel H. 2004a. “Gear Heat Treatment: The Influence of Materials and Geometry.” Gear Technology, March/April.
Herring, Daniel H. 2004b. “Reducing Distortion in Heat-Treated Gears.” Gear Solutions, June.
Herring, Daniel H. 2007a. “Oil Quenching Technologies for Gears.” With Steven D. Balme. Gear Solutions, July.
Herring, Daniel H. 2007b. “Heat Treating Heavy Duty Gears.” With Gerald D. Lindell. Gear Solutions, October.
Herring, Daniel H. 2012–2016. Vacuum Heat Treatment. Vols. 1–2. BNP Media Group.
Herring, Daniel H. 2014–2015. Atmosphere Heat Treatment. Vols. 1–2. BNP Media Group.
Herring, Daniel H., Gerald D. Lindell, D. J. Breuer, and B. Matlock. 2001. “Atmosphere vs. Vacuum Carburizing.” Heat Treating Progress, November.
Herring, Daniel H., Gerald D. Lindell, D. J. Breuer, and B. Matlock. 2002. “An Evaluation of Atmosphere and Vacuum Carburizing Methods for the Heat Treatment of Gears.” In Off-Highway Conference Proceedings. SAE International.
Otto, Frederick J., and Daniel H. Herring. 2002a. “Gear Heat Treatment: Today and Tomorrow, Part 1.” Heat Treating Progress, June.
Otto, Frederick J., and Daniel H. Herring. 2002b. “Gear Heat Treatment: Today and Tomorrow, Part 2.” Heat Treating Progress, July/August.
Otto, Frederick J., and Daniel H. Herring. 2005. “Vacuum Carburizing of Aerospace and Automotive Materials.” Heat Treating Progress, January/February.
Otto, Frederick J., and Daniel H. Herring. 2007. “Advancements in Precision Carburizing of Aerospace and Motorsports Materials.” Heat Treating Progress, May/June.
Otto, Frederick J., and Daniel H. Herring. 2008. “Improvements in Dimensional Control of Heat Treated Gears.” Gear Solutions, June.
Rudnev, V. 2000. “Gear Heat Treating by Induction.” Gear Technology, March/April.
About the Author
“The Heat Treat Doctor”
The HERRING GROUP, Inc.
Dan Herring has been in the industry for over 50 years and has gained vast experience in fields that include materials science, engineering, metallurgy, new product research, and many other areas. He is the author of six books and over 700 technical articles.
For more information: Contact Dan at dherring@heat-treat-doctor.com.
For more information about Dan’s books: see his page at the Heat Treat Store.
Ask The Heat Treat Doctor®: Why and How Do We Heat Treat Gears? Part Two Read More »
GM Invests in Casting Capacity Expansion
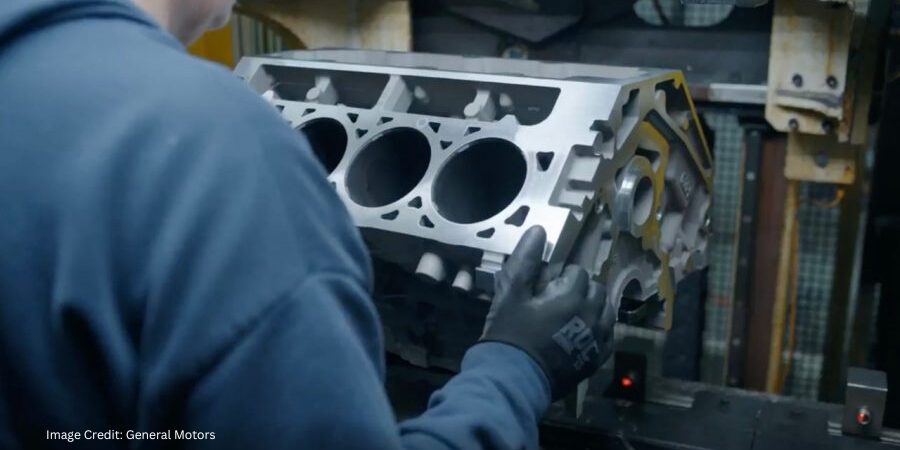
General Motors announced plans to invest more than $150 million in its Saginaw Metal Casting Operations facility in Michigan to support production of V8 engine blocks and cylinder heads used in full-size trucks and SUVs. The project includes new and upgraded equipment for casting and machining operations, enabling the facility to increase production capacity and maintain output for current engine programs. The Saginaw site has supplied engine components for multiple generations of GM vehicles.
This new commitment builds on the approximately $5.5 billion in investments GM made in 2025, underscoring GM’s support for U.S. manufacturing, while securing the future of this facility and its employees.
“By enabling the production of next-generation engine blocks and cylinder heads for full-size trucks, the plant is well-positioned for the future. This not only secures existing jobs but also strengthens the local economy, and ensures the plant continues to be an integral part of the automotive supply chain,” said John Lancaster, plant director.
Press release is available in its original form here, where readers can also watch an embedded video providing additional context on the investment.
GM Invests in Casting Capacity Expansion Read More »
News from Abroad: Energy, Automation, and Emerging Manufacturing Technologies
In today’s News from Abroadinstallment, we highlight several major global developments — from furnace installations to energy agreements to automation upgrades and additive manufacturing advances — underscoring continued investment in reliability, material innovation, and production efficiency across the global metals processing landscape.
Heat Treat Today partners with two international publications to deliver the latest news, tech tips, and cutting-edge articles that will serve our audience — manufacturers with in-house heat treat. Furnaces International, a Quartz Business Media publication, primarily serves the English-speaking globe, and heat processing, a Vulkan-Verlag GmbH publication, serves mostly the European and Asian heat treat markets.
Annealing Systems Back Expansion of High-Grade Steel
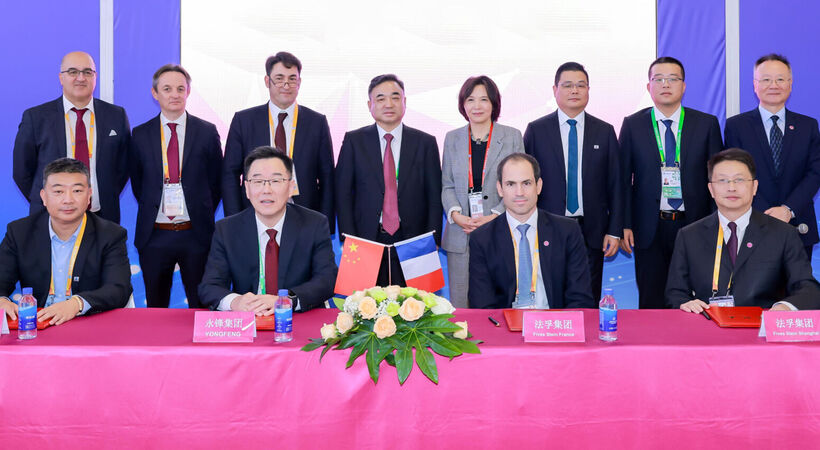
“Fives has signed a major contract with Yongfeng Group for three annealing furnaces of new strip processing lines. Yongfeng Group is building a new facility in Linyi, Shandong province of China to produce a wide variety of high-grade steel products, including exposed and non-exposed automotive sheets and advanced high-strength steels.”
“The new vertical annealing furnaces will be equipped with the latest generation of the AdvanTek combustion system, characterized by energy efficiency, fuel flexibility, and low emissions, as well as a FlashCooling rapid cooling system. The FlashCooling system is a unique cooling technology capable of using high hydrogen gas, offering operational flexibility in cooling rate control, temperature cycle control, and uniformity of cooling.”
Read more: “Fives delivers annealing furnaces for high-end steel lines” at furnaces-international.com.
Power Deal Secures Long-Term Future of Aluminum Smelter
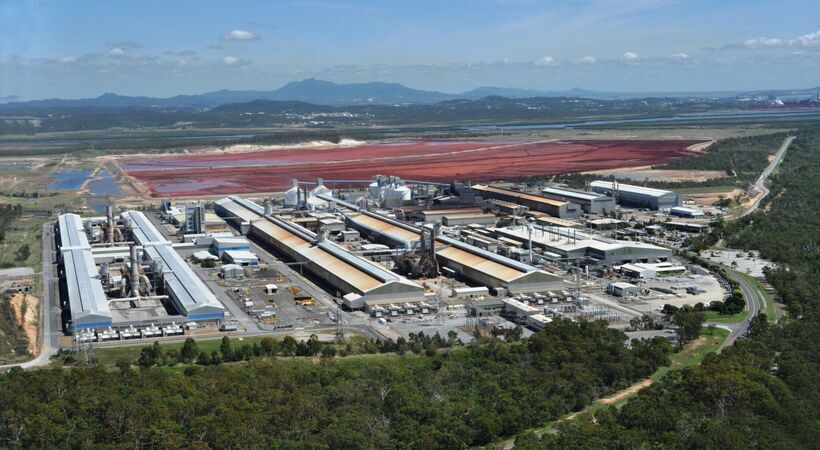
“The future of the Boyne aluminium smelter in Gladstone, Australia, has been secured until at least 2040. Rio Tinto, the Queensland Government, and the Commonwealth Government have struck a partnership to secure a long-term future for the smelter and ensure it remains internationally cost-competitive beyond its current power contract.”
“Rio Tinto Aluminium & Lithium Chief Executive Jérôme Pécresse said: ‘As fossil fuels become increasingly expensive, this investment, combined with the power purchase agreements we have already signed, positions Boyne to be among the world’s first aluminium smelters underpinned by solar and wind power. It also ensures heavy manufacturing like aluminium smelting can continue in Gladstone for the long term and preserves one of the few fully integrated aluminium value chains in the world — from bauxite mining to alumina refining to aluminium smelting all in Queensland — as demand for aluminium continues to grow with the energy transition.’”
Read more: “Boyne aluminium smelter secures power contract” at furnaces-international.com.
Updated Control Systems Boost Reliability at Hot Strip Mill
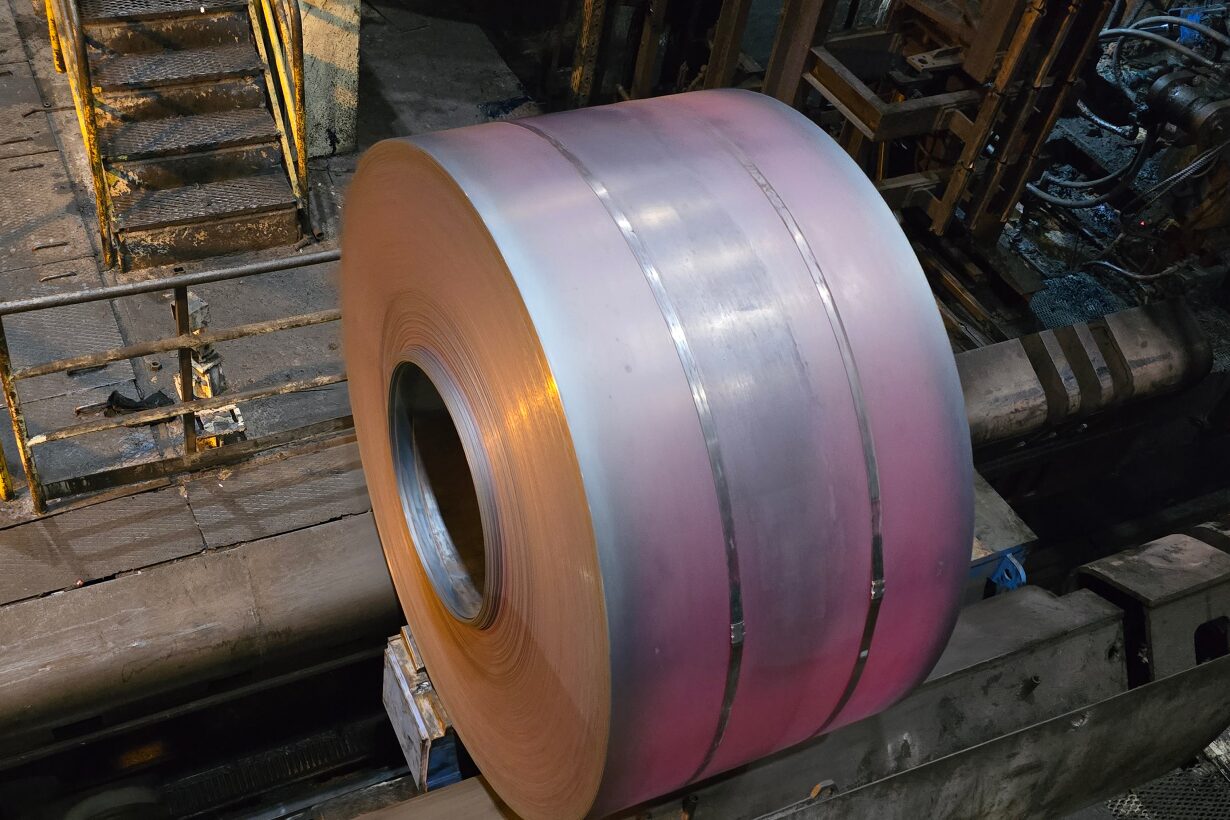
“Primetals Technologies has received the final acceptance certificate (FAC) from a Turkish steel producer after successfully completing a phased upgrade of its hot-strip mill.”
“Phase 1 focused on upgrading the process automation system, while Phase 2 included modernizing the basic automation system and implementing advanced profile and flatness control. Primetals Technologies also installed the ALEX condition monitoring system. The hot-strip mill was restarted as scheduled following installation and commissioning.”
Read more: “Primetals Technologies’ Modernization of Automation Systems Boosts Reliability at Hot-Strip Mill” at heat processing.
New Metal Powder Supports Additive Manufacturing for Aerospace Components
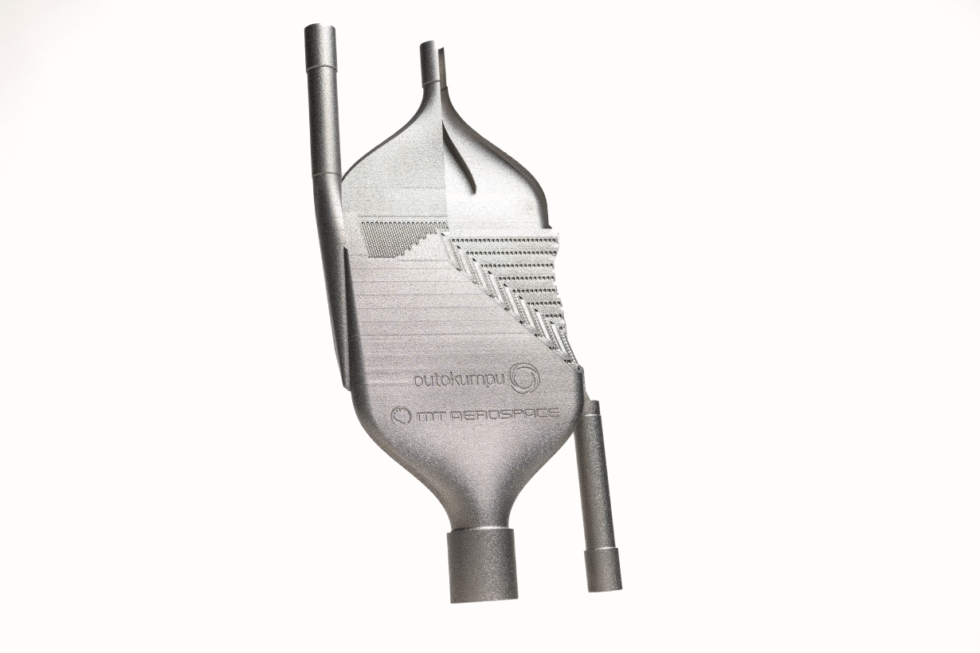
“Outokumpu, a supplier of sustainable stainless steels, has achieved significant progress in additive metal powder manufacturing in collaboration with MT Aerospace. As a result of the partnership, a modified 316L stainless steel powder was developed, specifically designed for aerospace applications.”
“The product development project, “Modified 316L powder for aerospace [1157],” was carried out at Outokumpu’s Metal Powder Research Center in Krefeld, Germany. The focus was on precise chemical adjustments within the ASTM F3184 standard and optimization of process parameters during powder production. The result is a modified version of the 316L powder, which allows MT Aerospace to achieve the desired mechanical properties in components using the powder bed laser melting process and meets the precision and performance requirements of the aerospace industry.”
Read more: “Outokumpu and MT Aerospace are advancing additive manufacturing for aerospace applications” at heat processing.
News from Abroad: Energy, Automation, and Emerging Manufacturing Technologies Read More »
Heat Treating Supports Aerospace Components for Artemis II Mission
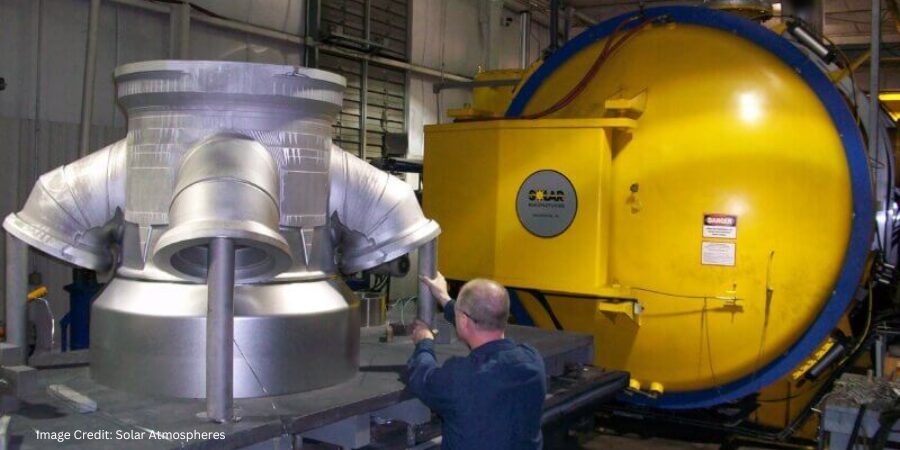
Solar Atmospheres has provided thermal processing services for materials and components used in the Artemis II mission, supporting aerospace applications that require precise control of material properties and performance under extreme conditions.
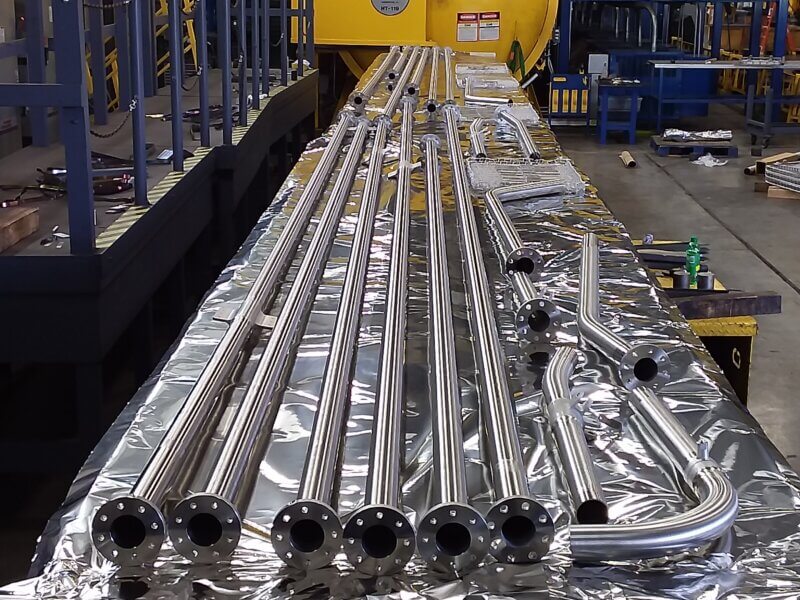
The heat treater specializes in thermal processing of a range of materials, including raw stock, nickel-based tubing, and other aerospace components that play a vital role in bringing next-generation space technology to life.
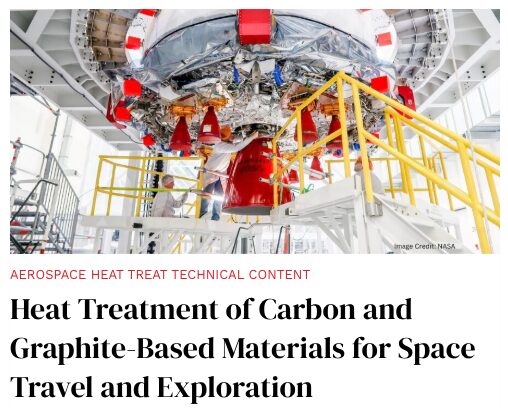
At the core of some of these components is the 6AI-4V titanium Launch Abort System (LAS), which is a complex safety system. The LAS aboard the Orion spacecraft functions as a rocket capable of outrunning another rocket in an emergency. In the event of a catastrophic launch anomaly, its manifold enables the abort motor to ignite and safely propel the crew module away from the rocket.
Components used in these applications must meet strict requirements for precision and reliability, with little margin for error in performance.
Press release is available in its original form here.
Heat Treating Supports Aerospace Components for Artemis II Mission Read More »
Heat Treatment of Carbon and Graphite-Based Materials for Space Travel and Exploration
Carbon and graphite-based materials are among the few engineered materials capable of withstanding the extreme thermal, mechanical, and environmental demands of space travel. In this Technical Tuesday installment, Kimberly Thompson, technology manager at Morgan Advanced Materials, examines how carefully controlled heat treatment directly governs the structure, purity, and performance of these materials and emphasizes the importance of furnace design, atmosphere control, and temperature precision required to achieve reliable properties for aerospace and space exploration applications.
This informative piece was first released in Heat Treat Today’s March 2026 Annual Aerospace Heat Treating print edition.
Space travel presents one of the most extreme operating environments encountered by engineered materials. Launch, orbital operation, atmospheric reentry, and deep space exposure all impose combinations of extreme temperature, rapid thermal cycling, oxidative attack, mechanical stress, and radiation. Among the limited class of materials capable of performing in these challenging conditions, carbon and graphite-based materials have played a critical role for decades, continuing to enable and innovate modern space exploration.
From carbon ablatives, which play a crucial role in heat shields and propulsion systems, to structural graphite components and ultra-pure graphitic elements, carbon materials are uniquely suited to survive and perform in extreme temperature regimes that exceed the limits of metals and ceramics. The performance of these graphite/graphite-like materials is directly linked to the heat treatment (aka graphitization) and processing steps used during their manufacture. The relationship between processing conditions and final product performance is driven by the technical foundations for heat treating carbon and graphite materials for space travel through the conversion, graphitization, and purification steps.
Carbon Materials in Space Applications
Carbon-based materials, such as those produced by the Performance Carbon division of Morgan Advanced Materials (see Figures 1-3), have a long history of being utilized in spaceflight systems due to their exceptional thermal stability, low density and mass, and resistance to thermal shock. Common applications include:
- Ablative thermal protection systems for atmospheric re-entry
- Nozzle throats and rocket motor components
- High temperature insulation and support
- Structural graphite parts
- Ultra-pure graphitic components for sensitive electronic or propulsion systems
The performance outcomes required in these applications are diverse but share common demands: survivability at extreme temperature exceeding 2000°C (3630°F) and down to -270°C (-450°F), predictable thermal behavior, low outgassing, and controlled erosion or sublimation rates. Achieving these characteristics relies heavily on heat treatment processing conducted through both low and high temperatures.
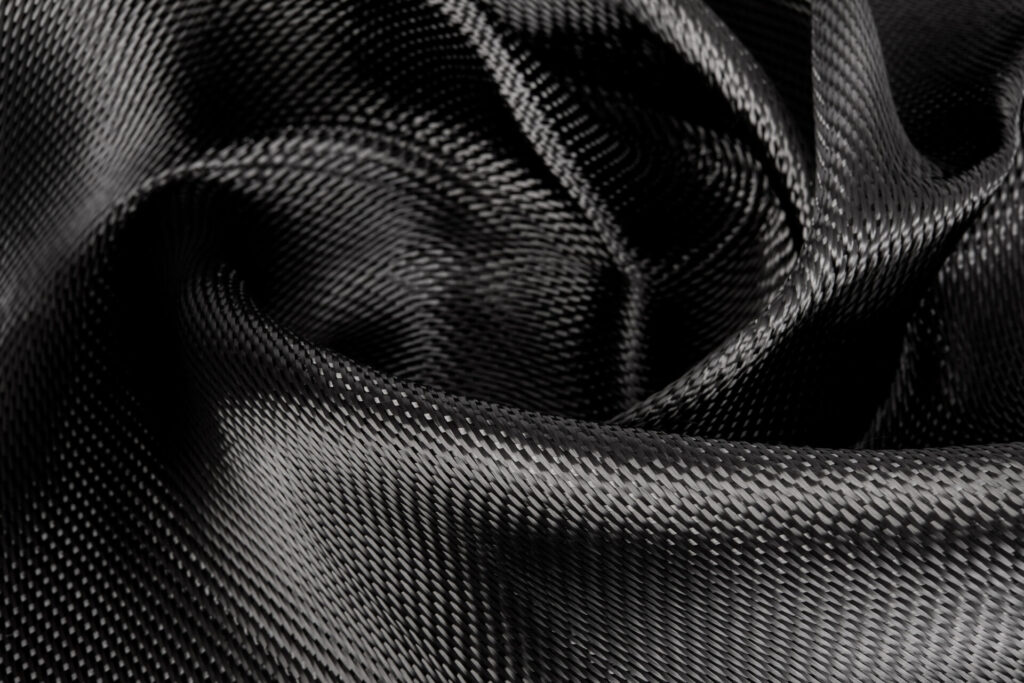
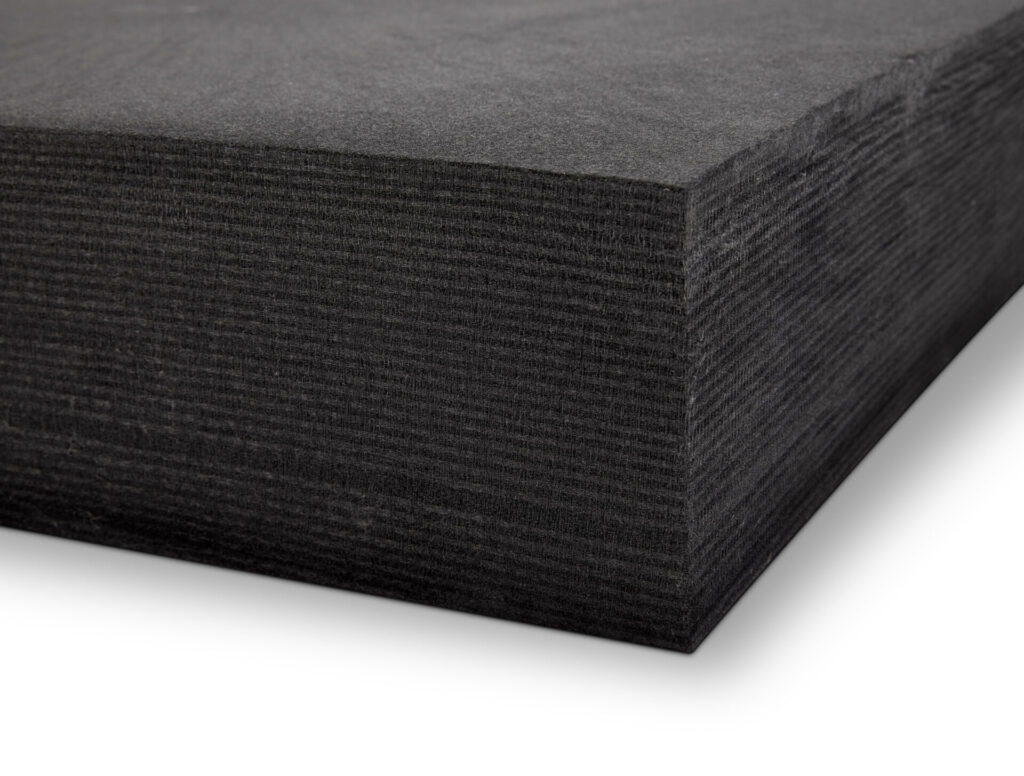
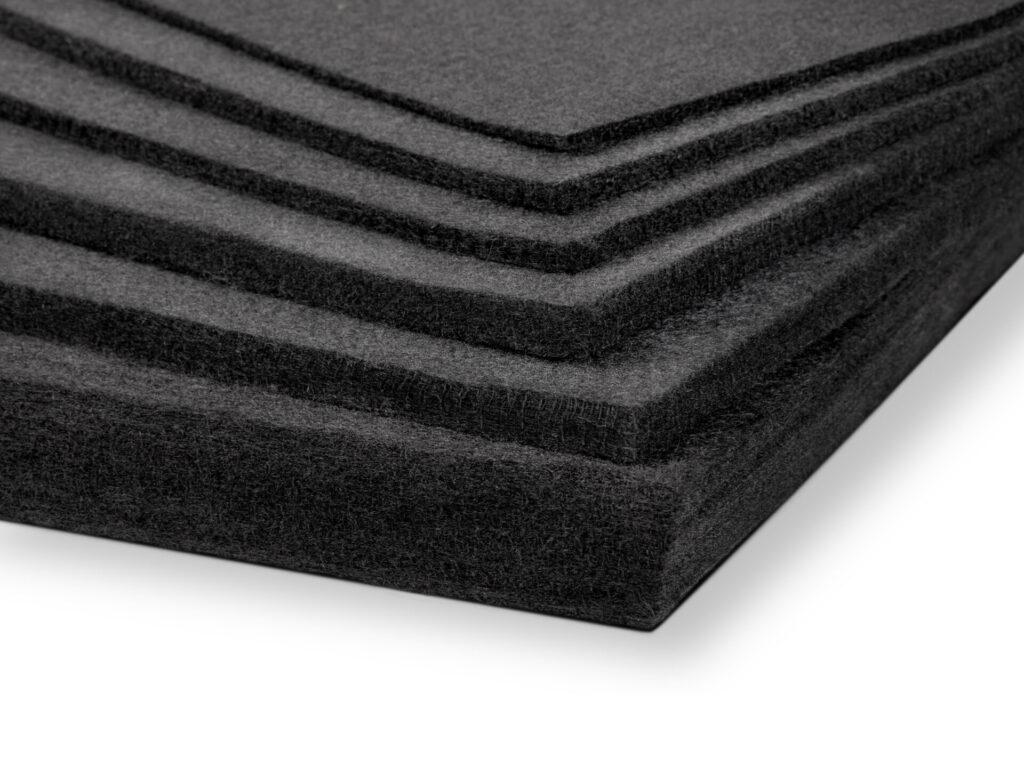
As the material is heat treated and temperatures increase, the carbon structure will undergo progressive stabilization. Precursor conversion or pre-carbonization will occur during low temperature thermal processing. Fundamental transformation will occur as the disordered carbon structure reorganizes into graphitic planes through realignment of aromatic carbon layers. The planes become progressively ordered in the presence of elevated temperatures, increasing crystallographic alignment. The transition from carbon to graphite is gradual and highly reliant on heat treatment process capability to maintain thermal uniformity throughout all process stages.
The extent of graphitization is typically tailored to meet specific application requirements, as carbon and graphite structures each offer distinct performance advantages. In certain applications, a predominately carbon structure is preferred due to its higher bulk density and superior mechanical strength as compared to graphite. These characteristics can be advantageous in space applications where structural integrity, load bearing capability, or erosion resistance under mechanical stress are primary concerns. However, carbon materials generally exhibit slightly lower carbon yield and may experience higher erosion or mass loss when exposed to extreme thermal flux or oxidative stress.
In contrast, materials processed to a graphitic structure offer enhanced thermal stability at elevated temperatures, improved resistance to thermal shock, and reduced impurity content due to high temperature volatilization of contamination. Graphite materials typically demonstrate superior performance in applications requiring sustained exposure to ultra high temperature or rapid thermal cycling. This benefit, however, is often accompanied by lower density and reduced mechanical strength relative to their carbon counterparts, which can limit their use in mechanically demanding roles.
Ultimately, the selection of a carbon- or graphite-based structure involves balancing thermal performance, mechanical requirements, erosion behavior, and environmental exposure. Heat treatment parameters must be carefully engineered to achieve the desired degree of structural ordering, ensuring that the final material delivers optimal performance for its intended spaceflight application.
Low Temperature Thermal Processing
Most engineered carbon precursors, such as cellulose, phenolic resin, acrylic (polyacrylonitrile), or pitch-based materials, require conversion into carbon through a sequence of controlled thermal processes. The first conversion process is considered low temperature in terms of graphite processing. During this process, hydrogen, oxygen, and nitrogen content decreases, volatile species are driven off, and the aromatic carbon structures begin to form. The thermal processing profile through this low temperature conversion is critical. Careful control of heat treatment parameters, tailored to the material system, supports uniform carbon conversion and minimizes defects as the foundational microstructure is established.
At these processing temperatures, a wide range of conventional heat treatment equipment can be effectively used. Because the operating temperatures remain below the limits of most metallic alloys, furnaces equipped with metal-based heating elements, structural components, and containment systems are generally suitable for this phase of processing. Additionally, these furnaces may be configured as batch or continuous systems, depending on part geometry, production volume, and process control requirements. Heat input is achieved through established industrial thermal processing approaches, with system selection guided by requirements for temperature uniformity, process control, and operational considerations. Regardless of the configuration, the selected furnace must be capable of maintaining stable inert or reducing atmospheres to prevent oxidation of the carbon precursor during thermal decomposition.
Successful low temperature processing demands a strong foundational understanding of carbonization mechanisms combined with sound materials science principles. As organic precursors are heated, complex chemical reactions occur that result in the formation of increasingly ordered carbon structures. The heating rate and soak durations must be carefully engineered to accommodate these reactions while minimizing internal stresses, distortion, or excessive porosity. Improper ramp rates or insufficient soak times can result in non-uniform shrinkage and irreversible defects that propagate through later processing stages.
Equally critical is the furnace’s ability to execute the programmed temperature profile with a high degree of precision and repeatability. Accurate control of heating ramps, dwell temperatures, and cooling rates is essential, as even modest deviations can alter the evolving microstructure of the material. Temperature overshoot, uncontrolled gradients, or localized hot spots can lead to uneven carbon yield, variations in density, and inconsistent mechanical or thermal properties in the final product. Consistency of temperature accuracy within the furnace ensures that the entire product load processes uniformly, reducing variation in the material to allow for uncompromised performance in demanding aerospace applications.
High Temperature Thermal Processing
Materials that have completed precursor conversion or pre-carbonization are subsequently subjected to high temperature thermal processing to complete carbonization or to initiate and advance graphitization, thereby establishing the final material structure and properties. Although the carbon microstructure continues to evolve significantly during this stage, the material experiences minimal additional mass loss, shrinkage, or chemical decomposition compared to earlier processing stages. Most volatile species have already been removed, resulting in a comparatively stable structure that is less susceptible to distortion, cracking, or dimensional change. As a result, parts processed in this temperature regime typically exhibit improved dimensional stability and reduced sensitivity to heating rates when compared to low-temperature carbonization operations.
High-temperature processing can be conducted at temperatures well above the lower temperature processing. At these elevated temperatures, the available furnace technologies become significantly limited. Conventional metal or ceramic based furnace systems are no longer suitable due to material degradation, contamination risk, and structural instability under these conditions. Instead, furnaces designed for high-temperature carbon and graphite processing are typically induction or resistance (i.e., vacuum furnace) heated and constructed primarily from graphite-based components.
These furnace systems are specifically engineered to withstand extreme temperatures while maintaining thermal uniformity and chemical compatibility with the carbon materials being processed. The use of graphite heating elements, insulation, and structural components minimizes contamination and allows operation in inert or controlled atmospheres required for carbon and graphite processing.
As relatively little chemical decomposition occurs during this phase, high-temperature processing cycles can often be completed more rapidly than low-temperature carbonization cycles. Additionally, moderate temperature variations within the furnace are less likely to produce significant variability in final material properties. However, precise temperature control remains critical, as the peak temperature achieved during processing largely determines the degree of carbonization or graphitization and, consequently, the final microstructure and performance characteristics of the material.
Continuous monitoring and accurate measurement of operating temperatures are therefore essential. Even small deviations in maximum temperature can lead to meaningful differences in crystallinity, density, thermal conductivity, and mechanical behavior. For space applications, where consistency and reliability are paramount, ensuring that each component reaches the intended peak temperature is a defining requirement of high-temperature thermal processing. As space missions continue to demand materials capable of performing in the most extreme environments, advanced heat treatment remains a critical enabler of reliability and innovation.
About The Author:
Technology Manager
Morgan Advanced Materials
Kimberly Thompson holds a bachelor’s degree in chemical engineering from Purdue University and a master’s degree in materials engineering from Auburn University. With nearly nine years with Morgan Advanced Materials, she currently serves as technology manager leading new product development and has spent six years as the technical resource for rayon-based carbon and graphite materials supporting space industry applications.
For more information: Contact Kimberly Thompson at Kimberly.Thompson@morganplc.com.
Heat Treatment of Carbon and Graphite-Based Materials for Space Travel and Exploration Read More »