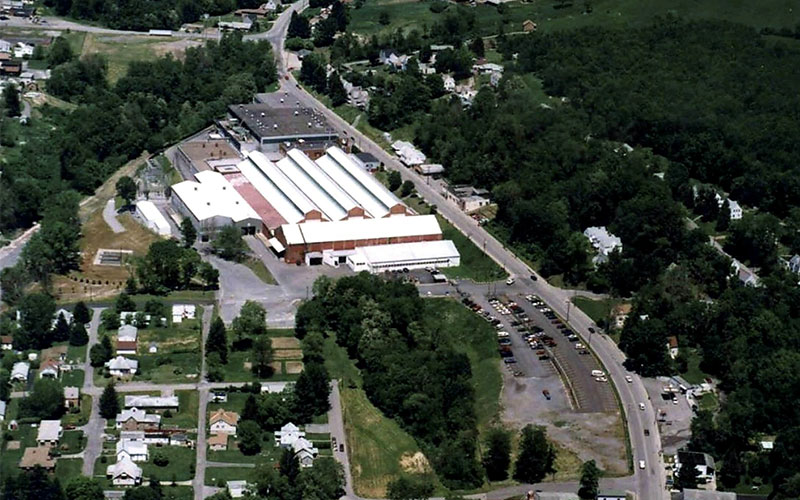
Advanced Heat Treat Corp. (AHT), a global provider of commercial heat treat services and metallurgical solutions, is expanding its Waterloo, Iowa, facility to increase capacity for carburizing, through hardening, normalizing, and other heat treatment processes. The 18,000 sq. ft. project broke ground on April 6 and is expected to be completed by fall 2026.
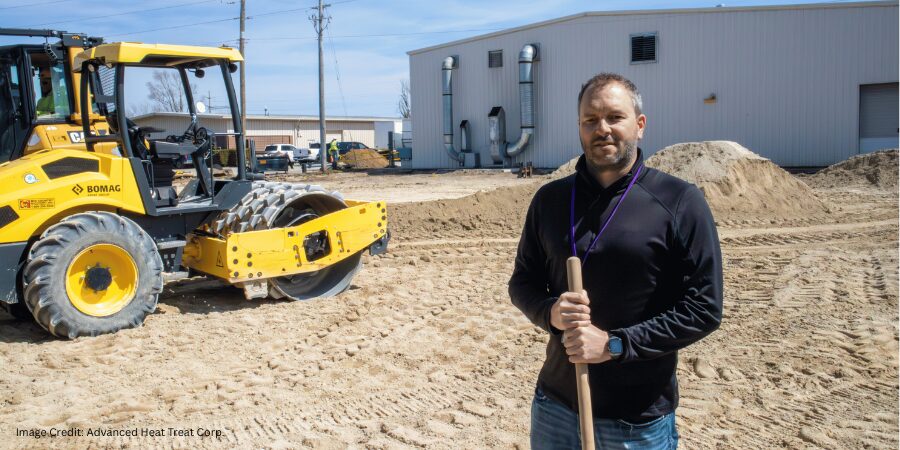
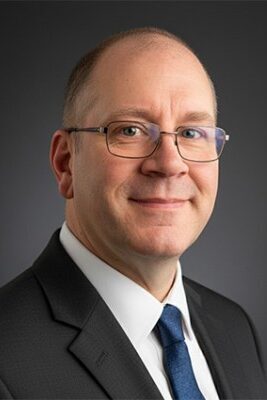
The expansion will include a custom-built furnace designed to accommodate larger components in length, height, and weight. “This expansion is about giving our [clients] more — more capacity, more capability, and more confidence in turnaround,” said Adam Kane, plant manager at AHT’s Waterloo facility pictured above. “With added production space and additional equipment, we’ll be able to process larger and heavier components, and we’ll have room to add even more equipment and services in the future.”
Mikel Woods President Advanced Heat Treat Corp.
The facility, in operation at Burton Ave. since 1981, provides services including induction hardening, annealing, cryogenic treatment, carbonitriding, and stress relieving. A second Waterloo location on MidPort Blvd. serves as the company’s corporate office and offers nitriding and nitrocarburizing services.
“Between the two Iowa locations, [clients] have access to multiple heat treatments within a short drive, allowing them to consolidate their vendors and potentially reduce freight costs,” added Mikel Woods, president of AHT.
Press release is available in its original form here. Main image shows AHT plant manager Adam Kane standing on the construction site of the 18,000 sq. ft. building expansion in Waterloo, Iowa.
Allied Graphite, a U.S.-based graphite materials manufacturer, is advancing the high-temperature thermal processing of its battery-grade material with a new technology partnership. This partnership to develop, validate, and provide engineering data for vertical furnace solutions will support the company’s progress toward commercial-scale production.
The effort aims to design, test, and refine vertical furnace configurations in partnership with Harper International, a U.S.-based global provider of high-temperature thermal processing systems for advanced materials, and ONEJOON GmbH, a global supplier of high-temperature thermal processing equipment. The systems are intended to support processing steps required for battery-grade graphite production.
As part of the collaboration, Harper International is contributing engineering and validation programs conducted at Harper’s Technology Center in Buffalo, New York. Meanwhile, the partnership with ONEJOON GmbH will include joint engineering work and advanced development activities intended to support the design and validation of commercial-scale furnace configurations.
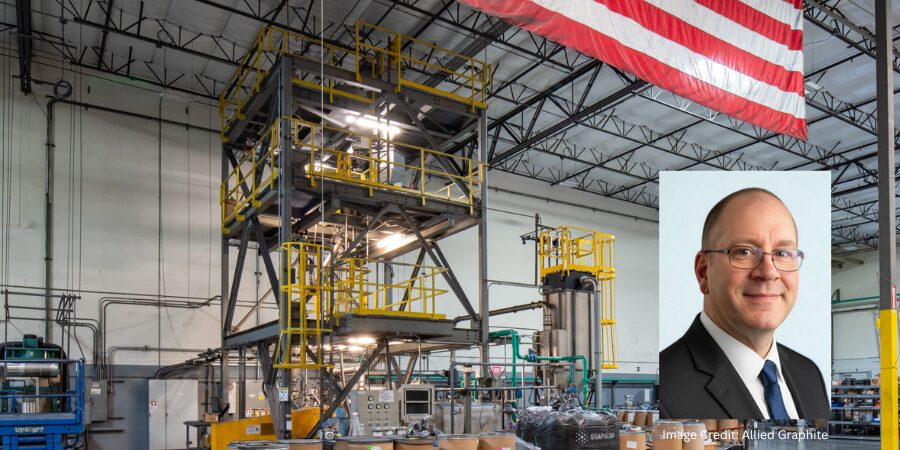
Andy Goshe Chief Executive Officer Allied Graphite
“Thermal processing performance is fundamental to delivering consistent product quality at scale. These partnerships reflect our commitment to rigorous engineering validation and disciplined equipment selection as we advance toward commercial-scale operations,” said Andy Goshe, chief executive officer of Allied Graphite.
The collaboration includes engineering development and validation programs to evaluate furnace designs under production conditions. The work is expected to generate process data to inform final equipment selection and support the transition from pilot-scale validation to commercial manufacturing.
High-temperature thermal processing is a key component of graphite production. Vertical furnace systems are being assessed for performance and scalability in production environments, key considerations as demand grows in the battery sector.
Press release is available in its original form here.
Heat Treat Today publishes twelve print magazines annually and included in each is a letter from the publisher, Doug Glenn. This letter from the March 2026 Annual Aerospace Heat Treating print edition highlights the growing presence of heat treat-focused podcasts in North American market, spotlighting both The Heat Treat Podcast with Carlos Torres and Heat Treat Radio, including the transition to a new host, Heather Falcone and the continued evolution of digital content in the industry.
It’s amazing to me that there are at least two professionally done heat treat podcasts in the North American heat treat marketplace. There are actually more than two podcasts, but the two I’m speaking of are ongoing and very targeted toward the North American heat treat industry. Check the end of this column for a link to some of the other podcasts I won’t be discussing at length here.
The Heat Treat Podcast with Carlos Torres
Let’s start with the podcast that it not part of Heat TreatToday — The Heat Treat Podcast with our friend Carlos Torres. Carlos is the CEO of TORSA Group Mattsa and a director at Mattsa Furnace Co. in San Luis Potosi, Mexico. Carlos’ video podcast is housed on YouTube (www.youtube.com/@theheattreatpodcast) and has roughly 70 episodes. Carlos cooperates with Super Systems Inc. (SSI) in Mexico, so it is no surprise that Episode #1 from 2021 featured SSI president and all-around great guy, Jim Oakes. Carlos is a very engaging podcast host and has interviewed the likes of Tracy Dougherty, AFC-Holcroft; John Hubbard, former CEO, Bodycote; Chip Keough of the Atmosphere Group; Chad Wright from Wirco; and many other industry notables including Joe Powell, Ben Rassieur, Karen Stanton, Jason Orosz, Jim and Andy Orr, Andrew Bassett, and Trevor Jones.
When Carlos first started his podcast, I joked with him that there was no way he could keep up the pace of turning out good quality heat treat interviews. That was at least four years ago — I was wrong. Carlos continues to do a great job interviewing and posting helpful, timely heat treat content.
Heat Treat Today
The podcast that is a part of Heat Treat Today is Heat TreatRadio. By the time this column is published in March of 2026, Heat Treat Radio will have deployed over 131 episodes since 2016. Initially, the podcasts were strictly audio, but since January 2023, episodes have been video, audio, and transcribed. The list of industry notables is too long, but suffice it to say, it is impressive.
Heat Treat Radio’s new host, Heather Falcone
The BIG news regarding this podcast is that starting last month (February 2026), Heat Treat Radio has a new host, Heather Falcone, former CEO of Thermal-Vac Technology and currently the CEO of Falcone Consulting. Since 2016, I’ve had the pleasure (and responsibility) of hosting the Heat Treat Radio. Heat Treat Today‘s managing editor, Bethany Leone, has been hugely instrumental in the scheduling and production of episodes for the past four years. Both Bethany and I have handed over the reins to Heather, and we are very excited about how the podcast will morph and grow under Heather’s leadership.
By the way, Heather, in her previous life, was interviewed by both The Heat Treat Podcast (Carlos Torres) and Heat Treat Radio. She is, by every measure, an industry legend in her own right.
The nice thing about having Heather take the lead is her ability to “talk turkey” with other industry experts…something I was not able to do being a lowly “publishing guy,” and her creativity and technical savvy when it comes to digital products like audio and video productions. We’re very excited to have Heather on the Heat Treat Today team.
If you have a topic you’d like to see covered on a future episode, or if you know of someone that you think Heather should interview, please reach out directly to Heather at heather@heattreattoday.com.
Whether it’s The Heat Treat Podcast or Heat Treat Radio, I hope you find some of the heat treat audio (and video) helpful.
Heat TreatToday offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry. Enjoy these 26 news items, including Boeing’s addition of vacuum furnace capacity to expand in-house heat treating for aerospace components, Solar Atmospheres’ role in supporting thermal processing for materials used in NASA’s Artemis II mission, Aalberts surface technologies’ renewal of Nadcap certification for another 24 months, and more!
Equipment
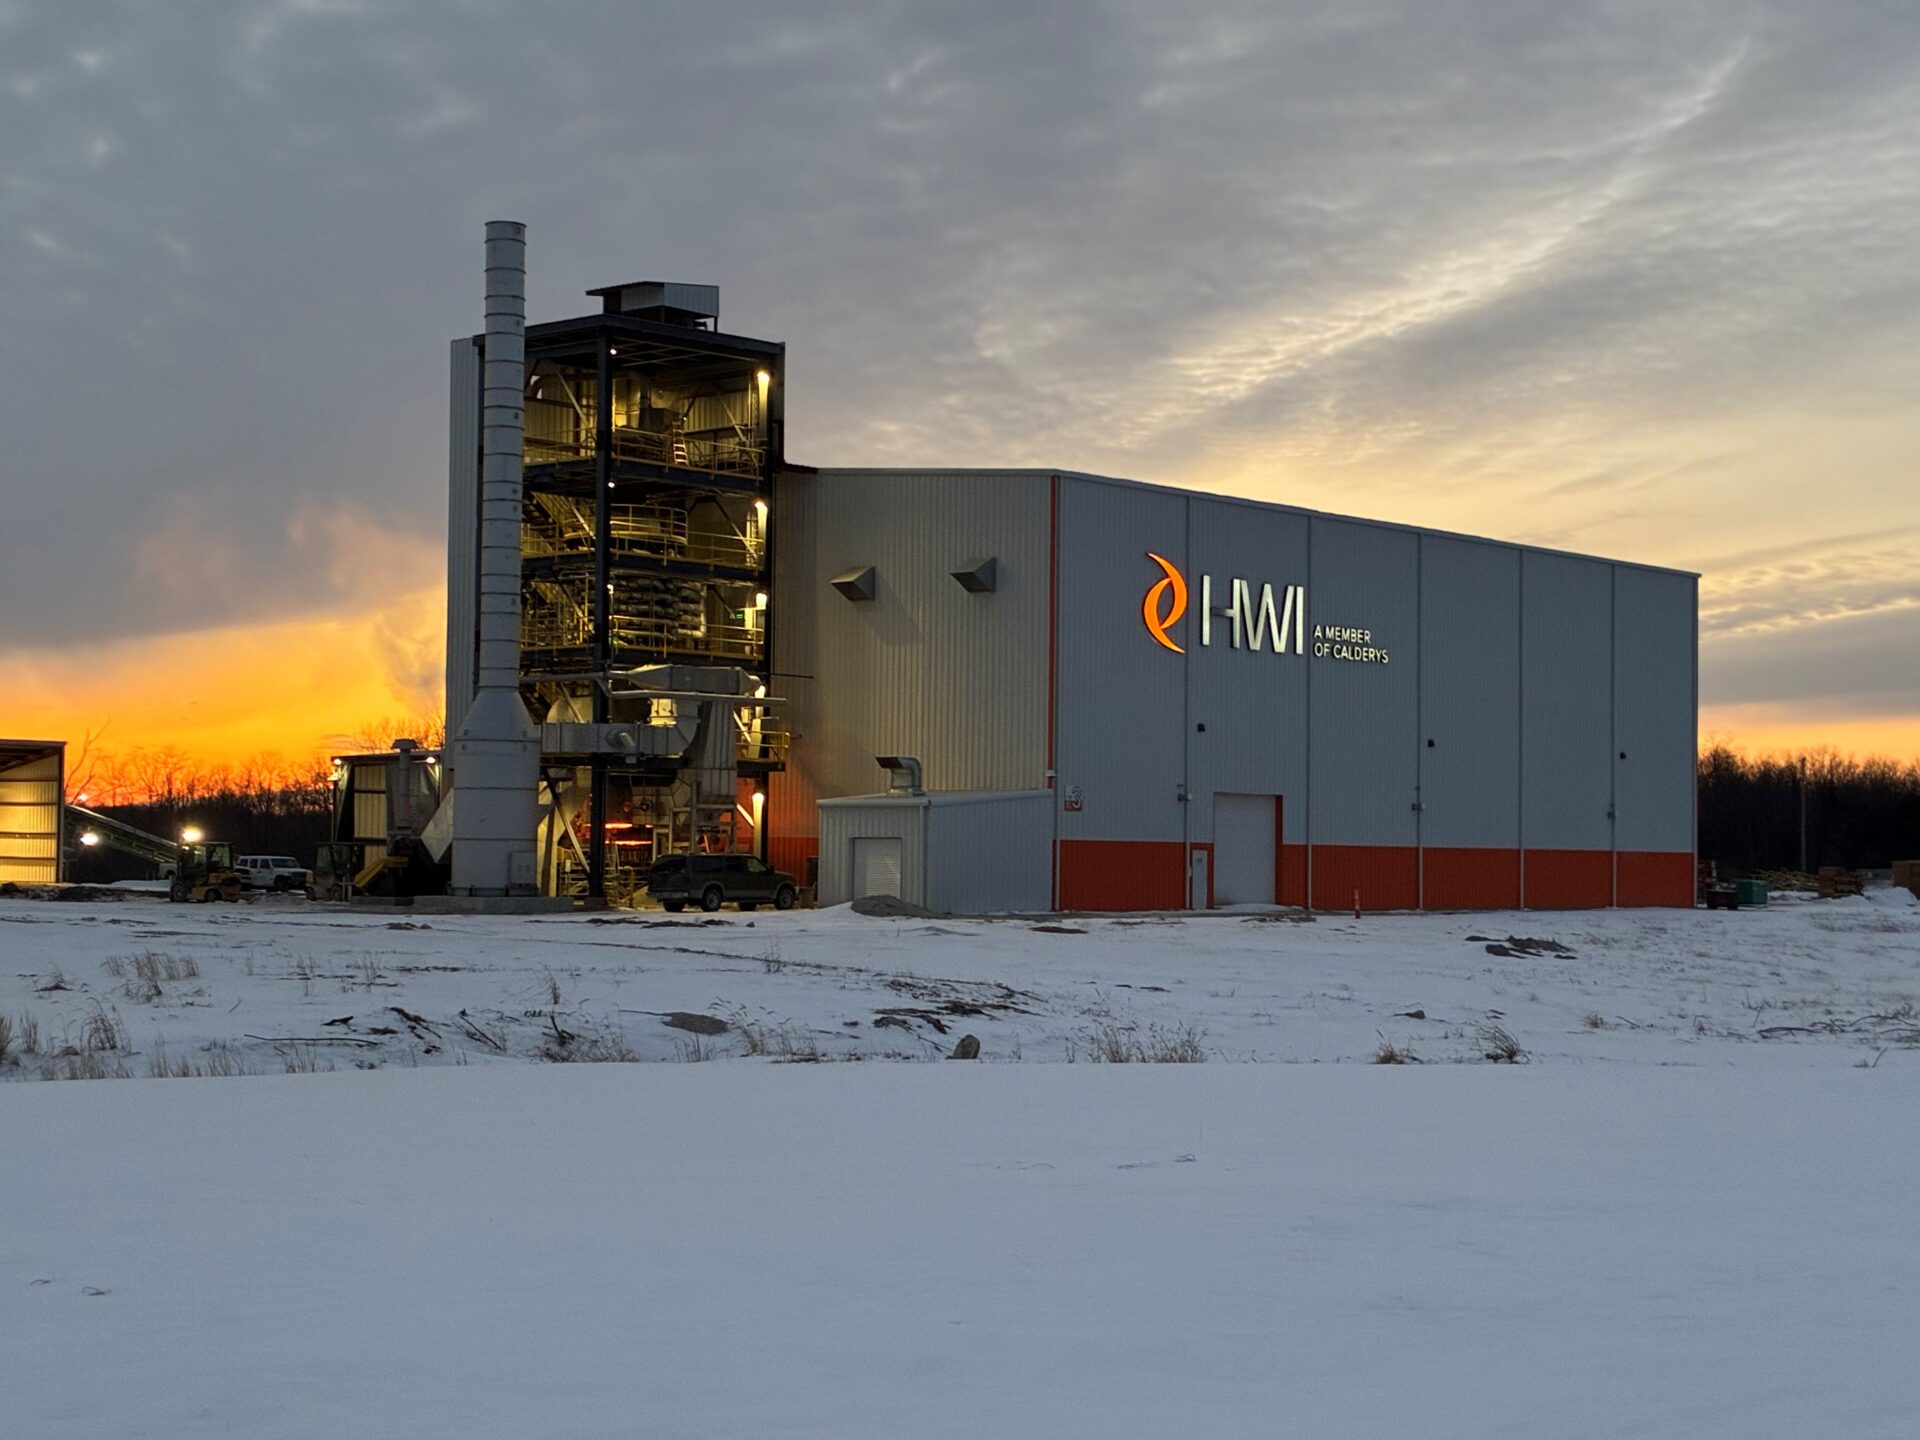
1. HWI, a member of Calderys Group, has opened a new lightweight monolithics production facility in Fulton, Missouri to expand manufacturing capacity for refractory materials used in high-temperature industrial applications. The facility increases supply and shortens lead times for furnace-lining materials critical to sectors like petrochemicals, aluminum, and power generation, enabling more reliable operations and supporting larger-scale projects.
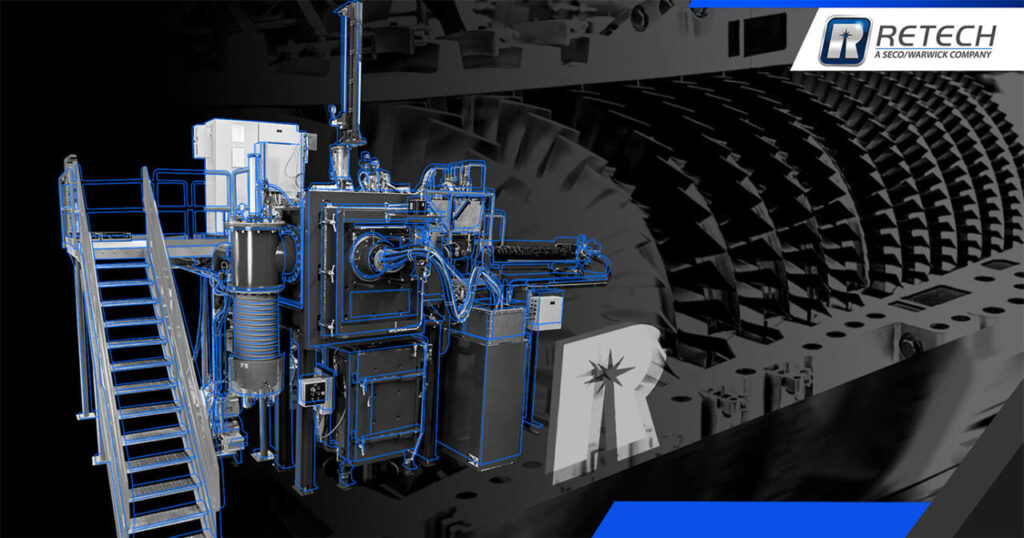
2. Retech, a U.S.-based member of the SECO/WARWICK Group, is supplying two vacuum induction melting (VIM) casting systems to support production of turbine components used in power generation. The systems are designed to produce advanced alloys with controlled microstructures for components operating under demanding thermal and mechanical conditions.
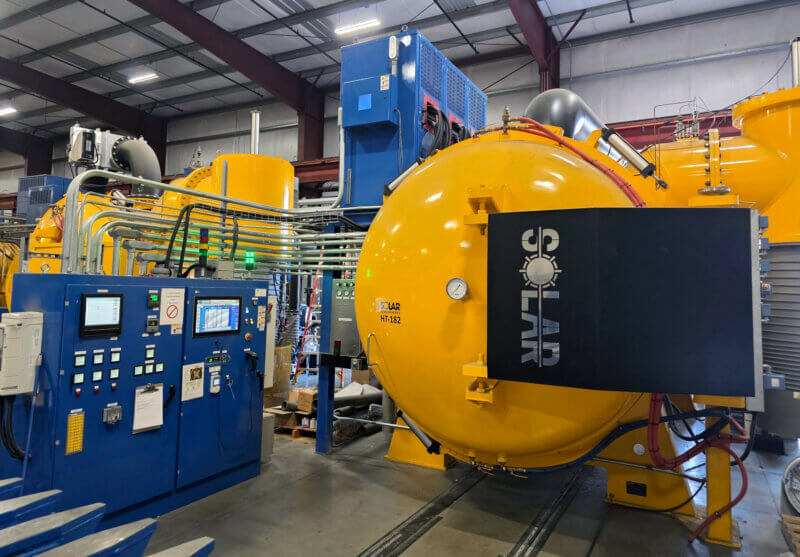
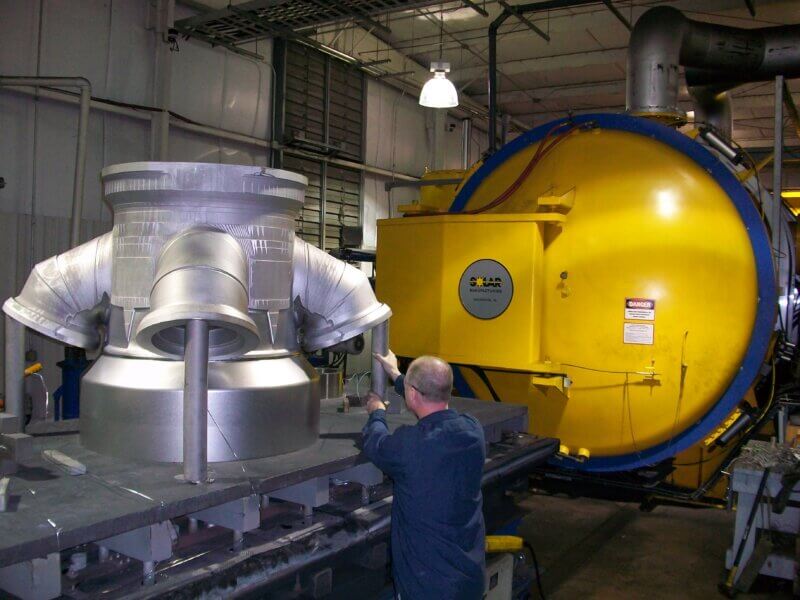
3. Solar Atmospheres has installed and commissioned a new 10-bar vacuum furnace at its Fontana, California, further expanding the company’s high-pressure vacuum heat treating capacity in the western United States. The system enables vacuum heat treating and high-pressure quenching of large components essential to high-performance applications across aerospace and other critical industries.
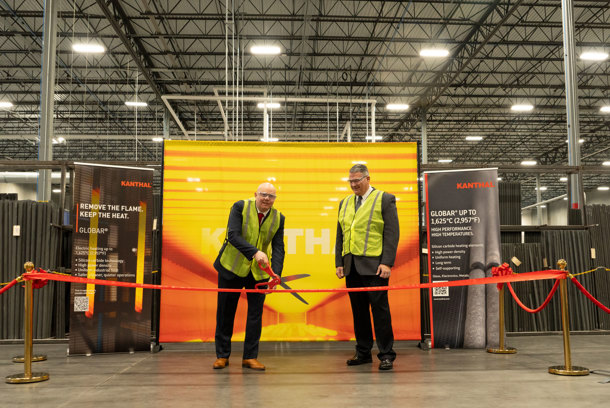
4. Kanthal, an Alleima company, has opened a new service center in Concord, North Carolina, adding U.S.-based production and service capabilities for silicon carbide heating elements used in high-temperature industrial applications across industries such as electronics, glass, and steel manufacturing.
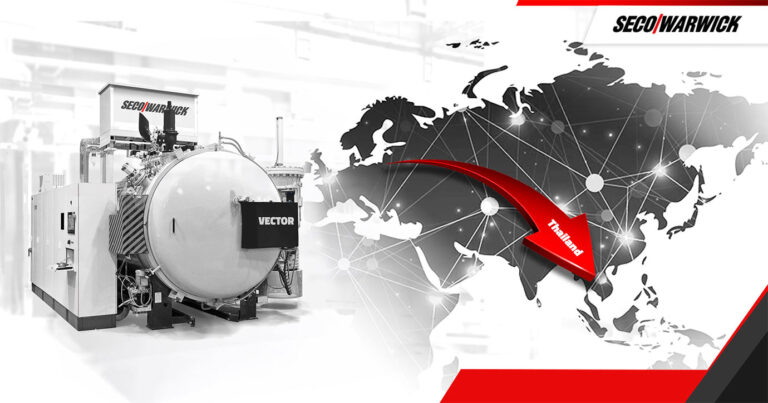
5. A Thai aerospace manufacturer has ordered a vacuum furnace from SECO/WARWICK to support heat treatment and vacuum brazing of high-performance alloys used in aircraft engine blades. The additional system expands production capacity and process control for critical materials like titanium and nickel alloys, strengthening the manufacturer’s ability to meet aerospace demand for high-precision, high-temperature components.
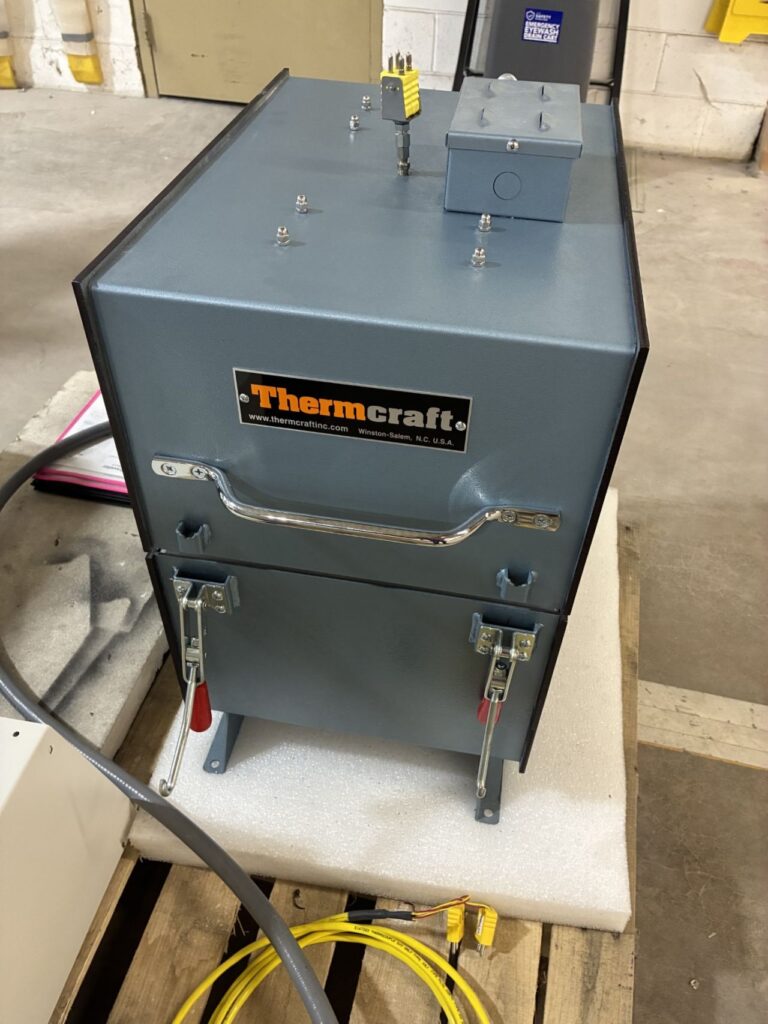
6. Thermcraft, a U.S.-based manufacturer of thermal processing equipment serving global markets, has completed the system for an application requiring materials to be tested under vibration while held at high temperature. The system was engineered to maintain a stable and uniform thermal environment while allowing measurement systems to interact directly with the test sample.
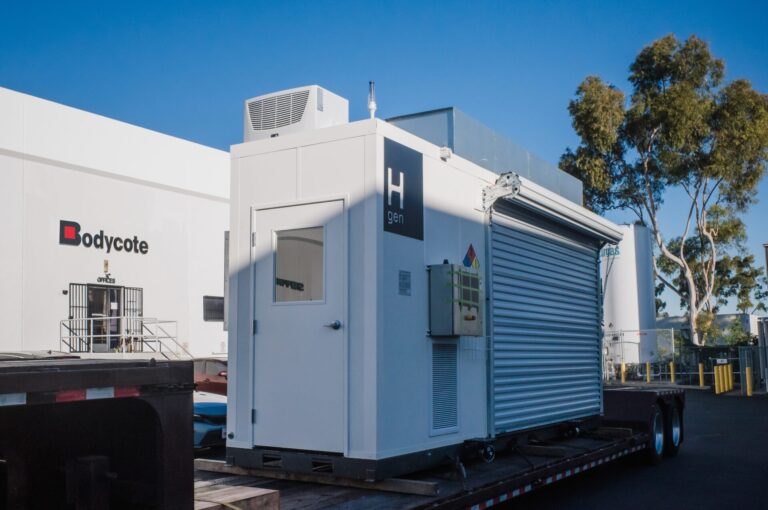
7. Bodycote, a global provider of advanced heat treatment and specialist thermal processing services, is improving heat treat efficiency and reducing process costs by generating hydrogen on-site at its Rancho Dominguez, California, facility. The system, developed in partnership with Hgen, supports controlled-atmosphere heat treatment and brazing operations for aerospace, automotive, energy, and defense applications while reducing reliance on delivered industrial gas.
8. Vacu-Braze, a commercial heat treater specializing in vacuum heat treating and brazing, has added a large-capacity nitriding furnace to support processing of oversized components requiring enhanced surface hardness, wear resistance, and fatigue performance.
9. Bodycote announced plans to open a new heat treatment facility in Apodaca, Mexico, expanding regional capacity for case hardening and nitriding processes used in automotive, industrial, and medical components. The additional capacity is expected to support growing manufacturing activity by improving supply chain responsiveness and access to localized thermal processing services.
10. A manufacturer has ordered a vacuum furnace system from SECO/WARWICK designed to consolidate multiple heat treating processes — including quenching, tempering, and cryogenic treatment — into a single unit for small arms component production. By replacing several standalone systems with one integrated solution, the furnace streamlines thermal processing, reduces labor and equipment needs, and improves efficiency and repeatability for high-precision manufacturing in the firearms sector.
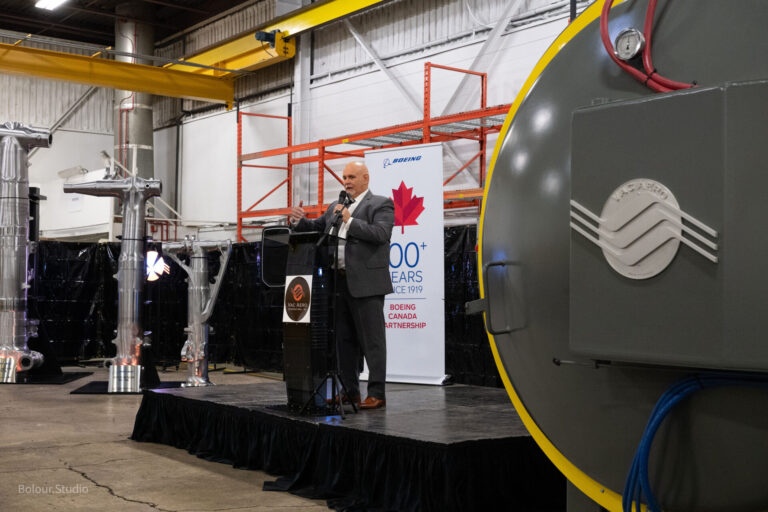
11. Boeing is adding vacuum furnace capacity at its Tube, Duct and Reservoir Center in Algona, Washington, to expand in-house heat treating capability for aerospace tube and duct assemblies. The system, supplied by Vac-Aero International, is intended to address production needs across commercial and defense aerospace programs.
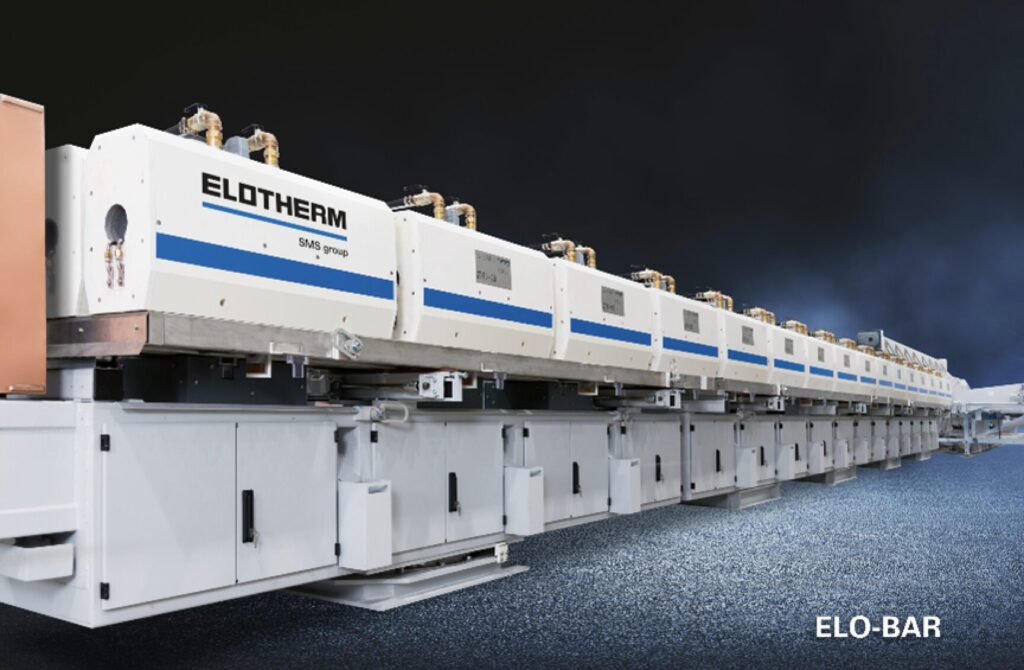
12. SMS group has received an order from Huzhou Hatebur Precision Forging Co., Ltd. to supply an SMS Elotherm induction bar heating machine for its forging operations. The system will be used to heat billets prior to forming, supporting more efficient and consistent production of precision components such as bearings and automotive parts. The investment reflects continued adoption of induction-based thermal processing to improve process control and energy efficiency in the forging industry.
13. Hirschvogel has partnered with SMS group, along with image-processing specialist Sightwise, to implement an AI-based automated inspection system for closed-die forgings at its Denklingen, Germany facility. The system replaces manual visual checks with fully automated, data-driven quality control — using robotics, high-resolution imaging, and synthetic data modeling — to improve inspection speed, reduce errors, and advance digitalization in forging production for automotive and other high-performance applications.
14. A custom vacuum induction melting (VIM) furnace has been delivered to support the controlled processing of advanced alloys, strengthening material quality for high-spec industries such as aerospace and energy. The system was supplied by SECO/WARWICK, which engineered the solution to meet specific production requirements. The technology is expected to support downstream heat treatment processes by improving alloy cleanliness, consistency, and performance.
The new lightweight monolithics production facility in FultonVIM casting system for power generation turbine manufacturingNew 10-bar vacuum furnace at Solar Atmospheres’ California facility
Kanthal’s official inauguration of its new service center in North CarolinaVector furnace order from Thai aerospace manufacturerHgen at BodycoteCustom split tube furnace by ThermcraftVacu-Braze expanding capabilities with large-capacity nitriding furnaceDave Farmery, president and COO of Vac Aero, speaking at the CP8A Poseidon ITB commitment event | Image Credit: Bolour StudioBodycote expansion in MexicoConsolidating four heat treat processes into one device3D rendering of the test stationELO-BAR induction heating machines for bar forgingSECO/WARWICK supplying a tailor-made vacuum induction furnace
Company & Personnel
15. G.S. Precision has acquired Lush Heat Treatment Ltd. and Headwater Precision, Inc., expanding its capabilities across machining, coatings, and thermal processing while extending its footprint in North America and Europe. The additions integrate heat treating and advanced manufacturing services under one platform, strengthening support for aerospace, defense, and other high-spec industries that rely on tightly controlled production of mission-critical components.
16. NUTEC Inc., a manufacturer of industrial insulation and fire protection products, has acquired ETS Schaefer LLC, a supplier of monolithic ceramic fiber insulation, expanding its capabilities in the high-temperature insulation segment. The acquisition strengthens NUTEC’s ability to support furnace and thermal processing operations with integrated insulation solutions, improving performance and efficiency for industries that rely on high-temperature environments. The company will operate as NUTEC ETS SCHAEFER under the leadership of Brian Bradley, recently named general manager of this wholly owned subsidiary of NUTEC.
17. Assan Alüminyum, through its subsidiary Kibar Americas, has acquired an aluminum foil production facility in Fairmont, West Virginia, marking its entry as a local producer in the U.S. market. The investment strengthens the company’s global footprint and improves its ability to serve North American clients with foil products for automotive, HVAC, packaging, and industrial applications, supporting more localized and resilient supply chains.
18. J.F. Lehman & Company has acquired Forged Solutions Group, a manufacturer of high-specification forgings used in aerospace, defense, and space applications. The company produces components including aeroengine discs, shafts, and structural parts from advanced alloys such as titanium, nickel-based superalloys, steel and aluminum before moving through machining and materials testing as part of the production process.
19. Linamar Corporation, a North American manufacturer with in-house heat treating capabilities, has acquired select assets of Winning BLW, strengthening its capabilities in warm forging and precision gear manufacturing for automotive and industrial applications. The acquisition supports production of bevel and helical gears, components that typically require controlled heat treating to achieve the hardness, wear resistance, and fatigue strength needed for drivetrain systems.
20. GE Aerospace has announced a $1 billion investment in its U.S. manufacturing sites and supplier base in 2026, marking its second consecutive year at that level of spending and including plans to hire 5,000 workers. The investment is aimed at accelerating jet engine production, strengthening defense manufacturing, and improving supply chain capacity, helping the aerospace sector meet rising demand for commercial and military aircraft while reinforcing U.S.-based manufacturing capabilities.
21. Solar Atmospheres has provided thermal processing services for materials and components used in NASA’s Artemis II mission, contributing to the production of critical aerospace systems. Its heat treating capabilities support high-performance materials required for extreme space environments, reinforcing reliability and precision in components essential to next-generation space exploration and the broader aerospace supply chain.
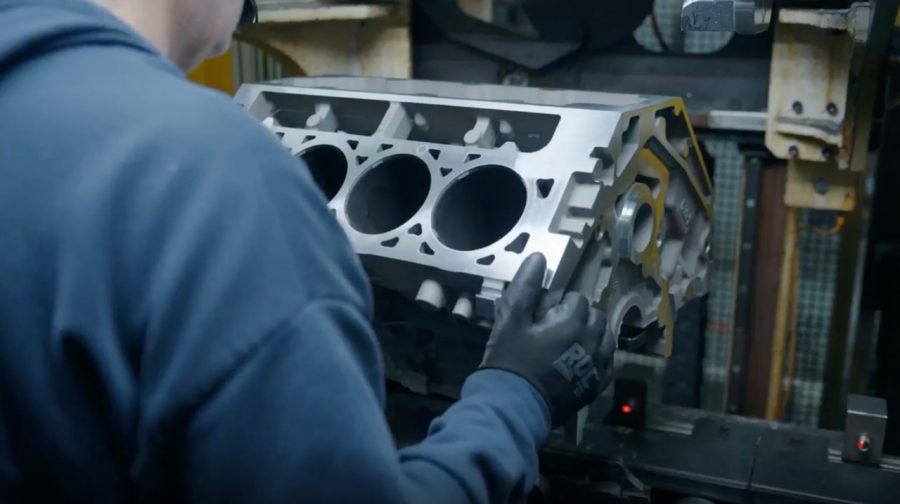
22. General Motors announced plans to invest more than $150 million in its Saginaw Metal Casting Operations facility in Michigan to support production of V8 engine blocks and cylinder heads used in full-size trucks and SUVs. The project includes new and upgraded equipment for casting and machining operations, enabling the facility to increase production capacity and maintain output for current engine programs. The Saginaw site has supplied engine components for multiple generations of GM vehicles.
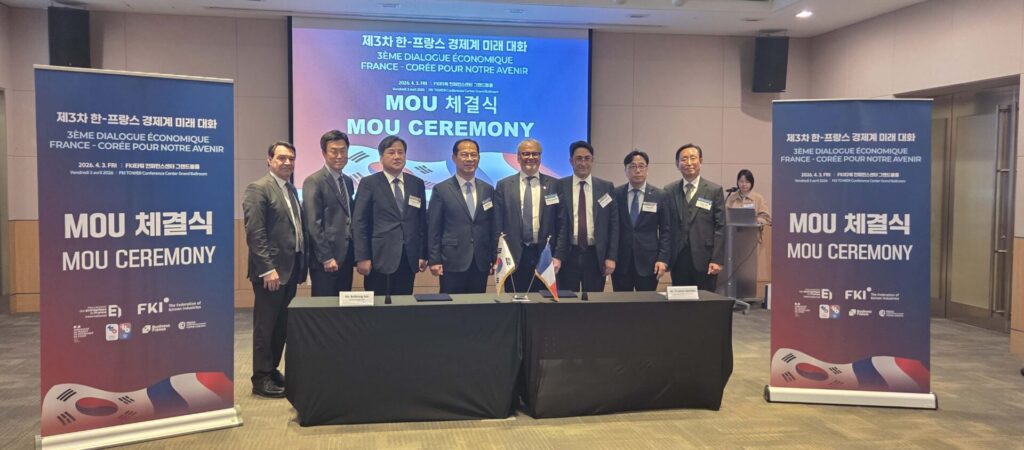
23. Hyundai Steel has signed a contract with Fives Group to supply key technologies for a new U.S.-based automotive steel production facility, advancing plans for a large-scale, electric arc furnace (EAF) mill. The project strengthens localized, low-carbon steel production for the automotive sector, improving supply chain resilience and enabling more efficient delivery of high-quality steel to U.S. vehicle manufacturing operations.
Brian Bradley, general manager of NUTEC ETS SCHAEFERThe Fairmont facilities in West VirginiaSolar Atmospheres supporting Artemis II launch
Linamar acquiring assets of Winning BLWGM’s $150-million investment in Saginaw Metal Casting Plant to support production of V8 engine blocks and cylinder headsHyundai Steel and Fives Group MOU signing ceremony in France
Kudos
24. Gamma Aerospace successfully passed their Heat Treat Nadcap audit, retaining Merit status that reflects the company’s commitment to delivering high quality products and services to their clients.
25. Aalberts surface technologies has expanded Boeing-approved heat treatment processes at its TEY facility in País Vasco, increasing its range of certified aerospace specifications and strengthening its position as a qualified supplier.
26. Aalberts surface technologies announced the renewal of their Nadcap certification for another 24 months at their Besançon facility, reflecting continuous commitment to quality, strict control of special processes, and full compliance with industry requirements.
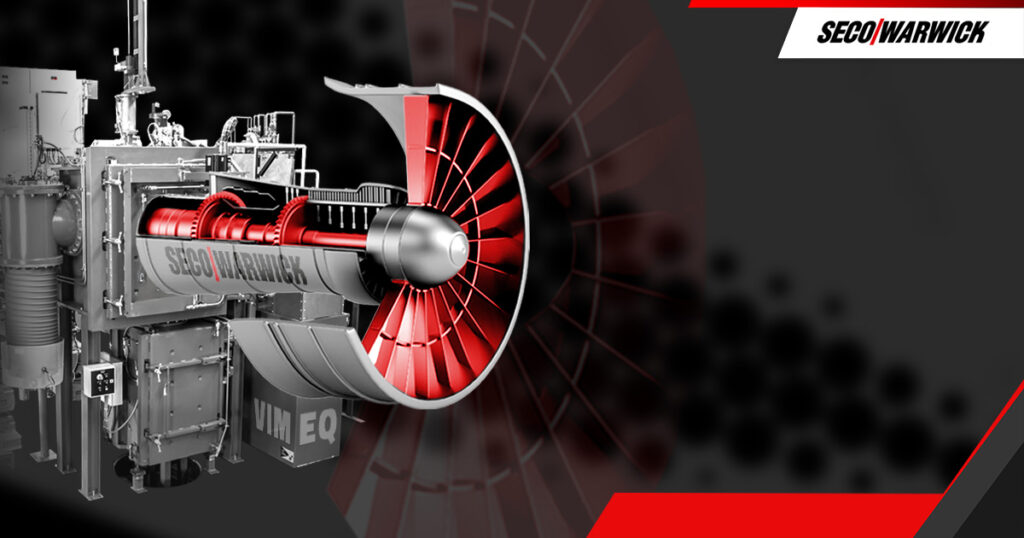
An aircraft engine manufacturer has purchased a custom-built vacuum induction melting (VIM) furnace to support the production of equiaxed (EQ) turbine blade castings for aircraft engines. The furnace enables melting in a controlled vacuum environment, with unique and intuitive control systems that help improve metallurgical consistency.
A tailor-made vacuum induction melting (VIM) furnace | Image Credit: SECO/WARWICKEarl Good Managing Director, Retech Vice President of Vacuum Metallurgy Segment, SECO/WARWICK Group
The system is a two-chamber 50 kg VIM induction furnace supplied by SECO/WARWICK, a global manufacturer of thermal processing equipment with operations in North America. It was engineered as a tailored solution with configuration and technical parameters adapted to the client’s production needs. “The furnace has a non-standard design in which the mold elevator was replaced with a special trolley that moves horizontally on rails. Thanks to this solution, the furnace fits perfectly into the available space without any impact on its performance,” said Earl Good, managing director of RETECH, a company within the SECO/WARWICK Group, and vice president of the Vacuum Metallurgy Segment at SECO/WARWICK Group.
The system includes a control platform for casting processes, temperature control, and comprehensive data acquisition, delivering the repeatability and throughput essential to the aerospace industry. Its two-chamber design and pumping system allow for continuous operation, and the furnace can be equipped with a mold heater to maintain thermal conditions for the casting mold.
The use of VIM furnaces continues across aerospace applications, where vacuum metallurgy supports the aerospace industry’s constantly changing production needs.
Press release is available in its original form here.
In this installment of Answers in the Atmosphere, David (Dave) Wolff, an independent expert focusing on industrial atmospheres for heat treat applications, examines the market realities shaping argon supply and demand.
This informative piece on argon’s sourcing and distribution landscape, safety considerations, and emerging growth drivers — from U.S. titanium refining and powder metallurgy to the reshoring of domestic steel production —was first released in Heat Treat Today’sMarch 2026 Annual Aerospace Heat Treating print edition.
Akin Malas Business Development Manager / Metallurgist Linde
If you are just beginning to read this column, welcome. I encourage you to read the February 2026 installment to have a better understanding of the attributes of argon as an industrial gas for the thermal processing industry. Akin Malas, business development manager and metallurgist at Linde, joins me in this foray into argon, and we’re exploring market realities in this installment.
Though many companies compete for market share in the supply of gases such as nitrogen, oxygen, and hydrogen because they are relatively less expensive to source and process, the number of companies that have sufficient scale and expertise to produce and market argon is generally considered to be limited to the top tier of industrial gas companies like Linde, Air Liquide/Airgas, Air Products, Matheson, and Messer. Many other companies operate ASUs; however, very few of the plants are large enough to separate and purify argon. In the case of some ASUs owned and operated by very large steel mills, they generally sell their crude argon to industrial gas suppliers for purification and subsequent marketing and sales.
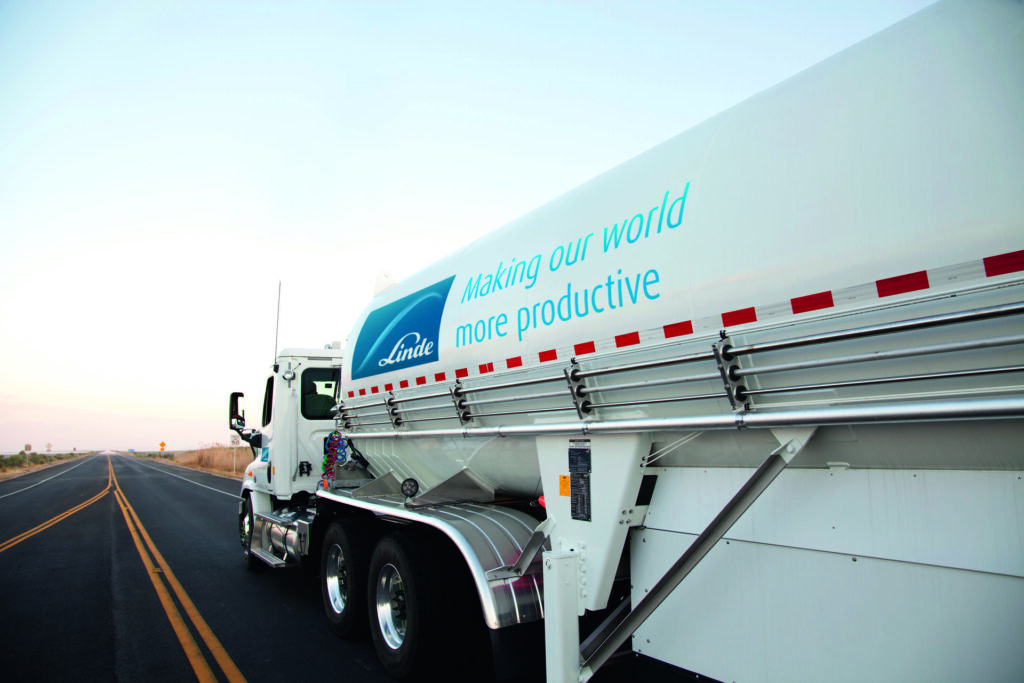
Linde gas delivery truck | Image Credit: Linde
Argon is delivered as a liquid cryogenic product (LAR), like liquid nitrogen (LIN), or liquid oxygen (LOX), but there may be differences in the storage and dispensing equipment installed at a client’s site due to the variety of uses for argon. Certain high-volume applications, such as ladle stirring and metals atomization, may require substantially higher pressure than normal cryogenic tanks are set up to store, making the use of boosters or cryogenic pumps necessary. If your application requires argon pressure to be above 100 psig, make sure that you are talking to a supplier that is experienced in providing and maintaining the equipment needed for your process.
From an NFPA codes standpoint, argon storage is comparable to nitrogen storage, and the clearances in NFPA 55 are the same for argon and nitrogen. But there are some key points to consider as far as safety in use:
While all cryogenic gases will create a vapor cloud that hugs the ground if there is a release, the clouds from nitrogen and oxygen will disperse and rise relatively rapidly as the gas warms. But because argon has much higher density than oxygen and nitrogen, a release will tend to hug the ground and can create a serious oxygen deficient atmosphere issue in low spots. Users of pit furnaces with argon need to be particularly aware of the unique characteristics of argon.
Because argon is generally shipped much longer distances than oxygen or nitrogen, tanks tend to be larger sized so that more can be delivered in a single visit. Since the transportation element of the price is considerable, keep in mind that your tank size (and NFPA clearance calculations) may be different than is typical for nitrogen.
While argon cannot be cost-effectively produced from air by non-cryogenic generation techniques (like membrane and PSA techniques used for nitrogen and oxygen), argon recovery/recycling is possible from argon-based industrial streams. A few of the larger industrial gas providers can provide recycling equipment that uses cryogenic separation technology to re-create very high purity argon from argon-rich offgas streams. Note that these installations are relatively expensive and specialized and are generally only of interest to the largest argon consumers.
After many years of relatively modest growth in the consumption of argon, several market segments are driving potentially important growth in argon use:
Several companies are developing U.S.-based titanium refining capabilities. Argon is required for processing and refining titanium metal, and the U.S. titanium production may become an important consumption driver.
Virtually all atomization of the special metals for powder metallurgical applications currently is done with argon used as the atomization gas. Though cheaper water-based atomization is being developed, it is not yet suitable for high quality powders. The metals powder industry has experienced strong growth and continues to grow.
The U.S. is reshoring iron and steel production, meaning that argon use for ladle stirring will rise. This means that overall argon use will rise, and that some new argon-capable ASU capacity will be built to serve the needs of new and refurbished steel plants.
Akin and I hope that these last two column installments have helped readers understand the factors in the market for argon that make it different in several ways from the more familiar nitrogen/oxygen marketplace.
About The Author:
David (Dave) Wolff Industrial Gas Professional Wolff Engineering
Dave Wolff has over 40 years of project engineering, industrial gas generation and application engineering, marketing, and sales experience. Dave holds a degree in engineering science from Dartmouth College. Currently, he consults in the areas of industrial gas and chemical new product development and commercial introduction, as well as market development and selling practices.
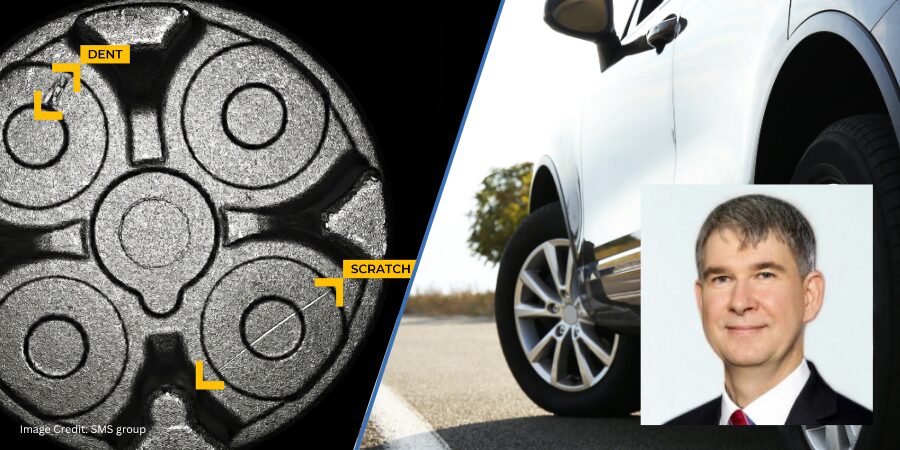
Hirschvogel is implementing automated inspection of closed-die forgings to replace manual visual checks, enabling faster detection of surface defects and dimensional deviations in automotive components. The approach supports more consistent quality outcomes in forged parts while reducing error rates and scrap in high-volume production environments.
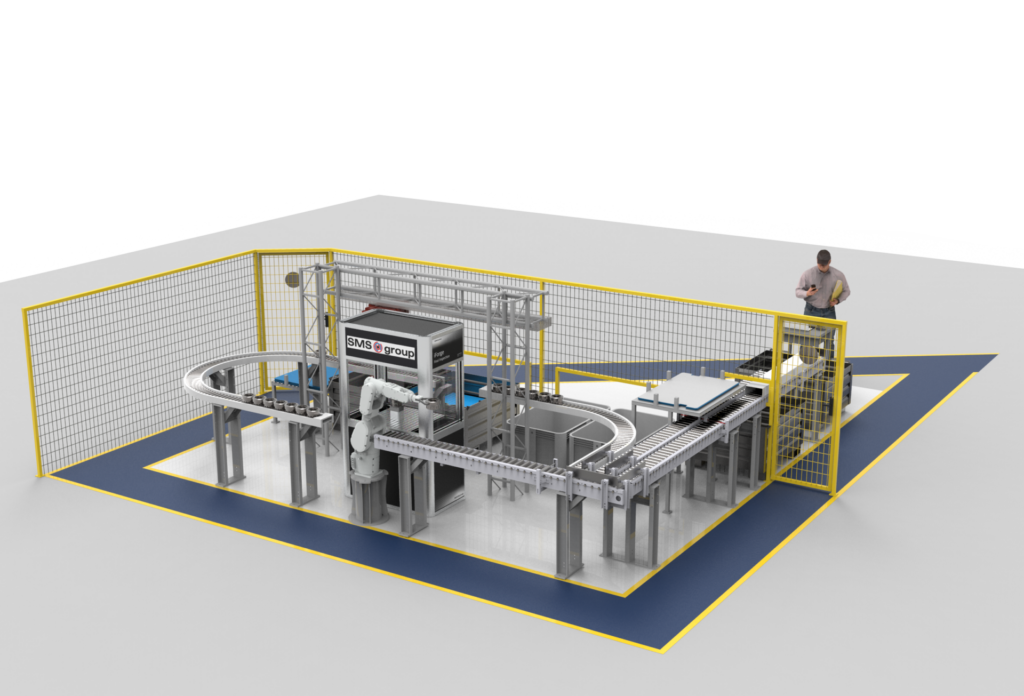
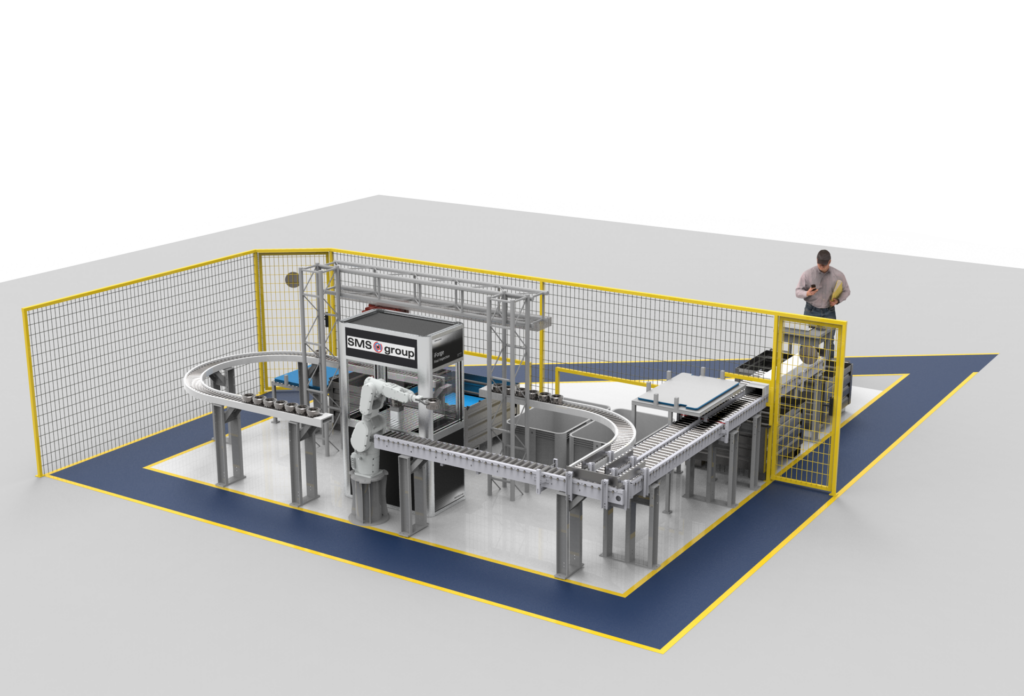
Working in partnership with SMS group, a global supplier of materials industry technology with North American headquarters in Pittsburgh, Pennsylvania, Hirschvogel, a global automotive supplier specializing in solid metal forming, has deployed an automated final inspection system for closed-die-forged components at its Denklingen, Germany, facility. The system replaces an existing manual testing station with a fully digital process designed to evaluate each component in seconds.
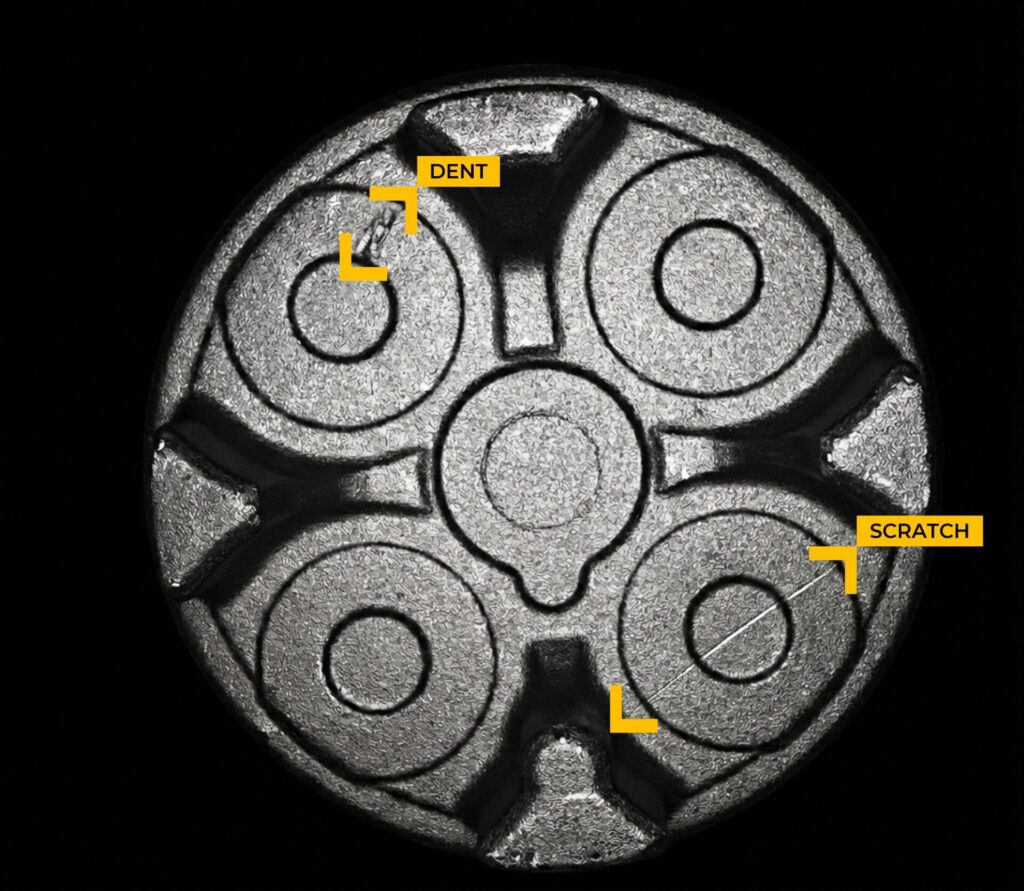
3D rendering of the test station: Visualization of the automated final inspection for closed-die-forged automotive components. | Image Credit: SMS groupThe automated final inspection allows various types of closed-die forging defects to be identified and categorized (example shown). | Image Credit: SMS group
The inspection solution integrates automated handling and high-resolution imaging to assess surface conditions and geometry. A robot moves forgings directly from transport containers, while camera sensors capture images that are analyzed in fractions of a second. Detected defects are classified against a digital catalog, reducing the likelihoos of misclassification and minimizing pseudo-scrap, or the disposal of acceptable parts.
The system was developed in cooperation with image processing specialist Sightwise as well. As part of SMS group’s iForge digitalization platform, the inspection is designed to integrate into forging production lines and support automated quality assurance workflows.
Axel Rossbach Forging Technology Expert SMS group
A key feature of the system is its use of synthetic training data to develop inspection models. Instead of relying on physical samples of defective parts, the system uses CAD and 3D model data to simulate material properties, surface textures, and defect types. This allows analysis models to be prepared within hours rather than weeks.
“The new system enables us to speed up the final inspection significantly and ensure maximum process stability in the line itself,” said Axel Rossbach, forging technology expert at SMS group. The scalable system can also be adapted to new product variants, supporting production flexibility in automotive forging operations.
Press release is available in its original form here.
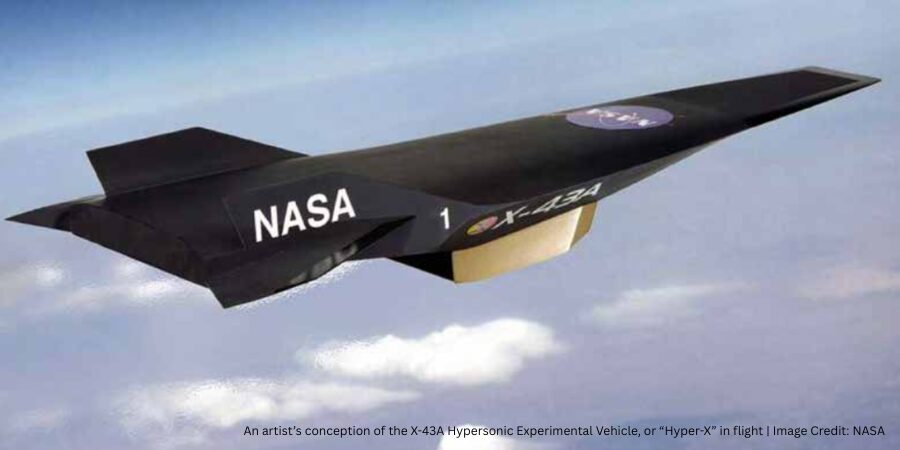
Hypersonic vehicles and missiles operating at Mach 5 and beyond place unprecedented thermal and environmental demands on aerospace materials. In this Technical Tuesday installment, Scott Robinson, product manager of ceramics and powder metallurgy at Centorr Vacuum Industries, examines how vacuum and controlled-atmosphere furnaces support the research, prototyping, and production of ultrahigh-temperature ceramics, carbon–carbon composites, and other advanced materials used in hypersonic applications.
This informative piece was first released in Heat Treat Today’sMarch 2026 Annual Aerospace Heat Treating print edition.
Introduction
Hypersonic missiles and vehicles are an emerging class of aerospace technology that is developing rapidly toward active use in military and potentially commercial applications. These machines can achieve sustained speeds of Mach 5 or greater within the Earth’s atmosphere (i.e., at altitudes below about 90 km). While conventional intercontinental ballistic missiles can also achieve hypersonic speeds during atmospheric reentry, they follow a high-arching ballistic trajectory with limited maneuverability, in contrast to the real-time in-flight maneuverability offered by hypersonic systems. As such, military actors prefer hypersonic missiles for precision strikes (Mesa 2024), while in the commercial realm, airliners are excited by the possibility of drastically shortened journey durations with hypersonic vehicles (TomorrowDesk 2025).
Because hypersonic missiles and vehicles move at extreme speeds within Earth’s atmosphere, they are subject to significant atmospheric compression and friction effects (Smith 2021). These effects result in considerable aerodynamic heating of the leading edges, nose tips, and exhaust-washed structures, from 1800°C (3200°F) to more than 3000°C (5400°F).
Traditional aerospace materials such as aluminum, stainless steel, and titanium cannot be used at these elevated temperatures without thermal protection engineering. In contrast, an emerging portfolio of materials including refractory metals, carbon-carbon composites, ultrahigh-temperature ceramics (UHTCs), and ceramic matrix composites (CMCs) can more easily deal with this extreme heat.
UHTCs and CMC materials typically are composed of metal carbides, borides, and nitrides, which means they are traditionally processed at very high temperatures. Currently, the leading candidate materials are silicon carbide (melting/decomposition point: 2730°C, or 4945°F) and zirconium diboride (melting point: ~3246°C, or 5875°F) due in part to their reasonable raw material costs.
Processing of UHTCs, CMCs, and other advanced materials for aerospace applications includes one or more of the following high-temperature processing steps, often using vacuum and controlled atmosphere furnace technology:
Chemical vapor infiltration
Chemical vapor deposition
High-temperature sintering
Graphitization
Silicon melt infiltration of carbon-carbon composites
Each stage of the product development cycle — from laboratory-scale research and development to prototype development to production-scale manufacturing — requires a portfolio of specialized furnaces to achieve the goals of each stage.
This article takes a closer look at the types of furnace solutions available to develop, process, and commercialize these high-performance materials.
Laboratory-Scale Research and Development
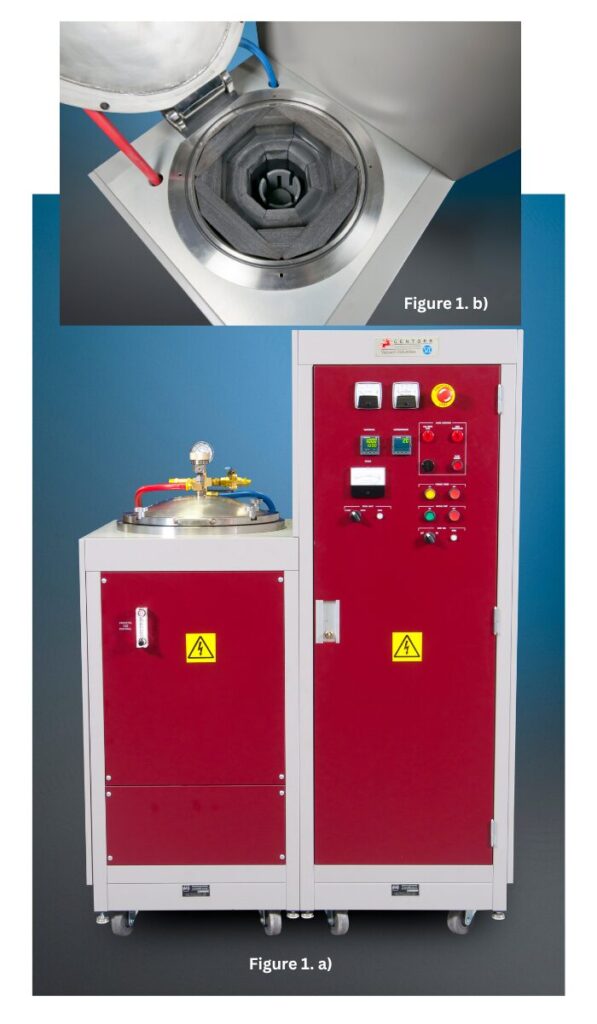
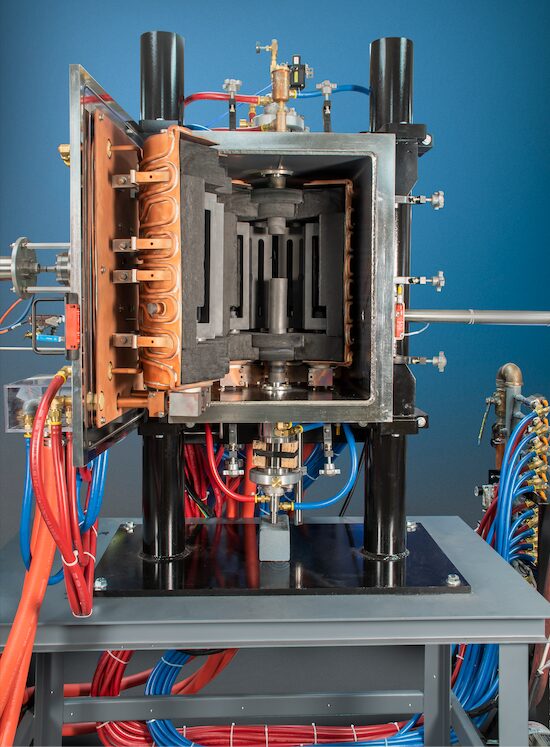
Figure 1. a) Centorr Vacuum Industries’ LF 3000°C (5400°F) graphite vacuum furnace and b) top view of hot zone; 3” x 4” (75 x 100 mm; Ø x h) hot zone. | Image Credit: Centorr Vacuum Industries
Laboratory-scale R&D activities focus mostly on the development, fabrication, and testing of small-scale parts, which require a small, adaptable furnace.
The LF graphite vacuum furnace is an example of the type of furnaces needed for small-scale parts (Figure 1). First designed in 2012, it is a robust, low-cost development furnace with temperature capability up to 3000°C (5400°F) in vacuum or inert gas. This temperature range covers most hypersonic, UHTC, and other applications. For example, current users fit the small 3″ x 4″ (75 x 100 mm; Ø x h) hot zone with small graphite crucibles to fire graphite-based powders for applications in battery and electric vehicle technology.
In another case, Dalhousie University in Nova Scotia, Canada, a research-based university, modified the base LF system by adding a small binder/off-gassing trap and positive pressure exhaust tower for processing of non-oxide ceramics produced by additive manufacturing. These samples include silicon-based ceramics (silicon carbide and silicon nitride), high-entropy ceramics, and cermet systems.
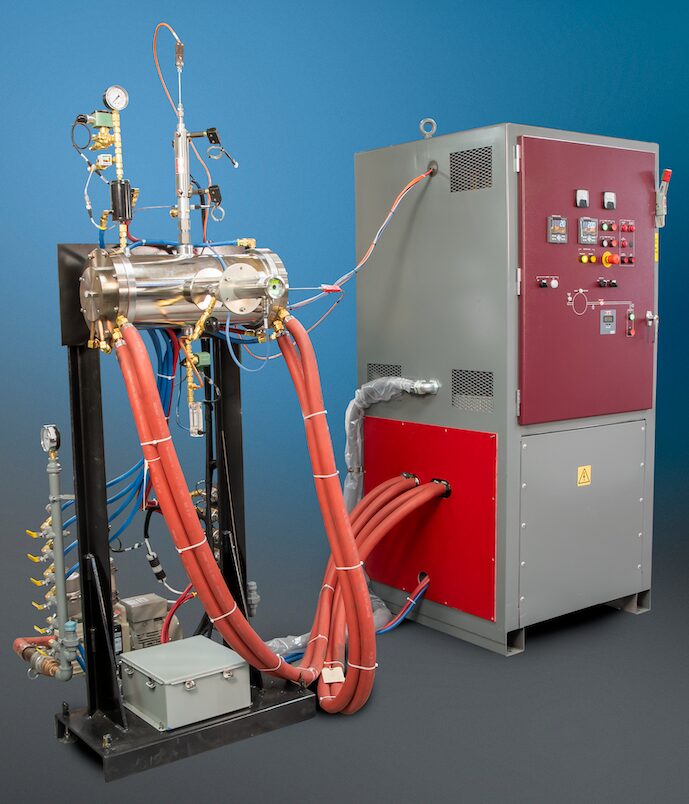
Subsequent laboratory applications require a larger hot zone furnace for processing bigger samples. One example of this type of furnace is the Series 10 graphite tube furnace (Figure 2). This tube furnace is based on a more than 50-year-old furnace design, although the traditional alumina or quartz tube has since been replaced with a solid graphite tube. Operating in vacuum or partial/positive pressures of argon, R&D centers use this furnace to process carbon powder formulations to maximize the percent conversion to graphite, as not all carbon-based starting materials will convert to crystalline graphite.
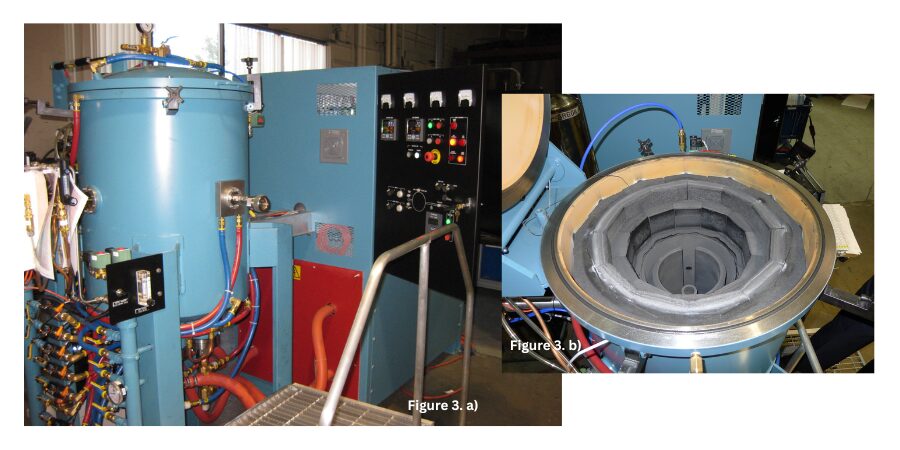
Figure 2. Series 10 3000°C (5400°F) graphite tube furnace; 4″ x 16″ (100 mm x 400 mm) hot zone diameter and height. Image Credit: Centorr Vacuum Industries Figure 3. a) Series 45 graphite top-loading furnace and b) top view of hot zone. Used for carbon/graphite work, this model offers a larger useable firing footprint at higher temperatures than the Series 10 furnace. The hot zone diameter and height dimensions approximate 6″ x 6″ (150 mm x 150 mm), and temperature is rated for 3200°C (5790°F). | Image Credit: Centorr Vacuum Industries
As R&D activities begin to focus on particular material compositions, larger furnaces are needed to synthesize meaningful sizes and quantities of candidate materials prior to scaling up for manufacture, like the Series 45 graphite top-loading furnace (Figure 3).
Characterization and Prototyping Stage
Figure 4. Front view of the Series TT Testorr graphite hot zone rated for 2700°C (4890°F) processing temperatures | Image Credit: Centorr Vacuum Industries
Once the final candidate materials are processed, aerospace design engineers need to test meaningfully sized samples of the materials at high temperature under mechanical loading. It is best to have a furnace that can be combined with mechanical test stands to take measurements of mechanical properties. This is the case for Wichita State University’s National Institute for Aviation Research, which leverages multiple Testorr® furnace units to measure tension, compression, and shear properties of ceramic matrix composites, refractory metals, and other materials at high temperature. Rated for temperatures up to 2700°C (4890°F) in vacuum or inert gas, the furnace can better simulate some aspects of hypersonic service environments (Figure 4).
An important task of the R&D and prototyping stages is to work out processing parameters that will be translated to production-scale manufacturing processes. For example, simple carbon structures will react with air during reentry and suffer damaging effects at temperatures as low as 500°C (930°F). Therefore, any carbon-carbon materials or solid carbon shapes used in hypersonic applications must be protected with advanced ceramic coatings for durability and oxidation resistance.
Chemical vapor deposition is one such coating deposition process, and one of the most popular protective coatings is silicon carbide. The coating is deposited on substrate parts by flowing hydrogen gas through a bubbler of liquid methyltrichlorosilane (MTS; CH3SiCl3) gas. Newer systems use a heated evaporator to vaporize the MTS liquid in a hydrogen carrier gas stream. The combination of hydrogen and MTS is introduced at partial pressures into the furnace hot zone inside a graphite retort, where the gases “crack” or decompose, depositing microns-thick coatings of silicon carbide onto the part’s surface.
Production Stage
Once the advanced materials are properly characterized and prototyped, it is time to look at equipment for full-scale production manufacturing. The furnace configurations for these processes can be conventional front-loading designs or may be oriented in vertical top- or bottom-loading designs for floor space savings and gas flow dynamics.
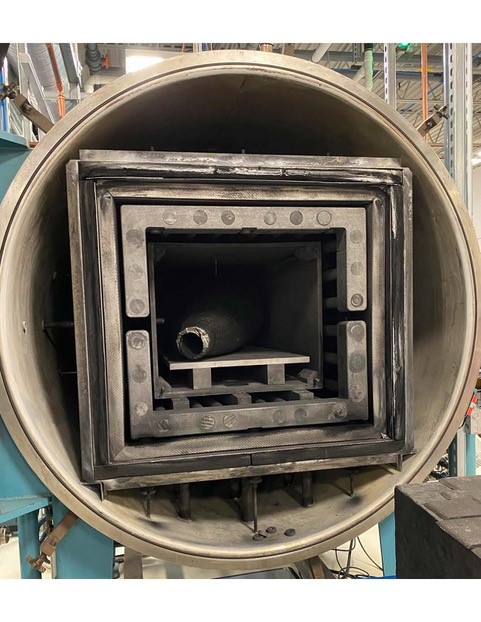
The Sintervac® front-loading graphite furnace (Figure 5) has integral graphite retort and dual gas flow to the main chamber and retort. These furnace systems include durable rotary piston pumping systems with inline binder traps and particulate filters to protect the pumping systems from damage from abrasive ceramic particulates. The internal graphite retort compartmentalizes the off-gassing that takes place and prevents it from escaping into the hot zone, where the oxide byproducts can attack and degrade the graphite heating elements and rigid graphite board insulation.
One common application for this type of furnace is melt infiltration of carbon-carbon composites to improve the physical properties and oxidation resistance of the composite. When processed in partial pressures (or even at positive pressures) of argon, silicon will melt at approximately 1450°C (2640°F). The silicon liquid and vapor infiltrate into the void spaces of the porous carbon-carbon composite via capillary action. The infiltrated silicon reacts with the free carbon in the carbon-carbon fiber structure, forming a silicon carbide matrix around the carbon-carbon fiber structure.
Firms like Exothermics (Amherst, NH) use this process for missile and aerospace applications. The silicon carbide matrix structure provides an environmental barrier to oxidation during reentry into Earth’s atmosphere and improves the matrix’s temperature performance to approximately 1600°C (2910°F) in air.
Smaller production units were also developed for carbon-carbon work at temperatures from 2450°C and 2600°C (4440°F and 4710°F). The addition of dedicated water-cooled filtration traps and 10-μ particulate filters helps deal with the heavy off-gassing expected from processing of carbon-carbon materials.
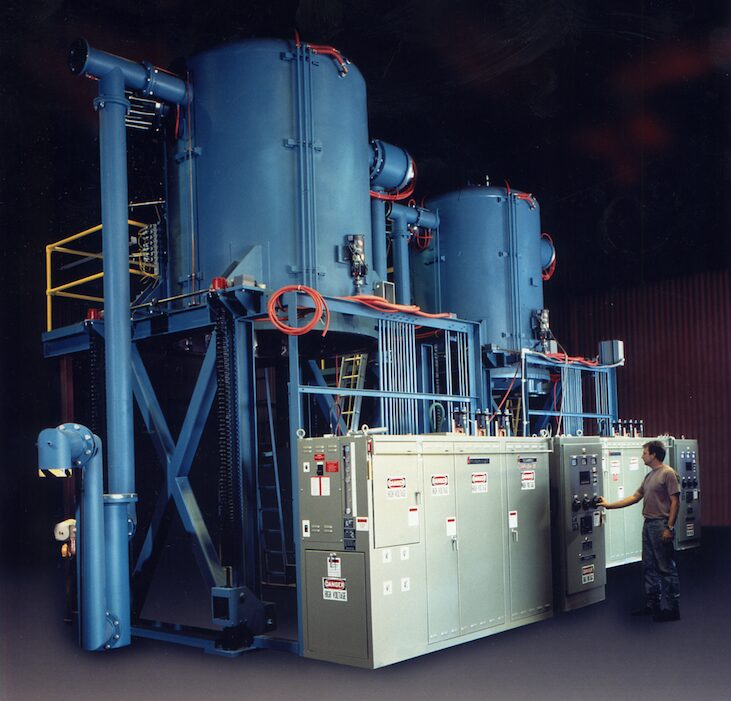
In contrast to melt infiltration, chemical vapor infiltration drives gaseous reactants into the porous matrix where the gas reacts with the porous structure to form a dense matrix. The chemical vapor infiltration process is used to fabricate larger parts for hypersonic applications, such as rocket motors and missile components, and carbon-carbon aircraft brakes. Vertical top- and bottom-loading chemical vapor infiltration units like the example in Figure 6 can be used for these types of applications.
Figure 6. Series 4300 vacuum furnace for chemical vapor infiltration and graphitization. The furnace may be built in a top-loading or bottom-loading configuration; the unit scales from 52″ to 80″ (1,320 mm to 2,000 mm) in diameter and heights from 80″ up to 120″ (2.0 to 3.0 meters). | Image Credit: Centorr Vacuum Industries
In the chemical vapor infiltration process, gases, including hydrogen, methane, and propane, are fed into the furnace chamber at high flow rates and at temperatures approaching 1000°C–1100°C (1830°F–2010°F). The methane and propane gases break down and deposit carbon deep into the matrix of the carbon-carbon fibrous parts. These cycles can be very long, approaching seven to ten days, for the material to fully densify, and multiple cycles are usually necessary.
Low operating pressures require extremely large mechanical pumping systems with large vacuum blowers or boosters. These furnaces include water-cooled “tar” traps (with a heated stripping system) and large Dollinger particulate filters for handling the resin off-gas byproducts.
These furnaces are almost always induction heated, using multizone induction coils and large, thick-wall graphite susceptors for optimal temperature uniformity. The insulation design uses carbon black powder, which is economical and highly efficient for temperature reduction.
While more conventional rigid or flexible graphite board or felt materials can be used, Centorr’s experience has shown that the degree of infiltration of carbon resins over time will affect the density and porosity of the insulation pack (as it does the load material), causing degradation and densification of the insulation. The denser insulation results in high coil water temperatures, which compromises hot zone life. Specialized carbon black installation and removal equipment is required by the end-user to maintain the insulation efficiency of the furnace hot zone. Because gas flow in the furnace is critically important, special diffusor plates or plenums are used to uniformly direct gas flow across the entire geometry of the parts.
Once the advanced materials undergo chemical vapor infiltration, they are still composed of a carbon base material, which needs to be converted to a more orderly crystalline graphite structure to impart the durability and strength required in aerospace applications. To accomplish this conversion, the material needs to be heated at temperatures greater than 2300°C (4170°F), a process called graphitization.
The graphitization process employs similar furnace designs to the chemical vapor infiltration process, but the induction heating power supply is changed to the more conventional single zone coil, and the vacuum pumping systems are smaller with no tar traps needed. Load sizes of 3,000–5,000 lb. (1,360–2,268 kgs) are possible. Both the smaller and larger chemical vapor infiltration and graphitization units have large, water-cooled heat exchangers inline with large cooling fans, which reduce cooling times from ten or more days to less than 175 hours.
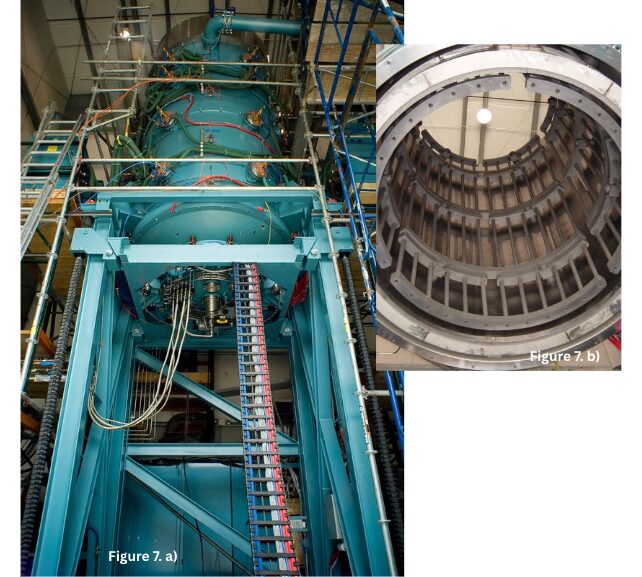
Figure 7. a) Series 3800 bottom-loading silicon carbide chemical vapor deposition furnace. b) Series 3800 chemical vapor deposition furnace hot zone with multizone control; 53″ diameter x 83″ height (1,350 mm x 2,108 mm) graphite hot zone furnace rated for 1600°C (2910°F) operation. | Image Credit: Centorr Vacuum Industries
A smaller graphitization unit was also developed in a 30″ diameter x 40″ height (76 mm x 1,000 mm) size rated to 2900°C (5250°F) maximum temperature in a vertical bottom-loading configuration for processing smaller parts in lower volumes for aerospace brakes.
The silicon carbide chemical vapor deposition units for laboratory applications discussed previously are also needed for production-size volumes (Figure 7). Due to tight temperature uniformity requirements, these units are multizone control with graphite hot zones constructed of rigid graphite board for process durability. The pumping systems can be either “dry” or “liquid ring” designs for processing the acidic off-gas materials. A post-exhaust chemical scrubber system is required to safely neutralize the hydrogen chloride off-gases.
Enabling the Next Generation of Aerospace Materials
The difficult design requirements of next-generation aerospace technologies will continue to push the existing limits of material performance. As characterization and development of new materials will be critical to the success of these aerospace programs, vacuum and controlled atmosphere furnaces will play an essential role in the production of such materials.
References
American Elements. n.d.a “Silicon Carbide Data Sheet.” https://www.americanelements.com/silicon-carbide-409-21-2.
American Elements. n.d.b “Zirconium Diboride Data Sheet.” https://www.americanelements.com/zirconium-diboride-12045-64-6.
Mesa, J. 2024. “What’s the Difference Between a Hypersonic Missile and ICBM?” Newsweek, November 21, 2024. https://www.newsweek.com/difference-between-icbm-irbm-missiles-1989780.
Smith, C. R. 2021. “Aerodynamic Heating in Hypersonic Flows.” Physics Today 74 (11): 66–67.
TomorrowDesk. 2025. “Hyperian Aerospace and the Dawn of Hypersonic Flight.” TomorrowDesk, March 29, 2025. https://tomorrowdesk.com/evolution/hyperian-aerospace-hypersonic-flight.
Heat Treat Todaythanks the American Ceramic Society for allowing us to print this piece. This article was originally published in ACerS Bulletin, September 2025.
About The Author:
Scott K. Robinson Product Manager of Ceramics and Powder Metallurgy Centorr Vacuum Industries
Scott K. Robinson is product manager of ceramics and powder metallurgy at Centorr Vacuum Industries (Nashua, NH).
Heat Treat Today has gathered the four heat treat industry-specific economic indicators for April 2026. The results suggest continued forward-looking stability compared to the March 2026 predictions.
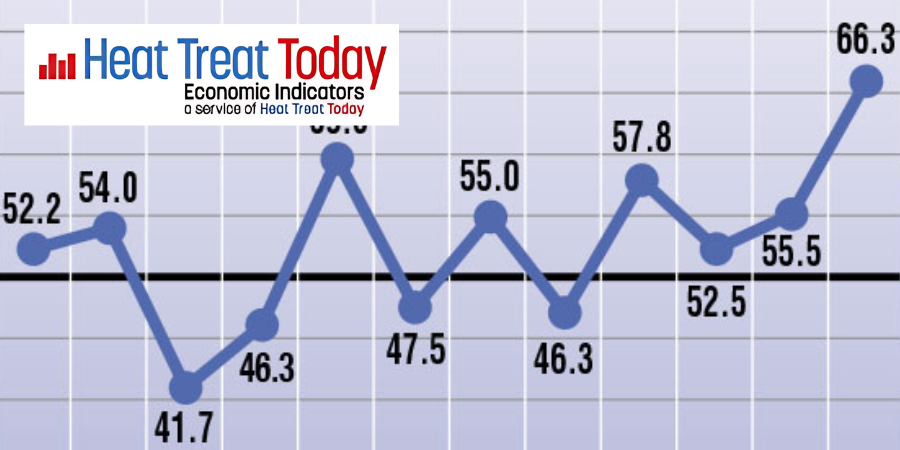
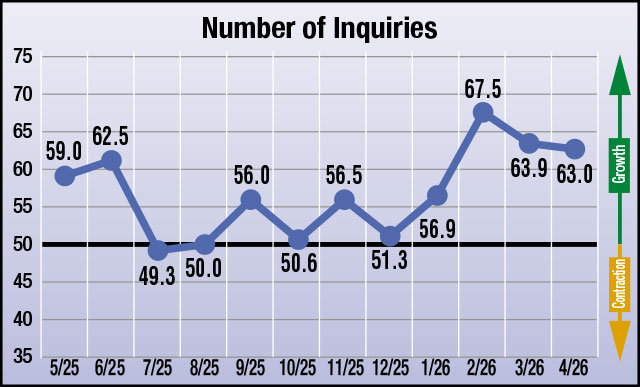
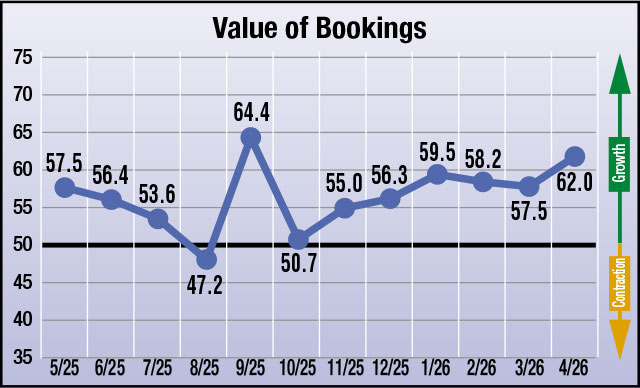
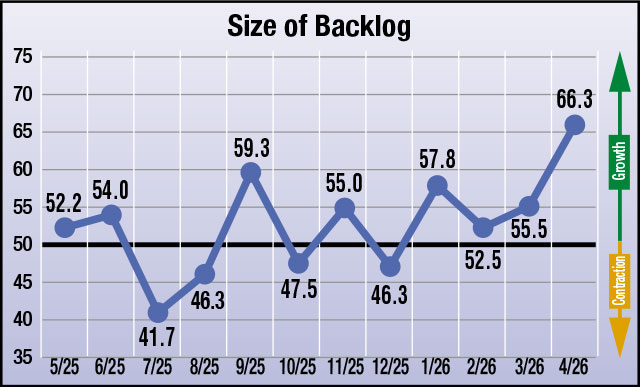
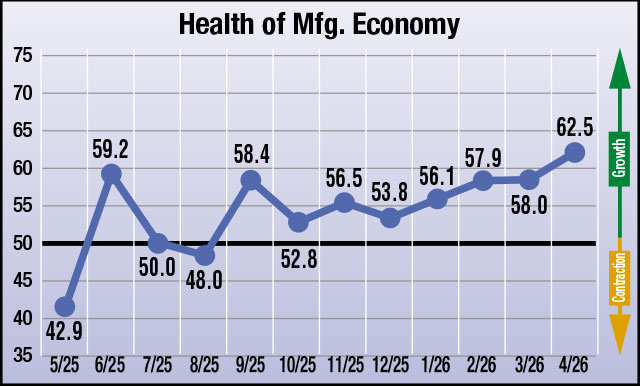
April’s data points to anticipated continued growth across the heat treat industry, as all four indices remain above the growth threshold. Inquiries are projected to remain strong at 63.0 (from 63.9 in March). Bookings are expected to strengthen to 62.0 (up from 57.5 in March). The Backlog index forecasts a notable increase to 66.3 (up from 55.5 in March). Meanwhile, the Health of the Manufacturing Economy index points to a more confident outlook at 62.5 (up from 58.0 in March).
April’s indicators suggest suppliers to the heat treat industry anticipate steady-to-strengthening demand conditions in the month ahead, with particular momentum in backlog and bookings supporting operational continuity. With all four metrics projected to remain comfortably in growth territory, the outlook reflects a manufacturing environment where suppliers can expect continued activity from heat treaters, supported by improving confidence and sustained demand across key markets as the second quarter begins.
The results from this month’s survey (April) are as follows: numbers above 50 indicate growth, numbers below 50 indicate contraction, and the number 50 indicates no change:
Anticipated change in Number of Inquiries from March to April: 63.0
Anticipated change in Value of Bookings from March to April: 62.0
Anticipated change in Size of Backlog from March to April: 66.3
Anticipated change in Health of the Manufacturing Economy from February to March: 62.5
Data for April 2026
The four index numbers are reported monthly by Heat Treat Today and made available on the website.
Heat TreatToday’sEconomic Indicatorsmeasure and report on four heat treat industry indices. Each month, approximately 800 individuals who classify themselves as suppliers to the North American heat treat industry receive the survey. Above are the results. Data collection began in June 2023. If you would like to participate in the monthly survey, please click here to subscribe.