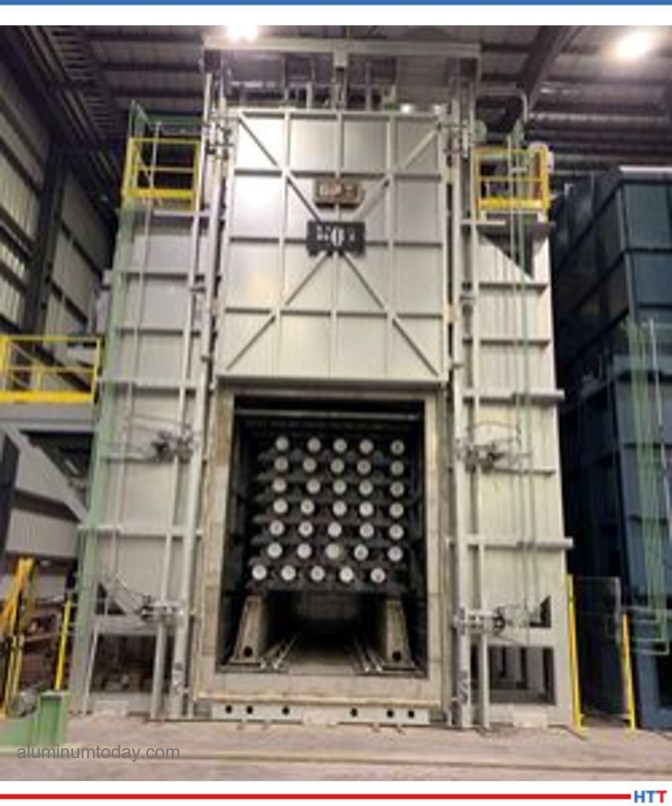
Sometimes our editors find items that are not exactly "heat treat" but do deal with interesting developments in one of our key markets: aerospace, automotive, medical, energy, or general manufacturing. To celebrate getting to the "fringe" of the weekend, Heat Treat Today presents today’s Heat TreatFringe Fridaybest of the web article discussing how to sell amidst global shortages.
We all remember the great toilet paper shortage of 2021, but supply chain issues have created shortages in other areas as well. How can manufacturers sell when warehouses may be empty and jobs may be on hold due to parts stuck somewhere in the supply chain? This video gives practical tips for how to sell to clients no matter where they are in the supply chain.
An excerpt:
"For one, companies should focus on being nimble, and that could mean adapting their sales strategy to the current circumstances. Creating promotions around goods that are readily available can help move customers over, but for those who are committed to a certain product, incentivizing or rewarding their patience can keep them from jumping ship while they wait."
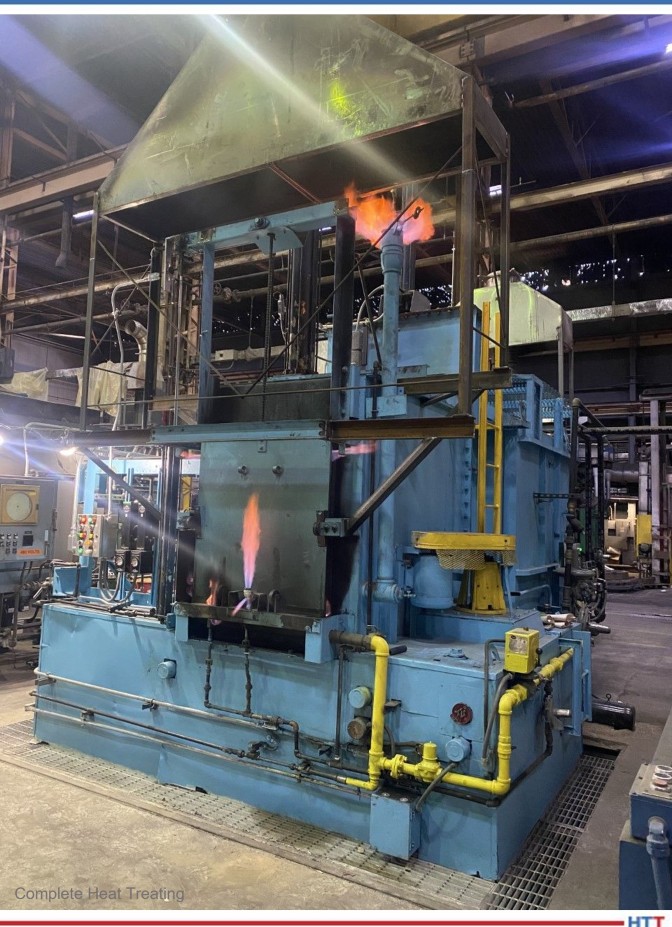
A company which has served construction, mining, and earth moving, but which is now involved in gas, power generation, military, aerospace, and more is Complete Heat Treating — this month’s MTI Member Profile company. They have many value-added operations under one roof combined with knowledgeable technical staff helping to select the optimum process to meet customer expectations.
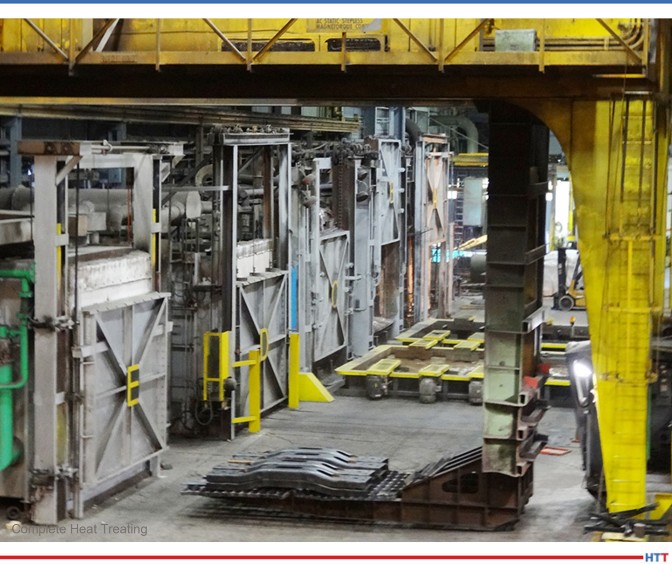
Complete Heat Treating was established in 2007 and has since acquired an additional two companies, increasing the company’s capabilities and markets. In 2011, they acquired Wisconsin Steel Industries, which was in operation since 1939. In 2018, they then acquired Commercial Heat Treat. After the acquisition in 2011, major rigging projects were undertaken to move furnaces, presses, and
other equipment to the present-day site in Milwaukee. One of the largest items moved was a large 53-foot car-bottom furnace.
A few of the company’s services include those in heat treating, blasting, coating,
straightening, and hardening. Heat treating capabilities encompass a wide variety of applications and part sizes. They offer stress relieving, annealing, quenching, tempering, and normalizing of parts up to 53’ long x 18’ wide x 15’ high and weighing up to 100,000 lbs. Open fire furnaces are available in multiple sizes and can reach up to 2200°F with heat outputs of 40,000,000 BTUs. In addition to having metallurgists on staff, other services offered are abrasive grit blasting, oil preserve coating, close tolerance straightening, and portable hardness testers.
Although all processes are important, control of the furnaces with properly calibrated pyrometry is critical to achieving quality specifications. The ability to successfully process the extreme size, shape, complexity, alloys, and quantity of parts is a unique feature of the company. They commonly heat treat large, heavy-section (10–20 ton) plates; 5,000+ tiny stampings weighing ounces; and finish machined precision parts with close tolerances. They can anneal, carburize, flame harden, straighten, blast—all to one part!
An interesting heat treat project is Complete’s involvement with large castings for the Space Launch System (SLS) for booster rockets. These were highly complex parts with a book of quality requirements.
They achieved the large heavy section mechanical property requirements and multiple hardness measurements to encompass the extremities of parts because of their procedural development that reviewed quenchant agitation direction and severity. Another interesting project involvement is the first
high-speed train in the U.S. It is a highly complex part consisting of castings, forgings, and plates with challenging quality requirements. The success of the lengthy procedural development made it memorable.
The company looks ahead to more memorable projects as new developments emerge, which include the commissioning of an integral-quench carburizing furnace and heat-treating aluminum components, and further expansion of flame hardening capability. Complete is best known for its diverse capabilities in both process and size of parts, but the quality of the 24-person workforce, their experience, technical competence, and honesty are the traits of which the company is proudest.
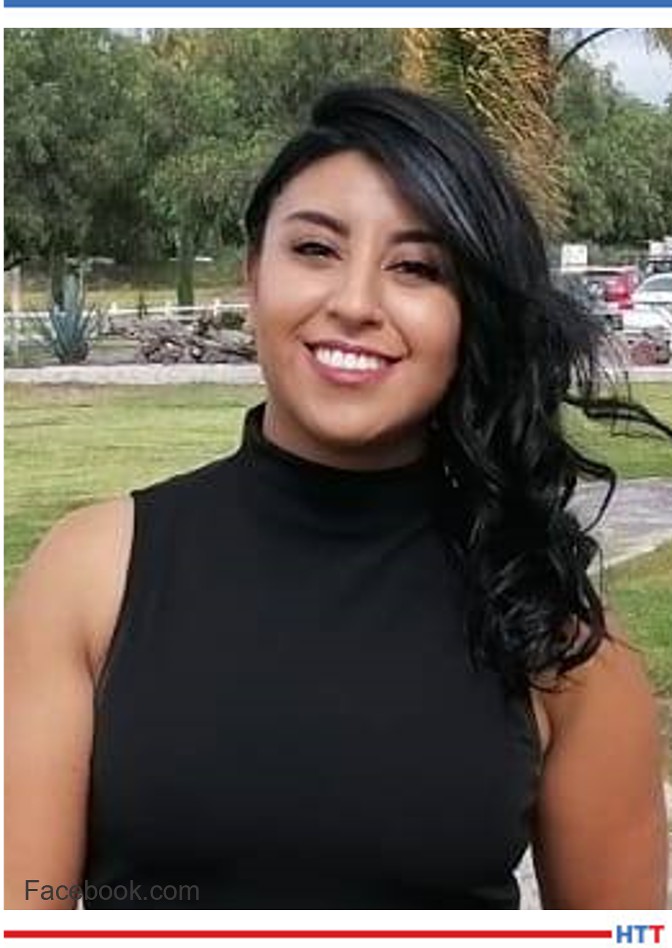
Karla Sarabia Plant Manager Watlow Electric Manufacturing Company
Watlow Electric Manufacturing Company, a North American manufacturer of industrial heaters, sensors, and controllers, will receive a high-vacuum furnace and auxiliaries for annealing thermocouple wires between every drawing stage.
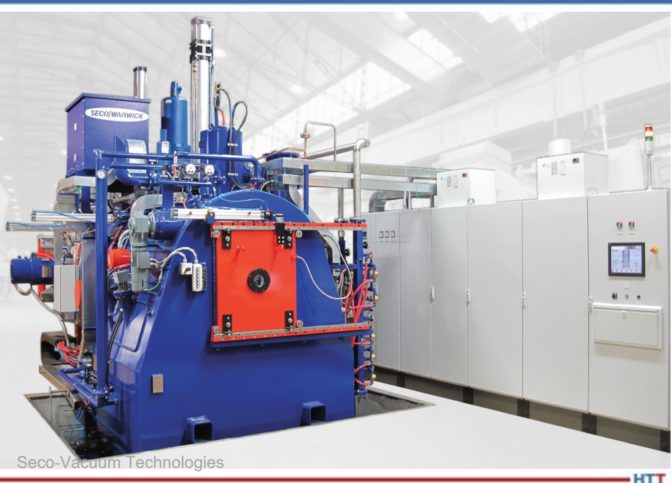
SECO/VACUUM will design and deliver the Vector®HPGQ 6-bar furnace with a customized 40"x40"x48" working zone and a 1.5 ton load capacity. The furnace package includes a 20,000 l/s diffusion pump for high-vacuum operation and a closed loop water system, loading cart, and nitrogen reservoir.
"We wanted a furnace that aligned perfectly with the exceptional capabilities and operation at our Illinois facility to ensure uniform product quality among plants," Karla Sarabia, manager of Watlow Electric Manufacturing Company's Mexico project said. "It’s also a big advantage that SECO/VACUUM has local maintenance support to serve our needs in Mexico."
We’ve assembled some of the top 101 Heat Treat Tips that heat treating professionals submitted over the last three years into todays original content. If you want more, search for “101 heat treat tips” on the website! Today’s tips are all things temperature: thermocouples, how to keep temperatures in check, TUS, and more.
By the way, Heat Treat Today introduced Heat Treat Resources this year; this is a feature you can use when you’re at the plant or on the road. Check out the digital edition of the September Tradeshow magazine to check it out yourself!
Temperature Monitoring When the Pressure is On!
Increasing in popularity in the carburizing market is the use of batch or semi-continuous batch low pressure carburizing furnaces. Following the diffusion, the product is transferred to a high-pressure gas quench chamber where the product is rapidly gas cooled using typically N2 or Helium at up to 20 bar pressure.
In such processes, the technical challenge for thru-process temperature monitoring is twofold. The thermal barrier must be capable of protecting against not only heat during the carburizing, but also very rapid pressure and temperature changes inflicted by the gas quench. From a data collection perspective, to efficiently perform temperature uniformity surveys at different temperature levels in the furnace it is important that temperature readings can be reviewed live from the process but without need for trailing thermocouples.
During the gas quench, the barrier needs to be protected from Nitrogen N2(g) or Helium He(g) gas pressures up to 20 bar. Such pressures on the flat top of the barrier would create excessive stress to the metal work and internal insulation / logger. To protect the barrier therefore a separate gas quench deflector is used. The tapered top plate deflects the gas away from the barrier. The unique Phoenix design means the plate is supported on either four or six support legs. As it is not in contact with the barrier no force is applied directly to the barrier and the force is shared between the support legs. The quench shield in addition to protecting against pressure, also acts as an additional reflective IR shield reducing the rate if IR absorption by the barrier in the vacuum heating chamber.
(PhoenixTM)
3 Tips to Meet Temperature Uniformity Surveys
Adjust the burners with some excess air to improve convection.
Make sure that the low fire adjustment is as small as possible. Since low fire will provide very little energy, it will make the furnace pulse more frequently and this will improve heat transfer by convection and radiation.
Increase internal pressure. This will “push” heat to dead zones allowing you to increase your coldest thermocouples (typically near the floor and in the corners of the furnace).
(Nutec Bickley)
Ways to Increase Temperature Uniformity in Heat Treat Furnaces
A (sometimes) simple way to increase uniformity in a furnace is to add a circulation fan. Circulation fans can be a quick way to add an additional 5°F tighter uniformity on a batch furnace application.
Be sure that the furnace is tuned optimally to reduce/eliminate any overshoot and oscillation around setpoint.
Eliminate any thermal lag by making sure that the control thermocouple and TUS thermocouples have similar sensitivity. If not, the control thermocouples can fall behind and cause the TUS thermocouples to overshoot and fail.
(L & L Special Furnace Co., Inc.)
Pack Your Thermocouples
When a thermocouple is used with an open-ended protection tube, pack rope or fiber between the thermocouple and the protection tube to prevent cold air infiltration from influencing the reading.
(Super Systems, Inc.)
A Good Fit
If a thermocouple fits loosely in a protection tube, avoid errors by ensuring that the tip maintains good contact with the tube.
(Super Systems, Inc.)
Introducing Your Common Thermocouple Types
What are the common thermocouple types?
Thermocouple material is available in types K, J, E, N, T, R, S, and B. These thermocouple types can be separated into two categories: Base and Noble Metals.
Types K, J, E, N, and T are Base Metals. They are made from common materials such as Nickel, Copper, Iron, Chromium, and Aluminum. Each base metal thermocouple has preferred usage conditions.
Types S, R, and B thermocouples are Noble Metals because they are made of one or more of the noble metals, such as Ruthenium, Rhodium, Palladium, Silver, Osmium, Iridium, Platinum, and Gold. Noble metals resist oxidation and corrosion in moist air. Noble metals are not easily attacked by acids. Some Noble metal thermocouples can be used as high as 3100°F.
(Pelican Wire)
Culprits of a Stable Thermocouple
Factors affecting the stability of a thermocouple:
The EMF output of any thermocouple will change slightly with time in service and at elevated temperatures. The rate and change are influenced by metallurgical and environmental factors. The four factors that can induce EMF drift are: Evaporation, Diffusion, Oxidation, and Contamination.
(Pelican Wire)
Does Length Matter?
Does the length of a thermocouple wire matter?
In a word, “Yes.” There are several factors when considering the maximum length of a thermocouple assembly. Total loop resistance and electrical noise. Total loop resistance should be kept under 100 ohms for any given thermocouple assembly. Remember, the total loop resistance would include any extension wire used to complete the circuit. Motors and power wires can create noise that could affect the EMF output.
(Pelican Wire)
Type N Thermocouple (Nicrosil/Nisil)
Type N Thermocouple (Nicrosil/Nisil): The Type N shares the same accuracy and temperature limits as the Type K. Type N is slightly more expensive and has better repeatability between 572°F to 932°F (300°C to 500°C) compared to type K.
(Pelican Wire)
Know Your Thermocouple Wire Insulations
Know your thermocouple wire insulations. When is Teflon® not Teflon®? Teflon® is a brand name for PTFE or Polytetrafluoroethylene owned by Chemours, a spin-off from Dupont. FEP is Fluorinated Ethylene Propylene. PFA is Perfluoroalkoxy Polymer. All three are part of the Fluoropolymer family but have different properties. Of the three compounds, PTFE has the highest heat resistance, PFA second highest and FEP third. The higher the heat resistance the more expensive the insulation. Keep that in mind when specifying the insulation and only pay for what you need.
We’ve assembled some of the top 101 Heat TreatTips that heat treating professionals submitted over the last three years into todays original content. If you want more, search for “101 heat treat tips” on the website! Today’s tips are all things temperature: thermocouples, how to keep temperatures in check, TUS, and more.
By the way, Heat TreatToday introduced Heat TreatResources this year; this is a feature you can use when you’re at the plant or on the road. Check out the digital edition of the September Tradeshow magazine to check it out yourself!
Temperature Monitoring When the Pressure is On!
Increasing in popularity in the carburizing market is the use of batch or semi-continuous batch low pressure carburizing furnaces. Following the diffusion, the product is transferred to a high-pressure gas quench chamber where the product is rapidly gas cooled using typically N2 or Helium at up to 20 bar pressure.
In such processes, the technical challenge for thru-process temperature monitoring is twofold. The thermal barrier must be capable of protecting against not only heat during the carburizing, but also very rapid pressure and temperature changes inflicted by the gas quench. From a data collection perspective, to efficiently perform temperature uniformity surveys at different temperature levels in the furnace it is important that temperature readings can be reviewed live from the process but without need for trailing thermocouples.
During the gas quench, the barrier needs to be protected from Nitrogen N2(g) or Helium He(g) gas pressures up to 20 bar. Such pressures on the flat top of the barrier would create excessive stress to the metal work and internal insulation / logger. To protect the barrier therefore a separate gas quench deflector is used. The tapered top plate deflects the gas away from the barrier. The unique Phoenix design means the plate is supported on either four or six support legs. As it is not in contact with the barrier no force is applied directly to the barrier and the force is shared between the support legs. The quench shield in addition to protecting against pressure, also acts as an additional reflective IR shield reducing the rate if IR absorption by the barrier in the vacuum heating chamber.
(PhoenixTM)
3 Tips to Meet Temperature Uniformity Surveys
Adjust the burners with some excess air to improve convection.
Make sure that the low fire adjustment is as small as possible. Since low fire will provide very little energy, it will make the furnace pulse more frequently and this will improve heat transfer by convection and radiation.
Increase internal pressure. This will “push” heat to dead zones allowing you to increase your coldest thermocouples (typically near the floor and in the corners of the furnace).
(Nutec Bickley)
Ways to Increase Temperature Uniformity in Heat Treat Furnaces
A (sometimes) simple way to increase uniformity in a furnace is to add a circulation fan. Circulation fans can be a quick way to add an additional 5°F tighter uniformity on a batch furnace application.
Be sure that the furnace is tuned optimally to reduce/eliminate any overshoot and oscillation around setpoint.
Eliminate any thermal lag by making sure that the control thermocouple and TUS thermocouples have similar sensitivity. If not, the control thermocouples can fall behind and cause the TUS thermocouples to overshoot and fail.
(L & L Special Furnace Co., Inc.)
Pack Your Thermocouples
When a thermocouple is used with an open-ended protection tube, pack rope or fiber between the thermocouple and the protection tube to prevent cold air infiltration from influencing the reading.
(Super Systems, Inc.)
A Good Fit
If a thermocouple fits loosely in a protection tube, avoid errors by ensuring that the tip maintains good contact with the tube.
(Super Systems, Inc.)
Introducing Your Common Thermocouple Types
What are the common thermocouple types?
Thermocouple material is available in types K, J, E, N, T, R, S, and B. These thermocouple types can be separated into two categories: Base and Noble Metals.
Types K, J, E, N, and T are Base Metals. They are made from common materials such as Nickel, Copper, Iron, Chromium, and Aluminum. Each base metal thermocouple has preferred usage conditions.
Types S, R, and B thermocouples are Noble Metals because they are made of one or more of the noble metals, such as Ruthenium, Rhodium, Palladium, Silver, Osmium, Iridium, Platinum, and Gold. Noble metals resist oxidation and corrosion in moist air. Noble metals are not easily attacked by acids. Some Noble metal thermocouples can be used as high as 3100°F.
(Pelican Wire)
Culprits of a Stable Thermocouple
Factors affecting the stability of a thermocouple:
The EMF output of any thermocouple will change slightly with time in service and at elevated temperatures. The rate and change are influenced by metallurgical and environmental factors. The four factors that can induce EMF drift are: Evaporation, Diffusion, Oxidation, and Contamination.
(Pelican Wire)
Does Length Matter?
Does the length of a thermocouple wire matter?
In a word, “Yes.” There are several factors when considering the maximum length of a thermocouple assembly. Total loop resistance and electrical noise. Total loop resistance should be kept under 100 ohms for any given thermocouple assembly. Remember, the total loop resistance would include any extension wire used to complete the circuit. Motors and power wires can create noise that could affect the EMF output.
(Pelican Wire)
Type N Thermocouple (Nicrosil/Nisil)
Type N Thermocouple (Nicrosil/Nisil): The Type N shares the same accuracy and temperature limits as the Type K. Type N is slightly more expensive and has better repeatability between 572°F to 932°F (300°C to 500°C) compared to type K.
(Pelican Wire)
Know Your Thermocouple Wire Insulations
Know your thermocouple wire insulations. When is Teflon® not Teflon®? Teflon® is a brand name for PTFE or Polytetrafluoroethylene owned by Chemours, a spin-off from Dupont. FEP is Fluorinated Ethylene Propylene. PFA is Perfluoroalkoxy Polymer. All three are part of the Fluoropolymer family but have different properties. Of the three compounds, PTFE has the highest heat resistance, PFA second highest and FEP third. The higher the heat resistance the more expensive the insulation. Keep that in mind when specifying the insulation and only pay for what you need.
(Pelican Wire)
Check out these magazines to see where these tips were first featured:
Do you always feel confident when selecting heat treating equipment? ¿Se siente siempre seguro cuando selecciona equipos de tratamiento térmico?
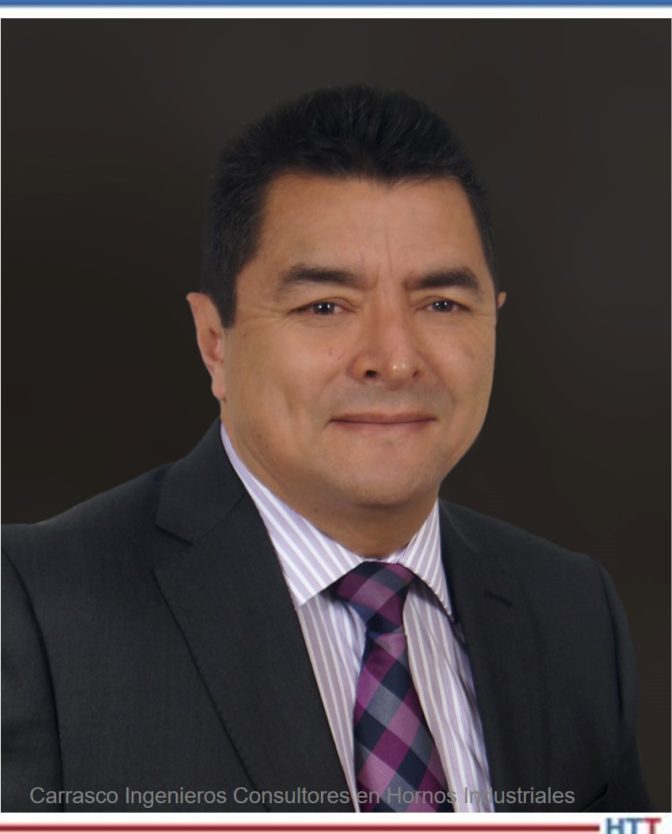
There are many factors involved when making a purchase. Often, key considerations may be missed. Read this guide on how to select and buy new equipment by Carlos Carrasco, founder of Carrasco Hornos Industriales.
This original content article was originally published inHeat TreatToday’s November 2021 Vacuum Furnaceprint edition in English and Spanish.
Carlos Carrasco Founder Carrasco Hornos Industriales
Why Is This Guide Helpful?
There are many reasons to select industrial furnaces carefully. One is the cost of the furnace. Another is realizing heat treating will affect the product and the bottom line. There is more specialized engineering in heat treating equipment than is apparent from the outside.
The purpose of this guide is to help engineers make the best equipment selection. The decision will affect not only the project, its budget, and results, but will also reflect the buyer’s knowledge. After the heat treating equipment is selected, the realization may occur that perhaps insufficient thought was given to potential maintenance problems or the work required to keep it in top working condition.
The following steps, gathered from more than 50 years of experience in the fields of manufacturing, sales, and maintenance, will be a useful guide to selecting heat treating equipment that will please both management and operators.
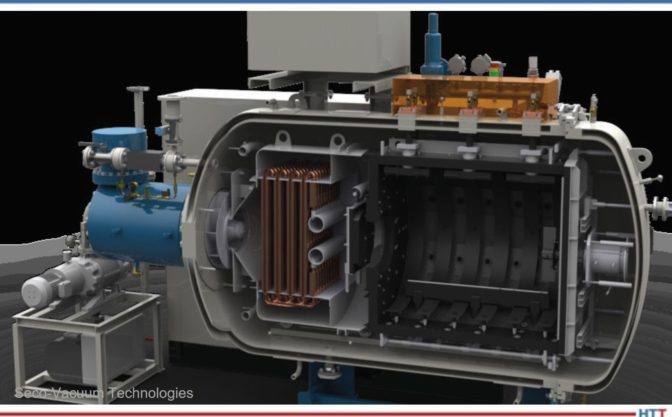
Vacuum high-pressure hardening furnace
Step One: Quote Request
When requesting a quote, management knows the exact requirements the heat treated products must have. A reliable supplier should be able to understand all requirements for a quote. Requests must be clear, concise, and contain at least the following information:
Heat treating processes that will be carried out on the equipment
Shape, general dimensions, and weights of the product(s) to be heat treated
Production volumes per hour, day, or month
Number of hours available for heat treating
Part material
Fuel type, or if the heating will be done with electricity
Voltage available in the plant
Space available for installation of equipment
Special considerations for handling loading and unloading
Furnace manufacturers need the above information to begin to create a series of options for the equipment that will be most suitable for the required processes. For example, hourly production defines: the dimensions of the space to heat the load, the type of furnace (continuous or batch), the amount of heat to be released in the furnace, the loading and unloading method, and the devices for accommodating or transporting the load such as trays, baskets, or conveyor belts. All these considerations influence both the initial cost and the operating cost, because in the end, the cost of the proposed equipment and its functionality are directly related to the specifications of the request for a quote.
It is difficult to attempt to use one furnace for all heat treating processes or to attempt to take into account future production needs that may not be necessary. It is impractical to carry out several processes that require different temperatures or have different production volumes. Trying to do so leads to oversized and over-budget equipment.
Vacuum low-pressure carburizing furnace
Step Two: Supplier Selection
Quote requests should only be submitted to manufacturers with the technical capacity and experience to prepare an offer that satisfies the request. Always use references from previous installations with similar quote requirements.
Considering the potential for financial gain, the cost of heat treating equipment can be appealing. The design and construction of heat treating equipment involves a considerable amount of engineering resulting from expensive investments in research and development. This research and development is influenced by user feedback detailing equipment failure. This feedback creates opportunities for manufacturers to fix equipment issues. Without the added benefit of other heat treater’s feedback, equipment failure is more likely. Finding a manufacturer with experience is crucial.
Only suppliers with experience and solid technical capacity will be able to guarantee results from the start. The goal is to receive equipment that requires no corrections after the first load leaves the furnace and to not have to rework the design.
Step Three: Study and Evaluation of Offers
A failed project is too much to risk, and so the responsible supplier will invest time and money in the study and preparation of the offer.
Every responsible supplier has been disappointed by an offer read backwards — when the potential customer reads the price first. Is the overriding need to stay within a certain budget or for heat treating equipment that is capable of processing parts to meet specifications? A careful reading of the offer may justify the cost of the furnace in relation to production needs. If there is a confusing section of the offer, it is important to clarify with the supplier. Investment in production equipment is very important, but it is even more important that the investment be profitable.
The heat treating equipment must satisfy a production need and certain metallographic specifications. Consequently, the dimensions of the space where the parts will be placed may be the main factor in the design of the furnace. This is because metals are only capable of heating up to a certain temperature at a rate that is determined by the heating method, geometry, and load arrangement. Only experienced vendors can make the correct calculations to meet the production needs of the project. Be sure to understand the calculations that lead to the sizing of the proposed system.
How are the parts supported and/or transported within the furnace? This is a point of great importance for the initial cost of these components and for the costs of future maintenance. Keep in mind that any mechanism that works at high temperatures will always be problematic for maintenance and replacement. Cast link belts, for example, have a higher initial cost, but they withstand heavy loads longer than metal mesh belts. However, there is a notable difference in the cost of components made of chromium-nickel alloy and those of carbon steel. Since chromium-nickel materials are able to withstand higher temperatures, their use is recommended and almost essential.
Furnaces tend to deteriorate rapidly where the heat is being lost. Make sure the door design is the best possible to avoid heat loss. Be sure that all doors included in the design are necessary. Doing so will save maintenance costs.
When it comes to quenching, oil or water circulation systems are extremely important, as is tank capacity. Otherwise, the quenching medium may overheat, causing unsatisfactory results.
In an oven intended for low temperature operations 356°F–1,112°F (180°C–600°C), for example tempering processes, it is necessary to have a fan to recirculate the hot air from the furnace. The uniformity of the temperature in the parts and the speed at which they heat up depends on the speed of recirculation, the weight of the air, and the design of the furnace, which must force the passage of air optimally through the load with the use of deflectors, screens, or distribution plenums. In high temperature furnaces, 1,292°F–2,192°F (700°C–1200°C), the heat transfer depends on the radiation toward the load and its exposed surface, so a recirculation fan is not necessary. Heat treatment is a critical process and temperature pyrometers must have the necessary precision.
List any doubts about the offer and ask the supplier to clarify at length in writing. The answers will make it easier to do a second analysis of the offer and compare it with other offers. In addition, the written clarifications will be a record for review by other collaborators on the project. Ask for feedback and observations on the proposals to get a second opinion.
Ask suppliers to provide a list of similar installations. Industry colleagues are generally unbiased in their comments about their experience with a particular supplier.
Finally, make a comparison chart in the most objective way possible. Keep in mind the fact that offers often do not include some subjective issues that may be important for a final selection. For example, some vendors are likely to have greater knowledge and experience in certain processes, simply because they have invested time and money to fi nd the best solutions to the process and those experiences could be beneficial.
Step Four: The Price
Understanding the scope of the received proposals that meet production and quality requirements is not all that goes into selecting heat treating equipment. After all this, there are still significant differences between various suppliers. Price is one of these differences. At this stage, the industrial furnace manufacturer will need to justify costs. It will be easy to tell if the manufacturer is thinking of the buyer as a future satisfied customer, or only of the economic benefits the sale will bring.
Conclusion
There are innumerable cases in which the equipment was poorly selected: “The substation and/or the cooling tower did not have the capacity;” or “The equipment is not what we expected;” or “They never told us that the furnace needed gas in those capabilities.” These are just a few of the possible comments everyone has heard.
Selecting heat treating equipment should be done slowly, analyzing all the options, weighing the differences between providers, and seeking clarification. Ask the supplier for multiple equipment options like requesting spare parts for the first year of operation.
Ultimately, time will tell if the furnace selected was the right choice. These recommendations provide a guide to making that decision. We sincerely hope that these recommendations will guide you in the selection of industrial furnaces for heat treating.
About the Author:
In addition to being the founder of Carrasco Hornos Industriales — furnace experts, consultants, and independent sales representatives for various furnace companies and spare parts — Carlos Carrasco is the founder and former president of ASM International, Mexico Chapter with more than 50 years of experience in the heat treat industry.
A worldwide supplier of high-temp piezo ceramics in the military, aerospace, and medical fields will receive a floor-standing, high-temperature, silicon carbide furnace. The furnace, powered by high-density silicon-carbide elements, will be used for processing glass products to 2,500°F.
L&L Special Furnace Co., Inc. will provide the furnace, model GLF836, which has a work zone of 18"x18"x36" with a double pivot horizontal door. The furnace, constructed from high-alumina refractory (with reduced silica), will help to delay the corrosive reaction between silica and the lead outgassing at elevated temperatures.
After the fourth annual nomination for Heat Treat Today’s 40 Under 40 Class of 2021 came to a close, Bethany Leone, editor at Heat TreatToday, shared what type of leaders would be recognized in the September 2021 Trade Showmagazine. Check out pages 32-55 for the full list of rising young leaders in the North American heat treat market.
Bethany Leone Heat Treat Daily / Heat Treat Radio Editor
Where did you come from? I mean, before you got into heat treating. And how did you become the heat treater that your colleagues know you to be today?
If you are like most people, heat treating was something that you fell into. You didn’t plan to go into the family business, but you did; your other opportunity at your dream job fell through and someone offered you this position; you were waiting for the chance of a lifetime and decided to pursue heat treat instead. . . .
The stories go on. Mundane, perhaps more often than not, but very much our stories.
Among the ordinariness of moving from point A to point B and making the small decisions to take on a new customer or take on a new cleaning or processing technology, we find rising young leaders of the heat treat market. The general manager at a small plant who continues to impress his colleagues and employer, or the young female operations handler whose capable, can-do attitude has driven her to vice president are the constantly felt, though not often recognized, leaders in our sphere.
Determining what is a leader is the first step to recognize these invaluable figures in our ordinary lives, hidden behind their families, books-of-the-month, and job transitions. But how to talk about a good leader? How do you put into words what is felt and not spoken? It’s a difficult question, but the best answer I can give you: tell a story.
These stories show hard work and initiative from one step to the next. . .
"Erick developed successful bilingual/bicultural work instructions and created a seamless process to develop new equipment using local resources, all during demanding project schedules and in the middle of the COVID crisis."
Leadership stories highlight cultivated talent on display. . .
"Lindsey’s communications background has helped Advanced Heat Treat Corp’s growth in technical material content for customers [. . .] Lindsey’s marketing expertise has increased AHT’s website traffic year-after-year, with a 45% increase since the pandemic."
A good story moves people with cutting edge reality and humanity of a leader. . .
"With [Matthew’s] newly acquired purchase of his first home, he is honing his abilities as a handyman from rough carpentry to finish work. Applying his perfectionist personality to every job, it’s truly hard to tell if it was done by him or a professional."
As you peel through these pages to look for the next technical article or skim for an advertiser who will meet your needs, pause for a moment with fresh eyes on the incredible narratives that make up Heat TreatToday’s 40 Under 40 Class of 2021.
Piotr Zawistowski Managing Director SECO/VACUUM TECHNOLOGIES, USA Source: secowarwick.com
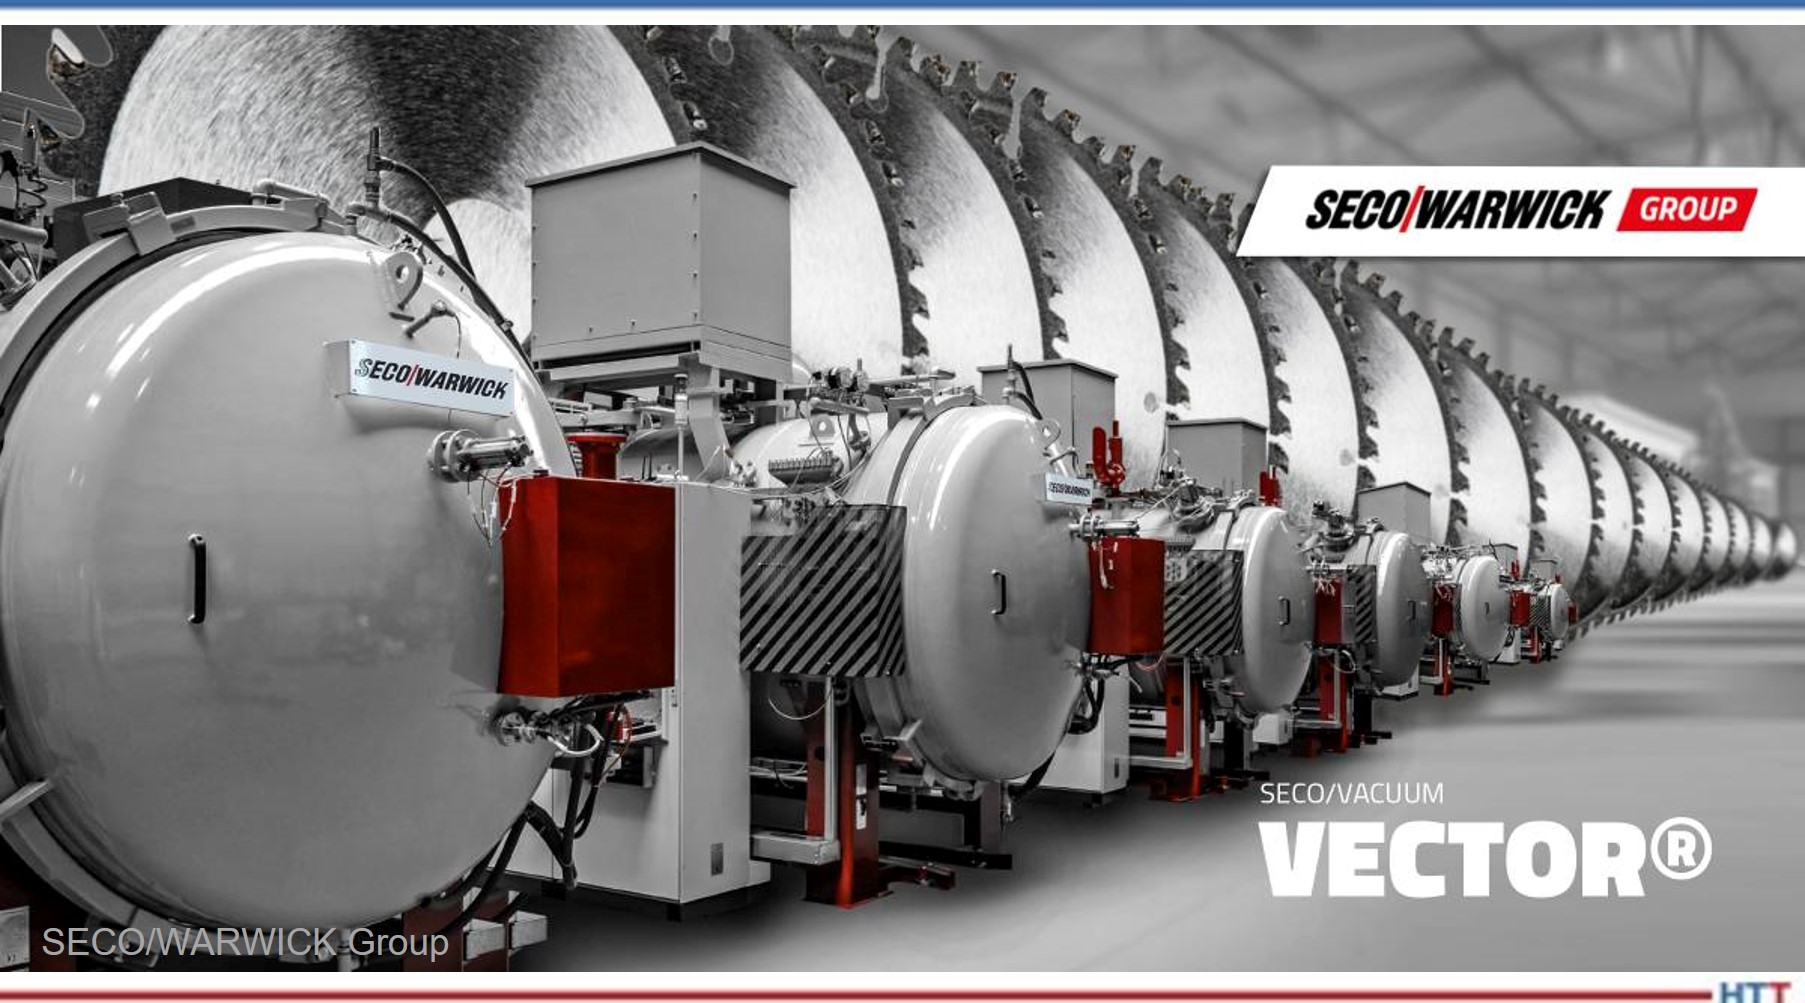
An international cutting tool manufacturer will augment the capacity of its heat treat vacuum temper furnaces with two more at their North Carolina manufacturing facility.
This expansion to the company's heat treat capabilities comes two months after ordering their fourth Vector® from SECO/VACUUM. The two single chamber, horizontal, front-loading furnaces are designed with an all-metal hot zone for clean vacuum processing. This style will be able to keep up with most standard hardening, tempering, annealing, solution heat treating, brazing and sintering applications, as well as low pressure carburizing.
"We are thrilled to be an ongoing partner in this [client's] growth," said Piotr Zawistowski, managing director of SECO/VACUUM. "We know they have multiple competitive options for their vacuum heat treat equipment, so we take nothing for granted, and work hard to earn their business every step of the way."
ELLWOOD Aluminum, an Ohio-based manufacturer of aluminum products, recently acquired a 200,000-lb. batch homogenizing furnace to complete the Phase 2 expansion of their plant in Hubbard, OH.
Gillespie & Powers, Inc., a family-owned supplier based in St. Louis, MO, will deliver the furnace to be operational in July 2022. The furnace, the second of its kind at ELLWOOD Aluminum, will be used for manufacturing large diameter aluminum ingots and billets, as well as rectangular slabs and cast plates.




 Source: ThomasNet.com
 A company which has served construction, mining, and earth moving, but which is now involved in gas, power generation, military, aerospace, and more is Complete Heat Treating — this month’s MTI Member Profile company. They have many value-added operations under one roof combined with knowledgeable technical staff helping to select the optimum process to meet customer expectations.





 The heat treating equipment must satisfy a production need and certain metallographic specifications. Consequently, the dimensions of the space where the parts will be placed may be the main factor in the design of the furnace. This is because metals are only capable of heating up to a certain temperature at a rate that is determined by the heating method, geometry, and load arrangement. Only experienced vendors can make the correct calculations to meet the production needs of the project. Be sure to understand the calculations that lead to the sizing of the proposed system.