Happy Memorial Day from Heat Treat Today. Join us as we reflect in thankfulness on those who have sacrificed all for our country. Thank you to all who currently serve to protect the land of the free. God bless America.
Heat Treat Today’s offices will be closed for the long weekend, and there will be no e-newsletter Monday, May 17. See you on Tuesday!
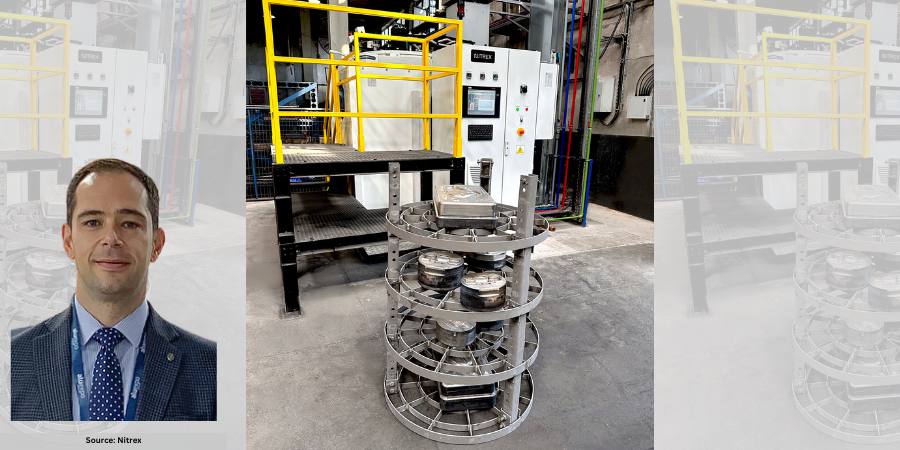
As part of their strategic efforts to enhance forging capabilities, Topçesan recently invested in a compact batch-type furnace with a 1,200 kg capacity, designed for nitriding and nitrocarburizing forging dies. These dies are utilized in the production of engine parts, transmission components, and chassis parts for vehicle manufacturing, catering to automotive clients like BMW, Tofaş, Fiat, and ZF Group across Europe and Türkiye.
Utku Inan
Sales Representative in Türkiye
Nitrex
Source: Nitrex
By integrating nitriding and nitrocarburizing processes into their operations, Topçesan aims to prolong the lifespan of their forging dies, increasing component production while reducing tooling costs. The NXK-812 compact batch-type furnace from Nitrex, a heat treat equipment supplier based in Canada, includes an ammonia dissociator; this will be essential for precision controlling nitriding potential, particularly when treating specific alloys that must align with AMS 2759/10 and AMS 2759/12 specifications.
Utku Inan, the Nitrex sales representative in Türkiye, commented, “This marks the first collaboration between Topçesan and Nitrex, and we’re truly excited to embark on this journey together. Our shared goal is to pursue operational excellence and maximize product potential within the forging and automotive supply chain industries.”
Topçesan is making a strategic investment that will not only enhance its in-house capabilities and cost efficiency but also contribute to a more efficient and sustainable future. According to Marcin Stoklosa, technical sales manager at Nitrex, “The operating software of the Nitrex system ensures optimal production media and utility consumption throughout the process, providing the customer with detailed analysis after each operation. This technological advancement underscores our commitment to customer satisfaction and operational efficiency, ensuring superior performance.”
“When it comes to who should lose their jobs because of changing times, I’d much rather leave the decision up to the market and millions of individual decisions being made independently around the world . . .”
Heat Treat Todaypublishes eight print magazines a year and included in each is a letter from the publisher, Doug Glenn. This letter first appeared in the May 2024 Sustainable Heat TreatTechnologiesprint edition.
To prove that it is not, I’d like you to meet Mr. Isaac Chan, a DOE employee. Mr. Chan, whom I met in March of this year at an Industrial Heating Equipment Association Annual Spring Meeting is a genuinely nice person with no ill intent toward any living soul. He is also the program manager at the DOE’s Office of Industrial Efficiency and Decarbonization.
Let’s pause for just a moment before we talk more about Mr. Chan and acknowledge that the name of this DOE Office, “Industrial Efficiency and Decarbonization,” will be, in some specific cases, an oxymoron. In specific industries, given the best available technologies (BAT), mandated decarbonization would cause industrial inefficiency.
Back to Mr. Chan. As I’ve stated, he is a very nice person, but the job he and hundreds of others at the DOE are being paid to do with taxpayer dollars is explicitly targeted at changing the energy composition of U.S. industry with the undeniable effect of putting many, if not all, combustion processes in the ash heap of history along with all those employed therein.
On the fourth slide of a presentation entitled, “Cross Sector Technologies Meeting: Day 2, Next-Generation Enabling Technologies,” presented by Mr. Chan on May 30, 2023, we find the following:
DOE Commitment to Industrial Decarbonization (slide title)
“Industrial Heat Shot™ — Developing technologies to reduce process heating GHG emissions by 85% by 2035”
“Industrial Decarbonization Roadmap — Net-zero CO2 emissions by 2050”
The same slide goes on to list four international organizations that the U.S. has joined to “decarbonize” energy-intensive industries. Those four organizations are:
Net-Zero World Initiative
G7 Industrial Decarbonization Agenda
Mission Innovation’s Net-Zero Industries Mission
UNIDO’s coordinated Industrial Deep Decarbonization Initiative
Who Decides
The issue here is who decides if the world will decarbonize or not. I personally have no axe to grind on whether combustion people stay employed or not. Economies change. Energy sources change. People in those industries lose and gain jobs. And assuming these changes are the result of millions of decisions freely made by millions of individuals daily, we can safely consider these changes to be progress. But when a change from one fuel to another — gas to electricity or carbon to no carbon fuels in this case — is pushed from the top down, when it is forced on us by “guideline” or “mandate” using our own money, that is not progress.
The market should decide. A free, unfettered market where millions of people make decisions daily is a more reliable indicator of what the people want than the well-meaning individuals in the DOE — no disrespect to any of these good people.
When it comes to who should lose their jobs because of changing times, I’d much rather leave the decision up to the market and millions of individual decisions being made independently around the world, than to a small group of well-meaning individuals who believe they know what is best for the world.
Let’s let the market do what it does so well. Let the market choose the winners and losers.
NASA has selected Elementum 3D (a developer and supplier of metal additive manufacturing (AM) advanced materials, print parameters, and services) to be one of four companies that will produce and distribute GRX-810 material under a commercial co-exclusive license. This is a material that has undergone significant post-processing heat treat research.
The 3D printable high-temperature metal superalloy material has been noted as “breakthrough technology” and will be offered to original equipment manufacturers of airplanes and rockets as well as the entire supply chain.
NASA’s goal of the licensing agreement is to accelerate the adoption of GRX-810 to benefit U.S. technologies, industry, and space exploration. The 3D printer supplier notes that engineers are eager to print with a material capable of creating lighter and thinner engine parts, reducing fuel burn, lowering operating costs, increasing durability, and lowering the tolerance for failure for critical applications.
GRX-810 is an oxide dispersion strengthened (ODS) alloy that can endure higher temperatures and stress. Its strength is derived from the dispersion of tiny particles containing oxygen atoms. The breakthrough superalloy was specifically developed for the extreme temperatures and harsh conditions of aerospace applications, including liquid rocket engine injectors, combustors, turbines, and hot-section components, capable of enduring temperatures up to 1,100°C. Compared to other alloys, GRX-810 can endure higher temperatures and stress up to 2,500 times longer. It’s also 3.5 times better at flexing before breaking and twice as resistant to oxidation damage.
Jeremy Iten
Chief Technology Officer
Elementum 3D
Source: LinkedIn
Over the past nine years, Elementum 3D has gained extensive knowledge and experience in developing, commercializing, and distributing “impossible-to-print” dispersion-strengthened materials similar to GRX-810.
“We are excited to be working with Tim Smith and NASA to bring this exceptional new alloy to the commercial market,” said Jeremy Iten, chief technology officer at Elementum 3D.
NASA’s investment in developing GRX-810 demonstrates its dedication to advancing additive manufacturing. Elementum 3D and the other co-exclusive licensees now assume the responsibility of investing the time and resources to supply the industry with a stronger, more durable superalloy.
Today’s News from Abroad installment brings us news of casting equipment supplied in China, heat treat supplier joint venture forged in Austria, and big standardization plans in Germany — where doing LESS is more.
Heat Treat Today partners with two international publications to deliver the latest news, tech tips, and cutting-edge articles that will serve our audience — manufacturers with in-house heat treat. heat processing, a Vulkan-Verlag GmbHpublication, serves mostly the European and Asian heat treat markets, andFurnaces International, a Quartz Business Media publication, primarily serves the English-speaking globe.
High-Performance Continuous Caster on Order
Representatives from Primetals Technologies and Wuyang Iron and Steel at the signing ceremony Source: Primetals Technologies
“Wuyang Iron and Steel has awarded Primetals Technologies an order for a 1-strand continuous caster with several record-breaking features. The continuous casting plant will be put into operation at the Wuyang plant in Wugang, Henan Province, and is expected to be the most powerful of its kind in the world. It will also produce the thickest slabs in the world, up to 460 millimeters thick. Thanks to the new facilities, Wuyang will be able to produce sheet metal for heavy-duty applications such as shipbuilding and the wind power sector. The annual capacity will be one million tonnes of high-quality slabs.”
Left to right, 1. row: Christian Grosspointner, CEO Aichelin Group; Mehmet Özdeşlik, CEO Sistem Teknik; 2. row: Wolfgang Brosche, Erwin Strauszberger, Beril Özdeşlik, Beste Özdeşlik, Gökhan Lale, Levent Sindel. Source: Aichelin
“The Aichelin Group and Sistem Teknik have signed an agreement to establish a joint venture in Austria. This joint venture will produce and distribute industrial vacuum heat treatment technologies and services in Europe. The Aichelin Group is thus adding a promising segment to its existing product portfolio.”
Two steelmaker groups, GMH (Georgsmarienhütte) Gruppe and Swiss Steel, have issued notes of approval for the proposal from German steel federation for a standard for low-emission steel (LESS). Source: worldsteel
Dec“Two steelmaker groups, GMH (Georgsmarienhütte) Gruppe and Swiss Steel, have issued notes of approval for the proposal from German steel federation for a standard for low-emission steel (LESS). Both mills happen to be makers of special bar qualities, and the word of Swiss Steel may have some international weight, given it has melt shops in Germany, Switzerland and France. WV Stahl announced on Monday that it has set a cornerstone for prime markets for climate-friendly streel with a standard its members developed together with the German economy and climate protection ministry. The Low Emission Steel Standard (LESS), as it is called, is the first standard that makes the main customary production routes, blast furnace and EAF, comparable in terms of their efforts to decarbonise. Its centrepiece is a labelling system for the classification of low-CO2 steels.”
Consider the numerous systems in your heat treat operations. What makes up the anatomy of each furnace or system? In this “Anatomy of a . . .” series, industry experts indicate the main features of a specific heat treat system. In this feature, the full-page spread identifies main features of induction coils.
The mark-ups for these reference images are provided by John Gadus, design and sales specialist, Induction Tooling, Inc.
View the full graphics by clicking the image below.
This Technical Tuesday article is drawn from Heat Treat Today’sApril/May 2024 Sustainable Heat Treat Technologiesprint edition, that had a special focus on green heat treat technologies.
Search www.heattreatbuyersguide.com for a list of induction equipment providers to the North American market. If you are an induction equipment supplier and are not listed here, please let us know at editor@heattreattoday.com.
This series will continue in subsequent editions of Heat Treat Today’sprint publications. Stay tuned!
Find Heat Treating Products And Services When You Search On Heat Treat Buyers Guide.Com
A nitriding service provider in Brazil will increase their production line with a single-chamber vacuum furnace from a manufacturer with North American locations.
Peter Lutz, president of Nitrion do Brasil says, “We were looking for a solution that would help not only increase our metal processing capabilities, but also efficiency and effectiveness.”
The SECO/WARWICK Vector vacuum furnace will operate in a new production hall and will handle Nitrion do Brasil’s increasing order volume. This order is a result of cooperation between SECO/WARWICK and their strategic partner in Brazil, Combustol.
Maciej Korecki Vice President of Business of the Vacuum Furnace Segment SECO/WARWICK
“Combustol supports SECO/WARWICK not only in sales but also in service activities and the supply of spare parts. Such a partner in such a remote location is a huge advantage,” commented Maciej Korecki, VP of the Vacuum Furnaces Segment in the SECO/WARWICK Group. He added, “[Nitrion do Brasil] bought a furnace that we could deliver quickly.”
The furnace on order will solve the commercial heat treater’s problem of hardening larger elements, because the furnace is equipped with a large working space. This will affect the process economics (energy savings and the graphite chamber’s increased efficiency) as well as the process cleanliness and speed. The furnace is equipped with convection heating – a system that improves the heat transfer efficiency when heating at lower temperatures, as well as directional cooling, which allows the system to efficiently cool parts with problematic shapes in various ways.
We’re celebrating getting to the “fringe” of the weekend with a Heat Treat Fringe Friday a press release detailing how additive manufacturing continues to move into the metals manufacturing industry.
While not exactly heat treat, “Fringe Friday” deals with interesting developments in one of our key markets: aerospace, automotive, medical, energy, or general manufacturing.
Desktop Metal, a global company at the forefront of additive manufacturing 2.0 technologies for mass production, announced that it has installed four Figur G15 Pro systems featuring digital sheet forming (DSF) technology to three manufacturers, including Evology Manufacturing in Waukesha, Wisconsin.
With 30+ years as a contract manufacturer, Evology has a full suite of both traditional and additive technologies to service companies in a wide range of industries, including aerospace, defense, automotive, agricultural, marine, mining, medical, electronics, and consumer goods. Evology serves companies ranging from small startups to Fortune 50 companies with prototyping and low-volume production, typically under 10,000 pieces.
Evology is now offering digital sheet form parts off its Figur G15 for cold rolled steel up to 2 mm thick and 6061 aluminum up to 3.175 mm thick, with more materials in development.
“We are delighted to offer our customers this cutting-edge rapid sheet metal forming technology from Desktop Metal,” said Sean Momsen, VP of Business Development and Marketing at Evology. “In addition to our ability to fabricate sheet metal parts rapidly, we also have a full suite of traditional finishing equipment to deliver finished final products to customers.”
Justin Nardone, CEO of Figur, a Desktop Metal brand, said, “We are encouraged by the continued demand we see for our rapid sheet metal forming technology, which truly saves manufacturers time and money when it comes to sheet metal production. The G15 eliminates a lot of the work required when forming metal, such as the design and manufacturing of tools and dies. Our system produces designs quickly, accurately, and repeatedly, so manufacturers are able to focus on the craftsmanship of design while getting their products to market faster and more efficiently.”
Introduced in 2022, the Figur G15 is the first commercial platform of its kind to shape sheet metal on demand directly from a digital file. A software-driven proprietary tooling system on an XY gantry forms the sheet with up to 2,000 lbs of force in a highly engineered and proprietary build zone.
With a maximum sheet size of 1,600 x 1,200 mm (63.0 x 47.2 in), the Figur G15 delivers parts with a draw depth up to 400 mm (16 in) in Z without custom forming tools, molds, dies, or presses. The G15 supports forming a range of metals and sheet thicknesses – including steel up to 2.0 mm and aluminum up to 2.5 mm – and delivers a high quality surface finish
Pro configurations of the Figur G15 include an automatic tool changer and measurement, through tool part lubrication, and automated work holding capabilities.
This press release is available in its original form here.
Given changing ecological and economic conditions, carbon neutrality is becoming more important, and the heat treatment shop is no exception. In the context of this article, the focus will be on how manufacturers — especially those with in-house heat treat — can save energy by evaluating heating systems, waste heat recovery, and the process gas aspects of the technology.
This article, written by Dr. Klaus Buchner, head of Research and Development at AICHELIN HOLDING GmbH, was released in Heat Treat Today April/May 2024 Sustainable Heat TreatTechnologiesprint edition.
Introduction
Contact us with your Reader Feedback!
Uncertainties in energy supply and rising energy costs remind us of our dependence on fossil fuels. This underlines the need for a sustainable energy and climate policy, which is the central challenge of our time.
European policymakers have already taken the first steps towards a green energy revolution, and the heat treatment industry must also take responsibility. Many complementary measures, however, are needed that can be applied to new and existing thermal and thermochemical heat treatment lines.
Heat Treatment Processes and Plant Concepts
The heat treatment process itself is based on the requirements of the component parts, and especially on the steel grade used. If different concepts are technically comparable, it is primarily the economic aspect that is decisive, and not the carbon footprint — at least until now. Advances in materials technology and rising energy costs are calling for production processes to be modified.
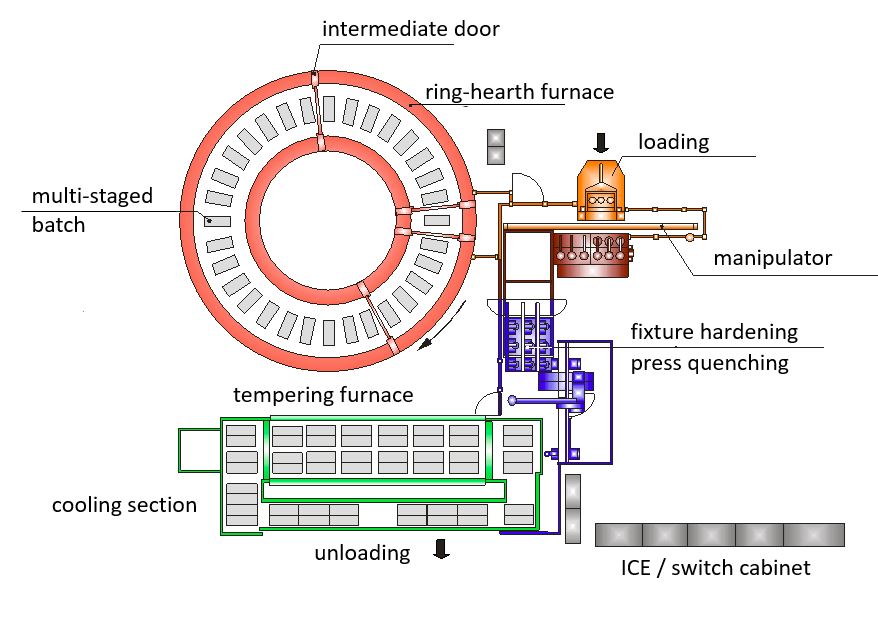
Figure 1. Donut-shaped rotary-hearth furnace for carburizing with press quenching Source: AICHELIN HOLDING GmbH
An example is the quenching and tempering of automotive forgings directly from the forging temperature without reheating, which has shown significant potential for energy and CO2 savings. Although the reduced toughness or measured impact energy of quenching and tempering from the forging temperature may be a drawback due to the coarser austenite grain size, this can be partially improved by Nb micro-alloyed steels and higher molybdenum (Mo) contents for more temper-resistant steels; it may also be necessary to use steels with modified alloying concepts when changing the process.1, 2 AFP steels (precipitation-hardening ferritic pearlitic steels) and bainitic air-hardening steels can also be interesting alternatives, since reheating (an energy-intensive intermediate step) is no longer necessary.
Similar considerations apply to direct hardening instead of single hardening in combination with carburizing processes because of the elimination of re-austenitizing. Distortion-sensitive parts often need to be quenched in fixtures due to the dimensional and shape changes caused by heat treatment. Heat treated parts are often carburized in multipurpose chamber furnaces or small continuous furnaces, cooled under inert gas, reheated in a rotary-hearth furnace, and quenched in a hardening press. In contrast, ring-shaped (aka donut-shaped) rotary-hearth furnaces allow carburizing and subsequent direct quenching in the quench press in a single treatment step. Figure 1 shows a typical ring-shaped rotary-hearth furnace concept for heat treating 500,000 gears per year/core hardness depth (CHD) group 1 mm.
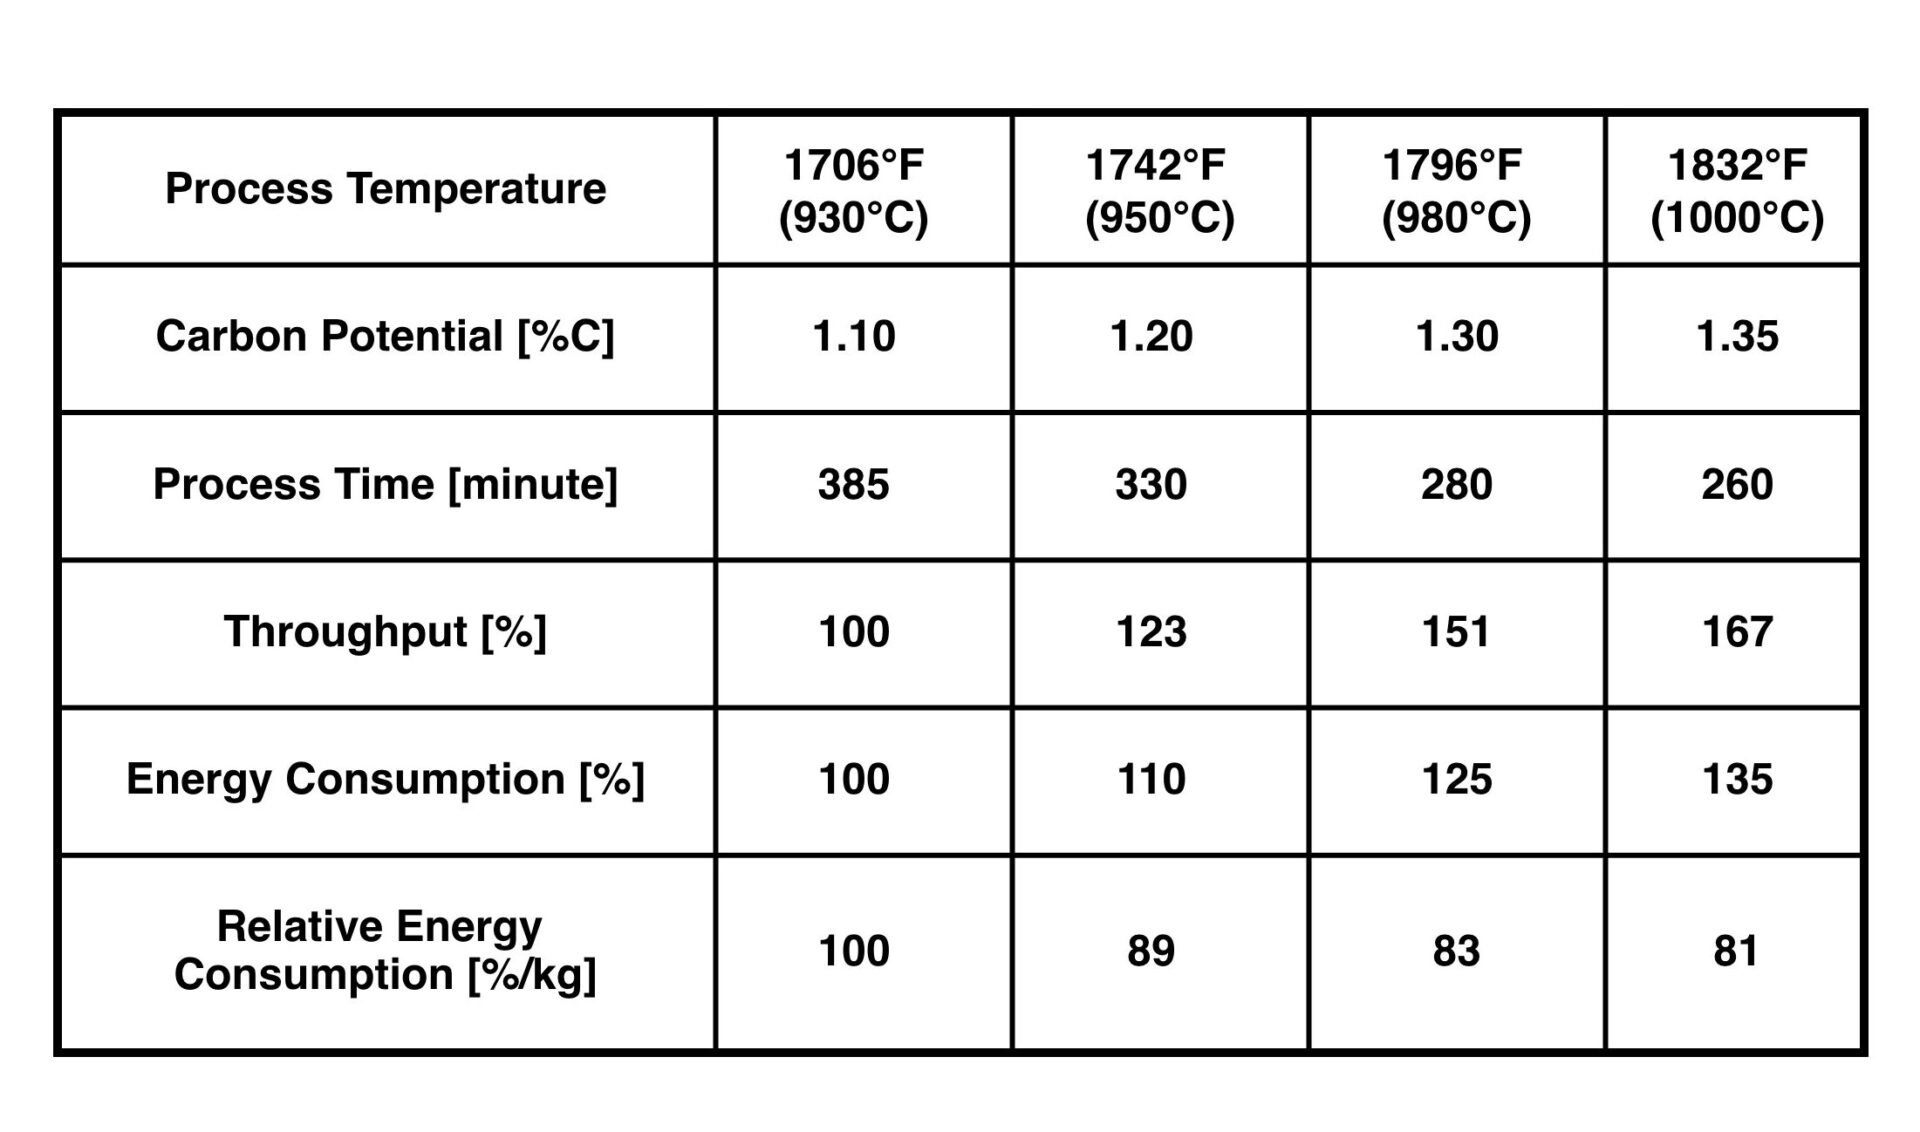
Table 1. Saving potential due to increased process temperature for gas carburizing (pusher type furnace, 20MnCr5, CHD-group 1 mm) Source: AICHELIN HOLDING GmbH
This ring-shaped rotary-hearth concept can save up to 25% of CO2 emissions, compared to an integral quench furnace line (consisting of four single-chamber furnaces, one rotary hearth furnace with quench press and two tempering furnaces as well as two Endothermic gas generators). Due to the reduced total process time (without reheating) and the optimized manpower, the total heat treatment costs can be reduced by 20–25%.
The high-temperature carburizing aspect should also be mentioned, although the term “high-temperature carburizing” is not fully accepted nor defined by international standards. As the temperature increases, the diffusion rate increases and the process time decreases. As shown in Table 1, the additional energy consumption is less than the increase in throughput that can be achieved. Therefore, the relative energy consumption per kg of material to be heat treated decreases as the process temperature increases.
There are three key issues to consider when running a high-temperature carburizing process:
Steel grade: Fine-grain stabilized steels are required for direct hardening at temperatures of 1832°F (1000°C). Microalloying of Nb, Ti, and N as well as a favorable microstructure of the steels reduce the growth of austenite grains and allow carburizing temperatures up to 1922°F (1050°C) for several hours.
Furnace design: In addition to the general aspects of the optimized furnace technology (e.g. heating capacity, insulation materials, and feedthroughs), failure-critical components must be considered separately in terms of wear and tear, whereby condition monitoring tools can support maintenance in this area.
Distortion: This is always a concern, especially in the case of upright loading of thin-walled gear sections. As such, numerical simulations and/or experimental testing should be performed at the beginning to estimate possible changes in distortion and to take measures if necessary.
Figure 2. Recuperative burner with SCR system for NOx reduction
Source: AICHELIN HOLDING GmbH
Heating System
Based on an energy balance that considers total energy losses, and preferably also temperature levels, it can be seen that the heating system plays a significant role. In addition to the obvious flue gas loss in the case of a gas-fired thermal processing furnace, the actual carbon footprint must be critically examined.
In the case of natural gas, the upstream process chain is often neglected in terms of CO2 emissions, but the differences in gas processing (which are directly linked to the reservoirs) and in gas transportation can be a significant factor.3 However, the analysis of energy resources in the case of electric heating systems is much more important. This results in specific CO2 emissions between 30–60 gCO2/kWh (renewable-based electricity mix) and 500–700 gCO2/kWh (coal-based electricity mix). Therefore, a general comparison between natural gas heating and electric heating systems in terms of carbon footprint is often misleading.
Figure 3. Comparison of specific CO2 emissions
Source: AICHELIN HOLDING GmbH
Nevertheless, in the case of gas heating, the aspect of combustion air preheating should be emphasized, as it has a significant influence on combustion efficiency. The technical possibilities in this area are well known and include both systems with central air preheating and decentralized concepts, where the individual burner and the heat exchanger form a single unit. Recuperator burners are often used in combination with radiant heating tubes (indirect heating) in the field of thermochemical heat treatment. With respect to oxy-fuel burners, it should also be noted that the formation of thermal NOx increases with increasing combustion temperature and temperature peaks. To avoid exceeding NOx emissions, staged combustion and so-called “flameless combustion” — characterized by special internal recirculation — and selective catalytic reduction (SCR) can be used. The latter secondary measure, together with selective non-catalytic reduction (SNCR), has been state-of-the-art in power plant design for decades and has become widely known because of its use in the automotive sector. This system can also be adapted to single burners (Figure 2). In this way, NOx emissions can be reduced to 30 mg/Nm3 (5% reference oxygen), depending on the injection of aqueous urea solution, as long as the exhaust gas temperature is in the range of 392/482°F (200/250°C) to 752/842°F (400/450°C).4
Whether electric heating is a viable alternative depends on both the local electricity mix and the design of the heat treatment plant, which may limit the space available for the required heating capacity. In addition to these technical aspects, the security of supply and the energy cost trends must also be considered. Both of these factors are significantly influenced by the political environment. Figure 3 shows an example of the specific carbon footprint per kg of heat treated material with the significant losses based on the example of an integral quench furnace concept in the double-chamber and single-chamber variants electrically heated (E) and gas heated (G). The electric heating is based on a fossil fuel mix of 485 gCO2/kWh. Once again, it is clear that a general statement regarding CO2 emissions is not possible; rather, the boundary conditions must be critically examined.
Waste Heat Recovery — Strengths and Weaknesses of the System
Although improvements in the energy efficiency of heat treatment processes, equipment designs, and components are the basis for rational energy use, from an environmental perspective it is important to consider the total carbon footprint. An energy flow analysis of the heat treatment plant, including all auxiliary equipment, shows the total energy consumption and thus the potential savings. Quite often the temperature levels and time dependencies involved preclude direct heat recovery within the furnace system at an economically justifiable investment cost. In this case, cross-plant solutions should be sought, which require interdepartmental action but offer bigger potential.
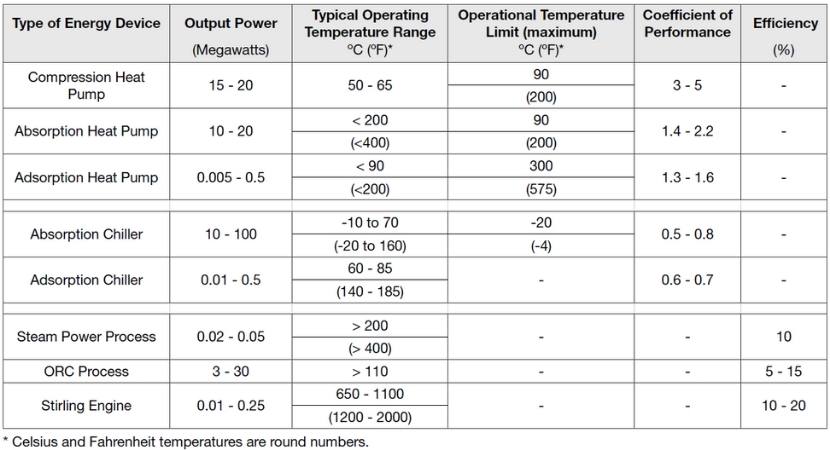
In addition to the classic methods of direct waste heat utilization using heat exchangers, also in combination with heat accumulators, indirect heat utilization can lower or raise the temperature level of the waste heat by using additional energy (chiller or heat pump) or convert the waste heat into electricity. The overview in Table 2 provides reference values in terms of performance class and temperature level for the alternative technologies listed.
Process Gas for Case Hardening
Case hardening — a thermochemical process consisting of carburizing and subsequent hardening — gives workpieces different microstructures across the cross-section, the key factor being high hardness/strength in the edge region. A distinction can be made between low pressure carburizing in vacuum systems and atmospheric carburizing at normal pressure. Both processes have different advantages and disadvantages, with atmospheric heat treatment being the dominant process.
Table 2. Overview of alternative waste heat applications5, 6 Source: AICHELIN HOLDING GmbH
In terms of carbon footprint, atmospheric heat treatment has a weakness due to process gas consumption. To counteract this, the following aspects have to be considered: thermal utilization of the process gas — indirectly by means of heat exchangers or directly by lean gas combustion (downcycling); reprocessing of the process gas (recycling); reduction of the process gas consumption by optimized process control; and use of CO2-neutral media (avoidance). This article focuses on avoidance by optimizing process gas consumption and using of CO2-neutral media.
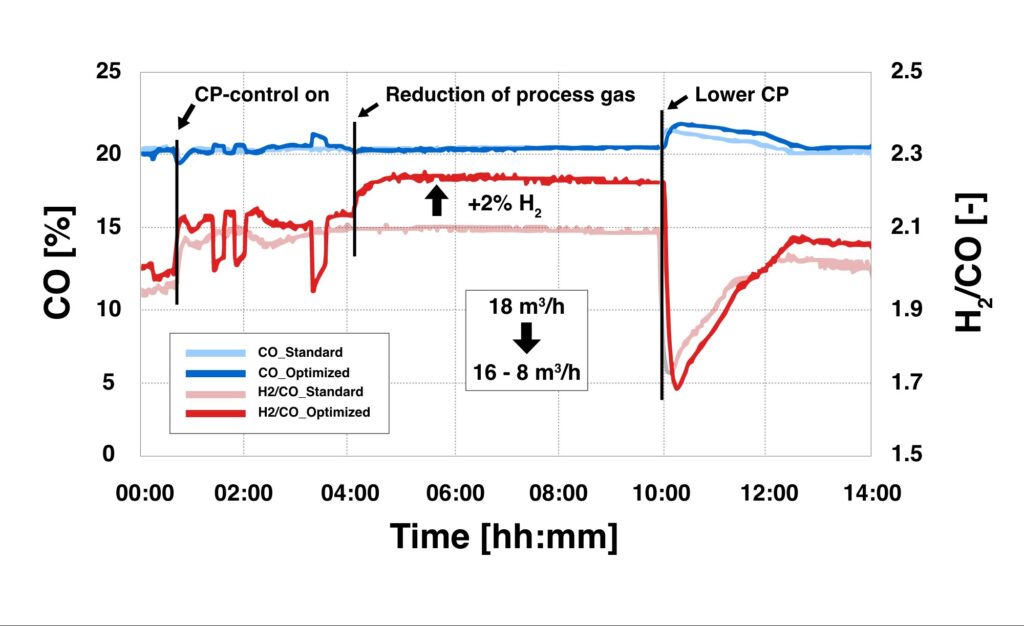
Typically, heat treatment operations are still run with constant process gas quantities based on the most unfavorable conditions. Based on the studies of Wyss, however, process control systems offer the possibility to adapt the actual process gas savings to the actual demand.7 In a study of an industrial chamber furnace, a 40% process gas savings was demonstrated for a selected carburizing process. In this heat treatment process with a case hardness depth of 2 mm, the previously used constant gas flow rate of 18 m3/h was reduced to 16 m3/h for the first process phase and further reduced to 8 m3/h after 3 hours. Figure 4 shows the analysis of the gas atmosphere, where an increase in the H2 concentration could be detected due to the reduction of the gas quantities. With respect to the heat treatment result, no significant difference in the carburizing result was observed despite this significant reduction in process gas volume (and the associated reduction in CO2 emissions). The differences in the carbon profiles are within the expected measurement uncertainty.
Figure 4. CO and H2/CO concentration at various process gas volumes
Source: AICHELIN HOLDING GmbH
The carbon footprint of the process gas, however, must be fundamentally questioned. In the field of atmospheric gas carburizing, process gases based on Endothermic gas (which is produced by the catalytic reaction of natural gas or propane with air at 1832–1922°F/1000–1050°C) and nitrogen/methanol and methanol only systems have established themselves on a large scale. Methanol production is still mostly based on fossil fuels (natural gas or coal), the latter being used mainly in China. Although alternative CO2-neutral processes for partial substitution of natural gas — keywords being “power to gas” (P2G) or “synthetic natural gas” (SNG) — have already been successfully demonstrated in pilot plants, there are no signs of industrial penetration. Nevertheless, there is a definite industrial scale in the area of bio-methanol synthesis, though so far, purely economic considerations speak against it, as CO2 emissions are still not taken into account.
The question of the use of bio-methanol in atmospheric gas carburizing has been investigated in tests on an integral quench furnace system. A standard load of component parts with a CHD of 0.4 mm was used as a reference. Subsequently, the heat treatment process was repeated with identical process parameters using bio-methanol instead of the usual methanol based on fossil fuels. Both the laboratory analyses of the methanol samples and the measurements of the process gas atmosphere during the heat treatment process, as well as the evaluation of the sample parts with regard to the carbon profile during the carburizing process, showed no significant difference between the different types of methanol. Although this does not represent long-term experience, these results underscore the fundamental possibility of media substitution and the use of CO2-neutral methanol.
Conclusion
Facing the challenges of global warming — intensified by the economic pressure of rising energy costs — this article demonstrates the energy-saving potential in the field of heat treatment. In addition to already established solutions, the possibilities of the smart factory concept must also be integrated in this industrial sector. Thus, heat treatment comes a significant step closer to the goal of a CO2-neutral process in terms of Scopes 1, 2, and 3 regarding emissions under the given boundary conditions.
References
[1] Karl-Wilhelm Wegner, “Werkstoffentwicklung für Schmiedeteile im Automobilbau,” ATZ Automobiltechnische Zeitschrift 100, (1998): 918–927, https://doi.org/10.1007/BF03223434. [2] Wolfgang Bleck and Elvira Moeller, Steel Handbook (Carl Hanser Verlag GmbH & Co. KG, 2018). [3] Wolfgang Köppel, Charlotte Degünther, and Jakob Wachsmuth, “Assessment of upstream emissions from natural gas production in Germany,” Federal Environment Agency (January 2018): https://www.umweltbundesamt.de/publikationen/bewertung-der-vorkettenemissionen-beider. [4] Klaus Buchner and Johanes Uhlig, “Discussion on Energy Saving and Emission Reduction Technology of Heat Treatment Equipment,” Berg Huettenmaenn Monatsh 168 (2021): 109–113, https://doi.org/10.1007/s00501-023-01328-5. [5] Technologie der Abwärmenutzung. Sächsische Energieagentur – SAENA GmbH, 2. Auflage, 2016. [6] Brandstätter, R.: Industrielle Abwärmenutzung. Amt der OÖ Landesregierung, 1. Auflage, 109–113, https://doi.org/10.1007/s00501 02301328-5. [7] U. Wyss, “Verbrauch an Trägergas bei der Gasaufkohlung,” HTM Journal of Heat Treatment Materials 38, no. 1 (1983): 4-9, https://doi.org/10.1515/htm-1983-380102.
About the Author
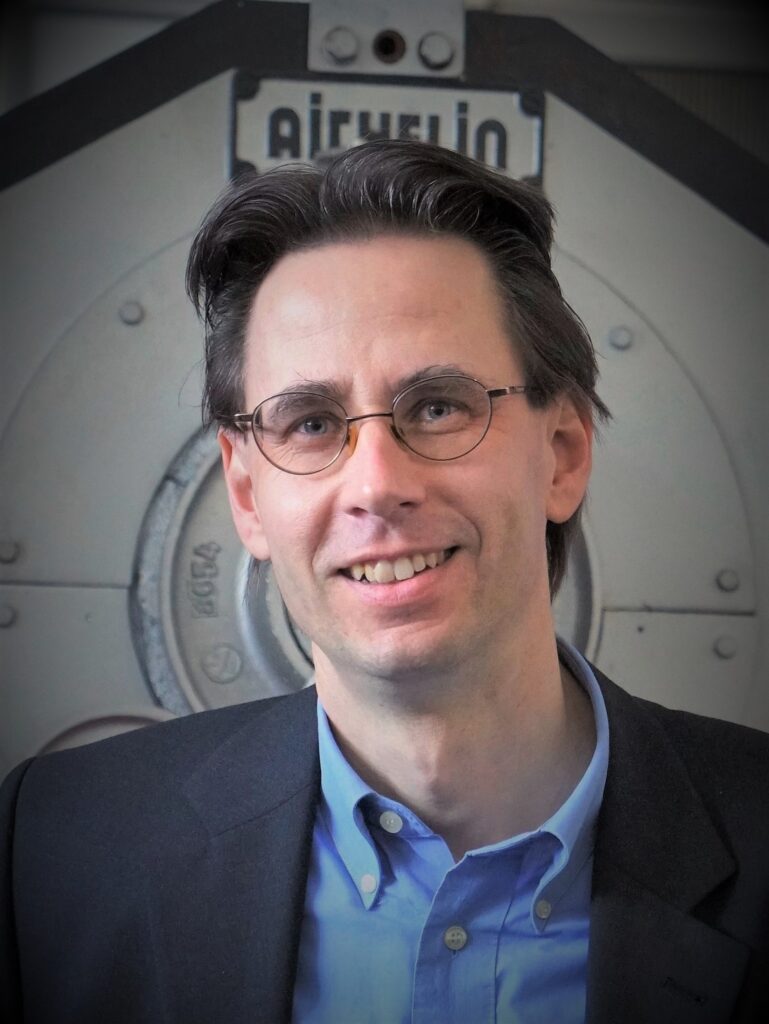
Dr. Klaus Buchner
Head of Research and Development
AICHELIN HOLDING GmbH
Klaus Buchner holds a doctorate and is the head of research and development at AICHELIN HOLDING GmbH. This article is based on Klaus Buchner’s article, “Reduktion des CO2-Fußabdrucks in der Wärmebehandlung” in Prozesswärme 01-2023 (pp. 42-45).
For more information: Klaus at klaus.buchner@aichelin.com.
This article content is used with the permission of heat processing, which published this article in 2023.
Find Heat Treating Products And Services When You Search On Heat Treat Buyers Guide.Com
When processing cemented carbide, there are a few considerations you need to understand to use the proper sintering equipment. One of the biggest factors is the actual material; what is the colbalt content level of the processed material?
In this best of the web article, walk through the steps of dewaxing, sintering for appropriate densification, and the processing temperatures that are required for sintering cemented carbide.
An Excerpt:
“Other than mechanical stresses due to the differential pressure between inside and ambient pressure outside the furnace, operating at relatively high temperatures with high pressure of gas would lead to significant dissipations of heat to the external environment. This is not only anti-economic from an efficiency point of view, but could also compromise the structural integrity of the water-cooled steel vessel of the furnace by overheating it.”