Precise heat treating is essential to enable components to withstand space exploration. In this Technical Tuesday, Mike Grande, vice president of Sales at Wisconsin Oven Corporation, discusses the role of aluminum solution treatment and aluminum aging in heat treating space exploration components.
This column was first released in Heat Treat Today March 2024 Aerospace Heat Treatprint edition.
Contact us with your Reader Feedback!
In space exploration, the various parts, electronic components, and materials used to make the rockets, crew capsules, rovers, and other equipment, are subjected to brutal extremes of temperature, vacuum, and radiation. In order to withstand these extreme environments without failure, the parts must be manufactured to very tight tolerances and precisely heat treated. Therefore, convection heat treatment emerges as a critical process in the manufacturing of space exploration components and materials, offering tight control over temperature profiles and the microstructure of materials.
Heat treatment involves heating a material to a specific temperature, holding it at that temperature for a certain duration, and then cooling it down at a controlled rate, which can be rapid or gradual, depending on the objective. The purpose of heat treatment is to improve the material’s mechanical properties, such as strength, ductility, and toughness. Probably the most common metal used in space exploration is aluminum. It is an excellent choice for spacecraft components because it is lightweight, durable, and has excellent thermal conductivity, which is necessary for components that need to dissipate heat.
The first stage of the Falcon 9, for example, utilizes four legs used during landing. They are manufactured from an extremely light, rigid, aluminum honeycomb material that also contains carbon fiber and has a very high strength to weight ratio. Another aluminum component common in space exploration is gas transfer tubes, used to transfer gases, such as methane, between chambers in the interior of rocket propulsion systems. Additionally, there are composite overwrapped pressure vessels (COPVs), which carry compressed fuels such as hydrogen and oxygen, among other gases. These are made of an aluminum tank covered with filament-wound, resin-impregnated composite material, which forms an extremely robust structure capable of withstanding the high pressures created by compressed gases and the rigors of high-speed propulsion. For aluminum to be useful in space applications, it must be heat treated to give it the strength and durability required.
Aluminum Solution Treatment
Since aluminum has such widespread use in space exploration, aluminum heat treatment plays a central role in this industry, with solution treatment and aging being the most common heat treatments utilized. All aluminum materials that require high strength are solution heat treated, then subsequently aged, in two separate heat treat processes. The purpose of solution heat treatment is to evenly dissolve the alloys contained in the aluminum, such as manganese, magnesium, copper, zinc, and silicon, and then rapidly quench it to retain the grain structure. The aluminum alloy is heated and held at a temperature of 800°F to 1000°F (420°C to 540°C), which is just below its melting point. The aluminum is then quenched in water or a water/glycol mixture quickly (within 7 to 15 seconds) to essentially “freeze” the microstructure before the alloying elements can redistribute themselves.
Aluminum Aging
After quenching, aluminum is precipitation hardened. Also known as artificial aging, this process involves heating the aluminum at a lower temperature, typically in the range of 200°F to 400°F (93°C to 204°C) for several hours. This final process dramatically increases the hardness, yield strength, and ultimate strength of the aluminum, making it suitable for use in space applications.
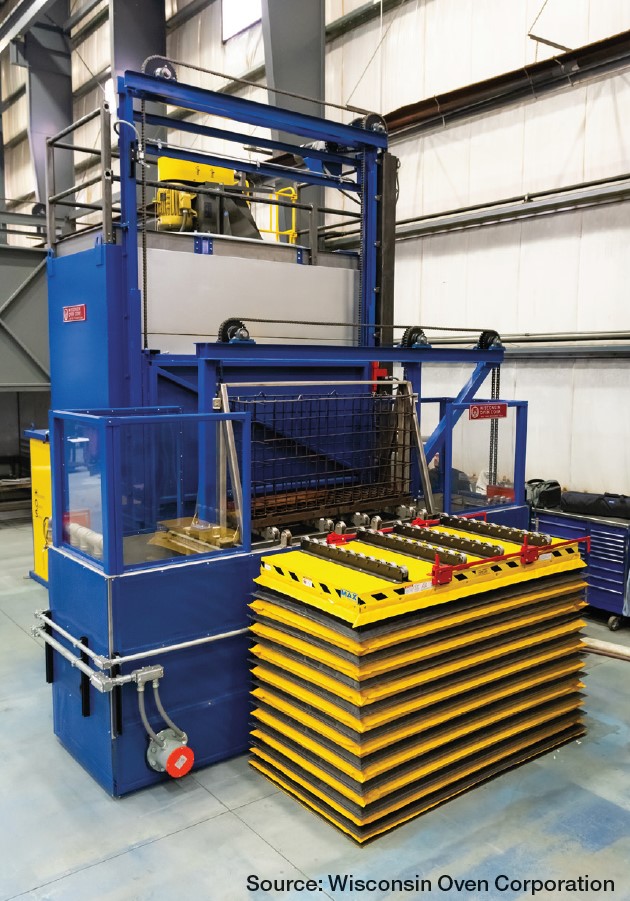
A solution treatment system for processing aluminum
The above is just a sample of the many types of heat treatments for materials used in space exploration. Other examples are annealing, tempering, normalizing, and hydrogen embrittlement relief, to name a few. In conclusion, heat treatment plays a critical role in the manufacturing of parts used in space exploration and is essential to the reliability and safety of space missions.
About the Author
Mike Grande,
Vice President
of Sales,
Wisconsin Oven
Corporation
Mike Grande has a 30+ year background in the heat processing industry, including ovens, furnaces, and infrared equipment. He has a BS in mechanical engineering from University of Wisconsin-Milwaukee and received his certification as an Energy Manager (CEM) from the Association of Energy Engineers in 2009. Mike is the vice president of Sales at Wisconsin Oven Corporation.
For more information: Contact sales@wisoven.com.
Find Heat Treating Products And Services When You Search On Heat Treat Buyers Guide.Com
Watch this video message from Bethany Leone, editor at Heat Treat Today, to learn how to nominate a rising young leader to Heat Treat Today’s 40 Under 40!
Who To Nominate
A young person working for a manufacturer with in-house heat treat (excellent!), or a colleague/yourself working in the heat treat industry
Based in North America
40 years old or younger at some point in the nomination year
Models excellent heat treat knowledge/abilities
Evidences significant accomplishments/contributions to the industry
Demonstrates leadership skills and character
How To Nominate – 3 EASY STEPS
Each nomination should take 10 minutes. Multiple nominations are allowed. Nominate your customer and be recognized as their sponsor. Points!!
Click to nominate!
1. Share nominee information:
current job title and employer
contact email
Optional: years in the heat treat industry and year of birth
2. Share why they stand out through concrete benchmarks/descriptions of their leadership. The best things to include are:
Leadership qualities and character
Evidence of initiative and/or accomplishments
Evidence of contributions to the industry
Demonstrable evidence of having positions of leadership and/or is on a leadership track
NGC Gears, a manufacturer of wind power gearboxes, has completed the installation of two additional Endothermic generators from a manufacturer with North American locations.
UPC-Marathon, a Nitrex company, installed the Endo generators at NGC Gears‘ its new facility in Jinhu, China. This acquisition brings the total of generator sets to five since 2022, collectively generating an impressive 800 m³/h (22,252 ft3/h) capacity of Endothermic gas supplied to carburizing and hardening furnaces used for processing various gear components. The latest installations in February and March of 2024 support the heat treating operations of the company’s wind energy gearbox production.
NGC’s decision to expand capacity is in response to the growing demand for wind power solutions in China and globally. The new Endothermic gas generating systems will significantly enhance the company’s production capabilities, enabling NGC to meet increasing market needs with greater efficiency and reliability.
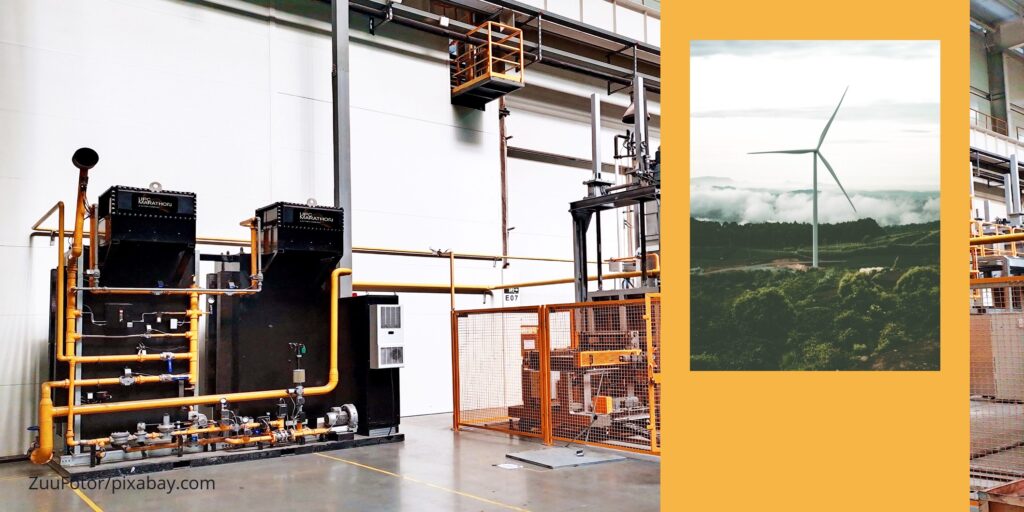
EndoFlex generators from UPC-Marathon (Source: Nitrex)
EndoFlex offers precise control of production media to the carburizing and hardening environments, leading to higher quality gear production with improved longevity and performance. The result is improved carburizing and hardening processes, higher-quality hardened gears, reduced operating costs, and increased efficiency, as well as immediate cost savings through reduced electricity and gas consumption and minimized waste.
Johnny Xu, general manager at UPC-Marathon China, shared, “The latest EndoFlex investments align with NGC’s development of low-consumption, high-efficiency gearbox products for large-scale onshore and offshore wind turbines.”
This press release is available in its original form here.
EcoTitanium, a European plant for recycling and refining titanium alloys for critical applications, was opened in France in 2017. It was the first plant in Europe to melt titanium with a cold hearth furnace – a technology that allows users to recycle titanium reverts coming from forging and machining castings from the aerospace supply chain.
The SECO/WARWICK Group was chosen as the main supplier of advanced vacuum metallurgy technology for this strategic European project, securing the creation of an autonomous European titanium channel.
Sławomir Tomaszewski, director of the Vacuum Melting Furnaces Team in the SECO/WARWICK Group, comments, “The innovative VAR furnace will increase the Partner’s production capacity and can respond to the increased demand for titanium in Europe. EcoTitanium has created the first integrated titanium processing plants in Europe, which opens the door to European, ecological, and innovative solutions for the aerospace industry. We are glad that our Group is part of this strategic project and that Retech and SECO/WARWICK brand solutions constitute the core of the machine park.”
Earl Good Managing Director Retech Systems, LLC Source: Retech
“For EcoTitanium, we, as Retech and SECO/WARWICK, delivered two furnaces seven years ago: a plasma furnace (PAM) for consolidation and refining of titanium scrap using plasma torches operating in an inert gas atmosphere, and a VAR arc furnace for further refining of titanium ingots obtained from the PAM furnace. The current contract is a continuation of this project. We will deliver a second VAR furnace, which will significantly increase the Partner’s processing capabilities,” said Earl Good, managing director of Retech.
The new furnace’s advantage is its perfect fit into the customer’s existing infrastructure. For safe operation, VAR furnaces require complex construction work: a bunker, an explosive tunnel, as well as a dedicated control room located outside the furnace operating area.
This system is unique because current solutions in the field of furnace safety will be implemented at the design stage. These solutions result from both the experience gained by EcoTitanium and the SECO/WARWICK Group’s experience.
Source: SECO/WARWICK
“The delivery of this new VAR furnace will help us to secure our customer’s growing needs for producing titanium in the context of unprecedented production ramp-ups. We are pleased to open this new chapter of EcoTitanium’s history with our long-term partner SECO/WARWICK. SECO/WARWICK has indeed offered us best-in-class solutions in the field of vacuum metallurgy technology, in particular with its PAM systems from its Retech brand, which allows us to use around 75% of recycled materials and to divide by up to four the CO2 emissions created by titanium melting,” says Jean-François Juéry, president of EcoTitanium.
Titanium, a transition metal with unique properties, is valued for its strength-to-weight ratio. It has comparable durability to steel but is 50% lighter, making it an attractive choice for industries looking for strength without additional weight. The aerospace industry consumes over 30% of global demand, and the chemical sector another 40%. Additionally, titanium has found use in medicine, especially in joint replacement procedures, dental implants, and electronics.
This press release is available in its original form here.
The amazing materials that are produced through additive manufacturing (AM) and 3D machining often require post-processing heat treatments before these become final components that launch into space. What are the trends of AM/3D outside our planet, and what technical resources are available to you as you make one step into this field? This original content piece from the Heat Treat Today editors will help you understand where technology stands in 2024.
Why Does AM/3D Go to Space?
Contact us with your Reader Feedback!
A broad spectrum of industries have found the appeal of additively manufactured parts, industries ranging from mining to medical and automotive to space. Much of this has to do with complexity of components that new engineering techniques require, the desire to save on material costs, and the ability to condense lead time. For some, additive manufacturing is becoming essential to the space industry; as Tobias Brune, head of the Business Unit Additive Manufacturing at TRUMPF, has commented, “With our 3D printing technology, we are driving the commercialization of the space-travel industry. If you want to be successful in the space-travel industry today, you have to use additive manufacturing.”
When should you expect this transition? Now.
In January of this year (2024), the first metal 3D printer for space was launched to the Columbus module of the International Space Station (ISS). This is a very active, integrated sense of seeing AM in the aerospace industry, and test runs with this equipment will ensue.
Flight model of 3D Metal Printer Launched on NG-20 Source: ESA
The Exploration Company in Europe plans to use 3D printers from TRUMPF (laser specialist) to print core components in engines for spacecrafts. The intent: missions in Earth’s orbit and to the moon.
Heat Treat & thermal Processing Requirements of Post-ProcessingAM
If you are going to get involved in AM, it is essential to have the right equipment. One of the most talked about equipment is hot isostatic pressing (HIP) technology. Often, heat treat operations use HIP equipment for post-process heat treating in order to get the solid part they desire. For the most part, commercial heat treaters have positioned themselves to handle the R&D required to navigate the terrain of overcoming processing challenges of new/complex parts and creating standardizations. However, privateR&D facilities and departments are also building out their capabilities to handle AM in HIP.
However, so also have vacuum furnaces been a key leader in heat treating AM components. Here, commercial heat treaters have also made moves to expand their equipment/process offerings to accommodate AM parts.
So also do atmosphere considerations need to be considered, withgasses like H2 competing trying to capture the limelight.
Continue the Exploration: AM/3D Articles for Space
Looking for an introduction to the AM/3D topic for heat treaters? Begin with this article by Animesh Bose, an engineering pioneer: “The Role Of Heat Treat in Binder Jetting AM for Metals.” The article uncovers the history of one of the most important types of AM/3D manufacturing — binder jetting AM.
Then, take a step over for an industry focus on what “heat treatments for space” look like. Mike Grande eloquently summarized the current processes needed in space in this editorial from the March 2024 Aerospace print edition. Read “The Role of Heat Treatment in Space Exploration” in the digital edition of the magazine.
In-house or commercial? This article presents critical considerations of space components — with a particular emphasis on the importance of AM/3D — when considering how to grow your processing expertise and capabilities. Several examples from the frontlines of R&D are presented by Noel Brady in his article. Read the editorial, “Thermal Processing for Space and Additive Manufacturing,” for excellent illustrations.
Finally, hone in on the topic with a case study about developments in HIP technology for space component post-processing. This article begins with context confronting issues of structural integrity, especially of complex space components, with HIP. Andrew Cassese gets to the case study towards the end of his article, “High Pressure Prepares Parts for Space.”
Find Heat Treating Products And Services When You Search On Heat Treat Buyers Guide.Com
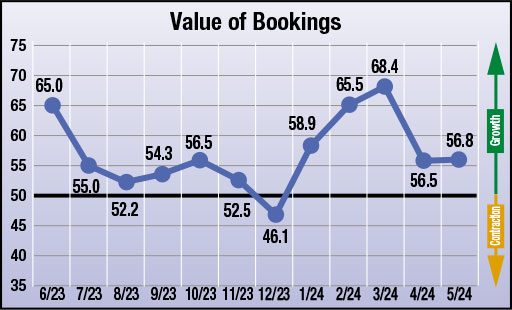
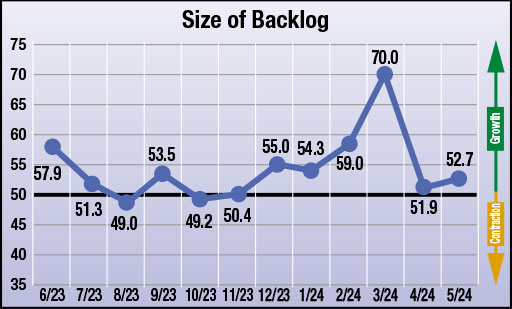
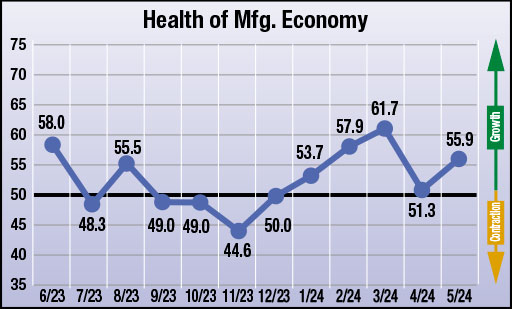
The four heat treat industry-specific economic indicators, gathered by Heat Treat Today each month since June 2023, indicate expectations for economic growth in May compared to what suppliers experienced in April. However, while growth is still expected, it appears that most suppliers are more tame in their projections for growth across most indicators.
The numbers, which were compiled in the second week of May, show that responding parties strongly anticipate all four indices — number of inquiries, value of bookings, size of backlogs, and health of manufacturing economy — to grow. Again this is growth as is compares to the previous month (April). One specific indicator does stand out, though: Manufacturers are expecting significant growth in number of inquiries.
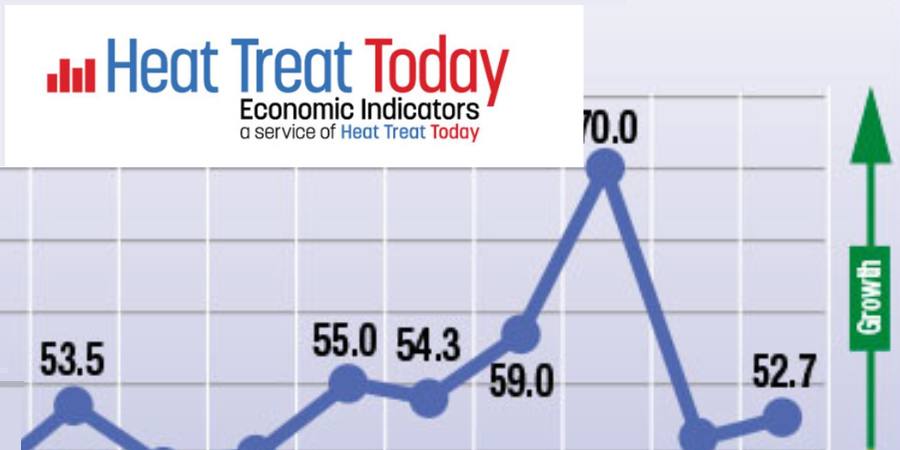
The results from this month’s survey (May) are as follows; numbers above 50 indicate growth, numbers below 50 indicate contraction, and the number 50 indicates no change:
Anticipated change in the Number of Inquiries from April to May: 61.5
Anticipated change in Value of Bookings from April to May:56.8
Anticipated change in Backlog Size from April to May: 52.7
Anticipated change in the Health of the Manufacturing Economy from April to May: 55.9
Data for May 2024
The four index numbers are reported monthly by Heat Treat Today and made available on the website.
Heat TreatToday’sEconomic Indicatorsmeasure and report on four, heat treat industry indices. Each month, approximately 800 individuals who classify themselves as suppliers to the North American heat treat industry receive the survey. Above are the results. Data started being collected in June 2023. If you would like to participate in the monthly survey, please click here to subscribe.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Readers are checking out Heat Treat Today’smagazine from March/April 2024. The annualAerospaceprint edition has a piece that sparked a comment from a reader. The letter from the publisher Doug Glenn entitled “Is It Time To Rethink the ‘Quality’ Movement?” discusses the current state of the quality movement.
Would you like to weigh in on the topic? Submit your question, comments, thoughts, or queries here or email Bethany Leone at editor@heattreattoday.com.
Here is an excerpt from the publisher’s page:
“One of the first thoughts I remember having about the corporate quality initiative I was involved with was the distinct lack of a definition of what ‘quality’ really meant. For many of the standards, they did not really care what you did (whether or not you did quality work), they just wanted you to prove you had documented your work, that your people knew said documentation existed, and they were following the processes you had described in documentation.”
This publisher’s page prompted this feedback from Jorg Demmel, founder, owner, and president of High Temperature Concept:
“There is one thing I’d like to ask you, because I just read your publisher letter. I like it, although the situation you describe is not ‘quality’ in my mind. It’s a great discussion, which is worth it!
“It’s, in my mind, an oversubscription of quality management and it’s industry. That’s something different than quality. I don’t like these guys called ‘auditors’. Some (or many) never learned what means ‘operational quality’.
“Did you know that e.g. an iso 9001 certified company doesn’t have to follow the iso 9001 10 chapters in their QM handbook. Or, that not all suppliers have to be rated. Or, that internal audits don’t have to be bureaucratic and elaborative. Etc.
“Conclusion: a QM system is only as good as it is based on the people on the shop floor, their motivation, experience and attitude, and the leadership commitment. I guess I missed something 😉.”
We welcome your inquiries to and feedback on Heat Treat Today articles. Submit your questions/comments to editor@heattreattoday.com.
The future of heat treating requires new manufacturing solutions like robotics that can work with modular design. Yet so also does temperature monitoring need to be seamless to know how effectively your components are being heat treated — especially through being quenched.In this Technical Tuesday,learn more abouttemperature monitoring through the quench process.
Gas Carburization
Contact us with your Reader Feedback!
Carburizing has rapidly become one of the most critical heat treatment processes employed in the manufacture of automotive components. Also referred to as case hardening, it provides necessary surface resistance to wear, while maintaining toughness and core strength essential for hardworking automotive parts.
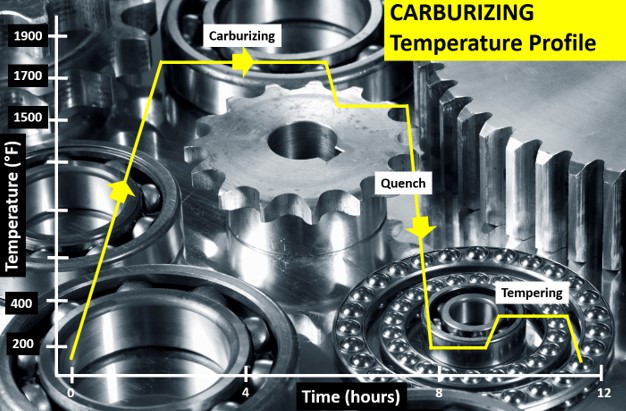
Figure 1. Typical carburizing heat treat temperature profile showing the critical temperature/time steps: (i) carburization, (ii) quench, and (iii) temper. (Source: PhoenixTM)
The carburizing process is achieved by heat treating the product in a carbon rich environment (Figure 1), typically at a temperature of 1562°F–1922°F (850°C–1050°C). The temperature and process time significantly influence the depth of carbon diffusion and other related surface characteristics. Critical to the process is a rapid quenching of the product following the diffusion in which the temperature is rapidly decreased to generate the microstructure, giving the enhanced surface hardness while maintaining a soft and tough product core.
The outer surface becomes hard via the transformation from austenite to martensite while the core remains soft and tough as a ferritic and/or pearlitic microstructure. Normally, carburized microstructures following quench are further tempered at temperatures of about 356°F (180°C) to transform some of the brittle martensite into tempered martensite to enhance ductility and grindability.
Critical Process Temperature Control
As discussed, the success of carburization is dependent on accurate, repeatable control of the product temperature and time at that temperature through the complete heat treatment process. Important to the whole operation is the quench, in which the rate of cooling (product temperature change) is critical to achieve the desired changes in microstructure, creating the surface hardness. It is interesting that the success of the whole heat treat process can rest on a process step which is so short (minutes), in terms of the complete heat teat process (hours). Getting the quench correct is not only essential to achieve the desired metal microstructure, but also to ensure that the physical dimensions and shape of the product are maintained (no distortion/warping) and issues such as quench cracking are eliminated.
Obviously, as the quench is so critical to the whole heat treat process, the correct quench selection needs to be made to achieve the optimum properties with acceptable levels of dimensional change. Many different quenchants can be applied with differing quenching performances. The rate of heat transfer (quench rate) of quench media in general follows this order from slowest to quickest: air, salt, polymer, oil, caustic, and water.
Technology Challenges for Temperature Monitoring
When considering carburization from an industry standpoint, furnace heat treat technology generally falls into one of two camps, embracing either air quench (low pressure carburization) or oil quench (sealed gas carburization/LPC with integral or vacuum oil quench). Although each achieves the same end goal, the heat treat mechanisms and technologies employed are very different, as are the temperature monitoring challenges.
To achieve the desired carburized product, it is necessary to control and hence monitor the product temperature through the three phases of the heat treat process. Conventionally, product temperature monitoring would be attempted using the traditional trailing thermocouple method. For many modern heat treat processes including carburization, the trailing thermocouple method is difficult and often practically impossible.1 The movement of the product or product basket from stage to stage, often from one independent sealed chamber to another (lateral or vertical movement), makes the monitoring of the complete process a significant challenge.
With the industry driving toward fully automated manufacturing, furnace manufacturers are now offering the complete package with full robotic product loading that includes shuttle transfer systems and modular heat treat phases to process both complete product baskets and single piece operations. Although trailing thermocouples may allow individual stages in the process to be measured, they cannot provide monitoring of the complete heat treat journey. Testing is therefore not under true normal production conditions, and therefore is not an accurate record of what happens in normal day to day operation.
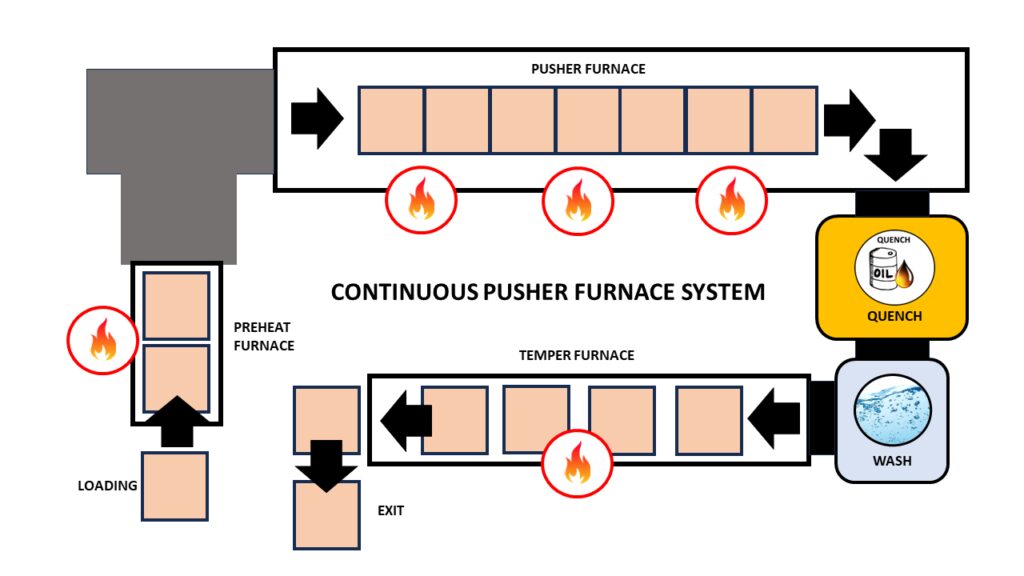
Figure 2 shows schematic diagrams of two typical carburizing furnace configurations that would not be possible to monitor using trailing thermocouples. The first shows a modular batch furnace system where the product basket is transferred between each static heat treat operation (preheat, carburizing furnace, cooling station, quench, quench wash, temper furnace) via a charge transfer cart. The second shows the same heat treat operation but performed in a continuous indexed pusher furnace configuration where the product basket moves sequentially through each heat treat operation in a semi-continuous flow.
Thru-process temperature monitoring as a technique overcomes such technical restrictions. The data logger is protected by a specially designed thermal barrier, therefore, can travel with the product through each stage of the process measuring the product/process temperature with short, localized thermocouples that will not hinder travel. The careful design and construction of the monitoring system is important to address the specific challenges that different heat treat technology brings including modular batch and continuous pusher furnace designs (Figure 2).2
The following section will focus specifically on monitoring challenges of the sealed gas carburizing process with integral oil quench. Technical challenges of the alternative low pressure carburizing technology with high pressure gas quench have previously been discussed in an earlier publication.3
Monitoring Challenges of Sealed Gas Carburization — Oil Quench
Figure 3. “Thru-process” temperature monitoring system for use in a sealed carburizing furnace with integral oil quench — (3.1) Monitoring system entering furnace with thermocouple fixed to automotive gears, product test pieces (3.2) System exiting oil quench tank (3.3) System inserted into wash tank with product basket (Source: PhoenixTM)
Presently, the most common traditional method of gas carburizing for automotive steels is often referred to as sealed gas carburizing. In this method, the parts are surrounded by an endothermic gas atmosphere. Carbon is generated by the Boudouard reaction during the carburization process, typically at 1562°F–1832°F (850°C –1000°C). Despite the dramatic appearance of a sealed gas carburizing furnace, with its characteristic belching flames (Figure 3), from a monitoring perspective, the most challenging aspect of the process is not the heating, but the oil quench cooling. For such furnace technology, the historic limitation of “thru-process” temperature profiling has been the need to bypass the oil quench and wash stations, missing a critical process step from the monitoring operation. Obviously, passing a conventional hot barrier through an oil quench creates potential risk of both system damage from oil ingress and barrier distortion, as well as general process safety. However, the need to bypass the quench in certain furnace configurations by removing the hot system from the confined furnace space could create significant operational challenges, from an access and safety perspective.
Monitoring of the quench is important as ageing of the oil results in decomposition (thermal cracking), oxidation, and contamination (e.g. water) of the oil, all of which degrade the viscosity, heat transfer characteristics, and quench efficiency. Control of physical oil temperature and agitation rates is also key to oil quench performance. Quench monitoring allows economic oil replacement schedules to be set, without risk to process performance and product quality.
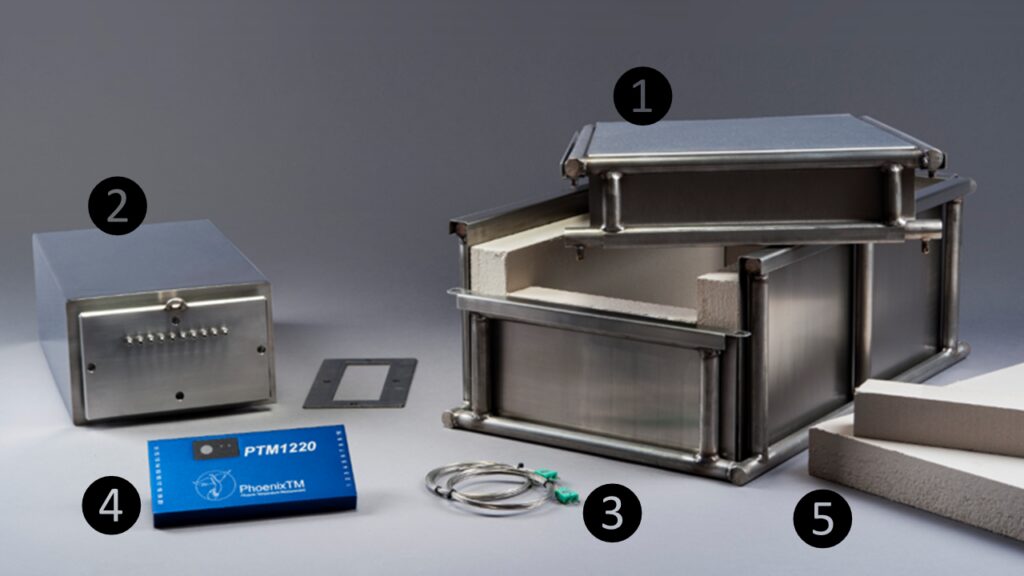
Figure 4. “Thru-process” temperature monitoring system oil quench compatible thermal barrier design: (1) Robust outer structural frame keeping insulation and inner barrier secure; (2) Internal thermal barrier — completely sealed with integral microporous insulation protecting data logger; (3) Mineral insulated thermocouples sealed in internal thermal barrier with oil tight compression fitting; (4) Multi-channel high temperature data logger; and (5) Sacrificial insulation blocks replaced after each run.
(Source: PhoenixTM)
To address the process challenges, a unique thermal barrier design has been developed that both protects the data logger in the furnace (typically three hours at 1697°F/925°C) and also protects during transfer through the oil quench (typically 15 mins) and final wash station (Figure 3). The key to the barrier design is the encasement of a sealed inner barrier with its own thermal protection with blocks of high-grade sacrificial insulation contained in a robust outer structural frame (Figure 4).
Quench Cooling Phases
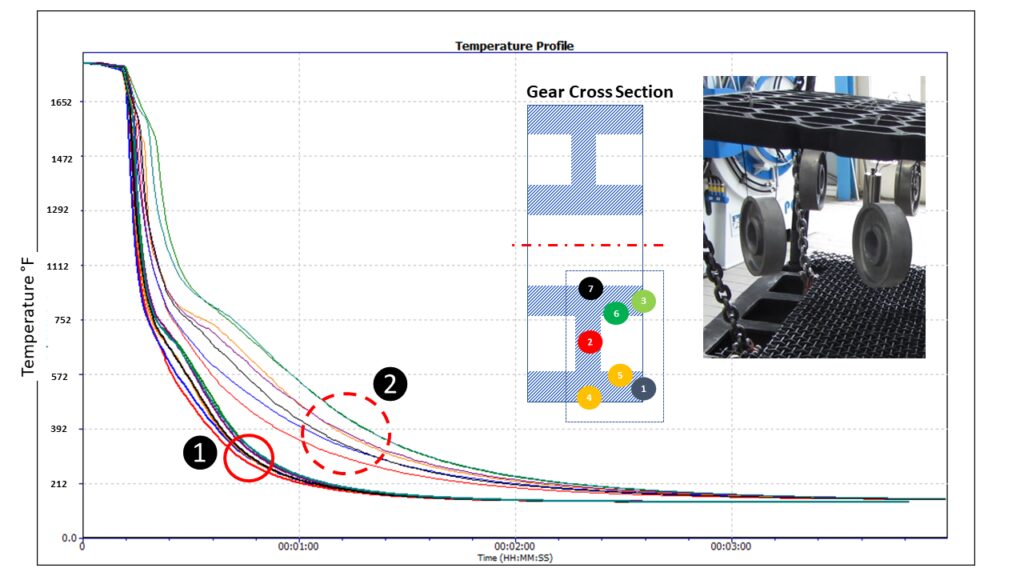
Monitoring the oil quench in carburization gives the operator a unique insight into the product’s specific cooling characteristics, which can be critical to allow optimal product loading and process understanding and optimization. From a scientific perspective, the quench temperature profile trace, although only a couple of minutes in duration, is complex and unique. From a zoomed in quench trace (Figure 5) taken from a complete carburizing profile run, the three unique heat transfer phases making up the oil quench cool curve can be clearly identified:
Figure 5. Oil quench temperature profile for different locations on an automotive gear test piece shows the three distinct heat transfer phases: (1) film boiling “vapor blanket”, (2) nucleate boiling, and (3) convective heat transfer. (Source: PhoenixTM)
Film boiling “vapor Blanket”: The oil quenchant creates a layer of vapor (Leidenfrost phenomenon) covering the metal surface. Cooling in this stage is a function of conduction through the vapor envelope. Slow cool rate since the vapor blanket acts as an insulator.
Nucleate boiling: As the part cools, the vapor blanket collapses and nucleate boiling results. Heat transfer is fastest during this phase, typically two orders of magnitude higher than in film boiling.
Convective heat transfer: When the part temperature drops below the oil boiling point. the cooling rate slows significantly. The cooling rate is exponentially dependent on the oil’s viscosity.
From a heat treat perspective, the quench step relative to the whole process (hours) is quick (seconds), but it is probably the most critical to the performance of the metallurgical phase transitions and achieving the desired core microstructure of the product without risk of distortion. By being able to monitor the quench step, the process can be validated for different products with differing size, form, and thermal mass. As shown in Figure 6, the quench curve profile over the three heat transfer phases is very different for two different automotive gear sizes.
Figure 6. Oil quench temperature profile for different automotive gear sizes (20MnCr5 case hardening steel) with different thermal masses: Passenger Car Gear (2.2 lbs) and Commercial Vehicle Gear (17.6 lbs) (Source: PhoenixTM)
Summary
As discussed in this article, one of the key process performance factors associated with gas carburization is the control and monitoring of the product quench step. Employing an oil quench, the measurement of such operation is now very feasible as part of heat treat monitoring. Innovations in thru-process temperature profiling technology offer specific system designs to meet the respective application challenges.
References
[1] Dr. Steve Offley, “The light at the end of the tunnel – Monitoring Mesh Belt Furnaces,” Heat Treat Today, February 2022, https://www.heattreattoday.com/processes/brazing/brazing-technical-content/the-light-at-the-end-of-the-tunnel-monitoring-mesh-belt-furnaces/.
[2] Michael Mouilleseaux, “Heat Treat Radio #102: Lunch & Learn, Batch IQ Vs. Continuous Pusher, Part 1,” interviewed by Doug Glenn, Heat Treat Radio, October 26, 2023, audio, https://www.heattreattoday.com/media-category/heat-treat-radio/heat-treat-radio-102-102-lunch-learn-batch-iq-vs-continuous-pusher-part-1/.
[3] Dr. Steve Offley, “Discover the DNA of Automotive Heat Treat: Thru-process Temperature Monitoring,” Heat Treat Today, August 2023, https://www.heattreattoday.com/discover-the-dna-of-automotive-heat-treat-thru-process-temperature-monitoring/.
About the Author
Dr Steve Offley (“Dr O”), Product Marketing Manager, PhoenixTM
Dr. Steve Offley, “Dr. O,” has been the product marketing manager at PhoenixTM for the last five years after a career of over 25 years in temperature monitoring focusing on the heat treatment, paint, and general manufacturing industries. A key aspect of his role is the product management of the innovative PhoenixTM range of thru-process temperature and optical profiling and TUS monitoring system solutions.
An automotive manufacturer in South America has recently placed a follow-up order for a second Endothermic generator from a manufacturer of industrial process control, automation, and digitalization solutions with North American locations.
UPC-Marathon, a Nitrex company, installed a 200 m³/h EndoFlex unit last year. The new generator, with a similar capacity, aims to enhance stability, to ensure consistent composition and gas flows, and to prioritize quality of automotive gear boxes while achieving efficiencies in heat treatment operations.
UPC-Marathon EndoFlex unit (Source: Nitrex)
Prior to adopting the EndoFlex solution, the manufacturer relied on four generator units, each with a capacity of 70 m³/h and consuming 80 kW of power. With the same 80 kW of power consumption, the EndoFlex generator delivers a 200 m³/h capacity.
This transition to the new unit represents a 75% reduction in power consumption and a contribution to operational efficiency and sustainability efforts. The new generator streamlines maintenance procedures, adheres to stringent quality standards, and reduces CO2 emissions. Control over gas quality and production for the neutral hardening furnace enhances product quality, reduces operating costs, and optimizes energy consumption. By automatically adjusting gas production to match real-time furnace demand, the generator eliminates overproduction and waste.
Marcio Boragini Sales Director for Brazil at UPC-Marathon
“We’re proud to continue our partnership with this automotive customer,” remarked Marcio Boragini, UPC-Marathon’s Sales Director for Brazil. “Moreover, EndoFlex . . . empower[s] the manufacturer to achieve their business objectives fast, while reinforcing our commitment to [drive] success together.”
This press release is available in its original form upon request.