We’re celebrating getting to the “fringe” of the weekend with a Heat Treat Fringe Fridaycovering news about a metals company enhancing its processing line with an atomizer, increasing its capability to produce metal powders for the advanced manufacturing industries that it serves. Atomization, a process that forces molten metal into a controlled environment through a nozzle at high pressure, improves sustainability and efficiency in metals production for industries such as aerospace, medical and defense.
While not exactly heat treat, “Fringe Friday” deals with interesting developments in one of our key markets: aerospace, automotive, medical, energy, or general manufacturing.
A multinational metals company recently bolstered its processing line by adding an atomizer for the production of metal powders. The atomizer will be installed at one of the company’s U.S. production facilities and is capable of producing a wide variety of metal powders, optimized for both throughput and maintenance.
Retech, a division of SECO/WARWICK Group and a pioneer in advanced metallurgical equipment, has announced the procurement and the delivery and installation of the advanced manufacturing equipment to the metals manufacturer.
Earl Good Managing Director Retech
“We stuck with them,” said Earl Good, president and managing director at Retech. “We maintained the response times they needed, going above and beyond. This level of dedication was crucial in meeting their ambitious timeline, from RFQ to turnkey execution.”
The atomizer system is designed to be highly efficient, reducing operational costs and environmental impact. The system’s all-electric process ensures zero carbon emissions, aligning with sustainable production practices, and the inert gas recovery and recycling enhances resource efficiency and reduces waste. Maintenance features allow for rapid changeover between heats, minimizing downtime.
The press release is available in its original form here.
Refractories, “the unsung hero of the manufacturing process,” can’t measure up to that moniker if their superpowers are worn down and not getting due maintenance. Guest columnist Pamela Gaul, director of marketing at Plibrico Company, LLC, examines the critical role the refractory lining plays in the success of manufacturing aluminum, why a refractory is susceptible to cracking under extreme conditions, and how to select and prepare refractory linings to achieve a longer service life.
Read more Maintenance columns in previousHeat Treat Today’s issues here.
As the old saying goes, “An ounce of prevention is worth a pound of cure.” This is certainly true when it comes to your refractories.
Manufacturers around the world rely on refractories to safeguard their multi-million dollar industrial-grade boilers, incinerators and furnaces from thermal damage and corrosion brought on by operating temperatures that can reach 3000°F (1650°C).
Without refractories — the unsung hero of the manufacturing process — it would be impossible to process the raw materials that go into automobiles, chemicals, power-generation equipment, buildings, roads and much more. As such, it only makes good financial and business sense to provide basic refractory maintenance for your machinery. By protecting your critical heat-processing equipment, you can minimize costly downtime, reduce energy losses, prevent employee injuries and, more importantly, avert a catastrophic equipment failure.
Given refractories’ importance to operations, it is important to remember that they are consumables and will wear out. This is significant because without proper maintenance your processing equipment may fail at the most inopportune time, and downtime for a furnace or dryer — even one day — can cost a company hundreds or thousands of dollars. The rewards of proper maintenance far outweigh the expense.
It is also important to remember that refractories are not commodities. Even within the general classification of refractories, there are significant variances in chemical compositions. As a result, refractories will have different maintenance schedules and repair practices.
Refractory maintenance has a cost. That is why maintenance needs must be factored in when evaluating which refractories to install in your application. For example, the upfront costs of engineered shapes may be 20-30% more than monolithic refractories. However, they require little to no dryout, are easy to install and in some cases last longer than some traditional castables. Also, if there are high-wear areas that may be difficult to reach due to their location or geometry, financially it is well worth going with the precast shapes to minimize future maintenance expense.
The Wear Factor
What causes refractories to wear? Time, temperature, corrosive gases, slag and operational practices will all take their toll, as will the overall engineering of the heat-processing equipment. Other culprits leading to the degradation of a refractory lining can be incorrect combustion controls, improper flame set-up, anchor failure or thermal shock resulting from severe temperature fluctuations. More times than not it is a combination of these or other factors that lead to refractory damage — not a single cause.
Not following the manufacturer’s recommended curing and dryout schedule can also lead to degradation. If an end-user is looking to accelerate the process due to production demands, quick dryout products might be a good option.
Some manufacturers offer refractory materials that provide reductions in dryout time and may offer nearly the same properties as their traditional, non-fast dryout counterparts. The benefit to these quick-cure/dryout products are that dryout times are cut about in half, which can represent a time savings of up to 40-50 hours. While they offer an easy, time-saving solution, however, there are limitations to their material properties as well as cautions on dryout.
It is a good idea to use the dryout time to check items such as the vessel pressurization, exhaust system, temperature monitor, thermocouple position and moisture wicking.
How You Can Help with Refractory Longevity
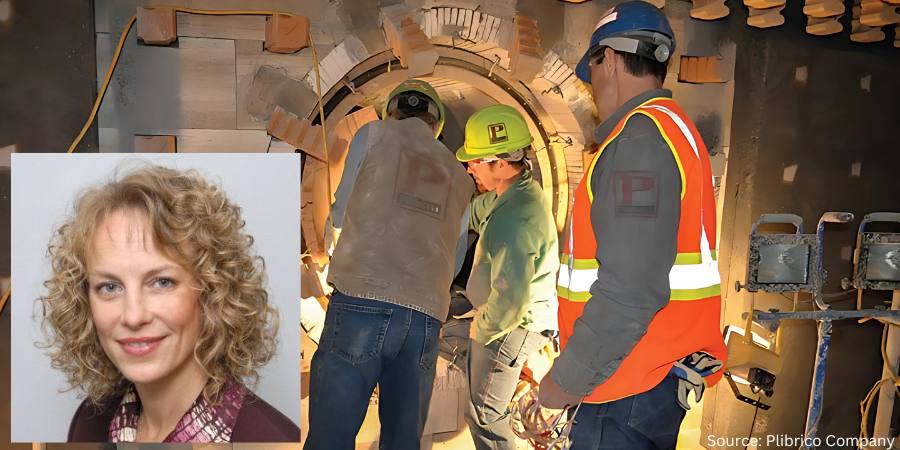
The goal of periodic inspection, maintenance and repair is to ensure the longevity and performance of refractories (Fig. 1). During maintenance, worn parts and areas of excessive wear are repaired before turning into bigger issues.
Figure 1. During the inspection process, the refractory team will provide a comprehensive condition assessment to help determine the need for repair. Source: Plibrico Company
Depending on operational make-up, skills and budget, employing a permanent staff to perform these services might not make financial sense. Instead, working with an outside professional refractory contractor with extensive industry expertise who can provide maintenance services, emergency response and repair operations might be far more cost-efficient for the end-user.
Under either service structure, there are precautionary steps that can be taken in-house to extend refractory operation and increase longevity.
Furnace heat up and cool down: Follow procedures established by the furnace manufacturer. Proper heating creates positive pressure in a furnace, ensuring an equal distribution of temperature. Expansion or contraction control is vital to avoid damage to the refractory.
Dust removal: Keep the dust off the steel in roofs that have an exposed anchoring structure. This simple step keeps the stainless steel hardware from becoming too hot and fatiguing.
“Good” cracks vs. “bad” cracks: Understand the important differences between good cracks and bad cracks. Good cracks in the refractory are created and visible as part of the natural cool-down process. These should be left alone because they will disappear during the heat-up process. If the end-user fills “good” cracks, they will have problems down the road with shell bulge because the refractory will naturally expand during heat-up and production.
An Ounce of Prevention
Contact us with your Reader Feedback!
Develop a relationship with a reliable, knowledgeable and nimble professional refractory expert who has your best interests at heart. During the inspection process, your expert and their refractory team should provide you with a comprehensive condition assessment to help determine the need for repair. Assessments allow the refractory contractor to analyze the state of the refractory and select the proper solution to ensure durable repair.
Often, the first indication that there might be a problem with the refractory lining is the appearance of a “hot spot” on the shell. A hot spot is where an area of the shell is found to be operating at a higher temperature than the surrounding area. This can be due to cracking, spalling or other issues that result in deterioration of the refractory lining.
When hot spots are identified, the refractory professional will typically pack, grout, caulk or “stuff” the area if it is accessible from the outside. They may also “hot gun” from the inside.
The number and severity of hot spots, usually found using an infrared camera and heat-flow analysis, can help the refractory professional or engineer determine the integrity of the refractory lining. Depending on the results, the manager/engineer should perform a full cost-benefit analysis to help evaluate which is the best option — repair or complete lining replacement (Fig. 2).
Figure 2. Depending on the inspection results, the plant manager should perform a full cost-benefit analysis to help evaluate which is the best option: repair or a complete lining replacement. Source: Plibrico Company
When faced with any type of refractory repair, best practice will come down to scope and timetable. A quick repair may be addressed using a gunning (cold/hot) or shotcrete refractory technique. Another possibility might be ramming plastic refractory just to fill a hole/spall or resurface the lining.
A more time-consuming and sometimes better option would be a full lining repair. These repairs are done to a more thorough degree, which allows for proper cure, dryout and anchoring.
A Pound of Cure – Premature Failure
Without proper refractory maintenance, you run the risk of premature failure of the refractory lining. The funny, or not so funny, thing about refractory failures is that you will usually not receive a notice on that day telling you that one of your critical systems will be failing. And once a failure occurs, it is all-hands-on-deck to address the issue and bring your operation back online as quickly as possible.
During the process, you or your refractory expert should collect samples of the existing refractory material to help identify the causes of failure. For example, glazing and excessive shrinking indicate exposure to excessive temperatures. Shearing away of the top refractory service can be evidence of thermal shock.
In addition, calculating a base-to-acid ratio will show if the type of refractory installed should have been selected in the first place. Refractory materials are manufactured to operate in different environments. A properly selected and installed refractory lasts longer, helps minimize shutdowns and leads to better fuel efficiency.
Lastly, fuel should be checked to determine if it is contributing to the degradation of the refractories. For instance, moisture content in fuel may be too high or contain chemicals that damage the lining.
Financial Implications of Non-Compliance
Compliance with CMMC 2.0 can be financially burdensome. Implementing measures such as multi-factor authentication, encryption and continuous monitoring can be costly, especially for businesses with limited resources. The lack of in-house cybersecurity expertise compounds this issue, requiring companies to hire or train specialized personnel, further increasing costs.
Failing to comply with CMMC 2.0 could result in losing valuable DoD contracts, which can be a significant portion of SMB revenue. Such losses could lead to layoffs, revenue declines or even business closures.
Drama-Free Refractory Removal and Replacement
In some cases, the maintenance needed for heat-processing equipment is more than repairs can handle. This leaves complete refractory lining replacement as the only option. This is highly specialized work requiring the skills of an experienced refractory installer.
To ensure drama-free refractory removal and replacement, follow these five key tips:
Enlist the support of a seasoned, knowledgeable and professional refractory contractor. Not all contractors are experts in refractory work. Make sure the contractor has quick access to refractory material.
Obtain a complete scope of work (SOW) and a solid plan. Some of the items that should appear in a good SOW include:
Amount of material needed and on hand
List of equipment supplied
Schedule and details for the tear-out plan
Proper curing/dryout plan
Prepare for the unforeseen. Often, problems do not reveal themselves until the unit has cooled and the tear-out begins. This reality necessitates contingency plans to be in place. Further, it underscores the importance of working with a fully stocked professional refractory contractor who has access to a refractory manufacturer that uses just-in-time manufacturing principles.
Where applicable, install and use precast shapes. These shapes are ready to install and require little to no dryout.
Discuss with your refractory expert if fast-dryout refractory material may be an option for you. Incorporating quick-dryout materials like Plibrico’s FastTrack® can cut traditional dryout time in half.
When working with your refractory installer, it is important to focus on your specific application to drive refractory material requirements. It is easy to get caught up in flashy new refractory compositions and features. The application should determine the refractory material, not the other way around.
Good for Your Equipment, Good for Your Wallet
Proper refractory maintenance is not only good for your critical heat-processing equipment, but also for your wallet. The reality is that the life of your refractory can be reduced by as much as 50% (or more) without proper maintenance. In fact, failing to provide basic refractory maintenance for an aluminum furnace, for example, can leave the end-user with an unbudgeted and unexpected bill for $150,000 or more to fully replace the roof. This is an expense that might have been put off many years with properly maintained refractory. It could then have been scheduled, budgeted and drama-free.
Worse yet, in the event of catastrophic refractory failure where the anchor tile system or full wall is snapped, the repair bill can easily top $200,000. Keep in mind these figures only address repairs. Add on the large cost of lost production and the total skyrockets quickly!
As Benjamin Franklin would agree, take care of your refractory — the unsung hero of the manufacturing process — and it will take care of you with a safe and efficient work environment, minimized downtime, reductions in energy losses and, more importantly, avoidance of catastrophic critical heat-processing equipment failure.
About the Author
Pamela Gaul Director of Marketing Plibrico Company
Pamela Gaul is the director of marketing at Plibrico Company LLC.
Loy Instrument, Inc., which supplies process control and combustion solutions for heat treaters in multiple industries, has been acquired by Relevant Industrial, LLC (Relevant), a leading provider of industrial equipment and engineered solutions. This partnership enhances the company’s ability to serve clients in industries such as aerospace, metals, refining, petrochemical, manufacturing and power generation.
John Carte CEO Relevant Industrial LLC
Loy, headquartered in Indianapolis, Indiana, has over 80 years of industry knowledge and a team with more than 900 years of combined experience. This acquisition marks a significant milestone for Relevant, strengthening its position as an industry leader and expanding its geographic footprint into Indiana, Ohio, Kentucky and Michigan.
“Joining Relevant Industrial is an exciting step for Loy Instrument, our employees, and our customers,” said Ken Bradway, president of Loy Instrument, Inc. “Together, we’ll leverage our combined expertise and resources to expand our capabilities and continue delivering exceptional solutions to the industries we serve.”
“The addition of Loy Instrument’s expertise strengthens our ability to tackle complex challenges in combustion and process control, providing even greater value to our customers,” said John Carte, CEO of Relevant Industrial. “We’re excited to welcome this exceptional team into the Relevant family and look forward to driving innovation together.”
The press release is available in its original form here.
Industry experts agree: 2025 is a year of significant, high-tech developments. In this Technical Tuesday, hear from three heat treat industry consultants on current and incoming technological advances, from miniaturization and customization to artificial intelligence.
Michael Mouilleseaux, general manager at Erie Steel, Ltd, opens the discussion by asking what role AI has in a perfect world of heat treating; Thomas Wingens, president of Wingens Consultants, predicts six major technologies to look for in 2025; and Dan Herring, a.k.a. The Heat Treat Doctor® and owner of The HERRING GROUP, Inc., points out how the trend toward smaller is affecting the heat treat industry.
This informative piece was first released inHeat Treat Today’sJanuary 2025 Technologies To Watch in Heat Treating print edition.
AI’s Place in Heat Treating?
by Michael Mouilleseaux
The benefits of AI are purported to be the ability to reduce the time required to complete complex tasks, such as data analysis, while reducing human error and providing both unbiased decision making and data-driven system enhancements … and by the way, it can operate 24/7 without breaks!
Does AI have a place in heat treating?
Here’s what I would want my heat treat AI (HT AI) to be able to do with a gas-fired atmosphere furnace.
Combustion System:
My HT AI will continuously monitor the free oxygen of all the burners and keep them at a perfect ratio, thereby optimizing performance and gas consumption. It will track these changes and provide analysis of any trends that it “perceives,” so to speak.
My HT AI will continuously monitor combustion air pressure and message me in time to have the air filters changed before it affects performance. It will track this and provide historical and prescriptive information.
My HT AI will periodically perform a “tube check,” whereby it will shut off combustion in a tube and monitor the free oxygen, recognizing that any diminishment from “atmospheric” O2 levels indicate the potential of a tube leak. It will track this and provide analysis of any trends that it perceives.
My HT AI will track when system thermal stasis is achieved, monitor gas consumption for each discrete heat treat cycle, provide analysis of trends that it perceives, and recommend thermal cycle changes to optimize these cycles.
My HT AI will facilitate the optimization of the critical human assets in process engineering, product quality and equipment maintenance.”
Michael Mouilleseaux
Atmosphere Control System:
My HT AI will continuously monitor the atmosphere flows required to achieve the requirements for each heat treat cycle. It will track “atmosphere recovery” and provide analysis of any trends that it perceives (i.e., increased usage as a precursor to a furnace leak).
My HT AI will periodically perform a furnace check, whereby it compares the composition of the Endo gas in the furnace to that exiting the generator, providing a measure of furnace integrity. It will track this and provide analysis of any trends that it perceives.
My HT AI will confirm “tube check” data (see above) with atmosphere usage to evaluate its potential effects on process integrity and make actionable recommendations. It will track these incidents and provide analysis of any trends that it perceives.
My HT AI will provide assurance of system performance and actionable information.
Shoot for the Moon:
My HT AI will have the unique ability to integrate metallurgical results with process information and thereby provide the ability to optimize the heat treating process AND metallurgical results.
My HT AI will allow me to input material chemical and hardenability data and, by comparing actual results with the calculated, or prospective results, provide confirmation of the thermal and quenching segments of the process.
My HT AI will be able to correlate IGO results with furnace integrity checks (i.e., leaks) and over time establish hard limits for allowable leak rates.
My HT AI will be able to correlate actual retained austenite levels in carburized case with furnace carbon potential and make data-driven process modifications to optimize this.
My HT AI will be able to correlate the shape of the case depth curve with the carburizing cycle and the material type, and it will make data-driven process modifications to optimize this.
My HT AI will have the ability to develop new heat treat thermal cycles specific to my furnaces extrapolated from existing data.
My HT AI will provide a level of system performance heretofore not achieved, that not only assures adherence to established standards but provides a clear path of continuous improvement via data analysis and actionable actions. Product results will be validated by total process control, and total process control will assure attainment of product results.
My HT AI will facilitate the optimization of the critical human assets in process engineering, product quality and equipment maintenance.
In short, my HT AI will afford the heat treating community the ability to finally jettison the mantle of “black art” and join the community of high-tech engineered processes.
About the Author:
Michael Mouilleseaux General Manager Erie Steel, Ltd
Michael Mouilleseaux has been at Erie Steel in Toledo, OH, since 2006 with previous metallurgical experience at New Process Gear in Syracuse, NY, and as the director of Technology in Marketing at FPM Heat Treating LLC in Elk Grove, IL. Having graduated from the University of Michigan with a degree in Metallurgical Engineering, Michael has proved his expertise in the field of heat treat, co-presenting at the 2019 Heat Treat show and currently serving on the Board of Trustees at the Metal Treating Institute.
2025 will be the year of invention and application. There are six major technologies to be looking out for: AI management software, giga casting for the EV industry, high-pressure quench furnaces, thermal processing specialty materials, processing for steel enrichment, and practices for cleaning consistency.
AI Management Software
Some new heat treat shop management software is now available. It utilizes artificial intelligence to save labor while documenting all processes in real time. The software easily adapts to the way we work and is much easier to learn and implement than the software of the past. I see this as the number one investment item for commercial heat treaters in 2025, as it is the cheapest and easiest way to automate with a great ROI while increasing quality and customer service.
Giga Casting
With Tesla as the main driver, very large so-called “GIGA” H13 aluminum dies of 3 to 8-ton weight have really taken off in the last years, in particular for new electric car models, and the demand for very high pressure quench furnaces is increasing in the U.S. (more to come in a later article).
Vacuum Oil Quenching
However, even with the most advanced designs and high-pressure efforts, gas quenching with nitrogen has its limits, and the use of helium is not considered anymore because of its immense cost, even with a recycling system in place. Vacuum oil quenching has become a viable alternative in recent years not only in combination with LPC (low-pressure carburizing) but also with the use of materials like AISI 52100 that would be typically heat treated in atmosphere integral quench furnaces but show lesser distortion with the variation of pressures over the oil bath, which can shift the oil boiling phase peak to lower temperatures (e.g., from 650°C (1200°F) at atmospheric pressure to 400°C (750°F) at 1 mbar pressure). Some new modern vacuum oil quench furnace designs have recently entered the market, showing excellent surface cleanliness and distortion results. Aside from the better quality, they offer a much safer, cleaner and more pleasant work environment.
Specialty Materials
In general, we see a higher demand for the thermal processing of specialty materials; for example this is seen with the hydrogen decrepitation of titanium, tantalum, niobium, or rare earth element materials, powder processing or sinter processes, and surface diffusion processes.
Steel Enrichment
Enriching stainless steel with nitrogen is not new, but it is gaining momentum and more applications. One method for\ low-temperature processes on austenitic stainless steels around 370°C (690°F) is called S-phase case hardening, and the high temperature version around 1100°C (2010°F) is called solution nitriding. Both processes were initially established in the early 90s in Europe but seem to be gaining momentum and more comprehensive applications worldwide over the last years.
Figure 1. For 2025, “We see more fully enclosed vacuum solvent cleaning in heat treat shops to ensure a higher standard and consistency of the surface cleaning results compared to the fading of water cleaners.” – Thomas Wingens, WINGENS CONSULTANTS
Cleaning Consistency
Speaking of surface processes: The cleaning of components has been a thankless process, especially in commercial heat treatment, as it is seen as a necessity that is not necessarily paid for by the clients but is necessary to have uniform dissociation on the surface of a part to ensure a uniform case (e.g., nitriding case). There are well-defined standards for temperature uniformity and hardness testing, but cleaning consistency needs to be addressed, as it can be very impactful. We see more fully enclosed vacuum solvent cleaning in heat treat shops to ensure a higher standard and consistency of the surface cleaning results compared to the fading of water cleaners.
About the Author:
Thomas Wingens President WINGENS CONSULTANTS
Thomas Wingens has been an independent consultant to the heat treat industry for nearly 15 years and has been involved in the heat treat industry for over 35 years. Throughout his career, he has held various positions, including business developer, management, and executive roles for companies in Europe and the United States, including Bodycote, Ipsen, SECO/WARWICK, Tenova, and IHI-Group.
Everywhere we turn today, the products we use are getting smaller, more compact and more powerful. This is true across all industries, from aerospace to automotive, from medical to electronics, and from energy to semiconductors to name a few. Today, miniaturization, portability and customization have become major design objectives for almost all manufacturing segments.
These trends are irreversible and are, or will be, found even in the most unlikely of places — both in mining of resources taking place deep under the ocean floor and eventually on other planets. The key question then becomes, how will all of this influence our heat treating operations?
Miniaturization, Portability and Customization Today
Given the ever-increasing demand for higher performance in a smaller footprint, we have often focused our energies on taking existing products and adapting them for use. But in the long term, this is not sustainable. For example, not only is gear noise reduction critical in our submarines, but the medical and robotics markets are continuously searching for smaller, more efficient, more application specific and more intelligent drive systems and motors with increased torque density.
Heat treatment will experience a metamorphosis and emerge more broadly as thermal treatment. The age of metals as we have known it has become the age of materials: ceramics, composites, powder materials, glasses, polymers, fiber-reinforced plastics, and even nanomaterials.
Dan Herring, The Heat Treat Doctor®
Another example, although not new, is miniaturization in vehicle electronics, especially as it relates to data collection where demand is high for smaller, more powerful and, yes, cheaper components. Integration into the electronic control units via on-board power systems has seen the need for more cables in vehicles and positioning connectors, which means more contacts/connections on the electronic components without significantly increasing the installation space.
Similarly, there is a huge demand for portability. This is true not only in our electronics (just think about how cell phones or computers have changed over the last ten years), but there is a growing need for portable medical devices so that medical care can be brought to the patient rather than the other way around. For example, longer battery life and lighter weight are critical for devices such as portable oxygen concentrators.
What Does This Mean for the Heat Treatment Industry?
Looking ahead, we will see both short and long-term changes to our industry. Happening today and continuing in the near term, heat treaters are working closer than ever with design and manufacturing engineers as they focus on products that reduce environmental impact, are produced at lower unit cost, and with improved part quality. Still, the era of mass recalls must come to an end. And the cost of heat treating is less than it was even a decade ago. But as manufacturing demand evolves due to consumer expectation, process and equipment flexibility will become keys to meeting the highest quality standards in an on-demand world.
Historically, changes in the heat treat industry has been evolutionary and incremental in both nature and effect. There have been notable exceptions such as the invention of the oxygen probe or low pressure vacuum carburizing. But to meet the manufacturing demands of the future, change will need to be more revolutionary and abrupt in nature, a game changer.
Given the ever-increasing demand for higher performance in a smaller footprint, we have often focused our energies on taking existing products and adapting them for use. But in the long term, this is not sustainable. For example, not only is gear noise reduction critical in our submarines, but the medical and robotics markets are continuously searching for smaller, more efficient, more application specific and more-intelligent drive systems and motors with increased torque density.
Dan Herring, The HERRING GROUP, Inc.
Heat treatment will experience a metamorphosis and emerge more broadly as thermal treatment. The age of metals as we have known it has become the age of materials: ceramics, composites, powder materials, glasses, polymers, fiber-reinforced plastics, and even nanomaterials. As a result, we will find ourselves needing, for example, to expand our heat treat capability and equipment to deal with such items as process temperature ranges from -200°C to 1850°C (-330°F to 3360°F) or greater or at pressure/vacuum levels heretofore only achievable in laboratories or specialty applications.
As product sizes decrease, load sizes will become smaller out of necessity. And as a result, our heat treat equipment must be small lot capable with tighter controls to achieve higher quality along with tremendous process flexibility.
Final Thoughts
History’s enduring legacy is that change is inevitable. Just think back to how the heat treatment industry has evolved, from the campfire to the blacksmith to the modern heat treater, from the artisan to the era of mass production, from the art of heat treating to the science of heat treatment. The lesson is that to adapt, one must constantly innovate and invent. Miniaturization, portability and customization in whatever form they take are here to stay. Perhaps even teleportation (the ultimate miniaturization?) isn’t that far off after all, considering flight was unheard of a little over a century ago.
About the Author:
Dan Herring (The Heat Treat Doctor®) The HERRING GROUP, Inc.
Dan Herring has been in the industry for over 50 years and has gained vast experience in fields that include materials science, engineering, metallurgy, new product research, and many other areas. He is the author of six books and over 700 technical articles.
Readers are checking out Heat TreatToday’smagazine, and the January 2025 Technologies To Watch print editionhas a piece that sparked comments from readers. The letter from publisher Doug Glenn entitled “What If We’re Wrong About CO2 & Global Warming?“ challenges the “assumption that global warming, and specifically man-induced global warming, is a real and settled science.“
Would you like to weigh in on the topic? Submit your question, comments, thoughts, or queries here or email Bethany Leone at editor@heattreattoday.com.
Here is an excerpt from the publisher’s page:
“I’d like to challenge that assumption. Firstly, legacy media, the federal government, academia, and the scientists who deliver the science we’re called to follow — i.e. “follow the science” — are all strong proponents of man-made global warming and the evil of CO2. This grouping of authorities, in and of itself, causes many to be suspicious, given this group’s historic record of dishonesty and deception. If this group has been so wrong in the past on macro-social economic issues (e.g., Covid) would it not be reasonable to question their claims about climate change?
Secondly, the science doesn’t seem to be as settled as claimed.”
This publisher’s page prompted this feedback from loyal reader Roger Hirdof W.H. Kay Company:
“Thank you for your column in the recent HTT issue. As a longtime climate skeptic, articles like yours are exactly what’s needed to push back on continued efforts to use climate change as a tool for massive government interference in all phases of life.
Sadly, the EU is much further down the road in their Climate zealotry, and we’re reading how these efforts are even pushing some European landowners to close down their farms to avoid crippling penalties in the decree of decarbonization.
This past election puts the proverbial ‘finger back in the dike’ of climate-based government intrusion in our economy and daily lives, and thank God for that!
Keep up the great work Doug.”
Doug’s reply:
“The well-meaning folks in our government will continually find ways of expanding their scope and power. Let’s assume 90% of them mean well. The fact is, the government should NOT be in 90% of the stuff they’re currently in. It is our responsibility to reign them in, politely if possible.
Keep fighting the good fight when and where you’re able. The publisher’s page is one place I’ve been blessed to use in my little corner of the world. Not everyone agrees, but that’s the way it ought to be.”
From reader Kevin O’Brien, Birmingham, Michigan:
“Quick note to thank you for your editorial. Yes, agree on the idea that we are re-shaping and re-orienting too many aspects of our economy and society because there is an agenda being pushed by a group. Even more so when you consider that many of the people pushing the agenda stand to gain from massive government spending in this arena. All too often, the environmental ‘movement’ seems to be acting on and reacting to published material that seems more like the flavor of the month rather than solid, steady scientific findings…. The result is that large numbers of people experience a negative outcome (higher prices, more regulations) with no means for redress.”
Doug’s reply:
“Very much agree with your assessment of ‘flavor of the month.’ My content is that we should trust the market and not well-meaning individuals in positions of power to determine the direction of the world’s environmental movement. If everyone in the world were genuinely concerned about global warming, they would demonstrate that sincere concern by spending money in that direction. That in turn would encourage companies to follow the consumer’s lead. We don’t have enough faith in the market … or as Adam Smith would say, the Invisible Hand!”
From reader Steve Maus:
“I have followed this issue with great interest for decades, and so I am familiar with the work and comments of the prominent figures you have referenced. My studies toward a metallurgical engineering degree included significant coursework in organic chemistry and thermodynamics, and in my career, I’ve done extensive hands-on work with CO2 and its many reactions. With that in mind, I tend to agree with the skeptics because the chemistry simply does not support the claims of those who predict catastrophic global effects due to small changes in atmospheric CO2.
It seems to me that our industry ought to encourage frank debate of the issue, and that we should demand that it be based on a critical look at the entire chain of generating process heating, and on the genuine effects of CO2 emissions. Simply moving the generation of CO2 away from the point of natural gas-based heating and transferring it to the source of generating electricity with fossil fuels or ‘renewable’ sources that have issues of their own or using fuels that require electric power to generate them, is not accurately addressing the situation. Otherwise, it appears to be a situation of doing something just to do something, for reasons that may not well-considered. And as we have seen with other attempts like EVs, solar panels and wind turbines, the solutions often come with problems of their own, so we ought to learn the lessons and apply them here.
But I digress. Doug, I applaud you for raising the question, and I look forward to the healthy discussions that will be provoked by it.”
Doug’s reply:
“Thanks for the encouragement, Steve. I hope you’re doing well. By the way, if you haven’t read the article I referenced from The Epoch Times, I highly recommend it. If what they are saying in that article is true (regarding ‘saturation’ of CO2), then the whole issue becomes moot … IMHO! It is worth the read.”
From reader Dean Keal of IGE Fans:
“I think you are spot on. Aside from all the science debunking this, history has shown the planet has been warmer in the past than it is currently. Heck, in the medieval warming period, the Vikings were grain farmers on Greenland. I think this whole fiasco is about power and control, not science. Unfortunately, there are so many people making money from this issue it has become entrenched. Perhaps President Trump will interject some common sense.”
Doug’s reply:
“Thanks, Dean. Appreciate the encouraging words. Not everyone agrees, but most everyone that has taken the time to respond has been respectful and MOSTLY in agreement. There was one who vehemently disagreed but we’re still on speaking terms!”
We welcome your inquiries to and feedback on Heat TreatToday articles. Submit your questions/comments to editor@heattreattoday.com.
A manufacturer which supplies agricultural ground engaging solutions has improved its production efficiency with two roller hearth furnace systems. The furnaces will be used to re-heat flat stock for hot forming, replacing existing equipment as part of a plant modernization initiative at its locations in both the United States and Canada.
The company commissioned the two 8000 lb/hr, high-temperature re-heat furnaces lines from CAN-ENG Furnaces International Limited (CAN-ENG) to heat steel plates to temperatures suitable for hotworking, where pieces are formed by a hydraulic press. The Ontario-based heat treating equipment provider designed the fully automated system to reduce energy consumption and floor space, while improving product flow and maintaining high-throughput requirements.
Scott Cummings Sales Manager CAN-ENG Furnaces International Limited
Each furnace is capable of operating up to 1750F and producing a part ready for forming every 15 seconds. The former equipment required alloy fixtures that consumed additional energy to heat up each time along with the product as well as costly periodic replacement and maintenance, heating the product directly on the furnace rolls increases the efficiency and reduces the overall equipment size.
“Can-Eng was selected as the supplier for this project based on our vast experience with high temperature roller hearth furnace systems and Can-Eng’s reputation to stand behind our equipment,” said Scott Cummings, sales manager for CAN-ENG.
Heat TreatToday publishes twelve print magazines a year, and included in each is a letter from the publisher, Doug Glenn. This letter first appeared in January 2025 Technologies To Watch print edition.
I recently attended the Industrial Heating Equipment Association Decarbonization SUMMIT in Indianapolis at the Conrad Hotel. Roughly 100 thermal processing industry professionals participated in this two-day long event. As I listened to all presentations over those two days and going back even further to the planning of the event — which, by the way, I’d like to commend Jeff Rafter of Selas Heat Technology for his leadership, Mike Stowe of Advanced Energy for his technical contributions, and Goyer Management for their diligent work to produce this SUMMIT — I noticed that nearly everything being discussed was predicated on the assumption that global warming, and specifically man-induced global warming, is a real and settled science.
I’d like to challenge that assumption.
Firstly, legacy media, the federal government, academia, and the scientists who deliver the science we’re called to follow — i.e. “follow the science” — are all strong proponents of man-made global warming and the evil of CO2. This grouping of authorities, in and of itself, causes many to be suspicious, given this group’s historic record of dishonesty and deception. If this group has been so wrong in the past on macro-social economic issues (e.g., Covid) would it not be reasonable to question their claims about climate change?
Secondly, the science doesn’t seem to be as settled as claimed.
John F. Clauser, a Nobel laureate in Physics, has been articulate in his doubts about the climate crisis.
“The popular narrative about climate change reflects a dangerous corruption of science that threatens the world’s economy and the well being of billions of people.”
“I don’t believe there is a climate crisis. The world we live in today is filled with misinformation. It is up to each of you to serve as judges, distinguish truth from falsehood based on accurate observations of the phenomena.”
“Great news! There is no climate crisis! Much as it may upset many people, my message is that the planet is not in peril.”
Ivar Giaever, another Nobel laureate in Physics, has been clear in his skepticism about global warming.
“Global warming has become a new religion. We frequently hear about the number of scientists who support it. But the number is not important: only whether they are correct is important.”
“It is amazing how stable temperature has been over the last 150 years.”
“I am a skeptic. Global warming has become a new religion.”
“We don’t really know what the actual effect [of CO2] on the global temperature is. There are better ways to spend the money.”
Richard Lindzen, professor emeritus of Earth, Atmospheric, and Planetary Sciences at MIT, has been a vocal critic of the consensus on human-caused global warming.
Willie Soon, an astrophysicist, geoscientist, and aerospace engineer at Harvard’s Smithsonian Center for Astrophysics, questions the extent of the human impact on climate change.
Frederick Seitz, former president of the U.S. National Academy of Sciences, has expressed doubts about the severity of global warming.
Ian Plimer, an Australian geologist and professor emeritus at the University of Melbourne, is a prominent climate skeptic.
Peter Ridd, a former professor at James Cook University in Australia, has been a vocal critic of climate change science.
Jim Mason, PhD in Experimental Nuclear Physics from McMaster University, Hamilton, Ontario, Canada, recently published an excellent article in The Epoch Times entitled, “A Physicist’s View of Greenhouse Gas Emissions and the Impact on Climate,” which seriously calls into question whether or not the concentration of CO2 gas in our atmosphere has the physical ability to produce global warming. Mason quotes the work done by two other physicists, William A. Van Wijngaarden and William Happer. Mason says, “The duo postulate that long-wavelength radiation (LWR) absorption does not increase in a linear fashion as CO2 increases but does so in an exponentially DECREASING fashion. Additional amounts of CO2 added to the [atmosphere] absorb ever-decreasing amounts of additional LWR, until at some point the CO2 is absorbing effectively all of the LWR in the [atmosphere] that CO2 can absorb. Absorption is saturated” (emphasis is mine).
The implication is that adding more CO2 to the atmosphere may have essentially no impact on global temperatures if CO2 is absorbing all that it can absorb. I highly recommend Mr. Mason’s article.
Given the above, I have a few questions:
What if we are wrong about decarbonization and these gentlemen are right?
Is there any wisdom in approaching this topic with a bit more caution?
Do any of you have doubts about the need to decarbonize, and if so, how do you reconcile those doubts with continued efforts to decarbonize and/or take Department of Energy grants and subsidies?
Is anyone concerned about the amount of money that we are throwing at this potentially non-problem and the enormous and devastating impact on our children’s financial future?
“The Cybersecurity Maturity Model Certification (CMMC) 2.0 aims to improve cybersecurity across the defense industrial base (DIB), but many small to mid-sized businesses (SMBs) struggle to meet the standards, putting them at risk of losing crucial contracts.” In this Cybersecurity Desk column, Joe Coleman, cybersecurity officer at Bluestreak Compliance, a division of Bluestreak | Bright AM™, raises the alarm ifsmall to mid-sized heat treaters neglect compliance standards and guides companies through the minefield of cyber threats facing all SMBs.
Read more Cybersecurity Desk columns in previousHeat Treat Today’s issues here.
Despite an increasing cyber threat landscape, many small to mid-sized businesses (SMBs) in the Department of Defense (DoD) supply chain remain unprepared for compliance with NIST SP 800-171 R2 and CMMC 2.0. The Cybersecurity Maturity Model Certification (CMMC) 2.0 aims to improve cybersecurity across the defense industrial base (DIB), but many SMBs struggle to meet the standards, putting them at risk of losing crucial contracts. Surveys suggest that nearly 70% of SMBs are unready for the new requirements, and the real figure could be even higher due to some businesses inaccurately reporting compliance by inflating their assessment scores.
Understanding CMMC 2.0
Contact us with your Reader Feedback!
CMMC 2.0 simplifies the original five-tier framework into three levels:
Level 1: Basic cyber hygiene for contractors handling Federal Contract Information (FCI).
Level 2: Advanced practices for those working with Controlled Unclassified Information (CUI).
Level 3: Stringent requirements for contractors involved in national security projects.
Compliance is mandatory for any contractor bidding on DoD contracts, including those working indirectly for federal contractors and subcontractors. SMBs should anticipate customers clients inquiring to inquire about their compliance as these standards will soon impact their business relationships. Achieving compliance is a lengthy process, typically taking 12 to 18 months.
Low Readiness and Risks
The lack of readiness among SMBs threatens both business continuity and national security. Many smaller contractors lack the resources and expertise to meet CMMC 2.0’s standards. Given the defense sector’s reliance on a wide variety of contractors, this gap could create widespread repercussions.
Financial Implications of Non-Compliance
Irreversible consequences from waiting to comply
Compliance with CMMC 2.0 can be financially burdensome. Implementing measures such as multi-factor authentication, encryption and continuous monitoring can be costly, especially for businesses with limited resources. The lack of in-house cybersecurity expertise compounds this issue, requiring companies to hire or train specialized personnel, further increasing costs.
Failing to comply with CMMC 2.0 could result in losing valuable DoD contracts, which can be a significant portion of SMB revenue. Such losses could lead to layoffs, revenue declines or even business closures.
Challenges to Compliance
Several challenges contribute to the widespread unpreparedness among SMBs:
Unclear timelines: Uncertainty surrounding DoD’s compliance timelines complicates planning and prioritization for SMBs.
Complexity of requirements: While CMMC 2.0 simplifies the original framework, its specific requirements remain difficult to interpret for many SMBs, particularly in identifying necessary security measures.
Resource limitations: The cost of achieving and maintaining compliance strains smaller businesses, which often lack the budgets for the required technology and expertise.
Lack of cybersecurity expertise: A shortage of qualified personnel poses a significant obstacle, as demand for cybersecurity professionals is high across industries.
Government Support Initiatives
To help SMBs, the DoD has introduced various programs, including training, grants and educational resources. A phased implementation timeline also provides additional preparation time. However, industry experts suggest that further support, such as tax credits or subsidies, could help SMBs offset the costs of compliance. Clearer guidance from the DoD would also be beneficial in helping businesses navigate the certification process.
Path Forward for SMBs
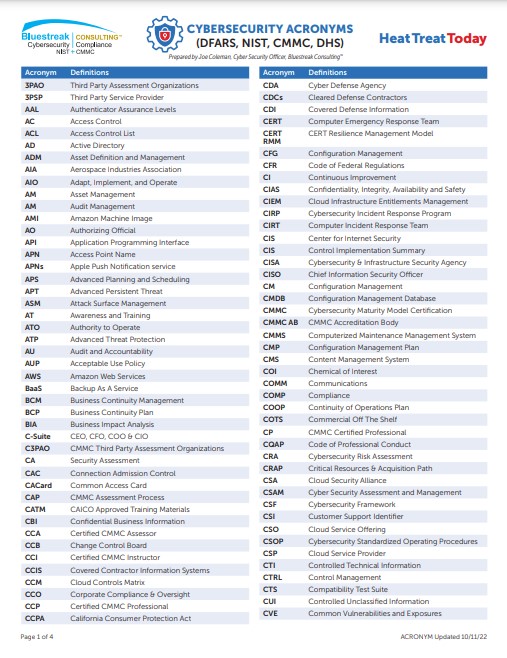
Click image to download a list of cybersecurity acronyms and definitions.
To secure future contracts, SMBs must prioritize cybersecurity. This involves conducting internal risk assessments, identifying vulnerabilities, and creating compliance plans. Partnering with cybersecurity experts or managed service providers can help SMBs develop cost-effective strategies. Additionally, leveraging government resources and adopting critical security measures early will better position SMBs for CMMC 2.0 certification.
Conclusion
The widespread lack of preparedness for CMMC 2.0 poses significant risks to both SMBs and the defense supply chain. As deadlines approach, proactive measures from both businesses and the government are necessary to close the readiness gap and ensure the continued participation of SMBs in the defense sector.
About the Author
Joe Coleman Cyber Security Officer Bluestreak Consulting Source: Bluestreak Consulting
Joe Coleman is the cybersecurity officer at Bluestreak Compliance, which is a division of Bluestreak | Bright AM™. Joe has over 35 years of diverse manufacturing and engineering experience. His background includes extensive training in cybersecurity, a career as a machinist, machining manager and an early additive manufacturing (AM) pioneer. Joe presented at the Furnaces North America (FNA 2024) convention on DFARS, NIST 800-171, and CMMC 2.0.
Retech Systems LLC welcomed participants to its Buffalo, NY, facility for a leak testing seminar last month, unveiling best practices and the basics of equipment on December 4-5, 2024. Vacuum technologies provider Busch Group co-hosted the event, which was open to employees and clients of both companies.
Leak detection expert Ron Ligthart in the classroom portion of the Retech – Busch Group seminar
Retech Systems LLC, which manufacturers metallurgical furnaces, is a daughter company of SECO/WARWICK Group. Busch Group brands include Busch Vacuum Solutions, Pfeiffer Vacuum+Fab Solutions and centrotherm clean solutions.
Ron Ligthart from the Busch Group, a leak detection expert with over three decades of experience in the industry, presented the seminar on the first day of the event to Retech and other SECO/WARWICK employees. Attendees learned the basics of how a helium mass spectrometer leak detector works and best practices on the techniques for leak testing large vacuum systems. After a few hours of classroom-based material, students were able to put their knowledge to the test on a vacuum furnace on Retech’s shop floor using a Pfeiffer leak detector.
On day two, local Retech, Busch Group and Pfeiffer Vacuum clients were invited in for a similar activity. Overall, the event focus was on:
best practices for tracer gas leak testing
how to properly spray helium and identify leak locations
minimizing the time spent leak testing
connecting the leak detector to the ideal location and using features of the instrument (i.e. zeroing) correctly
“We had a great time partnering with Retech on this event,” said John McLaren of the Business Development – Leak Detection division at Pfeiffer Vacuum, Inc. “We’re always happy to share the knowledge we’ve gained and help customers improve their leak testing process.”
Main image caption: Ron Ligthart, presenter, leak detection seminar
A North American nitriding company recently announced a building expansion to accommodate more equipment and services. The new production space at its Monroe, Michigan, facility will house two additional pieces of equipment, a gas nitrider and an ion nitrider, with room for more equipment.
Mike Woods President Advanced Heat Treat Corp.
“The building expansion and new equipment demonstrate our sustained growth and forward-looking investments as we continue to adhere to our mission of ‘exceeding expectations with UltraGlowing® results,'” said Mike Woods, president of Advanced Heat Treat Corp (AHT). “The additional nitriding units will increase our nitriding capacity and enable faster turnaround.”
AHT provides surface treatments, including gas and ion nitriding/nitrocarburizing, UltraOx®, induction hardening and stress relieving, at its locations, which comprises the Michigan facility as well as two additional sites in Waterloo, Iowa, and one in Cullman, Alabama. The company broke ground on the project in November 2024 and expects construction to be completed by Summer 2025.
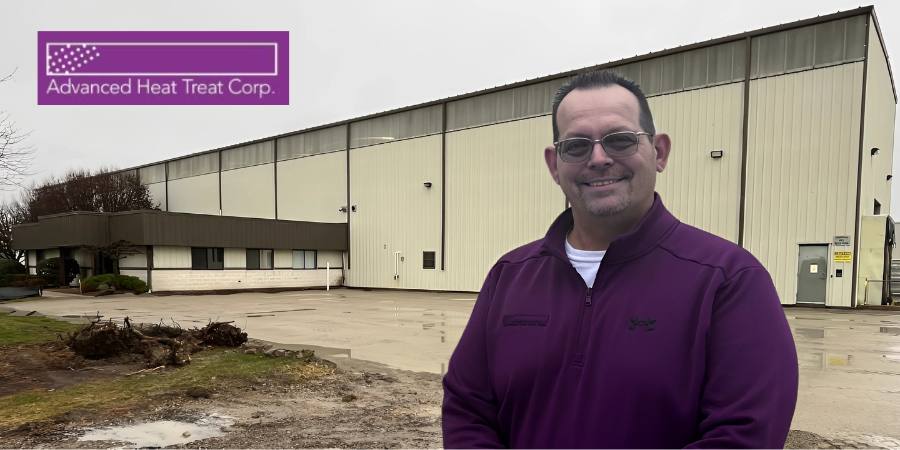
Main image caption: AHT plant manager, Chad Clark, at the southeast end of the building under expansion
The press release is available in its original form here.