Heat Treat Basics (Video): Steel Metallurgy from MetallurgyData.com #2

Guest post by www.MetallurgyData.com


MetallurgyData.com has produced a video series entitled Steel Metallurgy. Preview this episode at –http://www.metallurgydata.com/index.php/metallurgy-for-non-metallurgists-2/steel-metallurgy/. The preview runs under 4 minutes with the full video being just over 19 minutes long. The full video can be purchased for $4.99 from www.metallurgydata.com.


This is the second in a series of blogs titled ‘Metallurgy for the Non-Metallurgist’. The first blog looked at materials (https://www.heattreattoday.com//2016/08/metallurgy-for-non-metallurgists-from-metallurgydata-com/). In this second post we will look at the fundamentals of steel metallurgy.

Steel is primarily iron with up to 1% carbon, plus other alloying additions (generally totalling less than 5%).

A steel composition can be thought of as a recipe; different amounts of each ingredient make up your final product. In steel these ingredients are known as alloying additions and can affect the steel in different ways. We can affect the:

Properties of steels.
  • strength
  • hardness
  • toughness
  • ductility
  • fatigue
  • formability
  • machinability
  • weldability, and
  • corrosion resistance.

The addition of carbon to iron is probably the most important addition in steels which makes ‘The Iron Carbon Equilibrium Diagram’ very useful. Equilibrium means that enough time has been allowed on heating and cooling for any reactions to fully complete.

iron-carbon-diag-cropped
Typical Iron Carbon Diagram

In a steel <723°C, different structures are present and depending on the carbon content we can have at <0.8% Carbon – ferrite and pearlite, at 0.8% carbon – pearlite and >0.8% carbon – pearlite and cementite.

While the iron carbon diagram describes the structures of steel under equilibrium conditions, two further diagrams can be used when faster cooling rates are used; these are the CCT (continuous cooling transformation) diagram and the TTT (time temperature transformation) diagram. Both of these diagrams are helpful in selecting the optimum steel and process parameters.

When we cool a steel at faster cooling rates we can achieve additional structures, these can be bainite and martensite. CCT and TTT help determine the structures achieved.

In metallurgy the hardenability of a steel is a key parameter and when we talk about hardenability in steels we are often describing how deep into the steel we can achieve hardening. If a steel is described as having a low hardenability this will mean that the steel will produce a shallower depth of hardness. Hardenability is not to be mistaken for hardness; when describing the hardness we are often looking at the microstructure achieved during cooling. For a given steel it can be assumed that the quicker the cooling rate the greater the chance of achieving a harder structure and if that steel has a high hardenability this hard structure will be present deeper into the thickness.

In metals there are atomic defects called dislocations, these dislocations reduce the strength of the metal. The principle of strengthening mechanisms is to reduce the ability of these dislocations to move through the metal, this can be achieved by:
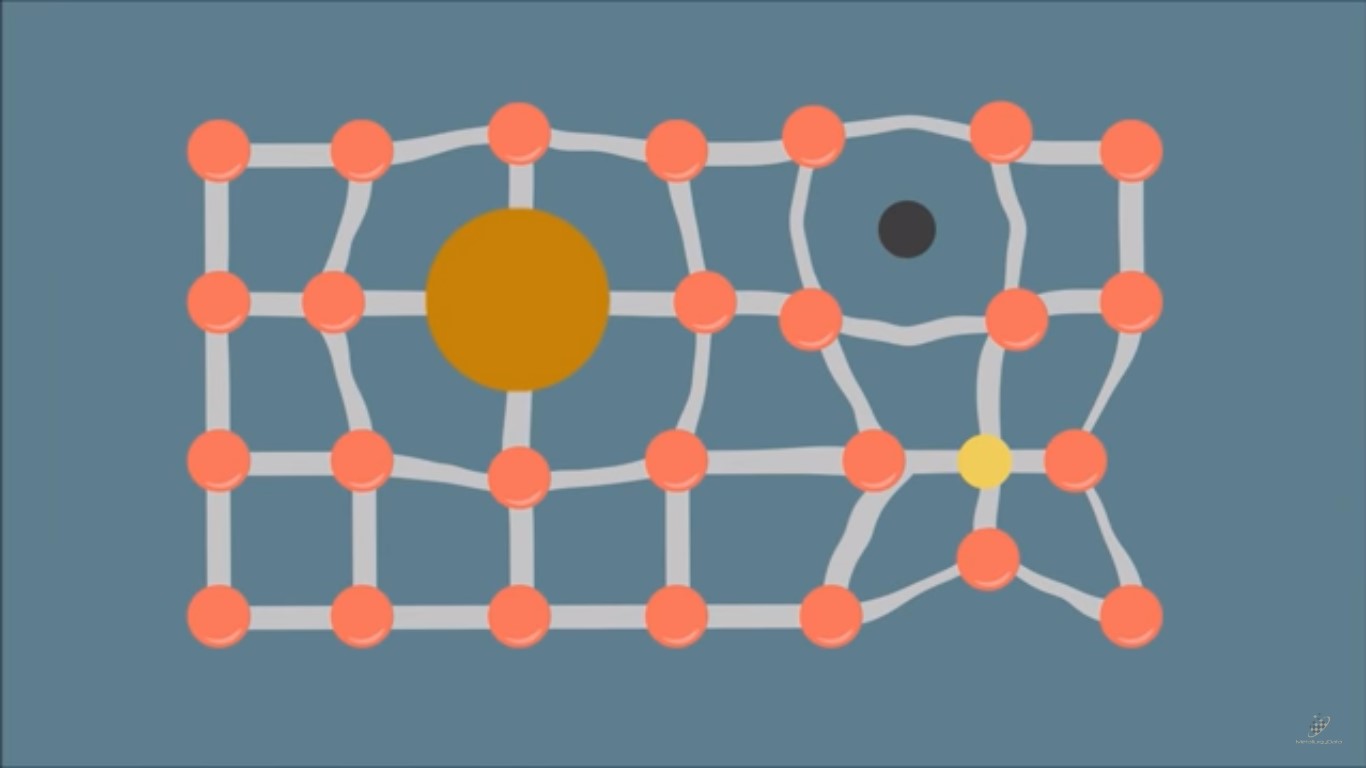
Atomic dislocations within the metal potentially reduce the metal's strength.
Atomic dislocations within the metal potentially reduce the metal’s strength.
  • Grain Size; the grains can interact with the dislocations preventing further movement. If we reduce the grain size we can increase the number of grains interacting with the dislocations, preventing movement and thus strengthening the metal.
  • Cold work introduces a large amount of strain into the metal; this strain interacts with the dislocations strain field, impeding the movement of the dislocations.
  • Solid solution strengthening is applied when we add other chemical elements to a metal. Addition of these elements can either be called interstitial or substitutional solid solution strengthening and will cause distortion in the atomic structure, restricting the dislocation movement and strengthening the steel.
  • Dispersion or precipitation strengthening is highly related to the structure of the metal and takes place when a phase is finely precipitated through a softer matrix. This precipitate acts as a barrier to dislocation movement.

The next in the series will be Steel Making and Casting.

Heat Treat Basics (Video): Steel Metallurgy from MetallurgyData.com #2 Read More »

NTSB: American Airlines Engine Failure Caused by Fatigue

BOTW-50w

Source: Airways Magazine


Gary Berwick, Dry Coolers

Special thanks goes to Gary Berwick of Dry Coolers, one of our first (and best) advertisers, for informing Heat Treat Today about the below article in Airways Magazine.


MIAMI — The National Transportation Safety Board (NTSB) issued and Investigative Update of American Airlines flight AA383, which caught fire on runway 28R at Chicago O’Hare International Airport after aborting its take-off.

The report states that the right engine number 2 stage high pressure turbine (HPT) disk failed and fractured into at least four pieces. A large disk fragment landed in a UPS warehouse located about 2,920 feet (890 meters) from the aircraft.

Read more about this failure in Airways Magazine.

NTSB: American Airlines Engine Failure Caused by Fatigue Read More »

American Axle & Manufacturing Holdings, Inc. Announces Acquisition

David C. Dauch, Automotive Heat Treat

David C. Dauch – Chairman and CEO of AAM

American Axle & Manufacturing Holdings, Inc. and Metaldyne Performance Group Inc. announced that the companies have entered into a definitive merger agreement under which AAM will acquire MPG for approximately $1.6 billion in cash and stock, plus the assumption of $1.7 billion in net debt.  The combination brings together highly complementary businesses and forms a premier, global Tier 1 supplier with broad capabilities across powertrain, drivetrain and driveline product lines, as well as diversified customer base and end-markets.

Under the terms of the agreement, each share of MPG’s common stock will be converted into the right to receive $13.50 per share in cash and 0.5 share of AAM common stock. Upon closing of the transaction, AAM’s shareholders will own approximately 70% of the combined company and MPG’s shareholders will own approximately 30%.  The transaction has been unanimously approved by the boards of directors of both companies and is anticipated to close in the first half of 2017 subject to shareholder and regulatory approval and other customary closing conditions.

Concurrent with the signing of the merger agreement, AAM entered into a voting agreement with an affiliate of American Securities LLC, the controlling stockholder of MPG, pursuant to which American Securities LLC has agreed to vote in favor of and otherwise support the transaction, subject to the terms of the voting agreement. Following the transaction, an affiliate of American Securities LLC will own approximately 23% of the combined company.

“AAM’s transformational acquisition of MPG brings together two complementary Tier 1 organizations to create a company with greater scale and increased diversity across products, customers and end markets,” said David C. Dauch, AAM’s Chairman and Chief Executive Officer.  “MPG’s expertise in complex, highly-engineered powertrain components and its global footprint will be tremendous assets to AAM. We are excited about the powerful industrial logic in this combination that will allow us to create additional value for our customers and other key stakeholders.  Together, we are forming a company with increased earnings potential and enhanced cash flow generation that will allow us to rapidly reduce leverage while fueling growth and delivering value to our shareholders.”

George Thanopoulos, MPG’s Chief Executive Officer, added, “This compelling transaction offers MPG shareholders an immediate premium and significant participation in the growth potential of the combined organization and its talented associates.   MPG and AAM share a similar culture and value system, laser focused on quality, operational excellence and technology leadership, which creates a natural fit and clear path to value creation for stakeholders of both companies.”

Compelling Strategic Rationale            

  • Creates a global leader in powertrain, drivetrain and driveline: The combined company will have the power to deliver a wide range of quality, highly engineered components, modules and sub-systems across multiple engine, transmission and driveline applications.
  • Diversified global customer base and end markets:  Accelerates AAM’s profitable growth and diversification objectives, significantly reducing product, customer and end-market concentrations.
  • Complementary technologies focused on light-weighting, fuel efficiency, vehicle safety and performance solutions:  Expertise in complementary product, process and systems technology strongly position the company to address the global automotive mega trends for both mechanical and alternative propulsion systems.
  • Stronger financial profile through greater size, scale and enhanced cash flow generation: On a pro forma basis, the combined entity will represent nearly $7 billion of annual sales and have the potential to generate over $1.2 billion of EBITDA and $400 million of free cash flow after full integration.
  • Powerful industrial logic with significant synergies:  Estimated annual run rate of targeted cost synergies estimated to be between $100 and $120 million by 2018.About AAM
    AAM is a world leader in the manufacturing, engineering, design and validation of driveline and drivetrain systems and related components and modules, chassis systems, electric drive systems and metal-formed products for light trucks, sport utility vehicles, passenger cars, crossover vehicles and commercial vehicles.  In addition to locations in the United States (Michigan, Ohio, and Indiana), AAM also has offices or facilities in Brazil, China, Germany, India, Japan, Luxembourg, Mexico, Poland, Scotland, South Korea, Sweden and Thailand. AAM has approximately 13,000 employees globally.About MPG
    MPG is a leading provider of highly-engineered lightweight components for use in powertrain and suspension applications for the global light, commercial and industrial vehicle markets. MPG produces these components and modules using complex metal-forming manufacturing technologies and processes for a global customer base of vehicle OEMs and Tier I suppliers. MPG has a global footprint spanning more than 60 locations in 13 countries across North America, South America, Europe and Asia with approximately 12,000 employees.


American Axle & Manufacturing Holdings, Inc. Announces Acquisition Read More »

Siemens Celebrates Commissioning of Power Project in Pennsylvania

Siemens and Panda Power Funds celebrated the commissioning of the Panda Liberty Power Project in Bradford County, Pennsylvania – an 829 megawatt natural gas-fueled power plant featuring Siemens advanced H-class gas turbines. Harnessing Marcellus Shale gas, “Liberty” is the first of two new Panda Power Funds generating stations to be commissioned in Pennsylvania this fall, with the Patriot Power Project in Clinton Township set to be dedicated in November. Combined, the two projects will be able to supply power for about two million households in large regional power markets, including Pennsylvania.

For “Liberty” and “Patriot,” Siemens’ scope of supply features advanced power generation technology, financing, and long-term service. The single shaft power plant blocks include two SGT6-8000H gas turbines, two SST6-5000 steam turbines, two hydrogen-cooled SGen6-2000H generators, and two heat recovery steam generators, along with the control system SPPA-T3000. The gas turbines and generators were manufactured at Siemens’ Charlotte Energy Hub, the global base for the company’s 60 Hz power generating equipment.

Siemens will provide maintenance and service for the main components associated with the gas turbine under a long-term service program. Parts, inspections, and scheduled service/maintenance, along with Siemens’ Power Diagnostics™ remote monitoring and diagnostics, are included in the comprehensive service agreement. For “Liberty,” Siemens Financial Services provided financing to aid in the project’s construction through a $50 million term loan.

“The commissioning of this highly-efficient power plant marks another milestone in our successful relationship with Panda Power Funds. This project demonstrates the full spectrum of Siemens’ portfolio, from our leading edge H-class technology, to financing, to service and maintenance,” said Martin Tartibi, Senior Executive Vice President, Energy Solutions Americas, Siemens Power and Gas. “As America continues to turn to cleaner-burning natural gas, we are proud that our world-class power generation technology can provide affordable, efficient and reliable power to about one million households – using the latest, most advanced emissions-control technology.”

“Designed to harness gas from the Marcellus Shale, this state of the art power plant represents the next chapter in Pennsylvania’s energy renaissance,” said Todd Carter, Chief Executive Officer of Panda Power Funds. “Working with Siemens over the last several years has proven they ‘walk the talk’ with their customer service and technological innovation, helping to bring online a world-class power asset in the Keystone State. We are very pleased to reach another important milestone in our collaboration with Siemens.”

The H-class technology in a single-shaft configuration, used in the “Liberty” and “Patriot” power stations, means that both the gas turbine and steam turbine are arranged on one shaft and drive the same generator. This design offers economic advantages as a result of low investment costs, excellent efficiency and a high degree of flexibility during operation.

The “Liberty” power project is one of seven for Siemens and Panda Power Funds in the United States, totaling over 5,800 MW. In addition to selecting Siemens to supply three Flex-Plants in Texas, Panda Power Funds chose Siemens to deliver three CCPPs in Pennsylvania – including “Liberty” and “Patriot” – and one CCPP in Virginia.

Siemens Celebrates Commissioning of Power Project in Pennsylvania Read More »

Practical Approach to Determining Effective Case Depth of Gas Carburizing

BOTW-50w  Source:  Gear Technology

“Effective case depth is an important factor and goal in gas carburizing, involving complicated procedures in the furnace and requiring precise control of many thermal parameters. Based upon diffusion theory and years of carburizing experience, this paper calculates the effective case depth governed by carburizing temperature, time, carbon content of steel, and carbon potential of atmosphere. In light of this analysis, carburizing factors at various temperatures and carbon potentials for steels with different carbon content were calculated to determine the necessary carburizing cycle time. This methodology provides simple (without computer simulation) and practical guidance of optimized gas carburizing and has been applied to plant production. It shows that measured, effective case depth of gear parts covering most of the industrial application range (0.020 inch to over 0.250 inch) was in good agreement with the calculation.”

Read More:  Practical Approach to Determining Effective Case Depth of Gas Carburizing by March Li

March Li Metallurgist, Automotive Heat Treating, Practical Approach to Determining Effective Case Depth of Gas CarburizingAuthor March Li -Metallurgist

Practical Approach to Determining Effective Case Depth of Gas Carburizing Read More »

TITAN® Vacuum Furnaces Take a Journey

Ipsen’s TITAN® product line has had quite the journey over the past few years. Found in facilities around the world, these vacuum furnaces can operate in most languages, feature several sizes and configurations and have a small footprint. Now, the PdMetrics® software platform for predictive maintenance also comes standard on TITAN heat-treating systems.

Most recently, Ipsen delivered two TITAN H2-size vacuum furnaces with 1.9-bar gas quenching and the PdMetrics platform to Japan. Shipped within three weeks of each other, these furnaces will be used by separate commercial heat treaters and feature 18” x 24” x 18” (455 mm x 610 mm x 455 mm) graphite hot zones with a 1,000-pound (450 kg) load capacity. They operate at temperatures up to 2,400 °F (1,320 °C) with ±10 °F (±6 °C) uniformity, and are capable of meeting applicable AMS 2750E and Nadcap requirements.

Through the PdMetrics platform – which securely connects to a network of integrated sensors on the furnace to gather and analyze data, run algorithms and provide real-time diagnostics – these TITAN furnaces provide sophisticated monitoring of critical systems and key parameters that improve the health and integrity of the equipment. Both companies also took a proactive approach to preventative maintenance by ordering one of Ipsen’s many spare parts kits. These kits consist of consumable and preventative maintenance items to help ensure equipment uptime and keep the furnace running smoothly.

Ipsen’s TITAN vacuum heat-treating systems provide an advanced solution in the form of speed, reliability and versatility of process capabilities. However, Ipsen is more than just an equipment manufacturer. They also offer expert-driven solutions for customers’ needs through all stages of the system’s life cycle, no matter the location – whether it is facilitating on-site installation, providing expert training and start-up assistance or delivering responsive field support and spare parts.

TITAN® Vacuum Furnaces Take a Journey Read More »

GE to Purchase LM Windpower

LM Group Holding A/S announces today that Doughty Hanson, the European private equity firm, has agreed to sell its stakes in LM Wind Power Holding A/S to GE for an enterprise value of EUR 1.5 billion.  The transaction is expected to close in the first half of 2017, subject to regulatory approvals. The acquisition is valued at 8.3 times 2016 forecast EBITDA. LM Wind Power Holding A/S is the parent company of LM Group Holding A/S. The closing of the transaction will constitute a change of control under LM Group Holding A/S’s EUR 130 million fixed rate notes due 2019 and NOK 475 million floating rate notes due 2020.

Originally founded in 1940 as a furniture manufacturer, LM Wind Power has evolved to become one of the leading manufacturers of rotor blades for the wind industry. It has a global manufacturing footprint of 13 sites in eight countries across four continents and continues to expand.

For the first half of 2016, the company reported sales of EUR 491 million and EBITDA of EUR 87 million which represented year-on-year growth of 40% and 81% respectively.  In June of this year, LM Wind Power unveiled the world’s longest ever blade at 88.4 meters long, demonstrating the Company’s continued strength in technology and manufacturing.

Commenting on the transaction, LM Wind Power CEO Marc de Jong, said:

“The offer from GE makes clear commercial sense for the growth of LM Wind Power and we are absolutely delighted with the prospects of having a world leader as our owner. It provides us with the necessary stability, visibility and strength to continue to realize the ambitious growth plans of the business and fully utilize our advanced design and technology, improve our manufacturing capabilities and reliability, expand our global footprint and reduce the Levelized Cost of Energy. It’s a great day for LM Wind Power and for the wind industry!”

GE to Purchase LM Windpower Read More »

Heat Treat Basics: Bringing Nadcap to the Medical Industry

BOTW-50w  Source:  Power Transmission Engineering June 2016

“For suppliers, the other way to get involved is obviously through getting audited for accreditation. If you’re interested in an audit, the process is fairly straightforward. Once in contact with MedAccred, a supplier details their products and figures out what categories they should be applying for.”

Find out what medical options are available to the heat treating world by reading:  Bringing Nadcap to the Medical Industry


Heat Treat Basics: Bringing Nadcap to the Medical Industry Read More »

Ampco-Pittsburgh Acquires ASW Steel Inc.


John Stanik CEO Ampco-Pittsburgh

John Stanik - CEO Ampco-Pittsburgh

Ampco-Pittsburgh said it would pay $3.5 million in cash and assume $9.6 million of the Welland, Ontario, company's liabilities. ASW will become a part of the Union Electric Steel Corp. division of Ampco-Pittsburgh. The manufacturing plant, with an electric arc furnace, is located close to the U.S.-Canadian border near Niagara Falls, N.Y., and Buffalo. It was founded in 1918 as the Dillon Crucible Steel Alloy Co. and was acquired by MMFX in 2010.

"This acquisition is a very important element in Ampco-Pittsburgh’s strategic diversification plan," said John Stanik, CEO of Ampco-Pittsburgh, in a statement. "ASW’s proven broad expertise in flexible steel refining methods will provide us with the capabilities to manufacture the additional chemistries needed to expand our reach in the open-die forging market. The transaction also enhances our ability to grow in markets in which we currently participate and to add new markets for customers in the oil and gas, power generation, aerospace, transportation, and construction industries.”

Ampco-Pittsburgh Acquires ASW Steel Inc. Read More »