Neil Hardy, Metallurgical Specialist and Creator of MetallurgyData (photo source: Neil Hardy)
In this Heat TreatLearningspecial, metallurgical technician and specialist Neil Hardy at MetallurgyDatashares about the background of developing his educational video endeavors for people in the heat treat industry. This information was taken from an interview with Heat TreatTodayand has been curated for educational purposes. This video is a part of Heat TreatTV.
Heat TreatLearning is a series of curated pieces for Heat TreatToday's audience, intended to aid end-users in their continual professional development. If you have a piece that you believe might be helpful on this platform, email any of our editors with your information and we will be in touch. Our contact info is Bethany Funk - bethany@heattreattoday.com, Karen Ganzter - karen@heattreattoday.com, or editors at editor@heattreattoday.com.
Back to the Basics: Heat Treatment Types, Processes and Structures
This "back to the basics" video demonstrates the different outcomes of heat treatment types, processes, and structures. In it, the video offers clear parameters for how and why different heat treating methods matter for particular metals and for intended outcomes. It is provided by MetallurgyData, a global informational training platform based on providing metallurgical principles to aid understanding for application.
MetallurgyData on YouTube
MetallurgicalData produces educational content, as well as topics of interest. "I am currently producing a video that follows the process of me replicating my late father’s wedding ring. He died at the age that I am now so this project has quite a lot of emotion associated with it for me," the creator of the platform, Neil Hardy, said, "This will be video-graphic ad show the process of making the ring while the other will be based around the science of each stage of the process including, melting, casting and forging."
About MetallurgyData and Neil Hardy
In 2005, Neil Hardy, a Metallurgical Specialist, gained his bachelor’s degree in material engineering while working in lab and testing settings. Continuing to work at an international steel company before finally arriving in 2010 at a UK forge, Neil's experience has been continuously focused on the cutting edge.
Recently in his career, Neil began something less bent on new technology but still cutting edge. A self-funded project, MetallurgyData, started about five years ago. "It evolved," Neil said, "from two ideas; the first was to produce an online property prediction calculator and the second was around providing online training courses."
While Neil did not pursue the property production calculator idea, the online training courses were a hit. They have evolved into the videos that are currently available on YouTube. "I think there is a gap in the market for producing online training courses in metallurgy and I initially thought to pursue this with a 'fundamentals in metallurgy' course."
[blockquote align="left"]I think there is a gap in the market for producing online training courses in metallurgy and I initially thought to pursue this with a "fundamentals in metallurgy" course.[/blockquote]
Neil is looking to expand his YouTube platform to provide additional content, and is eager to develop more videos for companies in order to facilitate more informational content for his growing audience.
For more information, email Neil Hardy at metallurgydata@gmail.com, message him via MetallurgyData on LinkedIn, or leave comments on his YouTube Videos.
Heat Treat Today publishes four print magazines a year, and included in each is a letter from the publisher, Doug Glenn. This letter first appeared in Heat Treat Today‘s Automotive Heat Treating magazine, June 2020.
Doug Glenn, Publisher, Heat Treat Today
For the record, the 2020 North American heat treat industry has been severely impacted by COVID-19. Everyone I’ve talked to agrees that the reality of 2020 will pale in comparison to the hopes and dreams for 2020 back in January and February of this year. March and April usually bring spring-like optimism, but this year those two months were marked by a grinding of the US economy to a nearly complete standstill, the heat treat industry included. As one of our Latvian foreign exchange visitors said in his broken English, “NOT GOOD.” Thus, it has been; and thus, it is even as of this writing.
Every situation, however, is 20% situation and 80% what you make of it, so let me suggest four positive things that will come out of this historic economic tragedy.
#1 “Sheltering at home” for 6-8 weeks might help us all slow down. For the vast majority, we’ve all been slowly heated in the waters of busyness to the point where we think it is normal. During my recent conversation with the executive director of an industry association, this person said, “I’m in favor of anything that will help us all slow down.” This person was fully convinced that our “normal” pace is not healthy. Perhaps this person was right. One other individual I spoke to was “forced” to ignore work for two weeks. His company furloughed individuals and sternly warned them NOT to check emails while furloughed because the company could be sued if furloughed workers were actually working. The national market manager that told me this story did so from his personal cell phone while preparing to paint a room in his house. No work for him. Like many of us, he had to slow down.
#2 Interacting face-to-face with other human beings is important. I know that many of you introverts are loving the forced isolation, but even you must admit that after a week or more seeing no one, it would be nice to be able to at least go somewhere where you can actually see and talk to other human beings besides those with whom you are confined to quarters. My favorite example of this are all of the technologically savvy young people who live on their phones. As long as they have their phones, they’re content. Come to find out, many of these now homebound young ones are now MISSING SCHOOL, not so much for the academics, but more for the interaction with their peers – even if it is sitting next to each other with their heads in their phones! People matter. COVID is helping us remember.
#3 COVID, or more accurately, the RESPONSE to COVID, is helping us all remember just how quickly we can lose our freedoms. For many of us, we lost the freedom to go to work, we lost the freedom to freely assemble, we lost the freedom to travel where and when we like, we lost the freedom to walk around without a mask, we lost the freedom to walk up a grocery store aisle in either direction, and we’ve even lost the freedom to worship where and when we like. Some even argue that we’ve lost our freedom of speech! Try asserting the opinion that the actual COVID virus is not significantly more dangerous than a normal flu. Try it once; you’ll not do it again! Of course, most of these freedoms will be lost only temporarily and for a good cause – our safety. But please remember what King Mongkut (Yul Brynner in The King and I) said about finding safety from others, “Might they not protect me out of all I own?” Or take it from Ben Franklin – “Those who would give up essential liberty, to purchase a little temporary safety, deserve neither liberty nor safety.”
#4 And finally, COVID is helping us all see just how quickly life can change … and this is a good thing … because it is true. We think we are safe, we think we are secure, we think that life will always be this way, we think we are in control. We are wrong. There’s only One in control – assuming you believe in God – and we are not Him. This might be a scary thought for some – to not be in control. But, it is better to live in an unpleasant reality than a dangerous fantasy. COVID is helping us deal with reality.
So, there’s a lot of good coming from this pandemic. Here’s to a more modestly paced life, here’s to time with friends and family, here’s to liberty, here’s to remembering Who’s in charge … and here’s to your health and safety and a return to a more “normal” North American heat treat market.
An international aerospace manufacturer orders two furnaces for its factories in the USA and Singapore. While both are single-chamber vacuum furnaces, they will serve different functions. One will be used for the heat treatment of exotic electrical steels, and the second will be used for annealing parts produced by 3D printing technology.
The furnace purchased for the heat treatment of exotic electrical steels has diffusion vacuum levels and a horizontal chamber. The chamber has the workload size of 24” x 24” x 36” and a 1300 lb. hearth capacity. Additionally, each furnace has a single-chamber, high pressure gas quench heat treat system adaptable to a wide variety of thermal processing applications including annealing, brazing, hardening, LPC and LPN, normalizing, solution heat treating, sintering and tempering.
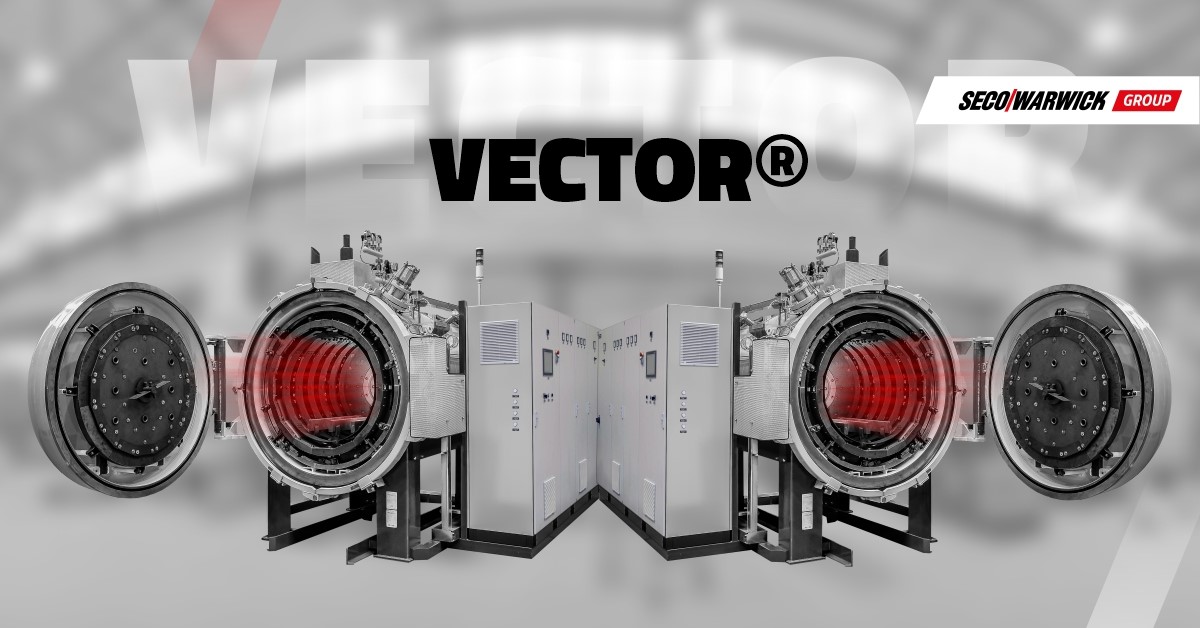
Two SECO?WARWICK Vector Furnaces (photo source: SECO/WARWICK)
Each of the furnaces were bought from SECO/WARWICK Vector furnaces lines. This is the manufacturer's first purchase for a US installation from this supplier. The Vector furnaces lines are used in multiple applications within the aerospace sector, including heat treating turbine blades and landing gear, as well as in the aerospace aftermarket to maintain fleets of aircraft.
Maciej Korecki, Vice President of Vacuum Business Segment, SECO/WARWICK (photo source: SECO/WARWICK.com)
“SECO/WARWICK Group," commented Maciej Korecki, Vice President of Vacuum Business Segment at SECO/WARWICK, "has delivered hundreds of Vector heat treat systems worldwide, many of which are in steady use supporting the aircraft industry. We offer Vector with either a horizontal or vertical chamber depending on part configuration and the process needs of the customer, and we support each customer all over the world with a dedicated team of aftermarket professionals to keep them running at peak efficiency.”
Vector 3D builds upon the single-chamber vacuum furnace technology to combine the advantages of gas quenching capabilities with the growing requirements of the additive manufacturing market. The result allows customers to perform processes such as sintering, debinding, stress-relieving, aging or solution heat treatment, which are essential for the metal 3D printing sector. It has numerous applications in such industries as aerospace, automotive, medical and energy.
Solar Atmospheres of Western PA is currently installing a new rapid quenching vacuum furnace that will ultimately eliminate the need for costly helium while increasing production throughput. In helium's place, the new furnace will use nitrogen only in the hardening process.
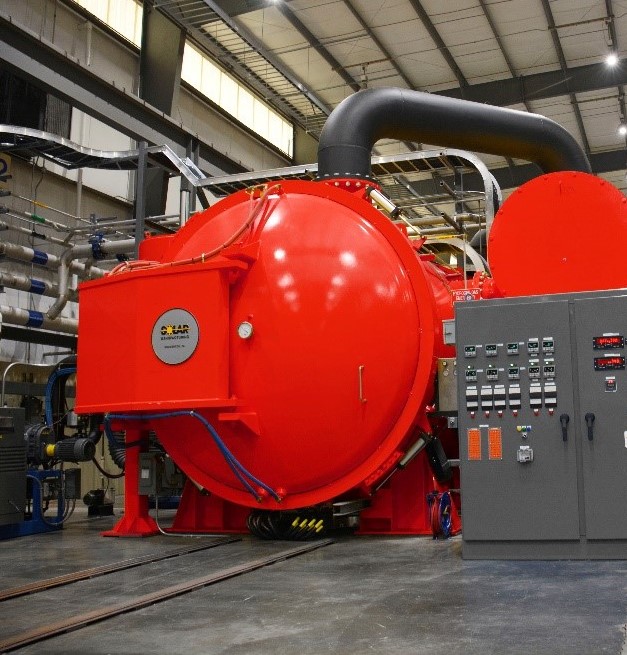
Solar Manufacturing Rapid Quench Furnace for Solar Atmospheres of Western PA (photo source: Solar Atmospheres)
The new 48” x 48” x 96” deep 10 bar vacuum furnace is produced by Solar Manufacturing. The important difference in this furnace from its older model is the cooling design, which is equipped with a 600 HP blower designed motor. This will allow the new furnace to outperform its older model by processing larger and heavier workloads with the use of nitrogen only.
Bob Hill, President, Solar Atmospheres of Western PA
“The difference in operating costs is a no brainer,” states president of Solar Atmospheres, Bob Hill. “To marginally harden one 2000-pound high-speed tool steel roll die in our older 2 bar vacuum furnace, the use of light helium gas was a necessity. The prohibitive cost of a two atmosphere helium backfill was $1,065. Our new furnace will enable us to fully harden three 2000-pound roll dies at once using the more cost-effective process gas of nitrogen. In contrast the cost of a 10 atmosphere backfill of nitrogen will be only $89.” Hill predicts that with these increased efficiencies and savings, his normal ROI on a new piece of equipment will be significantly advanced.
Once operational, Hill will author a technical paper with the actual cooling data derived from these similarly sized vacuum furnaces.
One of the great benefits of a community of heat treaters is the opportunity to challenge old habits and look at new ways of doing things. Heat Treat Today’s101 Heat TreatTipsis another opportunity to learn the tips, tricks, and hacks shared by some of the industry’s foremost experts.
Today’s tips come to us from Control Concepts, covering SCR Environmental Conditions. Another contributor, Messer, also shares a tip on “Preventing Furnace Downtime.” These are great tips to make those fixes that can fly under the radar.
Heat Treat Today welcomes you to submit your own heat treat tip for the 2020 Heat Treat Today fall issue to benefit your industry colleagues. You can submit your tip(s) to karen@heattreattoday.com or editor@heattreattoday.com.
Heat Treat Tip #50
Using a Grounding Rod in Noisy Environments
This may be beneficial if you have a bad system ground. (Control Concepts)
Heat Treat Tip #51
Seal Away Dirt or Dusty Environments
Use a sealed enclosure or alternative cooled power controllers for dirty and dusty environments. For heavy dirt or dusty environments, a sealed cabinet with air conditioning or filters is recommended. Alternatively, select a SCR manufacturer that offers external mount or liquid cooled heatsinks to allow you to maintain a sealed environment in order to obtain maximum product life. (Control Concepts)
Heat Treat Tip #52
De-Rate Controller Above 6,000 Feet
De-rate controller for installations above 6,000 feet. As the air thins at increased elevations, natural convection and forced air cooling becomes less efficient. Follow the manufacturer’s recommendations for de-rating the SCR power controller above 6,000 feet altitude. (Control Concepts)
Heat Treat Tip #64
Prevent Furnace Downtime
If your atmosphere heat treatment furnace is experiencing frequent downtime, and circulation fans fail, it is probably time for an upgrade. New injection mixing technology uses nitrogen to stir the atmosphere and maintain its uniformity. (Messer)
In the following original content from Heat Treat Today, Thermo-Calc Software's Adam Hope, PhD, materials scientist, and Paul Mason, president, delve into how modeling and simulation tools can help heat treaters make well-informed decisions.
This article first appeared in the latest edition (March 2020) of Heat Treat Today’sAerospace Heat Treating magazine.
Consistency in material properties and performance is critical to the aerospace industry, and small variations in material chemistry or process windows can have a large impact on the final parts performance. The ability to predict and adjust for these variations can reduce scrap and part re-work. Metallurgists and process engineers responsible for heat treatments must adapt their process when input variables change, such as material chemistry. They are routinely faced with questions such as:
Paul Mason President Thermo-Calc Software
*How will heat to heat variations affect the final part performance?
*What heat treatment should be given to a part that has been built via a novel approach such as additive manufacturing?
*How should one optimize a heat treatment schedule for a new alloy?
*When the data required to make these decisions does not exist, what are the options?
Experiments can generate this data, but this is costly and time-consuming. Handbooks might have data for known alloys, but this is often only for the nominal composition and may not be suitable for material processed under a novel route. Modeling and simulation tools can help fill this knowledge gap and help inform better decisions.
Integrated Computational Materials Engineering and CALPHAD
Adam Hope, PhD Materials Scientist Thermo-Calc Software
The publication by the National Academies in 2008 on Integrated Computational Materials Engineering (ICME)[1] outlined an approach to designing products, the materials they are comprised of, and their associated materials processing methods, by linking materials models at multiple length scales. The report highlighted the need for a better understanding of how processes produce material structures, how those structures give rise to material properties, and how to select materials for a given application, describing the need for using multiscale materials modeling to capture the process, structures, properties, and performance of a material.
Computational thermodynamics, and specifically CALPHAD (CALculation of PHase Diagrams)[2], enables the prediction of the thermodynamic properties and phase stability of an alloy under stable and metastable conditions. The CALPHAD approach captures the underlying composition and temperature dependence of properties and can also be extended to model atomic mobilities and diffusivities in a similar way. By combining thermodynamic and mobility data, kinetic reactions during solidification and subsequent heat treatment processes can be simulated. Computational thermodynamics and CALPHAD- based tools are an important component of an ICME framework because, through the use of such simulations, it is possible to vary alloy compositions and predict optimal solidification processes and solution heat treatment temperature ranges without performing many time-consuming and costly experiments.
Predicting Heat Treatments for Additively Manufactured Parts
Many additive manufacturing processes subject the material to rapid solidification with multiple subsequent reheat cycles. The effect of these thermal cycles on material properties is not always known and typically does not result in the properties that a similar cast or wrought metal would have. Additionally, many additively manufactured parts are built using conventional alloys which have been engineered for cast or wrought processes. In some cases these alloys are not suitable for additive processing, and problems such as deleterious phases forming during a post-build, stress-relief heat treatment, designed for conventionally treated alloys, may result.
Additive processes are typically associated with rapid cooling rates and large thermal gradients. This can give rise to the following:
High levels of residual stress in the final part
Microsegregation during solidification of each layer, which leads to local inhomogeneities in alloy composition
In the case of additive manufacturing, these separate heat treatments are often combined, and stress relief heat treatments designed for cast or wrought material may not be suitable for additively processed materials for two reasons:
The chemical inhomogeneities arising from rapid cooling can influence precipitation behavior, and some deleterious precipitates may precipitate more quickly than expected.
The multiple heating cycles of subsequent layers may have already started some precipitation reactions, making stress relief more difficult without first homogenizing these precipitates.
Zhang et al.[3] have studied laser powder bed builds of Alloy 625 and found that after applying an industry recommended stress relief heat treatment, delta phase can precipitate in the segregated regions much faster than in the wrought material. The formation of delta phase is extremely detrimental to material properties. They attributed this to increased Nb and Mo concentrations found in the interdendritic regions in the as-built microstructure.
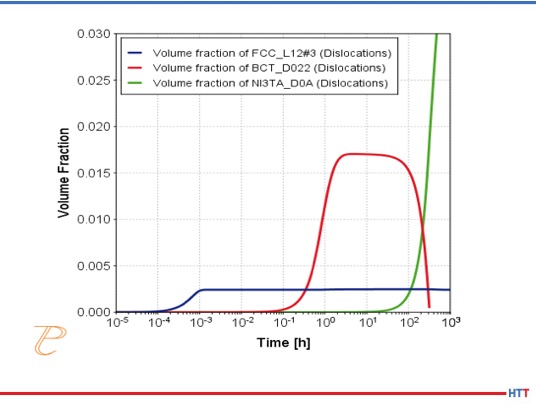
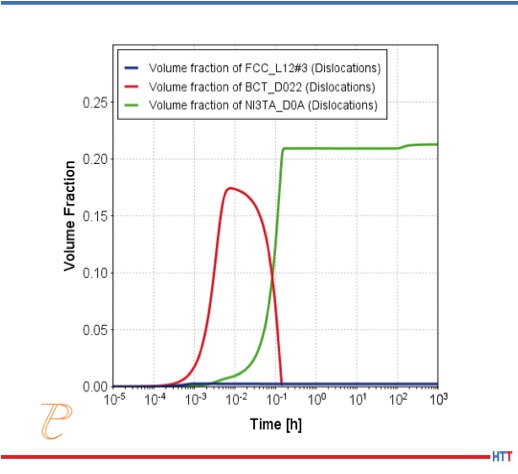
To understand this further, the authors first simulated the extent of this segregation using the Scheil-Gulliver model for solidification in Thermo-Calc[4] in conjunction with the diffusion module, DICTRA[4]. They then used the Precipitation module, TC-PRISMA to predict the precipitation kinetics of the deleterious delta phase for nominal feedstock compositions, as well as the compositions measured at dendrite boundaries. Both simulations, shown in Figures 1a and 1b, predict that a stable MC carbide forms, followed by some gamma double prime. Delta phase then forms at the expense of the gamma double prime. However the gamma double prime and delta phase both precipitate much more quickly in the segregated interdendritic region, due to the increased Nb and Mo. Delta phase is predicted to start forming around 1 hour, compared with 10 hours for the wrought material.
Figure 1. TC-PRISMA Precipitation simulations using nominal IN625 powder compositions (top) and segregated compositions (bottom) measured at the dendrite boundaries. Recalculated based on Reference 3.
While these calculations give insight to the reason why the conventional stress-relief heat treatment is not suitable, additional simulations can be made to identify a suitable temperature and time to both homogenize and stress-relieve the part, while avoiding deleterious phases. The authors of the study determined a post-build homogenization treatment was required to avoid deleterious delta phase precipitation.
Gas Carburizing Highly-Alloyed Steels
Highly-alloyed stainless steels can be gas carburized to increase the surface hardness, as well as improve the overall mechanical characteristics of the surface. However, an increase in chromium-rich carbides such as M23C6 or M7C3 can result in the decrease of chromium in the solid solution which leads to a reduction in corrosion resistance. Balancing these properties can be time consuming through trial and error experimentation, but CALPHAD-based tools can be used to identify suitable alloy compositions and heat treat windows, which are optimal for the application needs prior to testing in the laboratory.
Turpin et al. 5 made such a study, combining both experimental work and theoretical simulations to investigate carbon diffusion and phase transformations during gas carburization of high alloyed martensitic stainless steels. First, using thermodynamic calculations performed with Thermo-Calc 4 they determined the optimal balance between the carbide formation and chromium content of the alloy for corrosion resistance. They concluded:
At 1750°F (955°C), which corresponds to the austenitization temperature of their alloy, M23C6 and then M7C3 will be the first carbides to precipitate in the austenite phase as the amount of carbon content in the alloy is increased.
If the amount of carbon exceeds 3.8 wt% then M3C carbides are predicted to be stable. M3C carbides have a structure similar to cementite and preferentially precipitate at the grain boundaries which weaken the microstructure. Therefore, to avoid these phases, the overall content of carbon in the steel must be below this amount at the end of the carburizing process.
Above 1.7 wt% C, the mole fraction (an indicator of the volume fraction) of M7C3 carbides exceeds 20%, and the chromium content of the alloy associated with these carbides is 65 wt%. Therefore, there is a correspondingly strong depletion of chromium from the matrix.
To balance the desire for adding carbon into the matrix phase to obtain hardness with depleting the matrix of carbon, it was determined that the optimal amount of carbon in the matrix phase should not exceed 1 wt%. Thus, the thermodynamic calculations were used to establish a limit, without yet any consideration of the kinetics or time.
The second stage of the study then considered the diffusional reactions in the multi-component system during i) the carbon enrichment step and ii) the diffusion step of the gas carburizing process, and to determine how the composition and the amount of each phase vary with time and distance from the gas/solid interface and the carbon profile of the alloy as a function of time and distance. These calculations were made using the diffusion simulation software, DICTRA 4.
Consider the carbon enrichment step first. In DICTRA, several boundary conditions can be used for such a simulation, and in this work the carbon flux was determined experimentally using thermogravimetric measurements. During the diffusion step, the N2-CH4 mixture is replaced with pure N2, and the carbon flux at the surface of the samples is zero. To simulate this step using DICTRA, a zero carbon flux was applied as the boundary condition for two hours.
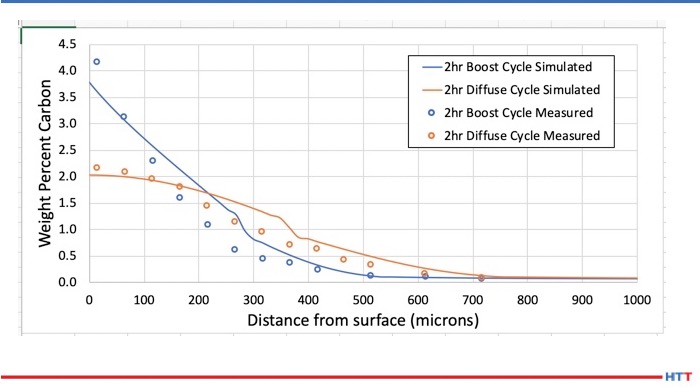
Figure 2 shows a simulated carbon profile for Fe-13Cr-5Co-3Ni-2Mo-0.07C, which is found to be in good agreement with the experimental values reported by Turpin et al. The authors concluded from this study that the carbon profile can be calculated and followed at any time if the boundary condition evolution at the gas-solid interface is known during the carburizing treatment.
Figure 2. DICTRA carbon diffusion profiles for Fe-13Cr-5Co-3Ni-2Mo-0.07C. Recalculated based on Reference 5.
Predicting β-transus Temperatures in Ti-Alloys
Many Titanium alloys respond well to heat treatments, through which the microstructure can be manipulated to optimize properties for a particular application. For example, some microstructures are better for high temperature creep, and some are better for fatigue strength. This is primarily achieved by controlling the nature and amount of α and β phases in the microstructure.
At high temperatures, titanium alloys are primarily β phase. At the β-transus temperature, the α phase becomes stable and can start to form. The β-transus temperature can change as a function of alloy chemistry. Knowing the β-transus temperature is critical to determining the nature and amount of α phase that will form during a heat treatment or thermal cycle.
Many alloying elements in Ti alloys have a strong effect on β-transus temperature. Knowing the actual β-transus for a specific chemistry is critical to determining suitable heat treating windows to obtain a specific set of material properties. However, even within a particular alloy specification, there can still be small compositional variations that have a significant effect on the β-transus. Thermo-Calc [4]can be used to calculate this if the exact chemistry is known, or to determine the potential distribution of β-transus temperatures for a given chemistry range.
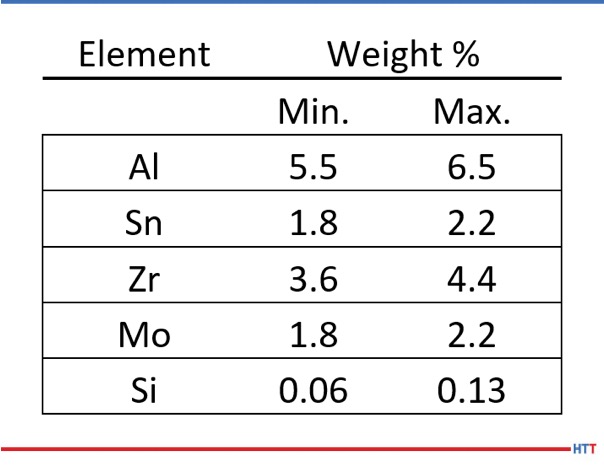
Table 1 -- Composition specification for major elements in Ti-6-2-4-2 Alloy
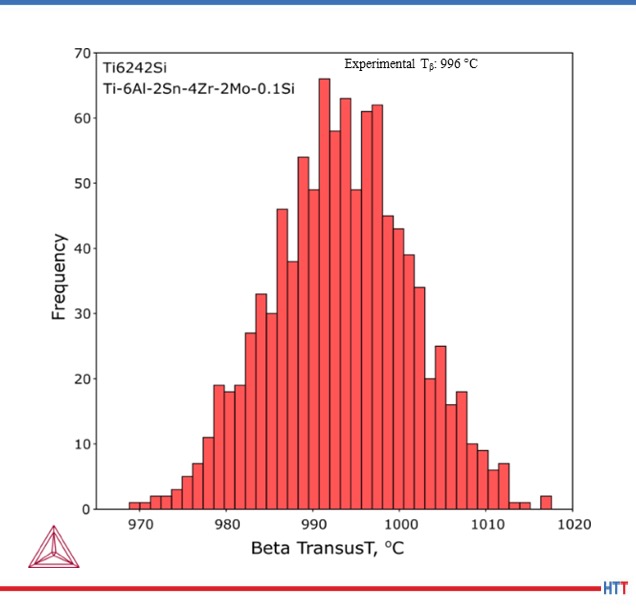
Table 1 shows the composition ranges for the major elements in Ti6-2-4-2Si (AMS 4919). Figure 3 shows the calculated distribution of β-transus temperatures in the composition specification of Ti6-2-4-2. Over 40 degrees variation is possible for compositions that lie within the specification and the calculations show good agreement with the experimentally measured values of 995°C ± 15°C (1823°F ± 27°F).[6]
Figure 3. Variation in Beta transus temperature for 1000 possible compositions within Ti-6-2-4-2 specification
Summary
In the 100th Column of the Heat Treat Doctor [7],Dan Herring, stated that heat treating can best be defined as “the controlled application of time, temperature and atmosphere to produce a predictable change in the internal structure (i.e. the microstructure) of a material.” However, variability arising from composition differences in materials can sometimes be challenging for heat treaters. The examples shown here have illustrated how modeling and simulation tools such as those based on the CALPHAD approach can be used to predict variability arising due to material composition. HTT
References
[1] National Research Council. 2008. “Integrated Computational Materials Engineering: A Transformational Discipline for Improved Competitiveness and National Security.” Washington, DC: The National Academies Press.
[2] Kaufman, L and Bernstein, H. Computer Calculation of Phase Diagram. New York: Academic Press Inc, 1970.
[3] Zhang, Fan, et al. “Effect of heat treatment on the microstructural evolution of a nickel-based superalloy additive-manufactured by laser powder bed fusion.” Acta Materialia 152 (2018) pp 200-214.
[4] Andersson, J O, et al. “Thermo-Calc and DICTRA, Computational tools for materials science.” Elsevier, CALPHAD, Vol. 26, (2002) pp. 273-312.
[5] Turpin, T, et al. “Carbon diffusion and phase transformations during gas carburizing of high-alloyed stainless steels: experimental study and theoretical modeling.” Met. Trans. A, Vol. 36A, (2005) pp 2751-2760.
[6] TIMET datasheet for TIMETAL® 6-2-4-2, TMC-0157 (2000).
[7] Herring, D “What is Heat Treating and Why Do We Do It?” Industrial Heating Magazine BNP Media (2011).
About the authors:Paul Mason is the president and Adam Hope, PhD is a materials scientist for Thermo-Calc Software, whose products assist academia, government, and industry to make calculations which predict or assist in the understanding of complex multicomponent alloys and non-metallic systems, as well as processes of industrial and scientific relevance.
For more information, contact Paul or Adam at info@thermocalc.com or (724) 731 0074
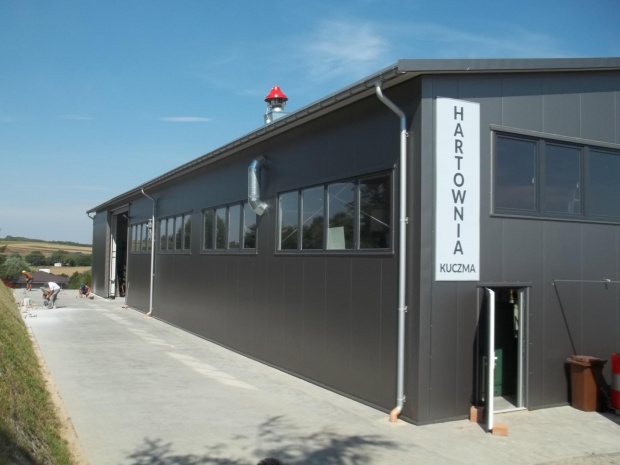
A family-run, commercial heat treating plant in Rzeszów, Poland, Kuczma Hardening Plant, will expand its heat treating capabilities with a new single-chamber vacuum furnace. A particular addition to this furnace is the directional cooling, which will allow the plant to perform quenching from both the sides and the top and bottom in order to precisely adjust the gas cooling system to the batch configuration.
The Vector® vacuum furnace from SECO/WARWICK is equipped with 1.5 bar gas quenching pressure. It will increase the capacity of the Kuczma Hardening Plant and will enable the plant to process parts with dimensions up to 600x600x900 mm. This furnace model specializes in heat treating many types of materials and metal alloys; additionally, its functionality includes gas hardening and tempering, annealing, brazing and degassing.
"Kuczma Hardening Plant," said Jerzy Kuczma, Kuczma Hardening Plant owner, "specializes mostly in vacuum quenching in gas, oil and gas nitriding of injection mould components and dies... On one hand, the SECO/WARWICK furnace will enable us to process larger components and increase our output for smaller ones on the other it will enable directional cooling sideways or top/bottom."
The hardening plant also performs carburizing, quenching, and tempering under protective endothermic atmosphere as well as clean stress relieving under nitrogen atmosphere.
Welcome to Heat Treat Today'sThis Week in Heat TreatSocial Media.As you know, there is so much content available on the web that it's next to impossible to sift through all of the articles and posts that flood our inboxes and notifications on a daily basis. So, Heat Treat Todayis here to bring you the latest in compelling, inspiring, and entertaining heat treat news from the different social media venues that you've just got to see and read!
"Quality aerospace bolts are more rigorously tested, more carefully manufactured, and more carefully studied than almost any other component on an aircraft. The reason?" Read more here, and check out the video to see high-impact landing that is required of fighter jets. See 5:10-8:06 for a forced landing on a stool when the pilot's nose gear failed.
2. Hot Heat Treat Technologies
Walk through this CGI Animation of Vacuum Brazing process to see the breakdown of the heat treating process without getting burnt.
3. Advancing Technologies
Check out TWO uses of cutting edge digital systems when applied to heat treat, and industry related processes. See below for the videos.
Digital Transformation of Thermal Processes
.
Tracking All Processes with Digital
SMS Digital: BIG RIVER STEEL - THE FIRST LEARNING STEEL PLANT
4. The Podcast and Reading Corner
Ever wanted to have access to resources for on the job training? Read or listen to the sources below to learn a new technique, tip, or other aspect of the industry.
.
A NEW Metal? Check out what carburizing and hardening can do.
"...carburized A-21 exhibited superior corrosion resistance in salt fog testing versus the other stainless steels. It also maintained good core mechanical properties of..."
.
The "How" Behind Nitrex's Rebranding
.
Finding a Balance: Read Ipsen's Blog, The Herald, on additive manufacturing and the thermal processing industry.
[blocktext align="center"]"Additive manufacturing is a disruptive technology with the potential to lower cost, increase speed and create parts once thought to be too complex and intricate to manufacture by conventional methods."[/blocktext]
"Balancing the Speed and Technology of Additive Manufacturing with the Mature and Methodical Thermal Processing Industry" (photo source: IpsenHarold.com)
5. Metal Music
Finally, here is some not-so-heavy metal music to start your weekend. Big thanks to Rosanne Brunello of Mountain Rep for the find! Have a great weekend, folks.
The rebuild included a new 330 stainless steel muffle, new silicon carbide heating elements, new cooling sections, and new furnace controls to meet CQI-9 requirements. The CQI-9 controls package includes data acquisition, preventative maintenance alerts, remote connectivity, furnace parameter trending, and temperature deviation alarms.
The partner chosen for this rebuild, Gasbarre Thermal Processing Systems, designs, manufactures, and services a full line of industrial thermal processing equipment, offering batch and continuous thermal processing equipment for both atmosphere and vacuum applications as well as a full line of alloy fabrications, replacement parts and auxiliary equipment.
Magnetic Shields Ltd. of Kent, England, a producer of medical industry equipment, has ordered a new vacuum furnace for their facility, set to be one of the largest horizontal vacuum furnaces in the UK.
Solar HFL-7496-EQ Vacuum Furnace (photo source: Solar Manufacturing)
The new HFL-7496-EQ vacuum furnace, being built with a SolarVac® Polaris control system, will be designed to accommodate loads up to 48” wide x 48” high x 96” deep, (1220 x 1220 x 2440mm) with a maximum weight of 5,000 lbs (2270 kgs). Operating at a vacuum level of 10-5 Torr, the furnace will be able to reach temperatures up to 2400°F (1315°C). It will feature a partial pressure hydrogen gas process and an external quench system designed for negative pressure quenching.
Magnetic Shields Ltd. Director Colin Woolger (see image below) says, “Magnetic Shields is delighted to order our second vacuum furnace from Solar Manufacturing. The new furnace will enable us to more than double the maximum size of shields we can now produce in one piece and also increase the general heat treatment capacity for our growing company... We look forward to the new furnace arriving later this year.”
Magnetic Shields Ltd. of Kent, England began its relationship with their seller, Solar Manufacturing of Sellersville, PA, in 2016 when Magnetic Shields Ltd. bought a vacuum furnace from the heat treating furnaces provider.
Rick Jones, VP of International Sales at Solar Manufacturing also adds, “Solar Manufacturing is very pleased to be selected as the supplier to further support Magnetic Shields in leading the production of equipment for the medical industry and other high technology applications, specifically, high performance large magnetic shields and low field shielded rooms.”
Read more about Magnetic Shields Ltd.'s first vacuum furnace from Solar Manufacturing in this press release.
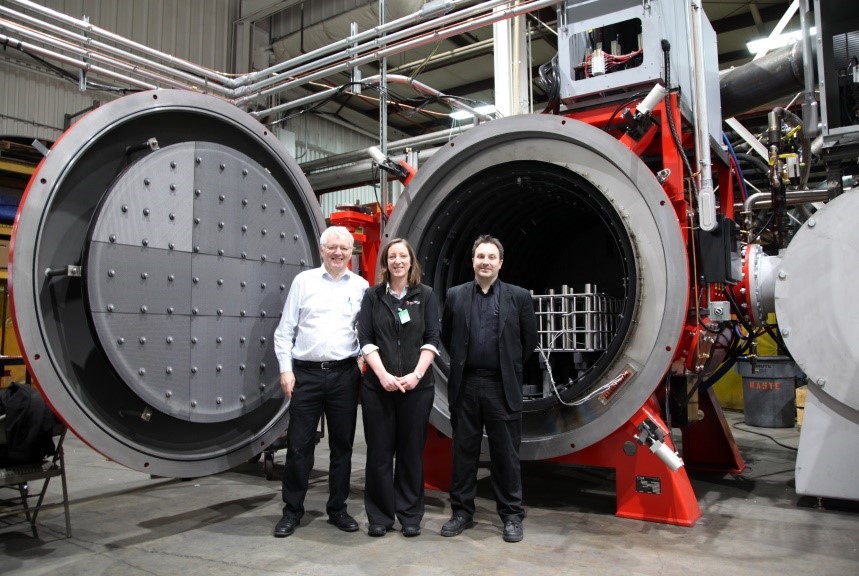
To read more about the 2017 Magnetic Shields Ltd.'s reception of their first Solar Vacuum Furnace, click here. Pictured on the left is Colin Woolger, Chairman of the company, Suzie McKay, Rob Latter. (Photo source: magnetshields.co.uk)





 Heat Treat