Pulse Plasma Nitriding Improves Surface Treatment, Wear Resistance, Fatigue and Material Performance

OCPulse plasma nitriding systems deliver uniform case-hardening and increased speed of processing when treating high wear parts.

Did you think purple was just a fashion statement? Explore the advantages, applications, and future of advanced pulse plasma nitriding in this Technical Tuesday. Heat Treat Today hopes you enjoy this original content piece by technical writer Jeff Elliott in cooperation with PVA TePla.


Jeff Elliott
Technical Writer
Source: Jeff Elliott

When case-hardening the surface of steel, or steel alloy parts, commonly used in the transportation industry, such as gears, crank pins, dies, camshafts, the options have traditionally included one-of-three processes: carburizing, salt-bath nitrocarburizing and gas nitriding.  Each process has advantages and disadvantages, but those seeking more precise control of the diffusion layer formation, depth of case hardening, and preservation of component dimensions are increasingly turning to plasma nitriding.

Although pulse plasma has been utilized for decades, advanced pulse plasma nitriding offers absolute control of the DC (direct current) pulsing signal.  In addition, improved chamber design and construction allow for more precise temperature control and uniform distribution of the heat zone throughout the hot-wall chamber. The result is extremely consistent and uniform nitriding batch-to-batch and part-to-part, with less gas consumption.

“The benefits are more precise control of the diffusion layers, and its broader appeal to heat treat more diverse materials, beyond steel, that include titanium, stainless steel, and even aluminum,” says Thomas Palamides, senior product and sales manager at PVA TePla America.

In addition, commercial heat treat shops and high-volume part producers can now select from multiple system configurations that offer flexibility, efficiency, repeatability, and throughput optimization. As a result, global manufacturers in machined parts, tool design, die forming, die cutting, medical device manufacturing, additive manufacturing, electric vehicles, trains, electric generators, and land-based power systems are now leveraging these systems to run a cleaner, more efficient operation.

Pulse Plasma Nitriding Advantages

For steel and steel alloys, case-hardening can be achieved by carburizing, nitriding, cyaniding, or carbonitriding. Although carburizing is a traditional approach, the part has to be raised above the A3 temperature (727°C or 1341°F) on the Iron-Carbon diagram, usually in the temperature range of 900-930°C (1652-1706°F) or higher. Since the solubility of carbon is higher in the austenitic state, than the ferritic state, a fully austenitic state is required for carburizing.

Along with the high temperatures and time-at-temperature associated with carburizing, parts can be distorted. Depending on the part, and its geometric tolerances, limited machining may also be required.

An alternative to carburizing is nitriding, a lower-temperature, time-dependent, thermo-chemical process used to diffuse nitrogen into the surface of metal.

Superior controls for the DC pulsing signal and improved chamber design allow for more precise temperature control.
Source: Jeff Elliott

One method is salt bath nitriding. In this process, liquid immersion is required, and is typically conducted at 550 to 570°C (1022 to 1058°F). The source of nitrogen is a nitrogen-containing salt, such as sodium cyanide, often greater than 50% in concentration. However, with salt bath nitriding, post-bath cleaning is required to remove the residual cyanide-based treatment. In addition, there are disposal costs for salt and washing , also known as sodium hydroxide, environmental handling costs, as well as safety and operational liabilities.

Gas nitriding (500oC or 932°F) and gas nitrocarburizing (540-580oC or 1004-1076°F) are universally accepted procedures, and typically require a high concentration of ammonia (NH3), and a high amount of carrier gas flow (normal pressure process) compared with pulse plasma nitriding.  The elemental nitrogen gas constituent diffuses into iron and forms hard nitrides.  Because of the reduced temperature compared to carburizing, no quenching is necessary, and therefore the chance for distortion and cracking are lower.

Several disadvantages of gas nitriding are that it requires the use of flammable gases like ammonia, and high gas consumption compared to pulse plasma.  Gas nitriding is also not able to treat rust- and acid-resistant steels (i.e. stainless steels with greater than 12% Cr content) due to the impenetrable layer of the protective surface oxide layer.  Where as the energized pulsed plasma signal, during heat up, allows for the dissolution, or breakdown, of this thin protective layer, in effect cleaning the surface, allowing atomic nitrogen to penetrate.

With recent advancements in pulse plasma nitriding, however, a new level of precision and control is possible which results in uniform and consistent case hardening. Together with the advantages of using environmentally friendly gases only – in contrast to the use of ammonia in gas nitriding – plasma-based nitriding has become a focal point for additional innovations and a requirement for those that seek a more environmentally and safe solution.

In pulse plasma nitriding, parts are loaded into a heated vacuum chamber. After evacuating the chamber to a working pressure of 50 to 400 Pa, on a supporting fixture, to be covered by a bell chamber.  The chamber is evacuated to below 10 Pa (7.5 x 10⁻² Torr) prior to heating and a pulsating DC voltage of several hundred volts is applied between the charge (cathode) and the chamber wall (anode).  The process gas in the chamber is then ionized and becomes electrically conducting. For this type of process, nitrogen and hydrogen gas mixtures and gases with carbon additions, like methane are often utilized.

Depending on treatment time and temperature, nitrogen atoms diffuse into the outer zone of components and form a diffusion zone. This can be is atomic nitrogen, dissolved in the iron lattice, as well as in the form of included nitrate deposition.
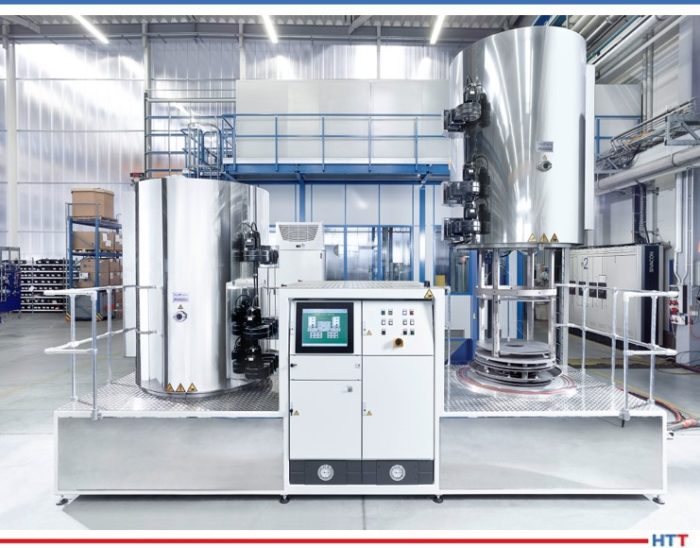
With recent advancements in pulse plasma nitriding, a new level of precision and control is possible.
Source: Jeff Elliott

Adding further precision, innovators in advanced pulse plasma have discovered methods to optimize the process through better control of the pulses. In the PulsPlasma® process developed by PVA TePla AG Industrial Vacuum Systems, for example, a precision regulated gas mixture of nitrogen, hydrogen, and carbon-based methane is used. A pulsating DC voltage signal of several hundred volts is delivered in less than 10 microseconds per pulse to ionize the gas. This serves to maximize the time between pulses for superior temperature control throughout the chamber.

“If you have a temperature variance of plus-minus 10 degrees within a batch, you will get completely different treatment results,” says Dietmar Voigtländer, sales manager at PlaTeG – Product Group with PVA Industry Vacuum Systems (IVS), Wettenberg, Germany, the manufacturer of PulsPlasma nitriding systems. “However, by controlling the pulse current by means of an exact pulse on and off time management, the overall temperature can be precisely managed with a uniform distribution, from top to bottom, throughout the hot wall chamber.”

A unique feature with this approach is that the system can be switched on to a stable glow discharge at room temperature. Most systems cannot do this because the generators do not supply stable plasma. To compensate, those systems must first be heated to 300-350°C (572-662°F) before plasma can be applied, adding time to the process.

[blocktext align="left"]“The benefits are more precise control of the diffusion layers, and its broader appeal to heat treat more diverse materials, beyond steel, that include titanium, stainless steel, and even aluminum." -Thomas Palamides, PVA TePla America.[/blocktext]Even the materials of construction used to manufacture the nitriding systems furnace itself have been optimized. In all systems, PlaTeG uses insulative materials developed in the aerospace industry to create a furnace wall as thin as 40 millimeters, compared to the industry standard of 150 millimeters. With less wall mass, the furnace requires less energy and time to heat, while still protecting workers that may accidentally touch the outside of the chamber.

With better overall control, advanced pulse nitriding furnaces offer multiple heating and cooling zones with each controlled by its own thermocouple. “This will create a very uniform temperature distribution within plus or minus 5 degrees Celsius (9 degrees Fahrenheit) from the bottom to the top of the furnace,” said Voigtländer.

Uniformity of temperature within a chamber pays a dividend beyond the consistency of nitriding results. With an even temperature throughout the chamber, the entire space is available for loading components which effectively increases the chamber’s capacity.

Stainless Steel – a Softer Steel

One of the key advantages of pulse plasma nitriding is that it is more suited to heat treating of high alloy materials such as stainless steel. When working with steels that have a higher chromium content, liquid nitriding can react with chromium and other elements, resulting in a loss of corrosion resistance.

Stainless steel has a natural passivation layer of chromium oxide, which inhibits corrosion. To bring nitrogen into the material, the chromium oxide layer must first be removed. With gas nitriding, removal of the passivation layer requires the application of a special gas chemistry, stainless steels can also be nitrided in salt baths, but only with a sacrifice of some level of corrosion resistance.

In the case of PulsPlasma nitriding, the treatment is applied directly through controlled ionic bombardment of the surface. By choosing a nitriding temperature below 450°C (or 842°F), and with exact control of the gas mixture, the material surface can be treated without reducing the corrosion resistance of the material.

Dies, Stamping & Injection Molds – a Harder Steel

Today, various molds and dies are used to shape everything from plastic bottles, to automobile quarter panels, to extruded wire, to metal injection molded (MIM) parts. Depending on the intricacy of the mold and die, it can cost a customer hundreds of thousands of dollars to fabricate. Customers require die longevity, while maintaining part tolerance, throughout the life of the die to ensure return-on-investment (ROI).

Despite being made of hardened steel, however, injecting melted resins at high temperatures and pressure into cavities over thousands of cycles begins to wear away and erode die edges, cavities, and moving components. Even the thermoplastic material can be abrasive, acting like sandpaper or leaving residue that wears down the surface. With the ever-increasing utilization of even more abrasive material, in the form of long glass and composite fibers, the amount of abrasion and friction within molds is increasing.

According to Voigtländer, pulse plasma nitriding is an ideal solution both to protect molds against damage and corrosion, but also because the diffusion of nitrogen increases the lubricity of the surface, facilitating quick removal of parts. “The diffusion of the nitrogen into the mold surface," he explains, "increases the fatigue strength of the material. In doing so, you can protect the surface against scratches… and increase the lifetime of the mold or die."

Sintered Parts

Pulse plasma nitriding also represents a strong option for sintered, or sinter hot isostatic pressing (HIP) components manufactured though additive manufacturing.

Salt baths have historically been used to nitride sintered components. However, the process of immersing components in molten salt makes it very difficult to remove the salt from open surface porosity. When gas nitriding is used, the nitriding atmosphere permeates all open pores resulting in the entire component, the surface, and the core, being completely nitrided.

“With pulse plasma nitriding, the atmosphere goes through the pores and only the surface area is affected, leaving the core or base material soft,” said PVA’s Voigtländer. “Most designers prefer having a wear-resistant surface with a soft, elastic core.”

Increased Production Throughput

Nitriding is a batch process. Innovation in furnace design, through an optimized mechanical operation, can increase efficiency and increase production capacity. While the actual time for nitriding does not change, efficient loading and unloading scenarios plays an important part. The PlaTeG plant design can use any one of a Mono, Shuttle or Tandem footprint, to manage throughput, resources, and operations costs.

As a batch process, nitriding typically requires waiting for the prior batch to be treated, cooled, and unloaded before a new batch can be started. Shuttle and tandem extensions are now available to streamline the batch process.

Multiple system configurations can offer flexibility, efficiency, repeatability, and throughput optimization.
Source: Jeff Elliott

With a shuttle extension, an additional vacuum chamber bottom may be added to a furnace. During a running nitriding process, the unloading of an earlier batch and the loading/preparing of a subsequent batch on the second vacuum chamber is possible. The cycle time therefore for two consecutive batches is reduced because of the overlapping of the time for unloading/loading of a vacuum chamber with the treatment time of the running process.

With a tandem extension there are two complete vacuum chambers which are operated alternately by the vacuum pumps, the process gas supply, the plasma generator and the control unit of the system. In situations such as unmanned weekend operations, an automatic process can be started and controlled for both batches in succession. With this type of operational structure, “it is possible to increase overall nitriding capacity by 30-60% annually,” according to Voigtländer.

Because plasma nitriding uses environmentally friendly nitrogen and hydrogen, the furnaces can be collocated with the machining of components without requiring a separate room. Moreover, the pulse plasma nitriding systems produce no polluting gases. This makes nitriding more efficient as part of an overall manufacturing process as an operator can locate the furnaces beside their drilling machines.

Pulse plasma offers significantly more precision in nitriding through the control of the mixture of gases, the controllability of glow discharge intervals, the design of the Pulsed signal, and the use of a highly insulated hot wall nitride furnace. Together with innovations in the design of the furnaces to streamline batch management in nitriding operations, manufacturers who depend on nitriding components can benefit from greater uniformity of results, better-protected materials, and increased throughput.


About the AuthorJeff Elliott is a Torrance, California-based technical writer. He has researched and written about industrial technologies and issues for the past 20 years. He wrote this article in cooperation with PVA TePla.

Pulse Plasma Nitriding Improves Surface Treatment, Wear Resistance, Fatigue and Material Performance Read More »

8 Heat Treaters Improve Processes with Simulation Software

Source: CENOS

Heat Treat Today brings you this best of the web content to highlight how 8 companies have been using simulation in their heat treat processes. In the article, the companies attest to saved time and costs as well as the benefits of visualizing accurate results. Check it out!

An excerpt:

[blockquote author=”CENOS” style=”1″]Old coil design failed and started leaking after 20,000 shots, while the redesigned coil is still running after 122,000 shots – more than five-fold improvement of the coil lifetime. By summing all of the benefits of the simulation software adoption in the engineering routine of the plant, Kevin got a 9% increase of the overall equipment efficiency (OEE).[/blockquote]

Read More: “8 Stories on How Computer Simulation Helped Companies to Improve Induction Heating in 2020”


All images provided by CENOS.

8 Heat Treaters Improve Processes with Simulation Software Read More »

This Week in Heat Treat Social Media


Welcome to Heat Treat Today’s This Week in Heat Treat Social MediaAs you know, there is so much content available on the web that it’s next to impossible to sift through all of the articles and posts that flood our inboxes and notifications on a daily basis. So, Heat Treat Today is here to bring you the latest in compelling, inspiring, and entertaining heat treat news from the different social media venues that you’ve just got to see and read!

This week, get a taste of the changes in the industry from the new U.S. President’s plans to neon heat treating signs to aerospace “demos”.

If you have content that everyone has to see, please send the link to editor@heattreattoday.com.


1.  It’s General, But You’ll Want To Know These 5 Things

“Upon entering office, President Biden quickly set to work undoing executive actions taken by his predecessor, President Trump, and issuing new ones reflecting his own priorities. During his first week as President, Biden signed executive orders on topics as varied as COVID-19, supply chains, and climate change. Here are five of Biden’s early-term executive actions with potential impact on the manufacturing sector.” (Industry Week)

(Click the Image to view slideshow)


2. People Talk!

Catch up on the latest things that people have been talking about on social media!

Walk Around the Plant Floor

.

That Neon Glow

.

Heat Applications: Waffle Iron

.

Too Hot To Touch, Or…


3. What’s with the #?

Did you know that you can find the topics you love by typing a hashtag (#)? And if you see a # in a post, did you know that you can find other content by CLICKING that term? Give it a try on one of our posts on LinkedIn! Hit the “see more” and click #heattreatment. 

#HeatTreatment

#HeatTreatToday

#HTTTechTuesday

#heattreatnews

#heattreatradio

#HTT40Under40


4. Reading and Podcast

Get into the meat of it with these podcasts and articles from all around the heat treat industry.

What is Electron Beam Welding?

.

Heat Treat Radio Series

We just completed a series with Thomas Wingens with podcast episodes on Washing and Ferritic Nitrocarburizing. You can also find the complete Heat Treat Radio series with James Hawthorne of Acument Global Technologies and Justin Rydzewski of Controls Service, Inc. on CQI-9. All of these and more on our Heat Treat Radio page.

.

Prerecorded Webinar:

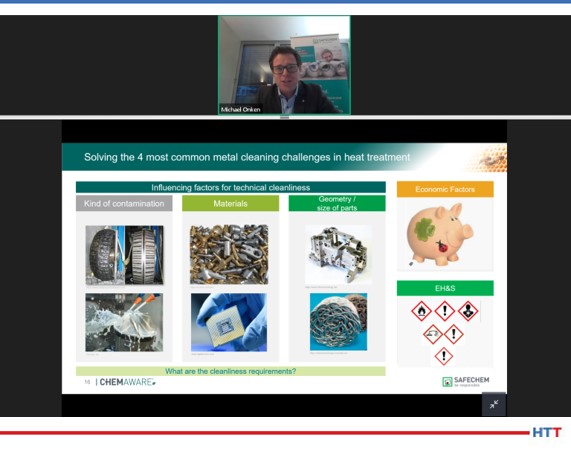
“Solving the 4 most common metal cleaning challenges in heat treatment”

In January 2021, Hubbard-Hall hosted a free webinar with Thomas Wingens of Wingens International and Michael Onken of SAFECHEM. These two experts described the influencing factors for technical cleanliness and some solutions for washing. We shared an original content overview of what happened at the virtual event here.


5. When Your Client Wants a Demo…

In honor of the March Aerospace edition of Heat Treat Today’s print magazine, check out this aerospace “demo”.


Have a great weekend!

This Week in Heat Treat Social Media Read More »

Is Additive Manufacturing Changing Heat Treat?

Source: Kanthal®

Heat treat methods are going to change in more ways than one, claims Dilip Chandrasekaran, head of R&D and Technology at Kanthal. “What we’ll see in the future as the industry grows is more automated processes where 3D printers feed parts into post-treatment. It will need to be smooth and streamlined, and the heating will need to perform different processes.”

Heat Treat Today brings you this quick, best of the web piece to keep you current with the latest insights in additive manufacturing.

An excerpt:

[blockquote author=”Kanthal®” style=”1″]The growth of additive manufacturing is creating new challenges in the field of heat treatment technology and prompting a shift toward electrification and greater flexibility from heat treatment equipment. These changes are expected to affect heat treatment in other industries too.[/blockquote]


Read More: “What Next for Heat Treat Technology”


All images provided by Kanthal.

Is Additive Manufacturing Changing Heat Treat? Read More »

$149 Million U.S. Navy Contract to StandardAero

HTD Size-PR Logo

Marc Drobny
President, Military Aviation
StandardAero.com

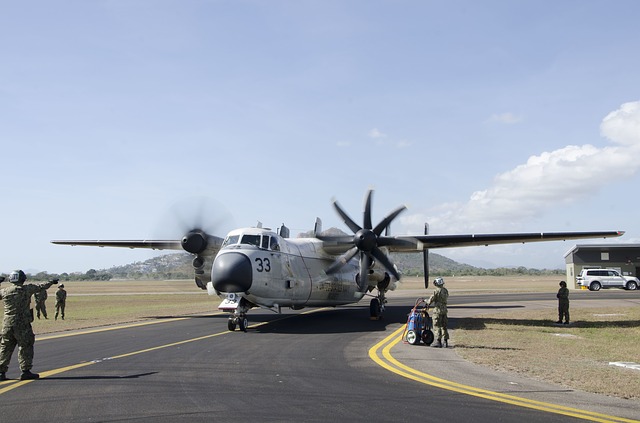
The United States Navy has awarded StandardAero a $149 million multi-year contract to provide engine maintenance, repair, and overhaul (MRO) services for Rolls-Royce T56 Series III engines powering the U.S. Navy and U.S. Marine Corps fleet of C-130s, C-2, P-3 and EP-3 aircraft.

The multi-year contract will continue into 2026 with the work being performed at StandardAero’s San Antonio and Winnipeg, Manitoba, Canada facilities. StandardAero was part of a Multiple Award Contract (MAC) on this program over the last five years, having recently completed option year four in support of this customer. Under the new contract, StandardAero will provide the same service experience the Navy and Marine Corps has received through the previous multi-year contract.

“We are thrilled to continue expanding our successful partnership supporting Navy and Marine Corps aircraft engine MRO,” said Marc Drobny, president of the military division at StandardAero. “Powering these aircraft is a strategic and logical continuation within our portfolio of services.

“Our employees, many of whom have served in the military, take great pride in serving the Navy – Marine Corps Fleet. As a former Naval aviator, I take great personal pride in our team’s ability to provide exceptional operational readiness through reliable and high-performing engines.”

StandardAero also supports the Rolls-Royce Series IV engines including support for the Marine Corps C-130J AE2100 engine and the Navy E-2D T56-A-427/A MRO requirements as a sub-contractor to Rolls-Royce.


(photo source: Military_Material at Pixabay )


$149 Million U.S. Navy Contract to StandardAero Read More »

Announcing: New HIPing Ebook!

Heat Treat Today is excited to bring you a NEW and FREE ebook this Technical Tuesday! 

In an ever-changing world where production efficiency, reduced environmental impact, and improved process reliability are in focus, some well-known technologies are seeing a renaissance. 

Hot isostatic pressing (HIP), is one such technology, which until now has been an essential process to densify porosity and improve the mechanical properties of materials for components. The outlook for HIP technology has never been brighter, helped by technology shifts that are accelerated by recent global events. 

In this book written with the expert insights of Quintus Technologies, explore high pressure heat treating through the many facets of hot isostatic pressing.

Get the FREE EBOOK here!

Announcing: New HIPing Ebook! Read More »

IHEA Monthly Economic Report: Dark Economic Clouds Cautiously Giving Way to Bright Recovery

“It is not that there is no longer anything to be concerned about as far as the economy is concerned, but the constant worries about whether the impact of the recession would fade seems to be ending. . . . The aggressive recovery predictions that were dismissed a month or so ago are now seen as the most likely.” This optimistic introduction leads February’s Industrial Heating Equipment Association’s (IHEA) Executive Economic Summary.

There are three factors that account for this enthusiasm, the summary reports. The first is the acceleration of vaccine distribution. “The US is now ranked number five in the world in terms of numbers vaccinated (behind only a few Asian states like Japan and Taiwan).” This has helped to reduce pandemic protocols. The second factor is that consumers have money and are willing to spend it. The summary states, “There is an estimated $6 trillion on the sidelines between consumers, investors and the business community. The consumer alone sits on over $2 trillion.” And finally, the third factor is tied to the money that will be infused into the economy by the $1.9 trillion stimulus/rescue plan.

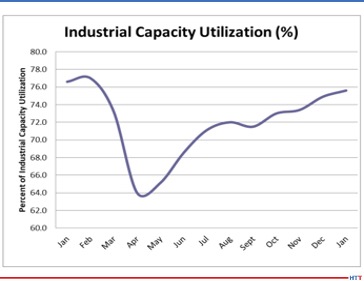
The measurement of capacity utilization is a key indicator for future activity. It basically measures how efficiently a manufacturer is operating – do they have slack capacity in terms of either the machinery or their workforce? At the moment, the capacity numbers are a very long way from provoking inflation.

But, there’s that “what if,” hanging out there. The report cautions, “There is always a caveat when talking economics and that stimulus money is behind some of the trepidation regarding the future of the economic growth pattern. The risk from the stimulus is that it will overheat the economy and trigger a serious burst of inflation. If that surge in prices is dramatic enough, it could provoke the Fed to hike rates and start to put a damper on the growth we are starting to see.”

There are three prime motivators for inflation. The first one, wage inflation, hasn’t been an issue since there are still millions of people out of work. The second motivator, which has been manifesting dramatically is the price of commodities. They have been rising quickly–think oil and lumber prices. The third motivator is the money supply issue which could potentially lead to much angst. “The US economy is about to get hit with nearly $2 trillion just when there is substantial growth underway. This has the potential to set off a cycle of money chasing money. There will be a substantial part of the consumer population that will see some of this money and will be eager to spend it. If there is too much demand and not enough supply the price of things will go up.”

In conclusion, it will be interesting to see the response from the Fed–currently, there doesn’t seem to be a desire to hike rates– as well as the spending of the consumer. Will they continue to spend on services or for long-desired products? Hopefully, there are economic sunny days ahead.

The purchasing managers’ index is fairly volatile at the moment, but the good news is that the numbers have been consistently in the 60s for the last several months and anything over 50 is considered expansionary.

Check out the full report to see specific index growth and analysis which is available to IHEA member companies. For membership information, and a full copy of  the 12-page report, contact Anne Goyer, executive director of the Industrial Heating Equipment Association (IHEA). Email Anne by clicking here.

Anne Goyer, Executive Director of IHEA


IHEA Monthly Economic Report: Dark Economic Clouds Cautiously Giving Way to Bright Recovery Read More »

Box Furnace for Annealing Firearm Barrels

Medium-Sized Floor-Standing Box Furnace
Source: L&L Special Furnace Company

HTD Size-PR LogoA leading Midwest manufacturer of custom firearms and rifles will use a medium-sized floor-standing box furnace for annealing gun barrels for rifles.

This is the second furnace from L&L Special Furnace Company that the manufacturer has acquired. This model is the L&L Model XLE 3636, which has a work zone of 34” wide by 30” high by 32” deep. It is designed for use with inert blanketing gas for atmosphere control to minimize surface de-carb.

Other features include a programmable flow panel with regulator and two flow meters for high and nominal flow rates along with a visual flow indicator light are included. There is a high-temperature air-cooled fan with packing gland to maintain the case seal integrity. A cast alloy hearth provides a good flat work platform for the fixturing of parts.

Honeywell controls and a Yokogawa recorder enable temperature control and chart representation of the furnace cycle. The power control is a series of solid-state relays and the furnace is constructed in accordance with NFPA86 compliance for safety.


(photo source: Vidar Nordli Mathisen at unsplash.com)


Box Furnace for Annealing Firearm Barrels Read More »

Heat Treat Radio #50: Justin Rydzewski and James Hawthorne on CQI-9 Rev.4 (Part 4 of 4) – Expert Advice

Welcome back to the show. Heat Treat Radio host, Doug Glenn, wraps up a four-part series on CQI-9 Revision 4 changes with Acument Global Technologies’ James Hawthorne and Controls Service Inc. Justin Rydzewski. In this final episode, both of these experts give their advice on how to navigate and comply with Rev 4.

To find the previous episodes in this series, go to www.heattreattoday.com/radio.

Below, you can listen to the podcast by clicking on the audio play button or read the edited transcript.


The following transcript has been edited for your reading enjoyment.

Doug Glenn (DG):  We're here today with Justin Rydzewski who is the director of sales and marketing of Controls Service, Inc. in Livonia, Michigan and also with James Hawthorne, heat treat specialist at Acument Global Technologies.  Both of these gentlemen have been with us for two or three of the last three episodes that we put together.  James, was the committee chair, I believe that's the right title, for the Revision 4, and Justin, of course, was right alongside on the committee getting things done.  Gentlemen, first off, welcome back to Heat Treat Radio.

Justin Rydzewski (JR):  Glad to be here.

James Hawthorne (JH):  Thank you, Doug.  Glad to be here.

DG:  We've covered a lot of the major changes, a lot of the main points that people ought to know, on the first three episodes.  We want to wrap it up today by asking a couple of very practical questions, a couple of “opinion” questions, but, I think, also a couple of very practical questions on implementation, and things of that sort, of the new CQI-9 Rev 4.

Justin, if you don't mind, I'd like to start with you and address an issue that I think you and I touched on in the very first episode, and that was the difference between the CQI-9 standard and AM2750F, specifically, about the automotive industry.  Why doesn't it just adopt AMS2750F as opposed to having this separate CQI-9 standard?

Episode 1 of 3 of AMS2750 series

JR:  I think that both specifications are appropriate for their industries.  But, there are some significant differences between the two.  First and foremost, one is intended for aerospace and the other for automotive.  AMS2750F, as we've mentioned in a previous episode, is a pyrometry standard, whereas CQI-9 is a system assessment; it is a process-based approach to things, whereas AMS2750 is more equipment based.  You classify things by temperature tolerances, by the instrumentation type that you have, whereas requirements within CQI-9 are generally based on your type of process and specific to your process, in particular.

I would say that the most significant difference between the two documents is AMS2750 is part of the NADCAP program and requires accreditation and an auditing body, PRI, to come out and say, “Yep, you're good to go.  Here's your certificate.  We'll see you in a year”.  CQI-9 is intended to be a self-assessment.  It's intended for heat treaters to implement themselves to provide them with a process of managing their heat treat and that doesn't require somebody to come in and accredit them and hand them a certificate.

There is a big difference between the two; they are not equals.  There are similarities, especially in the pyrometry section.  At one point, AMS was heavily sited inside of CQI-9.  Since its removal, however, we've had success, and that success has been measurable; it's been significant.  I would image that the OEs have been rather happy with what it is that they have there in the document, especially in the 4th edition, and I think that the thought of going to an AMS2750 and abandoning CQI-9 is well outside the realm of plausible.

JH:  One thing I would add here is, if you read the headers for each section of the HTSA, section one is “Management Responsibility and Quality Planning”, section two is “Floor and Material Handling Responsibilities”, and section three is the equipment.  On the equipment side, you're going to get more into the pyrometry side of things- the metrology and the maintenance specifics to that equipment, as well.  So, the all-encompassing HTSA is a system that is a management system, or at least a system that you can develop a management system based behind, and ensure compliance.

DG:  For those who are just joining on this episode, HTSA, heat treat system assessment, is one of the main parts of the CQI standard.  Justin, I think your point is good.  James, I think, as well, the point is well taken.  CQI-9 is meant to be an internal tool, a continuous improvement tool that helps a company that is involved with heat treating to continually improve their process.  AMS2750F specifically, is pretty much exclusively a pyrometry certification program, where you've got to have somebody coming from the outside.  I remember, back in the day, when they were first starting one of the QS standards, they said, no longer are you going to have to comply or get qualified by this OE, or this prime, or this prime, now you can have one standard.  Has that been the case here?  Has it been effective in the automotive industry, CQI-9?

JH:  I think, 100%, Doug.  It's like IATF – all of the automotive industry has to be compliant to that.  Same thing with CQI-9.  It provides that commonality for all heat treaters in all the different processes that are employed at their facilities, or the multiple facilities that they may have.  For a company like ours, we have 8 companies in North America.  For the North American side of things that have heat treat furnaces in them, we have induction furnaces, we have carbonitriding furnaces, and we have stress relief furnaces.  So that commonality even helps us internally with our management system and how we take steps to provide that common approach and compliance to CQI-9.

[blockquote author="Justin Rydzewski" style="1"]The CQI-9 intent largely was that this is something that you can do yourself and implement yourself.  We'll provide you with the guidance and put it in simple terms and give you all the research you need to support this on your own.[/blockquote]

JR:  I think that also bodes well, up the ladder as well, for the OEs.  The more commonality that exists in the industry, the wider that, for lack of a better term, talent pool is.  The more people, the more sources that you can go to in order to have work done and have it what you expect it to be, from a quality standpoint.

I think one of the things that CQI-9 has done really well is they've made a concerted effort to make that document easier to understand and to simplify things down to just its bare bone necessities, whereas some of the other specifications that exist in industry can be lacking.  There is a real good reason why a lot of the work of some of those other pyrometry specifications out there are outsourced, because the expertise to adhere to those things and be confident that you're adhering to those things is possessed by an in-house team; they have to go outside.  The CQI-9 intent largely was that this is something that you can do yourself and implement yourself.  We'll provide you with the guidance and put it in simple terms and give you all the research you need to support this on your own.

Justin Rydzewski, James Hawthorne, and Doug Glenn (clockwise from the left) sat around the virtual screen to hash out a few final expert opinions on CQI-9.

DG:  I'm pretty sure, based on everything we've talked about, that you guys really like CQI-9.

JH:  100%!  I embrace it and our company embraces it.

DG:  So, I know you guys like it, you're the main cheerleaders.  What is your perception about companies outside of yourself?  Has it, in fact, been embraced, or has it kind of been “Heisman trophied”, the stiff arm – “We'll embrace you with one extended arm”.

JH:  If I may, I will say that it's been embraced across the industry through all heat treaters.  I think anywhere that anybody deemed it to be a burden, I think with the changes to the format, the added clarity, the improvements to the document, the knowledge base that's now been updated in the glossary, it is all going to help those guys cross any bridge that they were struggling with and make it better for them.

I believe we touched on a little bit in one of the past episodes, or maybe it was when Justin and I were talking about this offline, but one of our customers, who is a non-automotive customer, embraces CQI-9 and our systems and our approach to our heat treat.  That is a huge step because that particular company has a lot of internal specification as it pertains to heat treat, but CQI-9 is either equal to or exceeds what their expectation is.  It makes it easy for them to embrace it.  That was one of the things that was brought up in the roll-out presentation we did through AIAT – one of the other industries had mentioned they were following it.

DG:  It sounds like, overall, it has been fairly well embraced and this Rev 4 is going to make it even easier to cuddle up with a cup of hot cocoa and feel comfortable with it.

JR:  Generally speaking, in my travels, I have two categories of people that I come across.  You have the sort that is looking to embrace it.  They recognize that it's a “have to do” and they just want to know what the rules are.  They want to make sure that they understand what the rules are and that they make sense.  Maybe there is a point or two that they take exception to about, not fully understanding what the intent is of it, but, for the most part, by and large, they want to adhere to the requirements.  They recognize that they need to.

The other category includes those who fight anything that they're asked to do, no matter what it is.  “No, I don't want to do that.  We've been doing it this way forever.  Convince me, show me, that I'm doing it wrong.  I do some sort of subsequent testing and it always come out fine.  I've never had any complaints.  Why do I have to go do this?”  While that group is definitely the minority, I can tell you that that group, almost 100% of those people are going to be those types that you find more issues with than any other.  That's because they fight it and they try to find ways to circumvent things.  That's a real slippery slope there.

I think CQI-9 does a real good job at trying to keep things in its lane and recognize that if there's something that we're asking the heat treater to do, that that requirement needs to provide value on some level, or it needs to mitigate risk on some level, and a meaningful one at that.

You asked, “Do I like CQI-9?”  I like AMS2750 too.  There are some things in AMS2750 I like better than what we did in CQI-9.  Talking from experience of having to write some of the requirements in the document, and how difficult that can be to say what it is you want to say but in a manner that makes sense outside of your own brain, it's difficult.  I think AMS states some things very, very well.  I like their thermocouple calibration certificate requirements better than ours; I think they're more detailed.  But I think both work really well, and embracing it sometimes just requires a bit of an education or an understanding of the intent side of things, the purpose side of things.

DG:  When was CQI-9 Rev 4 released?

JR:  The last week of June.

DG:  It's been going on for months now.  How about timing?  I would imagine that a lot of people that are listening to this probably know that they need to comply with certain aspects of CQI-9.  What is the timing for them?  When do they need to have all their ducks in order?

JH:  During the roll out presentation, the OEMs made a joint statement.  We did that roll out presentation in September, and they essentially said that the time between the June release and that (roll-out) presentation was the grace period.  When the 3rd edition expired, you have to do 4th edition assessment and they will no longer accept 3rd edition assessments at that point.  So, whenever your expiration is, you shall do it to the 4th edition.

JR:  The 3rd edition is officially obsolete.

DG:  So if you're doing another assessment, it's going to be a Rev 4 assessment.  Are there any other timing issues that people need to be aware of?

JR:  That should pretty much cover everything.  If you're outsourcing an element of your service or of a material, you should be specifying adherence or conformance to the 4th edition at this point.

DG:  So, James, I want to address this next question to you, if you don't mind.  I know you said in your organization, you've got how many North American locations?

JH:  8 plants in North America.

DG:  OK, 8 plants.  And you've, obviously, rolled out Rev 4.  How did you handle the transition?  How did it go?  What was complicated and difficult, and how did you address it?

JH:  For me, I think it's a little easier, because I was in the room while we were writing the 4th edition.  The heat treat systems for all of our locations, I wrote.  So, I have a very unfair advantage.  But, that being said, even knowing and being as intimate as I am with our own system and the 4th edition of CQI-9, we have made a concerted effort to slow down the process of doing the heat treat system assessment and slow down the process of doing the job audit and doing the process tables to ensure that we are capturing everything.

We've made this statement many times, whether it was here with you or if it was through our roll-out presentation, it is essential to read this document.  It is essential to understand what's happening in it.  If it takes just a little bit of extra time to read a little bit further to do the checks and balances, pop into the glossary, just to make sure that you are answering the questions as compliant as you possibly can, is the most important thing.

A wise man told me once, Compliance is a circle and if you're just outside the circle, all I want you to do is get you just inside the circle.  And next year I'm going to tighten the circle a little bit and if you're still sitting outside, we're going to move you inside.  You don't have to hit a bullseye every time, but you have to be inside the compliance circle.  So, if you understand that, and if you manage it that way, it's going to make it easy and more effective.  Then, you can stick to the intent of the document, and the intent of the document is within the acronym itself of CQI-9: it's continuous quality improvement.  Never take your foot off the pedal.

Source: Heat Treat Today

DG:  Right.  It never ends.  Justin, how about you?  Same question.  I know you're going in through your company into a variety of other companies who are trying to comply.  What are you seeing, from their perspective, as far as the difficulty?  How are they handling it?

JR:  I think the most difficult aspect of things, I guess, is probably one of the most obvious: implementation.  You've been doing it one way for the last 8-9 years and now we're going to need to implement something new.  And when do you want to implement something new?  It's really nice when you work for an organization that has process specifications and certain test specifications very well defined, because then you can hold onto them and say, “Here are the things that we were doing,” and you can go through them and see where things need to be different.

Where they're less defined, or they're defined in some manner that is not on the forefront of things – like I define things in a quote or in a purchase order – those become difficult. There could be elements of implementing something too soon, and now, all of a sudden, I violate something that they've done internally, or sometimes if they had it stated internally for a requirement.

For us, the most difficult thing has been the implementation side of things.  It's meant a lot of conversations and trying to determine what this is going to look like, what things we are going to need to do differently, what things we want to check on, and the finally to, for lack of a better word, “coach” my customer along.  Here are things you need to consider, here are things you might need to do differently, here's how I would state it for the new edition for making revisions.  But to the horse that has been thoroughly well beaten, you have to read the document.

The CQI-9 audio book, coming soon, we'll have that on tape for you.  Whether you're driving to work or putting your kids to sleep, it will work either way.

DG:  Last question for you guys.  For a company who's wanting to become CQI-9 compliant, what are some of those must do's and what are some of the practical advice you've got for them as they start down that path?

JH:  If, I may, I think the first and most important thing there is to evaluate the talent that you have on site.  Who is your in-house expert?  Who is the guy that most fits what you need to be the driver of those next steps?  As long as you have that, and that guy understands your system, then the journey can begin and I think your process is more linear with less hills and valleys.  You start to win, and you start to win with less drop-off, and that's what you want to do.  First and foremost, have the right guy in place.

[blockquote author="James Hawthorne" style="1"]First and foremost, have the right guy in place. [/blockquote]

DG:  So, in your estimation, James, you're saying it's a personnel issue.  Right away, make sure you do a good assessment and get the right guy in the spot to oversee the process.

JH:  Right.  You don't want to be a commercial heat treater and you just hired a quality manager from a widget factory to come be the champion of your heat treat.  You want him to be a heat treater.  You want to have a heat treater in place that knows his stuff.

DG:  Right.  And who has an attention to detail, I'm sure.

JH:  I think it's important to the extent of what Justin was just talking about is, when that person talks to his suppliers, his service providers, you want to have somebody that has some wherewithal and understanding in that field so when that communication does take place, and you have folks like Justin and others in his field, trying to help educate the heat treater on what it takes to be compliant with, whether it's reporting, whether it's through the process or whatever, having that understanding is going to make even the service provider’s job easier.

JR:  I think that organizations that struggled with the 3rd edition are probably going to continue to struggle with the 4th edition.  If you're comfortable with the 3rd edition and you're doing well with the 3rd edition, the 4th edition is going to be relatively easy to adapt to and to implement.  Like with any math story problem, you've got to write down what it is you know.  So you go through the document itself, you start making notes on things, you start citing where things might need to be different, you start red flagging things, you review what you have, may do a Ctrl + F for any mention of 3rd edition and replace with 4th edition, or something simple like that. It is what you have created and try to continue on with the successes you had for the 3rd edition into that 4th one.  If you've struggled with the 3rd edition, the likelihood that you're going to struggle with the 4th is also pretty great.  It is likely that the document isn't the issue, the issue is likely a lack of awareness.

It cannot go understated how valuable it is to invest in training, especially if you're bringing some new guy on to champion the effort, or if you've got a team that's eager and hungry and looking to prove their worth – get them trained.  It's readily available.  Our organization offers it, the AIG offers training on the HTSA side of things; there are plenty of organizations out there that will offer this training.  The benefits to working with a high-end service provider in many of these regards, is that they'll help you through the process as part of their service offering.  That's how the true value of a good service provider can be measured is in these sorts of situations.  I'd lean on your experts.  Invest in your staff.  Get the training to get everyone up to speed.

Again, if you fought it in the 3rd, and your plan is to fight it on the 4th, it's going to be an unenjoyable road and you might need to figure out ways to embrace what it is you know and acknowledge what it is you don't, and then fill those gaps in so that you can get to where you need to go.


Doug Glenn, Publisher, Heat Treat Today

Doug Glenn, Heat Treat Today publisher and Heat Treat Radio host.


To find other Heat Treat Radio episodes, go to www.heattreattoday.com/radio.

Heat Treat Radio #50: Justin Rydzewski and James Hawthorne on CQI-9 Rev.4 (Part 4 of 4) – Expert Advice Read More »

When Heat Treat and St. Patrick’s Day Collide…

op-edWhen heat treat and St. Patrick’s Day collide, Heat Treat Today editors have a little fun. Today’s post is inspired by furnaces and Ireland. Happy St. Patrick’s Day, and enjoy the hot topics!


| The Irish Turf Fire |

Have you heard of this heat treating solution? The fuel for this furnace is turf. “Turf is dried-peat and was a primary fuel source for Irish people for thousands of years[…] In the past, Irish people used turf to heat their homes and cook their food. Turf was harvested from a bog. Cutting turf by hand is a laborious task.” Not sure your general manager will let this one by... (Mairead Geary, “Smell of an open fire in Ireland is intoxicating but what is Irish turf?” IrishCentral)


| Irish Terms |

Here are some Irish and Gaelic terms that a heat treater may want to use instead of the same ol’ same ol’. Just for today. Search more options for yourself here.

  • Cóir teasa: heat treatment
  • miotaleolaíocht: metallurgy
  • foirnéis: furnace
  • prásáil: brazing
  • gaibhnithe: forging
  • ainnéalta: annealing

| Heat Treatment in Ireland |

Content at Heat Treat Today is focused on the North American heat treat industry, however, we would be remiss if we didn’t highlight heat treatment going on in Ireland.

For a featured in-house heat treater, “medtech” company Stryker has heat treat processes going on at their Ireland R&D base in Cork. After a commitment to invest in three facilities in Cork, Stryker’s Spencer Stiles said, “Our team in Ireland has built considerable research and development and new product development capabilities through the partnership of multiple divisions over the past 20 years in an effort to serve multiple market segments.”

Screen Capture of Stryker’s Landing Page

BOC is a provider of industrial, medical and special gases in Ireland and has been producing atmospheric gases, including oxygen, nitrogen and argon in Ireland for over 70 years.

Source: About BOC, a member of Linde Group

While you may not have heard of these heat treater providers, they are a member of the international Linde Group.

A heat treatment service provider, Hi-Life tools has been providing heat treatment service for a wide range of Irish based tool making, engineering and medical device companies for more than 20 years.

Source: PTG webpage

The company, part of Precision Tool Group, has built up a vast amount of experience of heat treating a wide range of metals from tool steels, stainless steels, and exotic metals. These can be treated using the standard processes or a custom made process can be developed to suit the customer requirements.

| Irish Voices: Winter, Fire, and Snow |

Thankfully, winter and snow are melting away, but fire remains! Listen to this beautiful ballad sung by Irish Tenor, Emmet Cahill. If you want to listen to a full playlist of Irish folk music, check out The High Kings.


That’s all for now, Happy St. Patrick’s Day!

Heat Treat Today Team


When Heat Treat and St. Patrick’s Day Collide… Read More »