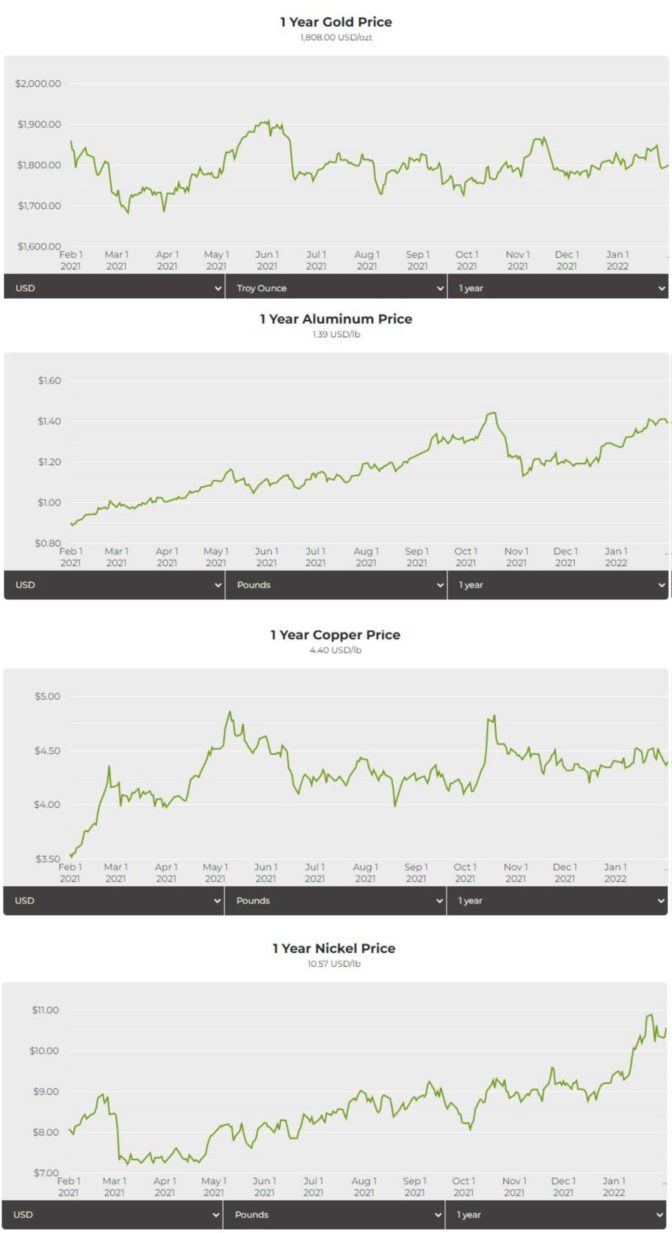
The “Known – Unknown,” the “Undiscovered Country,” the “Movement from cocksure ignorance to thoughtful uncertainty.” It doesn’t matter if you get your catch phrase from Donald Rumsfeld, Star-Trek, or that plaque your mother kept above the kitchen sink, the implication is the same: we really don’t know what the future holds. But, the Unknown of which I speak in this article is natural gas prices.
This column is a Combustion Corner feature written by John Clarke, technical director at Helios Electric Corporation, and appeared inHeat TreatToday’sMarch 2022 Aerospace print edition.
If you have suggestions for savings opportunities you’d like John to explore for future columns, please email Karen@heattreattoday.com.
John B. Clarke Technical Director Helios Electric Corporation Source: Helios Electrical Corporation
Does “What happens in Eastern Europe stays in Eastern Europe” hold true? Unfortunately — no.
We have learned from recent and ongoing supply chain issues just how interconnected our economy and manufacturing sector is with the rest of the world. The standoff in Ukraine has the potential to impact the world energy markets for years to come, and I suspect this impact will be felt no matter what transpires. I am certainly no expert, but I have a sinking suspicion that our country offered some American methane molecules to Germany to stiffen their resolve to cancel the Nord Stream 2 pipeline. If the EU works to reduce their dependency on Russian natural gas, a significant portion of worldwide exports are removed from the supply side of the equation. From a practical standpoint, these shifts in supply will take some years to achieve, but we have seen a new realization on the part of business and governmental leaders about the importance of robust and reliable supplies of commodities, and manufactured goods and manufacturing capacity. So, less natural gas supply with rising demand equates to higher prices. And as we have discussed previously, liquefied natural gas transportation from the U.S. to the rest of the world is connecting our natural gas market with the world market — and our natural gas price will be affected by consumption and production factors worldwide, just as the price we pay for petroleum oil today is determined in New York, London, and Riyadh — following the consumption patterns in Beijing, Sydney, and Tokyo.
Ok — let’s get back to what we can do in our own facilities to insulate ourselves, to some degree, from unpredictable world events.
Recuperation, or preheating combustion air using the waste heat exiting the furnace or oven is a time proven method to reduce fuel gas consumption. Before we quantify the effect of preheating air, we need to briefly discuss what affects this heated air has on the combustion process. Higher combustion air temperatures are associated with the following:
Peak flame temperatures are increased. As less energy is used to heat the incoming air, the energy in the natural gas can raise the products of combustion (CO2, H2O and N2) to a higher temperature than would be achieved without combustion air preheating. This can be either beneficial or problematic for a specific application. If the work being heated can accept increased radiation from these higher temperatures — heating rates are improved and throughput increased, but these higher temperatures may reduce the life of furnace components, or, in extreme cases, lead to a catastrophic failure.
Flame speeds are increased, so the combustion process concludes in less space. Again, this is a double-edged sword, benefiting some and leading to a loss on temperature uniformity in others.
Total products of combustion required for any quantity of heat input is reduced. Mass flow is especially important in systems where the operating temperature is below approximately 1200°F. If the energy saved leads to a loss in temperature uniformity, it may be a Pyrrhic victory.
NOx formation is increased. Burner technology has come a long way in recent years to allow for systems to use these higher temperatures without greatly increasing NOx emissions, but the rule of thumb is that by increasing the combustion air temperature from 70°F to 800°F, we basically double NOx formation.
Each of these drawbacks, other than NOx formation, may be a plus rather than a minus for any application. Float glass furnaces (plate glass used in windows) and ingot reheat furnaces are examples of applications where recuperation was applied a century or so ago, at a time where fuel costs where not much of a factor. In both cases, the increased flame temperatures accelerated the heat transfer to either the glass or the steel, increasing production. These applications required furnace temperatures where combustion without preheating would have been impractical — as most of the energy would have been lost in the flues, and very little heat would be available to do any useful work.
What questions should I ask? How much can I save? What is my project’s estimated payback? All are critical questions. To start with, can your existing furnace accept these higher flame temperatures, and can you capture the heat and apply a cost-effective heat exchanger? An example would be a radiant tube furnace. Applying recuperation may require an upgrade in the alloy used in the burner and radiant tube. In direct fired applications, will my uniformity suffer? In general, this is a greater concern at temperatures below 1600°F. As the operating temperatures increase, we can generally expect better uniformity. (I can hear the furnace and burner experts reading this cry “foul,” and they are right, it is not wise to rely on my generalizations — always consult an expert about your specific application.)
How much will it cost? With recuperation, it is best to take advantage of an experienced person’s mistakes, rather than making them on your own. Consult a qualified contractor, OEM, or consultant to help with the application and costs.
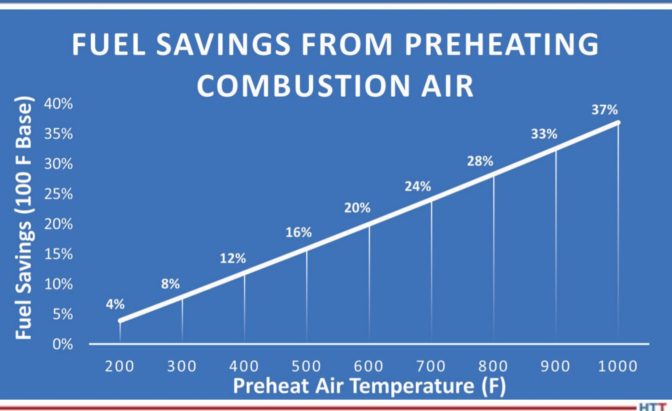
How much can be saved? To answer that question, I provide the above graph. It is not the end all be all but will provide a rough estimate of potential savings. It is for an application with an exhaust temperature of 1600°F operating with 15% excess air.
As we can see, in this application, if we apply recuperation to preheat the air to 800°F, we will save 28% of the natural gas we would otherwise consume.
Before investing your money, an individual analysis of each application is required. This article’s purpose is simply to motivate the reader to invest the time necessary to properly determine, as I mentioned last month, if they have “uncashed checks” lying around their shop.
As always, please let me know if you have any questions.
About the Author:
John Clarke, with over 30 years in the heat processing area, is currently the technical director of Helios Corporation. John’s work includes system efficiency analysis, burner design as well as burner management systems. John was a former president of the Industrial Heating Equipment Association and vice president at Maxon Corporation.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
The tragedies of war are many. In today's post, we're looking at a very small slice of the consequences of the war in the Ukraine: How might this affect the heat treat industry? What should you prepare for? We've located four insights to reflect on this Friday.
Supply Chain Bottle Necks
"Representing 200 million tons of transit potential, Ukraine is one of the foremost—yet often overlooked—components of both the European and global supply chains. Therefore, any disruption in the region can have massive knock-on effects for countries throughout the world." With that in mind, three industry considerations are energy, resilience, and capacity. (Read more)
Businesses Are Interrupting Trade with Russia
Adding to the supply chain changes, you may find businesses you work with or even your own ceasing to do business with Russian companies in an effort to show solidarity with the Ukraine. In one case, "A group of 3D printer OEMs and other companies involved in additive manufacturing have released a statement in support of Ukraine and are calling for a quick end to Russia’s war in the country." (Read more)
Heightened Cybersecurity Preparedness
It's hard to say whether cyber attacks are absolutely increased because of the conflict since there has long been a high rate of cyberattacking originating from Russia. However, cyberattacking is a known threat in modern war, and there have been increased email phishing attacks on specific targets. (Read more)
"We are seeing cybercriminals use Russia and Ukraine-centric social engineering efforts, like phishing emails, leveraging current events to solicit an emotional response to the war,” says Rosa Smothers, former CIA cyber threat analyst and technical intelligence officer, now at KnowBe4. 'In other words, people are less likely to think before they click.'" - Dennis Schima, "Does the War in Ukraine Increase the Risk of Russian Cyberattacks?"
Humanitarian Pressures
Whether near or far, we've been seeing fundraising efforts, medical support, and humanitarian aid being sent to the frontlines. Perhaps you've done business internationally and have contacts who need support, or, like SECO/WARWICK, have found a way to raise funds and send support: "With your help, we’ve sent humanitarian aid to the border and each day we support our Ukrainian colleagues."
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Heat TreatRadiohost, Doug Glenn, and several other Heat TreatToday team members sit down with long-time industry expert Dan Herring, the Heat Treat Doctor®, to discuss the difference between heat treating and thermal processing. If you’ve ever wondered about the difference – if one actually exists(!), then you’ll enjoy this highly informative Lunch & Learn with Heat TreatToday.
Below, you can watch the video, listen to the podcast by clicking on the audio play button, or read an edited transcript.
The following transcript has been edited for your reading enjoyment.
Doug Glenn (DG): So, Dan, I want to turn it over to you, but I want to give a context though of what we’re going to be talking about. As you just mentioned, before we hit the record button, we’re pretty heat treat centric in our world, but there are a lot of other thermal processes that go on that aren’t exactly heat treat. We talk about some of them in our publication, not all, so what we’d like to do is turn over to you to talk about the difference between “heat treating proper” and “thermal processing, generally speaking.”
Dan, welcome and thanks for educating us.
Dan Herring (DH): Well, thanks, Doug, and good afternoon, everybody. First of all, for everyone listening, I hope to cover the basics providing information without confusing everyone. If there are any questions as I go along, please don’t hesitate to ask them. I think it’s always better to have an interactive, back and forth discussion on things.
You are absolutely correct, Doug. we live in a heat treat centric world. I’m going to start off in familiar territory by discussing a little bit about heat treating. Then, we’re going to move into the differences between heat treating and thermal processing.
To give a simple definition of heat treating — simple yet complicated at the same time — is heat treating is the controlled application of time, temperature and atmosphere to produce a predictable change in the internal structure (that means the microstructure to metallurgists) of the material being treated. Now, the interesting part is that heat treating is (a) predictable, which is why metallurgists exists in the world and it is (b) controlled, which is why heat treaters exist in the world, and the darndable thing about heat treating is that it happens inside the metal or the material and, unfortunately, you (c) can’t see the changes that are taking place.
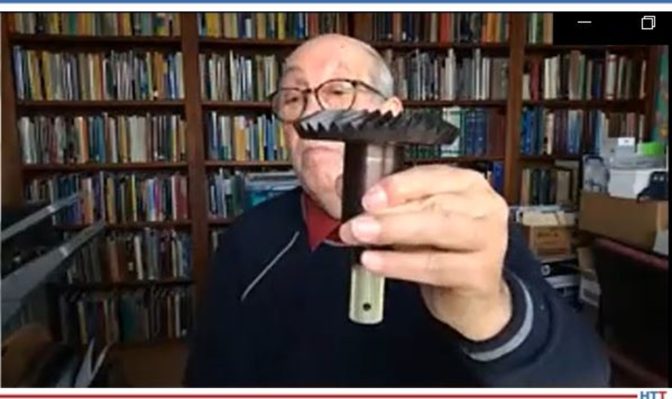
"Let me give you an example, if I can: I’ll hold this up; I don’t know if people can see it that well, but what this is is a helicopter transmission gear."
Let me give you an example, if I can: I’ll hold this up; I don’t know if people can see it that well, but what this is is a helicopter transmission gear. And if we were manufacturing this particular gear, one of the things we would do to measure, if we were successful or to see if we were successful, is to measure the dimensions of the gear that we were actually taking and manufacturing. But in the world of heat treating, because the changes happen inside the material, it’s very difficult to know if the part is good or not. But heat treating has the ability, as we say, to vary the mechanical properties, the physical properties and the metallurgical properties of a material. The problem is that we can change them either for the better or, as most heat treaters know, we can change them for the worst. That’s why there is something called quality control and quality assurance. But I’m drifting away from the main point.
In the world of heat treating, with that definition — the controlled application of time, temperature and atmosphere to produce the predictable change in the internal structure of a material — not only are we heat treat centric in this industry, but we are also often steel or iron and steel centric in this industry. Metallurgists tend to be either ferrous metallurgists (specializing in irons and steels) or nonferrous metallurgists, specializing in things called aluminum, or as the British and Europeans would say, “aluminium,” titanium, and some of the super alloys and things of this nature. The idea being the fact that there are a lot of different materials that can be heat treated.
We often limit ourselves, if you will. But there are parts of our industry that heat treat: for example, precious metals — the golds, the silvers, the platinums and things of this nature. There are also parts of our industry that deal with copper and brass. There are parts of our industry that deal with ceramics which deal with powder metal, if you will. So, one of the things as heat treaters we must remember is that even under just the heat treat umbrella, there are a lot of different disciplines out there. There are a lot of things that we cover, and we look at. There are a lot of different materials that are processed. And again, we think, in general, as heat treaters and probably incorrectly so, we think about what are called “semifinished goods.” What we think about are parts that are manufactured from steel, aluminum, titanium, copper or powder metal. We think of automotive parts, aerospace parts. We think of something like weapons or military equipment, ammunition, firearms. We think of agricultural products, farm implement products and things of this nature. So, one of the things we must be aware of is that there is a whole world outside of our comfort zone, and that is something that we’re going to explore today.
Before I go on, does that make sense to everyone, or does anyone have any questions about the heat treatment side of what we do?
"Heat treating is the controlled application of time, temperature and atmosphere to produce a predictable change in the internal structure (that means the microstructure to metallurgists) of the material being treated." - Dan Herring
DG: No, I think that makes sense. You mentioned on the inside of the part that things can’t be seen so much. You will probably get to this Dan, but I assume that also includes surface treatments, or would that be something different?
DH: We’ll talk a little bit about the difference between surface treatments and they fall into an area probably referred, in general, as “coatings” and things of this nature. But that is a good question, Doug- plating and coating and things of this nature.
Also, one of the things about heat treating that seems a little bit, possibly confusing is that heat treaters consider processes like brazing (which is a joining process), and they think of soldering (which is a low temperature joining process), as heat treatments. Similarly, we think of sintering, and we think of heat treatments of powder metal products, or we think of powder metallurgy as falling under the subject of heat treatment because we think so much about sintering. But sintering is a bonding or a diffusion process. So, heat treaters think of heat treatment, they think of brazing, and they think of powder metallurgy all combined into that big umbrella. For any brazers who are listening, or any powder metal people who are listening — they probably died of cardiac arrest at this moment in time — but, in general, that’s what heat treating does: it considers those separate entities as part of it.
Let’s go on and look at the fact that I can say to you — automotive components, gears, bearings, aerospace components, landing gear transmission boxes, fasteners, screws, nuts, bolts, farm implement equipment -- those are things that commonly come to mind. People don’t often think, for example though, of things like jewelry which is something that is commonly heat treated or “processed,” if you will, more on the thermal processing side. A lot of electronic materials are also thermally processed, and a lot of castings and things done in the foundry industry.
But, as I said, we think of semifinished goods where a semifinished goods-centric/heat treat-centric world; but there are other worlds out there. Let’s kind of talk about them. But mill practices, or what we call “primary metals,” are another area that’s covered, interestingly enough, under heat treating. Because in steel mills and things of this nature, you’ll find soaking pits, for example. In aluminum processing facilities or aluminum foundries, you might find solution heat treating and aging ovens and things of this nature. So, there is, in a very broad or general sense, heat treating also done on the mill or the material production side of things. Again, unless we’re in that industry, we don’t tend to think about it that much. So, we have to.
But, if I also said to you that things like cosmetics are being processed, not heat treated, but thermally treated, if you will. Or things like cement, or minerals in raw ore, ore materials and things- these all fall in the category of now “thermal processing.”
Let me try to give everybody just a feel for what the different categories of thermal processing are. The number one category, of course, is heat treatment. There is another thermal process . . . . And, by the way, thermal processes are also confused a little bit because we use heat, or we use cold — those are both thermal processes. For all the heat treaters out there, we do things like deep freezing, and we do things like cryo-treatments, cryogenic treatments. Those fall under the umbrella of heat treating. But there are other deep cooling or cooling processes that fall under this umbrella of thermal processing.
Besides heat treatment, thermal processing consists of a few areas which you are maybe familiar with and then again maybe you’re not that familiar with. One of them is calcining which I often call the drying of powders, if you will. This can be in the form of ores, it can be in the form of minerals, it can be in the form of coke (which is a coal byproduct, if you will), it can be in the form of cement. So, there are drying processes that occur under thermal treatment which is in the area of calcining.
There is also a big category called fluid heating where what we’re doing, (and by the way, air is a fluid as well as water and liquids are fluids), so we can turn around and do things like chemical processing which is done at elevated temperature. I had a client that was producing mayonnaise and the mayonnaise has held at 180 degrees Fahrenheit- it is a thermal process, if you will.
Distillation. We won’t talk about alcohol much in the world. I will only comment that all of you think this is a bottle of water, but you could be mistaken about that.
The idea is that fact that fluid heating, calcining, drying, smelting, metal heating in general, curing and forming — which is done a lot on ceramics, on paints, paint drying and things of this nature. There is, just in general, other methods of heating. I’ll give you a simple example: waste incineration. We know that our trash is burned at ultra-high temperatures to reduce emissions, if you will, but avoid going into landfills or, worse yet, dumping it in the ocean and believing that somehow it won’t return to our ecosystem. But incineration is an example of a thermal process.
There are quite a number; there are literally hundreds of thermal processes that are occurring all the time that we don’t, in general, think very much about. Heat treating is typically divided into two general categories — processes that soften a material and processes that harden a material. So, in the category of softening, we think of things like aging, we think of things like annealing, we think of things like normalizing, or even stress relieving (in other words, taking the stress out of material is a softening process).
DG: Tempering, as well, Dan? Would it be in that?
DH: Well, tempering, in a sense, could be considered a softening process. It’s a good one. I consider it more a softening process than a hardening process, but it’s typically so intimately linked with hardening that people think of it as a hardening process. But, hardening and case hardening, austempering, and then, of course, brazing which is a joining process, soldering, sintering which is a bonding process, homogenizing (when we talk about aluminum), solution treating (when we talk about aluminum). Solution treating is not a hardening process, interestingly enough- it’s the aging or the precipitation hardening process after the solution heat treatment that is actually the hardening process.
The idea of the fact is that we’re very familiar with those terms; we’re less familiar with coke ovens or waste incinerators or distilling facilities, or things of this nature. We’re not used to processing resins or composite materials, even though there are autoclaves that use a combination of high pressure and temperature to form some of the composite materials that are used in the aerospace industry.
The way I like to think about it is there is a giant umbrella which is called thermal processing. Under that umbrella is a small segment, maybe not so small, called heat treating, and then heat treating is divided into semifinished goods and raw materials (or primary goods), and then it’s subdivided into irons and steels and nonferrous alloys. Now, in my day, when you graduated university, you graduated with a degree in metallurgy. Today, you become a material scientist which means that you’re dealing with composites, ceramics, electronic materials, a whole series of materials outside the realm of just iron and steel and aluminum and titanium, if you will.
The other thing that’s very interesting about our industry, in general, is probably the aspect of energy usage. The thermal processing industry, in general, and this is a rather stunning number, uses, in round numbers, about 38% of the energy produced in the United States. Now think about that as a number. Of all the energy consumed by people in the U.S. or in Canada or in Mexico or anywhere else in the world, two-thirds of it or greater — 40% of it, almost — is used in thermal processing. About 25% is used by transportation, and another 20% or so is used by residential. Then, there’s about 15% used in, what we call, “other” category. But, in thermal processing, which is also true in heat treating, about 80% of the energy comes from natural gas. And only 15%, (round numbers), comes from electricity.
We have to realize that we’re not only, as heat treaters “heat treat-centric,” “iron and steel-centric,” “aluminum-centric,” but we’re also “natural gas-centric.” Those are staggering numbers to consider. The reason for it, the reason we’re natural gas centric, not only in the heat-treating industry but in the thermal processing industry as a whole, is simply because natural gas is the cheapest energy source available right now. And, these numbers, although they apply specifically to North America, can also apply, if you will, to the world in general. The numbers vary a little bit throughout the world, they may be different in Europe and different in Asia, but not so much that it varies so greatly.
What I’ve tried to cover — and I realize I haven’t left a lot of room for questions here and I apologize for that — but I’ve tried to give you the idea that heat treating is a very important part of a much larger industry that services the manufacturing community.
Let’s open for discussion from anybody.
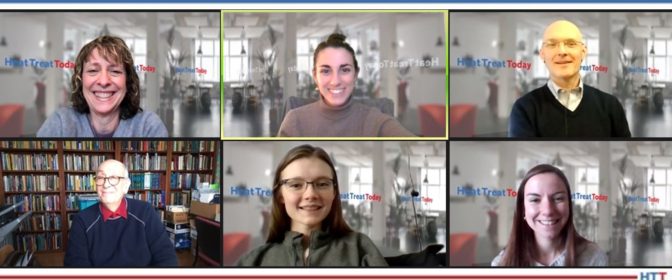
Dan Herring and the Heat TreatToday team: Karen Gantzer, Bethany Leone, Doug Glenn, Dan Herring, Evelyn Thompson, and Alyssa Bootsma
DG: That sounds good. Do any of you have questions, at all?
Alyssa Bootsma: I did have one. I think it was very helpful in understanding everything and the idea that thermal processing is an umbrella and heat treatment is just a part of that really clicked for me. I was wondering if you could talk about calcining a little bit more and what that process actually is.
DH: Sure. But before I do that, I want to mention one thermal process that I forgot to mention. Because I have a number of clients that work in the baking of cookies, and because I’ve consumed a few of those in my life, I don’t want to forget the baking industry.
DG: The brewing industry?
DH: Absolutely! By the way, the brewing hall of fame is located here in Chicago, unless I’m grossly mistaken.
Before we get to far afield, let’s talk about calcining a little bit. A number of powders, whether they be ores or whether they be things like cement or various minerals, are often processed in, what we call, a slurry. They’re processed in a form in which they are either cleaned or washed with water or with different chemicals. As a result, you have a wet mixture of a mineral and, let’s say, water, or in some cases they can be different chemicals, if you will, that go to either clean the minerals or dilute the minerals or things of this nature. But to go to further processing of those minerals, you have to dry them and put them into a form that they can be used. If this makes any sense, then let’s take cement as an example. It’s no good to keep the cement in a slurry because what’s going to happen to the cement? It’s going to dry and harden. So, what you have to do to send it to the consumers is you have to dry the powder, if you will, deliver it to the end-user who will then add liquid to it to once again form it or turn it into liquid cement. Calcining, is really, in simplest terms, to answer the question directly, I always consider it, a powder-drying process.
DG: Dan, any idea why they call it “calcining?” I’ve always wondered this.
DH: Well, in the old days, I believe that limestone, (which is calcium carbonate), and so "calcining" and "calcium" from the calcium carbonate, I think that’s where the name originally came from. A good thing to look up, however- that’ll be my homework assignment.
DG: There you go. Just as another example of a thermal process, it’s certainly not heat treat, just down the road from where I live, north of Pittsburgh, they have a lot of sand and gravel places. Believe it or not, there is a large, what I would call a, horizontally-oriented “screw furnace” — it’s a cylinder and it just rotates, and inside it’s heated up and they’re just simply burning off the moisture so that they can get the materials, or whatever it is they’re harvesting out of the earth, and get it down to a certain level of moisture so that they can process it. So, sand and gravel. That’s just another area.
Here's another one — and Dan, I want you to hit on glass if you don’t mind, in a minute — but here’s another one where thermal processing is used, which you might not think of, and that’s in the manufacturing of paper production. They’ve got to actually dry the paper and you wouldn’t think of it but they’re passing paper through flame (between flames, not actually in the middle of the flames) simply to dry paper before it goes onto these huge rolls.
One last comment, Dan: We often talk about energy intensity and how much energy it actually takes to perform a certain process. One of the highest thermally intense processes that is used is not so much a heat treatment, but it is actually the manufacturing of concrete, believe it or not. There is very, very high energy intensity — it takes a lot of gas, in this case, to produce concrete.
But Dan, if you don’t mind, could you hit on glass production? We’re all looking out windows here and the manufacturer of glass is a thermal process.
DH: Absolutely it is. But before I do that, quickly, that rotary drum that you saw, the one with the screw inside it, if you will, that helps move the powder, if you will, or the sand and gravel through, is a very typical calcining furnace. Rotary drums are also used in the heat treatment industry to process screws and fasteners, nuts and bolts, small products, if you will, typically.
But yes, paper is a good example but glass furnaces, too, where the glass is actually brought up and the sand and other elements, if you will, are melted into glass. Very disconcerting. You may find this interesting but roughly the walls on a glass furnace (I’ve seen 10-20,000-pound glass furnaces) are something like 4 inches thick, holding back all that molten glass. But again, you’re taking glass that is basically silicone dioxide, its sand is a major component of it. In colored glasses, you add different chemicals. Like, for example, if you want to form a bluish colored glass, you might add a copper oxide, for example, which will change or tint the glass to a different color.
You’ve heard of leaded glasses, for example. In the old days you added lead to glass to make it, again, more formable, if you will. But yes, glass furnaces or the manufacture and production of glass is very energy intensive, as well as cement, as is the production of aluminum, by the way, which basically uses electricity, which is why all of the aluminum facilities are located either near hydroelectric or thermal energy like in Iceland, for example, where you have geothermal energy which is used to heat and produce electricity. But yes, glass is definitely an example of a thermal process, as well.
Glass is interesting because we don’t necessarily do a lot of heat treatment of glass, but you may have heard of glass-to-metal sealing, where we’re actually taking a glass and sealing it into or onto a metal component. Like, for example, the site ports of burners where we look in to see the flame — those site ports are made by glass-to-metal sealing. But, in general, yes, melting and production of glass is a thermal process.
DG: Dan, correct me if I’m wrong, and I could be wrong on this, but cellphones, right? Your glass on the front of that — the reason it is actually quite strong and won’t break is because it’s been thermally processed, a tempering process of some sort, I believe. Correct me if I’m wrong, but isn’t it the thermal process that can make a glass really, really difficult to break?
DH: It is, plus the fact that glass is a quasi-solid, as we say. It’s a solid but it’s really not; it has more characteristics of a liquid, which, again, makes it more ductile or resistant to things It makes it more shock absorbing, for example. But yes, cellphones and cellphone glass are something I’ve got to do some more research on.
DG: Right. They’ve got some stuff called “gorilla glass.”
I just want to recap a couple things for our team here and for other people that might be listening: When we talk about heat treat, which is what we’re centered on, it’s helpful for us to know what processes, materials and things that includes, and what processes and materials that doesn’t include, and that’s why this conversation on thermal processing versus heat treat is helpful for us. The way I like to describe it to our team and to most of the people who would be reading our publication or listening to this podcast, is typically Heat TreatToday is not involved with the making of steel but almost everything else after the making of steel we would deal with, almost everything. So, we don’t really do the steel making. Steel making, however, is very much a thermal process but we just don’t cover it. There are other publications that cover that. And we are very much steel-centered; we do aluminum, as well. However, in the aluminum world, we actually do deal with aluminum making. For reasons that basically have to do with the temperature range: the temperature range isn’t quite as high with aluminum making as it is with steel making. So, we do some of that. We don’t do a lot with aluminum making but a lot after aluminum is made. We do a lot of the homogenizing, annealing, solution heat treating and that type of stuff.
So, that is us. In heat treating, we define things like brazing, even though it’s a joining process, we tend to cover it. Soldering we don’t tend to cover because it tends to be a lower temperature. Dan didn’t mention it, but I’m sure he would, is welding: it’s a joining process but it’s not exactly anything we cover either. It’s not what we consider to be heat treating.
There is another joining process that we didn’t cover, and maybe we could hit on it briefly next time, and that is diffusion bonding which, to be quite honest with you, I haven’t done a lot of study on it so it would be interesting to know what that is. I know it’s done in vacuum and under high pressures, I believe, but things of that sort.
At any rate, that what’s we mean when we talk about heat treat — it’s primarily steels, aluminums, titaniums and typically not steelmaking and probably not titanium making either, but aluminum making and everything downstream from that tends to be us, and our temperature ranges tend to be, very generally speaking, 800 degrees Fahrenheit and above, or as Dan mentioned, we can also do some things in the cryogenic range which are subzero temperatures. So, that is us. Everything that falls outside of that we would consider to be a thermal process, which is a lovely thing, but just not our cup of tea.
DH: Look at this, Doug, a whole new business opportunity for you. With that, I’m extending myself beyond metallurgy, so I’ll quit there.
DG: Dan, we really appreciate it. We look forward to more of these. We are going to try to do other topics, again, what I would call heat treat 101 type topics, our Lunch & Learn series with Dan Herring, The Heat Treat Doctor®. Dan, thanks a lot, we appreciate your time.
Maciej Korecki Vice President of Business of the Vacuum Furnace Segment SECO/WARWICK
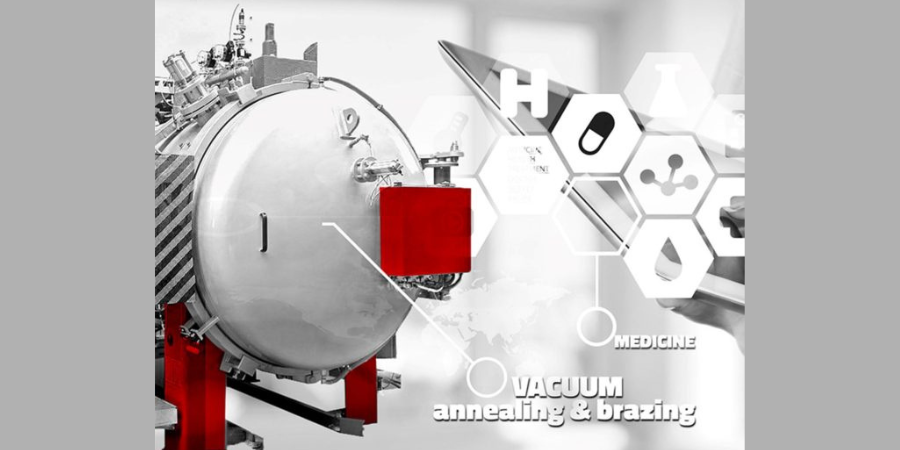
A medical device manufacturer is set to receive a vacuum furnace for annealing and brazing processes at their plant in France. The parts processed in this furnace will include X-ray and radiotherapy equipment among other products that require high quality standards of heat treatment.
The vacuum furnace scheduled for delivery is called the Vector®. "[This furnace] has proven performance in many fields in precision industries such as aviation, automotive and medical branches," commented Maciej Korecki, vice president of the Vacuum Furnace Segment at SECO/WARWICK Group, and international heat treat systems supplier. Korecki continued, "This time, our partner is an expert when it comes to brazing complex components that require high precision."
The high-tech medical industry is one of the most demanding industries in terms of standards, procedures, and process parameters to be met by the equipment involved in the production process. Medical equipment components (e.g., RF components, X-ray tube components, ceramic components) are precision manufactured to the highest quality standards. This is because these components are used for processes that are decisive not only for the quality of treatment, but also for human life.
According to "Dr. O" – Dr. Steve Offley, product marketing manager at PhoenixTM – temperature control of the heat treatment application is critical to the metallurgical and physical characteristics of the final product, and hence its ability to perform its intended function. Explore today's Technical Tuesday article to find the light at the end of your mesh belt furnace tunnel.
This article first appeared in Heat TreatToday’sFebruary 2022 Air & Atmosphere Furnace Systems print edition.
Dr. Steve Offley, “Dr. O" Product Marketing Manager PhoenixTM
Introduction – The Need for Accurate Product Temperature Measurement
Even though modern furnaces are supplied with sophisticated control systems, they are still not always capable of truly giving an accurate picture of the actual product temperature as it passes through the process. Temperature sensors positioned along the furnace give a snapshot of what the environmental temperature is possibly zone by zone. Furnace controllers, as the name suggests, can give confidence that the process heating is performed in a controlled manner but will never give an accurate view of what the actual product temperature is. When monitoring, it is important to be able to distinguish between process and product.
The challenge to any process engineer is understanding how the product heating cycle relates to the operation of the furnace. A furnace environment may be well controlled, but very different product temperatures can be experienced with variation in key properties such as product material, size, shape, thermal mass, and position/orientation in the furnace. Infrared (IR) pyrometers and thermal imagers can provide surface temperature measurements only and require line of sight, so they limit the areas of the product that can be measured. Setup can sometimes be complex considering surface characteristics (emissivity) and process background/atmosphere compensation. As with air sensors, being fixed, typically IR sensors only give information at that specific furnace location which prevents accurate calculation of soak times at critical temperatures. Without additional information, soak times and temperatures may need to be extended well beyond the target to guarantee the heat treat process is completed with confidence with an obvious compromise to throughput and energy conservation.
Product Temperature Profiling
To fully understand the operational characteristics of the heat treat process it is necessary to measure both the environment and product temperature continuously as it travels through the process. Such technique provides what is referred to as a “temperature profile” which is basically a thermal fingerprint for that product in that furnace process. This thermal fingerprint will be unique but will allow understanding, control, optimization, and validation of the heat treat process.
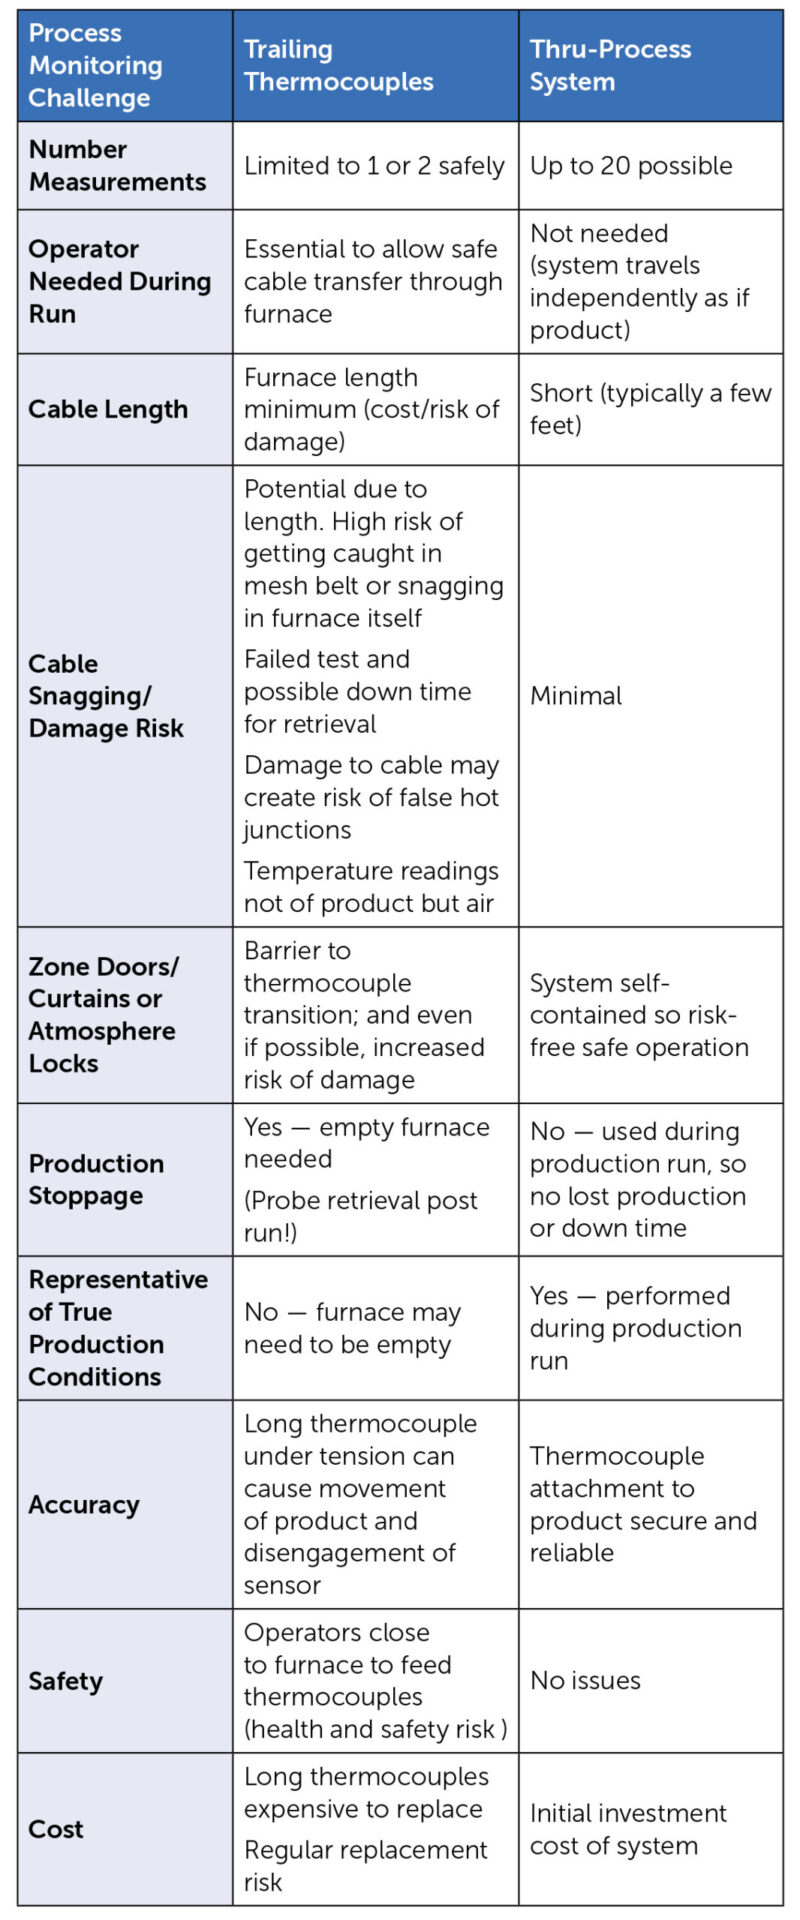
Table 1. Table showing the numerous benefits of thru-process temperature monitoring over traditional trailing thermocouples methodology for a mesh belt furnace
Historically, trailing thermocouples have been the go-to technique for product temperature monitoring. A very long thermocouple is attached to the product in the furnace. The data logger measuring the live temperature reading is kept external to the furnace. Although possible for static batch processes, the technique has significant limitations in a continuous/semicontinuous process, especially mesh belt furnaces (See Table 1).
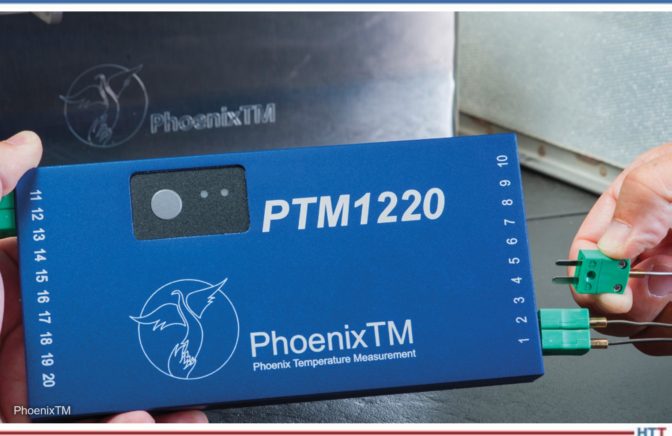
Fig 1. Robust multichannel data logger designed specifically for thru-process temperature profiling
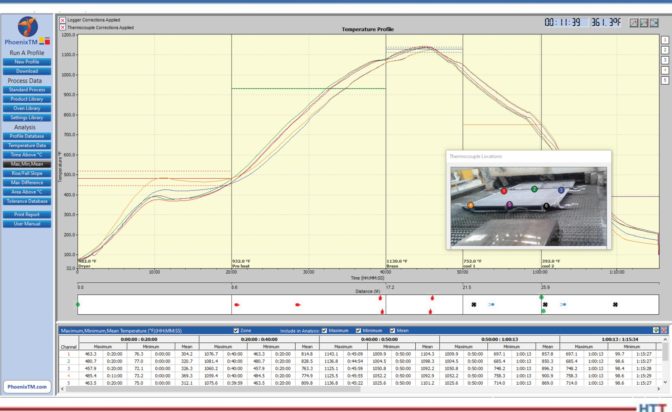
In thru-process temperature profiling the data logger travels with the product through the furnace. The data logger (Figure 1) is protected by an enclosure, referred to as a thermal barrier, which keeps the logger at a safe operating temperature (Figure 2). Temperature readings recorded by the data logger from multiple short length thermocouples can be retrieved post run. Alternatively, if feasible, the data can be read in real time as the system passes through the furnace using a two-way radio frequency (RF) telemetry communication option. The resulting temperature profile graph (Figure 3) provides a comprehensive picture — product thermal fingerprint — of the thermal process.
Fig 2. Thermal barrier protecting the data logger safely entering the conveyor furnace during the temperature profile run. Barrier size is customized to suit process credentials.
Fig 3. Typical temperature profile recorded for an aluminum CAB brazing line giving a complete temperature history for a brazed radiator at different product locations.(1)
Monitoring Your Heat Treat Process Temperature at the Product Level
Applying thru-process temperature monitoring product temperature measurement can focus on the micro product level which at the end of the day is most important. Static control thermocouples give an environmental temperature of the furnace in a zone, but this only reflects the true temperature wherever the thermocouple is located. This may be some distance from the product and may give some bias to its position if located on one side of the furnace. The thru-process monitoring system allows simultaneous product and/or air temperature measurement directly at the mesh belt. Monitoring can be performed across the belt with thermocouple placement on and in the core of the product and can be made to identify areas of different thermal mass resulting in differing heating characteristics.
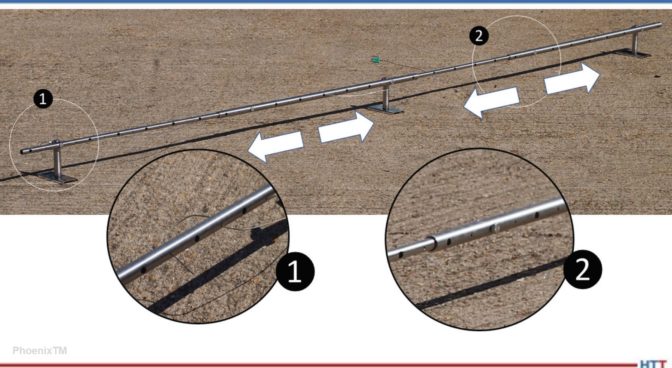
A useful strategy to use before looking at the product temperature is to thermally map the furnace. Thermocouples, connected to the data logger protected within the thermal barrier, are positioned across the mesh belt using a mount jig such as that shown in Figure 4. The jig guarantees reliable location of the measurement sensor run to run and adjustment means it can be adapted to different belt widths. Applying this principle, the thermal uniformity of air across the belt width through the entire furnace can be measured.
Fig 4. Thermocouple mount jig allowing accurate positioning of thermocouples (1) across the mesh belt width with adjustment to suit different belt dimensions (2).
Such data can be compared with zone control thermocouples to see what temperature differential the product may be experiencing at the belt level. Temperature imbalances across the belt and hot or cold spots along the process journey can be identified.
Furnace mapping can be further developed to satisfy either CQI-9/CQI-29 or AMS2750F pyrometry standards where a two-dimensional jig is constructed to perform the temperature uniformity survey (TUS).2 Employing the plane method, a frame jig is constructed to match the furnace work zone with the necessary number of thermocouples to satisfy the furnace cross section dimensions. Temperatures recorded over the working zone are compared to the desired TUS levels to ensure that they are within tolerance as defined in the standards.
Discover the True Root Cause of Your Furnace Problems
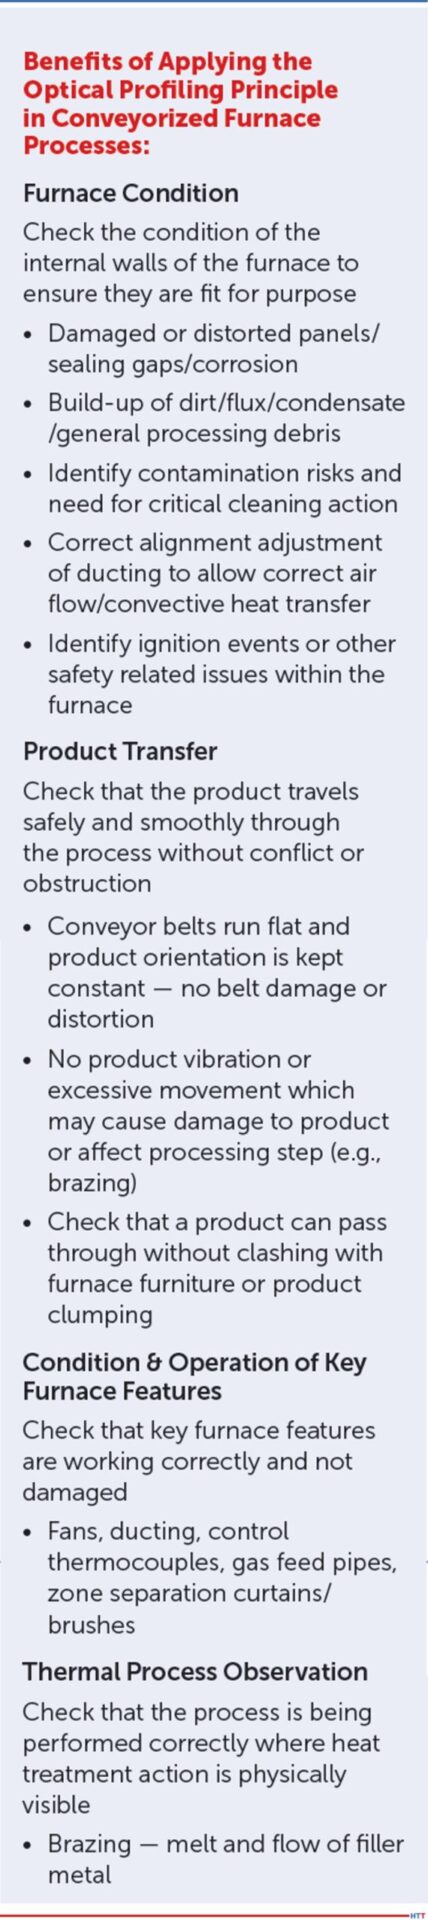
When it comes to product quality and process efficiency in any mesh belt furnace applications, temperature monitoring is only part of the story. Gaining an insight into what is physically happening in the product’s furnace journey can help you understand current issues or predict issues in the future, which can be corrected or prevented. To allow true root cause analysis of temperature related issues, it is sometimes necessary to “go to Gemba” and inspect what the product is experiencing, directly in the furnace. This is not always possible under true production conditions.
For a classic mesh belt furnace application such as controlled aluminum brazing (CAB), internal inspection of the furnace is not a quick and easy task. Operating at 1000°F, the cool down period is significant to allow engineers safe access for inspection and corrective action and then further delay to get the furnace back up to a stable operating temperature. Such maintenance action may mean one or two days lost production, from that line, which is obviously detrimental to productivity, meeting production schedules, satisfying key customers, and the bottom line.
In addition to process temperature problems there are many other production issues that can be faced relating to the furnace operation and safe reliable transfer of the product through the furnace. In the CAB process a day-to-day hazard is the build-up of flux debris. Flux materials used to remove oxides from the metal surface and allow successful brazing can accumulate within the internal void of the furnace. These materials are most problematic at the back end of the muffle section of the furnace where, due to the drop in temperature entering the cooling zone, materials condense out. Flux buildup can create many different process issues including:
Physical damage to the conveyor belt or support structure requiring expensive replacement
Reduction in belt lubricity creating jerky movement and causing unwanted product vibration
Lifting of the mesh belt creating an uneven transfer of products causing possible excessive product movement, clumping, or clashing
Reduction in inner furnace clearance creating possible product impingement issues and blockages
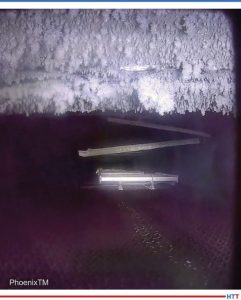
To prevent such problems, regular scheduled inspection and clean out of the furnace is necessary. This is not a pleasant, quick operation, and requires chipping away flux debris with pneumatic tools. Often requiring a furnace down time of 1 to 2 days, this task is only performed when essential. Leaving the clean-up operation too long can be catastrophic, causing dramatic deterioration in product quality or risk of mid-production run stoppages.
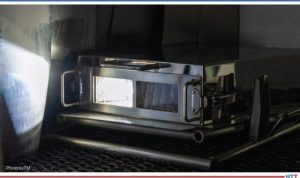
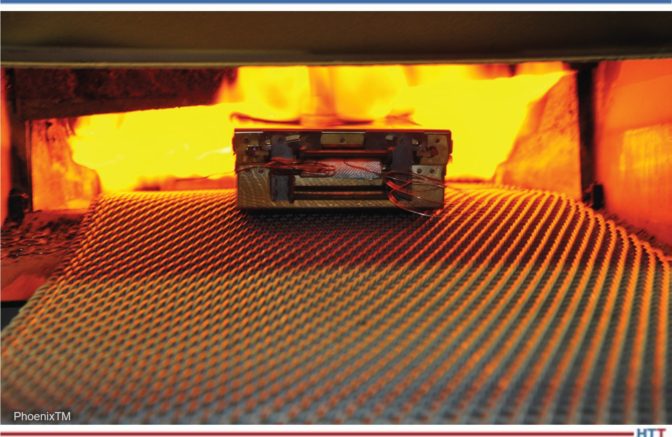
Figure 5. PhoenixTM Optical profiling ‘Optic’ System - Optical Profile View. System adaptable for both temperature and optical profiling.
Figure 5.1. High temperature thermal barrier for aluminum brazing system protecting camera and torches through CAB furnace
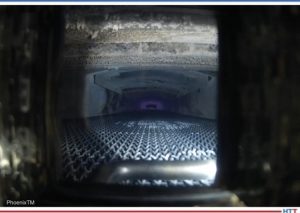
Figure 5.2 Video image in inner CAB furnace showing condition of inner furnace, mesh belt and product transfer
Figure 5.3. Identification of flux debris at back end of muffle furnace prompting scheduling of clean down operation
Optical Profiling – The Efficient Alternative
Optical profiling is a new complementary technique to that of thru-process temperature profiling. The innovative technology allows for the first-time process engineers to view the inner workings of the furnace under normal production conditions. Traveling through the furnace with the products being processed, the optic system gives a product’s eye view of the entire heat treatment journey. A thermal barrier, similar in design to that used in temperature profiling, protects a compact video camera and torch that are used to record a video of what a product would see traveling through the furnace (Figure 5). The principle is just like your car’s dash cam, the only difference being that your journey is being performed in a furnace at up to 1000°F. The resulting video, “Optical Furnace Profile,” shows process engineers so much about how their process is operating without any need to stop, cool, and dismantle the furnace. This allows safe routine furnace inspection without any of the problems of costly lost production and days of furnace down time.
Summary
Monitoring your mesh belt furnace from a temperature and optical perspective allows you to fully understand what truly happens in that black box. Understanding leads to better control, which helps you get the optimal performance out of your heat treat process from a quality, productivity, and energy efficiency perspective.
Don’t get left in the dark. Consider the power of temperature and optical profiling which will literally provide a light at the end of your furnace tunnel!
References:
[1] Steve Offley, “Unveiling the Mystery of Your Al Brazing Furnace with ‘Thru-Process’ Temperature Profiling," Heat Treat Today Magazine, June 2020, p40.
[2] Steve Offley, “Applying ‘Thru-process’ Temperature Surveying To Meet the TUS Challenge of CQI-9.” HeatTreatToday.com. June, 2019. https://www.heattreattoday.com/heat-treat-news/automotive-heattreat-news/applying-thru-processtemperature-surveying-to-meet-thetus-challenges-of-cqi-9/
About the Author:
Dr. Steve Offley, “Dr. O,” has been the product marketing manager at PhoenixTM for the last 4 years after a career of over 25 years in temperature monitoring focusing on the heat treatment, paint, and general manufacturing industries. A key aspect of his role is the product management of the innovative PhoenixTM range of ‘thruprocess’ temperature and optical profiling and TUS monitoring system solutions.
"The inventory levels for almost every industrial metal have been as low as they have been in decades and at the same time there has been more demand as industry starts to stage a recovery in key areas."
As we emerge from pandemic slowdowns and disruptions, there are still "lions, tigers, and bears — oh my!" that manufacturers face. The monthly Industrial Heating Equipment Association’s (IHEA) Executive EconomicSummary released in February notes that in economic terms, it has been "inflation, supply chain, and labor — oh my!" for several months, but at least two of these may be letting up in 2022.
First, inflation. Inflation is the highest it has been in decades: 7.5%. The report reveals the reasons why this is the case: "For the better part of the last four decades the US was able to essentially export inflation . . . If one was facing higher labor costs and higher production costs the easiest response was to either produce or source overseas where the costs were dramatically lower." Now, many U.S. companies are undoing this in light of rowing costs from overseas suppliers and supply chain upheaval.
And high inflation rates and the supply chain are recovering. While the "stimulus effort dumped the equivalent of the Japanese GDP into the hands of consumers," they were unable to continue normal purchasing habits, and cash tied up in savings contributed to inflation. But now, consumers have fed most of that cash back into the economy. Additionally, producers are slowly catching up with demand, which will stabilize commodity costs from contributing to inflation. The last contributing factor to inflation is less positive; the report notes that cost of labor -- having risen over the course of the pandemic -- are unlikely to come down, which will likely inhibit the full return "back to normal." Still, even the supply chain's 2021 recovery is cause for celebration, having been "far more aggressive than anyone had expected and producers were unprepared. They are starting to gain ground and by mid-year they are expected to have caught up with the majority of current consumer demand. The primary issue now is China."
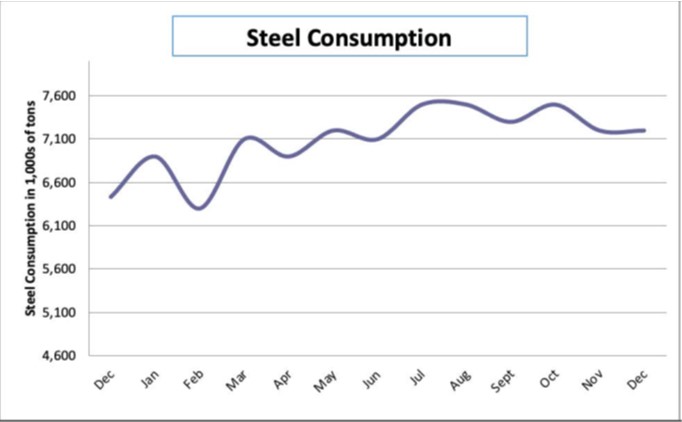
Steel consumption will surge later this year as orders from Congress's infrastructure spending plan are placed.
Unfortunately, the retirements of key workers as well as a simple lack of hands put pressures on labor costs. Paired with increased wage demands, "Skilled workers have more leverage than they have ever had and the number one means by which companies are expanding their workforce is by poaching from one another." This leads to paying new hires and longtime employees higher wages to disincentivize job hopping.
Anne Goyer, Executive Director of IHEA
The report concludes, "labor costs soared by over 5.0% last year and these costs are heading in the same direction in 2022."While we may not be out the thicket yet, there is still hope along two of the three economic indicators.
Check out the full report to see specific index growth and analysis which is available to IHEA member companies. For membership information, and a full copy of the 12-page report, contact Anne Goyer, executive director of the Industrial Heating Equipment Association (IHEA). Email Anne by clicking here.
Welcome to Heat TreatToday's This Week in Heat TreatSocial Media. You know and we know: there is too much content available on the web, and it’s next to impossible to sift through all of the articles and posts that flood our inboxes and notifications on a daily basis. So, Heat TreatToday is here to bring you a hot take of the latest compelling, inspiring, and entertaining heat treat chatter from the world of social media.
We're looking at helicopters for space, celebrations in heat treat, quick diagrams to keep you on your toes, and much more.
We're moving faster and further into the journey beyond earth. . . "At the end of Ingenuity’s mission, Perseverance will drive off, leaving the little helicopter that could behind, and continue its own mission: to search for signs of past life in Jezero crater, and to store rocks for a future mission to return to Earth." (NASA’s Ingenuity Helicopter Made History by Flying on Mars)
2. Heat Treating "Wow" Factors
Quick social media posts that make you go "wow."
"We Work Well Together" -Robot 1
.
Enjoying the North American Market?
When Steel Loses Its Magnetism
3. Deep Dive Learning
Have a little extra time? Check out these engaging media about heat treatments below.
Tips to reduce retained austenite in carburizing and carbonitriding by David Pye (www.htcourses.com)
.
What To Do In the Event of a Safety Failure
Tensile Properties
4. Social Moments in Our Community
There's almost (almost) always a reason to celebrate. See some favorites from around the industry.
Employee Gets Some Kudos
."CELEBRATING THE KANTHAL STORY"
Children's Day and National Metallurgists Day in India
5. The Reading Corner
Soak in some knowledge on austenite, robotics, and salt quenching in these key podcasts that you can watch, listen to, or read the transcripts of.
Heat Treat Radio: Robotics in Heat Treat, a Conversation With Dennis Beauchesne, ECM-USA: Click to -->Watch | Listen | Learn
Heat Treat Radio: The Greenness and Goodness of Salt Quenching with Bill Disler: Click to -->Watch | Listen | Learn
We’re flipping through Heat Treat Today’s technical articles today to highlight four processes: annealing, brazing, carburizing, and forging. Read our top picks of technical articles from these categories like a case study on parts failure (annealing solution) and a new competitor to tried-and-true brazing.
When an automotive manufacturing began loosing time, money, and the steel itself due to frequent cracking, a third party stepped in to solve the part failure.
[blockquote author=”” style=”1″]In this case, the life cycle of these parts began in a steel mill, where coils of AISI 1045 carbon steel were produced. The parts were then annealed in preparation for fine blanking at our customer’s facility. Then, the parts would be through hardened and sent to the automotive manufacturer.[/blockquote]
Electric vehicle production, semiconductor development, and a whole wealth of novel products are pushing at the fringes. Does this demand change to tried-and-true heat treat applications? You tell us!
[blockquote author=”” style=”1″]The most sophisticated global companies in electronic instrumentation and semiconductors view diffusion bonding as the wave of the future. The functional-value that 21st-century diffusion bonding technology now offers is a unique-and-beneficial solution in a class by itself; designers came to this realization after being confronted with component performance issues that could not be resolved by traditional brazing. Materials currently under consideration include pure aluminum, aluminum alloys, stainless steels, and nickel-based alloys as well as any other material, such as coated substrates for power electronics or glass and special material combinations (dissimilar joints).[/blockquote]
This technical article can be found under “Carburizing” in the navigation bar, but as the name implies, you’ll be diving into five essential case-hardening processes. BONUS! this one includes an excellent table to break down the differences.
[blockquote author=”” style=”1″]Case hardening processes are some of the most common heat treatments performed, but each process has its own unique needs. The table below [in the article] provides a summary of the considerations that need to be made when selecting the optimum process. This list is by no means exhaustive; it is encouraged to work with a furnace manufacturer familiar with each process to help select the correct process and equipment needed.[/blockquote]
Here’s a brain spinner: Direct from Forge Intensive Quenching. If you just asked “What?” Best read the full report (or at least the abstract) that tests this novel method — a method that could eliminate normalizing, quenching, and tempering.
[blockquote author=”” style=”1″]Data obtained on the mechanical properties of DFIQ forgings were compared to that of forgings after applying a conventional post-forging heat-treating process. Values of heat transfer coefficients in the DFIQ tank were determined experimentally using a special probe. This data was needed for calculating an optimal dwell time when quenching forgings in the DFIQ tank. It was shown that the application of the DFIQ process allows elimination of. . .[/blockquote]
A large gas-fired normalizing furnace has been sent to a global manufacturer of pipe, tube, and fittings used for various military contracts. Supply chain issues prevented the manufacturer from receiving the furnace on the original delivery date in Q4 2021.
This L&L Special Furnace Co., Inc. car-bottom-style gas-fired normalizing furnace is rated to operate at temperatures from 1,300°F/704°C to 2,200°F/1204°C and heated with six medium-velocity burners. The furnace will be able to maintain uniformity of ±25°F/12.5°C at temperatures above 1,300°F/704°C.




 The “Known – Unknown,” the “Undiscovered Country,” the “Movement from cocksure ignorance to thoughtful uncertainty.” It doesn’t matter if you get your catch phrase from Donald Rumsfeld, Star-Trek, or that plaque your mother kept above the kitchen sink, the implication is the same: we really don’t know what the future holds. But, the Unknown of which I speak in this article is natural gas prices.
 Find heat treating products and services when you search on Heat Treat Buyers Guide.com





 DG: Dan, any idea why they call it “calcining?” I’ve always wondered this.

 According to "Dr. O" – Dr. Steve Offley, product marketing manager at PhoenixTM – temperature control of the heat treatment application is critical to the metallurgical and physical characteristics of the final product, and hence its ability to perform its intended function. Explore today's Technical Tuesday article to find the light at the end of your mesh belt furnace tunnel.
 Furnace mapping can be further developed to satisfy either CQI-9/CQI-29 or AMS2750F pyrometry standards where a two-dimensional jig is constructed to perform the temperature uniformity survey (TUS).2 Employing the plane method, a frame jig is constructed to match the furnace work zone with the necessary number of thermocouples to satisfy the furnace cross section dimensions. Temperatures recorded over the working zone are compared to the desired TUS levels to ensure that they are within tolerance as defined in the standards.