Let’s discover new tricks and old tips on how to best serve air and atmosphere furnace systems. In this series, Heat Treat Today compiles top tips from experts around the industry for optimal furnace maintenance, inspection, combustion, data recording, testing, and more. Part 2, today's tips, examines burner and flame safety. Look back to Part 1 here for tips on seals and leaks.
This Technical Tuesday article is compiled from tips in Heat Treat Today's February Air & Atmosphere Furnace Systems print edition. If you have any tips of your own about air and atmosphere furnaces, our editors would be interested in sharing them online at www.heattreattoday.com. Email Bethany Leone at bethany@heattreattoday.com with your own ideas!
1. Operating with a Multiple Burner System
Contact us with your Reader Feedback!
If a furnace or oven has a multiple burner combustion system with only one valve train, a multi-burner combustion safeguard should be used. This ensures that if one burner fails, they all go out.
Source: Bruce Yates, "Ten Tips for Safeguarding Combustion Processes"
#multiburner #combustion #safety
2. Regularly Inspect Retort Alloys
Source: Nitrex
Retort alloys must be inspected on a regular basis. Hot spots can be identified by bulges. Plastic deformation occurs due to overheating, causing the hotter section to bulge because it is surrounded by stronger metal. Inspect your retorts or radiant tubes for deformations. In addition, constant thermal cycling can cause problems with some alloys. Look for cracks in welds or near welds. Some leak detection methods can also detect alloy issues or overheating.
Localized overheating could indicate a problem with the burner or the heating element. Early detection and correction can save you a lot of money on expensive alloys.
Flame supervision may be defined as the detection of the presence or absence of flame. If a flame is present during the intended combustion period, the supervisory system will allow a fuel flow to feed combustion. If the absence of flame is detected, the fuel valves are de-energized.
This basic definition does not consider the hazard potential during startup or ignition, however. A dangerous combustible mixture within a furnace or oven consists of the accumulation of combustibles (gas) mixed with air, in proportions that will result in rapid or uncontrolled combustion (an explosion). It depends on the quantity of gas and the air-to-fuel ratio at the moment of ignition.
Source: Bruce Yates, "Ten Tips for Safeguarding Combustion Processes"
#flamedetection #combustion #valves
4. Remember that Flame Safety Starts with Purging
The sequence for flame safety starts with purging the furnace or oven. Purge time should allow for four air changes.
Fuel valves can — and do — leak gas. The purpose of purging is to remove combustible gases from the combustion chamber before introducing an ignition source. The four air changes in the combustion chamber are based on a worst-case scenario that includes having a burner chamber that is completely filled with gas.
Once airflow for purge is verified, the proof-of-valve closure is confined and safety limits are proven. Then the purge timer — which may or may not be integral to the combustion safeguard — determines the period of time required to evacuate the combustion chamber.
Source: Bruce Yates, "Ten Tips for Safeguarding Combustion Processes"
Maciej Korecki Vice President of Business of the Vacuum Furnace Segment SECO/WARWICK
A manufacturer of a wide variety of vacuum circuit breakers ordered vacuum furnaces for metal heat treatment. The circuit breakers must be brazed with high vacuum.
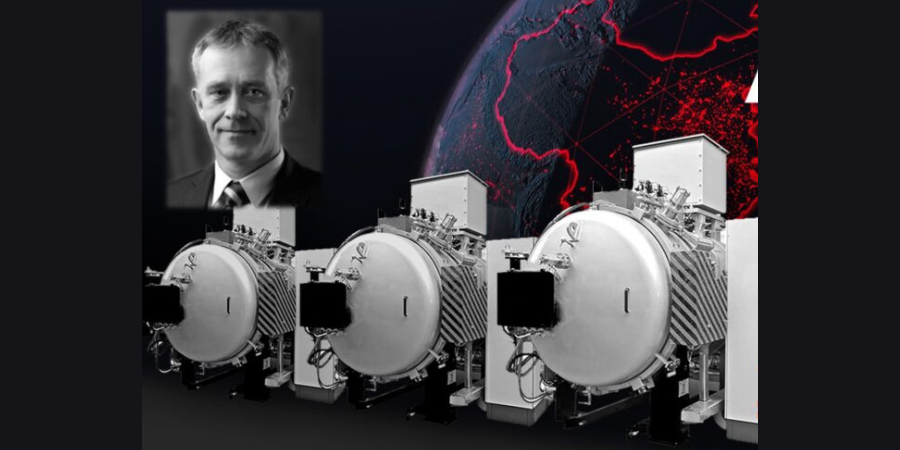
In 2017, the first furnaces provided were two SECO/WARWICK furnaces. The most recent expansion is three Vector vacuum furnaces that provide high vacuum level and temperature uniformity within the entire load.
"[T]he specificity of this electric power control production requires incredible precision. Circuit breakers need a high level of vacuum and temperature uniformity. They are brazed in vacuum furnaces in a very high vacuum; therefore, it was necessary to use an efficient pumping system consisting of a turbomolecular pump and a dry pump." Maciej Korecki, vice president of the Vacuum Products Segment at SECO/WARWICK Group, a manufacturer with North American locations.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
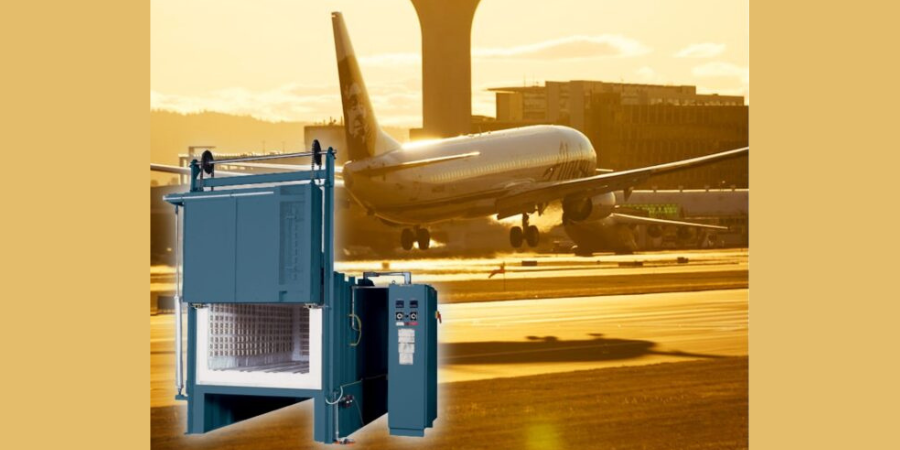
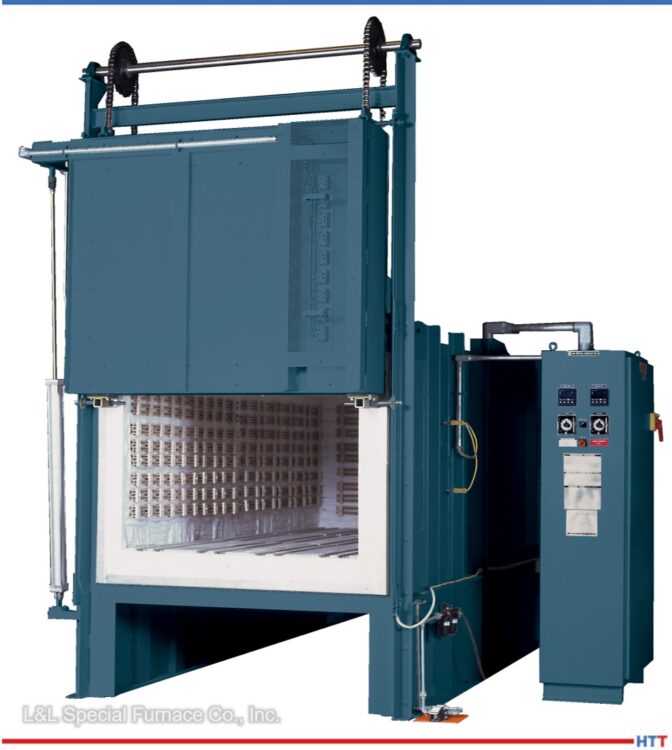
A front-loading box furnace delivered to a northeastern U.S. supplier of titanium castings will expand the manufacturer’s aerospace and gas turbine castings heat treat abilities. The company supplies to the aerospace and power generation fields and deals with exotic metals that are ideal for superior products using the lost wax process for castings, such as nickel and cobalt-based alloys.
L&L Special Furnace Co., Inc. Box Furnace Source: L&L Special Furnace Co., Inc.
The L&L Special Furnace Co., Inc. model FB435 has an effective work area of 48” wide by 32” tall by 60” deep and has certifiable temperature uniformity of ±10°F from 500 to 1,850°F. Additionally, the elements are very evenly spaced around the chamber and the furnace is lined with ceramic fiber on the sides and top.
The furnace case is sealed internally for atmosphere control, and an inert blanketing gas such as nitrogen is used to displace oxygen present within the work chamber. This provides a surface finish in which oxidization is less likely to form on the part. The atmosphere is delivered automatically through a flow panel by the furnace control.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Where did the ±0.1°F AMS2750 requirement come from and how should heat treaters approach this specification, an important change that entails major buy-in? Andrew Bassett, president and owner of Aerospace Testing and Pyrometry, was at the AMS2750F meeting. He shares the inside scoop on this topic with Heat Treat Today and what he expects for the future of this standard.
Heat Treat Radio podcast host and Heat Treat Today publisher, Doug Glenn, has written a column on the topic, which you can find here; read it to understand some of the background, questions, and concerns that cloud this issue.
Below, you can watch the video, listen to the podcast by clicking on the audio play button, or read an edited transcript.
The following transcript has been edited for your reading enjoyment.
Doug Glenn: Andrew Bassett, president and owner of Aerospace Testing and Pyrometry, Inc., somewhere in eastern Pennsylvania. We don’t know because you’re on the move! What is your new address, now, by the way?
Contact us with your Reader Feedback
Andrew Bassett: We are in Easton, Pennsylvania at 2020 Dayton Drive.
Doug Glenn: Andrew, we want to talk a bit about this ±0.1°F debate that is going on. It was actually precipitated by the column that I wrote that is in the February issue.
I just wanted to talk about that debate, and I know that you’ve been somewhat involved with it. So, if you don’t mind, could you give our listeners a quick background on what we are talking about, this ±0.1°F debate.
Andrew Bassett: To be honest with you, being part of the AMS2750 sub team, one of the questions came up for us during the Rev F rewrite was this 0.1°F readability — wanting to kind of fix this flaw that’s been in the standard ever since the day that AMS2750 came out. With instrumentation, for instance, you have ±2°F (the equivalent would be 1.1°C). At 1.1°C, the question became, If your instrumentation does not show this 0.1 of a degree readability, how can you show compliance to the standards?
Andrew Bassett President Aerospace Testing and Pyrometry Source: DELTA H
Then, it morphed into other issues that we’ve had in the previous revisions where we talk about precise temperature requirements, like for system accuracy testing: You’re allowed a hard number ±3° per Class 2 furnace or 0.3% of reading, whichever is greater. Now, we have this percentage. With anything over 1000°F, you're going to be able to use the percentage of reading to help bring your test into tolerance. In that example, 1100°F, you’re about 3.3 degrees. If your instrumentation doesn’t show this readability, how are you going to prove compliance?
That’s what it all morphed into. Originally, the first draft that we proposed in AMS2750F was that all instrumentation had to have 0.1°F readability. We got some feedback (I don’t know if I want to say “feedback” or "pitchforks and hammers") that this would be cost-prohibitive; most instrumentation doesn't have that readability, and it would be really costly to go out and try to do this. We understood that. But, at the end of the day, we said: The recording device is your permanent record, and so that’s what we’re going to lean on. But we still had a lot of pushback.
We ended up putting a poll out to AMEC and the heat treating industry to see what their opinions were. We said that with the 0.1 readability (when it came to a percentage reading), recording devices would read hard tolerances. So, for instance, an SAT read at 3° would be just that, not "or .3% of reading."
There was a third option that we had put out to the community at large, and it came back as the 0.1° readability for digital recorders, so that’s where we ran with the 0.1° readability.
When it was that big of an issue, we didn’t make the decisions ourselves; we wanted to put it out to the rest of the community. My guess is not everyone really thought the whole thing through yet. Now people are like, ok, well now I need to get this 0.1° readability.
Again, during the meetings, we heard the issues. Is 0.1° going to really make a difference to metal? If you have a load thermocouple that goes in your furnace and it reads 0.1° over the tolerance, does it fail the load? Well, no, metallurgically, we all know that’s not going to happen, but there’s got to be a line in the sand somewhere, so it was drawn at that.
"...that hard line in the sand had to be drawn somewhere..." Source: Unsplash.com/Willian Justen de Vasconcellos
That’s a little bit of the background of the 0.1° readability.
Doug Glenn: So, basically, we’re in a situation, now, where people are, in fact (and correct me if I’m wrong here), potentially going to fail SATs or tests on their system because of a 0.1° reading, correct? I mean, it is possible, correct?
Andrew Bassett: Yes. So, when the 0.1° readability came out in Rev F, we gave it a two-year moratorium that with that requirement, you still had two more years. Then, when Rev G came out, exactly two years to the date, we still had a lot of customers coming to us, or a lot of suppliers coming back to us, and saying, “Hey, look, there’s a supply shortage on these types of recorders. We need to buy some time on this.” It ranged from another year to 10 years, and we’re like — whoa, whoa, whoa! You told us, coming down the pike before, maybe you pushed it down the road, whatever, probably Covid put a damper on a lot of people, so we added another year.
So, as of June 30th of 2023, that requirement is going to come into full play now. Like it or not, that’s where the standard sits.
Doug Glenn: So, you’re saying June 30th, 2023?
Andrew Bassett: Yes.
Doug Glenn Alright, that’s good background.
I guess there were several issues that I raised. First off, you’ve already hit on one. I understand the ability to be precise, but in most heat treatment applications, one degree is not going to make a difference, right? So, why do we push for a 0.1° when 1° isn’t even going to make a difference?
Andrew Bassett: We know that, and it’s been discussed that way. But, again, that hard line in the sand had to be drawn somewhere, and that was the direction the community wanted to go with, so we went with that. Yes, we understand that in some metals, 10 degrees is not going to make a difference, but we need to have some sort of line in the sand and that's what was drawn.
Doug Glenn: So, a Class 1. I was thinking the lower number was a tighter furnace. So, a Class 1 (±5), and you’re saying, that’s all the furnace is classified for, right, ±5? So, if you get a reading of 1000°, it could be 1005° or it could be 995°. Then, you’re putting on top of that the whole idea that your temperature reading has got to be down to 0.1°. There just seems to be some disconnect there.
So, that was the first one. You also mentioned the instrumentation. It’s been pointed out to me, by some of the instrumentation people, that their instruments are actually only reading four digits. So up to 99.9 you actually have a point, but if it goes to 1000°, you’re out of digits; you can’t even read that. I mean, they can’t even read that down to a point.
"So, if you get a reading of 1000°, it could be 1005° or it could be 995°." Source: Unsplash.com/Getty Images
Andrew Bassett: Correct. On the recording side of things, we went away from analog instrumentation. The old chart papers, that’s all gone, and we required the digital recorders with that 0.1° readability, as of June 30th of this year.
Again, the first draft was all instrumentation. That would be your controllers, your overtemps, and we know that limitation. But everyone does have to be aware of it. We still allow for this calibration of ±2 or 0.2%. If you’re doing a calibration, let’s say, on a temperature control on a calibration point at 1600° and the instrument only reads whole numbers, you can use the percentage, but you would have to round it inward. Let’s use 1800°, that would be an easier way to do it. So, I’m allowed ±2 or 3.6° if I’m using the percentage of reading, but if the instrument does not read in decimal points for a controller or overtemp, you would have to round that down to ±3°.
Doug Glenn: ±3, right; the 0.6° is out the window.
Andrew Bassett: Correct. I shouldn’t say we like to bury things in footnotes, but this was an afterthought. In one of the footnotes, in one of the tables, it talks about instrumentation calibration that people need to be aware of.
Doug Glenn: Let’s just do this because I think we’ve got a good sense of what the situation is, currently. Would you care to prognosticate about the future? Do you think this is going to stand? Do you think it will be changed? What do you think? I realize you’re speaking for yourself, here.
Andrew Bassett: I’m conflicted on both sides. I want to help the supply base with this issue but I’m also on the standards committee that writes the standard. I think because we’re so far down the road, right now — this requirement has been out there since June 2022 — I don’t see anything being rolled back on it, at this point. I think if we did roll it back, we have to look at it both ways.
If we did roll this back and say alright, let’s just do away with this 0.1° readability issue, we still have to worry about the people processing in Celsius. Remember, we’re pretty much the only country in the world that processes in Fahrenheit. The rest of the world has been, probably, following these lines all along. If we rolled this back, just think about all the people that made that investment and moved forward on the 0.1° readability and they come back and say, “Wait a minute. We just spent a $100,000 on upgrading our systems and now you’re rolling it back, that’s not fair to us.”
At this point, with the ball already rolling, it would be very interesting to see when Nadcap starts publishing out the audit findings when it comes to the pyrometry and this 0.1° readability to see how many suppliers are being hit on this requirement and that would give us a good indication. If there are a lot of yeses on it then, obviously, a lot of suppliers haven’t gone down this road. My guess is, for the most part, anybody that’s Nadcap accredited in heat treating — and this goes across chemical processing, coatings, and a few other commodities — I think has caught up to this.
Personally, I don’t think this is going to go away; it’s not going to disappear. It’s going to keep going down this road. Maybe, if people are still struggling with getting the types of devices that can have that 0.1° readability, then maybe another year extension on it, but I don’t know where that is right now. I haven’t gotten enough feedback from aerospace customers that say, "Hey, I can’t get the recorder." I mean,
Doug Glenn: I just don’t understand, Andrew, how it’s even physically possible that companies can record something as accurately as 0.1° if the assembly or thermocouple wire is rated at ±2°? How is that even possible that you can want somebody to be accurate down to ±0.1° when the thing is only accurate up to ±2°?
Andrew Bassett: Right, I get that. We can even go a lot further with that and start talking about budgets of uncertainty. If you look at any reputable thermocouple manufacturer or instrument calibration reports that are ISO 17025, they have to list out their measurements of uncertainty, and that gives you only the 98% competence you’re going to be within that accuracy statement.
Yes, I get the whole issue of this .1° readability. There were good intentions were to fix a flaw, and it spiraled. We’ve seen where PLCs and some of these high logic controllers now can show the .1° readability, but they automatically round up at .5°. Are you now violating the other requirements of rounding to E29? Now, I think we’ve closed out the poll in the standard, but you’re right. We were trying to do the right thing. Personally, I don’t think we gave it all that much further thought on that except hey, let’s just make recorders this way and this should be okay.
Doug Glenn: Right. No, that’s good. Let me be clear, and I think most everybody that was involved with the standards are excellent people and they’re trying to do the right thing. There is no dissing on anybody that was doing it. I’m not a furnace guy, right, I’m a publisher — but when I look at it, I’m going: okay, you’re asking somebody to be as accurate as 0.1° on equipment that can only do ±2°. That’s a 4° swing and you’re asking them to be within 0.1°, basically.
Andrew, this has been helpful. It’s been good hearing from you because you’re on the frontline here. You’ve got one foot firmly planted in both camps.
Andrew Bassett: I’m doing my best to stay neutral with it all.
Doug Glenn: Anyhow, I appreciate it, Andrew. You’re a gentleman. Thanks for taking some time with us.
Andrew Bassett: Thanks, Doug. Appreciate it.
About the expert: Andrew Bassett has more than 25 years of experience in the field of calibrations, temperature uniformity surveys, system accuracy testing, as well an expertise in pressure, humidity, and vacuum measurement calibration. Prior to founding Aerospace Testing & Pyrometry, Andrew previously held positions as Vice President of Pyrometry Services and Director of Pyrometry Services for a large commercial heat treater and Vice President and Quality Control Manager for a small family owned business.
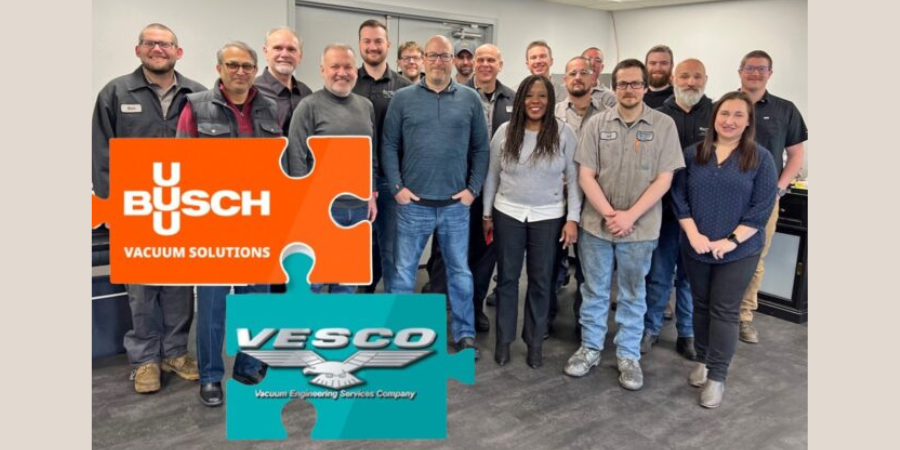
Busch Vacuum Solutions U.S. has acquired the VESCO Division (VESCO-McLaughlin, Inc.) from McLaughlin Furnace Group. The VESCO Division, located in East Windsor, CT, is an industrial service company specializing in heat treating and metallurgy industries and was purchased by McLaughlin Furnace Group in 2017.
Turgay Ozan President of Busch LLC Source: LinkedIn
McLaughlin Furnace Group, the seller of the VESCO Division, continues to serve clients in the aerospace & defense, automotive, energy & environment, metalworking & fabrication, and semiconductor fabrication industries focusing on atmosphere heat treating equipment and best-of-class customer service.
“With this acquisition, we are excited to be able to offer our customers an even more comprehensive range of vacuum services in the heat treat and metallurgy industries,” said Turgay Ozan, president of Busch LLC.
VESCO will be rebranded and will expand its current business operations under the brand name of VESCO – A Company of the Busch Group, while continuing uninterrupted service.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Let’s discover new tricks and old tips on how to best serve air and atmosphere furnace systems. In this series, Heat Treat Today compiles top tips from experts around the industry for optimal furnace maintenance, inspection, combustion, data recording, testing, and more. Part 1, today's tips, examines seals and leak points.
This Technical Tuesday article is compiled from tips in Heat Treat Today's February Air & Atmosphere Furnace Systems print edition. If you have any tips of your own about air and atmosphere furnaces, our editors would be interested in sharing them online at www.heattreattoday.com. Email Bethany Leone at bethany@heattreattoday.com with your own ideas!
1. Tip-Up Furnace Perimeter Insulation Maintenance Is Key to Efficiency & Quality
Contact us with your Reader Feedback!
Due to their construction, the insulation at the perimeter of a tip-up furnace is subject to more abuse than typical furnace insulation. Whether from the repeated stress of cycling the case open and closed — or from high temperature operation — fiber modules will eventually begin to shrink/compact. Be watchful for high case temperatures (or worse: case discoloration and paint damage) as a signal that insulation issues are present in that area.
Heat-damaged case wall Source: Premier Furnace Specialists
An air/atmosphere tight seal is critical for maintaining heating efficiency and process quality. Inspect the seal material around the furnace perimeter often and replace sections that are worn. Common perimeter seals are sand seals, fiberglass tadpole tapes, and insulating fiber blankets. These sealing materials are easy to keep on hand to ensure a quality seal is never delayed by lengthy lead times or supply chain issues.
Seals are everywhere on any furnace. Do you know where all the seals and leak points are? Rope gaskets is an obvious example; high temperature gaskets need to be flat, smooth, and unbroken. Another clear example is in the world of vacuum furnaces: O-rings need to be clean and protected from abrasion. Almost every item of your furnace is sealed in some manner. It is best to replace seals as part of a preventative maintenance program. While your nose can detect ammonia, vacuum leaks require special helium leak detectors and a lot of training. Your furnace manufacturer’s service technician can assist in identifying problem areas and developing a maintenance routine to keep your furnace running. And a simple electronic manometer is great to have handy for running leak-down tests using positive pressures. Auto supply stores sell inexpensive halogen detectors, and some people use smoke bombs to detect leaks.
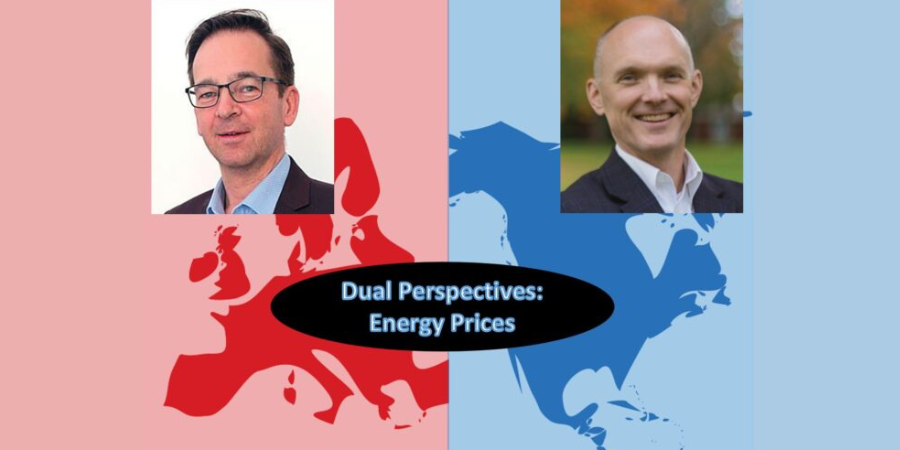
Changes are inevitable, but the world today is shifting oh so rapidly, keeping us on our toes. Two men from different parts of the world, both with significant experience within the heat treating community, reflect on the implications of these changes in the heat treat industry. With each new topic, will their views align?
The experts are Thomas Schneidewind, editor-in-chief of heat processing magazine, and Doug Glenn, publisher and founder of Heat TreatToday. Thomas’s expertise lies in the European market while Doug’s resides in the North American market. We will feature their responses in each print magazine. Will their views align? Time will tell. Enjoy this fifth installment of an ongoing column. This column was first published in Heat TreatToday’s February 2023 Vacuumprint edition.
To what extent have high energy prices affected heat treaters?
Thomas Schneidewind, Editor-in-Chief, heat processing magazine
Thomas Schneidewind Editor-in-Chief heat processing Magazine
In Europe, many companies are in shock. The energy crisis threatens the existence of energy-intensive companies. The hardening industry is coming under pressure as sharp price increases for electricity and gas lead to business losses. This is because the higher prices cannot be passed on to the customers, whose contracts do not allow price increases during the term of a contract. Most hardening shops are small or medium-sized businesses, while their customers are large companies and corporate groups.
Contact us with your Reader Feedback!
Hardening plants must find short-term solutions to cushion the cost shock and ensure the survival of their business. Add this with a view to the long-term goal of decarbonization. Because, in the future, process heat must be carbon free. Whether energy-intensive production is still possible in Europe in the future will be decided by the flexibility and inventiveness of the industry. The task now is to find intelligent answers and to reduce the use of fossil fuels more quickly than planned.
An important step in this direction is the modernization of existing plants – retrofitting can become the efficiency turbo that saves the day in difficult times. Hardening plants should further develop electrically operated equipment and strive for intelligent furnace control. The use of energy saving motors for pumps, circulators, and fans is another option. Insulation on side walls and ceilings in high temperature furnaces and energy recovery from waste heat are among the basic measures.
Modern burner technology also offers the potential to reduce energy consumption. Hydrogen as a heating gas will become an important option in the future. Hydrogen fueled burners have been around for some time but are not currently used in contract hardening shops. Because there are good ideas and positive trials, but no long-term experience and reliable cost comparisons, it will take a little longer until a significant introduction in contract heat treatment takes place. Until then, there are still some problems to be solved, such as safety, availability, investment costs, and especially the price of green hydrogen.
One thing is certain: investments are necessary. OEMs are already making high demands on future carbon-neutral processing and delivery in their contracts, since many automotive manufacturers are striving for a climate-neutral value chain – dictated by regulatory framework conditions. Hardening shops first must survive this difficult phase to then benefit from modernization investments. The aim is to offer customers carbon-neutral heat treatment. Companies can only achieve this by using green technologies. There is no other way.
Doug Glenn, Publisher, Heat Treat Today
Doug Glenn Publisher and Founder Heat TreatToday
In North America, energy is typically one of the top three expenses in nearly all heat treat processes. Commercial heat treaters know this well because it is their business to know the costs associated with their livelihood. Manufacturers with in-house heat treaters, on the other hand, often don’t properly allocate all the true costs associated with their heat treating processes. However, energy costs are fairly easy to allocate, even for them, and it’s safe to say: energy prices are skyrocketing.
The impact of rising energy prices can be measured in the price for each BTU that goes into the heat treat process. Often, 50% to 200% increases have not been unusual in the U.S.
But less obvious costs that are not so easy to measure also impact heat treaters. For example, transportation, which is energy intensive, adds to overall processing costs, especially if not done in-house.
Even LESS obvious is the effect that rising energy costs have on quality, innovation, and standard operating procedures (SOP). When corporate profits plummet due to rising energy costs, all aspects of the business are scrutinized, not just the areas where energy is most intensively used. This oftentimes results in cuts to “non-essential” expenses, which may mean reducing new product or process development initiatives, cutting back on borderline or “unnecessary” quality or safety measures (!), and re-examining SOPs to make further cuts.
The rising cost of energy could even impact the competency of heat treat operators. During COVID, I spoke to a nurse who explained that quality of care was reduced when a large number of nurses left the profession because they chose not to take the vaccines or boosters. Patients receiving emergency medical care did not notice any shortage of personnel, but the fact was that the nurses filling the critical roles were not as proficient or qualified as the expert nurses they replaced. In a similar way, when energy prices skyrocket and cuts must be made, the internal allocation of resources may compromise some aspects of the business that are not as clear to the customer.
When energy prices rise as drastically as they have, companies will examine how they can cut costs and help maintain profits, which is a GOOD and appropriate thing. It will take time for heat treaters to adjust to the recent energy price spike. Adjustments won’t be cost-free. The question is: Which part of the company will pay?
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
The Korea Institute of Materials Science (KIMS), a government-funded research institute under the Ministry of Science and ICT, has invested in a new vacuum furnace from a manufacturer headquartered in North America.
Nikola Dzepina Nitrex Regional Manager – Asia Source: NITREX
KIMS conducts a wide range of technological R&D activities, including process improvements, application development, material enhancement, testing, and evaluation. The new Nitrex vacuum furnace will support domestic companies -- including Hanwha Aerospace, Doosan Enerbility, Sung-il Turbine, and Samjeong Turbine -- in a development project that aims to improve the cycle efficiency of industrial land-based gas turbines.
The furnace is a horizontal type 2-Bar external quench equipped with a curved molybdenum wide band heating element arranged in a circular configuration around the main hot zone. Its work area measures 15″ in width by 15″ in height by 24″ in length (381 x 381 x 610 mm).
“The Nitrex system can support a wider range of R&D projects and metals,” said Nikola Dzepina, regional manager in Asia at Nitrex. “With the ability to achieve higher vacuum levels with 10-6 Torr ultimate range, the furnace can heat treat parts at temperatures up to 1,371°C (2,500°F).”
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Heat Treat Today is partnering with two international publications: heat processing, a Vulkan-Verlag GmbH publication that serves mostly the European and Asian heat treat markets, and Furnaces International, a Quartz Business Media publication that primarily serves the English-speaking globe. Through these partnerships, we are sharing the latest news, tech tips, and cutting-edge articles that will serve our audience — manufacturers with in-house heat treat.
In this installment, we look at updates on industry events around the globe, such as mills, mint, and the Middle East.
Mathevon Group and Bodycote Partner for Oil & Gas Industry Solution
Mud rotors for surface coating Source: Bodycote
“Bodycote has entered into a partnership with Mathevon Group to develop the market in the [Middle East] and, in particular, Saudi Arabia. The agreement brings together Bodycote’s expertise in thermal spray coatings for the oil & gas industry and Mathevon’s knowledge of the production of internal components of gate valves for oil & gas. Mathevon is a world-class provider of safety parts in stainless steel and superalloys, which are subject to severe service applications and has a long history of servicing oil & gas OEM supply chains.”
Shiu Wing Steel to produce recycled steel Source: Furnaces International
“Shiu Wing Steel, Hong Kong’s first and only steel-rolling mill, plans to produce recycled steel to meet growing demand created by China’s green ambitions in Hong Kong and other cities in the Greater Bay Area (GBA) development zone, according to a report by South China Morning Post. The 65-year-old steelmaker plans to build an electric-arc furnace at its plant in Tuen Mun to produce 700kt (kilotons) of recycled steel a year by 2025 and expand its presence in the GBA, Dario Pong, Shiu Wing’s executive director, said in an interview.”
European Mint Chooses Vacuum Furnace To Harden Dies for Coins
Vector furnaces to harden the dies Source: SECO/WARWICK
“This is the eighth mint to choose SECO/WARWICK solutions. The Vector furnaces will be used to harden the dies necessary for the production of coins for both circulation and collector series. Vector vacuum furnaces with 15 Bar high-pressure gas quenching perfectly match the mint’s operating characteristics. Vector enables fast heat treatment while the working space is optimal for the production of dies, coins, medals and orders.”





 Find heat treating products and services when you search on Heat Treat Buyers Guide.com








 Heat Treat