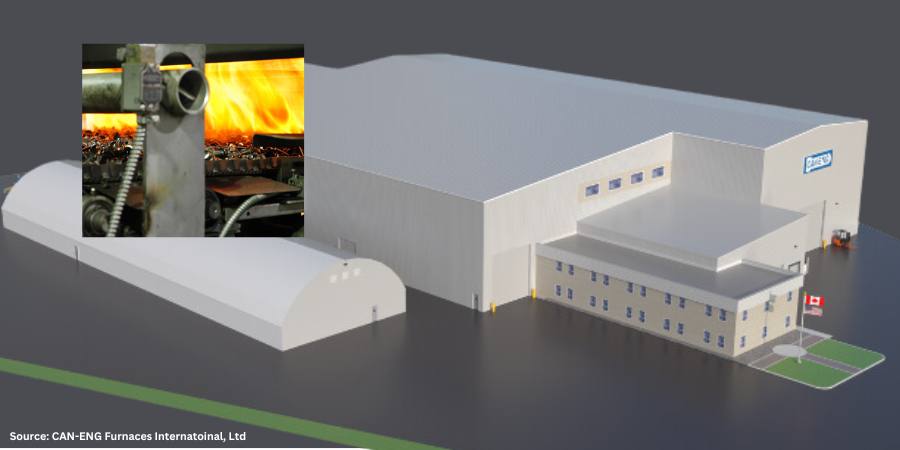
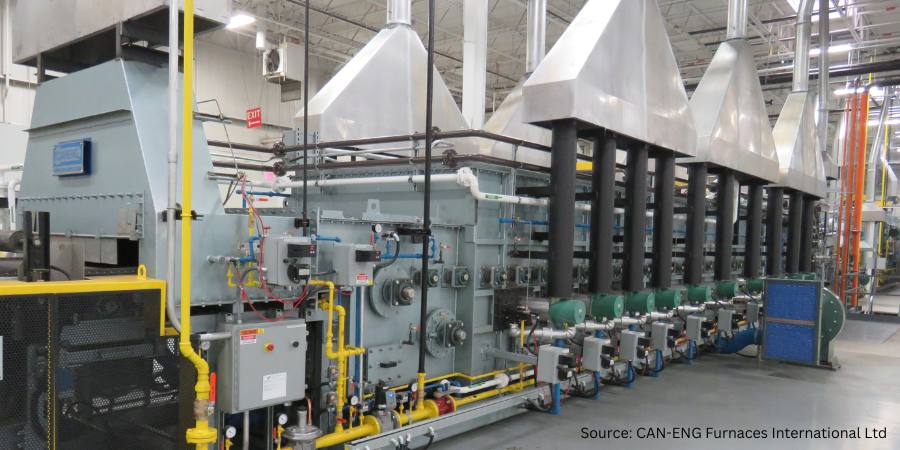
A North American furnace manufacturer recently announced plans to increase production capabilities by expanding its Ontario facility. The investment will consist of adding 45,000 square feet of modern manufacturing space as well as 18,000 square feet of office space. Construction is underway and is expected to be complete May of 2025.
CAN-ENG Furnaces International, Ltd., based in Niagara Falls, Ontario, CA, indicated the capacity expansion will be to their Plant #2 Operations in St. Catharines, Ontario. The manufacturing space will be outfitted with fabrication, assembly, and testing equipment to serve the changing needs of the industries they serve with thermal processing equipment, including stamping and fastener companies, electric vehicle and automotive component producers, the iron and steel industries, aluminum foundries, and agricultural, and construction manufacturers.
This expansion will double the current floor space and integrate enhanced overhead lifting capabilities to accommodate larger thermal processing systems being demanded by EV component and battery material processors. Upgrades include the addition of two 30-ton and two 20-ton overhead cranes to accompany the existing units presently in use. Future expansion plans that include foundation and utility upgrades have been considered during the design process.
The press release is available in its original form here.
IperionX, a U.S. titanium metal and critical materials company, recently delivered its first successful titanium furnace production run at the company’s Titanium Manufacturing Campus, based in Virginia. The furnace was installed in April 2024 with full run rate target capacity of at least 125 metric tons per year anticipated by the end of the year.
Anastasios (Taso) Arima CEO IperionX Source: IperionX
IperionX announced the commissioning of the Hydrogen Assisted Metallothermic Reduction (HAMRTM) furnace, noting that the titanium de-oxygenation production run represents a technological milestone for the company with a breakthrough +60x increase in titanium production capacity. The company’s titanium metal and critical minerals are processed for the consumer electronics, space, aerospace, defense, hydrogen, electric vehicles, and additive manufacturing industries.
“Over the last two years, we have successfully operated our pilot titanium production facility in Utah, producing high performance titanium products for customers and importantly – delivering first revenues for our company,” said Anastasios (Taso) Arima, CEO of IperionX.“Today, we demonstrated that our HAMR technology works at commercial scale. We successfully increased the furnace production capacity by ~60x times and produced high performance titanium that exceeds industry quality standards.”
The HAMR furnace is produced entirely from 100% scrap titanium (Ti-6Al-4V alloy, Grade 5 titanium), with a confirmed reduction in oxygen levels from 3.42% to below 0.07%, far exceeding the ASTM standard requirement of 0.2% for Grade 5 titanium. IperionX’s proprietary HAMR technologies offer a range of competitive advantages, including lower operating temperatures, reduced energy consumption, enhanced process efficiency, and accelerated production cycles.
The press release is available in its original form here.
An East Coast manufacturer has purchased six new vacuum sintering furnaces to replace the 1980s-era sintering furnaces it has used for heat treating components.
SECO/VACUUM received the commission to transition the production line from nine 40-yr-old SECO/WARWICK sintering furnaces to the six Vector sintering vacuum furnaces with 2-bar gas cooling. The furnace hot zones will be 26″ wide, 30″ high, and 62″ deep (660 x 760 x 1575 mm), which are the same size as the retiring furnaces, allowing them to continue using their existing heat treat fixtures.
Sintering is a critical process used to fuse metals together without reaching melting temperature. It is generally used for fixing the strands of wire mesh in place, consolidating powder metals, or any application where the objective is fusing metals together while remaining below melting temperatures.
The press release is available in its original form here.
The advent and increasing adoption of electric vehicles (EVs) has brought a wave of change to the automotive supply chain, including the heat treating industry. While the internal combustion engine (ICE) and all its related components may one day become a thing of the past, there are several key areas of every vehicle that aren’t going anywhere fast. In this Technical Tuesday article, Rob Simons, metallurgical engineering manager at Paulo, discusses the difference between EV and ICE vehicles and the latest heat treating trends to be aware of.
This informative piece was first released in Heat Treat Today’s August 2024 Automotive print edition.
ICE vs. EV Technology
The most apparent difference between EVs and ICE vehicles is that, with EVs, fuel and internal combustion engines are no longer needed. The two vehicle types rely on different sets of key components, and when it comes to making the cars run, EVs use fewer parts that require heat treatment.
Table 1. Existing ICE technology vs. EV technology
Without ICE systems, EVs require fewer fasteners, shafts, gears, and rods — all parts that are typically heat treated. But that doesn’t mean heat treatment is less critical for EVs. In fact, certain parts require additional attention on EVs when compared to ICE vehicles, and many safety-critical parts remain the same across both categories. Let’s begin our discussion with the differences in braking systems between the two technologies and what that means for heat treatment.
Latest Trends in Disc Brake Rotors
How EV Brake Systems Work
There’s no question that electric power innovations have completely revolutionized the way vehicles (and the automotive industry) operate. The regenerative braking system is just one aspect of this. Instead of relying on the conventional hydraulic system every time you press the brakes (which uses friction to decelerate), manufacturers have found a way to use the vehicle’s kinetic energy to put the electric motor into reverse, slowing down the vehicle and returning energy to the battery.
Although regenerative braking is more efficient, hydraulic braking still has one key advantage: stopping power. EVs today are equipped with conventional braking mechanisms for emergency purposes.
The Rust Conundrum
To address recurring rotor corrosion, heat treaters introduced ferritic nitrocarburizing (FNC). FNC is a thermal process traditionally used for case hardening, and for brake rotors, it’s used to achieve corrosion resistance.
The Solution: Corrosion-Resistant Rotors with FNC
To address recurring rotor corrosion, heat treaters introduced ferritic nitrocarburizing (FNC). FNC is a thermal process traditionally used for case hardening, and for brake rotors, it’s used to achieve corrosion resistance.
Figure 1 shows a perfect example of the difference that FNC makes. These are pictures of brake rotors from electric vehicles owned by two Paulo team members — one has brake rotors that were ferritic nitrocarburized and show no signs of rust, whereas the other did not go through the FNC process.
Figure 1a. EV brake rotor without FNC
Source: PauloFigure 1b. EV brake with FNC
Source: Paulo
Ferritic Nitrocarbonizing Process
FNC is a case hardening technique that uses heat, nitrogen, and carbon to toughen up the exterior of a steel part, improving its durability, decreasing the potential for corrosion, and enhancing its appearance. FNC is unique in that it offers case hardening without the need to heat metal parts into a phase change (it’s done between 975–1125°F). Within that temperature range, nitrogen atoms can diffuse into the steel, but the risk of distortion is decreased. Due to their shape and size, carbon atoms cannot diffuse into the part in this low-temperature process. However, carbon is necessary in the FNC process to generate desirable properties in the intermetallic layer.
Heat Treated Materials for Automotive Seating Components
Safety-Critical Components
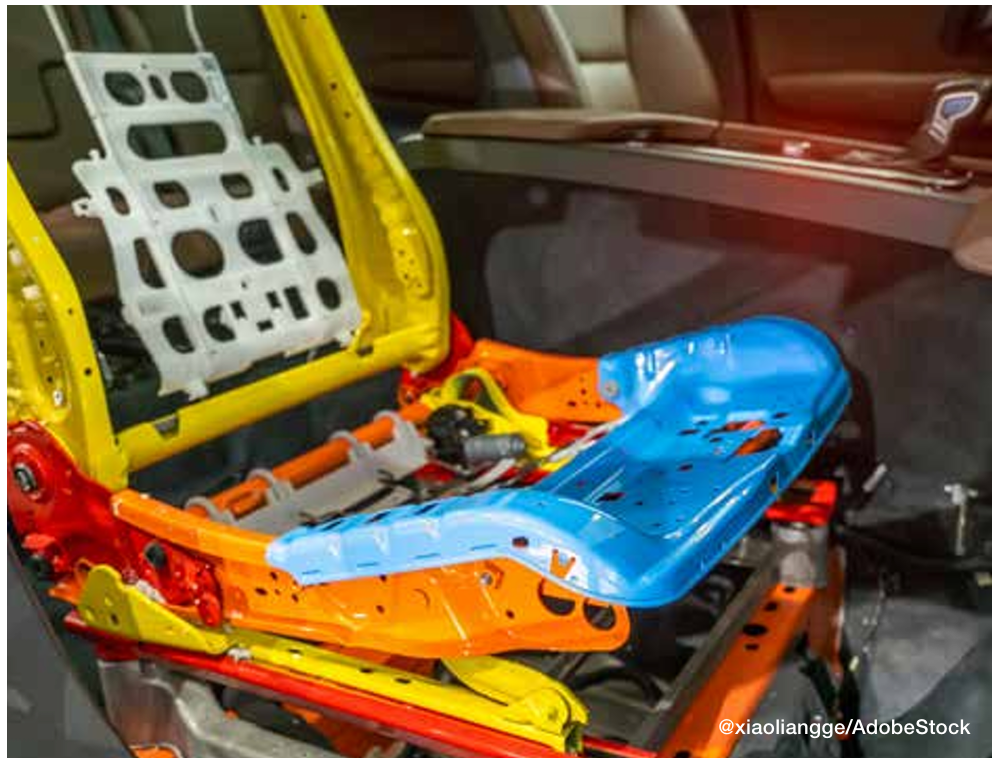
Like brake rotors, many automotive seating components (like mechanisms for seat recliners) are here to stay. Thermal processing is used to achieve stringent specifications that are put in place to keep drivers safe in the event of a collision. EV seat components and the thermal processes used to make them crash-ready are identical to those of ICE vehicle components.
Figure 2. To achieve the stringent specifications for components like seat recliners, identical
thermal processing is implemented for both EVs and ICE vehicles.
Seating Components
Generally, these components are case hardened (either carburized or carbonitrided), typically using one of the following materials:
1010 and 1020 carbon steel: These are plain carbon steel with 0.10% carbon content, fairly good formability, and relatively low strength.
1018 carbon steel: 1018 is a grade that’s often chosen for parts that require greater core hardness and better heat treatment response than 1010 or 1020.
10B21 boron steel: Boron steels are becoming more popular in the automotive industry due to their excellent heat treatment response.
4130 alloy steel and 8620 alloy steel: Alloy steels are more responsive to heat treatment than plain carbon steels, so the thermal processing specifications for parts made from these materials are often adjusted to account for the material’s innate strength properties.
Seat Belt Latches
High-strength seat belt latches are usually made from the following materials:
4140 and 4130 alloy steels: 4140 alloy steel is one of the most common engineering steels used in manufacturing. For seat latches and hooks, 4140 and 4130 will be neutral hardened to increase their strength and hardness throughout due to the high performance and precision required of these parts.
1050 carbon steel: 1050 is a medium carbon steel that contains 0.47–0.55% carbon content. Carbon steels are a less expensive choice when compared to alloy steels such as 4140 or 4130.
Seat Frames and Brackets
Seat frames (also known as seat brackets) give car seats their shape using slender pieces of steel joined together to form the skeleton of the seat. These components are often made from boron steels:
10B21 or 15B24 boron steel: These are a good choice for seat brackets because they are only marginally more expensive than other steels used in seating but have impressive toughness, have a good heat treat response, and are weldable.
A Closer Look: Case Hardening for Seating Components
Case hardening diffuses carbon or carbon and nitrogen into the surface of a metal from the atmosphere within a furnace at high temperatures. Adding carbon or carbon and nitrogen to the surface of steel hardens a metal object’s surface while allowing the metal deeper underneath to remain softer, creating a part that is hard and wear-resistant on the surface while retaining a degree of flexibility with a softer, more ductile core. This softness and ductility create toughness in parts, allowing them to respond to stress without failing. Case hardening is a general term for this heat treating method. Depending on the materials and specifications for the part, we apply various case hardening techniques, including carburizing and carbonitriding.
Figure 3. When it comes to heat treating, innovations are rarely exclusive to EVs.
Carbonitriding
During carbonitriding, parts are heated in a sealed chamber well into the austenitic range — around 1600°F — before nitrogen and carbon are added. Because the part is heated into the austenitic range, a phase change occurs, and carbon and nitrogen atoms can diffuse into the part. Carbonitriding is used to harden surfaces of parts made of relatively inexpensive and easily machined or formed steels, which we often see in automotive metal stampings. This process increases wear resistance, surface hardness, and fatigue strength. It is also good for parts that require retention of hardness at elevated temperatures.
Neutral Hardening
Also called through hardening, neutral hardening is a very old method for hardening steel. It involves heating the metal to a specified temperature and then quenching it, usually in oil, to achieve high hardness/strength. In this process, the primary concern is increasing hardness throughout the part, as opposed to generating specific properties between the surface and the core of the part.
All of the metal components of a seat belt, including seat belt loops, tongues, and buckles, are neutral hardened. Specifications typically dictate that these components are hardened to up to 200 thousand pounds per square inch (ksi).
Because seat belt components are visible to the end consumer, their cosmetics are important in addition to their mechanical properties. It’s important to keep the furnace free of soot and thoroughly clean the parts both before and after heat treatment. Proper cleaning readies the part for secondary processing, ensuring the success of activities like polishing and chrome plating.
The Convergence of EV and ICE Vehicles
To learn more about automotive heat treating, download the free Paulo Heat Treat Guide at paulo.com/AutoGuide.
The EV revolution has significantly transformed automotive manufacturing. Despite these changes, EV parts remain remarkably similar to those of their internal combustion engine (ICE) counterparts. Consequently, any advancements in materials or heat treating processes are swiftly adopted across the entire automotive sector. When it comes to heat treating, innovations are rarely exclusive to EVs.
About the Author:
Rob Simons Metallurgical Engineering Manager Paulo
Rob provides internal and external customer support on process design, material behavior, job development, reduction of variation, and physical analyses at Paulo. He holds a Bachelor of Science in Metallurgical Engineering from the Missouri University of Science & Technology (formerly known as the University of Mines and Metallurgy) and has worked at Paulo since 1987. Rob has analyzed several million hardness data points and/or process behaviors, leading him to develop many process innovations in the metallurgical field.
Heat TreatToday publishes eight print magazines a year, and included in each is a letter from the publisher, Doug Glenn. This letter first appeared in August 2024 Automotive Heat Treat print edition.
In a thought-provoking RealClear Energy(“The Many Problems With Batteries” at RealClearEnergy.org) post on May 30, by Iddo K. Wernick, Ph.D., senior research associate at The Rockefeller University’s Program for the Human Environment and 2013 and 2014 candidate for the Nobel Prize in Literature, Dr. Wernick raises some challenging questions about the belief that battery technology will develop quickly enough, if at all, to achieve net zero by 2050. The complete elimination of combustion, including internal combustion engine (ICE) vehicles, is, in fact, the stated goal of the U.S. Department of Energy — see the Letter from the Publisher in the Heat Treat Today May 2024 Sustainability print issue.
In this issue of Heat Treat Today, we’re talking about heat treatments that are common for the automotive industry, an industry abuzz with talk of EVs and, by necessity, the use of EV batteries. Some of the basic facts and questions raised by Dr. Wernick bear repeating here.
“Batteries provide the essential lynchpin in plans to reduce global carbon dioxide emissions . . . . The dramatic global expansion of in-battery energy storage over the coming decades is deemed necessary to facilitate the growth of wind and solar power and electrified transportation.” In other words, if batteries don’t advance significantly, net zero by 2050 is not going to happen.
Dr. Wernick next points out that “batteries store energy less efficiently than hydrocarbon fuels and release that energy far more slowly than fuels do during combustion.” In fact, the energy density of relatively seldom-used and less efficient “biomass fuels like straw and animal dung is twenty times greater than . . . today’s best lithium-ion batteries, and gasoline has an energy density over 50 times greater.” In other words, with all the technical advances in battery storage over the past decades, batteries are still 50 times less effective and efficient than ICE vehicles.
And while energy densities are substantially lower than carbon-based combustion fuels, a more serious obstacle will be mining (yes, energy-intense, pollution-creating mining) enough minerals to produce these batteries. According to a report issued by the Internation Energy Agency, “supplying the many critical minerals necessary for [the] enormous increases in battery manufacturing” will require “a projected five to 30 times increase in demand for the different battery metals by 2050.” Given the green movement’s propensity to shun any type of mining anywhere, it would appear that battery manufacturers are in the same situation that Moses was in when the Egyptians demanded more bricks but didn’t provide more straw.
China’s dominance in critical battery minerals and battery manufacturing is also mentioned as problematic.
He also covers the inherent bulkiness of batteries: “The inherent bulkiness of battery energy storage quickly shows itself in real world applications. Using current technologies, half of the power produced by the battery pack of an electric vehicle goes to moving the batteries themselves, a basic problem for a mobile power source.” (My emphasis added.)
Some reasonable solutions are offered by Dr. Wernick such as, “incremental changes to the energy system that might reduce emissions more effectively and have greater potential for implementation. Consider the fact that increasing power production from natural gas and nuclear energy could reduce carbon emissions more effectively than building and maintaining the elaborate physical infrastructure necessary for solar and wind and batteries. Or the fact that hybrid electric vehicles require much smaller battery packs, leverage consumer familiarity, and may offer more promise for reducing aggregate vehicular emissions than do fully electric vehicles in the long run.”
Doug Glenn Pubisher Heat Treat Today
Our current world leaders and influencers appear to be somewhat unrealistic and myopic on net zero by 2050. They seem to be ignorant that technologies and materials development are both slow moving and market-driven beasts which cannot be rushed. I don’t know too many people who are opposed to EVs simply because they are electric, but I do know oodles of thinking people who understand that making a quantum leap from ICE vehicles to EVs is something best “driven” (pardon the pun) by the market, and that it takes time.
The Michigan expansion of a furnace manufacturer and heat treating company has advanced with the erection of the entire steel structure in one week. The new 20,000-sq-ft building for Solar Atmospheres of Michigan Inc. will not only house additional vacuum and air furnaces but will also serve as a new shipping and receiving space.
Solar Atmospheres, headquartered in Souderton, PA, relocated equipment to its Michigan facility in April, 2024, where the ten vacuum furnaces are fully operational. The expansion project, which began in July, 2024, will more than double the company’s current footprint in Chesterfield, MI, and is on track for completion by the end of 2024.
The press release is available in its original form here.
Follow the development of this story in the previous Heat TreatToday posts found here, here, and here.
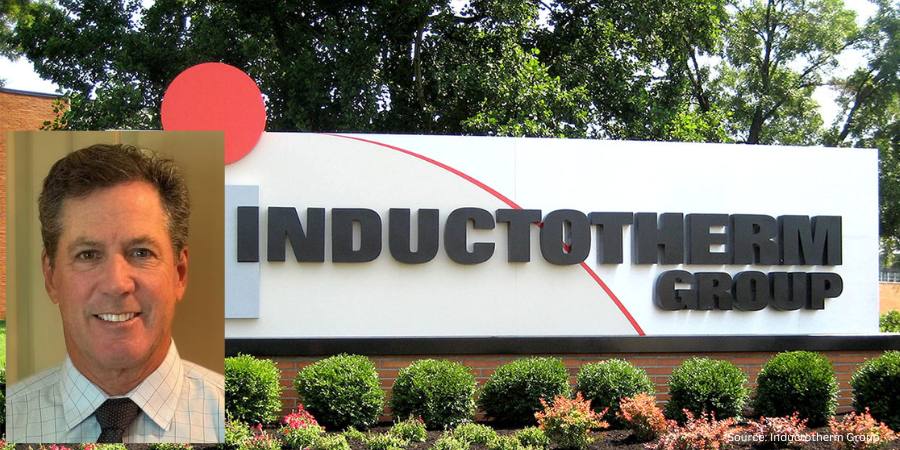
Inductotherm Group, which provides thermal processing technologies, has announced a significant leadership transition as part of a planned succession strategy of the company. After 15 years as CEO and 38 years with the company, Gary Doyon has stepped down from his role as CEO, effective July 1, 2024, coinciding with Mick Nallen and Satyen Prabhu taking over as co‐leaders.
Although he is stepping down as CEO, Mr. Doyon will remain actively involved with the company. He will continue to serve as the only non family member on the parent company Board, assisting with specific operational needs of other businesses owned by the Rowan family and pursuing new business avenues and opportunities for the Inductotherm Group.
Gary Doyon retiring CEO Inductotherm Group
“We greatly appreciate and thank Gary Doyon for his exceptional leadership over the past 15 years,” said Virginia Rowan Smith, chairman of Inductotherm Group. “As we move forward with our succession plans, we are confident that the new leadership will continue to uphold the high standards and legacy that Gary has established.
“We are pleased to announce that Mick Nallen and Satyen Prabhu have been selected to be co‐leaders,” added Ms. Smith. “This management strategy fits perfectly with the fact that our business is large, growing fast, and becoming wider in product technologies around the world. Mick and Satyen have come up with strong business plans that meet our family’s goal of maintaining a stable, customer‐focused, and technology‐centric business. We have an exciting future ahead of us.”
The unique co-leadership arrangement of Mick Nallen and Satyen Prabhu is designed to leverage their complementary strengths and experiences. In their new roles, they will focus on thought leadership, market comprehension, and a deep understanding of the thermal processing industry’s various sectors. with a goal to preserve the core values and vision of the company’s founder, Henry Rowan.
Under Doyon’s tenure as CEO, Inductotherm Group, which offers advanced technology for the engineering, manufacturing and service of thermal processing equipment used in the melting, heating, heat treating, forging, galvanizing, coating, cutting and welding of metals, has diversified its product offerings. In addition, the company has expanded its global footprint, bringing together 40 companies with 38 manufacturing facilities located in 19 countries under the brands Inductotherm, Inductoheat, Thermatool, Radyne, Consarc, and others.
The press release is available in its original form here.
Two different specialty automotive components manufacturers have expanded their heat treating processing lines in order to meet the growing needs of their clients. The new furnace equipment will replace existing systems and bolster oil quench hardening and salt quench austempering capabilities.
CAN-ENG Furnaces International Ltd, based in Niagara Falls, ON, Canada, will supply mesh belt furnace systems, oil quench and salt quench systems, post quench wash systems, CAN-ENG PET™ SCADA system, and integrated controls. The automotive parts manufacturers chose designs that provide low energy consumption, reduced part mixing, reduce part damage and part distortion potential, and high uptime productivity.
The press release is available in its original form here.
In this episode of Heat TreatRadio,Doug Glenn discusses the hardenability of materials with guest Michael Mouilleseaux, general manager at Erie Steel LTD. Michael walks us through how to interpret hardenability charts and provides detailed insights on reading these charts, including addressing the importance of understanding the nuances of complicated part geometry.
Below, you can watch the video, listen to the podcast by clicking on the audio play button, or read an edited transcript.
The following transcript has been edited for your reading enjoyment.
Understanding a Hardenability Chart (01:59)
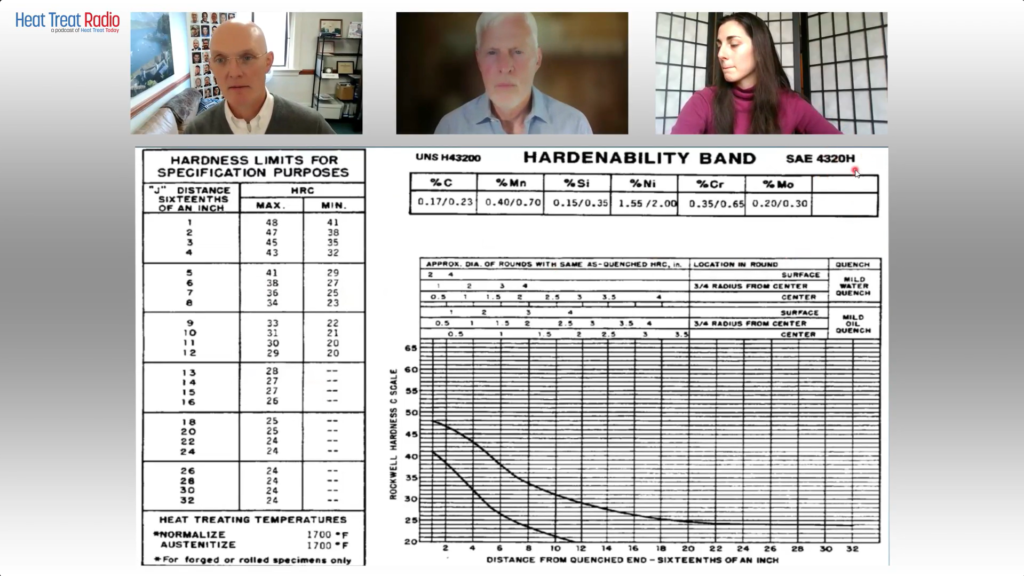
Doug Glenn: What I’d like to do is talk through this chart and learn how to read this a little bit better. And I’d like to ask questions about it because I’m not familiar with this, and I’m sure there are going to be some listeners and viewers who aren’t familiar with it. This will be just a quick tutorial on how to read these charts.
Go to the upper, right-hand corner. First off, SAE 4320H is the grade of the steel that we’re talking about?
The Heat Treat Lunch & Learn crew: Doug Glenn, Publisher of Heat Treat Today; Michael Mouilleseaux, General Manager at Erie Steel LTD.; Bethany Leone, Managing Editor of Heat Treat Today Use this chart to follow along with the conversation. Source of chart: Erie Steel, Ltd.
Michael Mouilleseaux: Correct.
Doug Glenn: Then the table right below that you’ve got percentage C (carbon). Is Mn manganese?
Michael Mouilleseaux: Manganese.
Doug Glenn: Thank you very much. Silicon, nickel, chrome, moly. My question is about those ranges. Is this basically saying the percentage carbon on the far left in 4320H goes anywhere from 0.17–0.23?
Michael Mouilleseaux: That is correct.
Doug Glenn: Okay. So that’s variability right there. All of those are basically telling you what the ranges are in those alloys in this grade of steel?
Michael Mouilleseaux: That is correct.
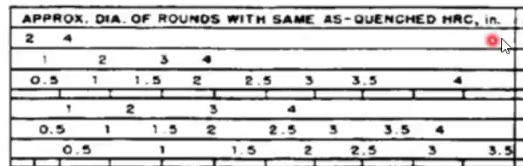
Doug Glenn: Then you go down to the top columns of this table below, and it says “Approximate diameter of rounds with same as quenched HRC in inches.” Right?
Approximate diameter of rounds with same as quenched HRC in inches Source: Erie Steel, Ltd.
Michael Mouilleseaux: Yeah. Essentially, the first three rows are for water quenching. And the bottom three are for oil quenching.
Doug Glenn: If you go over to the second major column called “Location in round,” what’s the size of the round we’re working on here?
Michael Mouilleseaux: It can vary. Go down to where it says, “Mild Oil Quench,” then left to “Surface,” then left then go to “2 inches.” Then, go straight down to the bottom, and that’s approximately J5. So, the “Distance from Quenched End — Sixteenths of an Inch” is Jominy position 5.
Michael Mouilleseaux: If you go to Jominy position 5 on the left-hand chart, you can see the hardness limits for that; the maximum is Rockwell C 41, and the minimum is Rockwell C 29. So, the chemistry can vary provided the hardenability at J5 is 29–41.
Doug Glenn: That’s the acceptable range?
Michael Mouilleseaux: That’s the acceptable range. That’s one way of looking at it. The chemistry would allow you to do that.
Now, go back to the chart on the right-hand side and to “Surface,” move down one row to “¾ radius from center,” and go left to two inches. Moving down from there you see that is Jominy position 8. So, the surface of a two-inch round is Jominy position 5, and the ¾ radius is Jominy position 8.
If you go to the hardness chart on the left-hand side, that says that if you had a two-inch round of 4320H, and it was oil quenched, and you check the hardness at ¾ radius, then the expectation is that it would be 23–34.
Now, go back to the same chart that we were just at, and go to the “Center” row of “Mild oil quench.” Continue left to two inches, and that’s J12. Go back to the left-hand chart, and J12 is 20–29 in the center of the part.
So, the surface of the part could be 41, ¾ radius, center of the part would be 34, and the center of the part would be 29.And that would all meet the criteria.
Doug Glenn: The maximum for J5 would be 41.But at J12 you could get a 20 in the middle.
Michael Mouilleseaux: Right. That is one way to look at this chart. But there is another way.
Notice that it says “rounds.”There are some nuances to having flats and rectangles because, if you think about it, for the cross-sectional area of a rectangle, the hardenability is going to be determined by the direction that it is thinnest, not by the direction that it is thickest.
Take a gear tooth, for example: in the chart that we just made up the gear teeth, the root of the gear was about a half inch, just slightly more; and if we go to this same chart, go to “Center” of “Mild oil quench,” and then go to a “0.5 inch,” and when you go straight down, that’s the J3.
Is a gear necessarily a round? Of course, the answer to that is no. So, in complex shapes you can use this data, but you have to interpolate it in order to understand it.
To some extent, the first time you run this, you’re going to say, “I have a gear, and the root is a half inch across. And I know that the J3 is 40. And I’ll run this part, and I’ll section it and I’ll measure it and it’s 40. And I’ll say that’s a good approximation of that.” And experientially, you build confidence in this, that is, it’s your operation, your quenching operation, and your components. It allows you to interpolate these, and they become extremely useful.
So, is it definitive? No. Is it useful? Yes.
Doug Glenn: It gives you a ballpark, right? I mean, it’s giving you something, maybe guardrails.
Michael Mouilleseaux: It gives you a ballpark; it gives you guardrails. And I can tell you that after having run gear product in the same equipment for ten years, I can say that it’s definitive. I can say that if I have this hardenability, and I get this hardenability number for this heat, and these gears are made from this heat of steel, and it has a J3 of 42. If I’m at 38, I know something is going on other than just hardenability. And, at that point, I would suspect my heat treat operation.
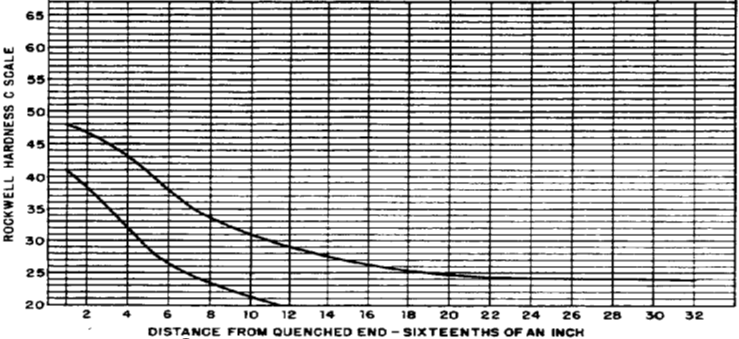
Doug Glenn: Yeah. I have one more question about this chart: On the bottom right part of the graph there are two plot lines on there. What do those represent? I was thinking one represented the water quench and the bottom one represents the oil quench.
Plot lines representing maximum hardenability and minimum hardenability Source: Erie Steel, Ltd.
Michael Mouilleseaux: The top one represents the maximum hardenability. And the lower the lower one represents the minimum hardenability.
Doug Glenn: That’s your band. Okay. Those are basically your values over on the left-hand side then. Very good.
I don’t know about you, but I found that helpful. I really didn’t ever know how to read these tables. So, maybe someone else will find that useful. Thanks, Michael. I appreciate your expertise.
Michael Mouilleseaux: It’s been my pleasure.
About The Guest
Michael Mouilleseaux General Manager at Erie Steel, Ltd. Sourced from the author
Michael Mouilleseaux is general manager at Erie Steel LTD. Mike has been at Erie Steel in Toledo, OH, since 2006 with previous metallurgical experience at New Process Gear in Syracuse, NY, and as the Director of Technology in Marketing at FPM Heat Treating LLC in Elk Grove, IL. Having graduated from the University of Michigan with a degree in Metallurgical Engineering, Mike has proved his expertise in the field of heat treat, co-presenting at the 2019 Heat Treat show and currently serving on the Board of Trustees at the Metal Treating Institute.
The SECO/WARWICK Group, the parent company of SECO/VACUUM Technologiesand SECO/WARWICK USA, has announced plans to bolster its production capacity in the U.S., increasing its footprint and workforce. The expansion will include relocating a portion of its manufacturing and a metallurgical lab for vacuum furnaces from its headquarters site in Poland to Crawford County, Pennsylvania.
The 120,000-sq ft facility located in Meadville, PA, will house equipment for furnace production and serve the company’s North American customers through the addition of parts, service, and training capacity, resulting in an increase in its heat treat manufacturing workforce. an international furnace manufacturer
SECO/WARWICK Group announced that this expansion received support from the Commonwealth of Pennsylvania through a $2 million package of matching fund grants from the Department of Community and Economic Development (DCED) through its Redevelopment Assistance Capital Program (RACP). The primary use and intent of RACP funds is for reimbursement of eligible construction costs which SECO/WARWICK Group companies will match on a 1:1 basis. The Commonwealth will also provide an additional $69 thousand in matching funds for job training through the Workforce & Economic Development Network (WEDnet).
Employees of SECO/VACUUM Technologies and SECO/WARWICK at the announcement of the Meadville, PA, site expansion, held jointly by The SECO/WARWICK Group and the Commonwealth of PA Department of Community and Economic Development Source: Heat Treat Today
State, county and local officials as well as representatives from the international and US-based offices of the SECO/WARWICK Group were present at an event marking the expansion.
“Governor Shapiro is committed to making Pennsylvania an economic leader by investing in the growth of businesses like SECO/VACUUM and SECO/WARWICK,” stated the Commonwealth in the grant award letter. “In addition to the financing package outlined above, the Governor’s Action Team is prepared to provide both companies with any assistance that may be required throughout the application process, as well as to coordinate the involvement of all other state agencies in the project.”
“We look forward to working with our local partners including the City of Meadville, the Economic Progress Alliance of Crawford County (EPACC), the Workforce and Economic Development Network (WEDnet), and the Pennsylvania Department of Community and Economic Development (DCED) to make this expansion happen!” said Piotr Zawistowski, president and managing director of SECO/VACUUM.
Pictured in feature image (L to R): Don Marteeny, vice president of engineering; Slawomir Wozniak, president and CEO, SECO/WARWICK Group; Piotr Zawistowski, president and managing director of SECO VACUUM Technologies
The press release is available in its original form here.