Hiperbaric, the Spanish manufacturer of high-pressure technology, will present its range of hot isostatic presses (HIP) at Formnext as the solution to densify critical components and eliminate porosity in 3D-printed parts.
As the global additive manufacturing (AM) ecosystem gathers for its annual event, Hiperbaric’s presence underscores a commitment to providing technology that maximizes the performance of 3D-printed metal and ceramic parts. HIP technology is key to improving the mechanical properties and structural integrity of critical components.
HIP 38 press for thermal post processing of materials Source: Hiperbaric
“For an industry seeking nanometric perfection, eliminating internal porosity is not an option, it is a necessity,” says Andrés Hernando, CEO of Hiperbaric. “HIP is the technological enabler that dramatically improves the mechanical properties and structural integrity of critical components, making AM viable for mass production in the most demanding sectors.”
Hiperbaric’s technology directly addresses the primary challenge of metal AM. Processes such as Selective Laser Melting (SLM) or Electron Beam Melting (EBM) create parts layer-by-layer, a method that can inherently leave residual micro-porosity. While this may be irrelevant for a prototype, for a turbine blade, a medical implant, or a high-performance racing engine part, this porosity represents a potential failure point.
HIP is the post-processing step that elevates an AM part to the quality of a forged material. It transforms a porous or micro-cracked material into a solid, monolithic, and homogeneous structure, guaranteeing it meets the strictest mechanical specifications.
How Hot Isostatic Pressing Works
HIP is an advanced manufacturing and heat treatment process that subjects components to two simultaneous forces: high temperature and high isostatic pressure. The component is placed inside a high-pressure vessel. This chamber is heated to temperatures that can reach 2,000°C (3,632°F) and is simultaneously pressurized with an inert gas (usually argon) to pressures of up to 2,000 bar (29,000 psi).
Hiperbaric’s innovation and experience in high-pressure processing has enabled the manufacture of modern HIP equipment, improving performance and reducing costs. Its wire wound vessel technology not only has advantages from a safety and reliability point of view, such as increased service life or the “leak-before-break” design that prevents catastrophic failures, but also provides advantages from a thermodynamic point of view.
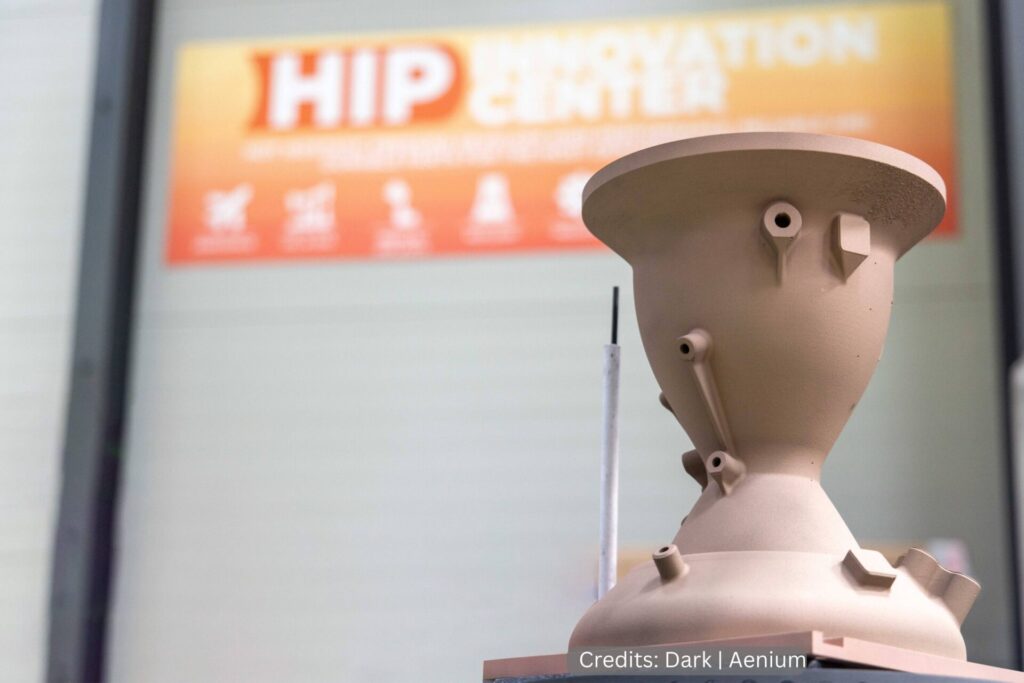
Rocket engine treated by HIP technology
Being a wire wound vessel, the cooling channels can be placed very close to the vessel wall and therefore very close to the hot zone, allowing the vessel to act as a heat exchanger, enabling fast cooling inside the equipment. Through a fan and valves located in the lower part of the oven, forced convection is activated by circulating the hot gas through a heat exchanger located in the upper cap, which exits and descends in contact with the wall of the vessel (which is cooled) and re-enters the oven.
The ability to fast cool within HIP equipment, in addition to the increased productivity, reducing production times and energy consumption – which translates into savings – has a series of advantages from a material science perspective, improving the microstructure and physical properties. Thanks to fast cooling, it is also possible to carry out heat treatments within the same equipment, opening the door to combined cycles (Combined HIP – Heat Treatment, CHIP-HT).
The effect is two fold:
Porosity Elimination: The combination of heat and pressure applied uniformly from all directions (“isostatic”) causes internal pores and microscopic voids to collapse and diffusion-bond.
Full Densification: The result is a component that achieves 100% theoretical density. This process drastically improves ductility, fatigue strength, impact resistance, and fracture toughness.
Hiperbaric has developed a cutting-edge range of HIP presses specifically designed to meet the exacting needs of the aerospace, energy, medical, and metallurgy industries.
A Technological Milestone: HIP Reaches Taiwan
Hiperbaric recently marked an industrial milestone by supplying the first 100% Spanish-developed HIP system to Taiwan. This equipment is Hiperbaric 93 HIP, destined for Taiwan’s highly demanding aerospace industry, serves as a crucial validation.
Heat Treat Today has gathered the four heat treat industry-specific economic indicators for November 2025. The November industry-specific economic indicators reinforce the overall trend toward growth that began in September of 2025.
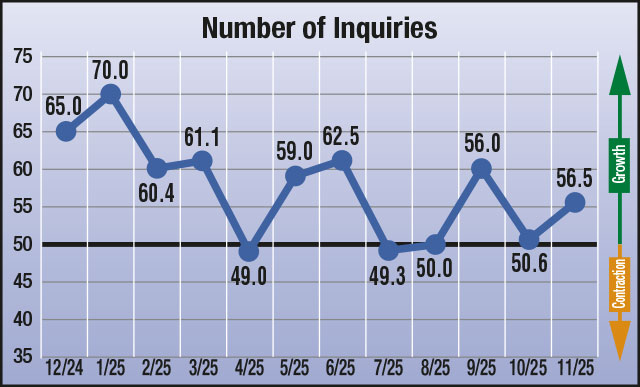
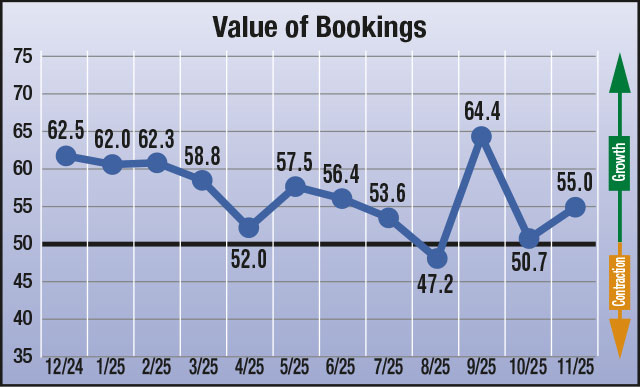
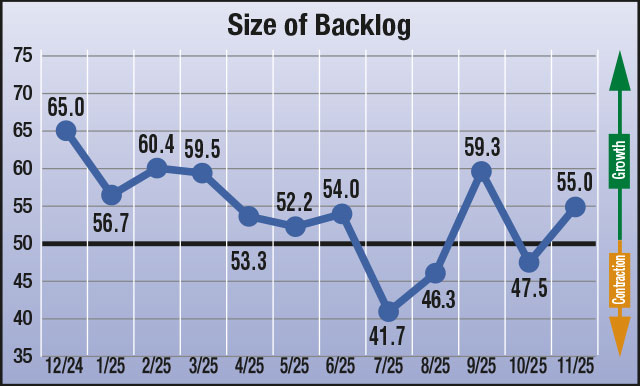
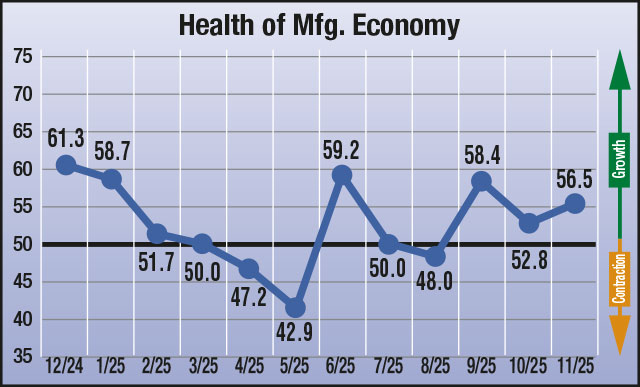
November’s industry-specific economic indicators showed all four indices in growth. The Inquiries stayed in growth, rising to 56.5 (from 50.6 in October). Bookings rose to 55.0 (from 50.7 in October). The Backlog index rose out of contraction to 55.0 (up from 47.5 in October). Finally, the Health of the Manufacturing Economy index remained in growth at 56.5 (up from 52.8 in October).
All of the graphs suggest that the undercurrent of growth, which began in late summer, is continuing to rise as we look to the end of the year.
The results from this month’s survey (November) are as follows: numbers above 50 indicate growth, numbers below 50 indicate contraction, and the number 50 indicates no change:
Anticipated change in Number of Inquiries from October to November:56.5
Anticipated change in Value of Bookings from October to November: 55.0
Anticipated change in Size of Backlog from October to November: 55.0
Anticipated change in Health of the Manufacturing Economy from October to November: 56.5
Data for November 2025
The four index numbers are reported monthly by Heat Treat Today and made available on the website.
Heat TreatToday’sEconomic Indicatorsmeasure and report on four heat treat industry indices. Each month, approximately 800 individuals who classify themselves as suppliers to the North American heat treat industry receive the survey. Above are the results. Data started being collected in June 2023. If you would like to participate in the monthly survey, please click here to subscribe.
Custom furnace design isn’t just about performance upgrades — it’s about process reliability. Vacuum furnaces built for general use, however, often fall short in high-precision industries. This Technical Tuesday installment comes to us from Scott Herzing, vice president of Engineering at Paulo. Explore how purposeful furnace design, smarter controls, and targeted customization can transform vacuum heat treatment.
This informative piece was first released inHeat Treat Today’sNovember 2025 Annual Vacuum Heat Treating print edition.
The reliability and consistency of vacuum heat treatment processes depend heavily on furnace design and performance. Standard furnace configurations typically serve general heat treating applications adequately. However, for industries with extremely demanding requirements, such as aerospace, automotive, and power generation, small variations in furnace design can lead to substantial impacts on part quality, increasing risks and costs. Achieving exceptional process control and repeatability often requires custom furnace modifications tailored specifically to the unique requirements of each process.
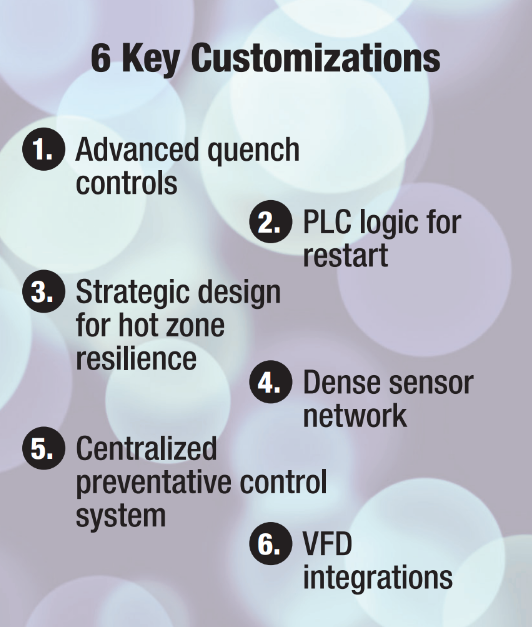
Extensive customization of vacuum furnaces can initially seem costly and complex. It takes experience operating and refining vacuum furnaces to know which adjustments deliver the greatest impact. This article taps into the more than fifty years of heat treating wisdom from Paulo with six key factors that drive better furnace performance, enhance reliability, reduce downtime, and create measurable efficiency gains.
Why Customization Matters
Conventional vacuum furnace models offered by manufacturers are generally designed to meet broad market demands. This often results in equipment that effectively balances functionality, affordability, and ease of use for a wide range of applications. However, certain high-precision thermal processing applications, especially those involving aerospace components like single-crystal turbine blades demand much stricter temperature uniformity, controlled quenching rates, and near-perfect repeatability from cycle to cycle.
In these cases, standard configurations can introduce variability that compromises quality. A better path is a case-by-case approach, evaluating specific process risks and targets critical components for modification. Precision upgrades can be integrated where they have the greatest impact, achieving the required level of process control. This makes it possible to achieve near-zero scrap rates, dramatically boost reliability, and achieve repeatability that far exceeds industry norms.
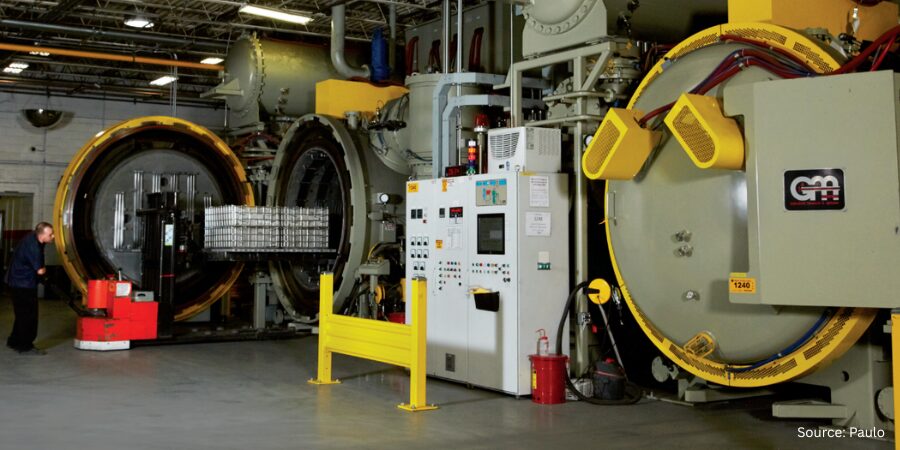
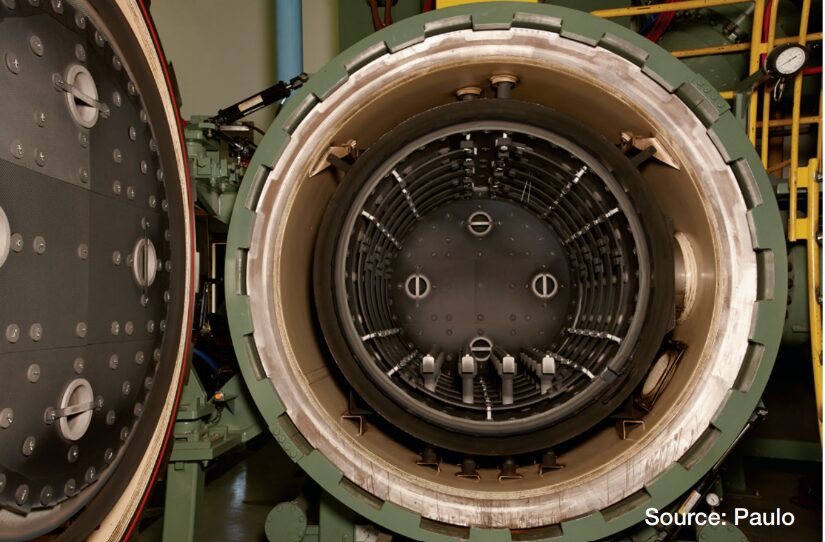
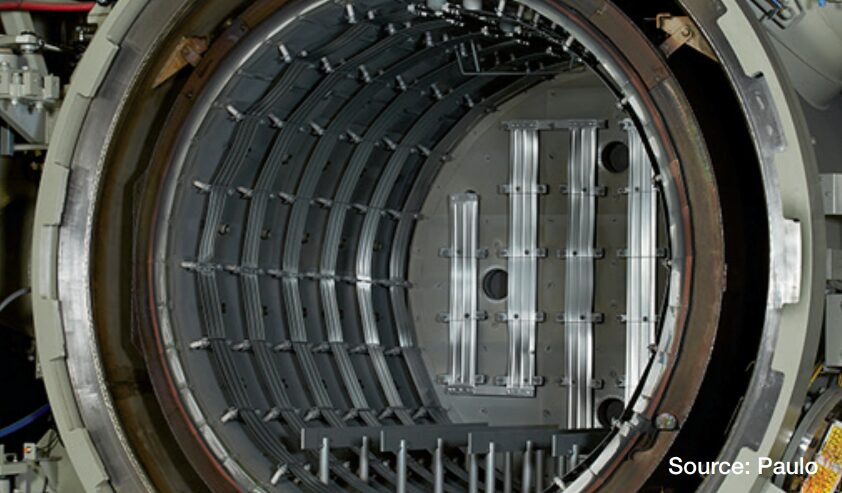
Interior of vacuum furnace
Advanced Pressure and Cooling Control
Repeatable quench dynamics is a game-changer when it comes to part quality. Integrating advanced gas control capabilities that extend beyond basic pressure management can help you improve heat treating results. To do this, you need to precisely control the rate at which gas is introduced into the vessel using proportioning valves, not just the pressure setpoint. For controlled cooling cycles, systems also need to manage the fan start speed, allowing you to tailor the convective heat transfer to the geometry and mass of each part. This level of precision ensures consistent metallurgical results and protects part integrity.
Automation-Ready Resilience
In multi-furnace environments that rely on automation and minimal staffing, power-failure restart behavior cannot be left to chance. Adding dedicated PLC logic for restart allows the system to record the exact state at interruption, verify safe conditions on recovery (atmosphere, temperature, motion, interlocks), and automatically sequence a safe restart when criteria are met. This reduces scrap risk, protects equipment, and stabilizes throughput, especially when only a few operators are covering many furnaces.
Hot Zone Design and Material Selection
A major component directly influencing furnace reliability and overall performance is the hot zone. As the central area where thermal processing occurs, the hot zone repeatedly experiences extreme temperature fluctuations, making its design crucial to operational efficiency and product quality.
Standard vacuum furnaces use thinner insulation layers and lower-cost materials to control initial investment costs. However, advanced hot zones can dramatically outperform these standards by incorporating thicker insulation layers, strategically placed air gaps, and specialized insulation materials, such as high-quality molybdenum, graphite felt, or carbon-fiber-carbon (CFC) boards.
Vacuum furnace hot zone
These advanced materials not only prolong hot zone life but also substantially reduce heat loss, minimizing energy consumption and improving thermal uniformity. The enhanced durability also results in fewer service interruptions, less downtime, and lower long-term maintenance costs, ultimately justifying the higher initial investment. At Paulo, this is how we’re able to reliably run around 29,000 cycles per year in over thirty furnaces at our Cleveland facility.
Additionally, the hot zone’s construction details, including how insulation and heating elements are attached, can significantly affect longevity and reliability. Standard fasteners or attachment mechanisms may perform well in general applications but frequently deteriorate under high-stress thermal cycling. High-performance fasteners specifically engineered for high-temperature stability reduce the risk of premature failure and minimize downtime.
Enhanced Sensor Integration
Furnace reliability and consistency rely heavily on the accuracy, quantity, and strategic placement of sensors within the furnace chamber. Manufacturers’ vacuum furnace designs typically include a limited number of sensors monitoring basic parameters, such as temperature, pressure, and vacuum levels. Increasing the number and distribution of sensors throughout the furnace interior allows for a more detailed and accurate understanding of conditions during processing. By placing multiple sensors at critical points within the hot zone and throughout key furnace components, operators can detect subtle differences in temperature distribution, heat flow, gas pressures, and quench rates that might otherwise go unnoticed. This enhanced sensor density provides the detailed data necessary for real-time process adjustments, early detection of equipment issues, and predictive maintenance interventions, significantly improving process reliability and part consistency.
In addition, the rich data captured by a denser sensor network improves traceability and enables rapid identification of root causes when process deviations occur, ultimately reducing the risk of quality issues and equipment downtime.
Centralizing Your Control System
One often-overlooked factor in achieving highly consistent heat treating results is the adaptability and responsiveness of furnace control systems. Modern furnace control architectures benefit from a centralized SCADA layer with deep PLC integration. By recording every PLC input (thermocouples, switches, interlocks, drives, flows, pressures), the system enables technicians to diagnose issues without walking out to the furnace and manually testing components. With complete signal histories available, furnace issues can often be diagnosed and resolved remotely in minutes, improving first-pass resolution and minimizing production disruption.
Integrated control software should do more than log data; it should actively protect quality:
Automated compliance control: Continuously track process parameters, alarm on deviations, and initiate quality quarantines when limits are exceeded to prevent suspect parts from re-entering the supply chain.
Element-health monitoring: Monitor heating-element resistance to detect early signs of a heating system issue. If an anomaly is detected, automatically stop the heating process to protect parts and prevent secondary furnace damage.
These safeguards shift intervention upstream and reduce reliance on manual inspection alone.
Extending Auxiliary Equipment Life with VFDs
Variable-frequency drives (VFDs) on pumping systems can substantially extend motor and bearing life by matching speed to process demand and reducing mechanical stress. When control logic conditions are met, slowing pumps lowers load, heat, and vibration, which are key contributors to premature failures.
Without VFDs: Bearings on 615 blowers typically require replacement every 1–2 years, and motor failures occur more frequently than acceptable.
With VFDs + logic-based speed reduction: Bearing-change intervals extend to 10–20 years, with no motor problems, reflecting a step-change in reliability and lifecycle cost.
This targeted upgrade is a practical, high-ROI improvement that also helps decrease unplanned downtime.
Practical Realities and Final Considerations
Extensive furnace customization offers clear advantages, but it is not always practical for every operation or budget. In many cases, targeted, incremental upgrades — such as refining hot-zone insulation and attachment methods, adding or repositioning select sensors, or phasing in improved control software and deeper data storage/analysis — deliver measurable gains in reliability and process quality without large upfront costs.
Another practical path is to partner with a commercial heat treater that has already engineered and validated these enhancements at an industrial scale. This option can accelerate access to higher levels of precision and repeatability without requiring capital investment, engineering bandwidth, and learning curve of doing it all in-house.
Ultimately, achieving reliable and repeatable heat treatment results involves careful consideration of furnace design and functionality, aligned closely with your process requirements and economic realities. While extensively customized furnaces represent the ideal for particularly demanding applications, understanding the targeted areas where smaller customizations can yield significant improvements empowers heat treaters across the industry.
About The Author:
Scott Herzing Vice President of Engineering Paulo
Scott Herzing is vice president of Engineering at Paulo. He leads the company’s metallurgical, project and automation engineering, fabrication, and lean technology groups. With over 27 years at Paulo, Scott applies his passion for leadership, engineering, and problem-solving to help customers achieve advanced heat treating outcomes.
For more information: Contact Scott Herzing at sherzing@paulo.com.
Alleima, a manufacturer of steel components and special alloys, will receive a new tube annealing furnace. The electric atmospheric furnace line is intended for bright annealing of high-alloy tubes and will be used in the production of nuclear applications components.
SECO/WARWICK is providing the furnace as their 5,000th device.
The tube annealing system Source: SECO/WARWICKPiotr Skarbiński Vice President of Aluminum and CAB Products Segment SECO/WARWICKMagnus Mellberg Production Unit Manager Alleima Source: LinkedIn
“Our partnership with SECO/WARWICK has lasted for many years. We are delighted that we could celebrate it in a special way, as our impressively large tube annealing line (over 140 meters long – 460 ft) happens to be the 5,000th SECO/WARWICK device. We feel that together we are creating not only a remarkable history, but also the future as this solution will help us spread our wings,” said Magnus Mellberg, production unit manager at Alleima.
“The furnace was created specifically for this partner’s needs. It will allow them to increase production capacity…This is important as the demand for high-alloy components in this market has increased. It is an unusual construction, verified through analysis and simulations, and implemented in reality. It offers very good technological results after the annealing process,” explained Piotr Skarbiński, vice president of the Aluminum and CAB Business Segments at the SECO/WARWICK Group.
Press release is available in its original form here.
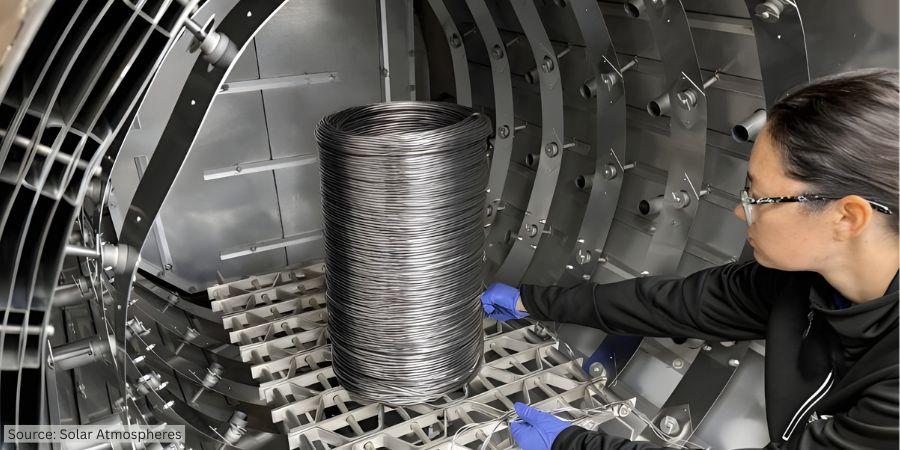
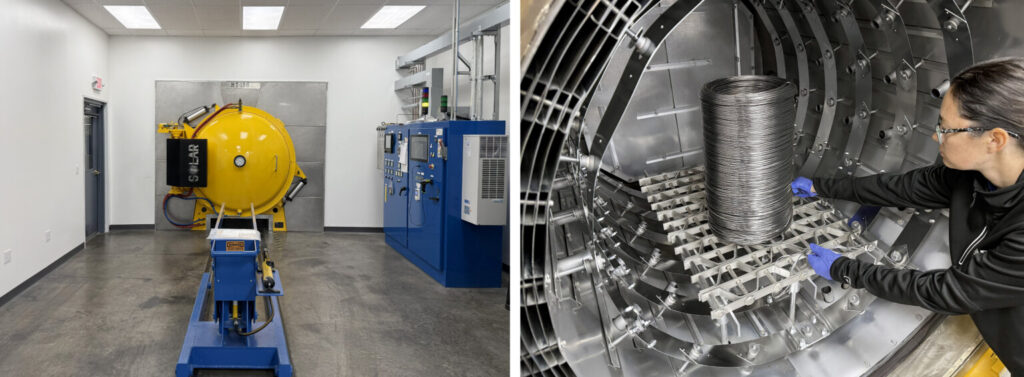
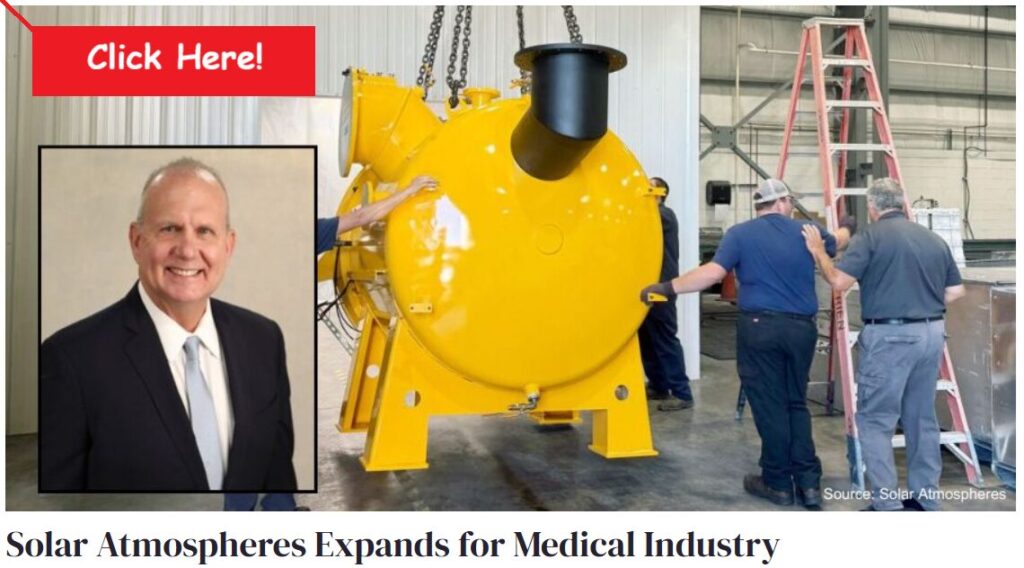
Solar Atmospheres has expanded its operations with an additional all-metal hot zone furnace. The new system significantly expands the company’s capacity to heat treat highly sensitive materials such as precipitation-hardened stainless steels, nickel-chrome-based superalloys, titanium, and niobium. The new unit is installed at their Hermitage, Pennsylvania facility and will meet the stringent demands of the aerospace and medical industries.
Additional all metal hot zone furnace for Solar Atmospheres Source: Solar Atmospheres
Michael Johnson, Sales Director at Solar Atmospheres of Western Pennsylvania, stated: “The all-metal vacuum furnace plays a critical role in delivering the purest possible processing environment. This level of cleanliness and control results in pristine end products that meet the most demanding industry standards. We’re proud to partner with the engineers at Solar Manufacturing to bring this advanced technology to fruition.”
The furnace incorporates strategically placed isolation valves, an oversized main valve, a high-capacity diffusion pump, and a polished stainless-steel chamber. Capable of achieving vacuum levels below 5 x 10⁻⁶ Torr, the system ensures bright, contamination-free results.
Press release is available in its original form here.
Heat Treat Today publishes twelve print magazines annually and included in each is a letter from the publisher, Doug Glenn. This letter is from theOctober 2025 Ferrous & Nonferrous Heat Treatments/Mill Processing print edition.
Karen Gantzer, associate publisher, and I recently visited a manufacturing plant with an extensive, in-house heat treat operation. We don’t often visit captive heat treat operations even though the vast majority of our audience are, in fact, captive heat treaters — manufacturers with their own in-house heat treat capabilities.
The conversation we had with the two heat treat specialists that hosted us was wide-ranging and enlightening. One of the topics was the rationale used for purchasing new thermal processing equipment. They have two mesh belt furnaces and a small number of integral quench furnaces. All the furnaces came from the same supplier.
We asked them straight up, “Why did you buy from this supplier and not from others?” The answer was instructive not only for furnace manufacturers, but for all suppliers in the industry.
What Didn’t Matter
While the three points listed below had some influence, these were not as important to the captive as many furnace manufacturers believe:
Price. In fact, they outright told us that they did not buy the least expensive equipment. When company purchasing agents get involved, the decision-making process is complicated, but with this mid-sized company, the two key decision makers — the two guys who spent time with us — assured us that price was not the main driver behind their decision.
Equipment and controls features. Features were not unimportant, but they were not the driving factor. Each company that bid for the job had slightly different solutions making it difficult to compare features. Our hosts told us that several of the designs would have worked. They chose one, but it was not because they preferred that design over the others.
Quality. What exactly does “quality” mean? If ever there was an overused marketing word, “quality” is it! Quality was not a determining factor in the purchase of the heat treating equipment. All of the equipment was “quality” equipment… whatever that means.
What Mattered
There were two key factors that swayed the decision for this captive heat treater:
1. Responsiveness was the #1 reason why this captive heat treater chose this furnace manufacturer. Responsiveness took several forms. First, during the bidding process, the manufacturer set itself apart by being prompt and creative with design changes. They obviously listened to what the captive heat treater was saying and responded in a timely fashion with alterations/solutions that demonstrated understanding. Second, the ability to reach the “top guy” at the furnace manufacturer day or night brought a level of comfort that heavily tilted the scales in their favor. Both guys indicated that they had the president’s cell number in their phones — not on speed dial, because that’s not necessary — but in their phones just in case. And they’ve used that number multiple times with good results. Finally, the furnace manufacturer continues to be responsive even after the equipment has been installed and commissioned. If there is something new or different the guys want to do, they call the furnace manufacturer, speak to a real person, they are heard, and they get a response in a timely fashion.
2. Location was the second most important reason. Here’s why. First, the buyers were happy to be stimulating the U.S. economy and, more specifically, the regional economy. Second, they felt that a geographically close furnace manufacturer would be more capable of providing speedy service and parts if and when those items became necessary. Third, proximity allowed the buyer to inexpensively visit the furnace builder for manufacturing progress updates. And finally, a domestic manufacturer eliminated tariff concerns.
Obviously, a furnace manufacturer can’t be geographically close to all their clients. However, alleviating concerns about parts and service, accommodating on-site progress visits throughout the furnace manufacturing process, and manufacturing as much as possible in the U.S. would all be steps in the right direction.
All this to say, it is not so much the hard inputs like engineering, manufacturing, and finance that persuade customers to make a purchase. Rather, it is the softer inputs — the human elements — that help furnace buyers become comfortable, giving you a leg up on your competition. Comfort is an emotion… and as we all know and agree, “Everyone always buys emotionally all the time.”
Doug Glenn Publisher Heat TreatToday For more information: Contact Doug at doug@heattreattoday.com
Ryerson Holding Corporation, a value-added processor and distributor of industrial metals, and Olympic Steel, Inc., a U.S. metals service center, announced that they have entered into a definitive agreement to merge. The merger will enhance the combined company’s presence as the second-largest North American metals service center and will bring Olympic Steel’s complementary footprint, tempering capabilities, and heat treated product offerings into Ryerson’s network of value-added service centers.
The deal is expected to generate approximately $120 million in annual synergies by the end of year two via procurement scale, efficiency gains, commercial enhancement, and network optimization. The merger adds Olympic Steel’s thermal processing services and metals to Ryerson’s existing offerings.
As part of the transaction, Michael D. Siegal, executive chairman of Olympic Steel’s Board of Directors, will be appointed chairman of the Board of Directors (“Board”) of the combined company and Olympic Steel will also appoint three other directors to the combined 11-member Board. Eddie Lehner, president and chief executive officer (“CEO”) of Ryerson, will serve as CEO of the combined company, with Richard T. Marabito, CEO of Olympic Steel, serving as president and chief operating officer.
Eddie Lehner said, “This merger represents an immensely attractive and unique opportunity for Ryerson and Olympic Steel as it combines our two organizations, which couldn’t be more complementary and synergistic around the products, services, footprint, and customer experience…The combination of our organizations will further scale the digital investments that Ryerson has made to bring Olympic Steel’s capabilities and formidable expertise into a larger network and provide our customers with greater network density, faster lead times, and a wider array of custom solutions from pick-pack-and-ship to finished parts…I look forward to working with Rick and the entire Olympic Steel organization with shared mission, passion, and purpose to unite our teams in reaching our vast potential together.”
“We are very excited about the combination of Ryerson and Olympic Steel and the trajectory of the business going forward,” added Steve Larson, chairman of Ryerson’s Board. “We look forward to welcoming Michael and the additional Olympic directors to the already strong Ryerson board. They bring a wealth of experience and perspective.”
Michael Siegal added, “This is a significant milestone for the business my father and uncle started more than 70 years ago. We went from private to public in 1994, and now we enthusiastically take this next step to accelerate Olympic Steel’s continued growth.”
Press release is available in its original form here.
The Atmosphere Group contains many familiar subsidiaries to the heat treatment world: AFC-Holcroft, Atmosphere Heat Treating, Inc., Austemper Inc., and Nitrex NTS (Nitrex, G-M Enterprises, and UPC-Marathon). Now, the U.S. operating holding company will carry out business for the Region Americas under a new name: Aichelin Americas.
Marty Poljan will continue to lead the region as president and CEO of Aichelin Americas. The group has announced that Tracy Dougherty has been promoted to president of Sales & Service and that Paul Oleszkiewicz has been promoted to president of Operations. Together, Tracy and Paul bring more than 50 years of leadership experience in the heat treating industry.
Marty Poljan President & CEO Aichelin Americas Source: LinkedinTracy Doughterty President of Sales and Service Aichelin Americas Source: AFC HolcroftPaul Oleszkiewicz President of Operations Aichelin Americas Source: Nitrex
“Our clients don’t simply buy equipment — they make a long-term decision about who they can rely on,” says Poljan. “This leadership structure reflects that reality. We are here to be a consistent, service-driven partner — not just at installation, but through every maintenance cycle, modernization and capacity expansion that follows.”
“This industry has shifted,” notes Dougherty. “Responsive service, modernization support, and clear accountability over the lifespan of their equipment. That’s where our focus is, and where it will remain.”
Delivering on that promise operationally is Paul Oleszkiewicz, president of Operations, whose three decades at Nitrex have been dedicated to engineering execution, process reliability, and technical precision.
“Engineering leadership in heat treating comes down to repeatability and trust,” says Oleszkiewicz. “A furnace isn’t just a product — it’s a long-term production system. Our responsibility is to deliver with consistency and to stand behind that equipment with real technical support.”
“A furnace isn’t just a product — it’s a long-term production system”
As Aichelin Americas continues to align its manufacturing capabilities, aftermarket service network, and engineering resources across its combined brands, it is able to offer access to a leadership team that has lived the operational realities of all things thermal processing.
Press release is available in its original form here.
When it comes to furnace linings, most heat treaters focus on the hot-face materials, the heavy-duty refractories taking the brunt of molten metal, corrosive slags, and extreme heat. And just behind that armor lies a quiet defender: the refractory insulation layer. This layer is often the last line of defense between a functioning furnace and a costly, catastrophic failure. In this Technical Tuesday installment, Roger M. Smith, director of technical services for Plibrico Company, LLC helps readers understand the valuable role of refractory insulation for thermal stability.
Refractory insulation is more than a buffer or a back-up. It provides structural support to the working lining, maintains shell temperatures within safe limits, and cushions the entire structure against the stresses of expansion and contraction. When this layer fails, you don’t just lose insulation, you risk cracks, shell overheating, and lining collapse. In other words, it can turn a maintenance project into a full-blown emergency.
The Strength Factor: Why Compressive Strength Counts
If there’s one property that deserves special attention, it’s compressive strength. The insulation layer is like the foundation of a house: if it cannot support the load above it, the whole structure suffers. Insufficient compressive strength can lead to creeping, crushing, and distortion, all of which compromise the stability of the hot-face refractory.
At green or ambient conditions, most types of insulating refractories, including monolithic, mineral wool, and ceramic fiber boards, exhibit similar compressive resistance, typically in the range of 40−50 psi at 10% deformation, but strength changes significantly once the furnace heats up.
For example, most mineral wool and ceramic fiber boards contain organic binders that burn off at around 475°F, reducing their compressive strength by roughly 50% at furnace operating temperatures (based on the board manufacturer’s technical data sheets, see Table A). Over time, this can increase thermal conductivity through the reduced thickness of the insulating layer.
In contrast, monolithic lightweight insulating castables, like Plibrico’s Plicast Airlite 25 C/G, not only retain their compressive integrity as the temperatures rise, but they actually gain strength, according to ASTM C165 test data as the material fully sets and stabilizes under heat.
Figure 1. Monolithic insulation, gunned in place, stays strong and gains compressive strength during heat-up.
This difference matters: compressive strength is not static. It changes as the material heats up and insulating products that hold their strength at service temperatures provide a more stable, safe, and reliable support for the hot-face lining.
The takeaway? Stronger, more stable insulation is not just filler. It’s an active structural layer that helps prevent hot-face sagging, cracking, and premature failure, directly contributing to longer furnace life.
Thermal Stability: More Than Just Heat Resistance
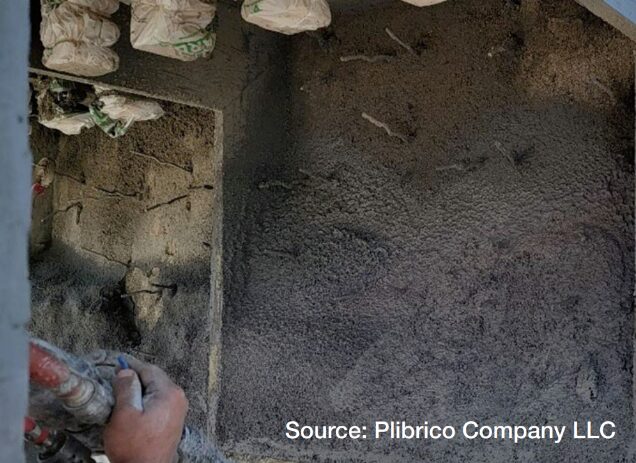
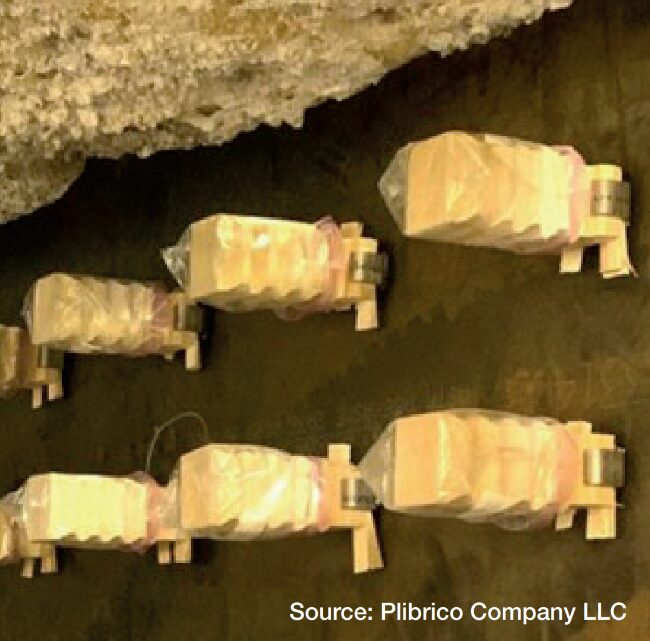
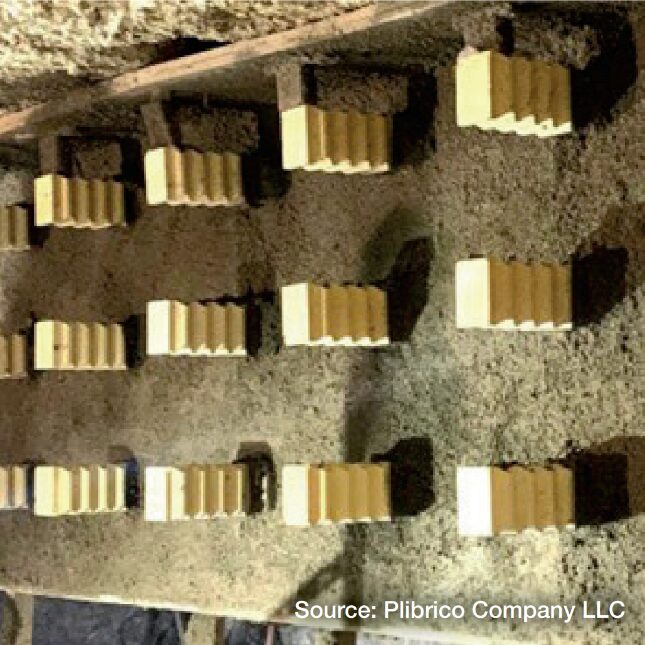
Figure 2. Confirmed anchor layout and fully prepped furnace wall ready for monolithic insulation installation.
Compressive strength plays a direct role in thermal stability. Denser, stronger castables with lower porosity are far better at resisting gas penetration, chemical attack, and erosion than lightweight, weaker alternatives.
When insulation loses stability, it can create voids, cracks, and hot spots, risks that threaten not only the hot-face layer but the furnace shell itself. This is why density and porosity are critical: denser insulating castables maintain their structure under load, resist infiltration, and provide reliable support for the hot face.
By contrast, mineral wool and board products often weaken as their organic binders burn off at service temperatures, leading to deformation and unpredictable thermal gradients.
Monolithic lightweight insulating castables can offer a more robust alternative. They retain their integrity as temperatures climb and can even gain compressive strength as they fully set and sinter during heat-up. This added stability reinforces the hot-face layer and helps prevent failures during thermal cycling.
There’s another layer to this: long-term thermal cycling. Furnaces rarely stay at one steady temperature; they ramp up, cool down, and undergo countless micro-cycles during operation. Insulation that can absorb these changes without cracking or delaminating is critical for avoiding premature lining failures.
In short, thermal stability is structural stability — the better your insulation performs under heat and cycling, the longer your furnace lining will last.
Designing for Expansion: Building Flexibility Into the System
Here’s where many lining failures start: in the different layers of lining expanding at different rates.
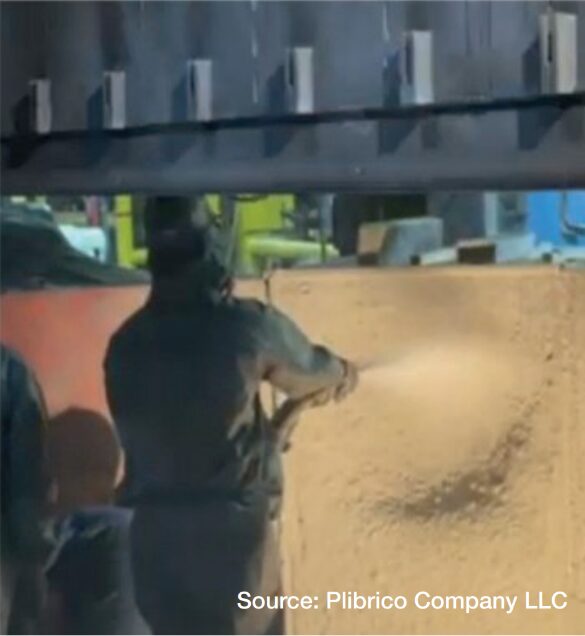
Figure 3. Completed furnace wall insulation
installation, finished in half the time required for board installation.
Hot-face refractories, often dense high-alumina castables, have significantly different thermal expansion coefficients compared to the lighter, more porous insulating castables behind them. The hot face may swell aggressively under load, while the insulation expands far less. If those differences are not accounted for, the result is tensile stresses, delamination, and cracking at the interface between layers. Over time, those cracks can grow, creating pathways for heat and corrosive agents to reach deeper into the lining.
This is where thoughtful design makes all the difference:
Anchor systems must hold both layers securely but flexibly, allowing each to expand without transferring destructive stresses. Using materials like monolithic refractories adds another advantage: their insulating properties help better protect the base of refractory anchors, reducing localized heat buildup and minimizing stress concentrations that can lead to cracking or premature anchor failure.
Installation sequencing should avoid locking the hot-face layer too tightly to the insulation, preventing “shear failure” during heat-up.
Layer composition must be selected so the expansion mismatch is minimized, balancing mechanical stability with thermal shock resistance.
When expansion is designed for, rather than ignored, the entire lining behaves like a single, flexible system instead of two incompatible parts competing for space.
Practical Tips for Getting It Right
Prioritize compressive strength. Choose insulation with enough strength to support the hot-face lining under load. Materials like monolithic lightweight insulating castables maintain or even increase compressive integrity at service temperatures, improving overall lining stability.
Figure 4. Gunned to the ideal thickness, insulation built with compressive strength can handle stress, prevent cracking, and maintain shape under heat.
Pick the right material for the zone. Not every insulating castable is created equal. Match density, chemistry, and expansion to the application.
Control the install. Low-water mixes, vibration placement, and proper curing are non-negotiables if you want consistent density and strength.
Don’t skip the heat-up schedule. Rushing dry-out or startup is one of the fastest ways to ruin a lining before it is even in service.
Revisit your anchor design and how you install around it. Poorly designed anchor layouts can lead to stress points and premature lining failures, so reviewing and optimizing the design is one of the cheapest ways to prevent costly mechanical issues. Plus, consider the installation method: board insulation requires time-consuming cutting and fitting around each anchor, while monolithic insulating refractories like Plicast Airlite 25 C/G can be installed around anchors in less than half the time, reducing labor while improving performance.
Built to Last
Insulation is not just about slowing heat loss, it is also about standing firm when your furnace is under its heaviest load. The right refractory insulation, engineered with compressive strength as a priority, gives your lining the backbone to absorb mechanical stresses, resist cracking, and maintain its shape through the punishing cycles of heat-up and cool-down. It does not just protect the shell; it supports the hot face, prevents hot spots, and preserves the entire system’s structural integrity.
3rd Party Test Lab – Orton Labs ASTM C165 Measuring Compressive Properties of Thermal Insulations
Note: Mineral Wool and Ceramic Fiber Boards contain organic binders that burn off by 475ºF. This reduces the strength of the board by 50% along with decreasing other important properties including thermal conductivity. Table A. Compressive strength at service temperatures: comparison of compressive resistance (10% deformation) between monolithic insulation lightweight castable/gunite materials such as Plibrico’s Plicast Airlite 25 C/G and mineral wool and ceramic fiber boards at increasing temperatures.
Choosing monolithic insulating castables that gain strength at operating temperatures, instead of mineral wool or ceramic fiber boards that lose half their capacity as binders burn away, is an investment in lining longevity. Get this layer right, and you secure longer campaigns, lower maintenance costs, and the confidence that your furnace can keep pace with production demands. Get it wrong, and you risk premature failures, costly outages, and avoidable downtime. In the end, refractory insulation built for compressive strength and stability is not just a detail, it is what keeps your furnace, and your operation, running at its best.
About The Author:
Roger Smith Director, Technical Services Plibrico
Roger Smith is a seasoned professional in the refractory industry. With Master of Science in Ceramic Engineering from the University of Missouri – Rolla, Roger has over 15 years of experience in the processing, development, and quality assurance of both traditional and advanced ceramics. He has a proven track record in developing innovative ceramic formulations, scaling up processes for commercial production, and optimizing manufacturing operations.