Heavy-Duty Trucks Power Up with Heat Treating


Source: Car and Driver Magazine, PickupTrucks.com


In the heavy-duty truck sector, the components of a 400-hp, 1000-lb-ft engine have been boosted with additional heat treating as part of the overhaul to update the company’s 6-speed automatic line and appeal to modern truck customers.

The 2019 Ram 3500 houses the first engine in the heavy-duty pickup class to reach 1,000 lb-ft of peak torque, powered by an all-new optional high-output turbo-diesel 6.7-liter Cummins inline-six-cylinder workhorse.

The new transmission benefits from stronger planetary gears and a new heat treatment system designed to significantly widen the range of optimum operating temperatures. ~ PickupTrucks.com


Read more:

“The 2019 Ram 2500 and 3500 Deliver a 1000-LB-FT Warhead to the Front Lines of the Truck War” at CarandDriver.com

“2019 Ram 3500 Reaches New Torque Territory” at PickupTrucks.com

Heavy-Duty Trucks Power Up with Heat Treating Read More »

Heat Treat Economic Report Continues Strong

Nine of eleven economic indicators from the monthly Industrial Heating Equipment Association (IHEA) were up in January. That miffed some who thought the industry was starting to soften. In fact, it is not conclusive one way or the other, but January’s numbers showed strength and surprisingly strong upward movements from a vast majority of the indices.

Graph of Capital Expenditures
Capital Expenditures for January were up significantly
Graph of Durable Goods orders.
Durable Goods orders were strong in January

The numbers, which we will dive a bit deeper into below, are provided monthly to members of the IHEA along with a 12-page report that digs into each index and how movement in that index will specifically impact the thermal processing industry. Anyone interested in receiving the report should contact Anne Goyer, Executive Director of IHEA, whose contact information is given at the end of this post.

Which indices were up? As mentioned earlier, nearly all of them.

  • New Home Starts took a significant jump.
  • Steel Consumption was up significantly.
  • Industrial Capacity Utilization was also up from the previous month.
  • Metal prices (aluminum, gold, nickel, copper) were also up.
  • The PMI was up significantly.
  • Capital Expenditures took a huge jump upward.
  • Durable Goods saw modest growth.
  • Factory orders rebounded from a previous month’s dip.
  • Transportation Index experienced a nice rebound after falling for several months.

The only two indices that did not improve were:

  • New Automobile and Light Truck Sales were essentially flat falling only slightly.
  • Credit Movement was significantly down

According to the IHEA report, this downward movement in the credit index causes one to pause and question whether 2019 will be as robust as 2018.

Ann Goyer, Executive Director of IHEA

Further analysis of each of these 11 indices can be obtained from Anne Goyer, Executive Director at IHEA, who can be reached at anne@goyermgt.com.


Heat Treat Economic Report Continues Strong Read More »

Meet the Consultants: Madhu Chatterjee

Heat Treat Today recently unveiled its Heat Treat Consultants page in the October 2018 print edition (available in digital format here) and at FNA in Indianapolis, Indiana. We offer this comprehensive listing of heat treat industry consultants as part of our efforts to help minimize the effects of heat treat “brain drain.” With so many heat treat brains growing older, the expertise that once used to reside inside of manufacturing operations is dwindling. Where, then, do manufacturers with in-house heat treat departments go when they need heat treat answers?

Turn to Heat Treat Today and our comprehensive list of heat treat industry consultants, which we will introduce to you one by one in this occasional feature, “Meet the Consultants”. There is no more comprehensive list of heat treat consultants. Learn more about Madhu Chatterjee of AAT Metallurgical Services LLC (who also provided the Technical Tuesday article this week, Comparative Study of Carburizing vs. Induction Hardening of Gears ), and then click through to the page to read more details about each consultant. We are adding more regularly. Contact them directly, or call us and we’ll introduce you to them. Whether it’s a technical process question, a safety concern, a compliance issue, or a business related question, one of our heat treat consultants will be able to help. If you are a consultant and would like to be listed, please contact Doug Glenn


Name: Madhu Chatterjee
Company Name: AAT Metallurgical Services LLC
Location: Troy, Michigan
Years in Industry: 40+
Consulting Specialties:

  • Manufacturing and Engineering
  • Process and Product Improvement
  • Automotive Research and Development

Send an email | Website | 614-519-0740, 352-315-9090

Briefly:

Madhu Chatterjee is a consultant with specialties in the automotive industry and experience in advanced engineering, research and development, and process and product improvement. He graduated from Indian Institute of Technology with a Bachelor’s Degree in Metallurgical Engineering and a Master’s in Ferrous Metallurgy. Madhu holds 10 patents and has won 5 awards in his areas of expertise. In 1977, he began working at General Motors as a Senior Staff Engineer. In 2001, he became the Director of Special Projects at Inductoheat during which time he gained a Master’s in Materials Engineering from Purdue University, and in 2010, he moved on to be the Director of Technology at Bodycote Thermal Processing. He returned to GM in 2014 as an Advanced Lead Engineer, working a total of 29 years at GM. He founded AAT Metallurgical Services LLC in Michigan where he is currently president of the company.

Significant Accomplishments:

  1. Bachelor’s Degree in Metallurgical Engineering and Master’s in Ferrous Metallurgy and Material’s Engineering
  2. Holds 10 U.S. patents in the area of Induction Hardening System and Method, Manufacturing Technique for Multi-layered Structure with Magnet Using an Extrusion Process, and Ring Assembly Manufacturing Apparatus and Method
  3. Recognized and awarded in 5 areas of expertise
  4. Possesses over 40 years of experience in heat treating, including 29 years in the automotive industry
  5. Co-author of papers presented at ASM International Conferences
  6. Regular present at ASM International, ASM Heat Treating Society, and other industry-related conferences
  7. Scheduled Co-Presenter at ITPS/IFCS 2018 on “Cutting Edge Trends: A Consultants Panel Looks at the Future,” International ThermProcess Summit/International Finishing & Coatings Summit 2018, Atlanta, Georgia
  8. Founded and served as president AAT Metallurgical Services, LLC

Links to Heat Treat Today Articles or Other Resources from This Consultant

References available upon request from the Consultant

Meet the Consultants: Madhu Chatterjee Read More »

Reader Feedback: On Heat Treating Firearms

Our Reader Feedback feature allows us to facilitate discussion between Heat Treat Today‘s content contributors and hard-working folks in the shop who have questions about an article.


This Reader Feedback exchange followed an inquiry to our publisher Doug Glenn about government regulation of heat treatment of firearms which we threw out to a few of our consultants and individuals who have knowledge and expertise in this field — and we added a few questions of our own. Our experts are Doug Shuler, lead auditor with Pyro Consulting LLC; John Quaglia, president of Bennett Heat Treating and Brazing; and Jamie Jones, president of Solar Atmospheres. If you have any questions about this or other topics you’ve seen covered on any Heat Treat Today platform, please submit them to editor@heattreattoday.com.


Do you know if any type of firearms license is required to heat treat firearm components?

Doug Shuler

Doug Shuler: It depends on which components are being heat treated.  Barrels, slides, etc. do not require a license, but if the receiver (the part with the serial number) is heat treated, a license is required and the heat treater is subject to ATF audits. . . . Basically, if serialized parts are heat treated it must be done under an FFL (Federal Firearms License) so the ATF can audit the whereabouts of any firearm at any time.

John Quaglia

John Quaglia:  To the best of my knowledge, based upon some pretty extensive experience heat treating firearm components for one of my customers, the only license I am aware of is an FFL which is required to heat treat serialized receivers. If the components are military or ITAR controlled, you must be registered with the DDTC and have ITAR certification, [as well as] for domestic (commercial firearms) if you are heat treating serialized components of a firearm (the receiver). Barrels, slides, sights, magazines, springs, firing pins, etc., are all easily acquired and interchangeable between firearms and therefore require no special permitting.

Jamie Jones

Jamie Jones: The US Department of Justice authorizes the ATF to regulate those who are manufacturers, dealers, collectors, and importers of firearms and destructive devices. Part of that regulation requires a license (Federal Firearms License [FFL]) be applied for and held by those who are involved with any of the above. For a contract heat treat company, this essentially only pertains to serialized components. Under the “manufacturing” definition, the ATF considers any activity which results in the manufacture of firearms for sale or distribution (including installing parts in or on firearm frames and receivers, and processes that primarily enhance a firearm’s durability), constitutes firearms manufacturing, and requires a manufacturer’s license.  The FFL does not include components related to fully automatic firearms or suppressors.  In order to possess and process those serialized items, the ATF requires a manufacturer’s FFL plus a special occupational tax stamp (SOT).  Prior to issuance of the FFL, the ATF will conduct an on-site audit of the operation and person(s) applying for the license/stamp.  The FFL needs to be renewed every three years.

What is the most challenging part of heat treating gun parts?

Spring Loaded Firing Pin thetruthaboutguns.com

JQ: Managing distortion is probably the most challenging as most components are very close to being finished machined. Special racking and methodizing is often required. Marquenching, ausquenching, and vacuum processing are often employed to minimize or eliminate the possibility of distortion. Also, due to the small size and complex geometry present, inspection of the parts is difficult. It is important to clarify the testing location with the manufacturer prior to punching hardness holes into areas of the parts that may be exposed after assembly. After all, manufacturers want their guns to look nice afterward. We have experienced delayed rusting on barrels due to the combination of steel wire and the 4150 barrel reacting to cause anodic corrosion after processing in a salt bath which would only expose itself after a few days. We would ship parts that were perfect, and two days later I would be on the phone with my customer trying to explain a mysterious rust line through the rifling in the barrel. We solved this with some tooling changes.

JJ: Frankly, it is no more challenging or different than heat treating any other parts for any other industry. Some parts are routine and some are challenging. Some materials are more challenging than others and some designs are more challenging than others.

Which parts are the most difficult and why?

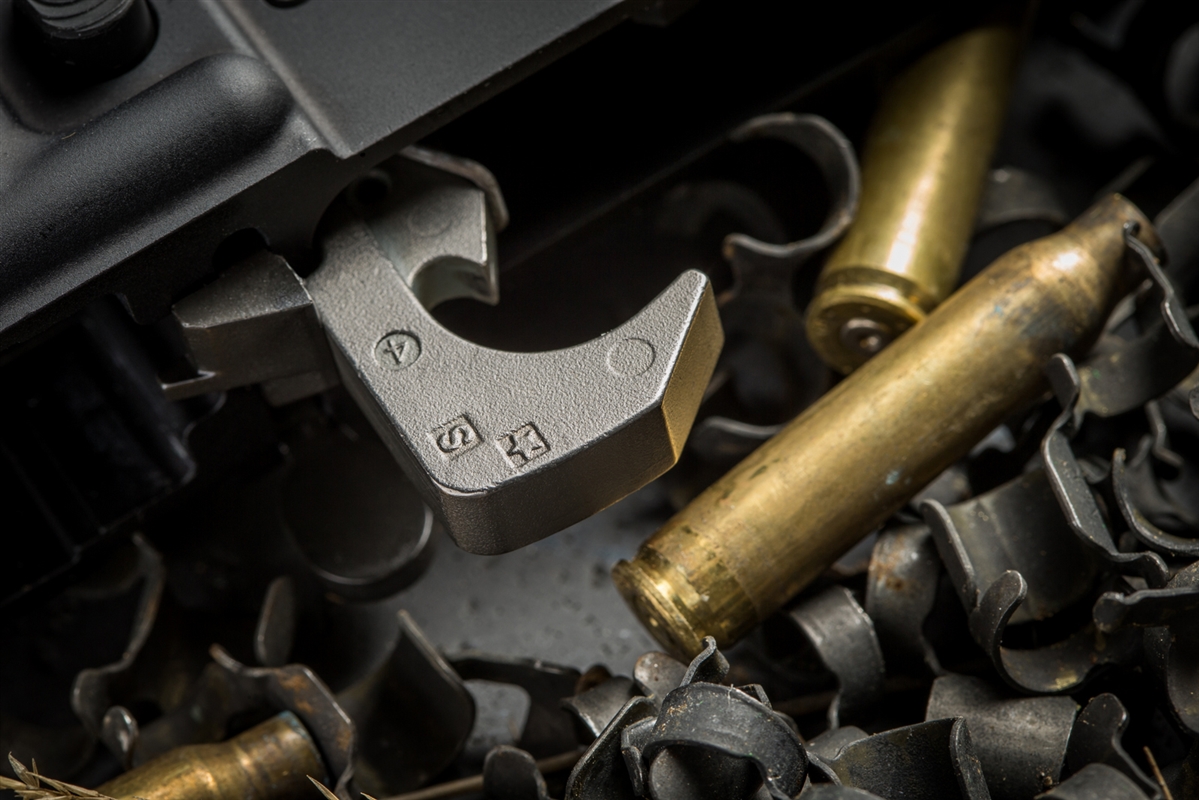
BCM PNT™ Trigger Assembly Bravo Company USA

JQ: They all present challenges. Slides and barrels present challenges due to the non-symmetrical nature which require special setup procedures. These also tend to have lots of crevices and blind or small holes which trap quenchants, salts, cleaning materials which tend to lead to unhappy customers unless the parts are thoroughly cleaned. Magazines present challenges because they are thin steel stampings which tend to distort due to the quench and induced stressed relieving themselves during heating. I could write a book on the challenges we have faced with the processing of gun parts.

JJ: Parts that require carburizing which have been machined to a finished or near-finished state, with intricate designs, cut-outs, and varying cross sections are the most challenging; a perfect example of this is an AR bolt carrier.  This kind of challenge is why we developed our version of low-pressure vacuum carburizing, as we now don’t need to worry about severe quench distortion or carbon potential control. With traditional carburizing, the austenitizing temperature of the steel can change if too much carbon diffuses into the corners and edges.  This can lead to retained austenite and carbide formation.  Our process negates that phenomenon by using precisely controlled boost-diffuse controls instead of carbon potential.  Our process also leaves the parts bright, with no post carburizing blasting or cleaning operations required.

Is it the materials that make it difficult or is it the configuration of the part?

JQ: The materials tend to be common that most heat treaters have worked with before so from a metallurgical standpoint I would say that the materials are not the problem. The configuration of the parts is definitely worse. Non-symmetrical parts tend to distort more than symmetrical parts. It also makes it difficult to inspect the parts. Test in the wrong area and you have spring-back or rocking. As I mentioned earlier, if you test in the wrong area the customer cannot sell the part. Some gun manufacturers have test methods that are unconventional, testing a shallow case depth using an HRC scale, so that the hardness reading is a combination of the case hardness, case depth, and core hardness.

JJ: It seems like you are assuming it is difficult all of the time! Please see my answer to question 2 above.

Are there any other special processes or regulations that need to be followed when heat treating gun parts? If so, what are they?

JJ: This answer is not to be taken as legal advice. If you want to apply for an FFL, or you get an FFL, you need to know the regulation. It is serious business: if you don’t follow regulation, you could end up in prison. You need to keep detailed records of EVERY serialized component that you receive, process, and ship. You don’t want to be on the tail end of a missing part or parts, especially if you don’t know about it. If something goes missing you need to report it immediately. Of course, reporting it could mean losing your license. So my advice to anyone considering this is: BE GOOD AT TRACEABILITY and RECORD KEEPING!


We welcome your inquiries to and feedback on Heat Treat Today articles. Submit your questions/comments to editor@heattreattoday.com.

Reader Feedback: On Heat Treating Firearms Read More »

Comparative Study of Carburizing vs. Induction Hardening of Gears

Modern rotary-wing aircraft propulsion systems rely on different types of gears to transmit power from the turbine engines to the rotors. The basic requirements of these gears are that they are high strength, sustain long life, meet weight considerations, and have a high working temperature and low noise and cost, among others.

Most importantly, these gears require a hard, wear-resistant surface with a ductile core.

Gas carburizing is the current heat treat method used to produce these aircraft quality gears, but this method of heat treatment is costly due to the large number of process steps, huge footprints, energy consumption, and environmental issues. Moreover, the final grinding of gear teeth to correct distortion produced during quenching reduces effective surface compressive stresses.

An investigation into low-cost alternatives for surface hardening aerospace spur gears was conducted where specimens of the selected gears were induction hardened using a patented process. Dimensional and microstructural analyses were conducted, and residual stress studies were performed. This article is a summary of the steps and observations of the case study that resulted from this investigation, which can be summarized this way:

The proposed induction process is a low-cost alternative to conventional gas carburization. In some applications, a 25% savings is estimated.

The first step to gear manufacturing demands a total understanding of aerospace gear requirements. As the gear transmits torque, the teeth are subjected to a combination of cyclic bending, contact stresses, and different degrees of sliding or contact behavior. It is, therefore, critical for a gear to have the proper case and core structure to withstand these loading conditions.

With every revolution, a cyclic bending load is applied, resulting in tensile stress at the root region of the gear. The core of the gear has to be soft to absorb impact load and prevent brittle failure. Due to high-speed contact between adjacent gear teeth, peak shear stresses generated at the surface act in the normal direction to the surface. Pitting, spalling, or case crushing types of failures can occur due to low residual stress or inadequate case depth.

For aircraft quality gears, typical surface hardness is around 58Rc to 60Rc. The case depth is in reference to 50Rc and is controlled by diametral pitch.

Carburization

Carburization hardening is the most widely used technique for surface hardening of aerospace quality gears. A brief introduction to carburization is necessary to understand the potential benefits of this process and how other surface transformation can improve on some of the drawbacks of this commonly used process.

After raw material is received, it is forged to achieve proper grain structure and core hardness. The alloy most commonly used is ASM 6260 (AISI 9310). This low carbon alloy steel exhibits high core toughness and ductility.

Parts are loaded in a furnace and heated to 1650ºF – 1750ºF in a carbon rich atmosphere, where approximately 1% carbon potential is maintained. The depth and level of carbon absorption depend on carbon potential, temperature, time inside the furnace, and the alloy content of the material. After the desired carbon gradient is achieved, the gears are cooled slowly. Then the parts are heated to austenitizing temperature and quenched.

The process depends on the size, geometry, dimension tolerances, and other gear requirements.

The heat treat cycles shown above are two commonly used carburization processes. The difference in post carburization steps depends on the alloy used and final product requirement.

The characteristic of carburization is the inherent distortion associated due to the difference in cooling rates between the thin web and thicker rim. Distortion can occur as a size growth, a change in involute profile, or the loss of crown in spur gears.

Case Hardening by Selective Heat Treatment

The number of process steps required to case carburize a gear can be significantly reduced only if the gear tooth surface areas are heat treated.

Processes for locally heating only the tooth surface include induction, flame, laser, and electron beam.

In order to use induction, steel with a minimum of 0.5% carbon must be used. Several different alloy steels were experimented with, such as AMS 6431, AlSl 6150, and AlSl 4350/4360/4370. These steels were selected due to their combination of toughness, temper resistance, hardenability, and strength. The hardened case is obtained by heating a specific volume of the tooth surface above the transformation temperature for that material. Rapid contour heating produced a case of martensitic structure around the profile-hardened area, resulting in high compressive residual stress at the surface at the root fillet. This compressive stress increases the tooth bending fatigue life, where tensile stress exists due to tooth bending.

Transformation hardening allows a significant reduction in process steps and associated fabrication costs, due to two different factors:

  1. Since sufficient carbon is already present in the base material, copper masking, plating, stripping and carburization steps are eliminated.
  2. In selective hardening, the area of the heated zone is limited to only the hardened sections, and distortion is minimal and predictable.

Surface hardening applications are generally controlled by three process parameters, namely frequency, power level, and time. In this respect, several different hardening processes have been used for gear hardening. The proposed method discussed in this presentation is known as Dual Pulse Induction Hardening (DPIH).

DPIH Process

The DPIH is a patented process (U.S. patent #4,639,279). The process uses single frequency for both the preheat and final heat cycles. Two different power levels are used. This allows the entire process to be performed in one setup, using a single solid-state power supply.

The DPIH process consists of the steps described below:


The heat treatment process steps for both the carburized and DPIH processes for the aircraft gear are compared below:


An 85% reduction in heat treat process steps occurs when the gear hardening method is changed from conventional gas carburization to DPIH.


Conclusion:

Comparison of the above data and the conventional carburization process to DPIH process.

Carburizing grade material has to be changed from low carbon to medium carbon steel for induction hardening. In both the processes, surface hardness achieved is comparable, but the characteristic of induction hardening is that the gear section maintains a constant hardness value from the surface up to the transition zone, where it rapidly drops to core hardness levels, unlike a more gradual decrease in hardness in case of carburized gears. Low distortion of induction hardening gear is also a major cost reducing factor.


Acknowledgment:

This work was performed at AGT, Division of General Motors.


Madhu Chatterjee is founder and president of AAT Metallurgical Services LLC in Michigan with extensive experience in advanced engineering, research and development, and process and product improvement. He is also one of the original dozen consultants that inaugurated Heat Treat Today’s Heat Treat Consultants resource page. You can learn more about Madhu Chatterjee here.


Look for more on aerospace heat treating in the upcoming special aerospace manufacturing edition of Heat Treat Today.

Comparative Study of Carburizing vs. Induction Hardening of Gears Read More »

United States Steel to Restart Construction of Electric Arc Furnace

David B. Burritt, U.S. Steel President & CEO

United States Steel Corporation announced recently the restart of construction on a technologically advanced electric arc furnace (EAF) steelmaking facility at its Tubular Operations in Fairfield, Alabama. U. S. Steel previously initiated construction of the EAF in March 2015 in order to replace an existing aging blast furnace, but the company suspended construction in December 2015 due to unfavorable market conditions.

The investment to complete the EAF, which includes modernization of the existing rounds caster, is expected to begin immediately and the furnace is expected to be on line in the second half of 2020. The U. S. Steel Fairfield Tubular Operations custom creates seamless steel casing with an outside diameter range of 4-1/2 to 9-7/8 inches and seamless steel line and standard pipe with an outside diameter range 4-1/2 to 8-5/8 inches.

“We are pleased to announce the achievement of the market and performance stage gates required to restart our Tubular Segment EAF,” said David B. Burritt, President and Chief Executive Officer. “This investment is an important step to improve our cost structure and positions our Tubular business to win over the long-term. We are committed to investing in the sustainable steel technology required to be a value-added tubular solutions provider for our customers,” said President and Chief Executive Officer David B. Burritt.

“Thanks to the President’s strong trade actions and improved market conditions, support from the United Steelworkers and incentives from the State of Alabama and the Jefferson County Commission, we are excited to add EAF capabilities to our company’s footprint and provide sustainable tubular solutions for our customers,” added Burritt.


Image Source: USSteel Tubular Operations

United States Steel to Restart Construction of Electric Arc Furnace Read More »

NDT Services Provider Expands Capabilities in Europe

A global provider of materials and product qualification testing, inspection and certification services recently opened a new 20,700-square-foot testing laboratory in Sheffield, UK.

Charles Noall, President & Chief Executive of Element

Element announced that the new center of excellence for non-destructive testing and inspection is strategically located close to Sheffield’s successful Advanced Manufacturing Innovation District (AMID) and will give customers within the aerospace and oil & gas industries the benefit of new equipment, expertise, and technical support all within one site. The facility complements the existing Magna Way laboratory which offers a well-equipped machine shop with up to date CNC machining facilities, and sample heat treatment capabilities, mechanical, chemical analysis, metallurgical testing and force calibration services.

Element has invested in equipment for immersion ultrasonic testing (IUT), as well as dye penetrant inspection, eddy current inspection, magnetic particle inspection, and on-site positive material identification. In preparation for the opening of the laboratory, the company, in partnership with the Advanced Manufacturing Research Centre (AMRC) at the University of Sheffield, has trained five new engineering support and machinist apprentices. The apprentices will work closely with the skilled on-site technical team and will all be based in the new facility.

“I am delighted to open this new facility which is part of the new industrial revolution within the Sheffield region,” said Charles Noall, President & Chief Executive of Element, in remarks at the opening of the center. “It greatly expands the range of equipment and skills we have to offer customers in the aerospace and oil & gas sectors. This superb site complements our existing NDT capabilities across Europe and North America and enables our highly experienced team to deliver a first-class experience for our customers using the latest testing techniques and equipment.”


NDT Services Provider Expands Capabilities in Europe Read More »

15 Quick Heat Treat News Items to Keep You Current

Heat Treat Today offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry.

Personnel and Company Chatter

  • Roger Smith has recently been appointed Technical Manager at Plibrico Company, LLC.  Smith will be responsible for development of innovative refractory formulas, oversee product quality, and assist in identifying the best materials for refractory construction projects.
  • William “Bill” Cowell has been promoted to the position of Vice President of Operations at Advanced Heat Treat Corp. (AHT). Cowell, who has been at AHT since 1999, will oversee operations for all AHT  facilities.
  • Wirco has announced the promotion of Aaron Fisher to Vice President of our Fabrication Division. Aaron has been with Wirco for 19 years. In addition, Wirco welcomes Marco Möser as the Vice President of our Foundry Division.
  • Thomas G. Gasbarre has stepped down as Chief Executive Officer of Gasbarre Products, Inc, a position he has held since his father George Gasbarre, the founder of the company, retired in 1990. Gasbarre also announced that Tom’s son, Alex Gasbarre, has been appointed Chief Executive Officer and is now leading the development and execution of the company’s short- and long-term strategies. Heath Jenkins has been promoted and will succeed Alex as President, Press & Automation, and Manufacturing Technologies.
  • John C Plant has been appointed to serve as Chairman and Chief Executive Officer at Arconic Inc. The Board has also appointed Elmer L. Doty, a current Director, to serve as Chief Operating Officer, and Arthur D. Collins, Jr., a current Director, to serve as Lead Director. These appointments are effective immediately.
  • Xerox, based in Norwalk, Connecticut, has acquired metal additive manufacturing company Vader Systems, which will enable it to offer its customers access to low-cost metal additive manufacturing with a greater variety of metals. Based in Buffalo, New York, Vader Systems is a developer of liquid metal additive manufacturing technology.
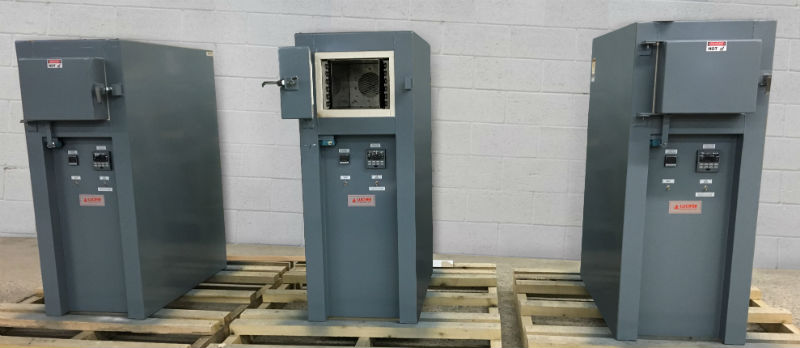
  • Several convection ovens were supplied to a manufacturer of small medical parts in the southern U.S. by Lucifer Furnaces. Model 42-B18 has a working chamber size of 9”H x 9”W x 18”L and heats to 1200°F.
  • A floor-standing furnace has been shipped by L&L Special Furnace Co., Inc. to a worldwide leader of high tech ceramics and associated components located in the Northeastern United States. The furnace will be used for glass components along with fiber optics and research and development. It will also be used to fill in on various thermal projects and development.
  • A Treet-All™ Box Furnace has been shipped to a Japan-based global battery manufacturing company by Lindberg/MPH.  The maximum temperature rating of this light industrial box furnace is 2050°F and has work chamber dimensions of 18” wide x 36” deep x 18” high. The Treet-All™ Light Industrial Box Furnace is suited for multiple applications, including annealing, ashing, austempering, brazing, preheating, solution treating, stress relieving, and normalizing.
  • A supplier of the aerospace industry received shipment of a Electrically Heated Horizontal Quench Solution Treat System from Wisconsin Oven Corporation. The Horizontal Quench Solution Treat System has a maximum oven operating temperature of 1,200° F and work zone dimensions of 5’4″ wide x 5’6″ long x 5’4″ high (above the rollers).
  • Chromalox, a thermal technology provider, recently contracted with Sierra Monitor Corporation  to enable cloud system connectivity on their Heat Trace solution.
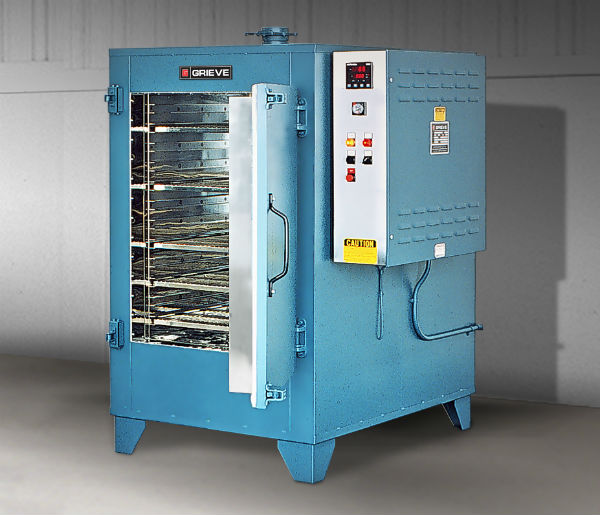
  • A cabinet oven is being used to finish batch loads of metal parts at a customer’s facility. The No. 828 is a 500°F (260°C) cabinet oven from Grieve Corporation.
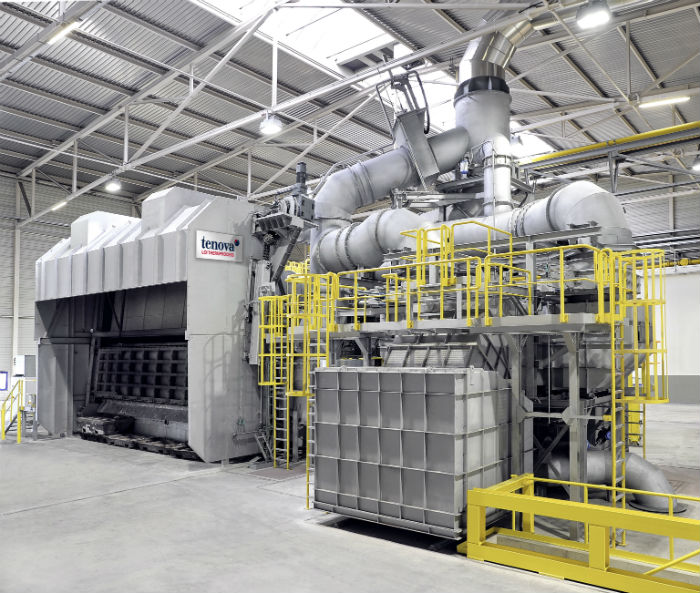
  • A recycling and melting group has ordered for installation a Twin-Chamber Melting Furnace TCF® from Tenova LOI Thermprocess. Italy-based Fonderie Pandolfo specializes in processing of aluminum, mainly for extrusions. The casted billets are mainly extruded in the extrusion shops of the main European extruders.

Kudos Chatter

  • Buehler, an ITW Company, and ASM International are celebrating 75 of continuous partnership in 2019. Buehler has continuously supported of the ASM World Training Center in Novelty, Ohio, through its innovations for metallography and hardness testing, solutions for the newest materials and participation in ASM International activities.
  • Pennsylvania-based Onex Inc recently completed a forge furnace refractory reline in one week.

Heat Treat Today is pleased to join in the announcements of growth and achievement throughout the industry by highlighting them here on our News Chatter page. Please send any information you feel may be of interest to manufacturers with in-house heat treat departments especially in the aerospace, automotive, medical, and energy sectors to the editor at editor@heattreattoday.com.

15 Quick Heat Treat News Items to Keep You Current Read More »

Arconic Splits Operations, Expands Hot Mill Capability

Arconic Inc., which specializes in lightweight metals engineering and manufacturing, recently announced plans to separate the company’s portfolio into Engineered Products & Forgings and Global Rolled Products, with a spin-off of one of the businesses. In addition, it will also explore the potential sale of businesses that do not best fit into engineered products & forgings or global rolled products.

The Global Rolled Products segment produces a range of aluminum sheet and plate products for the aerospace, automotive, commercial transportation, brazing, and industrial markets. The Engineered Products and Solutions (EP&S) represents Arconic’s downstream operations and produces products that are used mostly in the aerospace (commercial and defense), commercial transportation, and power generation end markets.

The New York City-based company’s decision to separate its portfolio comes after rejecting a $10 billion offer for the entire company and abruptly replacing its Chief Executive. John Plant, the newly appointed CEO, stated during the company’s 4Q18 conference call that he expects the spin-off would be completed within the next 9 to 15 months.

Arconic has also released investment plans to expand its hot mill capability and add downstream equipment capabilities to manufacture industrial and automotive aluminum products in its Tennessee Operations facility near Knoxville, Tennessee.

Tim Myers.

“This investment will add capacity to meet the growing demand for industrial products and automotive aluminum sheet,” said Tim Myers, President of Arconic’s Global Rolled Products business. “With this expansion, we are further diversifying the portfolio of one of our largest North American facilities.” The industrial market consists of products made with common alloy aluminum sheet, which is used in applications for commercial transportation, appliances, machinery, and construction.


Photo credit/caption: Bloomberg News / A worker controls a crane to move an aluminum coil at the Arconic Inc. manufacturing facility in Alcoa, Tennessee. 

Arconic Splits Operations, Expands Hot Mill Capability Read More »

Heat Treat Tips: Make and Stick to a Clear Preventative Maintenance Program

During the day-to-day operation of heat treat departments, many habits are formed and procedures followed that sometimes are done simply because that’s the way they’ve always been done. One of the great benefits of having a community of heat treaters is to challenge those habits and look at new ways of doing things. Heat Treat Todays 101 Heat Treat Tips, tips and tricks that come from some of the industry’s foremost experts, were initially published in the FNA 2018 Special Print Edition, as a way to make the benefits of that community available to as many people as possible. This special edition is available in a digital format here.

Today, we offer one of the tips published under the Vacuum Furnace category. 


Vacuum Furnace

Heat Treat Tips #3

Make and Stick to a Clear Preventative Maintenance Program

Make sure a preventative maintenance schedule is clearly defined and adhered to. Most modern furnace control systems include diagnostics to assist in determining when certain components of the equipment require maintenance. Use these tools to prevent downtime and avoid wasting unnecessary maintenance.

  1. Change pump oil regularly: roughing, pump, boosters, and holding.
  2. Check hot zone for wear, loose, or missing hardware; verify element to ground resistance is greater than 10 ohms, vacuum out loose debris (monthly).
  3. Check water chemistry and adequate flow to and from the furnace (weekly).
  4. Check front door O-ring integrity, make sure there is no damage and that the ring is not flat; light grease as needed.
  5. Bubble check process gas lines for potential leaks.
  6. Check motor belts.
  7. Grease the main valve (monthly).


This tip was submitted by Solar Manufacturing.

Heat Treat Tips: Make and Stick to a Clear Preventative Maintenance Program Read More »