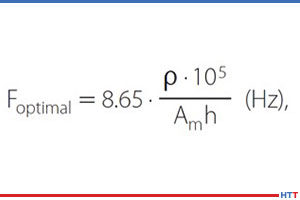10 Heat Treat Tips to Whet Your Appetite

Heat Treat 2019 is coming, and one of the great benefits of gathering with a community of heat treaters is the opportunity to challenge old habits and look at new ways of doing things. Heat Treat Today’s 101 Heat Treat Tips is another opportunity to learn the tips, tricks, and hacks shared by some of the industry’s foremost experts.
For Heat Treat Today’s latest round of 101 Heat Treat Tips, click here for the digital edition of the 2019 Heat Treat Today fall issue (also featuring the popular 40 Under 40), and to be distributed in print at Heat Treat 2019, in Detroit, Michigan, October 14-17, 2019.

Today’s Technical Tuesday features 10 Tips from a variety of categories, including SCR Power Controls (56), Cooling Systems (64), Combustion (66, 101), Induction Heat Treating (71), Thermocouples (79), AMS2750 (86), Vacuum Furnaces (92), and Miscellaneous (41, 87). These tips come from the 2018 list of 101 Heat Treat Tips published in the FNA 2018 Special Print EditionThis special edition is available in a digital format here.

If you have a heat treat-related tip that would benefit your industry colleagues, you can submit your tip(s) to doug@heattreattoday.com or editor@heattreattoday.com—or stop by to see us at Booth #2123 in Detroit!


Heat Treat Tip #41

Discolored Part—Who’s to Blame?

If your parts are coming out of the quench oil with discoloration and you are unsure if it is from the prewash, furnace, or oil quench, you can rule out the quench if the discoloration cannot be rubbed off. Check this before the part is post-washed and tempered.

Other possible causes:

  • Can be burnt oils as parts go through the quench door flame screen
  • Poor prewash
  • Furnace atmosphere inlet (particularly if it is drip methanol)

Submitted by AFC-Holcroft


Heat Treat Tip #56

Electrical Energy Savings

When we buy a pint of beer we don’t expect the head (or foam) to be ½ the glass. We can get this situation when we pay for our plant’s electricity; we pay for both the working power that drives the process (analogy: beer) and reactive power that doesn’t directly drive the process (analogy: foam/head). The lower the Power Factor the worse this situation. The latest SCR devices can help combat this while maintaining precise control and reducing overall peak load demands (using flexible firing methods).

Submitted by Eurotherm


Heat Treat Tip #64

Buy a Cooling System Capable of Growth
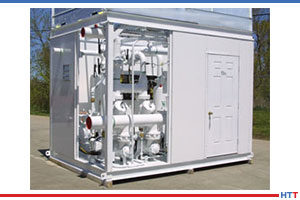
Plan for future growth. It is more cost-effective to provide additional capacity while equipment is being installed. Simple planning for the addition of future pumps (e.g. providing extra valved ports on tanks) and space for heat transfer equipment (e.g. pouring a larger pad or adding extra piers) can save considerable money down the road with little upfront expenditure. Consider installing one size larger piping for the main distribution supply and return. If this is not possible make sure you can add an additional piping run on the hangers you will install now.

Above all, be sure to include all necessary drains, vents, isolation valves, and plenty of instrumentation. These items are critical aids in maintenance and troubleshooting and future system expansion.

Submitted by Dry Coolers


Heat Treat Tip #66

Tune That Burner!

Don’t neglect burner tuning—a 1% reduction in excess O2 in the flue products can save you $1,000.00/year on your IQ batch or $2,000.00/year on a 2000-pound/hour continuous furnace—not to mention consistent temp uniformity, better heat-up rates. Pretty good payback for a couple of hours’ work.

Submitted by Combustion Innovations


Heat Treat Tip #71

Tube & Pipe Heat Treatment Is Different Than Solid Cylinder Heat Treating

Induction heating of tubes and pipes is somewhat different from the heating of solid cylinders. There is a difference in the frequency selection that would maximize energy efficiency for heating tubular products as compared to solid cylinders. In tube and pipe heating, the frequency, which corresponds to maximum coil efficiency, is typically shifted toward lower frequencies providing larger current penetration depth than the tube wall thickness (except for heating of tubes with electromagnetically small diameters). This condition can produce an improvement in electrical efficiency of 10–16 % and even higher. One simplified formula that is used in industry for rough estimate of the electrically efficient frequency is shown in the image, where:

  • ρ – electrical resistivity of heated metal (Ω*m)
  • Am = average diameter; Am = (Tube O.D. – h) (m)
  • h = wall thickness (m)

In cases when induction heaters cannot be considered to be electromagnetically long coils, the values of the optimum frequency will be higher than the values suggested according to formula, and computer modeling can help determining its exact value.

Submitted by Dr. Valery Rudnev, FASM, Fellow of IFHTSE Professor Induction Director Science & Technology, Inductoheat Inc., An Inductotherm Group company


Heat Treat Tip #79

Order SAT Probes All at Once

Place a yearly blanket order for your SAT probes and ask that they are made from the same coil. This will give you the same correction factors and temperature tolerances.

Submitted by GeoCorp


Heat Treat Tip #86
AMS2750 Is Golden

This standard is gold and unfortunately has a bad rap today because companies feel it’s just added cost into the process. Today’s technology means you can afford AMS2750E compliant controllers and digital recorders for only a few hundred dollars above a standard offer. This investment will be paid back many times over due to the longer lifetime expected with a quality instrument as well as the quality benefits from better drift performance between calibration intervals, redundant recording (in case of record loss), and overall accurate temperature control, leading to less rejects and reduced rework.

Submitted by Eurotherm


Heat Treat Tip #87
Pay Attention to Material Chemistry

When trying to determine a materials response to heat treatment, it is important to understand its form (e.g., bar, plate, wire, forging, etc.), prior treatments (e.g. mill anneal, mill normalize), chemical composition, grain size, hardenability, and perhaps even the mechanical properties of the heat of steel from which production parts will be manufactured. The material certification sheet supplies this basic information, and it is important to know what these documents are and how to interpret them.

Certain alloying elements have a strong influence on both the response to heat treatment and the ability of the product to perform its intended function. For example, boron in a composition range of 0.0005% to 0.003% is a common addition to fastener steels. It is extremely effective as a hardening agent and impacts hardenability. It does not adversely affect the formability or machinability. Boron permits the use of lower carbon content steels with improved formability and machinability.

During the steelmaking process, failure to tie up the free nitrogen results in the formation of boron nitrides that will prevent the boron from being available for hardening. Titanium and/or aluminum are added for this purpose. It is important, therefore, that the mill carefully controls the titanium/nitrogen ratio. Both titanium and aluminum tend to reduce machinability of the steel, however, the formability typically improves. Boron content in excess of 0.003% has a detrimental effect on impact strength due to grain boundary precipitation.

Since the material certification sheets are based on the entire heat of steel, it is always useful to have an outside laboratory do a full material chemistry (including trace elements) on your incoming raw material. For example, certain trace elements (e.g. titanium, niobium, and aluminum) may retard carburization. In addition, mount and look at the microstructure of the incoming raw material as an indicator of potential heat treat problems.

Submitted by Dan Herring, The Heat Treat Doctor®


Heat Treat Tip #92

Hacksaw Your Hearth!

When loading parts, carefully place the workload on the center of the hearth (front-to-back and side-to-side). Make sure it is stable and no part of the load is close to or touching the heating elements. This can create arcing and damage your parts. Tip: Once the load is in place, mark the hearth posts with a hacksaw to quickly find the front and back measurements each time.

Submitted by Ipsen USA


Heat Treat Tip #101

Can We Achieve Perfect Combustion?

Perfect combustion is based upon the concept of neither excess oxygen or a deficiency of oxygen in the combustion process. This is known as stoichiometric or theoretical combustion. Why is this considered as theoretical and not possible under normal field conditions? Consider the factors that can affect your combustion process: temperature of air or gas, pressure fluctuations, gas composition or supply changes, operating conditions, etc. Therefore theoretical combustion is just that: perfect combustion is only possible in a lab setting. Burner adjustment and calibration normally maintains a minimum of 10% excess air to compensate for these variables and avoid operating gas-rich with high levels of CO in the combustion process.

Submitted by WS Thermal

10 Heat Treat Tips to Whet Your Appetite Read More »
Heat Treat Today Launches Live Link to Digital Edition of 2019 Heat Treat Show Issue

Print copies of the Heat Treat Today fall 2019 publication began hitting mailboxes throughout the heat treat industry over the past couple of week, and now the digital edition is officially launched—today, Monday, October 7, 2019—with the following features:

  • 40 Under 40 Class of 2019, highlighting 40 enthusiastic, forward-thinking, skilled professionals who have made a mark on the heat treating industry before their 41st birthday (plus 8 Honorable Mentions)
  • 101 Heat Treat Tips—troubleshooting, preventative, green initiatives, safety reminders, time savers—from experts representing all facets of the heat treating industry
  • A round-up of News Chatter items featuring personnel and company news, equipment transactions, acquisitions and expansions, and kudos

Go here for the digital edition, or go to www.heattreattoday.com and click on the Resources tab to link to the Digital Edition.

If you’ll be at ASM’s Heat Treat Show, visit us at Booth #2123 to discuss how Heat Treat Today can help you do your business, and remember to check out your registration packet for a complimentary copy of the print magazine!

Heat Treat Today Launches Live Link to Digital Edition of 2019 Heat Treat Show Issue Read More »

2019 Heat Treat Today’s 40 Under 40 Honorable Mention

The privilege of unveiling the Heat Treat Today 40 Under 40 Class of 2019 comes with the disappointment that not every one of the nominees could be included in the final count, even though each young, up-and-coming, talented heat treating professional whose name was submitted is making a significant difference in their field. We will be back next year looking for candidates for the 40 Under 40 Class of 2020, and in fact, you can begin the process right now. Click here to nominate the young professional you have in mind who is not listed among the finalists or honorable mentions.

Consider this list a preview:

The 2019 Honorable Mentions

Muto-Andy.2020-SMALL

Andy Muto,
Paulo Heat Treating

Hiram-Martinez

Hiram Martinez,
Inductotherm HWM

Judith-Levermann

Judith Levermann,
SMS Elotherm GmbH

Mitchell-Kaltenbaugh

Mitchell Kaltenbaugh,
Peters’ Heat Treating, Inc.

McLaughlin,-Ryan

Ryan McLaughlin,
McLaughlin Furnace Group

Rassieur, Tee.2020 SMALL

Tee Rassieur,
Paulo Heat Treating

Rassieur, Will.2020 SMALL

William Rassieur,
Sales Leader,
Paulo Heat Treating

Vadims-Geza-cropped

Vadims Geza,
Chief Product Officer,
CENOS LLC

The individuals pictured are those we acknowledge in 2019 with an Honorable Mention for their contribution to their company, their dedication of service to their customers, their commitment to pursue skills and knowledge about their field. You should know that we at Heat Treat Today are rooting for you and have already rolled the names of any qualified Honorable Mentions into the nominations for the Class of 2020.

Heat Treat Today encourages the rest of you to keep your eyes open for young professionals you encounter within your heat treating sphere, especially in the captive heat treatment industry, who deserve recognition and encouragement to stick to the path that will take the industry to greater heights of technology, quality control, standards, and leadership.

2019 Heat Treat Today’s 40 Under 40 Honorable Mention Read More »

Introducing Heat Treat Today’s 40 Under 40 Class of 2019

Heat Treat Today is very pleased to present the 40 Under 40 Class of 2019. These enthusiastic, forward-thinking, skilled professionals are part of the reason the future of this industry is bright. We invite you to click to our newly unveiled page and read how Heat Treat Today’s 2nd class of 40 Under 40  is breaking barriers, saying yes to challenges, resolving the impossible, and reinforcing the culture of hard work and customer service.

Have a young professional in mind who should have been included? The nomination page will remain live to begin receiving submissions for the 40 Under 40 Class of 2020. Do it now!

Print copies of the Heat Treat Today Fall 2019 magazine have already been mailed out—we hear from many of you that you’ve received your issue—and if you’re at ASM’s Heat Treat Show next week, keep an eye out for your complimentary copy in your registration packet, or visit us at Booth #2123 and pick up a copy. This edition features the Class of 2019 40 Under 40, as well as the Honorable Mentions, and many articles pertinent to our industry such as 101 Heat Treat Tips and samplings from our News Chatter feature.

In addition, you can sneak a peek at the digital version of the print edition by clicking here.

Thanks to all those who nominated individuals for this inaugural 40 Under 40 Class of 2019.

Click here for the 2019 Honorable Mentions.

Introducing Heat Treat Today’s 40 Under 40 Class of 2019 Read More »

U.S. Steel Acquires Interest in Arkansas Steel Company, First Step Toward Consolidation

A leading integrated steel producer headquartered in Pittsburgh, Pennsylvania, announced a joint venture partnership agreement under which it has taken the first step toward acquiring an Arkansas-based steel manufacturer.

Big River Steel, which operates a LEED-certified Flex Mill™ in northeast Arkansas, will expand U.S. Steel’s technological capability and geographic presence through this agreement. U.S. Steel has purchased 49.9% ownership interest with a call option to acquire the remaining 50.1% over the next four years.

David B. Burritt, president and CEO of U. S. Steel

The Big River flat-rolled mill has advanced technology that allows it to produce a wide product spectrum, including advanced automotive steels and electrical steels, and provide high-quality products and services to customers in the automotive, energy, construction and agricultural industries. Big River’s recently announced Phase II-A expansion is expected to double the mill’s hot-rolled steel production capacity to 3.3 million tons annually.

“Our new partnership with Big River is designed to accelerate our strategy to offer our customers the ‘best of both’ by bringing together the capabilities of integrated and mini-mill steel production,” said David B. Burritt, president and CEO of U.S. Steel. “Big River operates the most advanced, state-of-the-art and sustainable mill in North America, and our investment would ultimately strengthen our competitive positioning in highly strategic steel-end markets, creating an unmatched value proposition for our stakeholders.”

“We have been investing in leading technology and advanced manufacturing so that we can assemble a portfolio of competitive assets with distinct advantages to serve strategic markets to better position U.S. Steel to be an industry leader in delivering high-quality, value-added products,” added Burritt. “The investment in Big River, coupled with our announced investments at Mon Valley Works and Gary Works, would ultimately position U.S. Steel with three core market-leading, differentiated and technologically advanced assets that will enable us to compete with anyone, anywhere, for generations to come. Each of these locations would be able to focus on the products that each facility is best designed to produce. As an organization, we will be nimbler, more resilient and our teams will be more efficient. Collectively, these actions will help us continue to create long-term value for our stockholders, customers, employees and the communities in which we live and work.”

David Stickler, CEO of Big River Steel

“U. S. Steel’s decision to partner with us through this investment in Big River is a decisive vote of confidence in our company, our vision and our people,” said Dave Stickler, CEO of Big River. “After just over two years of operations, we have built a unique platform that features the most advanced technology in our industry, and the very finest steel technicians in the business. We have always called ourselves a ‘technology company that just happens to make steel.’ In U. S. Steel, we have a likeminded technology-focused partner with an enduring tradition of excellence and a commitment to innovation. We are very excited about the possibility for what we can do together. As the newest steel production facility in North America, I could not be more proud to be partnering with a company started by Andrew Carnegie more than 118 years ago.”

Closing of the transaction is anticipated on October 31, 2019.

U.S. Steel Acquires Interest in Arkansas Steel Company, First Step Toward Consolidation Read More »

Aluminum Giants Progress Toward Merger with EC Approval

An industrial aluminum company headquartered in Atlanta, Georgia, recently received approval of its proposed acquisition of an Ohio-based aluminum rolled products producer, which would increase its capacity to provide lightweighting materials for the automotive market.

The European Commission announced approval for Novelis Inc. to acquire Aleris Corporation, conditioned upon the sale of Aleris’ plant in Duffel, Belgium, which produces aluminum for the automotive and specialties markets. Novelis is working expeditiously to market the plant to potential buyers, with the chosen counterparty and the definitive agreement for divestiture subject to European Commission approval.

With this conditional approval in the European Union, as well as a clear path forward for approval in the U.S., Novelis focuses on obtaining approval from the Chinese State Administration for Market Regulation (SAMR).

Steve Fisher, president and CEO, Novelis Inc

“Today’s announcement is another step forward in bringing Novelis and Aleris together, which will benefit our customers, employees, and the aluminum industry as a whole,” said Steve Fisher, president and CEO, Novelis Inc. “Overall, this transaction will strengthen our ability to compete against steel in the automotive market, meet growing customer demand for aluminum, achieve our recycling goals, and bolster our sustainability platform worldwide. In addition, it will further enhance our strategic position in Asia and diversify our overall product portfolio.”

The company expects to close the transaction by January 21, 2020, the outside date under the merger agreement.

Aluminum Giants Progress Toward Merger with EC Approval Read More »

Intelligent Cooling System Improves Operations for Alloy Manufacturer: A Case Study

Gary Burdardt, market development manager with Frigel North America

There’s only one constant about technology. It’s always evolving—revealing new innovations and opportunities. And as these new technologies come to light, heat treating operations have new opportunities to reduce cost, increase efficiency, and ensure consistent, optimized part quality, regardless of the job parameters. With the introduction of new process cooling technologies to the heat-treating market, previously unexplored systems become viable solutions for unanswered operating challenges.

When a tempered alloy manufacturer faced strict job requirements that demanded capabilities outside the competences of traditional technologies, a modular process cooling systems designer and manufacturer based in Italy with a North American operation located in East Dundee, Illinois, proposed a process cooling system that addressed key problem areas, while ensuring top system performance. As a result, the company was able to document operational cost savings of over $80,000 per year.

Gary Burdardt, market development manager with Frigel North America, is the author of this case study.


The Need for a Better Cooling Solution

Located on the East Coast, the manufacturer needed to find an alternative process cooling solution for its vacuum furnace cooling operation. It had been using air-cooled chillers, but the costs of continuous operation were too high. Operating as a batch furnace, the heat load of this particular application was specified to be approximately 200 tons, and process cooling water temperature, which was specified at 70°F, presented a significant challenge.

At 70°F, the required temperature was much lower than typical process cooling temperatures. For many vacuum furnace cooling processes, water temperatures can be specified as warm as 100°F for successful heat extraction. Because furnace vessels and resulting materials can reach temperatures as high as 1,300 to 1,700°F, water temperatures of at or near 100°F are able to maintain furnace vessel inner wall temperatures below a maximum (safe) temperature of 300°F. Though the final part temperature can be inconsequential, the batch of product needs to be cooled enough for comfortable handling in downstream operations.

Traditional technologies are capable of maintaining 100°F cooling water year-round. Maintaining temperatures consistently at 70°F is much more difficult. Facing high costs and strict temperature requirements, the manufacturer needed a new process cooling approach.

In this application, the manufacturer identified several process cooling areas of concern that, left unsolved, could jeopardize operations.

First and foremost, process cooling systems needed to adequately reduce heat transmission from the furnace vessel to the ambient environment. In addition, the air-to-water heat exchanger, used for batch cooling inside the chamber, needed to be cooled after the tempering process was complete. Likewise, the diffusion pump, used to evacuate air from the vacuum chamber, as well as the electrical cabinet relied on process cooling for optimized function. If the diffusion pump failed to perform as expected, part quality would be jeopardized, leading to potential contamination and material inconsistencies, and reducing the value of the final product.

Traditional Technology Limitations Explored

Initial investigations into solutions revealed apparent limitations. Traditional process cooling methods were unable to cost-effectively maintain water-cooling temperatures of 70°F. This made finding an alternative solution critical. Three traditional methods were explored:

Evaporative cooling towers

This technology is incapable of achieving consistent temperatures in the 70°F range. Cooling water temperatures are controlled by the wet-bulb temperature, relying on evaporation in ambient air conditions. As a result, they can often only provide 85°F or higher water temperatures to processes year-round. This cooling technology tends to be maintenance-intensive given the reliance on chemical treatment and filtration to maintain water quality. Additionally, evaporative towers consume excessive amounts of water.

Dry fluid coolers

This technology would only be effective in this application when air temperatures were at 55°F or below. Though reducing the need for chemical treatments and eliminating excessive water consumption, this system can only produce water that is typically 10-15 degrees warmer than the dry-bulb temperature, or the ambient air temperature without moisture. As a result, temperature tolerance would be lost during the warmer months. During the colder months, the use of glycol antifreeze solutions is necessary to maintain system functionality, which in many cases requires the use of additional pumping systems and water-to-glycol heat exchangers.

Central chillers

The conventional approach relies on a chilled water system that incorporates chillers to generate 70°F temperatures. This system can be supplemented with a dry fluid cooler if conditions for free cooling were significant enough for payback in three years or less. In many cases, the cold, consistent temperature of the water produced by the chillers is cooler than is necessary for most heat-treating components, leading to increased energy inefficiencies and accrued higher costs.

Faced with the limitations of traditional technologies, the manufacturer turned to an alternative process cooling system for the answer.

Considering an Alternative System

Once traditional methods were thoroughly analyzed, the choice was easy. Providing an alternative solution, the Frigel system design was selected and implemented into the vacuum furnace cooling application.

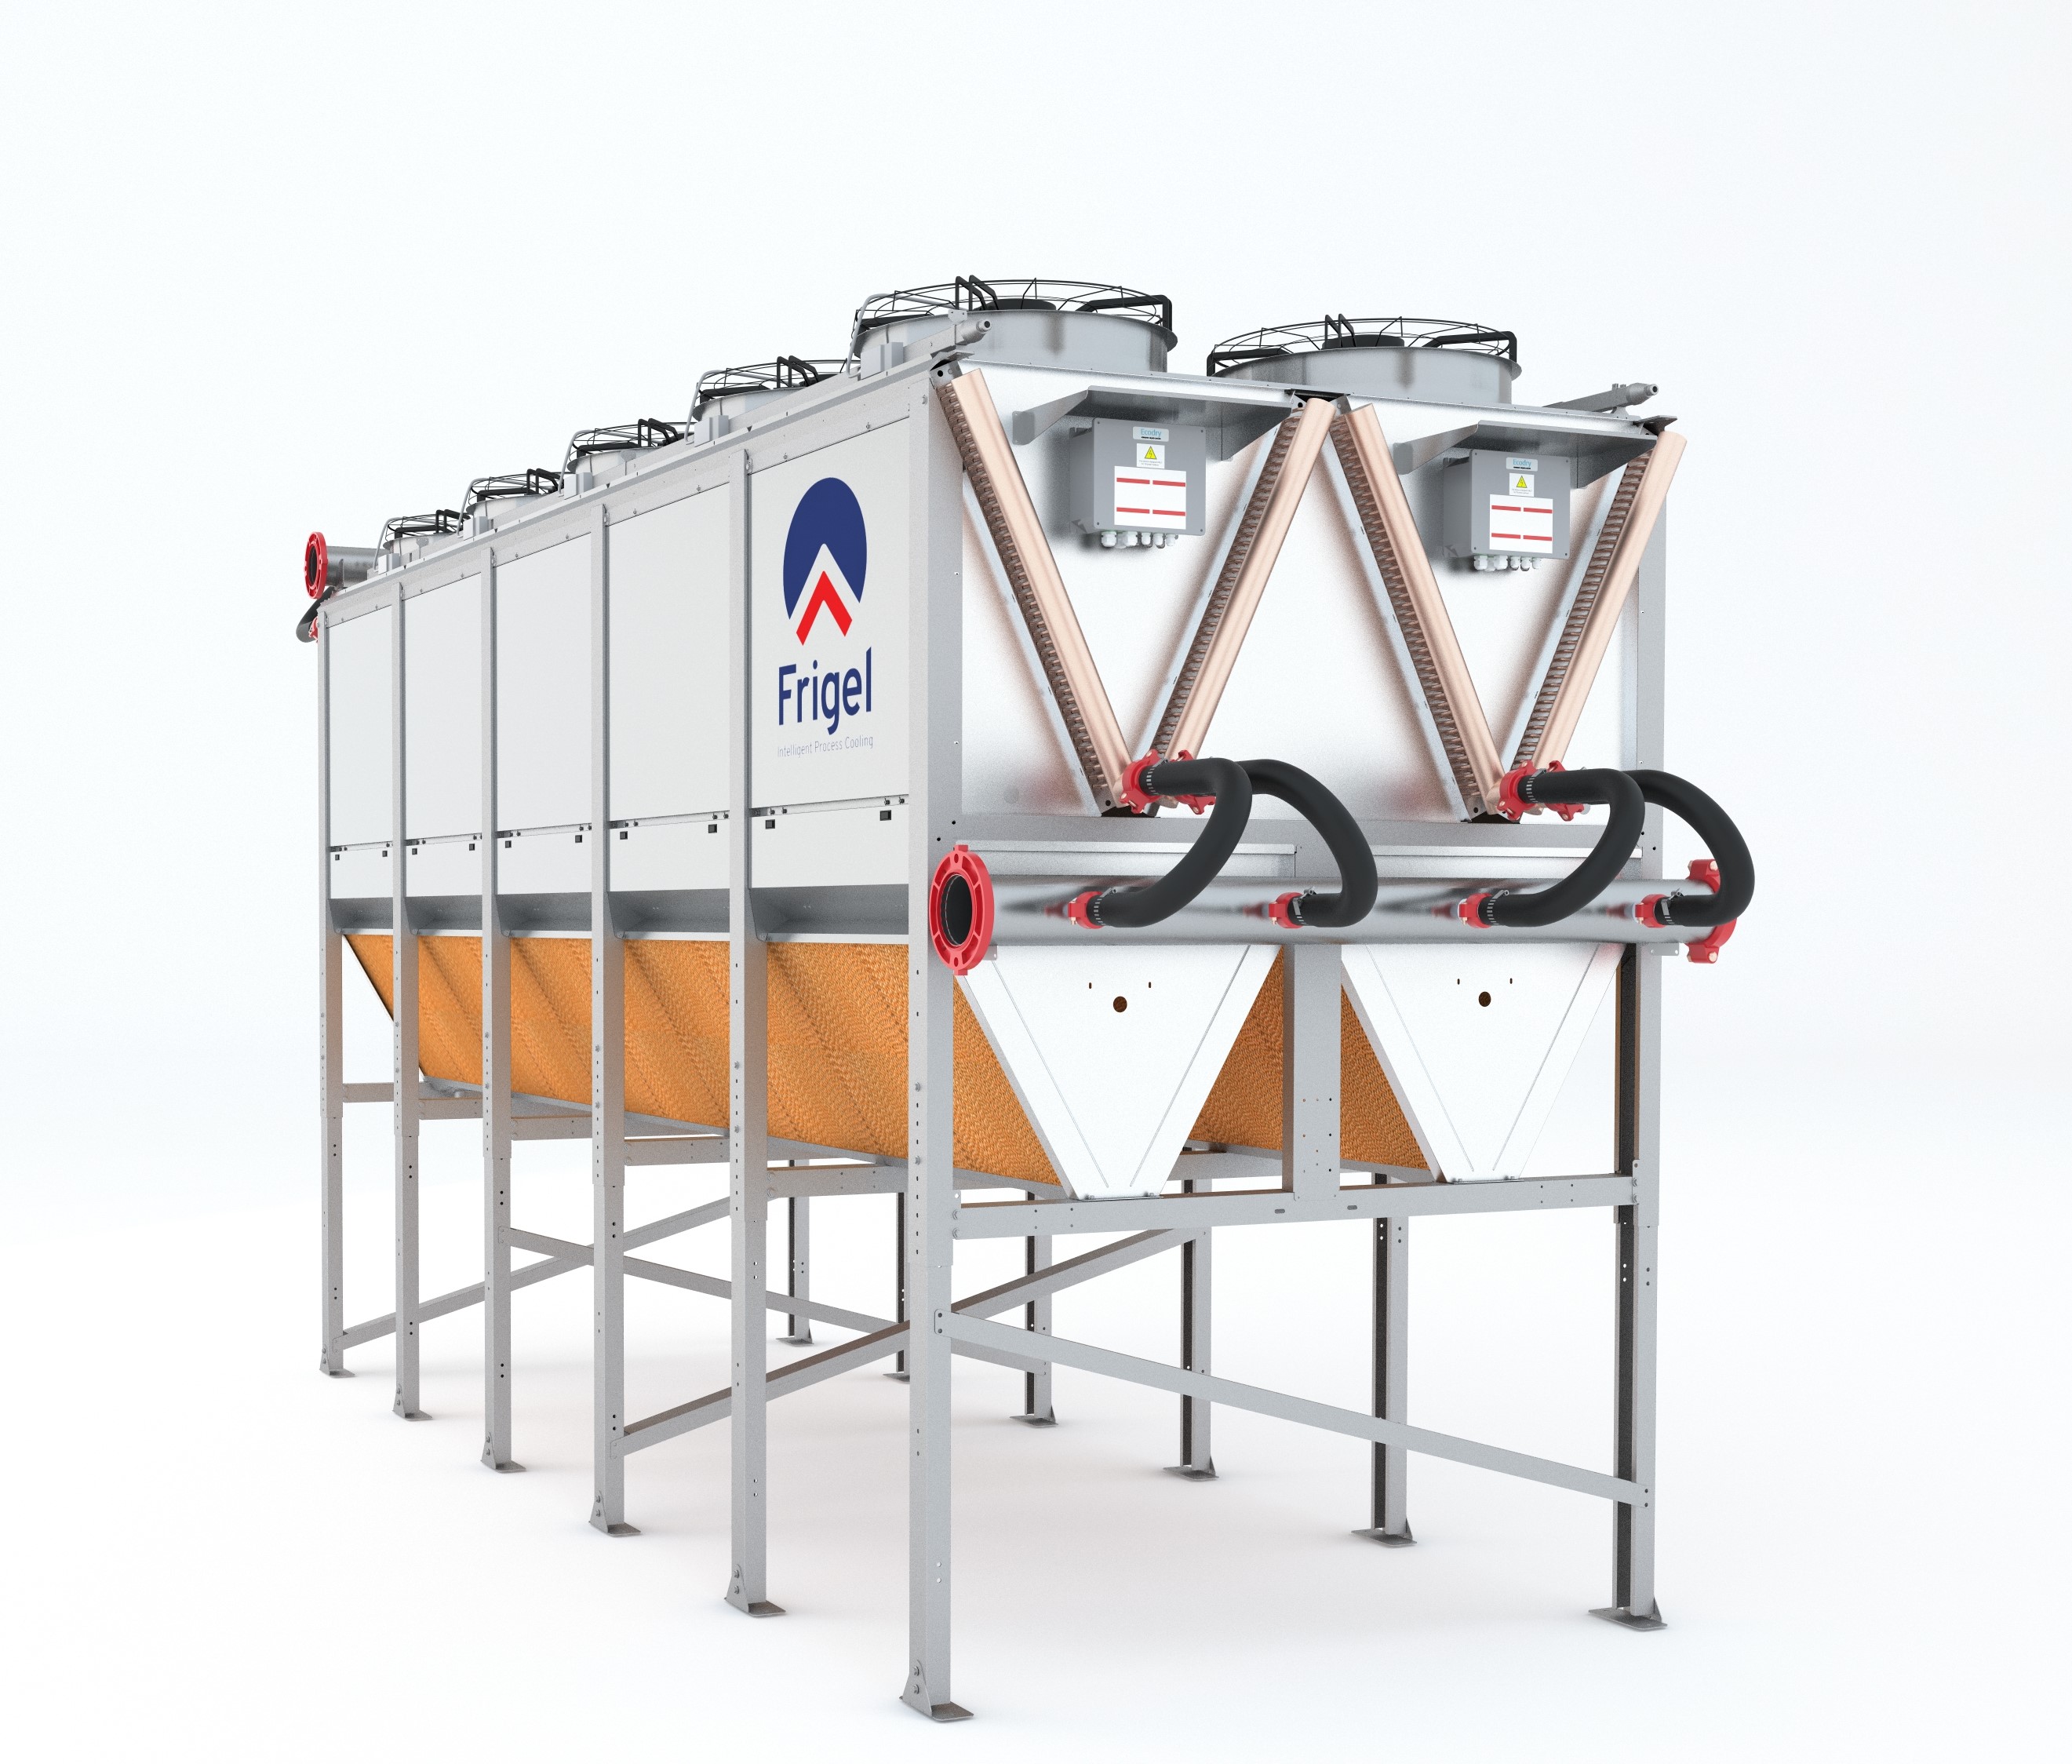
Frigel’s Intelligent Process Cooling systems are designed to create better processes for heat treating operations and provide a unique, flexible solution. The solution combines the use of its internationally patented closed-loop adiabatic fluid cooler with small, dedicated chillers to maximize opportunities for free cooling while ensuring consistent and reliable process cooling temperatures. The closed-loop adiabatic fluid cooler operates outside of the facility, with chillers located near each work cell or process. This approach allows for greater flexibility as individual process cooling needs change.

As a closed-loop system, it requires fewer resources and creates additional opportunities for free cooling capabilities. Water consumption is greatly reduced as opportunities for evaporation are removed. Water consumption is lowered by as much as 95% when compared to an evaporative cooling tower. The closed-loop system also prevents process cooling water from being exposed to the outside air, reducing the need for chemical treatments and additional filtration efforts.

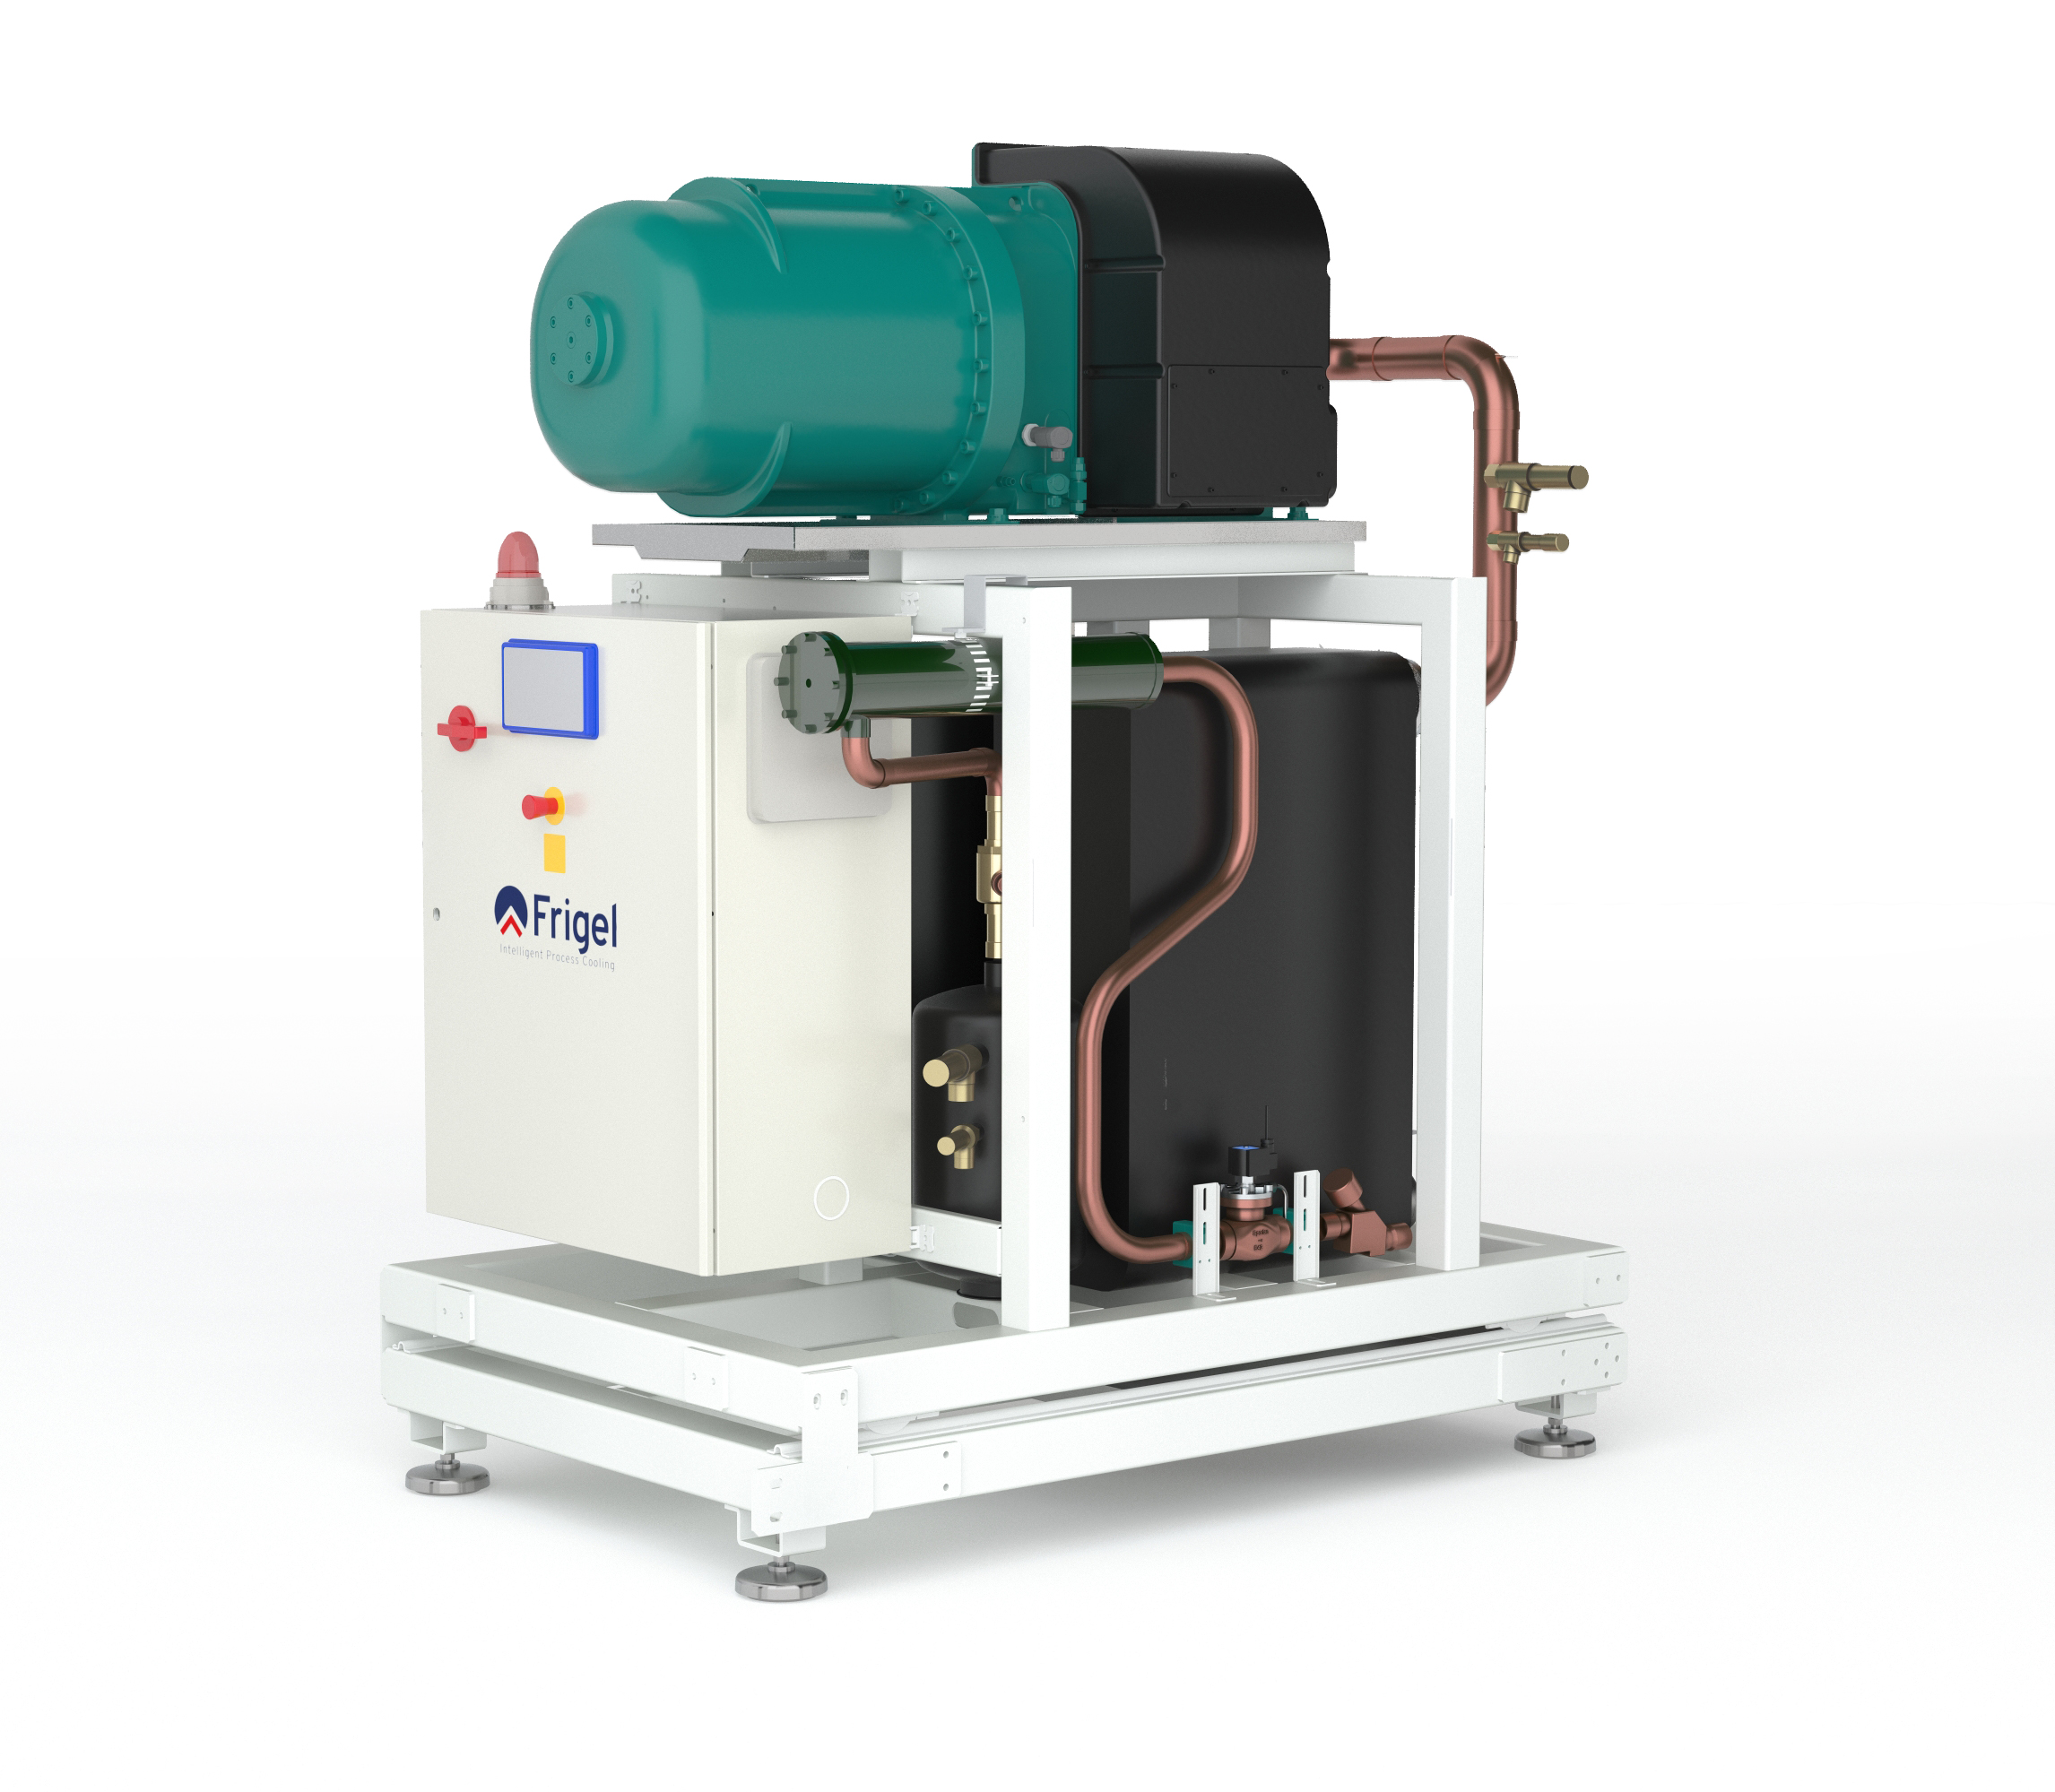
Frigel 3FX chiller

When compared to an evaporative cooling tower, chemical use can be reduced by as much as 40%, appealing to strict municipal water quality regulations while improving system reliability and uptime. Maintenance issues are also drastically reduced in comparison to open-loop systems. Contamination, corrosion, and deposits are all threats to machine performance. By reducing opportunities for cooling coils to interact with moisture, and cooling water exposure to the open air, maintenance-intensive issues are lessened. As a result, production uptime is optimized.

The closed loop-adiabatic cooler system also allows for greater free-cooling opportunities. When ambient conditions are appropriate, localized chillers are bypassed. Instead, heat is transferred to the air via copper tubes in the adiabatic chamber of the fluid cooler, and the cooled water is returned to the furnace vessel. Meanwhile, localized chiller compressors are automatically shut down, saving energy and reducing costs. Working together, the closed-loop adiabatic cooler system and localized chillers are able to provide cooling water temperatures at a wider range of ambient conditions, allowing greater flexibility throughout the heat-treating process.

Additionally, an Intelligent Process Cooling system provides a modular solution. With the fluctuation of job demands and shifting job requirements, the system can expand to fit each unique process cooling need. The use of dedicated chillers allows work cells to be self-contained, reducing disruption and downtime as new process cooling requirements adapt and develop with business growth.

Applying the Intelligent Process Cooling System

At the East Coast manufacturer’s operation, a Frigel Ecodry internationally patented closed-loop adiabatic fluid cooler operates outside the facility. The Ecodry unit is used in combination with dedicated Frigel 3FX water-cooled chillers inside the facility to maximize opportunities for free cooling while ensuring consistent and reliable process cooling temperatures.

At the alloy manufacturer, the Intelligent Process Cooling system installed includes an Ecodry fluid cooler with a patented adiabatic chamber and several water-cooled chillers.

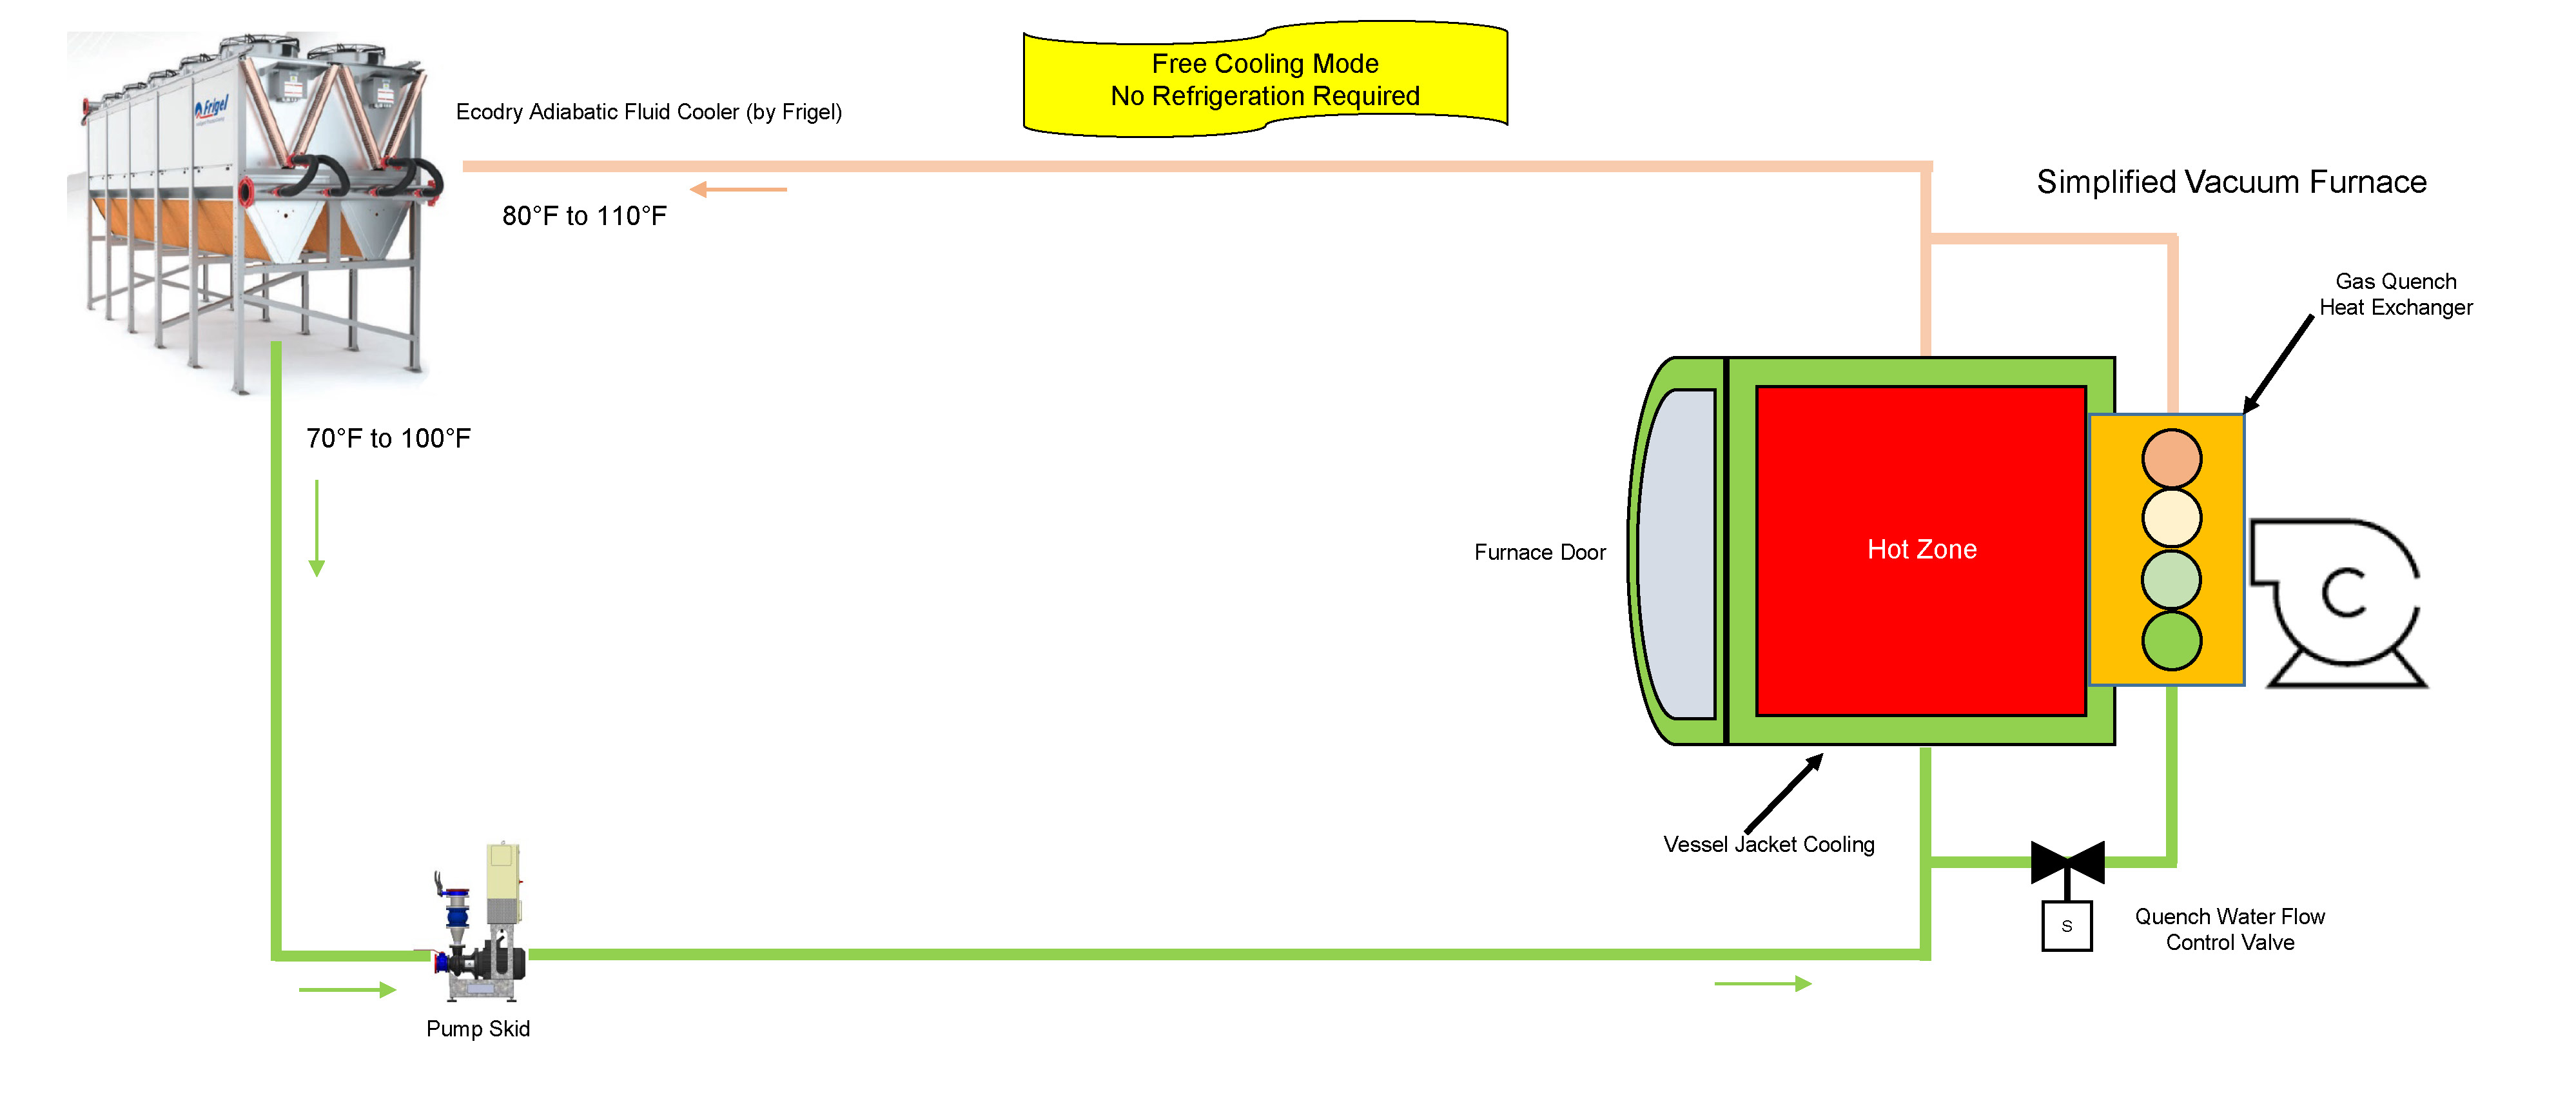
Throughout the year, this system leverages free cooling when ambient conditions permit (see Figure 1). For this manufacturer, the installation location provides ambient temperatures that are quite mild, reducing the necessity for localized chillers from approximately the beginning of October to the end of April. Instead, process cooling water transfers heat to the ambient air via the copper tube and aluminum coils in the adiabatic fluid cooler. Once cooled, water travels to the pump skid, then returns to the furnace vessel where it cools the furnace jacket, furnace door, diffusion pump, and heat exchanger.

Figure 1. The Frigel Intelligent Process Cooling system leveraging free-cooling opportunities.

While the furnace is in processing mode, process cooling water runs between the shells of the vacuum, cooling the inner walls, furnace jacket, furnace door, and diffusion pump. This ensures the furnace exterior maintains a safe temperature and the diffusion pump is able to sustain necessary atmospheric pressure within the furnace vessel. Following the completion of the processing cycle, the quench water flow control valve sends process cooling water to the heat exchanger, decreasing furnace vessel temperatures to the desired temperature for part handling and extraction.

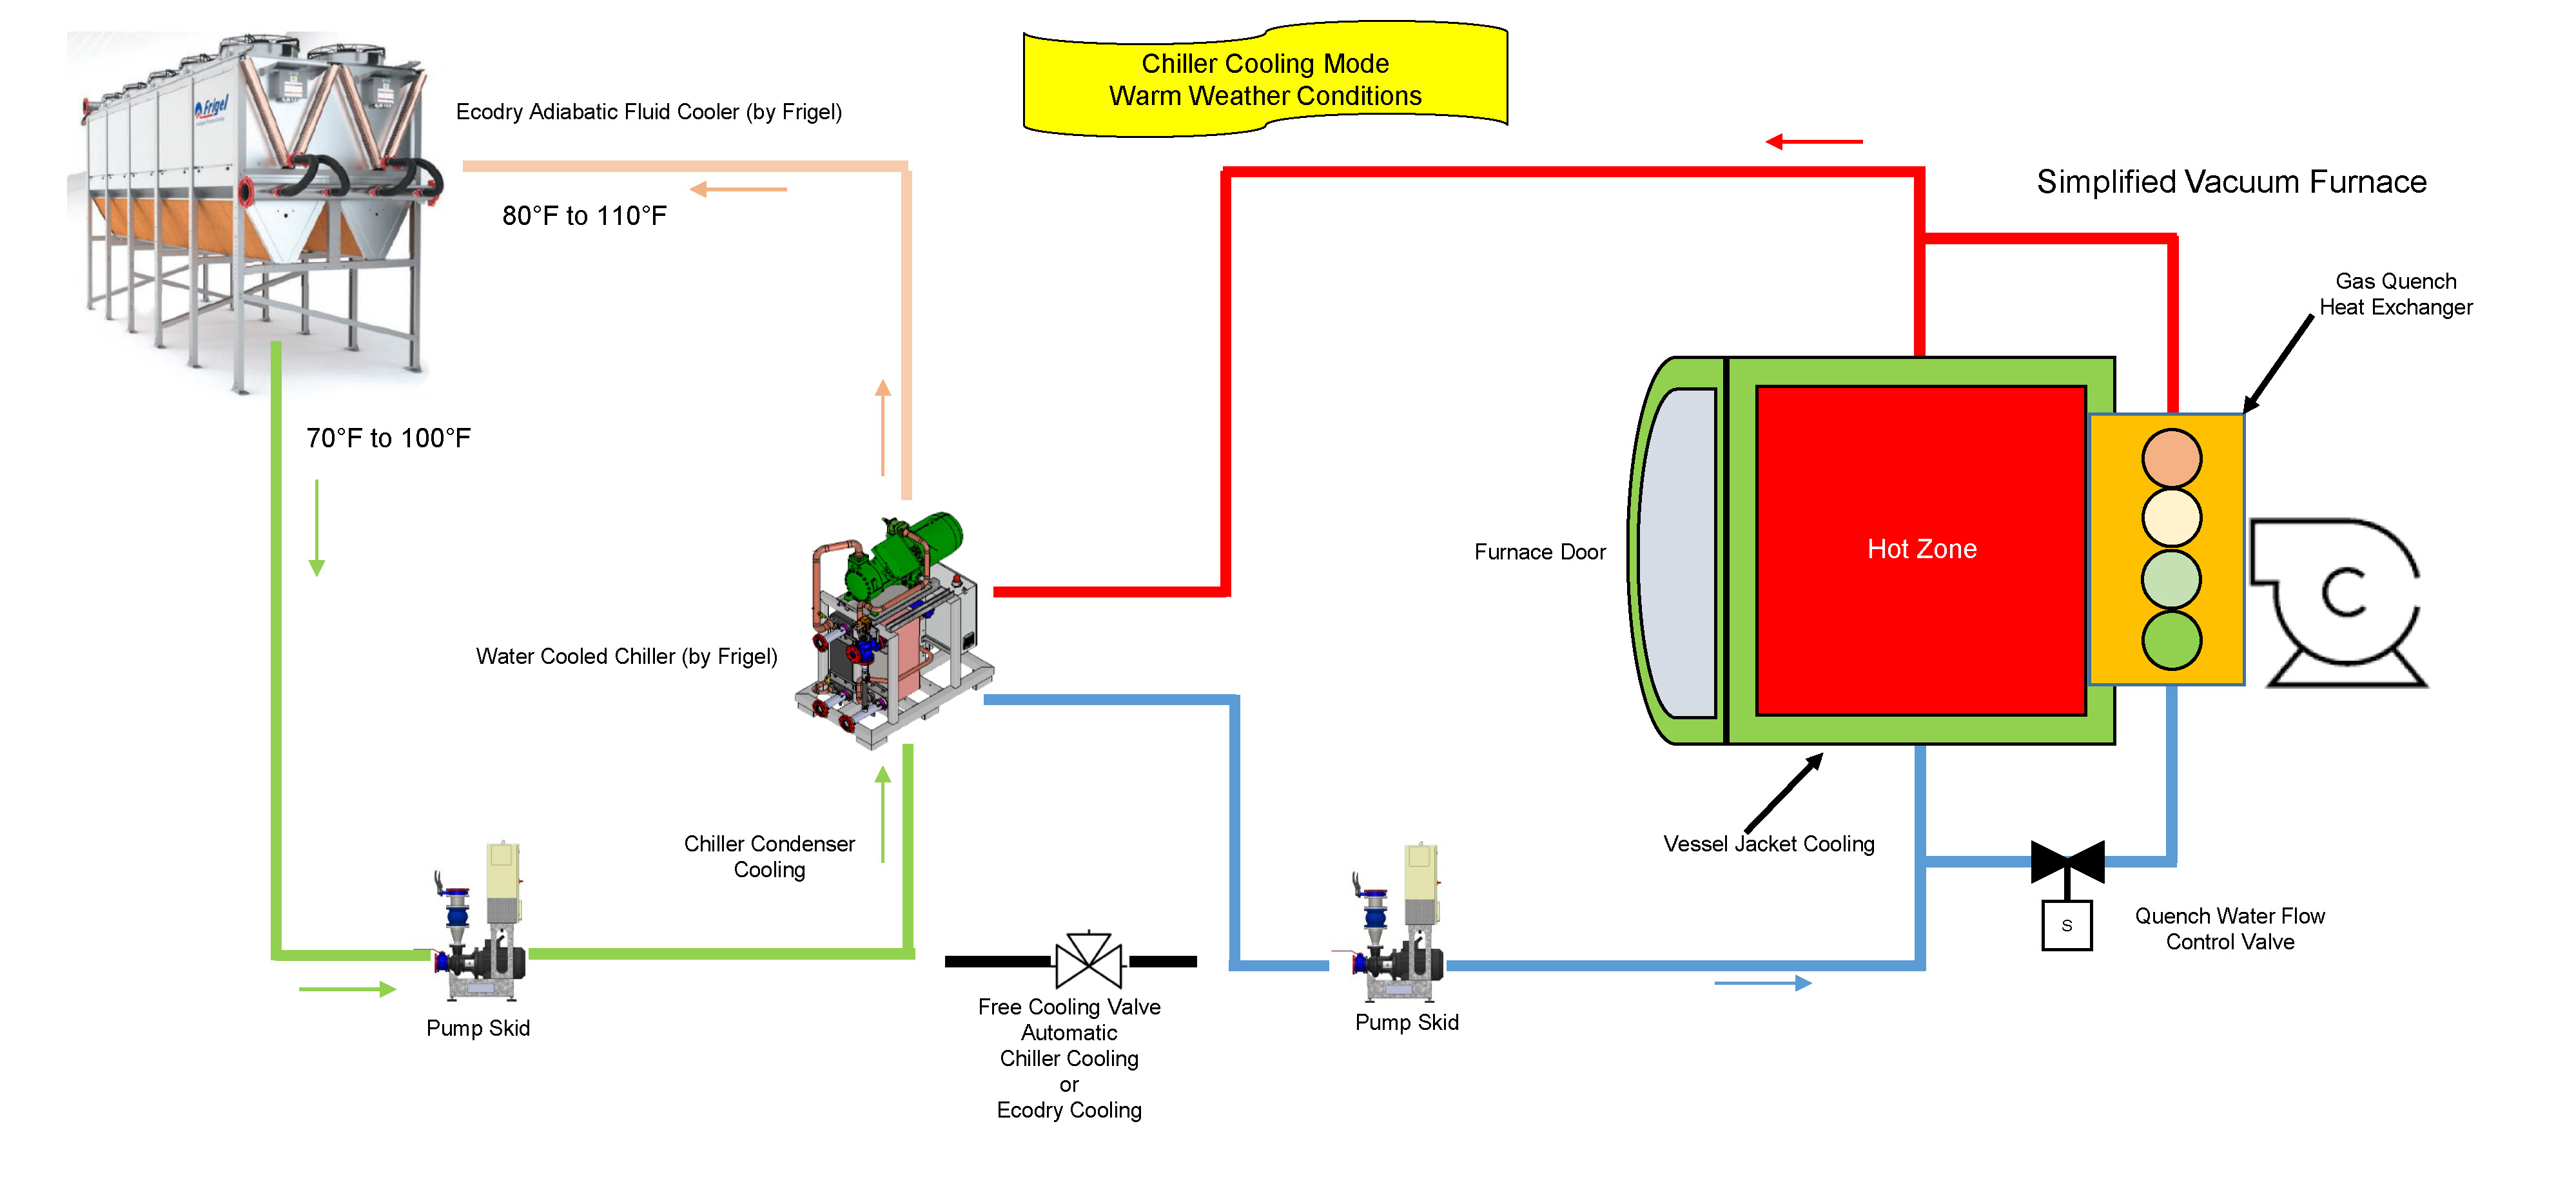
Existing water-cooled chillers supplement the cooling process during the rest of the year when set temperatures can no longer be maintained with the use of free cooling (see Figure 2). When temperatures are at their highest, the water-cooled chillers generate the 70°F coolant and the heat is transferred to the Ecodry loop via the chiller condensers. From there, the chilled water travels to the furnace vessel, cooling the furnace components. Once the water has passed through the process, it returns to the adiabatic fluid cooler, and the water-cooling process begins once again.

Figure 2. The Frigel system leverages chiller cooling mode in warm weather conditions.

If and when ambient temperatures exceed 85°F, the adiabatic chamber of the fluid cooler initiates the spray system to lower incoming air temperatures closer to the wet-bulb temperature. By doing so, the coolant is lowered to a temperature that maintains reliable, efficient operations.

Operational Savings of $80,000 Per Year and More

By leveraging a closed-loop system with an adiabatic chamber, the alloy manufacturer achieved benefits that weren’t possible with traditional technologies. Chiller run time is in the 1,500 hour-per-year range and adiabatic cooling is required less than 400 hours per year. Compared to an evaporative cooling tower and water-cooled chiller system, water use has been reduced by 95% and electrical energy costs have been reduced by 60%. Increased efficiencies and reduced water consumption have resulted in operating costs that are dramatically less than any other system. In total, the plant saves over $80,000 per year with the Frigel system.

For this manufacturer, an alternative solution to traditional process cooling technologies was the only viable option. High costs drove innovation and a need for a better approach. Frigel’s Intelligent Process Cooling system, leveraging the capabilities of a closed-loop adiabatic system and localized water-cooled chillers, allowed for greater operational flexibility while reducing costs and maximizing efficiency—providing the manufacturer with a better process cooling solution.

About the Author

Gary Burgardt, Frigel North America’s market development manager, works closely with prospects and customers to ensure every Frigel process cooling solution delivers measurable results based on each company’s unique processes and business goals. In addition to expertise in Intelligent Process Cooling, Burgardt leverages 30 years of experience in process cooling across a wide range of industries to assist customers at every stage of the planning and buying process.

For more information, visit www.frigel.com.


Intelligent Cooling System Improves Operations for Alloy Manufacturer: A Case Study Read More »

IHEA Economic Report Shows Bright Spots

IHEA 2019 August Credit Movement
Credit Moved Strongly Upwards in August

The monthly Executive Economic Summary, crafted for the member companies of the Industrial Heating Equipment Association (IHEA), showed that the global economy is slowing but there continue to be signs of potential growth as well. All in all, this month’s report was less optimistic than previous reports, but, to quote the report, “At this point, there is data to support whatever mood you choose to be in.”

Five of the eleven indices were trending upward. Among the positive trending indices were new automobile and light truck sales, steel consumption, metal prices, factory orders, and the credit managers index. All of these indices push upward.

IHEA 2019 August PMI
Purchasing Managers Index continues to slide

Six of the indices went south, including the Purchasing Managers Index (PMI),  capacity utilization, and durable goods. Housing and transportation also were soft.

According to IHEA’s economist, much of what we are seeing is a global slowing of the manufacturing economy. Citing concerns like Brexit and the looming trade war with China, the report indicates that much of what the global manufacturing economy is experiencing is bigger than the U.S.

The 12-page monthly report is comprised of an introductory summary page, and then one page each to analyze, in detail, eleven indices chosen specifically for their impact on the thermal processing market.

Anne Goyer, Executive Director of IHEA

To receive a copy of the report, contact Anne Goyer, Executive Director of IHEA.

IHEA Economic Report Shows Bright Spots Read More »

A Dozen Quick Heat Treat News Items to Keep You Current

A Dozen Quick Heat Treat News Items to Keep You Current

Heat Treat Today offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry.

Personnel and Company Chatter

  • Gregory Scheuring has joined Solar Atmospheres of Western PA (SAWPA) as plant metallurgist.
  • Precise Metal Products, a leading manufacturer of complex metal assemblies for many of the world’s largest aerospace and defense companies, was recently acquired by an affiliate of Staple Street Capital in partnership with Thompson Capital Partners.
  • A leading global provider of high-performance specialty materials used in thermal management, emission control, batteries, specialty filtration and fire protection applications recently signed a definitive agreement to acquire the assets of Shenyang JiuQing Dongxiang Glass Product Co. Ltd, a leading provider of high-performance specialty fibers in China. Unifrax, which is backed by Clearlake Capital Group, L.P., acquired the assets from the Li family.
  • American Axle & Manufacturing Holdings, Inc. (AAM) recently announced that it has entered into a definitive agreement to sell its U.S. iron casting operations to funds managed by Gamut Capital Management. Across 10 manufacturing facilities, Grede develops, manufactures, assembles and supplies ductile, gray, and specialty iron castings and machined components for automotive, commercial vehicle and industrial markets.  AAM will retain its El Carmen, Mexico, iron casting operations, which will continue to provide significant vertical integration benefits to AAM, while also continuing to serve external customers in Mexico and other global markets.
  • Magnetic Specialties, Inc. (MSI), which manufactures heavy-duty power supplies for the electric furnace industry, specialty transformers and reactors for various industries, and smaller specialty transformers for the electrical and electronic industry, announced the construction of a new 4,800 SF addition to its plant space in Telford, Pennsylvania. Mike Afflerbach, President of MSI, said the building addition is essential for added efficiencies and expansion of useable floor space in his main manufacturing building.

  • A nitriding system was supplied to Hydro Extrusion Solutions in Trzcianka, Poland, to address the company’s need for improved process performance and more accurate control of nitriding results. The Nitrex N-EXT 812 nitriding system provided by Nitrex Metals replaces a decommissioned nitrider that was phased out several years ago due to extrusion die failures and inconsistent metallurgical results.
  • An electric annealing furnace was manufactured for a major manufacturer by Gasbarre Thermal Processing Systems. This is the second 48″ wide belt furnace Gasbarre has supplied this company. The furnace came equipped with 3 heating zones that can heat up to 1200 degrees Fahrenheit.
  • A 350°F (177°C) clean room oven, No. 1048, being used for the final cure of hardcoated optical lenses, was recently supplied by Grieve to the customer at its facility.
  • A leading manufacturer of calcium phosphate materials used for medical devices recently purchased a furnace from L&L Special Furnace Co, Inc. This is the fifth Model GS1714 furnace shipped to this company. The calcium phosphate powder is sintered in the furnace at a temperature of about 2,200°F (1,204°C).
  • ALD recently delivered a SyncroTherm system to a well-known institute in the Beijing area, the first for the Chinese market.

  • Novelis’ Terre Haute, Indiana, facility recently celebrated 60 years with its 160 employees. Current and retired employees, their families and community leaders attended the celebration.
  • The Industrial Heating Equipment Association’s (IHEA) Infrared Equipment Division (IRED) recently completed revisions to its popular Infrared Process Heating Handbook for Industrial Applications. This quick introduction to the many applications of infrared heating in industrial processes has been updated to include new technical information, additional application examples, and new case studies.


Heat Treat Today is pleased to join in the announcements of growth and achievement throughout the industry by highlighting them here on our News Chatter page. Please send any information you feel may be of interest to manufacturers with in-house heat treat departments especially in the aerospace, automotive, medical, and energy sectors to the editor at editor@heattreattoday.com

A Dozen Quick Heat Treat News Items to Keep You Current Read More »

Automaker Fuels San Antonio Assembly Plant with $391 Million New Investment

A multinational automaker recently announced an investment of $391 million at its San Antonio truck assembly plant in response to customer demand and to expand multi-vehicle production capabilities by introducing various advanced manufacturing technologies.

Toyota’s announcement comes as part of a broader commitment from the company to invest $13 billion in its U.S. operations over five years through 2021. Toyota Texas also commits to continue funding local workforce development. As part of Toyota’s commitment to help San Antonio’s workforce and education, Alamo Promise will receive a $500,000 donation from Toyota Texas over a five-year period. Alamo Promise’s mission is to end poverty, enhance economic and social mobility and meet workforce demands throughout the city.

Separately, Aisin AW, a supplier to Toyota Texas and other automakers, announced that it will invest $400 million and bring 900 new jobs to a future facility in nearby Cibolo, TX.

Chris Reynolds, Toyota Motor North America chief administrative officer of manufacturing and corporate resources

“We’ve been in the U.S. for more than 60 years, creating a tremendous value chain in this country and creating an extensive footprint in the Alamo City since 2003,” said Chris Reynolds, Toyota Motor North America chief administrative officer of manufacturing and corporate resources. “With 10 U.S. plants, 1,500-strong dealer network, an extensive supply chain, and other operations, we directly and indirectly employ over 475,000 Americans and are committed to investing here.”

“The Lone Star State continues to build on its reputation as a manufacturing powerhouse thanks to investments from innovative companies like Toyota and Aisin AW,” said Governor Greg Abbott. “Their combined new investment of nearly $800 million in the San Antonio area is a testament to Texas’ unrivaled workforce and commitment to creating an environment where businesses can thrive free from the heavy hand of government regulation and over-taxation. I am grateful to Toyota and Aisin AW for bringing more jobs to the Lone Star State and I look forward to growing our already strong partnership.”

This is Toyota’s third investment at its San Antonio truck plant which assembles the full-size Tundra and mid-size Tacoma pickup trucks.


Main photo credit: Toyota

Automaker Fuels San Antonio Assembly Plant with $391 Million New Investment Read More »