Eurometal S.A., member of the Eko-Świat Group and manufacturer of highly processed aluminum products, purchased an aluminum coil annealing atmosphere furnace. This solution will be used by the only rolling mill currently in operation in Poland, with Polish-owned equity.
The new equipment is the third for this client from the parent company of North American furnace manufacturer, SECO/VACUUM. The SECO/WARWICK solution will consist of a Vortex® furnace for aluminum coil annealing and will be equipped with an external cooling system. The by-pass cooler will be for cooling under a nitrogen atmosphere, and SeCoil® — the control and simulation software — enables aluminum coil manufacturers to significantly shorten the production cycle.
The SECO/WARWICK solution will be used by the only rolling mill currently in operation in Poland, with Polish-owned equity.
As a result, Eurometal S.A. will benefit from the system in energy saving, increased productivity, and improved the surface quality of the processed coils. The key feature of the system is the increased heat-transfer coefficient, due to directing the atmosphere at a high speed simultaneously on both sides of the coil.
Sławomir Woźniak CEO SECO/WARWICK Source: secowarwick.com
Aluminum is an extremely plastic and light material, resistant to corrosion and many chemicals. Precise parameters of aluminum sheet enable its use for manufacturing various types of products and semi-finished mill products. Aluminum is used in the aerospace, automotive and machinery industries. Also, the construction sector uses aluminum sheet made with alloys characterized by high corrosion resistance and good forming ability. The ship building industry has also many applications for this alloy. Aluminum is certainly a crucial material for the development of many sectors.
"Aluminum replaces other conventional metals, in particular in modern state-of-the art products," commented Jarosław Śliwakowski, Eurometal S.A. "The automotive industry, with the dynamically growing share of aluminum, is at the forefront of replacing conventional metals[. . .] We have chosen Vortex due to the shortening of the total process time, even heating of the batch and reduced natural gas, protective atmosphere and electricity consumption in comparison with the products proposed by the competition."
"Eurometal has been our partner for many years," said Sławomir Woźniak, CEO of SECO/WARWICK Group. "[. . . ] From the very beginning, our cooperation has been based on trust. We always focus on approaching each order individually. We create a flexible system design, custom-made for the needs of a particular rolling mill."
"SLM"? You may have heard of AM -- additive manufacturing -- but how about selective laser melting, SLM? Stay on top of your acronyms with this overview on how vacuum furnaces and SLM, an AM technology, can increase fatigue performance of parts.
In this Technical Tuesday, the author not only shares what this technology can do, but also the results of SLM in laboratory studies and research at the University of Parma.
"When SLM processes are conducted within a vacuum heat process, it is possible to make more detailed components which have more intricate forms. Crucially, this means that they will often perform better than would otherwise be the case when they are in use."
A US manufacturer of radio frequency (RF) and microwave components recently received a small box furnace reaching 2300°F. This furnace will be used for precision heating to anneal their parts before milling.
The small load custom box furnace was delivered by Lucifer Furnaces. It is their furnace model HL7-A12 with a 6” x 6” x 12” chamber and is insulated with a combined 5” hot face insulating firebrick and cold face mineral wool backup. This box furnace is complete with a cast hearth plate to protect the floor insulation and heats with easy-to-replace coiled heating elements in cast assemblies for easy replacement, while still being built at the same quality as larger models.
Controls include a Honeywell digital time proportioning temperature controller and a TP1 Soak Timer which starts when the furnace reaches setpoint temperature and shuts off the elements at the end of the heating cycle. A door safety switch automatically disengages power to the elements when the door is opened. This furnace is part of Lucifer’s standard, general purpose, series 7000 box furnace line, a line which helps bring clients’ heat treating in-house and gain control over work flow and product quality.
A U.S. independent chemical distributor and manufacturer of surface treatment chemistry announced that it has acquired the assets of Arbortech, an Illinois-based manufacturer of patented membrane equipment. With the acquisition, the manufacturer becomes the first chemical company to offer specialty cleaning formulations designed specifically for the patented membrane separation technology.
This refers to Hubbard-Hall's Aquaease Infinity® platform, a complete cleaning and reclaim system, designed to save manufacturers up to 35% on chemistry while also reducing process defects.
The acquisition solidifies a longstanding relationship between the two companies. Aquaease Infinity® was the first line of degreasers and cleaners co-developed for use with Arbortech’s unique membrane technology. Unlike standard industrial cleaners/degreasers, the Aquaease Infinity® cleaning compounds fully pass-through Arbortech’s membranes, leaving soils and oils trapped. This guarantees the reclaimed cleaner is "as new" and remains a full-strength product. Customers report retaining 98% of their cleaning baths and reducing waste and total cleaning costs by 35% or more.
This development in cleaning technology gives customers more control over their cleaning processes, extends the life of the cleaning bath and reduces downtime and waste. The system is offered as a lease to reduce upfront capital costs.
"Hubbard-Hall is on a mission to help customers get better results with less chemistry, process complexity and, ultimately, lower costs,” noted Molly Kellogg, CEO of Hubbard-Hall. "By adding the Arbortech team and technology to the Hubbard-Hall product offering, we plan to aggressively expand the Infinity platform to industrial manufacturers seeking to improve quality while reducing cost and environmental impact."
Ray Graffia, Jr. Founder and President Arbortech
"It’s nice to be part of the Hubbard-Hall family," added Ray Graffia, Jr., founder and president of Arbortech. "This is a like-minded company that shares our value for sustainability and can expand the use of membrane technology into new areas. It just makes tremendous sense."
Bill Egerstaffer will join the Hubbard-Hall staff as equipment engineer. With 25 years of experience at Arbortech, Egerstaffer is responsible for the fabrication, installation, maintenance and design of the membrane units as well as programming the controllers. He will report to Mike Frechette, Business Development Manager.
The acquisition brings together more than 200 years of combined experience and a shared vision to create sustainable business.
An optical laboratory in northeastern USA will receive a second floor-standing box furnace for heat-treating ceramics and optics used in the medical field.
The L&L Special Furnace Company model XLE 3636 has an effective work zone of 34” wide by 30” high by 32” deep. It features a double pivot horizontal door. The ceramic hearth is supported on lightweight castable piers. A series of heat shields are included to ensure a safe case temperature while at operating temperatures. The furnace is designed for use with inert blanketing gas for atmosphere control to minimize oxidization. A manual flow panel with regulator and flow meter is included.
A Eurotherm program control and high limit safety are standard. The furnace has a stack light mounted to the top of the control panel for an audible and visual indication of current furnace status. Solid-state relays drive the furnace, which is NFPA86 compliant. Startup and training packages are also included to help the customer set up the furnace and process.
Explore how the shift from globalization to regionalization is making a positive impact for businesses in the manufacturing industry, not only in Europe and the U.S., but also in Mexico, especially in the aerospace and automotive sectors.
This article, written by Humberto Ramos Fernández, founder and CEO of HT-MX, first appeared in Heat TreatToday’s May 2021 Induction print edition. Find the digital upload and other past editions here.
Humberto Ramos Fernández Founder and CEO HT-MX
It’s an interesting time in the Mexican industrial ecosystem, to say the least. It has, of course, been a very abnormal couple of years for obvious reasons such as the pandemic, the oil and gas crisis, and even the aerospace industry problems with the Boeing 737 MAX. However, these events have triggered a shift in the global manufacturing industry away from globalization and into regionalization. US and European OEM companies are realizing that having their suppliers in the same region as opposed to halfway around the world is becoming more and more important as it lowers risks, allows for faster technology transfer, and reduces project implementation times and costs.
All of this helps move the T-MEC* zone, especially Mexico, into a strategic position to take advantage of these opportunities. A heavily industrialized country with over 30 years of complex manufacturing experience, Mexico has the infrastructure to attract and develop its industries during these global manufacturing shifts. A strong workforce including engineers and trained technical population, an industrial culture, and an actively developing supply chain are important components that contribute to Mexico’s strengths.
Regional manufacturing clusters have been developing in Mexico for several decades now, but more recently, there has been a strong push for a fuller, more complete high tech supply chain.
Mexico has several manufacturing hubs with a wide range of industries served, including the aerospace manufacturing hub located in Chihuahua (200 miles south of the Texas border) and the automotive manufacturing hub located in the El Bajío region, both of which have been continuously strengthening their supply chains with certified suppliers.
We must be ready, but we also must be able to communicate that we are ready to help these international companies successfully launch their Mexican initiatives, even in the shape of a joint venture between Mexican and international companies.
These hubs started as maquiladoras, or plants doing simple, but labor-intensive jobs and have slowly evolved into full-blown high-tech operations where aerospace assemblies (landing gears, engines, interiors, bodies, etc.) or fully assembled cars, roll out of the lines on a daily basis. Such evolution, where OEM and Tier 1 operations became more complex, forced the supply chain to start upgrading. This is still happening at the moment, but major gaps in the operation, such as heat treat and surface finish, are now fulfilled. Today you can have a part machined, heat treated, HIPed, surface finished, painted, and assembled without leaving Chihuahua.
A more complete regional manufacturing chain allows our customers to transfer more production lines or develop more products, thus benefiting the entire manufacturing industry. And we, along with many others, are here to help fill historically empty gaps in the manufacturing chain.
So, as a Tier 1 and Tier 2 supplier, secondary process companies in Mexico must be ready to help transition to regional manufacturing; and this transition must be as painless as possible. We must be ready, but we also must be able to communicate that we are ready to help these international companies successfully launch their Mexican initiatives, even in the shape of a joint venture between Mexican and international companies.
The ability to accompany the customer through the development of the manufacturing process, from machining, to heat treating, HIPing, surface finishing, assemblies and to even helping locate local suppliers for complementary processes, is key for Mexican market success.
It is indeed an interesting time here in Mexico. Come and take a look.
*Editor’s note: T-MEC is also known as the United States-Mexico-Canada Agreement or USMCA in the U.S. and in Canada as CUSMA.
About the Author: Humberto Ramos Fernández is a mechanical engineer with a master’s degree in Science and Technology Commercialization. He has over 14 years of industrial experience and is the founder and current CEO of HT-MX, which specializes in NADCAP-certified controlled atmosphere heat treatments for the aerospace, automotive and oil and gas industries. As of 2020, HT-MX became Latin America’s only hot isostatic pressing (HIPing) supplier. With customers ranging from OEMs to Tier 3, Mr. Ramos has ample experience in developing specific, high complexity secondary processes to the highest requirements.
Neota Product Solutions, a custom metal injection molding (MIM) manufacturer located in Loveland, Colorado, has recently partnered with a North American heat treat supplier to develop an exclusive sintering partnership.
Jason Osborne President Neota Product Solutions Source: LinkedIn
Neota provides comprehensive MIM solutions from early-stage prototyping to full scale manufacturing. The manufacturer and Solar Atmospheres of Western PA (SAWPA) developed a sintering thermal profile that densifies complex geometric shapes and also controls shrinkage. This results in a solid and strong metallic part, with near 100% density, while maintaining the tight tolerances that are required in their precision components.
Collaborating with Solar Manufacturing, the vacuum furnace production arm of the Solar family, SAWPA recently acquired a vacuum furnace which is engineered to handle MIM processing. The furnace has a work zone of 36” x 36” x 48” and a load capacity of 3,000 pounds.
Robert (Bob) Hill, FASM President Solar Atmospheres of Western PA
"Solar has been a class-act organization and has been instrumental in the aggressive growth of our company," stated Jason Osborne, president of Neota.
"We have sincerely enjoyed our relationship with the Neota team," added Bob Hill, president of Solar Atmospheres of Western PA stated. "As MIM industry experts, they know what they ultimately want in a finished part. As vacuum thermal processing specialists, we know how to achieve their high temperature processing parameters while not damaging our state-of-the-art vacuum equipment. Investing in our customer’s needs, ultimately results in lasting mutual relationships which become a successful endeavor for both parties."
Alternatives to internal combustion engines have long dominated conversations in the automotive world. Discover why induction heating is playing a vital role in the production of the electric vehicle in this Technical Tuesday original content article written by Michael Zaharof, regional sales and marketing manager at Inductoheat.
This article first appeared inHeat TreatToday's May 2021 Induction print edition. Find the digital upload and other past editions here.
Michael Zaharof Regional Sales and Marketing Manager Inductoheat
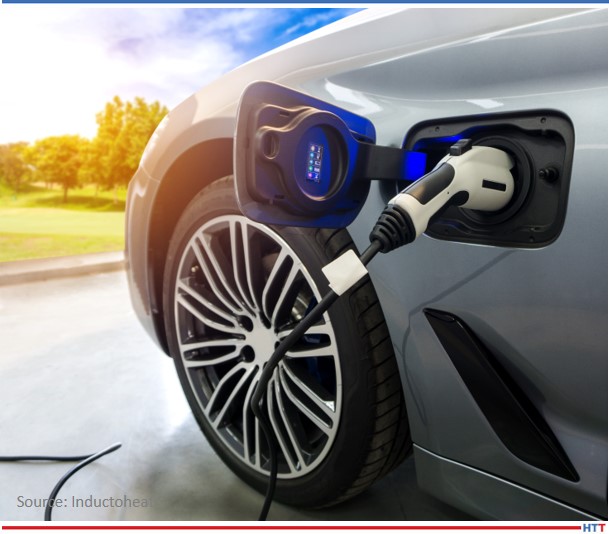
The electric vehicle (EV) sector of the automotive market is gaining momentum. Government mandates, fuel economy standards, and increasing consumer interest are all driving the push to EV. Some platforms are further along in the process, while others are just starting to enter the space. Many new ideas and vehicle configurations are being developed to deliver the best alternative to the internal combustion engine (ICE).
This industry is learning about the best way to configure drive mechanisms and control acceleration, be it a centralized power source operating a driveline or multiple motors powering different areas of the vehicle. Heat treating the necessary components properly to impart enough strength for the much higher torque delivery is more critical than ever compared to the traditional performance characteristics of those equipped on a standard ICE platform. Induction heating plays a critical role in the EV market as it permits several unique benefits over other thermal processing methods. Whether it is heat treating, shrink fitting, curing, or surface hardening, induction heating is one technology that has already proven itself to be beneficial for the manufacturing of electric vehicles.
Deeper Case Depth
Because of the almost instant torque delivery and fast acceleration characteristics of electric motors, EV driveline components must be more robust to handle the added torsional stresses. Combined with the need for wear resistance and fatigue life, these components must be heat treated to deliver these critical properties.
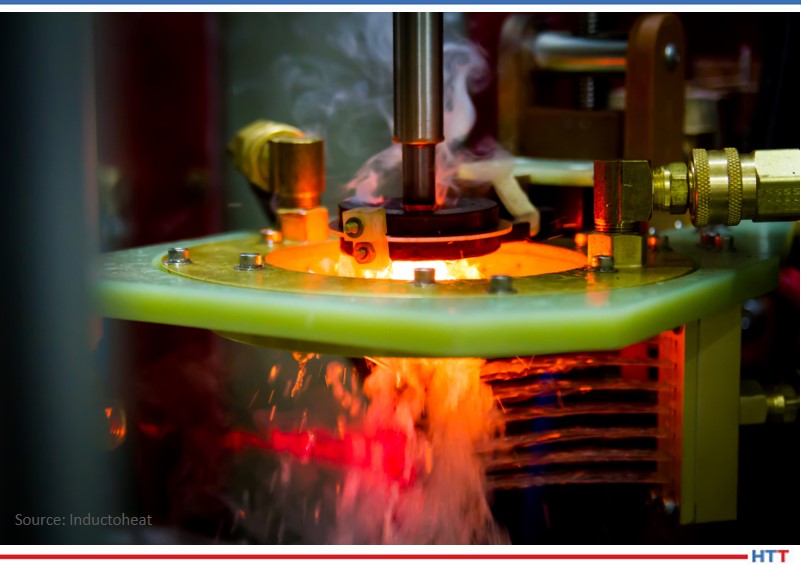
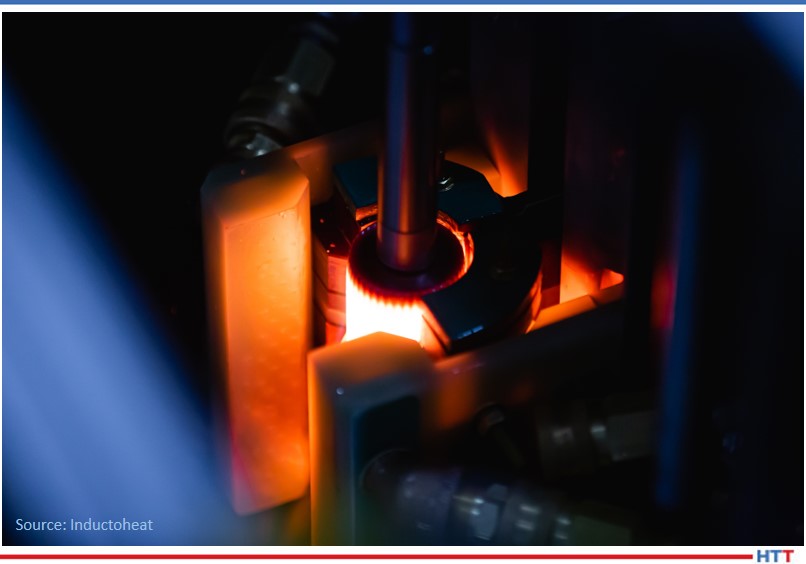
Induction heat treating of an automotive pinion
The powertrain components generally made with carbon steels (such as bearings, raceways, constant velocity joints, pinions, shafts, hubs, and gears), must be sufficiently hardened to provide enough strength, while remaining ductile enough to prevent premature failure. Induction hardening is ideal in many cases since it can deliver deeper hardened case depths, if desired, compared to other methods like conventional gas carburizing and nitriding. These alternative heat treatment methods must rely on diffusion mechanisms associated with a sustained and prolonged environment.
Alternatively, induction utilizes subsurface heating through electromagnetic current applied to a specified and customizable area achieving the desired casehardened depths. Because heat can be applied quickly to the specific area, electromagnetic induction produces much less metallurgical distortion compared to thermochemical methods that rely on through-heating and diffusion processes at high temperatures, which in some instances eliminates or diminishes the need for post heat treatment grinding or machining.
Fast & Flexible
The speed of manufacturing is an essential factor in keeping a supply chain moving and having enough product available. Many manufacturers and automotive part suppliers have adopted just in time (JIT) manufacturing workflow methodologies to increase speed to market while controlling production and inventory costs.
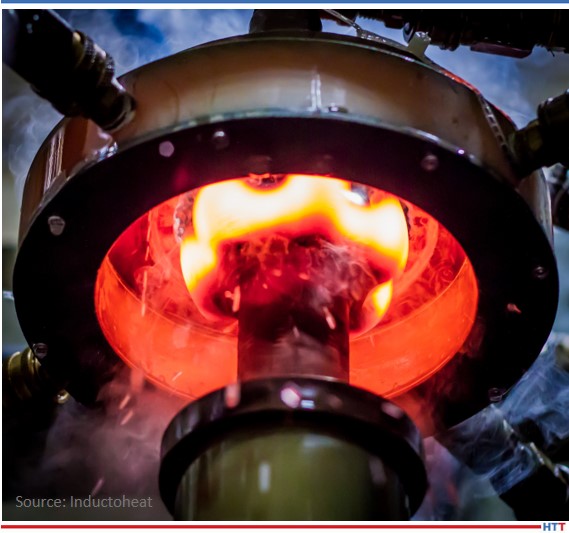
Induction heating of an automotive CV inner race
Induction hardening allows for parts to be processed as needed and in a way that does not require hours of processing time in contrast to alternative thermochemical heat treating methods. Because of the constant flow of individual parts and almost instantaneous time to heat, production can be incremental and consistent while still being flexible enough to adjust rates as needed. This flexibility and lean approach to inventory management can be more difficult when batches of parts are being processed together.
Also, because material distortion after induction heat treatment can be much lower, as previously mentioned, post-heat-treatment manufacturing operations can be reduced or eliminated.
Single Part Flow: Repeatability & Traceability
Part process flow is an important consideration when repeatability and traceability become essential, like in automotive manufacturing. When multiple parts are being processed simultaneously, such as in a furnace operation, individual parts cannot be validated while the heat treatment is in process. The part variability in batch operations can be impacted by part spacing, location in the furnace, gas concentration, and temperature from one batch to another.
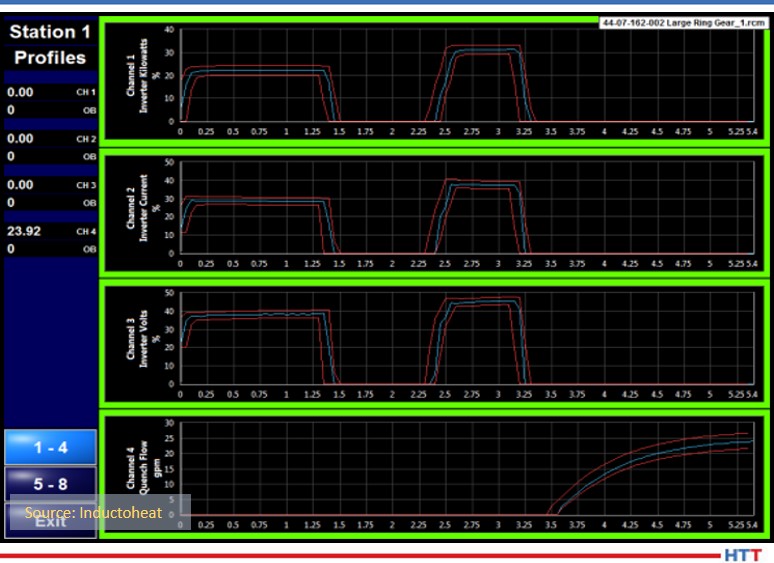
Many quality standards require tight control of the heating process and data collection during heat treatment to ensure that acceptable parts are being made. Induction heating allows precise monitoring and real-time evaluation of each stage in the heat treat process. The parameters of the process cycle – such as quench temperature, quench concentration percentage, quench pressure, quench flow, energy used, frequency, and part rotation – are just some of the points that can be analyzed by today’s sophisticated sensors and signature monitoring systems.
Signature monitoring system by Inductoheat
Some of the more advanced monitoring systems, like those offered by Inductoheat, allow the user to “teach” the induction machine what a “good part” signature looks like as all the data points of the process are plotted throughout the cycle and compared to established acceptable limits. As the process runs in production, the user can validate that all critical factors being monitored are in specification.
In the event of an issue in which one or more points are out of specification, the part will be rejected by the quality system. The cycle processing data can be instantly associated with each heattreated piece through part marking/reading or the most suitable such as radio frequency identification (RFID),u for example, for storage and later use by the manufacturer.
Environmentally Friendly
Induction heating uses electricity as its means of heat generation. Other methods such as carburizing and different batch heating processes employ gases such as ammonia and other chemicals in conjunction with fossil fuel-powered furnaces. Induction heating is considered a clean and environmentally friendly option for heattreating.
The process uses electrical energy and can quickly cycle through the desired operation and then sit idle until needed again. Most alternative systems require warm-up and cooldown time before and after production runs. In some cases, it is less expensive to keep the furnace running while continuing to burn natural resources and vent exhaust gases into the environment compared to shutting the system down in between uses.
More Efficient
Induction heating is a fast and efficient operation and can be scaled up easily to meet production requirements. Induction heating machines generally take up much less floor space than gas-powered batch furnaces. As mentioned above, they can be operated when needed without lengthy preheat or cooldown sequences.
Induction heating is associated with greater heat intensity, transferring more power directly to the workpiece in a concentrated fashion, compared to most other methods that rely on heating a surrounding environment. Induction coils can be designed to apply the required current density into an exact area of the part to be heat-treated instead of heating the entire piece.
The induction process is also more efficient as energy output can be controlled precisely to apply only the necessary power needed to obtain the desired temperature profiles at the desired production rate.
Induction heating of an automotive input shaft
Conclusion
Induction heating is a proven and environmentally friendly process that has a long history of precision and repeatability. The ability to heat parts quickly and more effectively is why many companies have opted for induction heating over other heat treat methods. Some other popular applications utilizing induction heating employed in EV production include shrink fitting, brazing, bonding, curing, battery production, stamping, forming, and varnishing of motor components.
Induction heating technologies are also dynamic, changing every day to meet new requirements and manufacturing goals. The use of multiple power levels and frequencies from a single induction inverter is one such innovation changing how some parts are being engineered and produced. Induction heating is a solution that will continue to assist the automotive manufacturing industry for years to come.
About the Author: Michael Zaharof is a regional sales and marketing manager at Inductoheat in Madison Heights, Michigan. He has been with the company since 2011 and has worked in the sales application, digital media marketing and outside sales departments. Michael has a bachelor of computer science in Information System Security. Michael currently works with customers in several states with their induction heat treating and induction forging needs.




 Eurometal S.A., member of the Eko-Świat Group and manufacturer of highly processed aluminum products, purchased an aluminum coil annealing atmosphere furnace. This solution will be used by the only rolling mill currently in operation in Poland, with Polish-owned equity.




 Explore how the shift from globalization to regionalization is making a positive impact for businesses in the manufacturing industry, not only in Europe and the U.S., but also in Mexico, especially in the aerospace and automotive sectors.