In preparation for Heat Treat Radio episode #87 (looking at ways to increase productivity especially with data management) coming tomorrow, take a look at these three articles from the Heat Treat Today files to get you warmed up. No matter where you are in the digitization process, you'll find something to help here.
Taking the step from a paper and whiteboard system to a computerized system is a big jump. Maybe that's been done, maybe that's still being considered. Already digital? Then there are always efficiency and organization improvements to run an even more productive shop. Lastly, what does the future hold? How best to stay on the cutting edge of data management?
Read this original content article for guidance and encouragement in the use of digital systems for the heat treat shop.
1. Heat Treat Control Panel: Best Practices in Digital Data Collection, Storage, Validation
Heat Treat Today asked six heat treat industry experts a controls-related question, "As a heat treat industry control expert, what do you see as some of the best practices when it comes to digital data collection and storage and/or validation of instrumentation precision?" This article gives reasons for why you collect and store data and some helpful ideas for making sure those records are preserved.
Contact us with your Reader Feedback!
One expert had this to say: "electronic data must be validated for precision; checked; and calibrated periodically as defined by internal procedures or customer standards. Data must be protected from alteration, and have specific accuracy and precision."
Read the entire piece to get even more perspectives.
2. Heat Treat Case Study: Predicative Maintenance with Digital Thyristor Power Control
Tony Busch Sales Application Engineer Control Concepts
Tony Busch, sales application engineer at Control Concepts, Inc., takes a look at digital maintenance systems. These systems play a part in recording and monitoring data, and they contribute to the overall productivity of the heat treat shop. This article makes a strong case for intelligent controllers.
"Digital power controllers can calculate resistance and provide precise power control. Predictive maintenance is achieved by knowing when an element has reached its useful life. Intelligent power control includes embedded algorithms with teach function to calculate data and predict what is likely to happen next in the life of a heating element," emphasizes Busch.
Find out more about the benefits of digital connectivity here.
3. DUAL PERSPECTIVES: The Heat Treat Shop of 2050
Global ideas emerge in this article, as two men from very different locations, give some thoughts about digitization in the next 20 years or so. Hear from each expert - one representing the European market; one representing the North American market - as they discuss the role of technology, the human element, and heat treating of the future.
Thomas Schneidewind says, "digitization must always remain only a tool, not an end in itself." He reminds readers that importance always must be placed on the human element. Doug Glenn counters with, "For commercial heat treat shops where variability is high and volumes are relatively low, much of the same will be true with less and less human interaction needed."
Explore the rest of the forecast from Thomas Schneidewind, the editor-in-chief of heat processing magazine, and Doug Glenn, the publisher and founder of Heat TreatToday here.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Additive manufacturing (AM) at a commercial scale began about 30 years ago and has expanded well beyond its original scope. As AM becomes increasingly prominent across different industries, heat treaters need to know how to handle AM parts in their shops. Learn about the history of binder jetting AM, the alloys used in this technology that require heat treatment, and what heat treaters should expect for the future.
Read why Animesh Bose of Desktop Metal thinks that binder jetting AM is only going to be used more and more in several heat treating sectors.
This article first appeared in Heat Treat Today’s December 2022 Annual Medical and Energy print edition.
Binder Jetting of Metals: Origins
Animesh Bose Vice President of Research & Development Desktop Metal Source: LinkedIn
Additive manufacturing (AM) at a commercial scale began about 30 years ago and has expanded well beyond its original scope. At the beginning, rapid prototyping (RP) was the name for the burgeoning technology; it emerged in the 1990s to bridge the gap between the need for quickly produced prototypes for manufacturers, not just plastic replicas. Rapid tooling (RT) of metal tooling parts joined RP R&D at this time as the research frontier for materials engineers. The current name for these technologies stands at “additive manufacturing,” or AM, though the popular terminology is simply “3D printing.”
Polymers
Developments in polymer AM also advanced rapidly with both extrusion-based technology as well as through advancements in Digital Light Processing of photopolymers. Stratasys Ltd., an American-Israeli manufacturer of 3D printers, software, and materials for polymer additive manufacturing as well as 3D-printed parts on-demand, began using a material extrusion-based process with their FFF (fused filament fabrication) technology to print parts, patented in 1989. This worked by feeding coils of polymeric materials though a printer, which would extrude the material through a small, heated chamber where the material would pass through a small orifice to extrude – or print – in a three dimensional design. This method allowed for very fine, hair-like material to print in a precise X ,Y, and Z motion, building layer by layer. Vat polymerization was another polymer AM technology that gained traction and involved photopolymer processing. Both technologies are currently used for polymeric materials. Interestingly, both processes have been adapted and are being used for metal 3D printing.
Metal AM
In 1993, an MIT engineering professor named Emanuel “Ely” M. Sachs – a man who could be considered the father of metal binder jetting technique – along with his colleagues from MIT patented the process of laying fluent, porous materials in layers between 50- to 100-micron thickness to form 3D parts. They were able to do this by spraying an organic binder on each layer of material where they wanted to increase the height of the part to produce a bonded layer in the selected area. This layering is repeated several times before the unbonded powder is removed immediately or after further processing.
One of the biggest advancements in metal AM happened in 2014 when GE Aviation combined multiple parts into one huge, complex design using a laser-based additive manufacturing method called direct metal laser melting. The end result was an airplane fuel nozzle made of 20 parts for the LEAP™ engine. All of AM came into the limelight, and direct metal laser melting – a melt-based technology – just took off.
But there were limitations to this laser process, the main one being cost and special powder requirements to layer and melt to form the part. The process was also technologically intensive and not fast enough for high volume production (as would be necessary for automotive or consumer good-type application).
Binder Jetting Technology
Binder jetting that had been developing in the early 2000s started to gain traction as a non-melt-based process for high volume mass production. Instead of melting the powder material, a binder is used to adhere the powder metal layers where needed. This method of printing results in a more uniform final part microstructure compared to the melt-based processes. ExOne, a binder jet 3D printing company, pursued the binder jetting technology using a license from MIT. In 2015, Desktop Metal was formed, and they focused on high volume mass production by binder jet using their Single Pass Jetting (SPJ™) technology. As binder jet gained traction, other companies entered the market (HP, GE, and Digital Metal). Desktop Metal recently acquired ExOne and efforts at developing standards for the technology are in full swing.
Heat Treating of AM Metals
Stainless Steels
There are two popular types of stainless steel for AM. The first is 17-4 PH, a precipitation-hardened stainless steel, which I like to call an “all purpose” stainless steel. When heat treated, one can achieve varying levels of strength, hardness, and elongation; and since it’s stainless steel it has a reasonable corrosion resistance. The aging treatments are already well-established – for example, H900, H1100, etc. The other popular grade is 316L, a non-heat treatable grade used in the food industry among others. Now, most stainless steels have chromium and nickel in decent amounts, so companies have developed a grade which is called “nickel-free stainless steel” for applications where people might be allergic to nickel. This class of alloy is also heat treatable. There are many more stainless steel grades that are being developed by the binder jet process.
Low Alloy Steels
Many low alloy steels are used in AM. For example, 4140 and 4340 have various, small amounts of alloying elements. These low alloy steels also need to be heat treated.
Tool Steels
Again, most tool steels are heat treatable. One of the most popular grades is H13; it is a tool steel that is heat treatable and can achieve fairly high hardness. It’s used for dies and other types of tooling.
Then, there is a category of tool steels known as A2 and D2; those are steels in which the strength can be changed through heat treatment.
Metal Alloys with Binder Jetting
There are also non-steel alloys that are used in binder jetting and require heat treatment. One example is nickel-based alloys, which fall in the broad category of super alloys. With some of these alloys, a heat treater would solutionize the part by taking it to a high temperature (950-1000°C), hold it for 60 minutes, and then quench in water, high pressure gas, or (in some instances) in air. The part then undergoes an aging treatment for several hours, depending on part thickness.
Additionally, there is a class of copper alloys with small amounts of zirconium and chromium that is heat treatable. These alloys have lower thermal and electrical conductivity compared to pure copper but have an advantage of higher strength and hardness over pure copper, which is very soft and malleable. For example, in applications that require additional strength and hardness compared to copper, the copper zirconium-chromium-based alloys may be appropriate since their strength and hardness can be increased by heat treatment.
This is just an introduction to the many alloys that have been used in binder jetting that need heat treatment.
Future of Binder Jet and Heat Treat
While heat treaters know about AM in the medical and aerospace industries, AM will likely gain more traction in the automotive industry. Presently, these are relatively small parts, but you will begin to see larger components coming from AM; one of the things to be aware of is that AM can create organic shapes, including all kinds of twisted and complex metal geometries. To ensure that these organic shapes do not distort or droop, larger parts must be well-supported. The development of a software known as Live Sinter™ by Desktop Metal offers the possibility of negatively distorting a complex shaped part (in the green state) so that after sintering, the part shrinks and distorts to eventually provide the desired complex shape at the end. This allows for the possibility of sintering parts either with minimal or without any support structures.
Heat treaters can also anticipate high volume AM production. This is one of the major focuses for binder jet engineers – to reduce costs for most automotive parts – as it will make AM very appealing to this cost-conscious industry.
Finally, optimizing sintering processes and related equipment for AM parts will result in meeting the production demands of the industry, and this will lead to AM parts being seen in heat treat shops more regularly. It would not be a stretch to consider (since there are heat treatments where gas atmosphere quenching at high pressures is possible), that the complete heat treatment cycle may be performed in the same furnace.
About the Author: Animesh Bose is the vice president of Research & Development at Desktop Metal, where he is responsible for building out the company’s palette of materials that can be used to print quality parts. He has been involved in the area of powder metallurgy and particulate materials (PM) for more than thirty years.
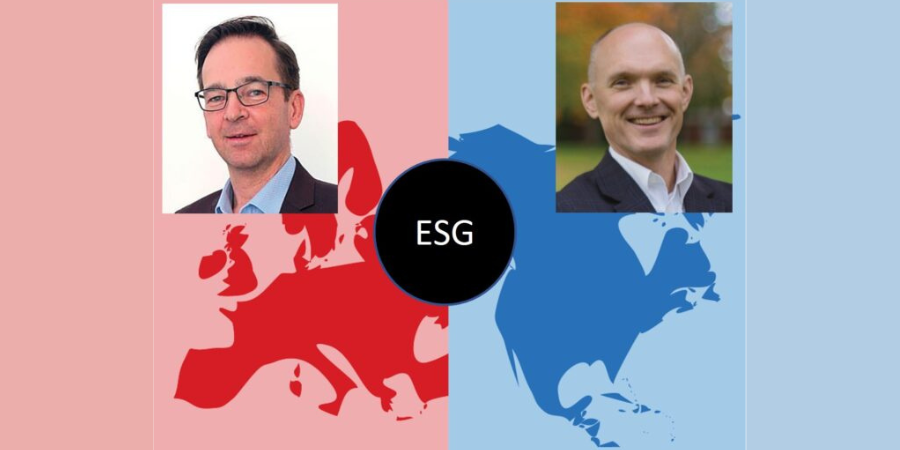
Changes are inevitable, but the world today is changing so rapidly that it’s constantly keeping us on our toes. Do two men from different parts of the world, both with significant experience within the heat treating community, have vastly different perspectives on the happenings in the heat treat industry?
We want to find out, so we asked a question that focuses on the world of heat treating to Thomas Schneidewind, the editor-in-chief ofheat processing magazine, and Doug Glenn, the publisher and founder ofHeat TreatToday. The question: How does government policy regarding ESG in the U.S. and nuclear power initiatives in Europe impact in-house heat treaters?
Thomas’s expertise lies in the European market while Doug’s resides in the North American market. We will feature their responses in each print magazine. Will their views align? Time will tell. Enjoy this fourth installment of an ongoing column. This column was first published in Heat TreatToday’sNovember2022 Vacuumprint edition.
How does government policy regarding ESG in the U.S. and nuclear power initiatives in Europe impact in-house heat treaters?
Thomas Schneidewind, Editor-in-Chief, heat processing magazine
Thomas Schneidewind Editor-in-Chief heat processing Magazine
The energy crisis paralyzes Europe. The European Union has been arguing for a long time about which energy is green. Finally, the European Commission classified both nuclear energy and gas-fired power plants as green energy production. This was a compromise between France and Germany in the discussion about the taxonomy that regulates in which energy sources investments should be made. Today, environmental associations are suing against this compromise, considering neither nuclear energy nor gas-fired power plants to be green energy.
Contact us with your Reader Feedback!
However, the discussion is long outdated. The Russian war of aggression on Ukraine has changed energy policy. Many nuclear power plants in France are at a standstill. Germany no longer receives gas from Russia, and the sabotage of the Nord Stream 1 and 2 pipelines is a politically motivated attack on the European energy market. Today, Europe is suffering from a major energy crisis. There has never been such a crisis in the energy sector in Europe since the Second World War. There is too little energy on the European market. At the moment, the focus is on security of supply.
This crisis threatens the existence of energy-intensive companies such as heat treatment shops. The hardening industry is also coming under pressure because it cannot pay the high electricity and gas prices. Entrepreneurs must find short-term solutions to cushion the cost shock, and ensure the survival of their business -with a view to the long-term goal of decarbonization. Because in the future, process heat must be CO2 free. A clear trend in this context is the switch from gas-heated industrial furnaces to electrically heated systems, whether resistance heating or induction. Managers must face these diverse issues today and respond quickly
Experts and practitioners will be talking about sustainability, materials, processes, and innovations in heat treatment at several events this fall. For example, in October, after a two-year pandemic break, the Hardening Congress (HK) was finally held again in Cologne. Here, too, the energy crisis was a dominant topic. We are talking about the future of Europe which must compete with the U.S. Many investment decisions are being put on hold because the uncertainty in Europe is currently too large. Europe, but especially Germany, faces a new recession.
Doug Glenn, Publisher, Heat Treat Today
Doug Glenn Publisher and Founder Heat TreatToday
Tremendously. A distinctive mark of the U.S. is that we’ve trusted the Market – what Adam Smith called the “Invisible Hand.” We haven’t believed that economies need to be planned or managed; attempts to manage or plan an economy result in more damage than good. We’ve believed that if proper natural or biblical law guardrails are established and enforced, the economy would run itself, self-adjusting as necessary. Today, many have lost faith in the Market. Instead, we put our faith in political processes and political leaders to handle the economy. Because we’ve lost faith in the Market, questions such as the one we’re addressing today make sense to ask. Government policy should have nothing to say about the type of energy we use, the people we hire, or the ideals we hold. Nonetheless, that is NOT the world we live in, so let’s address the question.
Nuclear Power Initiatives
This is really not an initiative; it is more of a “de-initiative” – a closing down of nuclear power plants in Europe (except France) – and the incentive to do so is not economic. According to those who know, nuclear is the cheapest, most reliable form of energy, vastly less expensive than “renewables.” So, in the hands of the Market, nuclear and natural gas generation power plants would win the day. Nuclear is being abandoned for purely political reasons. The effect on heat treaters and all other consumers of electricity: higher prices for energy, either in the form of explicitly higher prices per BTU or higher taxes to incentivize more expensive “renewable” energy sources.
Environmental, Societal, and Governance
As far as ESG goes, government policies in these areas will only increase the cost of doing business.
ONE of the three categories represents an area where the government might have a right to be heard: environmental. But even there, government’s scope is vastly overplayed – that is, if you have faith in the Market! Societal and governance are recent (non-economic) constructs being forced on businesses, NOT for the benefit of the end-consumer, but for the benefit of a vocal minority who believe the world should be a certain way and are using government policies to make it so.
For in-house and commercial heat treaters, ESG pressures and government recommendations or policies will raise the cost of doing business and ultimately the cost of the final product for consumers with very little measurable benefit for anyone. For in-house and commercial heat treaters, ESG pressures and government recommendations or policies will raise the cost of doing business and ultimately the cost of the final product for consumers with very little measurable benefit for anyone.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
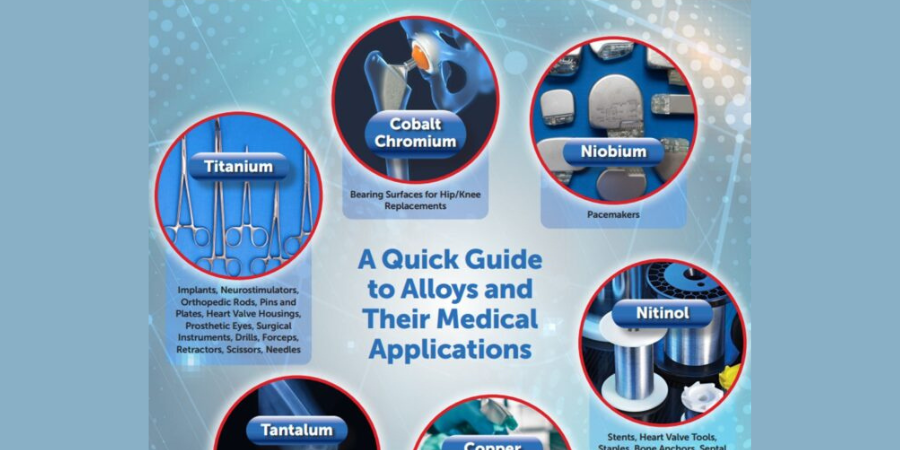
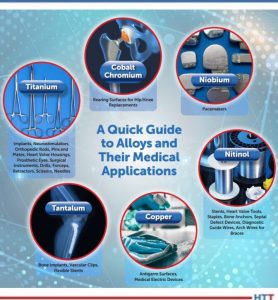
Do you know what are the most popular alloys in the medical market? What are their applications? This medical alloys reference graphic gives a quick overview of alloys and their specialized uses in the medical industry.
Ask average people walking along the street what metal/alloy comes to mind when they think of medical uses - things like hip and shoulder joints, the orthodontia their kids might wear, the forceps used to remove stitches - they might come up with the answer "titanium." While this certainly is correct, there are lots of other metals and metal alloys that are used in the medical industry. They probably wouldn't answer "nitinol," a titanium alloy. Nitinol is actually used in the aforementioned braces! Nitinol can be found in other things too: stents, staples, septal defect devices, etc. Take a look at the graphic to see what all these alloys, in fact, can do; you might be surprised!
Such important implements, devices, and components that are used in and on the human body need to be durable and reliable. These medical pieces can improve the quality of life (to put it mildly) or actually save a life (to put it dramatically). Some of these alloys are actually used in and around the heart and blood vessel system! Only the best of the best will do to make up these medical items; lives are literally preserved and saved with them.
What alloys have you found in medical applications? Maybe you have experience with a loved one or yourself incorporating one of these medical pieces in your life? Are you a heat treater involved in the making of these products? Let Heat Treat Today know in the Reader Feedback.
Download the full graphic by clicking the image below.
Boeing landed an order for 100 787 Dreamliners from United Airlines. Plans are in place to purchase 100 737 MAX jets, too. Both the 787 and 737 are known to have at least 20% better fuel efficiency than the aircrafts they are to replace.
The deal is the largest 787 order in Boeing's history. The 787 is listed from $248 to $338 million, but it's normal for airlines to negotiate significant discounts. With this acquisition, United Airlines hopes to expand with more international flights.
Boeing will begin deliveries of the Dreamliners in 2024.
Read more and watch a video about the new orders here.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Peter Zawistowski Managing Director SECO/VACUUM TECHNOLOGIES, USA Source: secowarwick.com
An electric vehicle manufacturer will move the heat treatment of their prototype gears in-house with a vacuum furnace. The company expects new product development to accelerate.
SECO/VACUUM, a SECO/WARWICK Group company, will deliver a CaseMaster Evolution (CMe) model with a working hot zone of 16”x16”x24” and a load capacity of 440 lb. The EV maker’s R&D lab will use furnace to low-pressure carburize and oil quench prototype gears. With this expansion, the manufacturer hopes to mitigate scheduling delays encountered when sending their prototype gears out to local commercial heat treatment shops.
“We have a strong partnership together," said Peter Zawistowski, managing director of SECO/VACUUM, "having commissioned a number of highly successful heat treat furnaces that provide a wide variety of processes in their plants across the world."
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Over the last few months, the Metal Treating Institute requested comments from members on how their current business insurance programs have been progressing with property, liability, errors-omissions, commercial auto, and workers compensation. What we learned is this is a huge pain point for most heat treaters of any size.
Contact us with your Reader Feedback!
Many are experiencing cancellation of coverage, refusal to be offered a quote, or large rate increases. The insurance industry is really backing away from writing policies for heat treating companies.
To help heat treaters deal with this huge challenge, the board of trustees of MTI is excited to announce that they have partnered with Precision Manufacturing Insurance Services out of California as the official insurance agency partner for business insurance coverages. They have already written several MTI members’ policies and provided quality coverage with significant savings averaging 35% to 50%.
Precision Manufacturing Insurance Services (PMIS) provides heat treating companies with comprehensive competitive insurance and risk management solutions. They are dedicated to protecting the future of this vital industry. They offer their knowledge, experience, and service to many types of metalworks that put people to work, contribute significantly to the U.S. national GDP, and deliver quality products worldwide.
They know there is nothing cookie-cutter about what a heat treating company does when altering the physical properties of material. That work is precise and custom. With PMIS, your company will get the same type of focused approach with your insurance and risk management plan. Recognized nationwide for their specialization in working with metalworking manufacturers, they’ll provide you with tailored solutions based on your unique risks. Their professional staff is available to support your industry and business.
Source: Precision Manufacturing Insurance
When prospective clients ask why they should partner with PMIS for their insurance and risk management needs, the answer is simple: They are metalworking manufacturing insurance specialists. This is who they are and the only thing they do. They are not a generalist broker who happens to write a few manufacturing accounts. PMIS has written over 1,000 policies for metalworkers — all attributed to their expertise, experience, and longstanding relationships with insurance markets. This enables them to deliver affordable solutions to MTI members that protect property, assets, employees, and reputation, while reducing risk and costs. The following are the types of coverages PMIS can create for you:
Custom Manufacturing Insurance
General Liability Insurance
Property Insurance
Workers’ Compensation
Manufacturers’ Errors and Omissions
Equipment Breakdown
Commercial Auto
To see more details on Precision Manufacturing Insurance Services and the MTI Insurance Program, including a link to request speaking to a PMIS team member about getting a free quote for your company, visit HeatTreat.net and click on the Business Insurance link under the Benefits tab at the top.
If you have any questions or would like more information, feel free to contact Tom Morrison at tom@heattreat.net
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
L&L Special Furnace Co, Inc. announced that they are under new ownership, Specialized Thermal Solutions, Inc. beginning with the new year. The manufacturing company will maintain their operations using L&L's name, with David Cunningham serving as both owner and president.
Gregory Lewicki (pictured above on the left) moved the furnace business to Aston, PA, in 1979. David Cunningham (pictured above on the right) has been with the company since December 2005. Aside from the name change, everything else about L&L Special Furnace Co, Inc., including contact info and email addresses, will remain the same. Specialized Thermal Solutions, Inc. will be absorbing all of L&L Special Furnace Co., Inc.’s order history and will continue to service any of its products.
The company will continue focusing on high-end, specialty industrial furnaces.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Heat Treat Today publishes eight print magazines a year and included in each is a letter from the publisher, Doug Glenn. This letter first appeared in Heat Treat Today’s December 2022 Medical and Energy Heat Treat Issue print edition.
Doug Glenn Publisher and Founder Heat Treat Today
It’s roughly noon on November 8, 2022, and I’m sitting outside Starbucks in downtown Beaver, Pennsylvania, about 40 minutes from downtown Pittsburgh, enjoying an unseasonably mid-70s, pure blue sky day. I live another 40 minutes away near New Castle, PA, but I’m here in Beaver to see the newest Glenn grandchild and stopped at Starbucks to buy a triple-shot decaf espresso – the mid-afternoon drink of choice for my wife — which the barista’s have affectionately dubbed “Why Bother.” (Think about it . . . three shots of DECAF espresso. Why bother?)
Contact us with your Reader Feedback!
There’s plenty of human activity here in downtown Beaver. People walking and talking. Many conversations and warm greetings — handholding, smiling, kids with parents, cars passing, movement and activity everywhere.
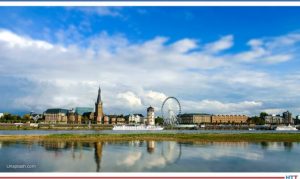
This moment in Beaver reminds me of the Altstadt in Dusseldorf, Germany in June of any given year. Aldstadt, which means “old town,” is the hub of activity in the evening after each of the five days of Thermprocess, the world’s largest heat treating trade show held every four years at the Messe (fairgrounds) in Dusseldorf, Germany. In fact, walking and eating dinner in the Aldstadt is one of the highlights of participating in Thermprocess.
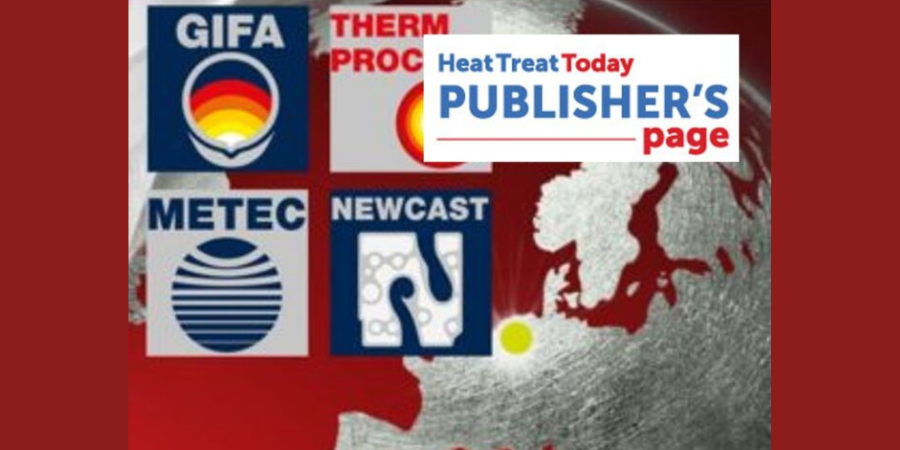
If you’ve never heard of Thermprocess and you’re involved in the heat treating industry, you need to know about it. It is one of four co-located metals trade shows held in mid-June every four years in Dusseldorf. It is an event to behold, and one highly recommended by the author of this column. In addition to Thermprocess, there is GIFA (a foundry event), NEWCAST (a casting event), and METEC (a metallurgical event). All-in-all, over 70,000 visitors and over 2,000 exhibitors flood the Messe every four years.
Düsseldorf, Germany Source: Unsplash.com
In 2023, Thermprocess is being held from June 12-16, and I would like to personally invite you to join me in Dusseldorf. As the largest heat treat event in the Western world (and arguably, the ENTIRE world), Thermprocess offers North American participants an opportunity to expand their view of what is happening in the heat treating/thermal processing world. And a broader perspective is exactly what we need. For those of you who have ever attended one of the larger manufacturing events here in North America, IMTS for example, Thermprocess and her three sister shows are MUCH bigger and better.
The Messe, where the event is located, is easily twice to three times the size of McCormick Place in Chicago, where IMTS is located. It would easily take you 20 minutes to walk from one end of the Messe to the other. During the full week it is open, the Messe is packed with metals-related exhibits and activities. It is not humanly possible to see all that is available to be seen.
Heat Treat Today is encouraging North American heat treat suppliers who market internationally to exhibit. We are putting together a group of like-minded North American exhibitors to join us. Assuming we get enough companies to join us, we will exhibit close to one another and share resources to make it more affordable for all concerned. We’ll share things like food & beverage, interpreters (if needed), and meeting rooms. By the way, unlike many North American shows, it is not unusual for people to actually strike deals and sign contracts at Thermprocess.
If you’re not a heat treat industry supplier, we encourage you, as a consumer of heat treat products, services, or supplies, to attend the event. The technology that you will see will be eye-opening. Please let us know if we can be helpful getting you to Dusseldorf in June 2023.
Find heat treating products and services when you search on Heat Treat Buyers Guide.com
Heat treating solutions are important for more than keeping an airplane flying in the sky or a bridge suspended above the water. These two examples are high profile, but what about the heat treating solutions that do not zoom through the air or mark the skyline above rivers? In the medical industry, heat treating solutions are often unseen unless something goes wrong.
When it comes to medical implant and device heat treating, what options are available to manufacturers that will benefit patients? What should we know about the heat treating processes that make metal parts functional as knees, hips, and elbows? Find out in this expert analysis from Quintus Technologies and ECM USA, Inc.
This Technical Tuesday article was first published in Heat Treat Today's December 2022 Medical and Energy print edition.
Introduction
Dan McCurdy, former president at Bodycote, Automotive and General Industrial Heat Treatment for North America and Asia, knows full well just how much time, energy, and pain the right medical heat treating practice and alloy composition can save a patient. Dan’s wife suffered from complications due to a nickel allergy in a traditionally thermally-processed ASTM F75 knee implant. She dealt with constant inflammation, swelling, and pain. Physical therapy and a second procedure did nothing to ease the discomfort. The best medicine for Dan’s wife? A specially heat treated medical implant (more of Dan's story can be found at the end of this article).
Contact us with your Reader Feedback!
To understand the stories behind final medical products, Heat Treat Today asked Quintus Technologies and ECM USA, Inc. to share two different approaches on medical implant and device heat treatment. These two companies at the forefront of the medical heat treating industry shared about hot isostatic pressing (HIP) with additive manufacturing, and vacuum heat treating. Read their answers to our questions and learn how, when it comes to implantable medical devices, heat treating can be the best medicine.
How do you ensure your equipment maintains the precise specifications required in the medical industry? What specifically is necessary to maintain compliance when it comes to medical implants?
Quintus Technologies
Chad Beamer Applications Engineer Quintus Technologies
Quintus Technologies has observed a trend in bringing Nadcap to the medical industry. Historically the medical industry has focused on the standards and regulations for the quality management system of their approved supplier, but a consistent transition to technical aspects of critical processes (including HIPing) is becoming the norm. Quintus Technologies’ background is one of delivering HIP equipment in line with Nadcap and AMS2750 specifications. The medical industry requires best-in-class temperature uniformity and accuracy; systems designed with production driven flexibility (such as thermocouple quick-connectors for T/C sensor installation
to minimize downtime); HIP furnaces equipped with uniform rapid cooling (URC®) for optimized cycle productivity; active involvement in standards committees; and working directly with the industry.
Requirements are increasing in terms of productivity and the introduction of more complex surface requirements. It is crucial to work closely with the industry to reduce oxidation of orthopedic implants during the HIP and heat treatment processes.
Steering of the HIP cycle is key, along with in-HIP heat treatments to achieve the desired microstructure for the application, which is a standard offering for High Pressure Heat Treatment™ (HPHT™) equipment.
ECM USA, Inc.
Dennis Beauchesne General Manager ECM USA, Inc.
Some of the features that are most important are leak rate at deep vacuum along with a chamber and furnace design that does not contribute to any contamination. In our systems, these features, along with others, are of the utmost importance when supplying equipment for the medical implant market.
What are the top 3–5 key requirements or compliance/quality issues needed to heat treat medical implants?
Quintus Technologies
There are several industry standards that have been released to establish key requirements for the HIP process that are often leveraged for medical applications demanding performance and reliability. For example, Nadcap has released AC 7102/6 which details the audit criteria for HIP. This document was developed with significant input from the industry and the government to define operational requirements for quality assurance. It offers a checklist for the HIP processing of metal products and includes requirements for:
managing the equipment per pyrometry standard AMS2750
qualifying technical instructions and personnel training
handling product during the loading and unloading operations
complying with gas purity requirements of the pressure medium
controlling temperature, including uniformity and accuracy evaluations and management
These aspects are critical to ensure product quality meeting medical customer requirements and expectations. Recent additions beyond conventional requirements highlighted above include high speed cooling in the HIP process (>200 K/min) for some materials which is important for metallurgical results.
ECM USA, Inc.
Key requirements include thermal performance (both uniformity and ramp control); real-time vacuum and gas management; traceability and production lot follow up through human machine interface (HMI); quality procedures for all sensor calibrations; and remote access for control and troubleshooting.
Can you share an example of how your equipment could be used to heat treat a medical implant/device from start to finish?
Quintus Technologies
Many medical implants — whether fabricated using conventional processing techniques such as casting, or more novel approaches such as additive manufacturing — require HIP to eliminate process related material defects. Defects include shrinkage porosity for castings and lack-of-fusion and keyhole defects for fusion based additive manufacturing techniques. These defects can have a negative impact on product quality, impacting performance and reliability. Once HIP has been applied to a material, post processing is often not complete, with additional thermal treatments required to achieve the optimum microstructure leading to the desired material properties and performance. Such thermal treatments are material and process dependent, but could include a stress relief, solution anneal, rapid cooling or quenching, and aging and are often applied in separate heat treat equipment.
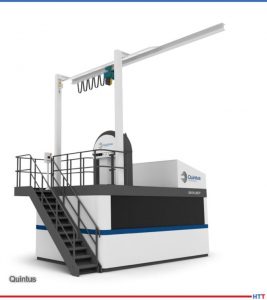
Hot Isostatic Press QIH 60 offering our most advanced Uniform Rapid Cooling (URC®) furnace technology with industry leading temperature control and accuracy
Quintus Technologies has introduced HIP systems providing capabilities beyond conventional densification. Decades’ worth of work in equipment design, system functionality, and control now offers an opportunity to perform HIP and heat treatment in a combined cycle, referred to as HPHT. Combined HIP and heat treatment for castings and AM implants can mitigate the risk of thermally induced porosity, as well as grain growth, which can offer advantages for mechanical and chemical properties in implants. This methodology provides a more sustainable processing route with improved productivity and energy efficiency. A joint HIP and heat treatment offers significant advantages with lead time, and this improvement in lead time couples well with the demands placed on the personalized medical implants. It also offers opportunities to further optimize microstructures for improvement in material properties coupled with ease of manufacturability. HPHT and modern HIP equipment may allow for a higher performing material system, which produces an implant with improved reliability and life.
Within the medical industry, fine grain AM microstructure, repeatability, and low porosity are key concerns. There are many reported benefits by applying the combined HPHT route such as reduced number of process steps, reduced cycle time and lead time, and improved process and quality control. Other advantages include spending less time at elevated temperatures helping to preserve the fine grain AM microstructure by minimizing grain growth. Tight control and steering of the cooling rates during the different steps of the HPHT cycle ensures repeatability of the properties. Manufacturability can be improved through HPHT as this approach reduces the cooling or quench severity during cooling segments which can often lead to part distortion or cracking. Improved functionality and
control go hand-in-hand with the high quality and reliability demanded in the medical industry.
ECM USA, Inc.
We have several customers making titanium alloy prothesis for various applications: shoulders, hips. Our furnaces are used for post printing processes, such as stress relieving and solution annealing.
Given concerns of metal poisoning, do you know of any changes in alloy composition of medical devices over the last decade?
Quintus Technologies
There are some metals that are becoming more common for implants, including tantalum, magnesium, CP Titanium, etc., and there have been major steps in improving ceramic materials to compete with metals for many applications.
ECM USA, Inc.
As a vacuum furnace equipment supplier, we are not deeply involved in the entire process of material selection. In the early stages of 3D printing joint replacements, from 2013 to 2014, we saw cobalt being part of some alloys. Lately it seems, indeed, that there is a trend in removing that element from the finished parts.
A Happy Ending
Dan McCurdy Former president, Bodycote, Automotive and General Industrial Heat Treatment for North America and Asia
(The rest of Dan's story from the beginning of the article....) The effects of metal poisoning and metal allergies post-surgery can be devastating. In the narrative below, Dan McCurdy shares the story of his wife’s struggle with an allergic reaction to a knee implant, and the heat treating solution that proved to be the best medicine for her.
My wife, an avid runner up and down the hills of Cincinnati, was diagnosed with osteoarthritis in both knees at the age of 53. Her orthopedist suggested a knee replacement for the most degraded one. The replacement was a well-known brand, made from investment-cast ASTM F75 (nominally a Co-Cr-Mo alloy) with full FDA-approval. After a successful surgery and diligent physical therapy, her recovery plateaued, and she experienced chronic inflammation, swelling, and pain.
A blood test, designed to detect allergies to materials used in orthopedic implants, showed a reaction to nickel that was nearly off the charts. We were surprised, as she had previously tested negative for nickel allergies through skin patch testing. The ASTM F75 specification allows for up to 0.5% bulk nickel as a tramp element in implantable devices; however, depending on foundry practices, the concentration of tramp alloys at any point on the surface of a casting can vary significantly. Titanium implants may be the solution to this, but FDA-approved titanium alloys can still contain up to 0.1% Ni.
The solution for my wife, as it turned out, was a different material, originally developed for the nuclear industry, along with an innovative heat treatment process. Created with an alloy of zirconium and niobium (with a maximum nickel content of 0.0035%), her new knee was heat treated at a high temperature in an oxidizing environment, which converts the soft zirconium surface into hard ceramic zirconia, increasing hardness and wear resistance. With this specially heat treated implant in place, my wife is back to nearly 10K steps a day.
References
[1] Magnus Ahlfors and Chad Beamer. “Hot Isostatic Pressing for Orthopedic Implants.” quintustechnologies.com/knowledge-center/hot-isostatic-pressing-for-orthopedic-implants. Quintus Technologies. 2020.
[2] Chad Beamer and Derek Denlinger. “Hot Isostatic Pressing: A Seasoned Player with New Technologies in Heat Treatment — Expert Analysis.” www.heattreattoday.com/processes/hot-isostatic-pressing/hot-isostatic-pressing-technical-content/hot-isostatic-pressing-a-seasoned-player-with-new-technologies-in-heat-treatment-expert-analysis/. Heat Treat Today. 2020.





 Find heat treating products and services when you search on Heat Treat Buyers Guide.com


 An electric vehicle manufacturer will move the heat treatment of their prototype gears in-house with a vacuum furnace. The company expects new product development to accelerate.
 Over the last few months, the Metal Treating Institute requested comments from members on how their current business insurance programs have been progressing with property, liability, errors-omissions, commercial auto, and workers compensation. What we learned is this is a huge pain point for most heat treaters of any size.

 If you’re not a heat treat industry supplier, we encourage you, as a consumer of heat treat products, services, or supplies, to attend the event. The technology that you will see will be eye-opening. Please let us know if we can be helpful getting you to Dusseldorf in June 2023.