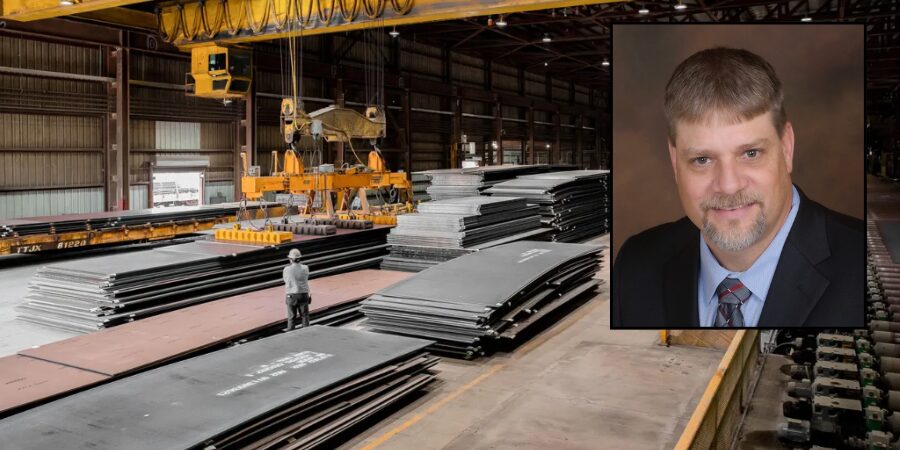
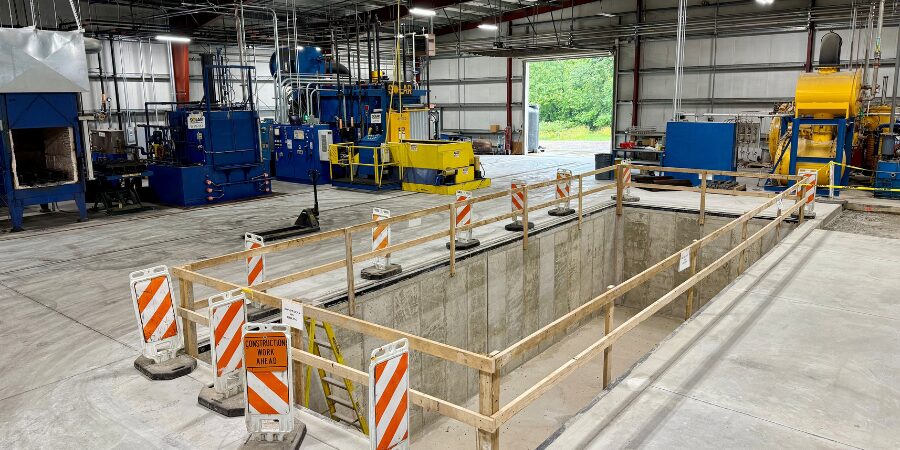
SSAB is investing approximately $74 million to expand its heat treat capacity at its Axis, Alabama facility. The expansion will support the production of premium steel products.
Andy Bramstedt General Manager SSAB Alabama Source: Linkedin
“This expansion will bolster our capacity to produce high-strength steel brands such as Hardox and Strenx and will also increase SSAB Alabama’s truck shipping capacity.” said Andy Bramstedt, general manager of SSAB Alabama.
The project will encompass the construction of a new building equipped with a state-of-the-art tempering furnace, and improvements to the infrastructure.
“We have been working on this investment for a long time, and it is very gratifying to see it come to fruition. This investment will not only expand our capacity for niche products, which are in high demand, but also enable us to offer a broader product range from our Alabama facility,” said Kjell Baeckman, head of Sales Special Steels for SSAB.
Mobile Chamber President and CEO Bradley Byrne Source: Mobile Chamber
The expansion anticipates the creation of 12 new jobs in the local community.
Mobile Chamber president and CEO Bradley Byrne said, “By expanding production of high-strength, specialized steel, SSAB is reinforcing Mobile County’s role in driving innovation and supplying critical materials to key sectors across North and South America.”
This initiative is set to commence in 2025 and is expected to be completed in 2027.
Press release is available in its original form here.
Following foundation preparations, Solar Atmospheres will be installing a new titanium drop bottom water quench furnace at their Hermitage, Pennsylvania, location. The new addition will ensure consistent metallurgical results for demanding aerospace and industrial applications.
The new furnace is rated for a maximum operating temperature of 1850°F ±10°F and is designed to process titanium bar and forging loads of up to 7,500 pounds. Measuring 14′ by 54″ wide by 48″ high, workloads will be rapidly transferred into a 7,000-gallon, recirculated water quench tank within seconds.
This investment opens the door to expanded titanium solution treating capabilities and supports Solar Atmospheres’ commitment to innovative thermal processing solutions.
Press release is available in its original form here.
Industrial Ceramic Products, Inc. (ICP) has been acquired by Allied Mineral Products, LLC (Allied). The acquisition includes all ICP’s product lines, equipment, facilities, grounds, and employee base. The deal will increase Allied’s capacity, applications, and expansion into precision, high-fired refractory shapes markets.
Paul Jamieson CEO Allied Mineral Products
“We have been each other’s’ customers and we have partnered with ICP on various projects for over 50 years. They have a strong management team, a highly tenured workforce and expertise in precision high-fired ceramic shapes. Their skill in manufacturing high quality ceramic refractory shapes is well known in our industry. Culturally we are very aligned,” said Paul Jamieson, president and CEO of Allied. “With this acquisition, we add a highly skilled workforce and plenty of room to grow and expand at ICP’s current location in Marysville. We will continue producing products under the ICP name for the foreseeable future.”
John Odenthal President ICP
“We recently celebrated ICP’s 89th year of quality manufacturing. We are proud of what we and our employees have accomplished over the years,” said John Odenthal, president of ICP. “As the marketplace continues to be more competitive, we realized we needed to align with a strong company to ensure we could continue to serve our customers and provide security for our employees. With this sale, we know our customers and employees will benefit, and that is especially important to us.”
ICP’s production facility in Marysville, OH, joins Allied’s existing U.S. manufacturing operations in Columbus, OH; Brownsville, TX; and Pell City, AL. Allied Mineral Products, LLC is a global manufacturer of monolithic refractories and precast, pre-fired refractory shapes. Headquartered in Columbus, OH, Allied serves a wide variety of industries with refractory solutions.
Press release is available in its original form here.
Alloy R&D has resulted in a material that combines the affordability of 310 stainless steel with the high temperature properties of more expensive higher nickel alloys, like alloy 600. Be it for your muffle belt conveyor or heat treating trays, this Technical Tuesday installment by Hugh Thompson, applications engineer of Rolled Alloys, will explore the strengths of this alloy variety to determine its best application.
This informative piece was first released inHeat Treat Today’sJuly 2025 Super Brands print edition.
Increasing nickel prices initiated the development of RA 253 MA®, a versatile alloy used in various thermal applications for equipment construction. With low chromium (Cr) and nickel (Ni) levels, this alloy provides a cost-effective alternative to other pricier nickel-based materials. With microalloying control, it is priced alongside 310 stainless steel while offering high strength properties similar to the more costly 600-series alloys.
Chemically similar to 309 stainless steel, the alloy offers significantly higher creep resistance and rupture strength than 310. Its benefits include:
Oxidation resistance up to 2000°F (1090°C)
Significant hot tensile strength comparable to that of the 600-series alloys
Noteworthy creep and rupture properties
This lean austenitic stainless steel uses cerium and silicon to create a very adhesive oxide, resulting in excellent oxidation resistance. The combination of nitrogen and carbon provides creep-rupture strength double that of 310 and 309 stainless steel at 1600°F (870°C).
Chemistry
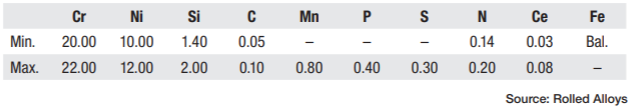
RA 253 MA has a specified chemistry, as indicated in Table A.
Table A. RA 253 MA chemistry
High Temperature Properties
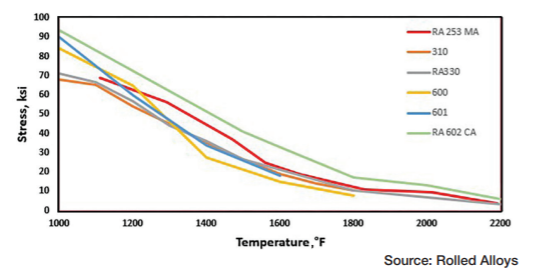
Figure 1 shows the hot tensile strengths of different materials. RA 253 MA can be seen to have higher hot tensile properties than alloy 600, 310 stainless, and RA330® but lower than RA 602 CA®. It’s worth noting that while its hot tensile strength is reported up to 2200°F (1200°C), practical use is limited to 2000°F (1090°C) in oxidizing environments due to a loss of oxidation resistance at this temperature.
Figure 1. Hot tensile strengths
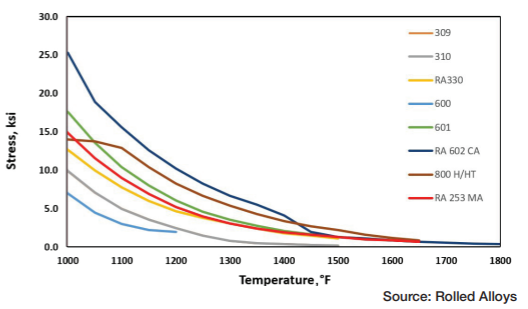
Figure 2 displays the allowable design stresses for pressure vessel plates according to Section II-D of the ASME 2023 (2024 revision) code. One can see that the allowable stresses for RA 253 MA are higher than those for 310 stainless and RA330 but not as high as alloy 601. ASME allows design stresses for this alloy up to 1650°F (900°C). However, RA 253 MA is utilized at higher temperatures for various applications because this temperature limit is only for pressure vessels.
Figure 2. Allowable design stresses
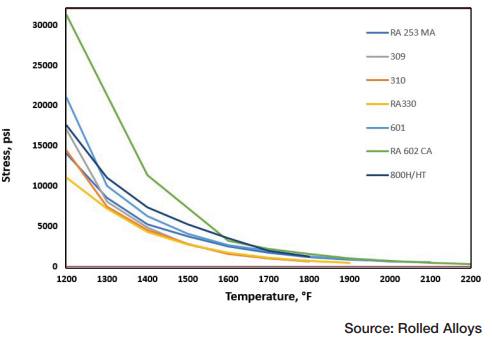
Figure 3 displays the actual 10,000-hour rupture strengths of different high temperature alloys. The data reveal that RA 253 MA exhibits high creep and rupture stress values comparable to alloy 601 and RA 602 CA, and it surpasses RA330; this would also surpass alloy 600.
Figure 3. 10,000-hour rupture strengths
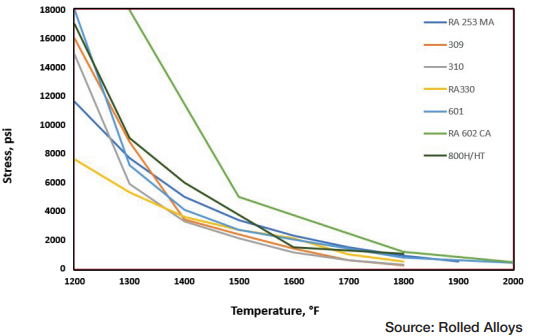
In Figure 4, data are presented for the minimum creep rate of 0.0001% per hour. Creep refers to the rate at which metal stretches, and it is usually measured in percentage per hour. There is a phase where the creep rate remains relatively constant, known as the secondary creep rate. This rate is a key factor in designing for high temperatures. It’s important to consider that metal will creep even under light loads, as the effects of creep can be observed in material with no load other than its own weight. Therefore, in practical applications, a creep criterion is utilized for design purposes.
Figure 4. Minimum creep rate of 0.0001% per hour
The furnace industry has traditionally used a design criterion based on the stress required for a minimum creep rate of 1% in 10,000 hours or 0.0001% per hour. The design stress is typically set at a fraction of this value. For one of its criteria, ASME uses 100% of the extrapolated stress for 1% in 100,000 hours (or 0.00001% per hour). It is not recommended to extrapolate stress rupture and creep data to 100,000 hours above 1800°F (980°C). Th is comparison is provided for general guidance only.
Rupture strength is reported as a stress and number of hours. It is the stress required at a specific temperature to break a specimen within a given time. In the furnace industry, a standard criterion for setting design stresses is to use a fraction of the stress that would result in rupture at 10,000 hours. ASME uses the lower of 67% of the extrapolated 100,000 rupture stress or 100% of the extrapolated 1% in 100,000 hours minimum creep rate.
Strengths and Limitations
When compared to alloys like 309 and 310, RA 253 MA has demonstrated equal or superior oxidation resistance. At 2000°F (1090°C), it displays outstanding oxidation resistance, on par with the limit for 310 stainless steel and surpassing 309. It is important to note that although short furnace excursions up to 2100°F (1150°C) can be tolerated, consistent oxidizing temperatures above 2000°F (1090°C) can quickly degrade the material. Therefore, it is best to avoid excursions above the suggested temperature limits for any alloy.
This material has also proven to perform well in mildly carburizing environments, despite its lower alloy content. Even small amounts of oxygen in the gas, like carbon dioxide or steam, can create a thin and tough oxide layer on RA 253 MA, offering excellent protection against carbon and nitrogen pickup. However, it’s not recommended to use it in carburizing environments. Due to its lower nickel content, it is less resistant to carburization compared to higher nickel alloys such as RA330.
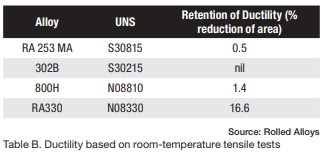
Table B. Ductility based on room-temperature tensile tests
In a simulation where coupons were exposed to fifteen weeks of simulated bake cycles between 1700°F–1950°F (930°C–1065°C) in “green mix” used for producing carbon electrodes, room-temperature tensile tests revealed the ductility as shown in Table B.
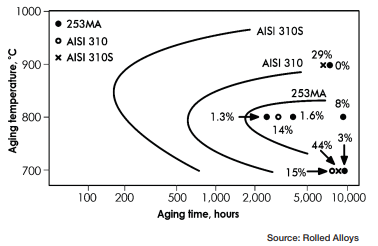
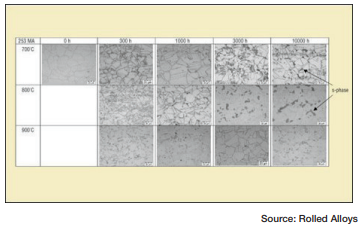
For RA 253 MA, the sigma phase formation process is much slower compared to 310S and 310, as shown in the TTT diagram in Figure 5 and the micrographs in Figure 6. At temperature, it is very unlikely material containing sigma phase will behave adversely. When the material is cooled to room temperature, it becomes very brittle, making it less resistant to thermal cycling. The material may crack if highly constrained and unable to expand freely during subsequent ramp-up.
Figure 5. TTT curve for sigma phase formationFigure 6. RA 253 MA grain structures with and without sigma phase
Corrosion Resistance in Salt Bath Applications
As shown in Table C, RA 253 MA may be comparable to alloy 600 when exposed to sodium and potassium salts for heat treating high speed steel.
Table C. Intergranular attack based on exposure to sodium and potassium salts
In this trial, plate samples were exposed to 210–252 cycles in preheat salts at 1300°F–1500°F (700°C–820°C), high heat salt at 2200°F (1200°C), and then quenched in 1100°F (590°C) salt. Table C shows that RA 253 MA has the potential to perform well in a salt bath environment due to its high silicon and chromium levels. While alloy selection is essential, regular maintenance and cleaning of the salt bath and surrounding areas are the most crucial factors.
In salt bath heat treating, the service life of the pot is primarily determined by maintenance not the alloy. Pots must be desludged regularly, and all old, spilled salt must be removed from the furnace refractory when changing pots
Corrosion Resistance
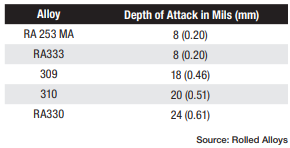
Table D. Sulfidation attack after exposure to an atmosphere
containing 13.6% SO2 at 1850°F (1010°C) for 1,860 hours
This alloy performs well, even in hot environments with sulfur in the presence of oxygen. However, it is not resistant to environments with reducing sulfur. Even in the presence of oxygen, the partial pressure of oxygen can be very low while stainless steel is in use. This low pressure can lead to a local sulfidation attack, even in what is considered an oxidizing atmosphere.
Table D displays the depth of intergranular oxidation and sulfidation in test samples exposed to an atmosphere containing 13.6% SO2 at 1850°F (1010°C) for 1,860 hours.
Microstructure
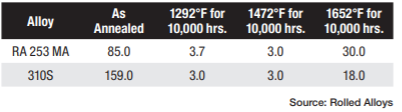
Table E. Charpy v-notch impact results as annealed and after
exposure (ft-lb)
The microstructure of RA 253 MA in the annealed and long-term exposure states is shown in Figure 6. In addition, Table E provides the Charpy impact values for the annealed state and at temperatures of 1292°F, 1472°F, and 1652°F (700°C, 800°C, and 900°C) over a long period of exposure.
Based on the microstructure and Charpy impact data, it is clear that sigma phase precipitation is almost non-existent at 1650°F. Moreover, the TTT diagram in Figure 5 indicates that RA 253 MA requires significantly more time to initiate sigma precipitation compared to 310 and 310S stainless steel.
Applications for Use
Given the above capabilities, RA 253 MA can be and has been successfully utilized in a variety of applications. From bell annealing furnace covers, muffle belt conveyors, car exhaust manifolds and exhaust gas flexible tubes to hot air ducts, cooling tower tubes in sulfite process pulp mills, and heat treatment trays for neutral hardening, its abilities can cover a widescope of applications throughout in-house heat treat operations.
References
Andersson, T. and T. Odelstam. “Sandvik 253MA (UNS S30815) — The Problem Solver for High Temperature Applications.” A Sandvik Publication, October 1984.
Kelly, J. Rolled Alloys. Rolled Alloys Bulletin 100. Revised September 2001.
Manwell, C. Rolled Alloys. Rolled Alloys Internal Report, Summary of Cyclic Oxidation Testing at 2000°F, August 2005.
Proprietary Report on the MA Heat Resistant Material Series.
Saum, W. Rolled Alloys. Rolled Alloys Internal Report, Summary of Oxidation Testing at 2000°F, August 2002.
About The Author:
Hugh Thompson Applications Engineer Rolled Alloys
Hugh Thompson is a metallurgical engineer at Rolled Alloys, leveraging his expertise from The University of Toledo College of Engineering to drive innovation in specialty alloy solutions. Based in Toledo, he combines deep technical knowledge with industry leadership.
Three induction vacuum melting furnaces will be delivered to an industrial foundry specializing in parts production for the aerospace industry.
Sławomir Woźniak CEO SECO/WARWICK Group
The three furnaces will increase the European partner’s production facilities and includes VIM technology for using directional solidification or single crystal casting of nickel and cobalt superalloys.
“In the VIM DS/CS furnace, the client can obtain castings using directional solidification or single crystal technology. The well-designed furnace structure…allows the user to produce the highest quality castings,” said Sławomir Woźniak, CEO of the SECO/WARWICKGroup, a thermal processing solutions provider with North American locations.
The furnaces on order have a maximum capacity of 40kg.
The growing importance of vacuum metallurgy is partly a consequence of the continuously changing production needs of aviation. The most modern jet engines utilize advanced blades cast using single crystal technology.
Press release is available in its original form here.
Heat TreatToday offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry. Enjoy these 12 news items, featuring steel mill and furnace upgrades, new CEOs, a 5000th device celebration, and more!
Equipment
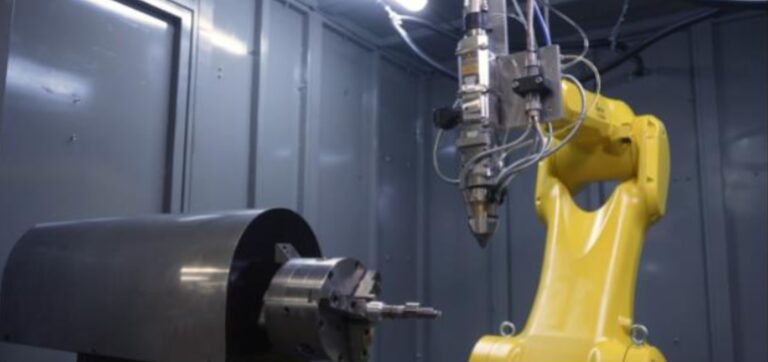
1. Synergy Additive Manufacturing LLCwas awarded Phase I SBIR by U.S. Navy to develop extremely high-speed laser cladding processes to enhance the performance of titanium cylinder bores used in critical helicopter components.
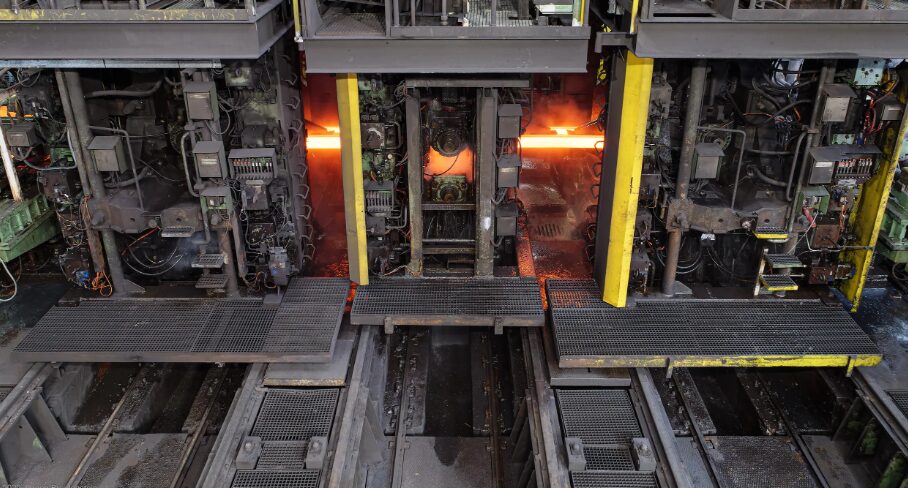
2. SMS group upgrades CELSA Barcelona’s medium section mill with new process automation. Upgrade of the outdated level 2 automation will secure the long-term operational stability and ongoing production efficiency of the medium section mill.
3. Nitrex upgraded seven furnaces for a Nevada manufacturer for the aerospace industry. The upgrades included retrofitted vacuum furnaces with modern automation utilizing QMULUS — Nitrex’s AI- and ML-powered SCADA platform.
4. Mercer Vacuum Components and Services, Inc., were commissioned to rebuild two vacuum furnaces, including the furnaces’ hot zones, gas cooling systems (to include the motor), and fan and heat exchangers. The rebuilding occurred at their Vacuum Technologies Center in Terre Haute, IN.
Synergy Additive Manufacturing LLC awarded phase I SBIRSMS Group upgrades millNitrex upgrades furnacesMercer Vacuum Components and Services, Inc. rebuilds
Company & Personnel
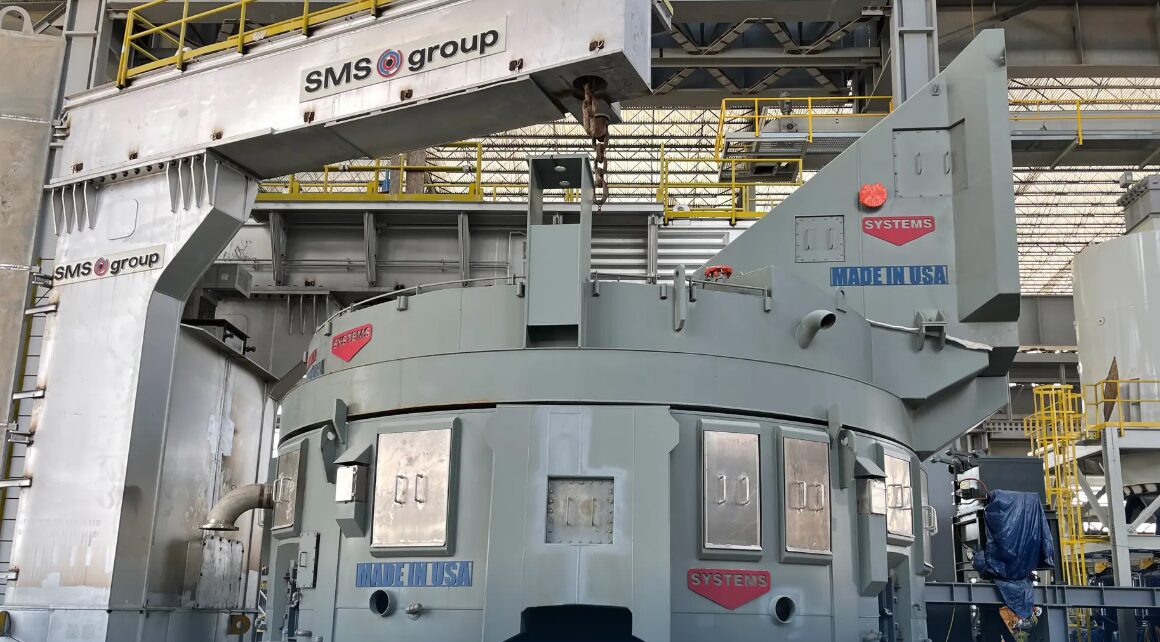
5. SMS group enters into strategic partnership with The Systems Group to drive safety and sustainability in steelmaking. SMS group now integrates Spray-Cooled® technology into its solutions for electric arc furnaces and secondary metallurgy plants.
6. Ipsen Group CEO Geoffrey Somary assumed the role of president of Ipsen USA, in addition to his current role leading the global organization.
7. Patrick McKenna has been appointed as chief executive officer and director of Bluewater Thermal Solutions, a portfolio company of Aterian Investment Partners.
SMS Group partners for furnace solutionsGeoffrey Somary CEO Ipsen USAPatrick McKenna CEO Bluewater Thermal Solutions
Kudos
8. Kowalski Heat Treating Company celebrated 50 years in business. The family company was founded in 1975, and remains a family company today.
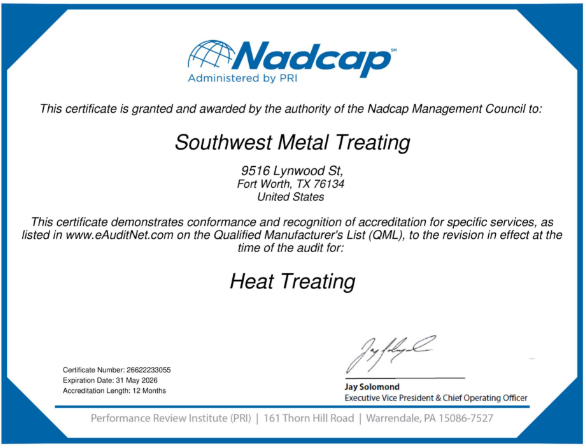
9. Southwest Metal Treating Corp. announced earning Nadcap® accreditation for heat treating, marking a milestone in its commitment to quality and precision in aerospace and defense manufacturing.
10. Nitrex celebrated the 35th work anniversaries of Karen Feciskonin and Bill Schmitz. They also recognized Bill Schmitz’s retirement after 35 years of serving on their team.
11. Akron Steel Treating Company announced 20 years of Nadcap® accreditation.
12. The SECO/WARWICK Group announced record-breaking dynamic growth results as well as the milestone of the 5000th device in production.
Kowalski 50 Year AnniversarySouthwest Metal Treating Nadcap CertificationNitrex celebrates anniversariesAkron Steel Treating Nadcap CertificationSECO/WARWICK 5000th device
Heat Treat Today has gathered the four heat treat industry-specific economic indicators for July 2025. While June industry-specific economic indicators rose up like weeds, July’s indicators have seen a mix of slowdown and growth.
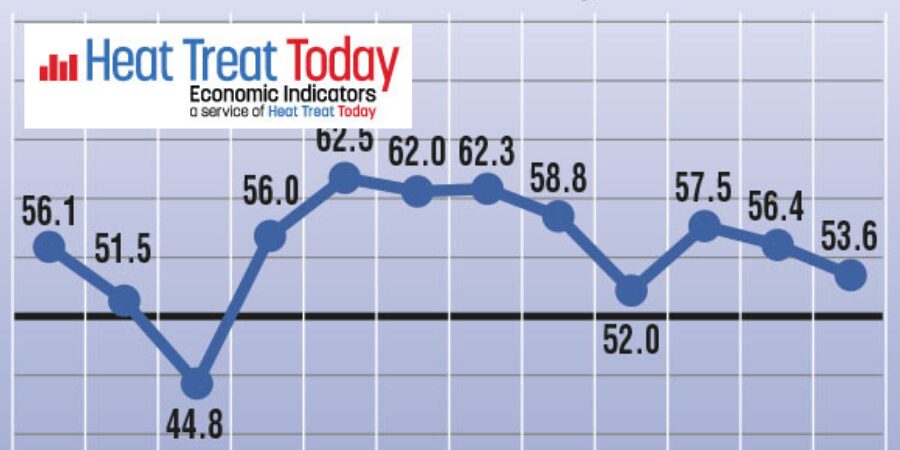
July’s industry-specific economic indicators showed growth in one index, no change in one index, and two indices slipping into contraction. The Inquiries index shows some anticipated contraction with Inquires declining to 49.3 (from 62.5 in June). Bookings continue to reflect suppliers’ anticipation for steady growth — as compared to June’s performance — at 53.6 (slightly below June’s 56.4). The Backlog index entered definite contraction, declining to 41.7 (from 54 in June). Finally, the Health of the Manufacturing Economy index showed no expectations for change, resting at 50 (compared to 59.2 in June).
The graphs overall suggest suppliers are preparing for a slight slowdown after expecting rapid growth in June.
The results from this month’s survey (July) are as follows; numbers above 50 indicate growth, numbers below 50 indicate contraction, and the number 50 indicates no change:
Anticipated change in Number of Inquiries from June to July:49.3
Anticipated change in Value of Bookings from June to July: 53.6
Anticipated change in Size of Backlog from June to July: 41.7
Anticipated change in Health of the Manufacturing Economy from June to July: 50
Data for July 2025
The four index numbers are reported monthly by Heat Treat Today and made available on the website.
Heat TreatToday’sEconomic Indicatorsmeasure and report on four heat treat industry indices. Each month, approximately 800 individuals who classify themselves as suppliers to the North American heat treat industry receive the survey. Above are the results. Data started being collected in June 2023. If you would like to participate in the monthly survey, please click here to subscribe.
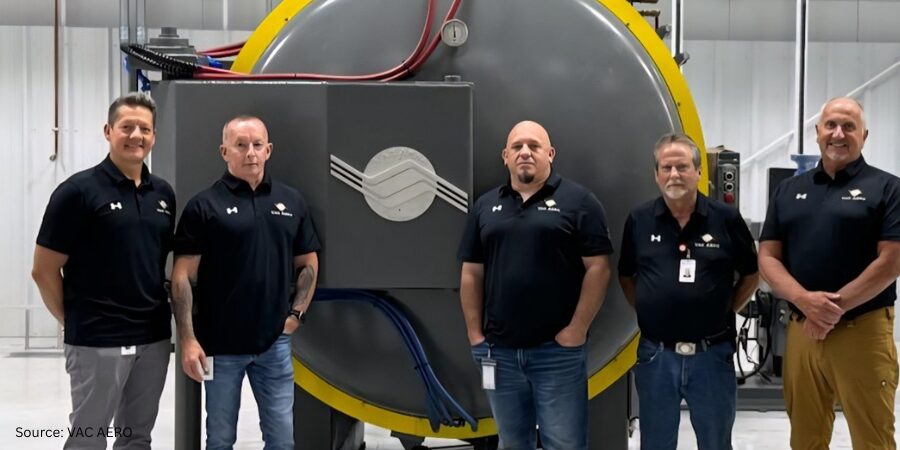
VAC AERO is investing $5.8 million to open its first U.S. operation in Greenville, SC. The facility will initially feature vacuum furnaces, with a defined goal of introducing advanced coating technologies.
Brent Davis President & COO VAC AERO U.S. Inc. Source: Linkedin
The Canadian thermal processing company will be partnering with Meyer Tool to deliver advanced heat treating solutions. The companies are working together to establish a “shop-in-shop” facility within Meyer Tool’s Greenville location. The “shop-in-shop” model enables VAC AERO to operate a fully integrated vacuum heat treating, brazing, and coating operation within Meyer Tool’s advanced manufacturing environment.
“We are excited to bring our expertise in vacuum heat treating directly into the heart of one of North America’s most respected regions for power generation and aerospace component manufacturing,” said Brent Davis, president and COO of VAC AERO U.S. Inc.
Dan Godin Executive Vice President Meyer Tool Source: Linkedin
Dan Godin, executive vice president of Meyer Tool, stated: “This collaboration is leveraging our combined expertise to offer the customers better control of their Value Stream.”
This strategic partnership marks VAC AERO’s first operational presence in the United States and underscores its renewed commitment to global expansion.
Press release is available in its original form here.
Patrick McKenna has been appointed as chief executive officer and director of Bluewater Thermal Solutions, a portfolio company of Aterian Investment Partners, effective immediately.
Patrick McKenna CEO Bluewater Thermal Solutions
“I’m honored to join Bluewater Thermal Solutions at such a dynamic time for the industry,” said McKenna. “With a strong operational footprint, a dedicated team, and a reputation for technical excellence, Bluewater is well positioned for growth. I’m eager to work alongside our employees, customers, and partners to build on the company’s momentum and drive our capabilities forward.”
McKenna has more than 25 years of leadership and innovation experience in the thermal processing industry. He most recently served as president & CEO of Ipsen USA, a global provider of vacuum furnace technology for the thermal processing sector. He oversaw a team of more than 250 employees at Ipsen’s U.S. based Vacuum Center of Excellence, while driving success across international markets.
Prior to Ipsen, McKenna was most recently co-founder, board member, and vice president of Nevada Heat Treating/California Brazing. There, he helped transform the business from a traditional commercial heat treating operation into a Nadcap-accredited provider of turnkey manufacturing solutions serving major aerospace OEMs.
Brandon Bethea, co-founder and partner at Aterian, expressed strong confidence in the new leadership: “Patrick has excelled in every role he’s taken on. His deep industry expertise and sharp eye for commercial growth make him the ideal leader to guide Bluewater into its next phase. We’re thrilled to welcome him to the team.”
Bluewater Thermal Solutions is headquartered in Greenville, South Carolina, and is one of North America’s largest providers of heat treating and brazing services. The company operates ten facilities across the U.S., offering thermal processing capabilities.
Press release is available in its original form here.