FPM Heat Treating has announced the acquisition of a vacuum furnace, enhancing the company’s capabilities to serve the manufacturing community, especially in the automotive and aerospace sectors. The furnace will meet an increasing demand for a specialized family of parts.
Bob Ferry Vice President of Quality & Engineering FPM Heat Treating
The furnace, fully compliant with NFPA, NADCAP, AMS, CQI-9, and other critical industry standards, has been installed at FPM Heat Treating by Solar Manufacturing. With an operating temperature of up to 2400°F (1315.5°C) and a weight capacity of 5,000 pounds, the furnace processes at specialized heat treatment cycles critical for automotive components as well as precise specifications for applications within consumer products and the military/aerospace sectors.
“We are committed to meeting the growing demands of our clients in the manufacturing community,” said Bob Ferry, vice president of quality and engineering at FPM Heat Treating. “The new Solar furnace enhances our capabilities and enables us to maintain the highest standards of quality and efficiency in our operations.”
Main Image: Adam Jones, Midwest regional sales manager at Solar Manufacturing, viewing the vacuum furnace’s 48” x 48” x 72” deep insulated hot zone
The press release is available in its original form here.
HART-TECH has expanded its capabilities with a vacuum furnace that will allow for the heat treatment of multiple steel types and the ability to implement a wide range of processes, from hardening through vacuum carburizing and carbonitriding. The furnace will efficiently heat treat large loads of research, test, and production elements.
Maciej Korecki Vice President of Business of the Vacuum Furnace Segment SECO/WARWICK
The commercial heat treater has previously incorporated over 10 SECO/WARWICK processing solutions. This system is being provided to work on the implementation of vacuum carbonitriding technology services that HART-TECH can now offer to a wide range of clients.
“We can say that we have a kind of synergy with the HART-TECH hardening plant,” said Maciej Korecki, vice president of the SECO/WARWICK Group’s vacuum segment. “Our partner, just like us, loves science, research, and development, and the common curiosity about the world motivates us to create further innovations.”
Dr. Eng. Robert Pietrasik, Sc.D. Management Board CEO & Technological Dept Head Director HART-TECH Sp. zo. o.
“This solution will help us to put into action a project concerning the implementation of vacuum carbonitriding technology at the HART-TECH plant with our customers in mind,” said Dr. Eng. Robert Pietrasik, president of HART-TECH. “We want to implement the low-pressure carbonitriding process and be able to use it in mass production.
“By expanding the machine park with a new vacuum furnace,” Dr. Pietrasik continued, “we will also significantly shorten the waiting times for heat treatment for our current and future customers. The large workspace will significantly increase our capabilities for processing elements hardened in gas. Thus, we will be able to gradually switch from hardening elements in oil to hardening in gas, which is more efficient, cleaner and ensures smaller deformations.”
The vacuum furnace supplied to the company has been enhanced with a gas system equipped with two acetylene mass valves, a hydrogen mass valve, and an ammonia mass valve. The furnace can use three gases for various technologies: acetylene, hydrogen and ammonia. HART-TECH specializes in hardening, carburizing, nitriding, sulfur nitriding, steel tempering, supersaturation and aging, annealing, vacuum brazing and low-friction layers, and hardening of machine and tool elements.
The press release is available in its original form here.
Nearly 100 attendees gather at the Conrad Hotel in Indianapolis for a three-day event to discuss industrial decarbonization and sustainable technologies. Targeting users and suppliers of industrial heating processes, the Industrial Decarbonization Summit is organized by the Industrial Heating Equipment Association (IHEA).
IHEA designed the SUMMIT to help everyone using heat technologies understand and overcome these important concerns and challenges.
Emceed by Jeff Rafter, vice president of sales and marketing, Selas Heat Technology Co. LLC, the event began yesterday (Tuesday, October 29th) with a keynote presentation by Dr. Avi Shultz, of the United States Department of Energy, Industrial Efficiency & Decarbonization Office (US DOE IEDO), who spoke on “Understanding the US DOE Industrial Decarbonization Initiatives.” Other speakers and topics covered during the 2-day event include:
Mr. Tim Hill from Nucor and Mr. Jeff Kaman from John Deere talking about the implementation of their companies’ decarbonization plans.
Mr. Perry Stephens from EPRI, Mr. Brian Kelly from Honeywell, and Mr. Erik Anderson from Ambient Fuels discussing alternatives to fossil fuel combustion.
Mr. Sandeep Alavandi of GTI Energy addressing how companies can get to net zero by reducing, converting, and trading.
Mr. Bryan Stern from Gasbarre Thermal Processing Systems addressing economic and business concerns related to industrial adoption of decarbonization technologies.
Dr. Avi Shultz Director U.S. Department of Energy (DOE) The Industrial Efficiency & Decarbonization Office (IEDO)Jeff Rafter Vice President of Sales and Marketing Selas Heat Technology Company, LLC Tim Hill General Manager Sustainability Solutions NucorJeff Kaman Manager, Energy Supply and Sustainability John DeerePerry Stephens Electric Power Research Institute (EPRI)Brian Kelly Honeywell Thermal SolutionsErik Anderson Vice President, Origination Ambient FuelsSandeep Alavandi Program Manager GTI EnergyBryan Stern Product Development Manager Gasbarre Thermal Processing Systems
Summit attendees come from a wide cross section of industries including companies such as Daido Steel, Whirlpool, Detroit Stoker Co, Wenger Mfg, Trane, Nucor Steel, Timken, John Deere, Oak Ridge National Lab, Siemens Energy, Dowa THT America, and many more.
The content of the Summit is targeted at company thought leaders who are attempting to learn how to navigate the decarbonization roadway. Click on the video below to view some of Jeff Rafter’s opening remarks.
The heat treat industry is rich with knowledgeable leaders, resourceful problem solvers, and innovative teams. One of our favorite things to do here atHeat Treat Today is to draw attention to the wealth of expertise in the field, so we are pleased to launch the Voices in Heat Treat series, pointing readers to a treasure house of recorded interviews and discussions diving into the fundamentals of thermal processing.
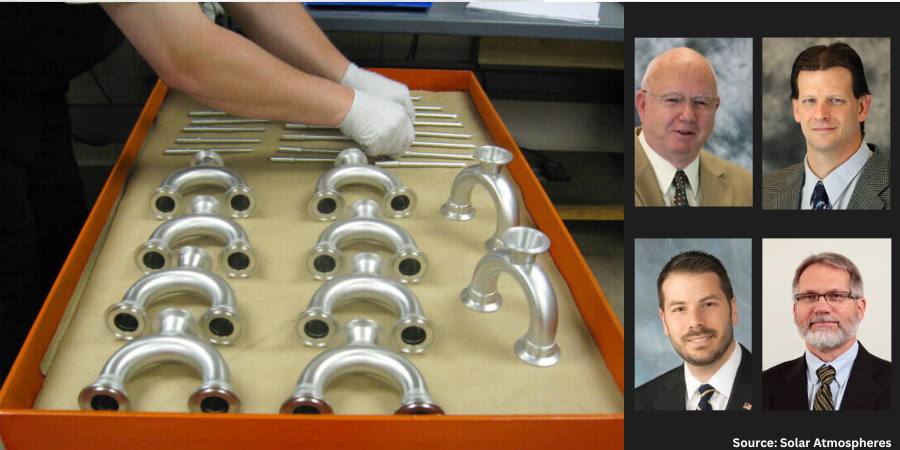
In this and coming articles drawn from the audio library at Solar Atmospheres, we will summarize topics on everything from basic heat treating how-tos, preventative maintenance, and troubleshooting to the history of hot zone designs, temperature uniformity surveys, and the distinctions to take into consideration when processing different kinds of metals and alloys. In today’s installment, our industry experts focus on vacuum brazing and the uniqueness of heat treating titanium.
In the premiere article of this series, Bill Jones, founder and CEO of Solar Atmospheres and Solar Manufacturing, interviews industry leaders about the advantages of vacuum furnace brazing. Read the highlights of their discussion about the process, in particular when used with stainless steel and titanium. The summary of a fourth episode recorded earlier has been added, expanding on the topic of the advantages of processing titanium in a vacuum furnace. The experts are Calvin Amenheuser, vice president of the Hatfield plant, and Mike Paponetti, sales manager of the southeast. Jim Nagy, senior vice president of Solar Manufacturing, hosts the episodes. A summary of each conversation is below, followed by links that will take you directly to that podcast episode.
Bill Jones and the Team Speak on Vacuum Brazing, a 3-Part Series
“Advantages of Vacuum Furnace Brazing”
December 2015
Brazing to form strong metallurgical bond where the brazed joint becomes a sandwich of different layers, each linked at the grain level
This episode is the first in a series on vacuum furnace brazing, with an overview of different types of brazing processes and why vacuum furnace brazing is superior to other joining methods, particularly torch brazing and welding.
The conversation explores various reasons why a vacuum furnace is well-suited to perform brazing because it provides:
a controlled, consistent atmosphere cycle after cycle
uniform heating throughout the hot zone
a controlled rate of heating
the elimination of air to prevent the formation of oxidation of the metal
Vacuum Furnace Brazing vs. Alternative Methods
Both Cal Amenheuser and Mike Paponetti speak about vacuum brazing being a superior process to alternative methods. Mike noted that torch brazing is effective for low volume loads, but the process risks flux entrapment and could produce messy, overheated and possibly carburized parts. In contrast, vacuum furnace brazing allows for higher volume loads, providing a repeatable process, precise temperature measurements, and versatility.
Brazing applications from parts to rockets
Calvin added that while welding melts the materials and produces a strong joint, the surrounding material is weaker. With vacuum furnace brazing, the brazed joint is just as strong or stronger afterward as before.
Finally, the panelists compared how batch vacuum furnace brazing eliminates distortion that is typical with torch brazing and welding because of hot zone uniformity. A batch furnace operator can modify the process to meet the demand of the load, and furnace charts provide proof of reveal what exactly happened during the run so that successful recipes can be repeated.
In this episode, second in the series on the vacuum furnace brazing, the Solar team reconvened to discuss advantages of and concerns with nickel-based and copper-based brazing alloys.
All agree that nickel-based alloy offers a cleaner braze but emphasize precautions must be put in place to avoid metal erosion and cracking. While readily available and a good match for low carbon steel, copper flashes during the braze. Inert gas is recommended to decrease evaporation of the copper-based alloy.
“Processing Titanium in Vacuum Furnaces: Active Brazing of Titanium in a Vacuum Furnace”
April 2016
In this third and final episode on the topic of vacuum furnace brazing, Bill Jones, Calvin Amenheuser, and Mike Paponetti consider significant challenges to brazing titanium, which is the need to reduce surface oxide to allow the process to take place and why active brazing is suggested as a means to meet that challenge. What follows is an informative discussion on composites that allow producing companies add to the material, like hydrated titanium, zirconium, and indium, to help overcome oxides, which are effective at wedding to the surface.
“Processing Titanium in Vacuum Furnaces: Advantages”
February 2013
175,000 pounds of 6Al-4V titanium in Solar’s 48-foot-long vacuum furnace
Although recorded earlier than and thus separately from the series on vacuum furnace brazing, this summary of an episode is included in this article to provide context about the advantages of processing titanium in a vacuum furnace. This is a solo Bill Jones episode.
Bill Jones highlights how vacuum furnaces provide a pure atmosphere for processing titanium compared to an argon atmosphere, saving machining costs and time. Additionally, vacuum processing uses forced inert gas quenching to cool titanium as opposed to water quenching which results in a more uniform result and eliminates part distortion. Finally, fixturing parts properly in a vacuum furnace with graphite allows heat treaters to preserve the part shape and avoid movement.
Bill Jones Founder & CEO Solar Atmospheres, Solar Manufacturing Source: Solar AtmospheresCalvin Amenheuser Vice President of Operations, Souderton plant Solar Atmospheres Source: Solar AtmospheresMichael Paponetti Sales Manager of the Southeast Solar Atmospheres, Inc. Source: Solar AtmospheresJim Nagy Senior Vice President Solar Manufacturing, Inc. Source: LinkedIn
Wrocław University of Science and Technology (WUST) is expanding its R&D capabilities in heat treatment and materials testing with a horizontal nitriding system. The furnace will support the university’s efforts in metallurgical research and collaborations with regional manufacturing industries, including testing forging dies for the automotive industry.
Marcin Stokłosa Technical Sales Manager NITREX Poland
The newly acquired Nitrex system is equipped with Nitreg® controlled nitriding technology for optimizing surface hardness, and Nitreg®-S technology for nitriding stainless steel. The system enables Poland-based WUST to conduct next-level materials research and leverage new technological and scientific capabilities to support industrial projects, optimizing heat treatment processes and enhancing the surface properties of metal parts. Furthermore, the furnace meets the stringent AMS 2759/10 standard for nitriding steel and AMS 2750 standard for temperature uniformity.
“While Nitrex primarily serves businesses in sectors such as automotive, aerospace, and manufacturing,” said Marcin Stoklosa, technical sales manager – EMEA region at Nitrex Poland, “our partnership with WUST underscores our commitment to advancing academic research and fostering innovations that directly benefit practical applications and advance metallurgical science globally. . . . I look forward to seeing WUST’s continued leadership in metallurgical research and its impact on both academia and industry.”
The press release is available in its original form here.
Heat TreatToday publishes eight print magazines a year and included in each is a letter from the editor, Bethany Leone. In this letter, Bethany ponders the variables that set leaders apart from the rest of the workforce. Are you a curious person? Does a pursuit of knowledge inform the approach you take to your place in the industry? Read more of what Bethany has discovered about the qualities of leaders in this letter, which first appeared in the September 2024 People of Heat Treatprint edition.
Feel free to contact Bethany at bethany@heattreattoday.com if you have a question or comment.
Leadership is nothing new. The buzz continues as we each have to lead, or be led, in every capacity of life. Too easily, that buzz becomes white noise, truisms filling an otherwise empty page. And that’s actually okay. I don’t mean that it’s good to become numb to valuable information, but the talk around leadership is confined to finding different ways to identify old truths. What we emphasize from space to space can only encapsulate a portion of leadership.
But this summer found me preparing for a book study I was to lead. (Would recommend the read: Till We Have Faces.) The questions to orient the group were sent in June, and we looked forward to converging our thoughts in a discussion mid-August. As the day approached, I found myself wrestling with ways to lead in a way where the group would not be harnessed to my way of thinking, nor would the reins be so loose that the discussion wanders into flat silence.
Coincidentally, I came upon podcast episode #66 on Rust Belt Rundown, interviewing a chronic entrepreneur. One old truism that I heard afresh was this:
Be a facilitator: Stay curious, asking the right questions at the right time.
It got in my head. “How does one stay curious?” This I had attempted again and again — in management, giving interviews, teaching — with varying measures of success. But I hadn’t unlocked this mindset. I pondered this in light of the upcoming book discussion.
The day came. I reconsidered what the plan would be. And we talked. And the discussion flourished. Somehow, I had remained curious. Was it just that? And why now?
A book group is a good place to explore curiosity.
It seems that curiosity was more than a mindset to assume, neither was it just a practice of asking questions at the right time. Its power comes in conjunction with several other attributes of leadership:
Know your expertise. It is not impossible to lead others if one is not an expert, but the best mentors, leaders, teachers, and managers all know what they know (and what they don’t know). For myself, the discussion was more enjoyable since I didn’t have to wrestle with the onslaught of new ideas; I could stay curious and consider when to ask the right question.
Know your exit strategy. What is the end goal of your leadership? Perhaps, like how my book discussion was to bring a group to a deeper place of shared understanding for independent thought others empowered, as with training new hires on inspection machinery. Whatever it is, know what you as a leader want to see happen when you “exit” the situation. This will determine how you begin, how you endure, and (of course) how you exit.
Know your lifestyle goal. This comes in opposition to “exit strategy,” but often, the end game is to become something or do something sustainably for life. It may mean, as it did for me, a mindset to not solve a problem that someone is working through and letting them work through tests, failures, and ultimate success for themselves.
Never undervalue character. It doesn’t matter how successful you are. A leader without character is only a powerful person. You may make things move, but you will move more people against you than with you.
The last of these four qualities is often the one that catches my eye when the final 40 Under 40 honorees are announced in each September magazine edition (click here to see the 2024 awardees). Perhaps this is the result of so many intelligent people lined up in rows of accomplishments. But somehow still, that father quietly serving a local charity apart from his vocation or young woman being thrilled to take on challenges because it assures a better working environment for her team kindles a desire to follow. In this magazine edition, there’s also a special focus on Heat TreatVeteran MG TJ Wright, and his willingness to take responsibility for the lives of those whom he leads only makes his accomplishments glow brighter (perhaps to his chagrin).
Being a leader isn’t the result of reading about it and forcing oneself to fake a certain set of skills. While those helpful truisms and guideposts about staying curious and asking the right questions can be helpful to prescriptively recognize leadership, the roots of a leader are deeper. In this edition, you’ll see these roots in hunger to know the industry, commitment to take the first step (even if the step trips us or turns us backwards), and ever-conscious care to place your people first.
Heat TreatToday offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry. Enjoy these 18 news items.
Equipment
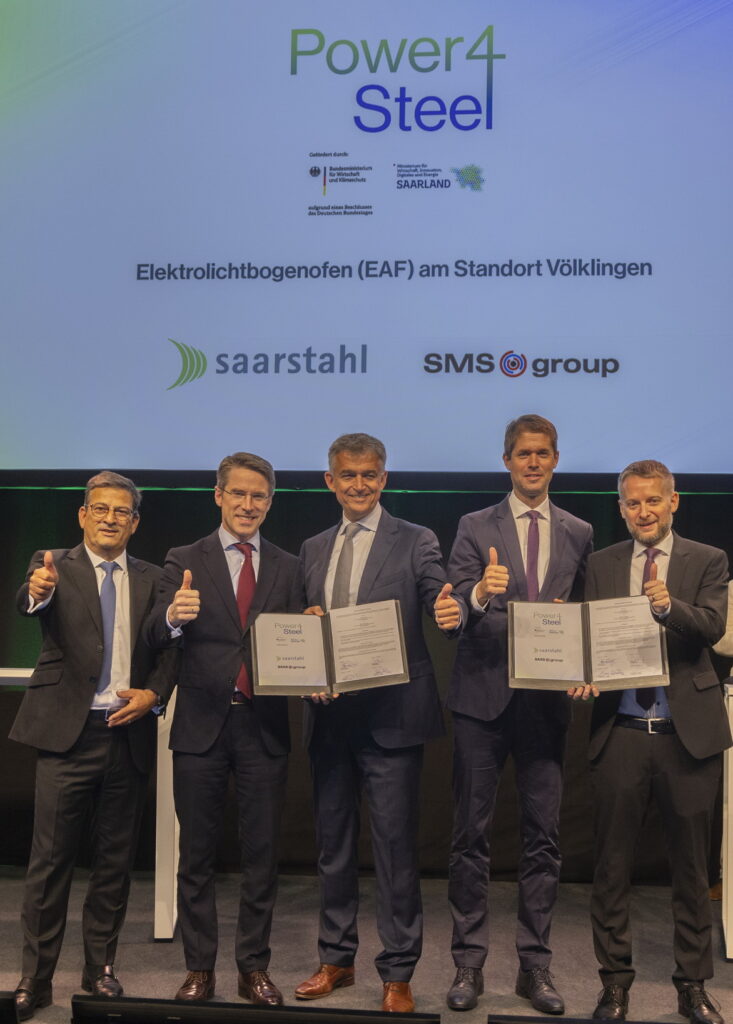
Saarstahl expands its production with an alternate current-electric arc furnace (AC-EAF) supplied by SMS group.
A Class A safety oven equipped with a solvent monitor and roll-in rack, meeting the stringent safety requirements of industries working with volatile materials, was recently shipped by industrial and laboratory ovens manufacturer Blue M.
A manufacturer in the defense industry has received shipment of a gas-fired walk-in batch oven from Wisconsin Oven Corporation, to be used for curing filament wound composite materials.
The Saarstahl team announces AC-EAF agreement with SMS Class A safety oven equipped to process volatile materialsGas-fired walk-in batch oven delivered to defense industry
Company & Personnel
Sean Patrick Murphy has been named product manager for laboratory and R&D furnaces at Centorr Vacuum Industries. He will be responsible for representing over 30 different vacuum furnace product lines to national laboratories, universities, and industrial sectors.
Charles (Charlie) Caldwell joins the team at Solar Atmospheres of Michigan Inc. as the quality manager for its new facility in Chesterfield.
Steel Goode Products LLC (SGP), a thermal spray specialist, has recently been acquired by Aalberts N.V., a provider of thermal spray coating and finishing services. The acquisition includes two operating facilities in Texas and one in Ohio.
The Wirco, Inc, team recently announced Chris Robbins as the new director of business development and Chad Kumfer to the position of director of sales.
Daniel Sonnenberg joins Nitrex Heat Treating Services as the new business development lead for North America. Daniel will focus on identifying and cultivating relationships with potential customers. His goal is to foster trust and drive growth by building enduring partnerships that deliver sustained value over time.
Dave Deiwart has begun a new position as president at Tracer Gas Technologies, based in Yorktown, Indiana. This follows a brief retirement after 35 years of providing leak detection and vacuum application support and training. Dave’s new focus will be on providing training and consulting.
Nel Hydrogen Electrolyser AS, a fully owned subsidiary of Nel ASA, has been awarded a grant from the EU Innovation Fund of up to EUR 135 million (over $145.4M USD) for industrialization of its next-generation pressurized alkaline technology. The technology is currently being prototyped, and the potential industrialization is planned at Herøya, Norway.
OTTO JUNKER GmbH, system providers for metallurgic processes and metal refinement, recently announced that the new business division OTTO JUNKER Solutions, which was established in late 2023, will be further expanded. The company’s focus will be on the development and implementation of green technologies. The new division is headed by R&D expert Tobias Mertens.
Sean Patrick Murphy Product Manager of Laboratory and R&D Furnaces Centorr Vacuum IndustriesCharles (Charlie) Caldwell Quality Manager – Chesterfield Solar Atmospheres of Michigan Inc.Chris Robbins Director of Business Development Wirco, Inc.Chad Kumfer Director of Sales Wirco, Inc.Daniel Sonnenberg Business Development Lead – America Nitrex Heat Treating ServicesTobias Mertens General Manager OTTO JUNKER SOLUTIONS GmbH
Kudos
Constellium SE has received the Supplier of the Year Award from Stellantis, recognized for its overall best-in-class performance as a long-time partner.
Gary Sharp, founder of Advanced Heat Treat Corp, has been honored with the Legends of Manufacturing Award at the Iowa Manufacturing Conference.
Global Thermal Systems (GTS) Mexico’s pyrometry laboratories recently completed the reaccreditation process in the ISO/IEC 17025 standard.
Rex Heat Treat has achieved its fourth consecutive merit-status Nadcap certification under the leadership of Conner Popo, quality assurance manager, and Vindon Griffin, technical services manager.
Aalberts surface technologies Dzierżoniów recently celebrated its tenth anniversary. Through acquisition and expansion, the company has grown from 16 employees in 2014 to a current team of over 90 employees, serving the automotive, aerospace, power, fasteners, agriculture, and mining sectors.
The Metal Treating Institute (MTI) recently celebrated its 2024 YES Management Training Program graduates at the final reception of Furnaces North America (FNA) 2024.
Bennett Heat Treating & Brazing Co. received the 2024 Master Craftsman Award, also known as the Heat Treater of the Year Award, at the Metal Treating Institute’s Final Night Dinner & Awards Ceremony following FNA 2024. The award was announced by Doug Glenn, publisher of Heat TreatToday along with a scholarship check for the heat treater to bestow upon a deserving young student going into heat treat.
Ingrid Joerg, Executive Vice President & Chief Operating Officer at Constellium, and Maxime Picat, Chief Global Purchasing & Supply Chain Officer, Greater Paris Metropolitan Region, at StellantisGary Sharp, founder of Advanced Heat Treat Corp, honored with the Legends of Manufacturing Award The Global Thermal Systems (GTS) Mexico’s pyrometry laboratories team completes ISO/IEC 17025 standard reaccreditation process
Cincinnati Radiator, a manufacturer of radiators and cooling products, recently expanded its production capabilities at its Fairfield, Ohio, facility with the addition of a vacuum aluminum brazing (VAB) furnace. This acquisition will enable the company to perform in-house radiator core brazing.
The VAB furnace, with a weight capacity of up to 2,000 lbs, is the third manufactured and installed by Ipsen.
Prasenjit Ray General Manager Cincinnati Radiator Source: Ipsen
“This furnace has so many recipes for us to use,” said Prasenjit Ray, general manager of Cincinnati Radiator. “We were planning to test it out for two months, but we weren’t expecting to get production-quality within those two months. What shocked and surprised me was that the first cores that came out were perfect. We’ve produced 10 (in the first month) and it runs like a new Cadillac.”
“We knew that we needed a way to make cores here. When customers had to rely on cores processed in China, it could mean a four-month lead time. If we had our own furnace, we could operate a just-in-time production,” said Ray. “We went with John Pease (Ipsen Regional Sales Representative) and Patrick McKenna (Ipsen USA President & CEO) to California to see a company operating two Ipsen VAB furnaces. Our team knew that, once we saw them in operation, we wanted to work with another company within the United States. Ipsen could offer great aftermarket support, and the delivery was worth the wait.”
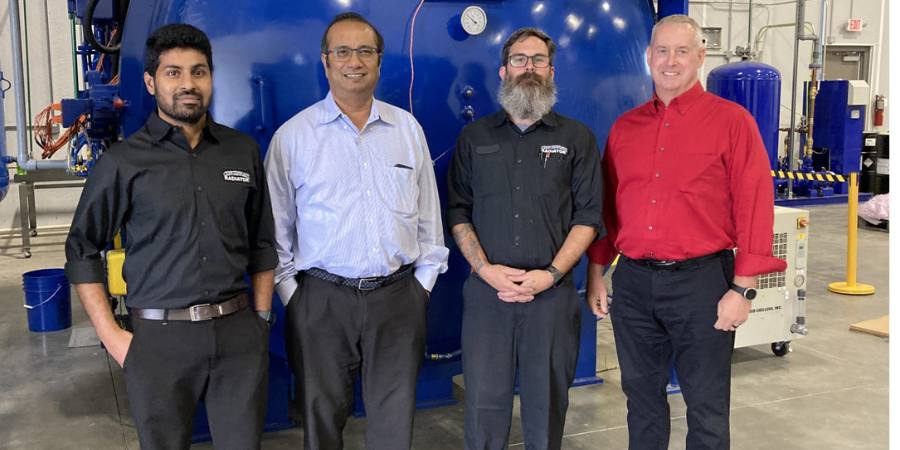
Main image (left to right): All of Cincinnati Radiator: Abhilash Uppala, Manufacturing Engineer; Prasenjit Ray, General Manager; Michael Petitt, Assistant Operations Manager; and James “Tom” Aynes, Accounting Manager. Source: Ipsen.
The press release is available in its original form here.
Today’s News from Abroad installment highlights some of the ups and downs in the global heat treating market which are largely driven by new technologies and sustainability initiatives. In growth news, a heat treater expands its product line with industrial furnaces and technologies and an Italian company invests in sustainable technology. In addition, a UK steelmaker closes its last remaining blast furnace.
Heat TreatTodaypartners with two international publications to deliver the latest news, tech tips, and cutting-edge articles that will serve our audience — manufacturers with in-house heat treat.heat processing, a Vulkan-Verlag GmbHapublication, serves mostly the European and Asian heat treat markets, and Furnaces International, a Quartz Business Mediapublication, primarily serves the English-speaking globe.
Heat Treater Expands Product Line To Include Vacuum Furnaces
Aichelin product range expands with vacuum furnaces and technologies Source: AICHELIN
“AICHELIN Group has expanded its product range to include innovative industrial vacuum furnaces and technologies. The modern, flexible, and environmentally friendly solutions were presented for the first time at the ‘HärtereiKongress’ in Cologne from October 8 to 10. The new vacuum furnaces are sold, designed, and produced by the joint venture company AICHELIN ST Vacuum GmbH, which was founded in May. With the addition of this important market segment, AICHELIN is now a full-service provider for heat treatment solutions.”
Italian Company Boosts Green Transition With Investment in ARP
Delna S.p.A. team at Tenova’s acid regeneration plant in Italy Source: Tenova
“Tenova, a developer and provider of sustainable solutions for the green transition of the metals industry, has been awarded a contract by Delna S.p.A., an ArcelorMittal CLN Distribuzione Italia Group company and primary provider of pickling service of coils and wire rod, for its plant in Brivio, Italy, for an acid regeneration plant (ARP) with a capacity of 2.000 l/h. Delna’s investment will boost the green transition of its plant, recovering the waste acid used in its pickling line and therefore minimizing its environmental footprint. The new ARP will be equipped with the BLUEdriven™ cutting-edge package solutions that will be controlled by a customized monitoring process, increasing production flexibility and optimizing operative costs, while guaranteeing minimal environmental impact.”
UK Steel plant shutters last remaining blast furnace
Final furnace shuts down at Tata’s UK plant Source: Tata Steel
“Tata Steel has begun the process of winding down operations at blast furnace 4 at Port Talbot and engineers have already started altering the raw materials poured into the top of the furnace to prepare for decommissioning. Blast furnace 5 was closed in July. The closure is part of Tata’s transition towards a greener form of steelmaking as it plans to build a £1.25 billion electric arc furnace for the Port Talbot site by 2027, which produces steel by melting scrap metal. The new Labour government agreed a taxpayer-backed deal earlier this month for the Port Talbot plant in which it will provide £500 million towards the construction of the new electric arc furnace at the site, with the plant’s Indian owners, Tata Steel, paying £750 million.”
The Heat Treat Doctor® has returned to offer sage advice to Heat Treat Today readers and to answer your questions about heat treating, brazing, sintering, and other types of thermal treatments as well as questions on metallurgy, equipment, and process-related issues.
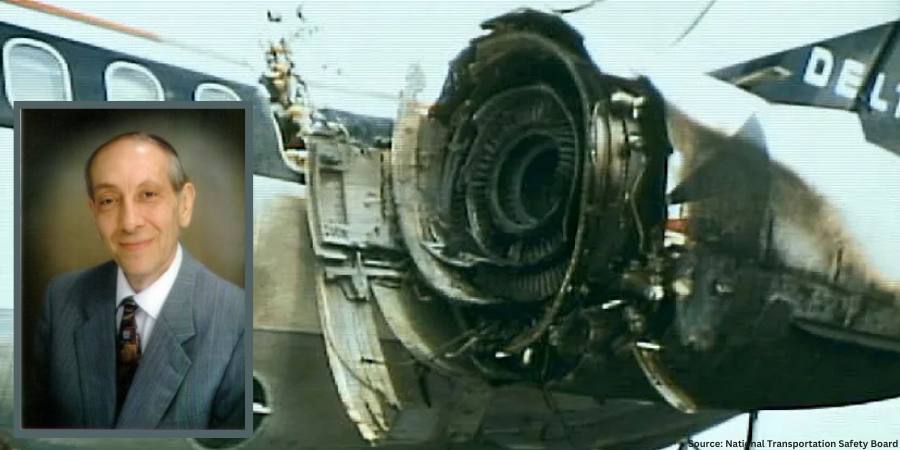
Product failures (Figure 1) can often be traced to deficiencies in design, materials, manufacturing, quality, maintenance, service-related factors, and human error to name a few. Examples of failures include misalignment, buckling, excessive distortion, cracking, fracture, creep, fatigue, shock, wear, corrosion, and literally hundreds of other mechanisms. Let’s learn more.
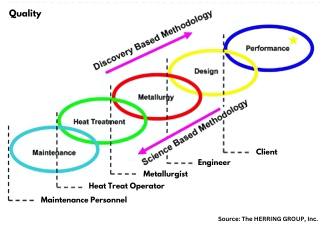
Figure 1. Image of damage to left fuselage and engine; fire damage to nacelle. Source: National Transportation Safety BoardFigure 2.: Model of material science depicting— key interactions and /interrelationships Source: The HERRING GROUP, Inc.
Whatever the source, it is important to recognize that it is next to impossible to separate the product from the process. Performance, design (properties and material), metallurgy (microstructure), heat treatment (process and equipment), and maintenance are all interconnected (Figure 2).
When considering ways to prevent failures from occurring, one must determine the factors involved and whether they acted alone or in combination with one another. Ask questions such as, “Which of the various failure modes were the most important contributors?” and “Was the design robust enough?” and “Were the safety factors properly chosen to meet the application rigors imposed in service?” Having a solid engineering design coupled with understanding the application, loading, and design requirements is key to avoiding failures. If failures do happen, we must know what contributed to them.
Let’s review a few of the more common failure modes.
Fracture Types on a Macroscopic Scale
Applied loads may be unidirectional or multi-directional in nature and occur singularly or in combination. The result is a macroscopic stress state comprised of normal stress (perpendicular to the surface) and/or shear stress (parallel to the surface). In combination with the other load conditions, the result is one of four primary modes of fracture: dimpled rupture (aka microvoid coalescence), cleavage, decohesive rupture, and fatigue.
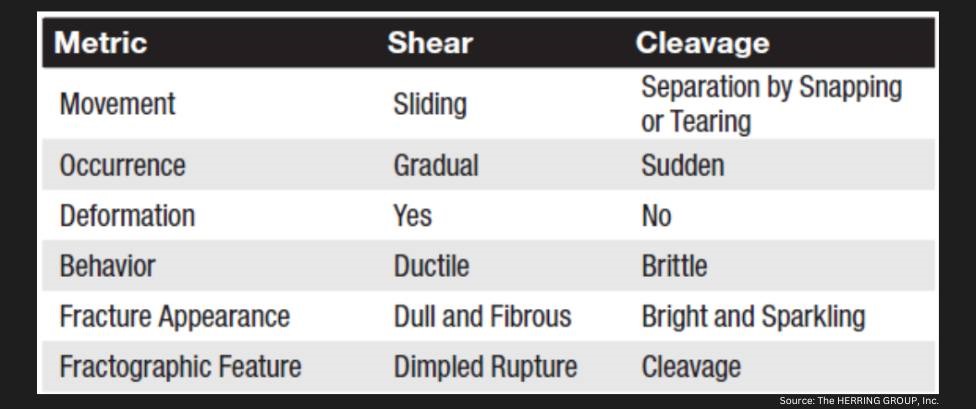
Virtually all engineering metals are polycrystalline. As a result, the two basic modes of deformation/fracture (under single loading) are shear and cleavage (Table 1). The shear mechanism, which occurs by sliding along specific crystallographic planes, is the basis for the macroscopic modes of elastic and plastic deformation. The cleavage mechanism occurs very suddenly via a splitting action of the planes with very little deformation involved. Both of these micro mechanisms primarily result in transgranular (through the grains) fracture.
Fracture Types — Ductile and Brittle
Numerous factors influence whether a fracture will behave in a ductile or brittle manner (Table 2). In ductile materials, plastic deformation occurs when the shear stress exceeds the shear strength before another mode of fracture can occur, with necking typically observed before final fracture. Brittle fractures occur suddenly and exhibit very little, if any, deformation before final fracture. (The following is based on information found in Wulpi, 1985.)
Ductile fractures typically have the following characteristics:
Considerable plastic or permanent deformation in the failure region
Dull and fibrous fracture appearance
Brittle fractures typically have the following characteristics:
Contact us with your Reader Feedback!
Lack of plastic or permanent deformation in the region of the fracture
Principal stress (or tensile stress) is perpendicular to the surface of the brittle fracture
Characteristic markings on the fracture surface pointing back to where the fracture originated
When examined under a scanning electron microscope, fracture surfaces seldom exhibit entirely dimpled rupture (i.e. ductile fracture) or entirely cleavage (i.e. brittle fracture), although one or the other may be more prevalent. Other fracture modes include intergranular fractures, combination (quasi-cleavage) fractures and fatigue fractures.
Fracture Types — Wear
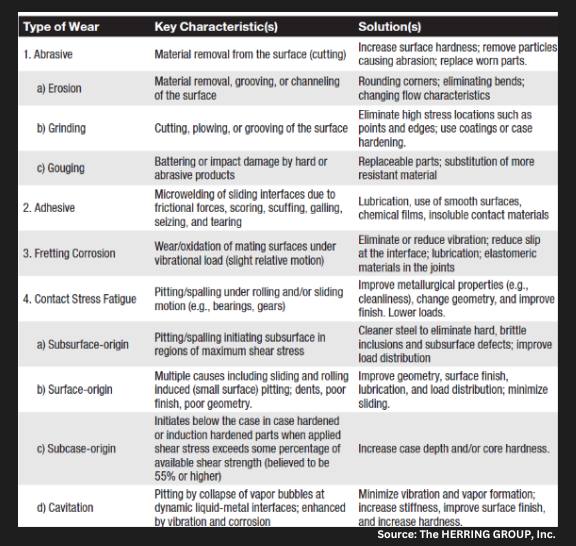
Wear (Table 3) is a type of surface destruction that involves the removal of material from the surface of a component part under some form of contact produced by a form of mechanical action. Wear and corrosion are closely linked, and it is important not only to evaluate the failure but to take into consideration design and environment and have a good understanding of the service history of a component.
Fracture Types — Corrosion
Corrosion is the destruction of a component by the actions of chemical or electrochemical reactions with the service environment. The major types of corrosion include galvanic action, uniform corrosion, crevice corrosion, stress-corrosion cracking, and corrosion fatigue. The mechanisms and effects created by each of these are well documented in the literature, as in Fontana and Greene’s Corrosion Engineering (1985) and Uhlig’s Corrosion and Corrosion Control (1985). It is critical to understand that the effects of corrosion are present to some degree in every failure analysis, which is one of the reasons why protecting fracture surfaces is so critical when sending parts for failure analysis.
Table 1. Differences between shear and cleavage fracture (Data referenced from page 23 of Wulpi, see References.) Source: The HERRING GROUP, Inc.Table 2. Typical characteristics of ductile and brittle fractures Source: The HERRING GROUP, Inc.Table 3. General categories of wear Source: The HERRING GROUP, Inc.
Final Thoughts
To avoid failures or their reoccurrence, it is important to document each step in the design and manufacture process (including heat treatment). In addition, careful documentation of failures if/when they occur is of critical importance as is assembling a team of individuals from different disciplines to perform a comprehensive investigation. This includes a thorough failure analysis to assist in determining the root cause (there is only one) and to avoid it from happening in the future.
Fontana, M. G., and N. D. Greene. Corrosion Engineering, 3e. McGraw-Hill Book Company, 1985.
Herring, Daniel H. Atmosphere Heat Treatment, Volume Nos. 1 & 2. BNP Media, 2014/2015.
Lawn, B.R. and T. R. Wilshaw. Fracture of Brittle Solids. Cambridge University Press, 1975.
Shipley, R. J. and W. T. Becker (Eds.). ASM Handbook, Volume 11: Failure Analysis and Prevention. ASM International, 2002.
Uhlig, H. H. Corrosion and Corrosion Control. John Wiley & Sons, 1963.
Wulpi, Donald J. UnderstandingHow Components Fail. ASM International, 1985.
About the Author
Dan Herring “The Heat Treat Doctor” The HERRING GROUP, Inc.
Dan Herring has been in the industry for over 50 years and has gained vast experience in fields that include materials science, engineering, metallurgy, new product research, and many other areas. He is the author of six books and over 700 technical articles.