In honor of Presidents' Day, Heat TreatToday takes a cue from the U.S. penny, where we find embossed on the copper coin the image of one of the two U.S. presidents celebrated on this day, President Abraham Lincoln (16th). The link below will lead you to an article on the basics of heat treating copper and copper alloys; their end products, including wire and cable, sheet, strip, plate, rod, bars, tubing, forgings, castings, and powder metallurgy shapes; and the purposes for heat treating these metals, such as homogenizing, annealing, stress relieving, and precipitation hardening.
FCA US recently announced that the new 2018 Jeep® Wrangler will be manufactured with lightweight, high-strength aluminum for closures, which includes parts of the doors, fenders, swing gate, and windshield surround, boosting fuel economy with a 200 pounds lighter structure than the previous steel version and an improvement of three miles per gallon in gas mileage. Jeep enthusiasts will also find it easier to remove the doors, which will be 14 pounds lighter compared to previous models.
Global aluminum rolled products manufacturer Novelis will supply the aluminum for the next generation Wrangler from its facilities in Oswego, New York, and Kingston, Ontario.
By incorporating aluminum into this design, FCA US joins a number of automakers that are turning to aluminum for the benefits they see in vehicle performance, agility and safety.
15 Quick Heat Treat News Items To Keep You Current
The heat treat industry is one of people transitioning and companies executing business, achieving goals, and receiving acknowledgments. Heat TreatToday offers News Chatter, a feature highlighting representative moves, transactions, and kudos from around the industry.
Personnel and Company Changes and Moves
Roberto Pancaldi, current Tenova Metals chief operating officer, has become the new Tenova Metals CEO, directly reporting to Andrea Lovato, CEO of Tenova.
Roberto Pancaldi, Tenova Metals CO
The Aluminum Federation, the trade body for the UK aluminum industry, has announced that appointment of a new chief executive. Mr. Tom Jones joins the organization from MMC Hardmetal UK, part of the Mitsubishi Materials group, where he was general manager. Tom has more than 35 years experience of working in manufacturing.
The Board of GKN Group plc has announced that Anne Stevens, currently Interim Chief Executive, has agreed to become the Group’s new Chief Executive with immediate effect. It was added that since her appointment, Stevens has taken leadership of an ongoing and wide-ranging internal review of all GKN’s businesses which has culminated in the development of a transformation plan to improve GKN’s performance.
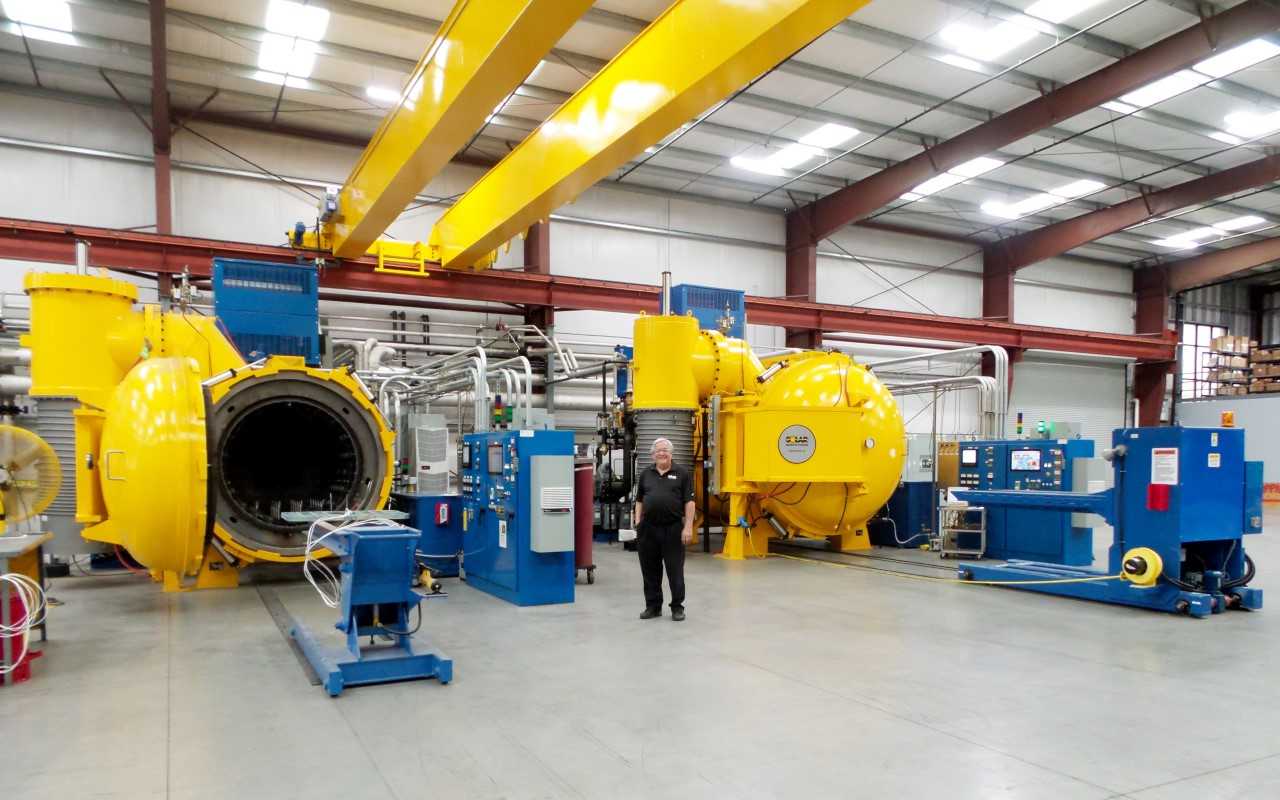
Solar Atmospheres of California's expansion includes installation of 4 new furnaces purchased from Solar Manufacturing, Inc
Solar Atmospheres of California (SCA) announce the completion of its most recent facility expansion. Project expansion began taking shape in July 2016 with groundbreaking for a new 25,000 sq. ft. building. In preparation for the added growth, SCA has procured an additional four vacuum furnaces from sister company Solar Manufacturing (SMI) based in Souderton, Pennsylvania.
Equipment Transactions
a heat treatment line from SMS group
German metal processor Ilsenburger Grobblech GmbH ordered a new heat treatment line from SMS group. The line, project name "Adjustage II", will be consist of a shot-blaster, two roller hearth furnaces, the MultiFlex-Quench®, a plate leveler, a cleaning and priming line, and a water treatment plant and be capable of processing more than 300,000 tons of heavy plate annually. Commissioning is scheduled to take place early in 2020.
Wisconsin Oven Corporation shipped two electrically heated standard horizontal quench systems to an aluminum manufacturer, each designed to heat 1,000 pounds of aluminum to a 950°F operating temperature with qualified operating temperature ranges of 775°F and 1,075°F.
Grieve recently supplied a 1000°F (538°C) top-loading oven that will be used for curing composite materials in large molds at a manufacturer’s facility. Workspace dimensions measure 168 inches wide x 48 inches deep x 48 inches high, and 120 kW are installed in lncoloy -sheathed tubular heating elements. A 12,500-CFM, 10-HP recirculating blower provides horizontal airflow.
Baker Furnace
Graftech Advanced Graphite Materials in Lawrenceburg, Tennessee, recently divested assets to refractory manufacturer Allied Mineral Products, Inc., located in Columbus, Ohio, and GTRefractory Solutions LLC in Wilmington, Delaware. Allied purchased the intellectual property rights to a collection of refractory cements and pastes, and GT Refractory Solutions acquired assets such as carbon and semi-graphite carbon brick, cement, pastes, porous carbons and graphite powders specialized for use in the steel, ferroalloy and iron industries.
Baker Furnace, Brea, Calif., the west coast division of the Thermal Product Solutions (TPS), moved to a new 40,000 sq-ft manufacturing space facility in 2017, which contributed to record shipments of custom and standard units in a variety of configurations. Among other projects, drop-bottom furnaces, crucible furnaces, car bottom furnaces, and batch ovens will be used for a variety of applications in the heat treating, foundry, composites, and automotive industries.
HBD Industries acquires True Position Technologies LLC
HBD Industries announced the expansion of its Precision Components Platform through the acquisition of True Position Technologies LLC (“True Position”), based in Valencia, California. A leading provider of complex machined components for flight control applications, True Position specializes in manufacturing high specification components that require multiple machining, testing and finishing processes all within extremely tight tolerances.
Accreditations, Certifications, Patents, and More
Conrad Kacsik Instrument Systems, Inc., has been reaccredited for ISO-IEC 17025:2005 by A2LA, a continuous A2LA accreditation since 2000.
Heat treaters Metallurgical Processing Inc., based in New Britain, Connecticut, has been awarded a 24-month Nadcap accreditation after being audited to 10 checklists.
Bodycote HIP now counts nine Nadcap-accredited sites with the recent award to the Surahammar, Sweden, location.
Advanced Heat Treat Corp., which has held Nadcap accreditation since 2013, has been awarded Nadcap Merit status for Heat Treating (Ion Nitriding) at the MidPort location in Waterloo, Iowa. This is the highest accreditation period that can be earned. "We are proud to achieve Merit status for the third time in a row and be granted a 24-month accreditation. We hope our customers take pride in the fact they send their parts to AHT," stated John Ludeman, Director of Metallurgy and Quality Excellence.
Bodycote, the world’s largest provider of heat treatment and specialist thermal processing services, announced that its Surahammar, Sweden, Hot Isostatic Pressing (HIP) location has earned its Nadcap accreditation. The Surahammar site has been producing Powdermet® Near Net Shape (NNS) and Selective Surface Net Shape (SSNS) components for many years, using its long experience of manufacturing complex, high integrity components from powder metal to serve markets such subsea, oil and gas, marine, nuclear, tool steel and automotive. Bodycote HIP now has nine Nadcap-accredited sites.
SAE International, Warrendale, Pa., announces that technical standard AMS2750 – Pyrometry, has received complete recognition by the U.S. Federal Drug Administration Center for Devices and Radiological Health, and it has been added to its list of recognized consensus standards database, List #47.
Heat TreatToday is pleased to join in the announcements of growth and achievement throughout the industry by highlighting them here on our News Chatter page. Please send any information you feel may be of interest to manufacturers with in-house heat treat departments especially in the aerospace, automotive, medical, and energy sectors to the editor at editor@heattreattoday.com.
A German steelmaker recently ordered a five-strand billet caster for their steelplant in Völklingen, designed for an annual capacity of 850,000 tons of billets.
The new casting machine to be installed by SMS Group for Saarstahl AG, a leading manufacturer of high-quality steel grades, will produce 7 x 7 foot (180 x 180 millimeter) square billets in a wide range of steel grades, including bearing steels, spring steels, cold heading wire rod and free-cutting steels. Products made of these steel grades are used in the automotive industry and in mechanical engineering applications.
Aluminium stud meets steel sheet IPH researchers have already succeeded in creating a form-fit connection. Now they want to realize a material bond between the two parts. (Photo: IPH)
Groundbreaking research on a forging process in Hanover, Germany, has taken place in which bulk aluminum parts can be bonded with steel sheets during the forming process, eliminating the usual joining step. This would contribute to a faster and more efficient production of load-optimized components.
The Institute of Welding and Machining (ISAF) of TU Clausthal cooperated with the Institut für Integrierte Produktion Hannover (IPH) gGmbH in releasing their joint research aiming to be the first to combine two lightweight materials and construction approaches to make the process more efficient. The project, known as hybrid compound forging, focused on the challenge of integrating steel and aluminum with a third material to avoid brittle intermetallic phases.
The researchers’ idea is to form and join a steel sheet and a solid aluminum stud in one process step. In the past, the individual parts have been formed first and then joined in a second step, for example using stud welding. The idea of hybrid compound forging is to eliminate the subsequent joining step.
Hybrid compound forging The novel lightweight production process firmly bonds bulk aluminium parts to steel sheets – already during the forming process without an extra joining step. (Photo: IPH)
Since aluminum has a considerably lower melting point than steel, the joint forming process is more complicated. Moreover, the mixing of steel and aluminum creates brittle intermetallic phases, a material bond which is not strong enough and thus unsuitable for car manufacture. For this reason, the researchers employ zinc-plated steel sheets and aluminum studs: Zinc firmly bonds to aluminum as well as to steel without creating brittle phases.
Within the scope of the research project, the researchers are tasked with determining the most suitable process conditions – i.e. optimal temperature, pressure and speed for successfully forming and joining the two parts. They also try to identify the suitability of the novel process with respect to different types of sheet thicknesses and stud shapes and to determine the joining zone’s capacity to withstand load as well as the machinability of the hybrid part after joining. The researchers have already succeeded in combining sheet and bulk metal parts of different materials in one single forming step – but only as a prototypic form-fit connection between steel sheet and aluminum stud. In the current research project “Hybrid Compound Forging”, the researchers are going for a material bond using zinc as filler material which also offers advantages as to contact corrosion in the steel-aluminum material combination.
In the future, hybrid compound forging could be used in the automotive and aerospace industry to produce components, such as longitudinal beams, tail lamp mounts or cargo tie-down rings.
Aluminum sheets and heat treating services are among the categories of upwardly trending activity that Tony Uphoff recently reported on at Thomasnet.com. In addition to how well each area is doing above historical averages, the analysis includes this tidbit: “according to U.S. census data, 96 percent of heat treatment companies employ fewer than 100 workers; 68 percent employ fewer than 20.”
A new sintering line suitable for PTFE insulation has been designed and installed by a manufacturer for a producer of aeronautic cables. This machine is suitable for the thermal treatment of the insulation on conductors with diameter 1-7 inches.
In order to guarantee the uniformity of the process, WTM, which specializes in the application of materials for aircraft and aerospace cables and devices particular attention, focused on the definition of the temperature profile to be applied to the cable passing through the sintering ovens. Considering the maximum cable dimension, WTM, which is located in Austria and Italy opted for the induction preheating in the first part of the equipment. The sintering process occurs successively by means of three infrared ovens, equipped with independent control zones, each of them with a maximum temperature of 1022°F.
A French manufacturer of high-performance automobiles has developed the largest titanium functional component produced by additive manufacturing in a 45-hour process that includes heat treating to achieve minimum weight with maximum stiffness.
The development department of Bugatti Automobiles, S.A.S., which established itself as a pioneer for new technical developments and innovations in the extreme performance sector of the auto industry with the Veyron and Chiron super sports car models, recently announced the successful design of an eight-piston monobloc brake caliper that can be produced by 3-D printing. Bugatti, in cooperation with Laser Zentrum Nord of Hamburg, bypassed aluminum and turned to aerospace-grade titanium alloy, with the scientific designation of Ti6AI4V, for a tensile strength of 1,250 N/mm2. This means that a force of slightly more than 125 kg (276 lbs.) be applied to a square millimeter of this titanium alloy without the material rupturing.
The development time for the 3-D-printed titanium brake caliper was about three months. The basic concept, the strength and stiffness simulations and calculations and the design drawings were sent to Laser Zentrum Nord by Bugatti. The institute then carried out process simulation, the design of the supporting structures, actual printing and the treatment of the component. Bugatti was responsible for finishing.
The printing process results in a brake caliper complete with supporting structure which maintains its shape until it has received stabilizing heat treatment and reached its final strength. Heat treatment is carried out in a furnace where the brake caliper is exposed to an initial temperature of 1,292°F (700°C), falling to 212°F (100°C) in the course of the process to eliminate residual stress and to ensure dimensional stability.
The new titanium brake caliper, which is 16.2 in. long (41 cm), 8.2 in. wide (21 cm) and 5.4 in. high (13.6 cm), weighs only 6.4 lbs. (2.9 kg). In comparison with the aluminum component currently used, which weighs 10.8 lbs. (4.9 kg), Bugatti could, therefore, reduce the weight of the brake caliper by about 40% at the same time as ensuring even higher strength by using the new part. The result is a delicately shaped component with wall thicknesses between a minimum of only one millimeter (.039 in.) and a maximum of four millimeters (.157 in.).
“It was a very moving moment for the team when we held our first titanium brake caliper from the 3-D printer in our hands,” said Frank Götzke, head of New Technologies in the Technical Development Department of Bugatti Automobiles S.A.S, which is a brand of Volkswagen AG. “In terms of volume, this is the largest functional component produced from titanium by additive manufacturing methods. Everyone who looks at the part is surprised at how light it is – despite its large size. Technically, this is an extremely impressive brake caliper, and it also looks great.”
The first trials for use in production vehicles are due to be held in the first half of the year.
A producer of steel and related products headquartered in Charlotte, North Carolina, recently selected the MI.DA® Micromill technology of Pennsylvania-based steel distributor Danieli to expand its presence in the Midwest with a new operation to be built in Sedalia, Missouri.
Nucor Corporation contracted Danieli to design the plant to produce in excess of 350,000 short tons per year of straight rebar products, in sizes, grades and custom lengths. The design of the mill will allow for the future installation of a spooling line for the production of twist-free, easy-to-store and transport, compact heavy coils up to 11,000 lbs.
The mill is scheduled to be in operation by the third quarter of 2019. It will be the third such mill in the USA alone and will join eight other MI.DA® Micromills with capacities ranging from 300,000 to 800,000 tons/year already (or soon to be) in operation worldwide.
As sure as the Alabama Crimson Tide wins NCAA championships, more and more representatives of the global automotive industry are finding the state of Alabama an appealing location for expansion of manufacturing operations. In 2017, Mercedes announced plans to build a new electric battery plant at its facility in Tuscaloosa, and Honda began expansion of its Lincoln factory near Birmingham.
Last month, Toyota and Mazda announced a joint venture, named Project New World, to invest $1.6 billion in a new plant in Huntsville, Alabama, where Mazda will produce a crossover model new to North American car buyers and Toyota will produce the Corolla, not far from the company’s existing engine plant.
With new automakers come automotive suppliers and industry support, therefore, the question is whether the good news of auto industry growth in Alabama will spell good news for heat treaters in the state. Dave Sullivan, product analysis manager at AutoPacific Inc., an automotive research company, said the Toyota-Mazda factory itself is a huge asset for the state, but it will also cause economic ripples by bringing spinoff jobs at suppliers and service companies in the area.
Don Hendry, president of Pinson Valley Heat Treating
That sounds like good news. We asked a commercial heat treater in Alabama.
Don Hendry, president of Pinson Valley Heat Treating, outside of Birmingham, notes that most major automakers do captive heat-treating or depend upon processing at established overseas locations, and posits that heat treaters who serve automotive support and parts suppliers will likely see improved business, especially since most commercial heat treating companies have already begun adjusting their equipment and facilities in response to the upward trend in the use of light-weight aluminum alloy for sheeting and structural applications. Pinson Valley added a drop bottom furnace in 2001 to solution treat and age aluminum parts due to the increase in automotive manufacturing.