State of the Art Furnace Designed, Delivered for Aerospace Supplier

A global aerospace supplier is the recipient of a newly designed, state of the art furnacethe first of its type in the worldboasting an entire side-on opening, with a door running the full eight-meter width, while maintaining an exceptionally high level of temperature uniformity.

At 1.75m high, the furnace enables two components to be loaded at one time by way of a trolley, with a gap of half a meter between the external tracks and the internal fixturing. This gap was required to enable the doors to close. The trolley then cantilevers across the gap, thanks in part to the unique design of its axels.

An additional challenge was the temperature conformity and accuracy needed by the customer. The maximum temperature difference across the part was specified to be no greater than +/- 2.5°C, to a maximum temperature of 175°C to be maintained for a number of hours to facilitate the heat treatment of highly specialized, CNC-machined aluminum components.

The furnace was designed, delivered and installed by U.K.-based AeroThermal, which designs and manufactures thermal processing equipment for clients in the aerospace, motorsport, military, electronics and tobacco sectors. Accuracy of better than +/- 2°C was achieved by using a multizone heating system on the top and bottom, with four different banks of heater cassettes and four fans, to ensure temperature uniformity. The cassettes were sheathed electrical heaters and produce 240kW.

The furnace is made of a steel structural frame and steel paneling. It is also highly insulated, to the extent that it is possible to touch the vast majority of the oven wall at a temperature marginally above that of ambient whilst the furnace is in operation, minimizing energy usage.

Aerothermal also designed and built in-house a plc control system with two controllers: one for the air temperature, one for the parts’ temperatures. When the manufacturing process is complete, the oven’s temperature is reduced by using a power-assisted ambient cooling system, through external ducts.

State of the Art Furnace Designed, Delivered for Aerospace Supplier Read More »

Memoirs of Heat Treating Leader Assigned October Publication Date

William R Jones, CEO of Solar Atmospheres Group and Author of The Golden Nugget: An Entrepreneur Speaks

Part memoir, part technical guide, The Golden Nugget: An Entrepreneur Speaks, by William R. Jones and co-author Heather Idell, is set for publication in October 2017, Solar Atmospheres announced Thursday.

The book includes the memoirs of Bill Jones, the founder and owner of Solar Atmospheres and a leader in the heat treating industry, taking the reader on a journey through Mr. Jones’ life and career–from a curious, technically adept young man to becoming one of the most lauded and respected leaders in the vacuum furnace and heat treating industries. Providing insight into the mind of an entrepreneur, the book also chronicles the technical innovations that propelled Mr. Jones to the forefront of these industries.

CLICK HERE TO ORDER THIS BOOK.


Memoirs of Heat Treating Leader Assigned October Publication Date Read More »

Panasonic Acquires AMP of UK


Source: ACR News

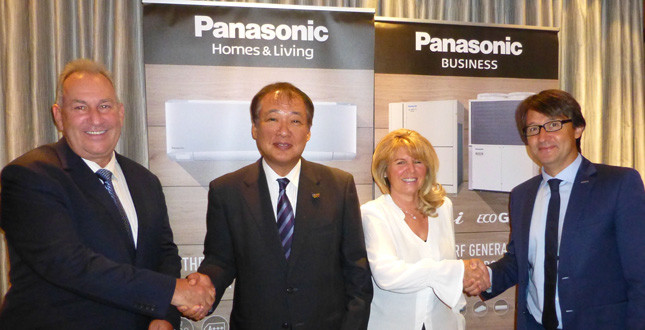
Left to right: Martin Michaelson (AMP), Makoto Takahashi (Panasonic), Polly McConachie (AMP), and Enrique Vilamitjana (Panasonic)


A.M.P. Air Conditioning Ltd (AMP) has recently been acquired by Panasonic Corporation as part of the latter’s plans to expand service in the commercial and industrial heating and cooling sectors.

Read more: “Panasonic Acquires UK Air Conditioning Equipment Distributor AMP”

Image above shows the Panasonic and AMP staff.

Panasonic Acquires AMP of UK Read More »

Tool and Die Failure, Heat Treatment Causes and Corrections

George Vander Voort has a background in physical, process and mechanical metallurgy and has been performing metallographic studies for nearly 50 years. He is a long-time member of ASTM Committee E-4 on metallography and has published extensively in metallography and failure analysis. He regularly teaches MEI courses for ASM International and is now doing webinars. He is a consultant for Struers Inc. and will be teaching courses soon for them.  His website, www.georgevandervoort.com, not only details his consulting services but also houses over one hundred articles, studies, or instructional graphics on topics related to physical, process and mechanical metallurgy. The following is an overview and an excerpt of failure factors from “Identifying the Cause of Tool and Die Failure”, published in 2016. There are particular elements to this study which relate to the heat treat industry.

Steels used for tools and dies differ from most other steels in several aspects. First, they are used in the manufacture of other products by a variety of forming processes. Second, tools and dies are generally used at a higher hardness than most other steel products; 58 to 68 Rockwell C is a typical range. Dies for plastic molding or hot working are usually used at a lower hardness, typically from 30 to 55 Rockwell C.

These high hardness values are required to resist anticipated service stresses and to provide wear resistance. However, the steels must also be tough enough to accommodate service stresses and strains without cracking. Premature failure caused by cracking must be avoided, or at least minimized, to maintain minimum manufacturing costs. Unexpected tool and die failure can shut down a manufacturing line and disrupt production scheduling. Tools and dies must also be produced with the proper size and shape after hardening so that excessive finishing work is not required. Heat-treatment distortion must be controlled, and surface chemistries must not be altered. Because of the careful balance that must be maintained in heat treatment, control of the heat-treatment process is one of the most critical steps in producing successful tools and dies. In addition to controlling the heat-treatment process, tool and die design and steel selection are integral factors in achieving tool and die integrity.

The following list is excerpted and abridged to highlight phases or processes related to heat-treat. The explanation behind each factor is available at the original post.

A number of factors can be responsible for tool and die failures. They include:

1. Mechanical design. The design must be compatible with the steel grade selected, the procedures required to manufacture the tool or die, and the use of the tool or die. . . .

The importance of good design cannot be overemphasized. Poor design can cause or promote heat-treatment failures before any service life is obtained, or it may reduce service life dramatically.

In designing a tool or die, a host of factors must be considered. In practice, separating the design stage from grade selection is difficult because the two steps are interdependent. The choice of a certain grade of steel, such as one that must be brine- or water-quenched, will have a substantial bearing on all aspects of design and manufacture. In general, any steel grade that requires liquid quenching demands very conservative, careful design.

Air-hardening grades tolerate some design and manufacturing considerations that could never be endured by a liquid quenching grade. The design must also be compatible with the equipment available–heat-treatment furnaces and surface-finishing devices, for example. . . .

2. Grade selection. The grade of steel selected must be compatible with the design chosen, the manufacturing processes used to produce the tool or die, and the intended service conditions and desired life. . . .

3. Steel quality. The material must be macrostructurally sound, free of harmful inclusions to the degree required for the application, and free of harmful surface defects.

Despite the care taken in the manufacture and inspection of tool steels, faulty materials occasionally cause tool and die failures. However, such problems are rare. The most common of these defects are voids from secondary pipe, hydrogen flakes, surface cracks, porosity or microvoids, cooling cracks, segregation, and poor carbide distributions. Improper control of annealing may also produce non-uniform carbide distribution or carbide networks that may influence heat-treatment uniformity, lower ductility, or impair machinability.

4. Machining processes. The machining processes used to produce the tool or die must not alter the surface microstructure or surface finish and must not produce excessive residual stresses that will promote heat-treatment problems or service failures.

Machining problems are a common cause of tool and die failures. It is generally best to avoid machining directly to the finish size unless pre-hardened die steels are used. Obtaining perfect control of surface chemistry and size during heat treatment is difficult. Thus, some final grinding is usually needed after heat treatment. The presence of decarburization is generally quite detrimental. Also, because stresses are high in heat treatment and in service, rough machining marks must be avoided. Identification stamp marks are another common source of failures in heat treatment and in service; they should be avoided.

5. Heat-treatment operation. Heat treatment of tools and dies must produce the desired microstructure, hardness, toughness, and hardness at the surface and in the interior.

Improper heat-treatment procedures are the single largest source of failures during heat treatment, in subsequent processing steps, or in service. Each tool steel grade has a recommended austenitizing temperature range, which is generally rather narrow; a recommended quench medium; and recommended tempering temperatures and times for optimum properties. Some grades are more forgiving than others.

6. Grinding and finishing operations. Grinding and finishing operations must not impair the surface integrity of the component.

7. Tool and die setup. Alignment of tools and dies must be precise to prevent irregular, excessive stresses that will accelerate wear or cause cracking.

8. Tool and die operation.


Read the full study and report, including images of tool steel failure examples, at “Identifying the Cause of Tool and Die Failure”.


 

Tool and Die Failure, Heat Treatment Causes and Corrections Read More »

Atmosphere Engineering to Bolster UPC’s Expansion

United Process Controls (UPC) announced the acquisition of Atmosphere Engineering Company (Atmosphere Engineering), a Wisconsin-based, family-owned and -operated business led by brothers Jason and Eric Jossart. Founded in 2002, Atmosphere Engineering designs and manufactures industrial flow control products, furnace control products, and data acquisition software for clients in North America, South America, and Europe.

Atmosphere Engineering will bolster UPC’s product offering and technical competencies. While the acquisition expands the company’s customer base, it will also provide a platform to expand into new markets and extend market penetration in the flow controls market.

Additionally, UPC has enhanced its organizational structure to align with the future direction of the company and its foundation for continued growth. As part of the new structure, Jason Jossart will serve as the company’s Vice President of Operations and report directly to UPC’s President, Paul Oleszkiewicz; Eric Jossart will join as Director of Sales, Heat Treat and report directly to Vice President of Sales and Marketing, Patrick Torok.

“Atmosphere Engineering represents a great fit with our flow and process controls business and is in line with UPC’s strategic direction to expand its repertoire of products and leadership in the industry,” commented UPC President Paul Oleszkiewicz. “Jason and Eric run an incredible business, and we are excited to welcome them and the entire Atmosphere Engineering team to the UPC family. This acquisition shows our ongoing commitment to provide customers worldwide with a comprehensive portfolio of process and flow control solutions that optimize the quality, safety, and control of heat treating operations.”

Jason Jossart, founder and President of Atmosphere Engineering commented, “We at Atmosphere Engineering are very pleased to join forces with UPC. My brother Eric and I have worked hard to build Atmosphere Engineering’s brand and reputation and are excited to see it grow further as part of UPC. Together we will emerge as a leader in flow and process controls to the heat treat industry and address new market challenges and opportunities for technical innovation and growth.”

Atmosphere Engineering to Bolster UPC’s Expansion Read More »

British Firms Explore Heat Treatment Regimens for Alloy in Additive Manufacturing

Two British firms recently announced a collaboration to establish process parameters for the use of aluminum alloy in additive manufacturing (AM), a project that will include the investigation of heat treatment regimens to deliver optimum properties in AM components for applications in multiple industries, including the aerospace sector.

Mike Bond, Aeromet

Renishaw, a global engineering technologies company based in Gloucestershire providing solutions and products for the aerospace, medical, energy and manufacturing sectors, and Worcestershire’s Aeromet International, a leading supplier of cast metal parts for the global aerospace and defense industries, recently debuted the highly refined alloy at the Paris Air Show in June. The two companies are working together to establish additive manufacturing process parameters and material properties for Aeromet’s A20X® aluminum alloy and to optimise the processing techniques for the alloy on Renishaw metal AM systems.  The results of these developments and the heat treatment research will be made available to Renishaw and Aeromet customers.

A family of high-strength aluminum alloy technologies developed and patented by Aeromet, A20X® includes the Metallic Materials Properties Development and Standardization (MMPDS) approved A205 casting alloy and AM205 powder for additive manufacturing.

Marc Saunders, Renishaw

“A20X is being rapidly adopted for additive manufacture of aero engine, airframe, space, defense and automotive parts.  It’s unique combination of high strength, high ductility and performance at high operating temperatures make it ideal for light-weight, stressed components.  We look forward to making processing techniques for this innovative alloy more widely available to accelerate its adoption,” said Mike Bond, Director of AMT a Division of Aeromet.

“Renishaw’s metal AM systems feature high-power lasers, an inert processing environment, and open parameters,” said Marc Saunders, Director of Global Solutions Centres at Renishaw, “making them ideal for supporting innovative new materials like A20X.  We are working closely with Aeromet to qualify this exciting new alloy on our machines. Through our network of AM Solutions Centres, we can help manufacturers to develop industrial AM processes using A20X.”

The two companies plan to release processing techniques and material properties information in the coming months.

Photo Credit: Aeromet/Monty Rakusen

British Firms Explore Heat Treatment Regimens for Alloy in Additive Manufacturing Read More »

Hoa Phat Orders 4 Blast Furnaces to Increase Production at Dung Quat Complex

Vietnamese steel producer Hoa Phat Steel has awarded a contract to an Italian steel production technology specialist for the design, supply, and supervision of four greenfield blast furnaces.

The project is part of the new Dung Quat iron and steel making complex committed to by Hoa Phat, which currently operates a 2 million metric ton per year (mtpy) iron and steel making plant in Hai Duong. The scope of the project also includes the hot blast mains, bustle mains, tuyere assemblies, level 2 automation systems and pulverized coal injection systems. The new plant will add 4 mtpy to Hoa Phat’s annual steelmaking capacity.

The four blast furnaces will have a 1080 m³ working volume and are designed for an annual production of 1 million tons of hot metal each. The furnaces will be supplied by Danieli Corus and equipped with the company’s high conductivity cooling and lining design based on copper plate coolers combined with graphite and silicon carbide refractories. The four furnaces will be completed and commissioned in sequence, with the fourth being scheduled for delivering the first hot metal in 2019.

Hoa Phat Orders 4 Blast Furnaces to Increase Production at Dung Quat Complex Read More »

Paulo Announces New Plant in Monterrey, Mexico

Heat treatment service provider Paulo has begun construction on a greenfield facility in Monterrey, Mexico.  The new plant will be completed in the fourth quarter of 2017 and processing of heat-treatment will begin in the first quarter of 2018.  Paulo will initially occupy 50,000 sqft with expansion up to 110,000 sqft.  Monterrey was chosen for its robust manufacturing community with close proximity to major providers of automotive, agriculture, aerospace and other industrial components.

Paulo will continue to add equipment throughout 2018.  Initially, the plant will serve the automotive industry, processing parts manufactured in Mexico. Paulo will also leverage automation with multiple robotic loading cells to improve safety in material handling while leaning production steps.


Paulo Announces New Plant in Monterrey, Mexico Read More »

Robots that Can Self-Heal like Humans


Source: Electronics 360

The human body has an amazing way to heal from injuries over time. Cut your hand, tear a muscle, break a bone and it typically returns to normal use over the course of time and treatment.

Now, researchers at Vrije Universiteit Brussel (VUB) in Belgium are applying this same principle to soft robots developing mechanisms for these machines to self-heal.

Read more: “Soft Robots that Can Self-Heal”

View video here.

Photo credit: Vrije Universiteit Brussel

Robots that Can Self-Heal like Humans Read More »

Heat Treating Projects Part of Pratt & Whitney Expansion

Aircraft engine maker Pratt & Whitney Canada is expanding its production at facilities in Québec with two recently announced furnace projects, with equipment supplied by local machining manufacturer Pyradia Belfab. The first is a low-temperature conveyor drying oven for steel parts complying with AMS2750 standards, and the second is a bottom-loading type furnace to be used for the stress relief of combustion chambers of P&W Canada aero engines. The latter unit will be a high temperature (2000 F) retort furnace using argon/nitrogen and hydrogen equipped with state of the art batching monitoring/logging capabilities.

The projects figure into an expansion effort by Pratt & Whitney, which includes a recently commissioned new fan blade manufacturing facility at its AutoAir plant in Lansing, Michigan. The new 93,000 square-foot facility adds to an already existing GTF fan blade production line in Lansing and is one of thirty dedicated manufacturing, production or assembly locations across the globe performing work on various parts and components of the GTF engine program.

“We are pleased to be a part of this successful engine program,” said Conor Tracy, general manager, Pratt & Whitney AutoAir. “The expansion of the Lansing plant is an opportunity for our employees to contribute to the future of the company, but it is also an exciting opportunity for Lansing to continue to participate in the advanced manufacturing sector and the economic growth of the region.”

In addition to the manufacturing expansion, Pratt & Whitney has four maintenance and repair operations (MRO) facilities to repair and overhaul GTF engines, and additional facilities will be added moving forward.


Heat Treating Projects Part of Pratt & Whitney Expansion Read More »