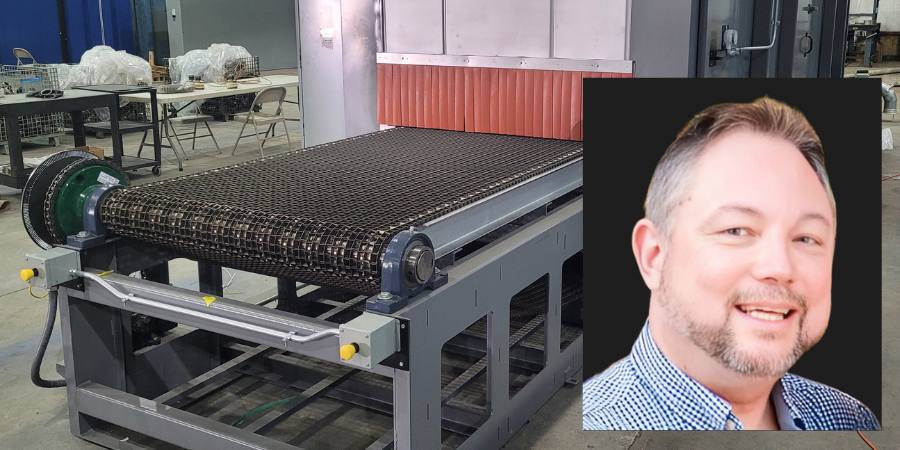
An auto parts manufacturer that specializes in the production of radiators and air conditioning systems recently ordered a fully electric furnace for brazing aluminum in a protective atmosphere. The EV/CAB line is designed for the production of tubular and plate-fin heat exchangers with uniform temperature distribution across the 1300 mm wide belt.
Piotr Skarbiński Vice President of Aluminum and CAB Products Segment SECO/WARWICK
SECO/WARWICK designed the uniform temperature distribution feature in the equipment to meet the company’s quality requirements of the finished products. The CAB line on order, the first this manufacturer has acquired from SECO/WARWICK, provides the continuous brazing of products with similar dimensions and features. The temperature is evenly distributed over the entire width of the belt due to several independent heating zones, resulting in long-term operation under industrial conditions.
“Uniform temperature distribution across the entire belt, regardless of how wide it is, is an important consideration influencing the final effect of the production,” said Piotr Skarbiński, vice president of the Aluminum Process and CAB Business Segment at SECO/WARWICK. “Our furnaces provide an optimal brazing temperature profile and a very clean atmosphere necessary to maintain high process quality. In China, we sell CAB lines for manufacturers of electric vehicle battery coolers, as well as for manufacturers of other heat exchangers. The furnaces on order by this partner are powered by electricity, making them ecological and free of CO2 emissions.”
Press release is available in its original form here.
In today’s News from Abroad installment, we highlight processing and initiatives that aim to improve operations and improve sustainability. Read more about a method used in the production of parts with complex geometries; a venture to create the world’s first fossil-free, ore-based steel with renewable electricity and green hydrogen; and a production plant that will generate around 9,000 tons of green hydrogen a year to be used for the production of carbon-reduced steel.
Heat TreatTodaypartners with two international publications to deliver the latest news, tech tips, and cutting-edge articles that will serve our audience – manufacturers with in-house heat treat. Furnaces International, a Quartz Business Media publication, primarily serves the English-speaking globe, and heat-processing, a Vulkan-Verlag GmbH publication, serves mostly the European and Asian heat treat markets.
Press Hardening Prevents Part Deformation
Press hardening neccessary due to part deformation during the rapid cooling phase induced by quenching
Source: Thermi-Lyon
“Press hardening serves a very specific purpose: to prevent part deformation during the rapid cooling phase induced by quenching. This process improves the performance of steels by giving them a martensitic structure without the need for reworking. Designed for high volume production of parts with complex geometries, press hardening is both highly effective and economical….
This process was initially developed for automotive manufacturers, to process large series of parts with complex geometries. In fact, this method is perfectly suited to the processing of large numbers of parts on a production line: since the cooling cycle is automatically programmed, it can be repeated ad infinitum. What’s more, the circulation of quenching fluid around the part held in the press results in uniform, controlled cooling that can easily be reproduced many times over.”
An electricity-based process gas heater for the hydrogen-based direct reduction process developed by HYBRIT (Hydrogen Breakthrough Ironmaking Technology)
Source: Kanthal
“Launched in 2016 as a joint venture owned by SSAB, LKAB, and Vattenfall, with support from the Swedish Energy Agency, HYBRIT aims to create the world’s first fossil-free, ore-based steel with renewable electricity and green hydrogen.
This involves shifting from coal-powered blast furnaces that use coal as a reduction medium to a direct reduction process using hydrogen produced via renewable energy. The first HYBRIT pilot plant in Luleå, Sweden, began operations in 2020, with commercial-scale production targeted by 2027.
Kanthal is proud to have contributed to HYBRIT’s groundbreaking journey by developing an electricity-based process gas heater for the hydrogen-based direct reduction process under the name Prothal®. This project showcased the feasibility of fossil-free industrial heating solutions and laid the groundwork for scaling up these technologies to meet the steel industry’s future needs.”
Largest Green Hydrogen Production Facility Underway
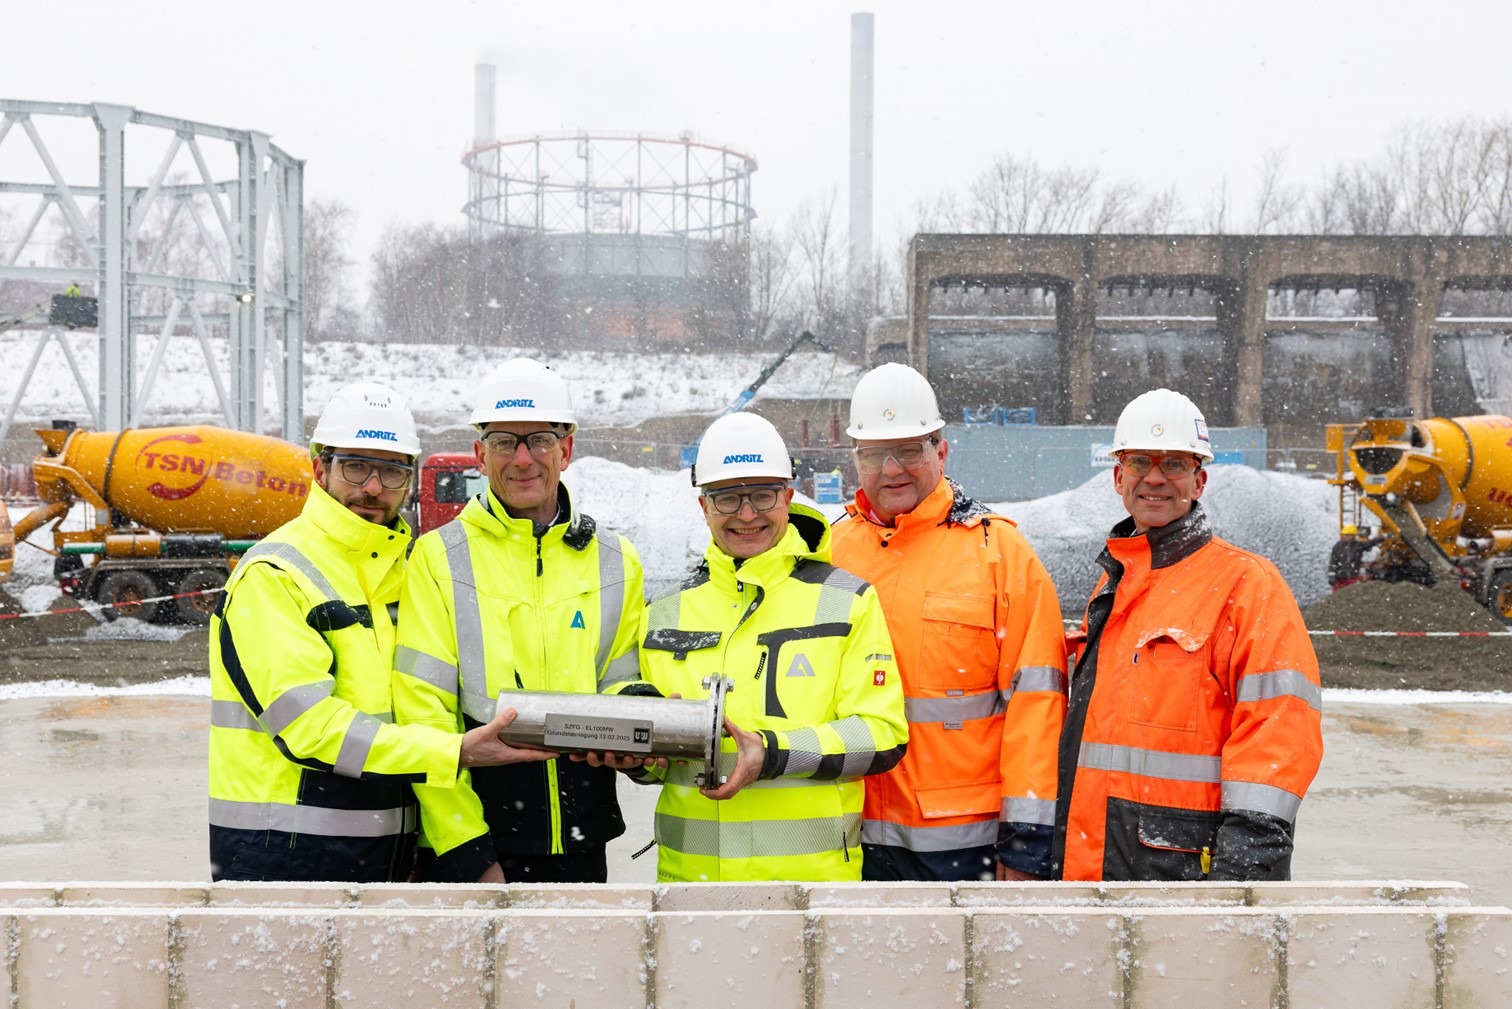
From left: Andrea Prevedello, Global Director Project Management of Green Hydrogen, at ANDRITZ; Walther Hartl, Project Manager of Electrolysis, at ANDRITZ; Sami Pelkonen, Executive Vice President of Green Hydrogen, at ANDRITZ; Gerd Baresch, Managing Director of the Technical Division, SZFG; Thorsten Hinrichs, Head of Pipeline Infrastructure, SZFG
Source: Andritz Group
“On February 12, 2025, the cornerstone was laid for one of the largest production plants for green hydrogen in the whole of Europe.
[Beginning in] 2026, the plant will generate around 9,000 tons of green hydrogen a year to be used for the production of carbon-reduced steel. This will mark the start of the industrial use of hydrogen in SALCOS®-Salzgitter low CO2 steelmaking. SALCOS® is aiming for virtually carbon-free steel production. The 100 MW electrolysis plant will be supplied on an EPC basis by the international technology company ANDRITZ, using the pressurized alkaline electrolysis technology of HydrogenPro.”
A new annealing and isolating line has been supplied to thyssenkrupp Steel for the production of high-grade NGO (non-grain-oriented electrical steel strip). This strip processing line comprises a precise heat treatment in which the structure of the cold-rolled strip is recrystallized during the annealing process, followed by the application of an insulating layer to ensure optimal electrical properties. This is particularly important for the materials used in motors and generators installed in electric vehicles.
The new processing line, supplied by the project partner, SMS Group, has an annual capacity of 200,000 tons and is designed to process electrical steel strip in widths of up is now in operation. SMS technology enables the production of electrical sheet for energy-efficient applications, for example electromobility. The technological core of the line is the combined heat treatment and coating process.
With this line, the modernization of thyssenkrupp‘s Bochum location is nearly complete, allowing the steel producer to better serve its clients in the automotive, energy, and other manufacturing sectors. The new plant will allow the manufacture of up to 0.2 mm thin electrical sheet with particularly homogeneous mechanical and magnetic properties, specially designed to meet the requirements of highly efficient motors used primarily in electric vehicles. The finishing line is scheduled to go on stream in 2026.
“This facility not only represents a huge step forward in our production capacities,” said Dr. Harald Espenhahn from thyssenkrupp Steel Europe, “it enables us to manufacture high-quality NGO steels that allow our customers to meet the changing demands of the market and to develop products with increased energy efficiency.”
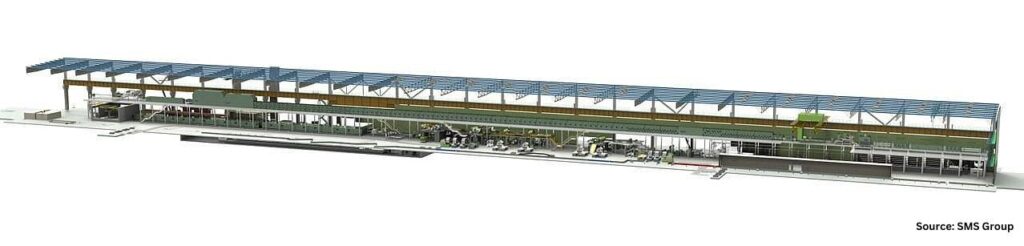
3D model of the new annealing and insulating line for the production of non-grain-oriented (NGO) steel at thyssenkrupp Steel Europe’s Bochum site
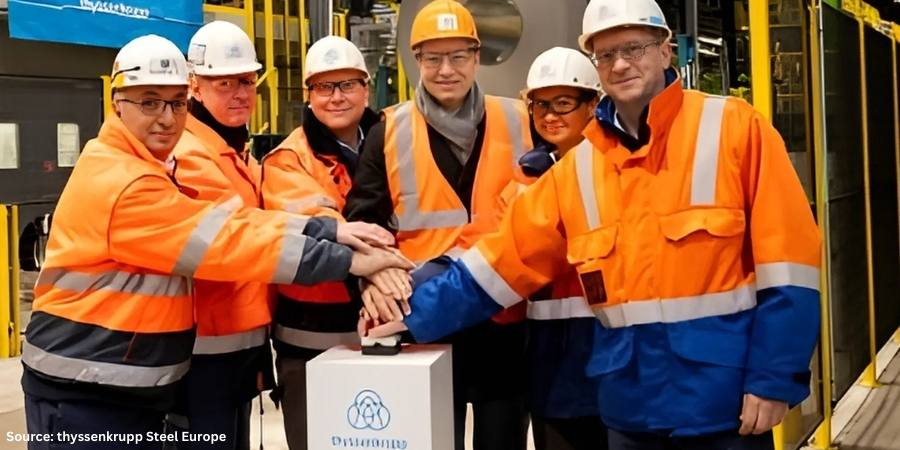
Main image: The team from thyssenkrupp Steel Europe and SMS Group preparing to start up the pioneering plant technology for the manufacture of high-grade electrical sheet / L to R: Engin Karakurt, Chairman of the Works Council of thyssenkrupp Steel in Bochum; Dr. Harald Espenhahn, Head of Technology and Environmental Management, thyssenkrupp Steel; Andy Rohe, Head of Downstream Operations, thyssenkrupp Steel; Thomas Eiskirch, Mayor of Bochum; Dr. Marie Jaroni, Chief Transformation Officer at thyssenkrupp Steel; Markus Kovac, Head of the Bochum Plant Area, thyssenkrupp Steel
Press releases are available in their original form here and here.
Aalberts N.V. has reached an agreement to acquire 100% of shares of Paulo Products Company (Paulo), expanding the company’s geographical footprint in the U.S. The acquisition will bolster the Dutch company’s capabilities to provide heat treating, brazing, and metal finishing operations for the North American automotive, aerospace, defense, and energy sectors.
Stéphane Simonetta CEO Aalberts N.V.
Pending regulatory approval, the management team of Paulo, which operates five heat treatment facilities in the USA and one in Mexico, will work with the management of Aalberts Surface Technologies in North America. The transaction is expected to be finalized in the second quarter of 2025 and generate an annual revenue of approximately USD 105 million with 522 employees.
“We are excited about the growth potential in the different end markets and are looking forward to welcoming Paulo’s employees to Aalberts,” said Stéphane Simonetta, CEO of Aalberts N.V. “This strategic acquisition will further enhance our proximity in North America and Mexico as per our ‘thrive 2030’ strategy. Together, our leadership position will enable us to serve our customers with short lead times, high quality and full-service capabilities.”
The press release is available in its original form here.
A North American manufacturer has bolstered its heat treatment capabilities for annealing steel parts after induction hardening. The two-zone belt conveyor furnace shipped to the facility ensures precise temperature control, energy efficiency, and compliance with AIAG specification CQI-9.
“The customer chose to enhance the operating efficiency of the oven with the E-Pack™ Energy Efficiency Package. Depending on utility rates, operating temperature, and weekly usage, customers may achieve significant annual energy savings with this upgrade,” said Tom Trueman, senior application engineer for Wisconsin Oven Corporation.
Tom Trueman Senior Applications Engineer Wisconsin Oven Corporation
Wisconsin Oven Corporation designed the conveyor furnace with the capacity to heat 2,400 pounds of steel per hour from 70° to 350°F with a maximum temperature rating of 500°F and the ability to anneal the components after induction hardening. The recirculation system features a top-down airflow design with a 32,000 CFM blower, with each of the two zones utilizing 16,000 CFM. The temperature for both zones is controlled by a Watlow F4T digital recorder/controller, which provides Ethernet communication capabilities and PID temperature control with adaptive tuning. As a factor in its CQI-9 compliance, a temperature uniformity survey was conducted, documenting uniformity of ±10°F at 350°F with verified part soak.
To maximize energy efficiency, the oven has been upgraded with an E-Pack™ Energy Efficiency Package, which includes 2” thicker insulation in the walls, floor, and roof, as well as variable frequency drives on the recirculation blowers.
The press release is available in its original form here.
A leading automotive manufacturer is updating its heat treating operations with Endothermic gas generators to enhance the carburizing process. The company, which produces engine parts that require high durability and wear resistance, is modernizing the facility’s aging, gas-heated generators with a more efficient, cost effective and sustainable solution.
Daniel Panny Head of Sales in Europe UPC-Marathon Source: UPC-Marathon
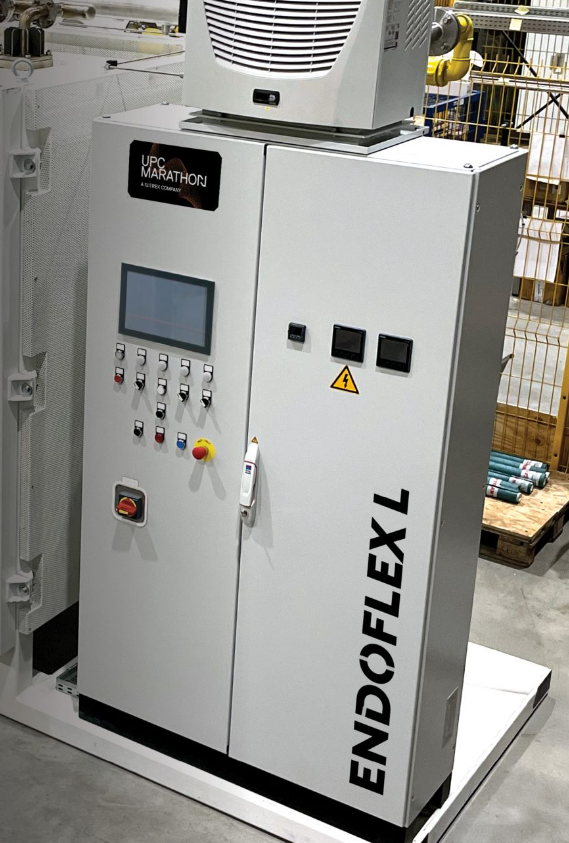
To support the company’s modernization initiatives, UPC-Marathon, a Nitrex company, is supplying five advanced, electrically heated EndoFlex L Endothermic gas generators designed specifically for carburizing, a heat treat process that hardens surfaces by introducing carbon into the material. The facility’s production had been caught in a bottleneck due to the age of the gas-heated generators, which were consuming excessive natural gas and contributing to CO₂ emissions.
UPC-Marathon’s EndoFlex L endothermic gas generator system Source: UPC-Marathon
“The partnership extends beyond this project,” said Daniel Panny, head of Sales Europe at UPC-Marathon. “Building on the success of past collaborations, where we upgraded legacy generators with the EndoInjector gas injection system to enhance and stabilize endothermic gas delivery, the customer selected the EndoFlex L for this major overhaul..”
Set for commissioning early next year, the Endothermic gas generators will play a key role in the manufacturer’s modernization strategy, supporting its long-term economic and environmental objectives.
The press release is available in its original form here.
Taiwan Hodaka Technology, an aerospace and automotive manufacturer, extends its market reach by adding an aluminum aging furnace to its heat treatment capabilities. The furnace, which is designed for aging using T77 technology, will allow the company to meet the highest safety and strength standards.
This is the first transaction between Taiwan Hodaka Technology, which is involved in the design and processing of parts made of aluminum alloys, and SECO/WARWICK. The furnace operates in the temperature range from 176° to 428°F (80° to 220°C) with a temperature uniformity in the last heating phase, of ±47.4°F (3°C) in accordance with the AMS 2750 standard.
“The solution supplied by SECO/WARWICK will allow us to enter a new market segment. We are a partner for many key players in the aviation industry. The T77 aluminum aging furnace will enable us to serve customer requirements even better. At the same time, the new technology will support our commitment to reducing our impact on the environment,” said Dr. Sam Chiang, vice president for R&D at Taiwan Hodaka Technology Co. Ltd.
Tomasz Kaczmarczyk, Sales Manager of the Aluminum Process and CAB Furnaces Teams, SECO/WARWICK
For heat treated alloys (2xxx, 6xxx and 7xxx series), the letter T and one or more digits are used after the alloy series symbol. The first digit is the most important, as it indicates the type of heat treatment applied to the alloy, while the remaining digits (if provided) indicate heat treatment variants or their modifications. The 7000 series of aluminum alloys have the highest strength of all other aluminum alloy series and are commonly used in aviation since they are held to the highest safety and strength standards.
“T7 denotes the process of solution heat treatment and artificial aging to an overaged state to obtain specific properties, e.g. increased corrosion resistance,” said Tomasz Kaczmarczyk, sales manager of the Aluminum Process and CAB Furnaces Team at SECO/WARWICK. “Sometimes, in addition to the digit denoting the standard heat treatment, an additional digit is used to denote modifications to the given treatment or stress relief procedures. For example, for 7xxx alloys, the symbol T77 denotes retrogression and re-aging. The use of this process improves the alloy’s corrosion resistance, which is so crucial in the production of aircraft parts. The applied technology will allow Taiwan Hodaka Technology to produce high-quality profiles used in the aviation industry in accordance with the AMS standard.”
Piotr Skarbiński Vice President of Aluminum and CAB Products Segment SECO/WARWICK
“The furnace on order equipped with electric heating will process 1500 kg of aluminum profiles with a maximum length of 5500 mm. This is a two-zone solution with a total heating power of 420 kW. The solution for aluminum aging, powered by electric heaters, eliminates the problem of CO2 emissions and is in line with the ecological trend increasingly common in heavy industry,” said Piotr Skarbiński, vice president of the CAB and aluminum products segment at SECO/WARWICK.
The furnace will be used at the company’s newly built plant in Taiwan.
The project partner was PEERENERGY, which offers thermal process consulting, project management, and equipment supply for the aerospace, military equipment, and semiconductor industries.
The press release is available in its original form here.
A heat treating company that processes stainless steel, titanium, and other specialty alloys is expanding its operations with a major investment in a larger facility, tripling its heat treatment and surface hardening capacity. The automotive and medical devices industries are among those the company serves at its Twinsburg, Ohio, location.
Thomas Sandholdt CEO Expanite, Inc
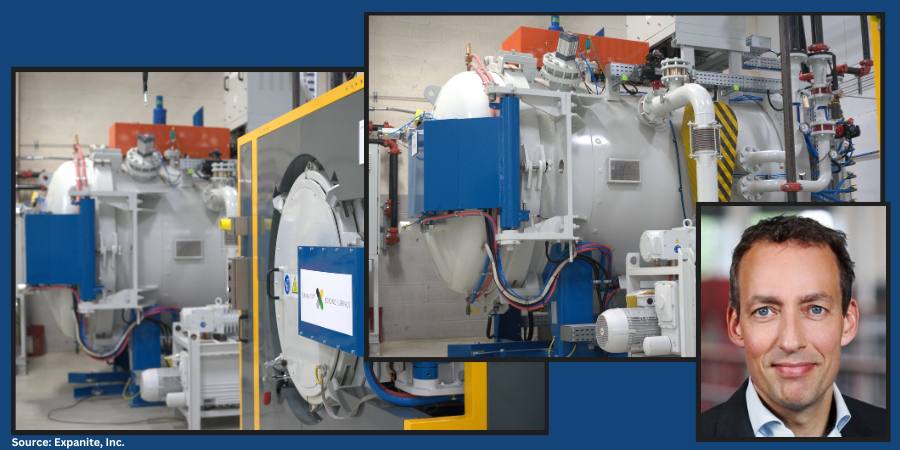
With the new equipment, Expanite Inc., a subsidiary of Expanite A/S, based in Denmark, will be able to meet the growing demand for advanced surface hardening and heat treatment solutions. The new furnaces, installed by SECO/WARWICK, have chamber sizes up to 24x24x36 inches and process larger and more complex components. This expansion will allow the company to meet its commitment to sustainability by offering greener alternatives to traditional technologies.
“Our investment is all about meeting the growing demands from our North American customers,” said Thomas Sandholdt, CEO of Expanite. “We’re now able to handle much larger volumes while maintaining the fast lead times and flexibility that our customers expect from Expanite.”
“Our expanded capabilities mean we can now offer our full range of Expanite technologies, including the processes for titanium, right here in the U.S.,” said Claus Løndal, country manager for Expanite North America. “This allows us to serve a wide range of customers while reducing lead times and costs.”
New furnaces installed as part of Expanite’s expansion at its Twinsburg, Ohio, location.
Besides the proprietary Expanite processes, standard vacuum heat treatment processes are offered, including hardening of tool steels (D2, A2, M2, H13, etc.), austenite annealing of stainless (304, 316, etc.), precipitation treatment of PH-steels (17-4PH, 13-8PH, etc.) and specialty treatment of alloys (Inconel 718, MU-metal etc.). The addition of vacuum heat treatment solutions extends the company’s capabilities, offering more solutions, and greater flexibility and ensuring clients receive hardening solutions tailored to their specific needs. In this expansion, Expanite is bringing its patented technology for hardening of titanium to North America.
A truck beam heat treat line with two large walking-beam furnaces is currently being installed for a leading Latin American auto structural component designer and manufacturer. The industry leader will use one furnace for austenitizing and the other for tempering. The truck beams are 13 in (33 cm) wide, 4.5 in (11.5 cm) high, and 49 ft (15 m) long, weighing at about 625 lb (285 kg). A closely controlled environment is necessary in order to induce the required change to the steel beams’ crystal structure.
The furnace line will be provided by NUTEC Bickley, their third such order for this auto industry manufacturer.
New furnace line from Nutec Bickley Source: Nutec Bickley
The austenitizing furnace is a continuous unit, capable of treating 60 beams (roughly equivalent to 17 tons of steel) per hour. It has an operating temperature of 1670°F (910°C), and a maximum temperature of 2010°F (1100°C). There are 10 automatic control zones, designed to promote temperature uniformity.
There are 29 high-velocity burners, sited above the load. These allow for low NOx emissions, featuring stable high excess air and excess fuel operation, direct spark ignition, integral air and gas meters, sturdy cast construction and flame rod ionization. The burner configuration creates gas recirculation and allows uniform heating of the load and better heat transfer to the product through radiation mechanisms and convection.
The furnace employs NUTEC Bickley’s IMPS™ combustion system for energy savings, enhanced process control, optimal kinetic energy utilization from burners, temperature uniformity without excess air, a high turndown ratio, and other key benefits.
The tempering furnace — capable of heat treating beams at a rate of 60 pieces per hour — has an operating temperature of 915°F (490°C) and a maximum temperature of 1110°F (600°C). There are six automatic control zones and the heating method for tempering is via air circulation with a vertical flow pattern, ceiling to floor with six centrifugal fans.
Both of these furnaces benefit from insulation based on the patented Jointless® ceramic fiber system that allows fast heating and cooling and reduces heat storage. Using MacroModules, this insulation is 8 in (20 cm) thick in the combustion zones. Thermal efficiency has also been guaranteed with a specifically design of the door frame and canopy for both access and exit doors. Both furnaces are fully NFPA 86 compliant.
The press release is available in its original form here.
FPM Heat Treating has announced the acquisition of a vacuum furnace, enhancing the company’s capabilities to serve the manufacturing community, especially in the automotive and aerospace sectors. The furnace will meet an increasing demand for a specialized family of parts.
Bob Ferry Vice President of Quality & Engineering FPM Heat Treating
The furnace, fully compliant with NFPA, NADCAP, AMS, CQI-9, and other critical industry standards, has been installed at FPM Heat Treating by Solar Manufacturing. With an operating temperature of up to 2400°F (1315.5°C) and a weight capacity of 5,000 pounds, the furnace processes at specialized heat treatment cycles critical for automotive components as well as precise specifications for applications within consumer products and the military/aerospace sectors.
“We are committed to meeting the growing demands of our clients in the manufacturing community,” said Bob Ferry, vice president of quality and engineering at FPM Heat Treating. “The new Solar furnace enhances our capabilities and enables us to maintain the highest standards of quality and efficiency in our operations.”
Main Image: Adam Jones, Midwest regional sales manager at Solar Manufacturing, viewing the vacuum furnace’s 48” x 48” x 72” deep insulated hot zone
The press release is available in its original form here.