Message from the Editor: It’s a Tool, Not a Magazine

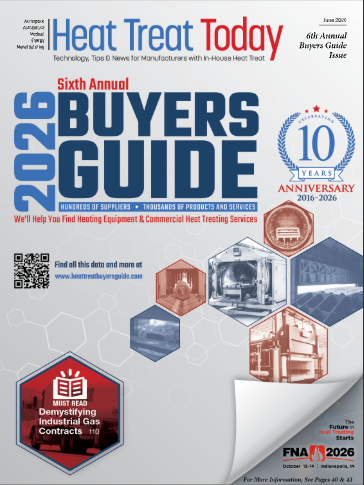
Heat Treat Today publishes twelve print magazines a year and included in each is a letter from the editor. This letter is from the June 2026 Sixth Annual Buyers Guide Issue print edition. In today’s letter, Bethany Leone, managing editor at Heat Treat Today, shares her insights on why a print directory still earns its place in an engineer’s toolkit.

The physical act of flipping pages, folding corners, and marking up listings creates a kind of accidental learning that a search bar can’t replicate. And the guide serves everyone differently — metallurgists, maintenance managers, and newcomers still learning the industry’s vocabulary all get something different out of it.


I’m a fold-the-spine-backwards kind of person. Chaotic annotate-at-an-angle kind of researcher. Audiobooks were designed to protect documents from people like me. But full immersion is sometimes the only way to really use information designed to help you learn or answer a question.

While the other issues in this magazine contain a slew of articles and stories to inspire and teach North American heat treaters about their equipment and processes, this issue is the industry directory. Its process-driven structure is designed to make the directory a practical next step for engineers and decision-makers evaluating their options.

A central use is finding out “who’s who” even before you need to call an equipment supplier or process provider. This can easily be done online at www.heattreatbuyersguide.com too, but in print, comparison becomes physical. Your eyes move faster than tabs open. A folded page, a pen mark, and a highlighted listing become part of the evaluation process itself.

Additionally, it is a tool to learn what’s outside your primary area of expertise. Search bars are excellent for finding answers to questions you already know to ask. Directories are different. They expose adjacent technologies, unfamiliar process names, and companies you may not have encountered otherwise. This accidental learning is hard to replicate online.

For an in-house heat treat operation mainly focused on annealing processes for steel grades but looking to enhance hardness profiles, Heat Treat Buyers Guide introduces you to the range of equipment, processes, and suppliers involved. Mark these, circle the companies, or leave a half page fold for your future self when it comes time to make a process improvement decision. While some sections may not matter today, a new alloy, distortion issue, or throughput challenge makes those folded corners and handwritten notes the starting point of the next improvement project.

The wide reach of this tool is critical for heat treating, a process dependent on an interconnected network of specialties. At my last trade show, an engineer who had transitioned from aerospace into furnace manufacturing told me, “Surprisingly complex! I had not anticipated all that goes into engineering a furnace. It is very different than aerospace, and not at all simple.” Every process step has its own expertise, from fixturing, atmosphere control, and quenching to testing, software, and beyond.

The table of contents provides the main equipment categories with color tabs that replicate on the pages of the corresponding sections. Be sure to check out the final few tabs which indicate listings for commercial heat treaters and a few leading consultants in the heat treat industry closer to the end.

The most representative categories to page through include:

  • Aluminum Heat Treating
  • Annealing
  • Hardening, Quench & Temper
  • Vacuum Heat Treating
  • Induction Hardening
  • Solution Treating & Precipitation Hardening

In line with new heat treat technology developments are increasingly represented categories around vacuum:

  • Vacuum Furnaces
  • Vacuum Carburizing
  • High-Pressure Gas Quench
  • Vacuum Hardening
  • Vacuum Brazing

The guide serves different purposes depending on who opens it. A metallurgist may use it to identify process capabilities. A maintenance manager may use it to source replacement systems or atmosphere components. A young engineer may simply use it to learn the vocabulary of the industry.

Whether you keep yours tidy and pages well-thumbed or take the closest sharpie to mark your next hit list, use this directory to better understand your options within the North American heat treat industry.


Bethany Leone
Managing Editor
Heat Treat Today
Contact: Bethany Leone at bethany@heattreattoday.com

Message from the Editor: It’s a Tool, Not a Magazine Read More »
Vacuum Heat Treat Capacity Grows in Northeast

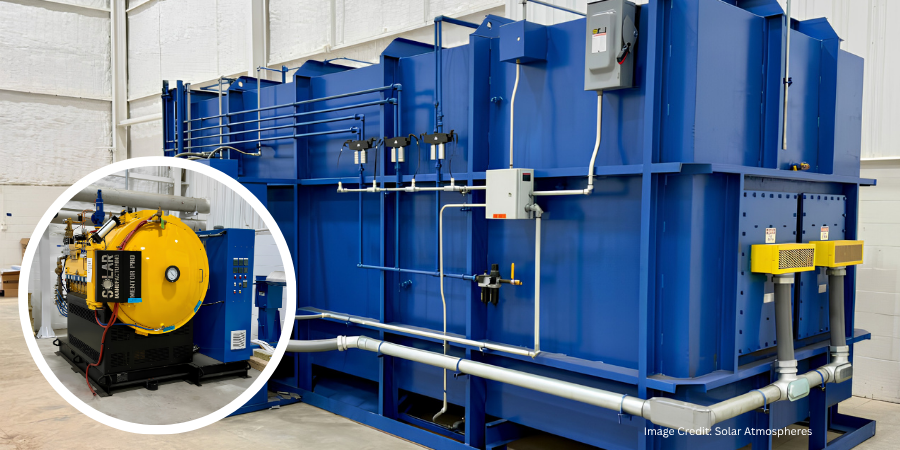
Solar Atmospheres, a commercial heat treater, is preparing to expand vacuum heat treating capacity in the Northeastern United States as construction progresses on its newest facility in Berlin, Connecticut. The 28,000-square-foot operation remains on schedule to begin serving clients in the fourth quarter of 2026.

Image Credit: Solar Atmospheres

Construction and refurbishment continue at the future home of Solar Atmospheres Connecticut, where several vacuum furnaces have already been installed. Office areas are nearing completion, while work continues on the facility’s piping, electrical systems, and supporting infrastructure.

Located in the Spruce Brook Industrial Park, the new facility is expected to expand the company’s vacuum heat treating capabilities throughout the Northeast when it opens later this year.

Press release is available in its original form here.
Related Reading: Solar Atmospheres acquired the 28,000-square-foot Connecticut facility in late 2025, laying the groundwork for the company’s Northeast expansion. Click here to read more.

Vacuum Heat Treat Capacity Grows in Northeast Read More »

Ask the Heat Treat Doctor®: What are the Heat Tint Colors for Stainless Steel and When Do They Form?

Ask The Heat Treat Doctor® has returned to bring sage advice to Heat Treat Today readers and to answer your questions about heat treating, brazing, sintering, and other types of thermal treatments as well as questions on metallurgy, equipment, and process-related issues. In this installment, Dan Herring explores the heat tint colors that form on stainless steel during heating and cooling — how the surface oxide layer thickens and shifts through straw, bronze, peacock, and blue hues at specific temperatures and explains the factors, such as chromium content, oxygen levels, time, and surface roughness, that influence how and when these colors appear.

This informative piece was first released in Heat Treat Today’s June 2026 Sixth Annual Buyers Guide Issue print edition.


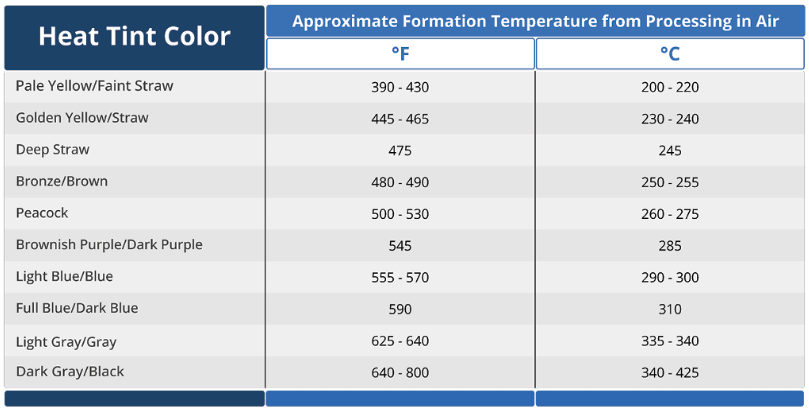
Most heat treaters, engineers, and clients are familiar with temper colors on steels (Herring 2014, ASM International 1991) and often assume that these color tints (hues) are the same for stainless steels (Table A). However, there are subtle changes that are worth noting. Let’s learn more.

Table A. Heat Tint Color Chart for Stainless Steels | Source: The HERRING GROUP, Inc.

The Science Behind Heat Tint Colors

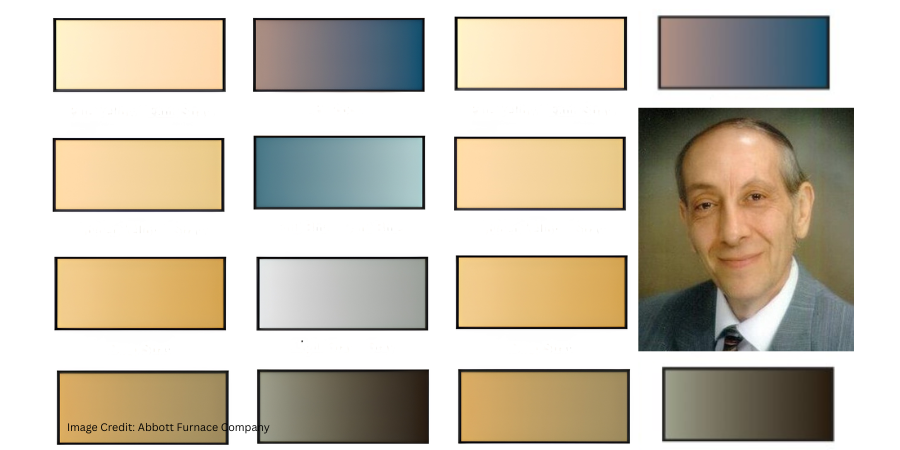
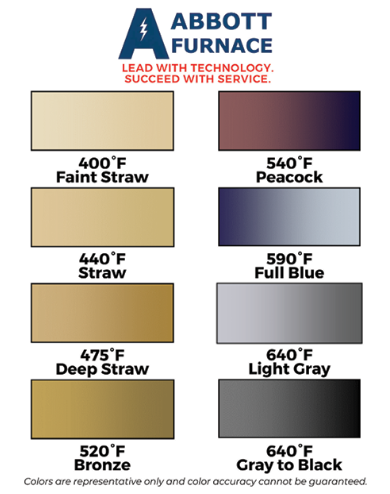
Figure 1. Examples of color tints | Image Credit: Abbott Furnace Company

When stainless steel is exposed to an air atmosphere, or a high dew point moisture-laden atmosphere during heating or cooling, its surface changes color; that is, a thin oxide layer forms on the surface (Figure 1). This heat tint color (aka temper color) is caused by a progressive thickening of the surface oxide layer.

As most of us know, an invisible (aka passive) layer occurs naturally on stainless steels. It is extremely thin, typically in the order of 1 to 3 nanometers (3.93 x 10⁻⁸ to 1.18 x 10⁻⁷ inches) thick.

Upon exposure to air during heating or holding at temperature, this oxide layer grows in thickness. When it is approximately 20–30 nanometers (7.87 x 10⁻⁷ inches) thick, it starts to become visible to the human eye as a light-yellow or straw yellow color tint.

As the oxide layer becomes even thicker it transitions from almost transparent to a variety of different colors (e.g., bronze, peacock, blue).

As the oxide layer thickness increases from 20 nm to roughly 50–100 nm (1.97 x 10⁻⁶ to 3.94 x 10⁻⁶ inches), the colors deepen changing to a golden yellow, to a deep straw, to a bronze or golden brown, to peacock (a purplish-blue), to full blue, then light gray, and finally dark gray.

Above 100 nm (3.94 x 10⁻⁶ inches,) up to approximately 850 nm (3.35 x 10⁻⁵ inches) the tint transitions from dark blue/gray to black.

Such shallow oxides are known to enhance corrosion resistance on various stainless steel grades.

Factors Influencing Color Change

Several factors influence the type of oxide that forms on the surface, its adhesion to the surface, and how quickly the thickness of the oxide will grow (BSSA).

Chromium

From a purely material standpoint, the single most important element is the chromium (Cr) content of the stainless steel. To be classified as a stainless steel, it must contain a minimum of 10.5–11% Cr. The higher the chromium content, not only is the alloy more heat resistant, but the heat tint color formation mechanism is retarded.

Oxygen Content

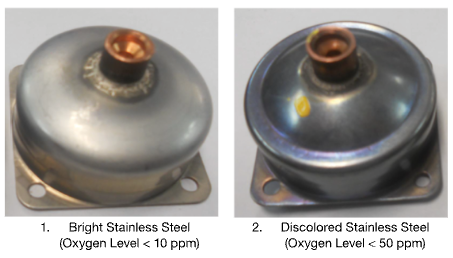
Figure 2. Bright and discolored stainless steel parts run in a continuous brazing furnace. The discolored part was caused by room air infiltrating into the cooling zone at high levels (> 50 ppm) from the exit of the furnace. | Image Credit: The HERRING GROUP, Inc.

Another factor that influences the rate of oxide formation and the thickness of the oxide is the oxygen content of the atmosphere (Figure 2). Air is approximately 21% oxygen. Nitrogen, however, will typically have between 0.001%–1% oxygen depending on its source, while argon typically has between 0.0005%–1% oxygen. By contrast, water vapor contains around 89% oxygen.

As anyone who has run stainless steel in vacuum furnaces knows, stainless parts can be discolored due to such factors as an air leak during heating or cooling, a pinhole water leak in a heat exchanger which opens during cooling in one temperature range and close again at a lower temperature, or air infiltration in the backfill gas supply.

Time

Time plays a factor as well. The longer the exposure time, the deeper the heat tint color.

Surface Roughness

Finally, surface roughness influences both the rate of oxidation and the heat tint color formation. Rougher surfaces tend to oxidize at a higher rate and with all other factors remaining the same, deeper colors are produced.

Final Thoughts

Knowing the color tints that may form on the surface of stainless steel is invaluable in helping the heat treater explain this phenomenon to their clients and/or troubleshoot their equipment and processes in an attempt to minimize or eliminate undesirable surface tints on the stainless steel parts that they run.

References

  1. Herring, Daniel H. 2014. Atmosphere Heat Treatment, Volume I (Section 5.8). BNP Media Group II.
  2. ASM International. 1991. ASM Handbook, Volume 4: Heat Treating. p. 960.
  3. British Stainless Steel Association (BSSA). bssa.org.uk.

About the Author

Dan Herring
“The Heat Treat Doctor”
The HERRING GROUP, Inc.

Dan Herring has been in the industry for over 50 years and has gained vast experience in fields that include materials science, engineering, metallurgy, new product research, and many other areas. He is the author of six books and over 700 technical articles.

For more information: Contact Dan at dherring@heat-treat-doctor.com.

For more information about Dan’s books: see his page at the Heat Treat Store.


Ask the Heat Treat Doctor®: What are the Heat Tint Colors for Stainless Steel and When Do They Form? Read More »

Stainless Steel Producer Upgrades Ladle Furnace Capacity

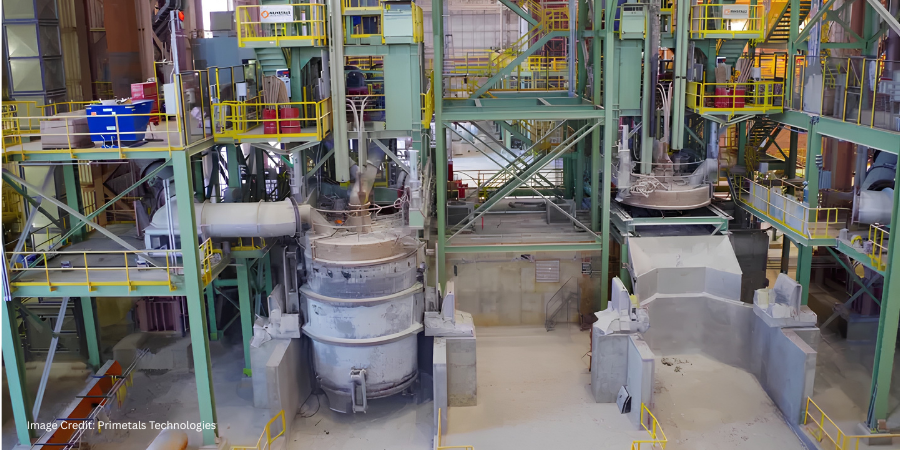
Outokumpu Stainless USA will upgrade its secondary metallurgy operations with a new 180-ton twin ladle furnace at its Calvert, Alabama, facility. The project will add electrical heating capacity following argon oxygen decarburization processing, improving operational flexibility and supporting stainless steel production.

Outokumpu has contracted Primetals Technologies to supply the furnace, which will replace a ladle treatment stand installed in 2012. Startup is scheduled for March 2028.

At the Calvert facility, Outokumpu melts up to 100% stainless steel scrap in an electric arc furnace before processing the material in an oxygen decarburization (AOD) converter. Upgrading one of the plant’s two ladle treatment stands will add electrical heating capacity after the converter and provide greater flexibility in the AOD process.

The project will use the plant’s existing layout and foundation. Primetals Technologies’ scope includes a water-cooled ladle cover integrated with a swing gantry system, an electrode conducting arm with a high-current system, automated argon lancing equipment, a hydraulic system, a power solution, Level 1 automation, and the supplier’s Melt Expert electrode control system.

The Melt Expert system provides dynamic control of the melting process to improve process stability, furnace productivity, and energy consumption. The upgrade is also expected to reduce the plant’s carbon footprint.

Press release is available in its original form here.

Stainless Steel Producer Upgrades Ladle Furnace Capacity Read More »

AI & Property Rights

Heat Treat Today publishes twelve print magazines annually and included in each is a letter from the publisher, Doug Glenn. This letter from the June 2026 Sixth Annual Buyers Guide Issue print edition examines the property-rights tensions AI raises for publishers.

Feel free to contact Doug at doug@heattreattoday.com if you have a question or comment. 


In early May of this year, leaders from the North American magazine publishing industry met in Chicago for a day and a half of industry talk and “saw sharpening.” Publishers of notable magazines like Fast Company, Inc., and Farm Journal attended as did Heat Treat Today. Two main topics dominated the event: events and artificial intelligence (AI). Conspicuously absent from the discussion was any emphasis on digital publishing (see last month’s Publisher’s Page for more on the contraction of digital media growth).

The conversations about AI were interesting but non-conclusive. In a nutshell, no one, not even the publishing “experts”, had any idea where AI was headed and what impact it would have on the publishing industry. Doomsday and utopian speculations abounded side-by-side. Either could be right; no one knows.

Private Property and Permission to Use

There are real and unique issues with AI and the publishing industry. Imagine what would happen to your business if every time you produced a product, an unrelated third party would access all the details of your products and make them publicly known to whoever wants to know without getting approval from you. And, of course, you would get no compensation for all the information accessed and disseminated by this third party. All your engineering drawings, vendor lists and purchasing specs, your proprietary designs, and perspectives would all be laid bare for unfettered, uncompensated use by an unrelated third party. I’m guessing you would scream “foul” and would do what you could to protect your property from unauthorized use.

Fortunately, for many of you, your product details are not splashed openly in excruciating detail on your website. For publishers, however, websites are one of our main distribution channels (albeit secondary to our print editions). For publishers, editorial content is our product, and by and large, it is available for public consumption, but not to help others make money without prior permission.

The issue seems to be one of private property and the use of that property without prior permission. When a magazine publishes an article, it is the property of the magazine and cannot be legally reproduced in part or in its entirety without prior written approval from the publishing company. As it currently stands, those wishing to access the content can have free access to it (unless it’s behind a paywall or registration wall), but they must come to the publisher’s website, which is of financial benefit to the publisher. If the public can get access to the publisher’s content without coming to their website, the publisher loses the financial benefit of traffic to their website. This is a real and tangible financial loss and is the result of someone accessing the content without due compensation to the publisher.

It is a unique situation that publishers are facing…thankfully for you! AI companies might object by saying that they give attribution to the sources of their findings and are therefore allowed to use the content. Citations help, but providing a footnote to the source of an AI answer is similar to a pawn shop listing the location of where they stole an item — it’s still the use of private property without permission.

It’s safe to say that legal action is inevitable. I fully anticipate that the publishing industry will do something to protect its product and its private property. Some will say that it is futile, like King Cnut the Great trying to hold back the tide. Could be, but it will be interesting to watch and see what effect AI will have on the publishing industry. As we’re watching that play out, Heat Treat Today will continue to do what we do — make people happier and help them make better decisions by keeping them well informed.

Doug Glenn
Publisher
Heat Treat Today
For more information: Contact Doug at
doug@heattreattoday.com

AI & Property Rights Read More »

Thermal Processing Investment Adds HIP Capacity

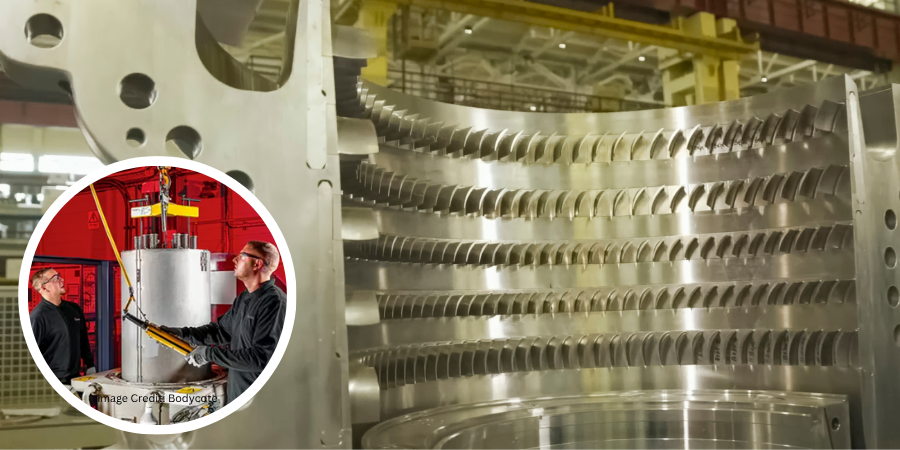
Bodycote, a global commercial heat treater serving manufacturers across North America and Europe, is expanding its hot isostatic pressing (HIP) and thermal processing capabilities to support growing demand from the aerospace and defense sectors. The expansion adds HIP equipment and powder metallurgy capabilities designed to increase processing capacity for critical, high-performance components.

More than €20 million is being invested at Bodycote’s Magny-Cours facility in France, one of the company’s European hubs for hot isostatic pressing. HIP combines high temperature with isostatic gas pressure to eliminate internal porosity and improve the mechanical properties of critical metal components.

The investment includes the installation of multiple large-format HIP vessels designed to increase available processing volume, allowing larger components to be treated while improving capability and energy efficiency. Once fully operational by the end of 2026, the expanded installation will provide Magny-Cours with multiple HIP units to support increased production across the aerospace, industrial gas turbine (IGT), and defense sectors. The expansion is also expected to create additional employment opportunities at the site.

Bodycote has also expanded HIP capacity at its Haag-Winden facility in Germany with the addition of two HIP vessels. The site specializes in both hot isostatic pressing and the company’s Powdermet product fabrication process, enabling near-net-shape components ot be manufactured and HIP processed on-site while also providing standalone HIP services for client-supplied parts.

Heidi McNary
President, Global Aerospace, Defence and Energy
Bodycote

“The new and upgraded sites will help deliver increased capacity for thermal processing at a time when demand from aerospace and defense [clients] is growing at a double-digit annual rate,” said Heidi McNary, president of Global Aerospace, Defence and Energy at Bodycote. The company plans to discuss the expanded capabilities with clients during the Farnborough International Airshow, scheduled for July 20–24.

Press release is available in its original form here.

Thermal Processing Investment Adds HIP Capacity Read More »

US Department of War Pauses CMMC Phase II Rollout

Defense suppliers gain additional time as the U.S. Department of War (formerly the U.S. Department of Defense) reviews its Cybersecurity Maturity Model Certification (CMMC) program. However, Heather Falcone, founder and principal of Falcone Consulting, LLC and Heat Treat Radio host and producer, cautions manufacturers with in-house heat treating and commercial heat treaters against interpreting the pause as a relaxation of their cybersecurity obligations.

What the Announcement Revealed

The U.S. Department of War has suspended the transition to Cybersecurity Maturity Model Certification (CMMC) Phase II requirements while it conducts a comprehensive review of the program.

The suspension pauses pending and future Phase II implementation milestones across Department of War solicitations and contracts. However, Phase I self-assessment requirements remain in effect, and contractors must continue protecting covered defense information under existing contractual requirements, including DFARS clause 252.204-7012. During the 60-day review period, cybersecurity compliance will continue through NIST SP 800-171 Revision 2 self-assessments and select government-led assessments.

Kristin A. Davies
Chief Information Officer
U.S. Department of War

The review is intended to reduce compliance burdens on small, medium-sized, and non-traditional defense suppliers while maintaining cybersecurity protections. A newly established CMMC Reform Task Force will evaluate industry feedback and submit recommendations within 60 days.

“In support of Secretary Pete Hegseth’s directive to reduce compliance barriers for small and medium-sized businesses, we are suspending the CMMC Phase II requirements and initiating a 60-day study of the future of this program,” said Kristin A. Davies, chief information officer for the Department of War. “Robust cybersecurity and operational resilience remain critical to protecting American innovation and supporting warfighter readiness. We believe the Defense Industrial Base (DIB) can achieve both, while we reduce unnecessary government red tape.”

What This Means for Heat Treaters: An Industry Expert Weighs In

While the announcement delays the rollout of Phase II certification requirements, Falcone said manufacturers should avoid assuming that cybersecurity preparation can be put on hold.

Heather Falcone
Founder and Principal of Falcone Consulting LLC / Host and Producer of Heat Treat Radio

“The most dangerous interpretation of this announcement would be that cybersecurity preparation can stop,” Falcone said. “Phase II has been suspended, but manufacturers remain responsible for protecting defense information and meeting their existing contractual requirements. Companies should use this period to confirm their scope, close material NIST 800-171 gaps, and strengthen the evidence supporting their compliance.”

Falcone described the announcement as a meaningful reprieve for many small and midsized captive and commercial heat treaters that supply the defense industry. Many companies, she noted, have been preparing for significant compliance costs while lacking dedicated cybersecurity staff or access to enough certified assessors.

“A rushed implementation could consume capital that would otherwise support equipment upgrades, workforce development, capacity expansion, and other investments the defense supply chain needs,” she said.

She added that the review provides an opportunity to address longstanding concerns over how controlled unclassified information (CUI) is identified, marked, and shared throughout the defense supply chain, as well as the availability of qualified assessors and the affordability of compliance for small manufacturers.

“This suspension acknowledges the capacity and cost problems small manufacturers have been raising for years,” she said. “A successful CMMC reset should preserve a serious cybersecurity baseline while giving small defense suppliers requirements they can clearly understand, afford, and execute.”

Although the November implementation deadline has been suspended, Falcone recommends that heat treaters continue strengthening their cybersecurity programs while reviewing spending decisions driven solely by the former deadline. She also encourages companies to consult with prime contractors before changing any contract-specific commitments.

Learn More About CMMC

For readers looking for additional background on cybersecurity requirements for defense suppliers:

Press release is available in its original form here.

US Department of War Pauses CMMC Phase II Rollout Read More »

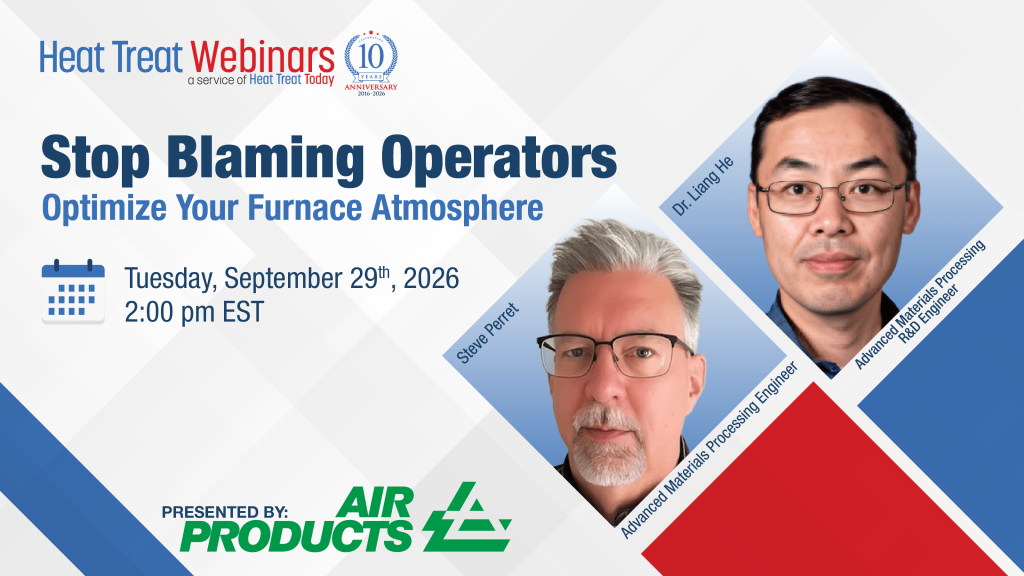
Stop Blaming Operators: Optimize Your Furnace Atmosphere

Tuesday, September 29, 2026

2:00 PM EST

Heat treating success depends on more than time and temperature—furnace atmosphere control is the missing lever. In this webinar, we break down the critical role furnace atmosphere plays, and how poor control leads to oxidation, decarb, sooting, and inconsistent mechanical properties. You’ll see real-world examples of how optimized atmospheres reduce scrap, improve repeatability, and increase throughput. We’ll also show how you can validate changes before implementation using advanced lab testing—so you can improve quality, lower costs, and get more out of your furnace.

Speakers:

Dr. Liang He, Advanced Materials Processing R&D Engineer
Liang Hi, Advanced Material Processing R&D Engineer, is a member of the Advanced Technology team. He develops gas application technologies for the metals processing industry. His primary research includes simulation software development on predicting carburizing / carbonitriding processes, using cryogenic coolant for quenching, and Smart Technologies for furnace operations. Liang received his BS in mechanical engineering and PhD in materials science and engineering.


Steve Perret, Advanced Materials Processing Engineer
Steve Perret is a member of our Commercial Technology team with over 40 years of experience in metals processing. He brings proven value in helping customers strengthen quality assurance and traceability, leveraging deep expertise in CQI-9 standards to prevent costly defects and support root cause investigations. Steve specializes in smart manufacturing and digital integration, with a long track record of implementing Manufacturing Execution Systems (MES) to connect equipment, optimize processes, and improve operational visibility.


Stop Blaming Operators: Optimize Your Furnace Atmosphere Read More »

Steelmaker to Double Rebar Production Capacity

Hybar LLC has secured financing to support construction of a second electric rebar mini mill, a project that will expand domestic steelmaking capacity through electric arc furnace technology. The additional mill will increase reinforcing steel production for the U.S. construction sector.

The company announced it has secured approximately $1.1 billion in financing to support the expansion, which will be built adjacent to the company’s existing facility in Osceola, Arkansas. Upon completion, the second mill is expected to double the company’s annual reinforcing steel production capacity to approximately 1.3 million tons.

SMS group supplied the company’s electric arc furnace, continuous caster, and rolling mill for the existing facility. Now, SMS group has been commissioned to supply the technology and equipment for the expansion mill. Construction is expected to be completed in about 24 months.

Hybar’s rebar is being used in data center projects, medical campus expansions, the energy infrastructure buildout, and the continued repair and upgrading of roads, bridges, and tunnels. Hybar plans to continue penetrating these markets with the expansion mill.

Press release is available in its original form here.

Steelmaker to Double Rebar Production Capacity Read More »

MTI Member Profile: Metal Treaters, Inc.

In the heart of Minnesota’s Twin Cities, a third-generation heat treating company continues to shape the backbone of manufacturing with precision and consistency. Established in 1948, Metal Treaters, Inc. began with a single Ipsen vacuum furnace used to treat door hinges for ovens and furnaces. From those early days, it has grown into a trusted partner for industries requiring meticulous control over metallurgical properties throughout the heat treating process.

The company expanded significantly in the 1970s when the second generation broadened its capabilities to include carburizing, induction hardening, and neutral hardening. That phase of growth laid the groundwork for today’s broader service offerings. Now under the guidance of its third generation, the focus is on integrating advanced technologies, enhancing efficiencies, and staying ahead of evolving compliance standards.

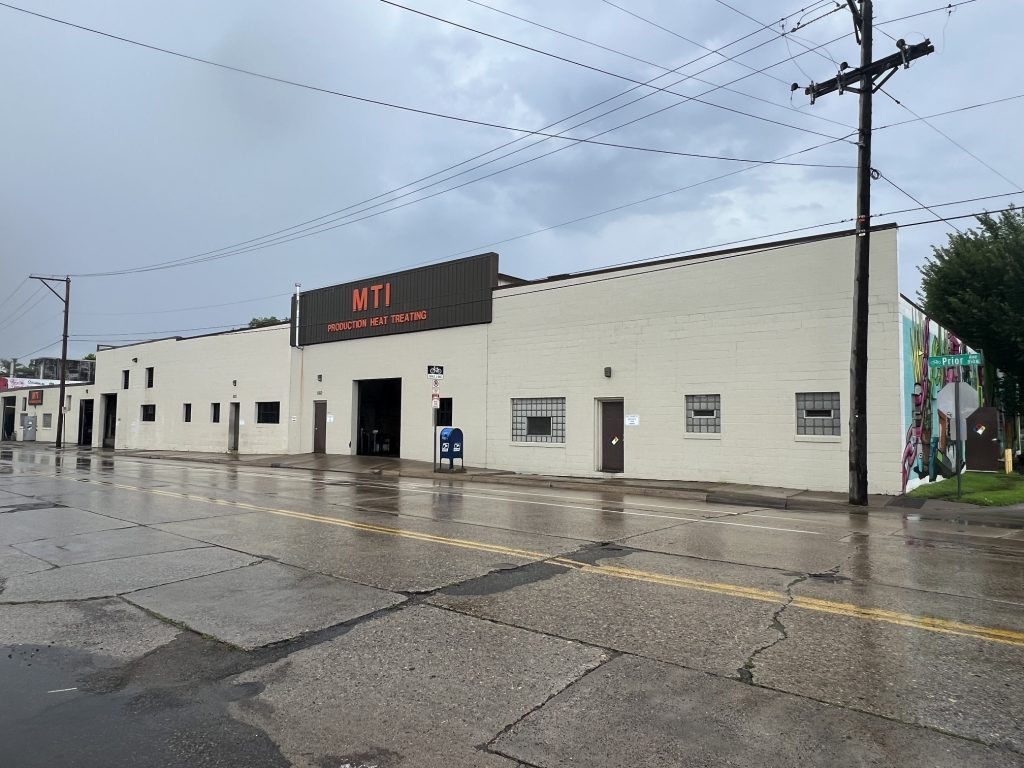
Metal Treaters, Inc. production, induction, shipping, and receiving side of facility | Image Credit: Metal Treaters, Inc.

Metal Treaters’ clients span the aerospace, defense, agricultural, construction, and medical sectors. A hallmark of the operation remains its vacuum heat treating expertise — a specialty dating back to its origin. Tool steels like A-2, D-2, and S-7, along with various stainless steels, are treated daily. Additional services include gas carburizing, carbonitriding, induction hardening and tempering, and cryogenic treatment.

What distinguishes this heat treater is its comprehensive internal control. Pyrometry is performed to AMS2750 standards, ensuring furnace accuracy and consistency. Metal Treaters also fabricates custom fixtures, racks, and induction coils, which allows them to tailor solutions, reduce job costs, and maintain quick turnaround times. These capabilities are especially valuable for manufacturers without in-house heat treating resources or those working with highly specialized components.

The facility operates eight furnaces, including four vacuum furnaces and four carburizing furnaces. They also utilize twenty-five tempering ovens, nine induction stations, seventeen hardness testers, and two deep freezers. All work is processed through batch ovens, which are optimized for flexibility and precision rather than oversized loads. With jobs that run in parallel and an established logistics network, including four daily route trucks serving the Twin Cities, the operation is built for both responsiveness and repeatability.

Growth has never depended on traditional advertising. Instead, the business has earned new work through word-of-mouth referrals and discussions at trade shows. This approach has attracted a wide range of challenging and high-profile jobs, from components used in space exploration and defense to tooling for medical and construction applications. Each project is approached with the same attention to detail, regardless of size or industry.

Looking ahead, the company aims to expand its use of automation in induction heat treating while continuing to meet the most rigorous technical standards. Plans also include maintaining a workplace culture that emphasizes collaboration, accountability, and long-term client relationships.

Through decades of change, Metal Treaters has remained grounded in technical excellence and responsive service. While tools, materials, and specifications have evolved, the guiding principles behind each treated part have stayed the same: precision, reliability, and craftsmanship.

For more information:

Metal Treaters, Inc.

859 Prior Avenue
St. Paul, Minnesota 55104

joannea@metaltreaters.com
metaltreaters.com

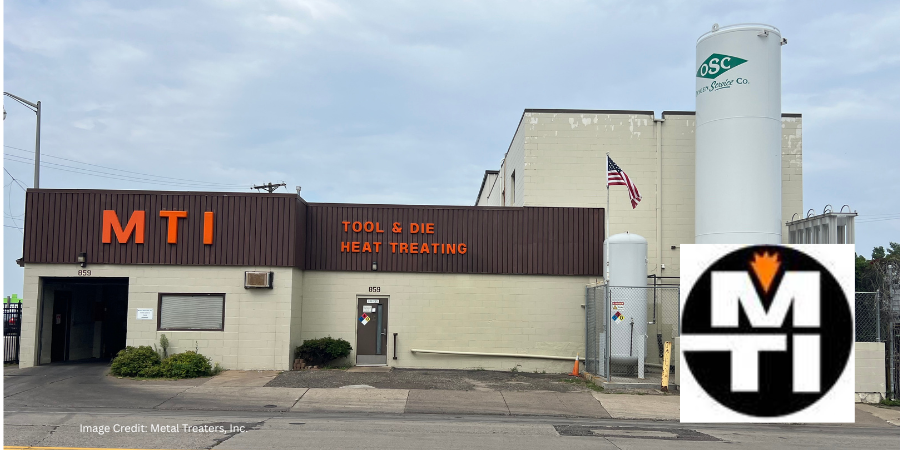
Main image: Metal Treaters, Inc. vacuum and office side of facility | Image Credit: Metal Treaters, Inc.

MTI Member Profile: Metal Treaters, Inc. Read More »